
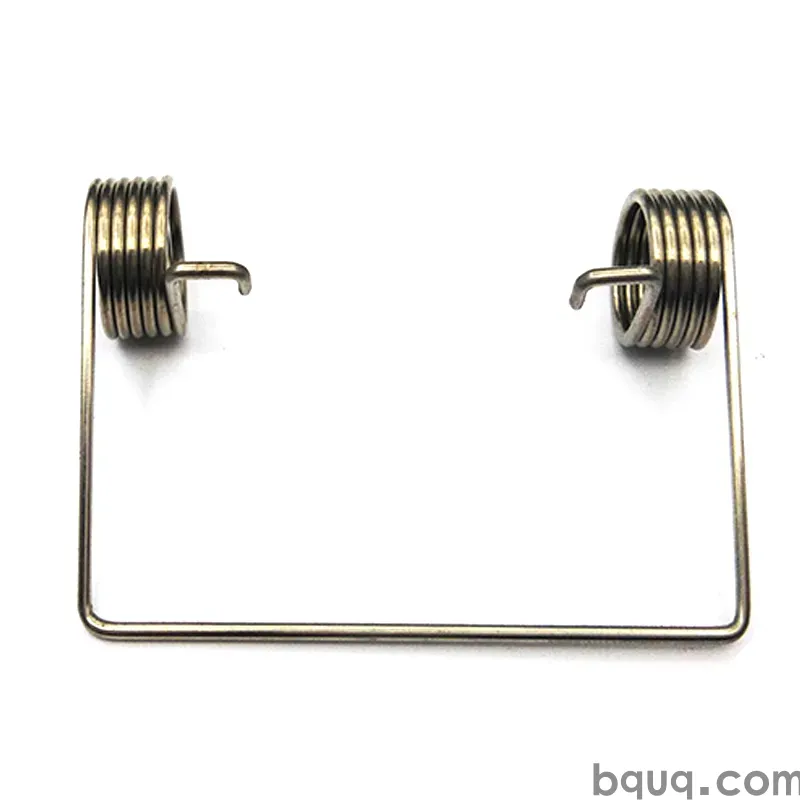
Overload and Yielding: When a Spring Stops Springing
Short answer: A spring stops springing when its internal stress exceeds the material's yield strength. The wire takes a permanent set, free length shortens, and load at a given height drops — often by 5–20% after a single severe overload. For music wire and 302 stainless, keep design stress under roughly 40–45% of tensile strength for static duty and 30–35% for cyclic duty. If you exceed that, expect set, fatigue, or fracture. BQUQ machines and winds springs to ±0.005 mm on CNC axes in one Dongguan ISO9001 factory, with quotes back in 12 working hours.
What Actually Happens Inside a Spring Under Load
A helical spring is a torsion bar rolled into a coil. When you compress it, the wire doesn't bend along its length — it twists. That torsional shear stress is what stores energy, and it's what eventually destroys the spring if you push too far.
Three things happen in sequence as load rises:
1. Elastic region. Stress stays proportional to strain. Remove the load, the spring returns to its exact free length. This is the only region you want to design in.
2. Yield point. Stress crosses the material's torsional yield strength. Some crystal planes slip permanently. Remove the load and the spring comes back shorter than it started.
3. Plastic collapse or fracture. At higher stress the spring takes a large permanent set, coils bind, or the wire cracks — usually at the inside of the coil where stress concentrates.
The first two are the ones that quietly ruin assemblies. A spring that has yielded still looks fine. It just doesn't push as hard.
Why "Set" Is the Real Failure Mode
Permanent set is the measurable symptom of yielding. You see it as:
- Free length shorter than drawing
- Load at installed height lower than specified
- Solid height reached earlier than expected
For a typical cold-wound compression spring, a single overload to 60% of tensile strength can produce 2–8% loss of free length. Push to 70% and you can lose 10–20%, plus a visible lean in the coil. That's the point where the spring "stops springing" in any useful sense.
How Do You Know a Spring Has Yielded?
Field symptoms are consistent across industries:
| Symptom | What it usually means | Quick check |
|---|---|---|
| Free length shorter than spec | Permanent set from overload | Measure unloaded length vs. drawing |
| Load at height low by >5% | Partial yielding or stress relaxation | Load cell test at installed height |
| Spring bottoms out early | Set + reduced travel | Measure solid height |
| Visible lean or uneven pitch | Localized plastic deformation | Visual + pitch gauge |
| Cracks at coil I.D. | Fatigue after yield, or hydrogen embrittlement | Dye penetrant or magnaflux |
| Rattles in assembly | Preload lost after set | Compare to first-article load |
If more than one of these shows up on a batch, the design stress is too high for the duty cycle — not the wire supplier's fault.
The Stress Limits That Decide Whether a Spring Survives
Every spring material has a torsional yield strength, typically 45–60% of ultimate tensile strength for spring steels. Design practice keeps working stress well below that.
| Material | Typical tensile (MPa) | Static design stress (% UTS) | Cyclic design stress (% UTS) | Notes |
|---|---|---|---|---|
| Music wire (ASTM A228) | 2200–2600 | 40–45% | 30–35% | Best small-spring fatigue life |
| Oil-tempered MB (A229) | 1600–1900 | 40–45% | 30–35% | Good for larger wire |
| Chrome-silicon (A401) | 1900–2100 | 42–48% | 32–38% | High-temp, shock duty |
| 302 stainless | 1500–1900 | 35–40% | 28–32% | Corrosion resistance, lower fatigue |
| 17-7 PH stainless | 1700–2000 | 38–42% | 30–34% | Better fatigue than 302 |
| Phosphor bronze | 900–1200 | 35–40% | 28–32% | Electrical, non-magnetic |
| Inconel 718 | 1800–2100 | 40–45% | 32–38% | High temp, expensive |
Numbers are typical for cold-drawn or cold-rolled spring wire at room temperature. Hot-wound or stress-relieved springs behave differently — always confirm with the wire mill's data sheet.
Why Cyclic Duty Needs Lower Stress
Fatigue cracks initiate at the coil I.D. where the stress concentration is highest. At 40% UTS you might get 10⁵–10⁶ cycles. At 30% UTS the same spring can run 10⁷+ cycles. The trade is real: lower stress means more wire, bigger envelope, more cost. The alternative is a spring that fails at 200,000 cycles in a valve train or a latch.
For dynamic applications, see our notes on spring dynamic load design.
Spring Index, Curvature, and Stress Concentration
Spring index (D/d — mean diameter divided by wire diameter) drives how much stress concentrates on the inside of the coil. Low index springs (under 5) are stiff and highly stressed at the I.D. High index springs (over 12) are floppy and hard to wind consistently.
| Index (D/d) | Curvature stress factor | Practical effect |
|---|---|---|
| 4–5 | 1.15–1.20 | High I.D. stress, tight tolerance risk |
| 6–9 | 1.08–1.12 | Sweet spot for most designs |
| 10–12 | 1.05–1.08 | Good fatigue, watch buckling |
| >12 | ~1.03 | Buckling and winding instability |
If your overload failures keep happening at the same spot — the inside of the first active coil — the index is probably too low. Revisit it before changing material. Our article on spring index and stress walks through the calculation.
Design Rules to Prevent Yielding
1. Keep working stress under 40% UTS for static, 32% for cyclic. This is the single biggest lever.
2. Design for the maximum load the assembly can ever apply, not the nominal load. Include handling, over-travel, and thermal expansion.
3. Add a solid-height margin. Leave at least 15% travel between max working height and solid height.
4. Preset (scragging) the spring. Compress to solid once during manufacturing to induce controlled set, then measure free length. This stabilizes the spring for its service life.
5. Shot peen for fatigue. Induces compressive residual stress at the surface, typically 20–40% fatigue life gain on steel springs.
6. Watch temperature. Above 120 °C for music wire or 250 °C for 302 stainless, stress relaxation accelerates even below yield.
7. Specify wire diameter and free length tolerances that match the load tolerance you actually need. Loosening free length tolerance rarely helps if load is the real requirement.
Presetting: The Cheap Insurance
Presetting (also called scragging or setting) means deliberately over-compressing the spring during production so it yields once, under controlled conditions, and then behaves elastically afterward. Done right, the spring's free length is stable to within 1% for the rest of its life. Done wrong — over-compressed or not stress-relieved — you get a spring that keeps creeping.
If your supplier doesn't preset high-stress springs, ask why. It costs almost nothing at volume and eliminates a whole class of field complaints.
When Overload Is Unavoidable
Some applications — shock absorbers, safety latches, recoil systems, die springs — are designed to absorb overload. In those cases:
- Use chrome-silicon or 17-7 PH, which tolerate higher stress
- Design for the overload case as the working case, not the exception
- Increase wire diameter rather than adding coils
- Accept a larger envelope
For die and stamping applications where springs take repeated impact, see spring die applications.
Manufacturing Controls That Prevent Yield Failures
At BQUQ, springs are wound on CNC coilers with in-process pitch and diameter monitoring, then stress-relieved in a controlled-atmosphere furnace. Four production lines under one roof in Dongguan cover compression, extension, and torsion springs, plus the stamping and CNC parts that go around them.
Key controls for overload-prone springs:
- Wire certification — mill certs on tensile and chemistry for every lot
- Stress relief — temperature and time logged per batch
- Preset verification — free length measured before and after
- Load testing — sampled at installed height, not just free length
- Traceability — batch ID on the bag, tied to furnace and coiler records
If you're sourcing compression springs or extension custom springs for a duty cycle that includes overload, send the load-height curve and the worst-case travel. We'll tell you whether the design survives or needs more wire.
Frequently Asked Questions
Q: Can a spring recover after it has yielded?
A: No. Yielding is permanent plastic deformation at the crystal level. Once the wire has slipped, the spring will not return to its original free length or load. You can sometimes re-set it to a new, stable length, but the original performance is gone. Replace yielded springs rather than trying to "re-train" them.
Q: How much overload causes permanent set?
A: It depends on material and index, but as a rule of thumb, exceeding roughly 45–50% of tensile strength in torsional stress will produce measurable set. For music wire at 2300 MPa UTS, that's about 1050–1150 MPa. Most well-designed static springs run at 800–950 MPa. The margin is deliberate.
Q: Does heat cause the same problem as overload?
A: Similar outcome, different mechanism. Heat causes stress relaxation — the wire slowly loses load even below yield. Music wire is generally limited to about 120 °C continuous; 302 stainless to about 250 °C; Inconel 718 to 600 °C+. If your spring loses load in service without visible deformation, temperature is the likely cause.
Q: Should I specify preset springs?
A: Yes, for any spring running above 35% of tensile strength or in a precision assembly. Presetting stabilizes free length and load, and typically costs little at production volume. Specify it on the drawing with the preset height and the acceptable free-length tolerance after setting. It removes a common source of field complaints.
Q: What tolerance can BQUQ hold on spring free length?
A: For typical compression springs, ±0.5 mm on free length and ±5% on load at installed height are standard. Tighter tolerances — down to ±0.2 mm free length on small springs — are achievable with in-process gauging. CNC axes hold ±0.005 mm on the tooling and end-grind geometry. Send your load-height curve for a specific quote.
Related Resources
- About BQUQ and our Dongguan factory: /about/
- Compression, extension, and torsion springs: /compression-springs/, /extension-custom-springs/, /torsion-springs/
- Industry trends in spring sourcing: /industry-dynamics/
- More technical articles: /bquq-blog/
- Frequently asked questions: /faq/
- Case studies: /case/
- Contact the engineering team: /contact/
Authored by the BQUQ Engineering Team. BQUQ (Dongguan) runs CNC machining (±0.005 mm), metal stamping, custom springs, and heat sink production in one ISO9001 factory. Source-direct from Dongguan, China — quote in 12 hours: sc@bquq.com | WhatsApp +86 13713157787 | www.bquq.com


