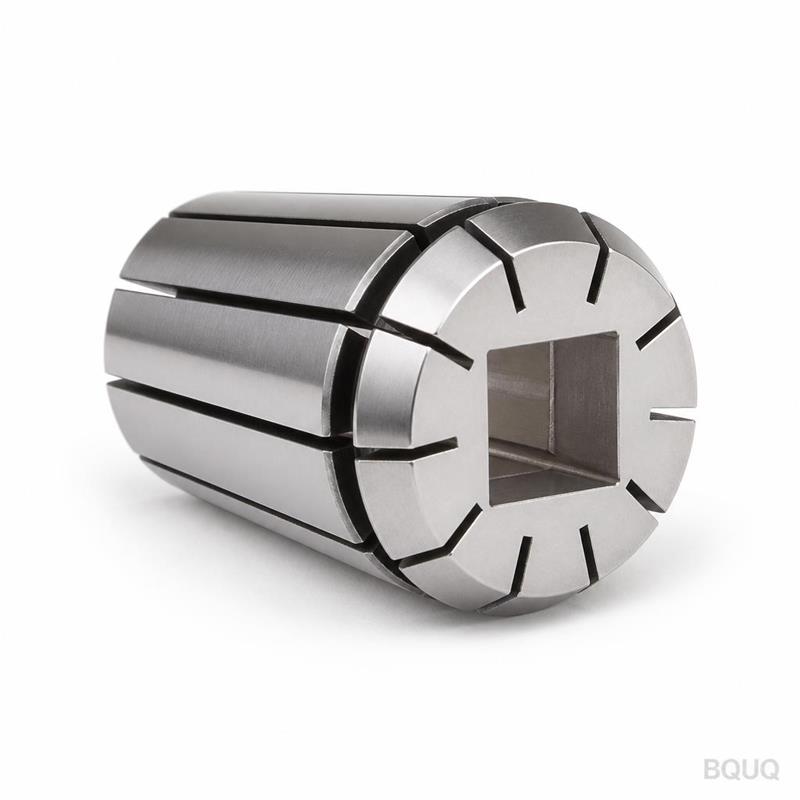
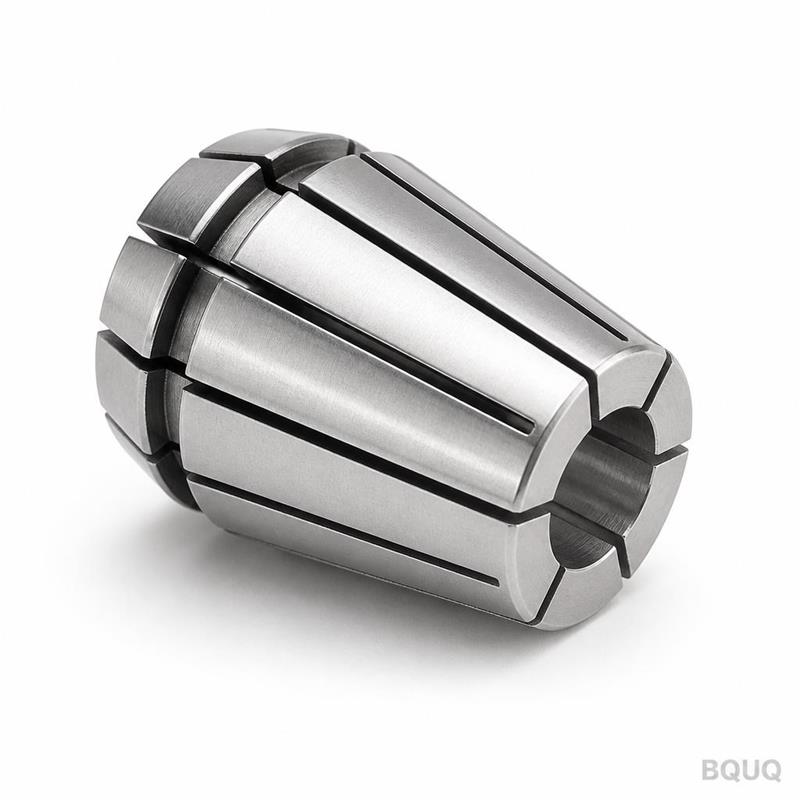
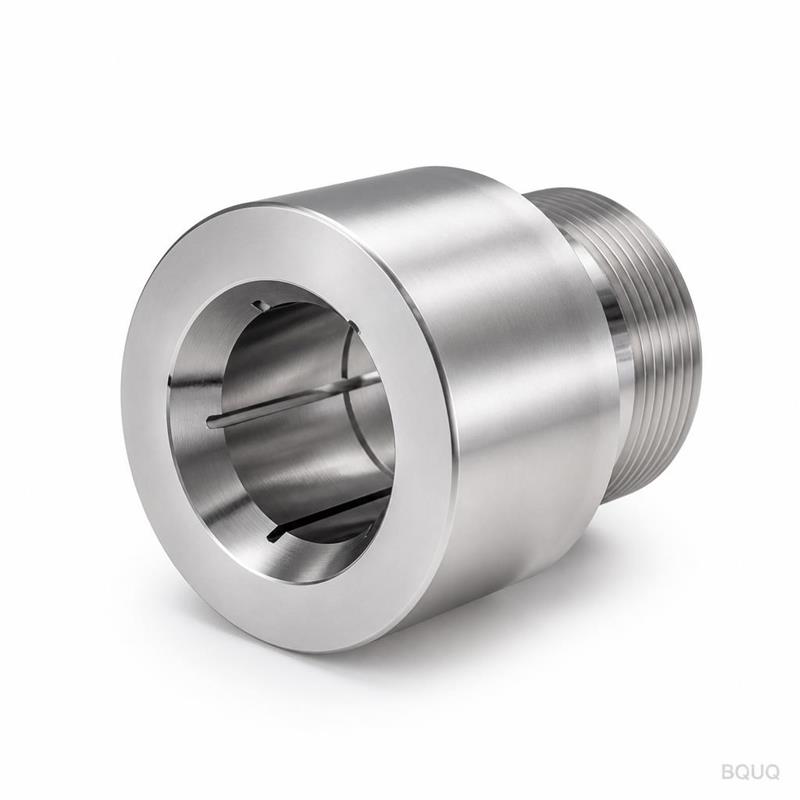
OpeningYour drawing defines the part. We build it exactly to that geometry. Every ER collet chuck and tool kit component is machined, heat-treated, and ground to your specified tol
OpeningYour drawing defines the part. We build it exactly to that geometry. Every ER collet chuck and tool kit component is machined, heat-treated, and ground to your specified tolerances. Before ship
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your drawing defines the part. We build it exactly to that geometry. Every ER collet chuck and tool kit component is machined, heat-treated, and ground to your specified tolerances. Before shipment, each unit is 100% inspected for runout, taper angle, and hardness. We do not ship guesswork.
At a glance: Tolerance ±0.005 mm on critical diameters, surface finish Ra 0.4 µm on taper seats, lead time 15–20 working days after drawing approval, no MOQ.
Specifications
Parameter
Value
Notes
Material options
20CrMnTi, 40Cr, 9Cr18, 65Mn
Carburized or through-hardened per application
Hardness
58–62 HRC (case), 40–45 HRC (core)
For collet chuck body and nut
Machining process
CNC turning, 5-axis milling, ID/OD grinding
Grinding after heat treatment for taper accuracy
Taper accuracy
AT3 or better
For ER11–ER40 collet seats
Runout (TIR)
≤0.005 mm at nose, ≤0.010 mm at 100 mm
Measured with precision test bar
Surface finish
Ra 0.4 µm on taper, Ra 0.8 µm on shank
Ground and lapped surfaces
Thread type
Metric fine (M12×1.5 to M60×2.0) or custom
For pull-back or push-out actuation
Coatings
TiN, TiAlN, black oxide, or none
Optional, per your drawing note
Batch size
1 piece to 5000 pieces
No MOQ, same process control
Inspection
CMM, hardness tester, runout gauge
Report per batch, photos included
Lead time
15–20 days for standard kits
Faster for existing tooling
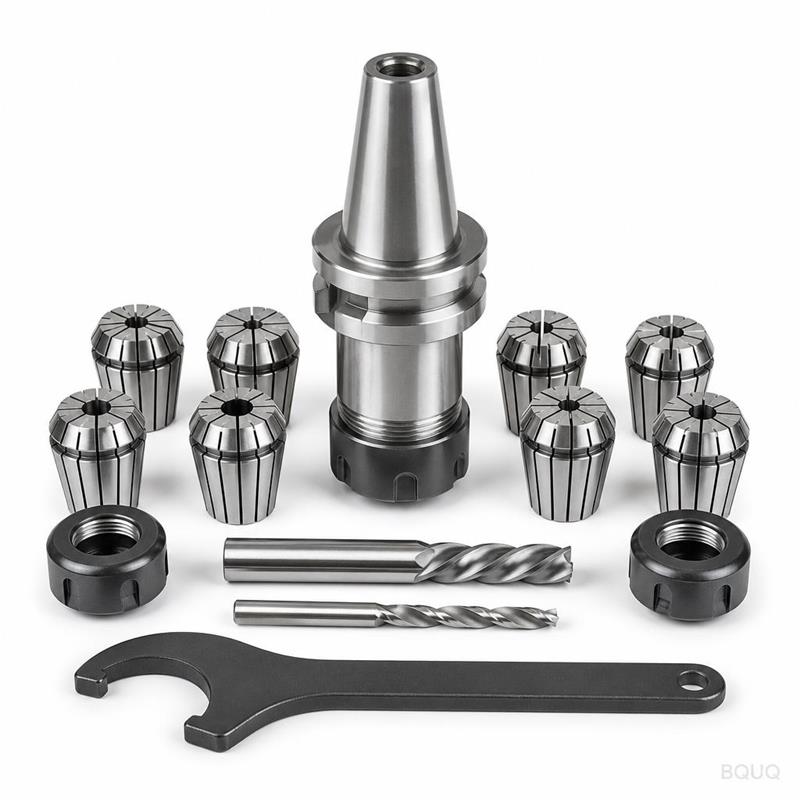
We run the full process in one factory: CNC turning, milling, heat treatment, grinding, and final assembly of the tool kit (collet chuck body, collets, nuts, and wrenches). No subcontracted steps, no hidden variation.
Three reasons buyers send us their drawings
1. Batch-traceable quality. Each heat number and material lot is recorded. If you need to trace a part back to its steel coil, we can do that. We keep records for 5 years. For aerospace or medical buyers, this is non-negotiable.
2. Inspection report per batch. You get a dimensional report for every batch, not just a sample. We measure taper angle, runout, hardness, and thread pitch. If a dimension is out, we flag it before shipping, not after you mount it on a spindle.
3. One factory for CNC + stamping + springs + heat sinks. Your collet chuck kit might need a spring washer, a stamped retainer plate, or a heat sink for a high-speed application. We make all of them under one roof. Fewer vendors, fewer logistics delays, one responsible party.
Where these parts are used
Custom CNC collet chucks are not shelf items. They go into machines where standard ER chucks fail.
High-speed milling spindles (30,000+ RPM): Balanced tool kits reduce vibration and extend bearing life.
Swiss-type lathes: Slender collet chucks for small-diameter bar stock, with custom pull-back threads.
Automotive transfer lines: Multi-spindle heads where each chuck must hold identical runout for consistent bore diameters.
Medical implant machining: Titanium and stainless parts require rigid, low-runout tool holding to hit ±0.01 mm features.
Aerospace structural parts: Deep-pocket milling with long reach tools—custom length chucks and hardened nuts prevent chatter.
Die and mold shops: Pre-hardened steel chucks that survive high torque without deformation.
If you are making chips and your current holder vibrates, drifts, or wears unevenly, send us the drawing. We will fix the geometry.
Q: What is your MOQ?
A: No MOQ. We accept one-piece prototypes and 5000-piece production runs. The unit price drops with quantity, but the first article gets the same inspection as the last.
Q: How do you guarantee tolerance and quality?
A: We grind the taper after heat treatment, not before. We measure every part with a CMM and a calibrated runout gauge. The inspection report is included in the shipment. If you find a bad part, we replace it at no cost, including freight.
Q: What is your lead time for a custom ER collet chuck kit?
A: Standard kits (ER20–ER32) ship in 15 days. Complex designs with special threads or coatings take 20 days. Tooling for repeat orders is kept on file, so reorders are faster.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. We supply mill certificates for the raw steel and a hardness report for every batch. Third-party testing (SGS, BV) is available at your cost.
Send your drawing
Send us your PDF or STEP file. We reply with a firm quote in 12 hours—not a range, a number. Include your target quantity, material, and any critical tolerance callouts. We will confirm what we can hold and what we cannot.
Email: sc@bquq.com
WhatsApp: +86 13713157787
Precision manufacturing, made in China, no MOQ. Your custom CNC collet chuck kit, verified before shipment.