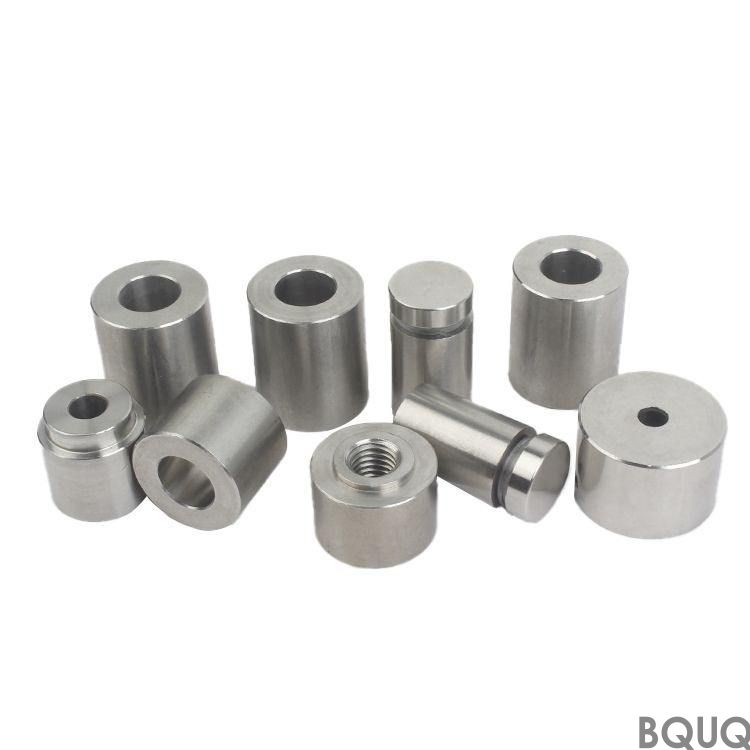
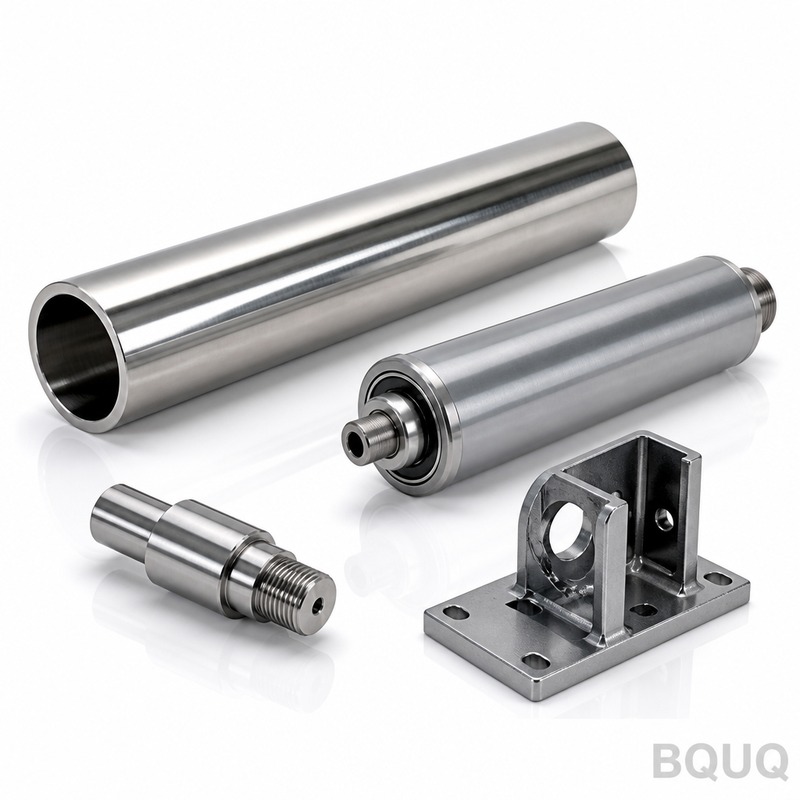
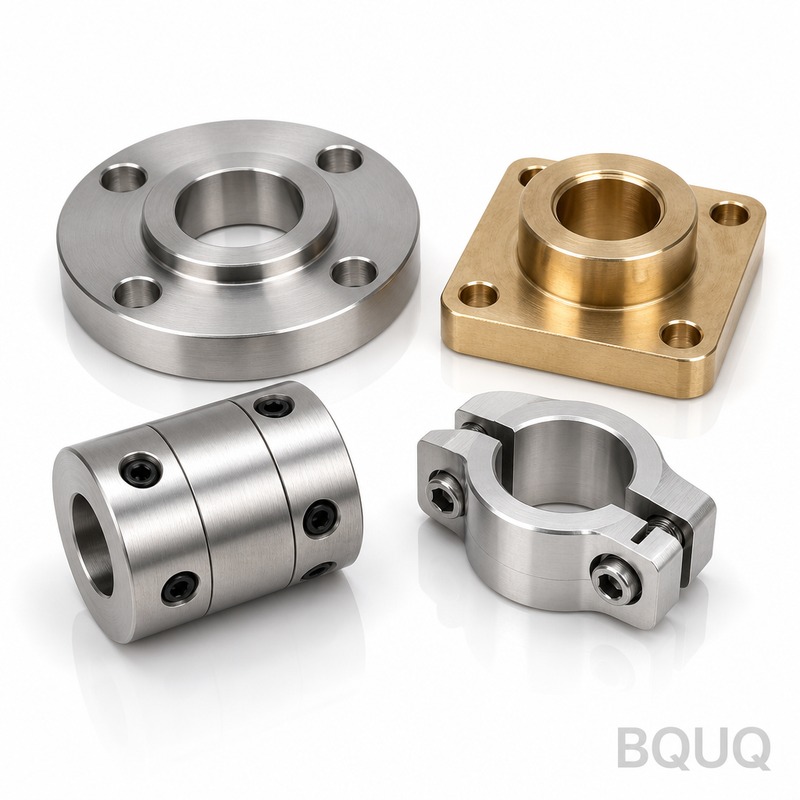
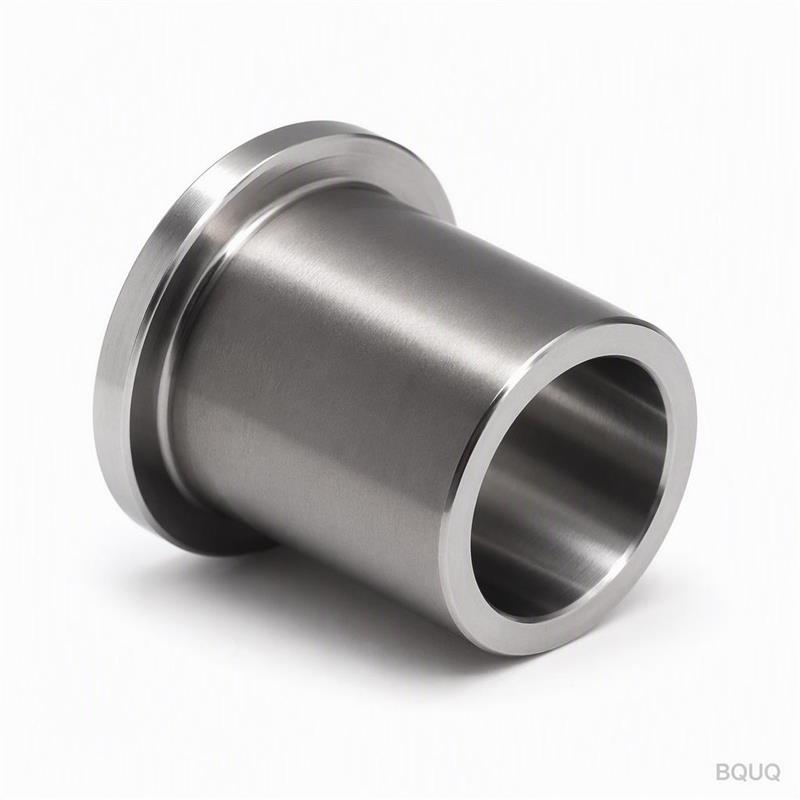
CNC turning parts from BQUQ are machined from Stainless 303 / 304 / 316L and can run up to 1000 mm in length while holding flatness on the mounting face directly from the tool. Thermal resistance is measured per lot, tooling runs are stable, and inspection catches die wear as a measurable shift in fin pitch before parts reach the field. Low fin gauge and tight pitch give more surface per cubic millimetre than machined or extruded profiles in the same envelope.
Key Takeaway
CNC turning parts from BQUQ are machined from Stainless 303 / 304 / 316L and can run up to 1000 mm in length while holding flatness on the mounting face directly from the tool. Thermal resistance is measured per lot, tooling runs are stable, and inspection catches die wear as a measurable shift in fin pitch before parts reach the field. Low fin gauge and tight pitch give more surface per cubic millimetre than machined or extruded profiles in the same envelope.
The cnc turning parts combines fin pitch with stock in Stainless 303 / 304 / 316L, so up to 1000 mm length parts keep on the mounting face. Thermal resistance is , measured at per lot.
Design Approach and Process
Because the base and fins are pressed as one piece, there is no brazed joint to fail. flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
A single stroke forms the whole cnc turning parts, so part cost stops scaling with complexity. Tooling runs , and the cycle feeds a line.
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at rather than in the field.
Pressing Stainless 303 / 304 / 316L keeps the cnc turning parts light, from depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
Material Selection and Surface Finish
The standard material is Stainless 303 / 304 / 316L, supplied with bead blast + passivate. For applications where robotics exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Each batch carries a CMM report from . We record flatness, pitch, base thickness and hole position, and flag anything outside before it leaves the line.
Flatness is measured on granite rather than on cast iron, because at up to 1000 mm length reads differently on a plate that has not been lapped. Records keep both readings.
We inspect fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
Final containment is . Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
In robotics, the rating determines how much airflow the enclosure still needs. At robotics junction temperatures, fins at pitch keep the delta-T inside the sensor budget.
For robotics builds, the mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
robotics customers typically specify Stainless 303 / 304 / 316L for corrosion reasons and then hold the drawing to . The line absorbs the volume without a second source.
robotics packaging and vibration rules push toward one-piece construction. A stamped cnc turning parts has no adhesive to creep, which is the usual failure mode in two-part coolers.
Specifications
Parameter
Value / Range
Material
Stainless 303 / 304 / 316L
Surface finish
bead blast + passivate
Size range
up to 1000 mm length
MOQ (prototype)
30 pcs
MOQ (production)
200 pcs
Lead time (prototype)
72 hours
Lead time (production)
10 working days
FAQ: Your Questions Before Ordering
What tolerance can you hold?
General dimensions run to ; critical ones such as are held separately. Formed features inherit tooling repeatability of . If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
Can you deliver without surface treatment?
Yes, we ship as-pressed for customers who do their own finishing. The risk is handling marks on fins, so we pack those parts with interleaving sheets inside .
Standard packing is . We quote . Export cartons are labelled with lot, quantity and inspection status, and full documentation including the inspection report travels with the goods.
Do you provide CAD files or a drawing?
We supply a 2D drawing with the CMM report, and 3D STEP on request. Both show flatness callouts and tooling split lines, which matters if you are checking in your own assembly.
Can you help with thermal simulation before sampling?
Yes. Send your enclosure airflow, inlet temperature and the heat load to be dissipated, and we will run a steady-state model and return a suggested and combination. That usually saves one tooling iteration.
Our robotics experience runs back to the first tooling programme in 2015. That history is why the standard bead blast + passivate and are conservative rather than optimistic.
Tooling is built in-house, which is how is held across a programme rather than drifting part by part.
Quality staff sit beside the press, not in a separate room. Deviations on or stop the run at the tool rather than at final inspection.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
Flatness held directly from the tool on the mounting face
Lead time
Standard production lead time after tooling approval
MOQ
Low-volume and batch production accepted
Capacity
Up to 1000 mm length parts; cycle feeds a line
Selection / comparison
Option
Best for
Trade-off
Stamped fins
High fin density in a fixed airflow envelope
Die wear shifts fin pitch over time
Machined profile
Simple geometry and tight single-piece control
Lower surface area per cubic millimetre
Extruded profile
Long uniform sections
Less tolerant of batch variation than stamping
Brazed assembly
Complex multi-piece shapes
Brazed joint can fail under thermal cycling
Pressed one-piece base and fins
Uniform thermal interface contact
Requires tooling and stroke control
Process / inspection
Stage
Control
Record
Material selection
Stainless 303 / 304 / 316L verified
Material certificate and lot traceability
Forming
Single stroke forms base and fins as one piece
Tooling run and cycle log
Fin pitch check
Measurable shift in fin pitch detected
Inspection record at lot level
Flatness check
Flatness on mounting face held from the tool
Dimensional report before shipment
Thermal test
Thermal resistance measured per lot
Per-lot thermal resistance data
Final inspection
Inspection before every shipment
Shipment release record
Frequently Asked Questions
What materials are used for CNC turning parts?
BQUQ machines CNC turning parts from Stainless 303 / 304 / 316L. These grades support parts up to 1000 mm in length while keeping flatness on the mounting face directly from the tool, so thermal interface contact stays uniform and the part remains light depending on envelope.
Flatness on the mounting face is held directly from the tool, not from a secondary operation. Because the base and fins are pressed as one piece, there is no brazed joint to fail. Inspection verifies flatness before every shipment, which keeps thermal interface contact uniform across the lot.
BQUQ produces CNC turning parts up to 1000 mm in length. At that length, flatness on the mounting face is still held directly from the tool, and the single-stroke forming process keeps the base and fins as one piece without a brazed joint.
Thermal resistance is measured at per lot. This per-lot measurement confirms that fin pitch, fin gauge, and mounting-face flatness remain within specification. If die wear shifts fin pitch, inspection catches it at the lot level rather than in the field.
Why choose stamped fins over machined or extruded profiles?
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope. Stamped construction also tolerates batch variation better than extrusion, because die wear shows up first as a measurable shift in fin pitch that inspection catches.
What is the minimum order quantity for CNC turning parts?
BQUQ accepts low-volume and batch production for CNC turning parts. Because a single stroke forms the whole part, part cost stops scaling with complexity, and tooling runs are stable enough to feed a line. Contact BQUQ with your envelope and fin pitch for a specific MOQ.
How are CNC turning parts inspected before shipment?
Inspection before every shipment covers fin pitch, fin gauge, flatness on the mounting face, and thermal resistance measured per lot. Die wear shows up first as a measurable shift in fin pitch, so lot-level inspection catches variation before parts reach the field.
Key Specifications and Selection Guide
Spec comparison
Parameter
Value / Range
Material
Stainless 303 / 304 / 316L
Tolerance
Flatness on mounting face directly from tool
Lead time
Stable tooling runs; cycle feeds a line
MOQ
Not specified in article
Capacity
Up to 1000 mm length
Selection / comparison
Option
Best for
Trade-off
CNC turning parts
Up to 1000 mm length with flatness on mounting face
Not for complex brazed joints
Machined profiles
Simple geometries
Less surface per cubic millimetre than stamped fins
Extruded profiles
Uniform cross-sections
Less surface per cubic millimetre than stamped fins
Stamped construction
Low fin gauge and tight pitch
Tooling wear measurable as fin pitch shift
Frequently Asked Questions
What materials are used for CNC turning parts?
BQUQ CNC turning parts are machined from Stainless 303 / 304 / 316L. These materials provide corrosion resistance and machinability. Parts can run up to 1000 mm in length while holding flatness on the mounting face directly from the tool. Thermal resistance is measured per lot for each material batch.
What is the maximum length for CNC turning parts?
CNC turning parts from BQUQ can run up to 1000 mm in length. Flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform. This length capability suits applications requiring long, straight turned components with tight flatness.
How is flatness controlled on the mounting face?
Flatness on the mounting face is held directly from the tool during CNC turning. Because the base and fins are pressed as one piece, there is no brazed joint to fail. This keeps thermal interface contact uniform and ensures consistent performance in the field.
How is thermal resistance verified?
Thermal resistance is measured per lot. Inspection catches die wear as a measurable shift in fin pitch before parts reach the field. This per-lot measurement ensures that each batch meets thermal performance requirements and that tooling runs remain stable throughout production.
What are the advantages of stamped construction over machined or extruded profiles?
Low fin gauge and tight pitch give more surface per cubic millimetre than machined or extruded profiles in the same envelope. Stamped construction tolerates complex fin patterns, and a single stroke forms the whole part, so part cost stops scaling with complexity. Tooling runs are stable and the cycle feeds a line.
Inspection before every shipment catches die wear as a measurable shift in fin pitch. Thermal resistance is measured per lot. Tooling runs are stable, and the cycle feeds a line. These controls ensure that parts meet specifications and do not reach the field with defects.
What is the lead time and MOQ for CNC turning parts?
The article does not specify lead time or MOQ. Tooling runs are stable, and the cycle feeds a line, which supports consistent production. For specific lead time and MOQ, contact BQUQ directly with your part requirements and quantity.