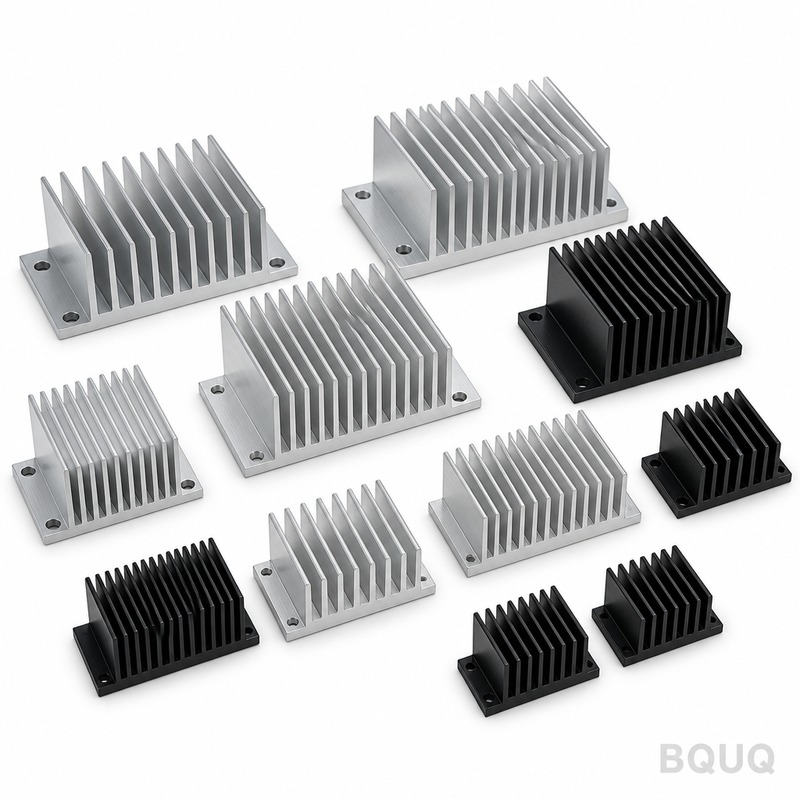
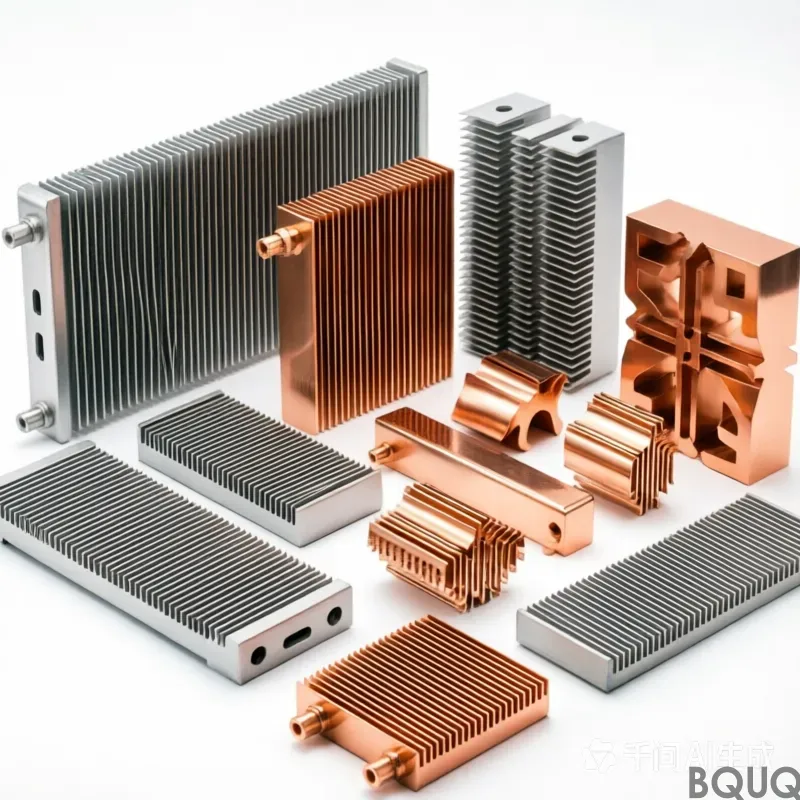
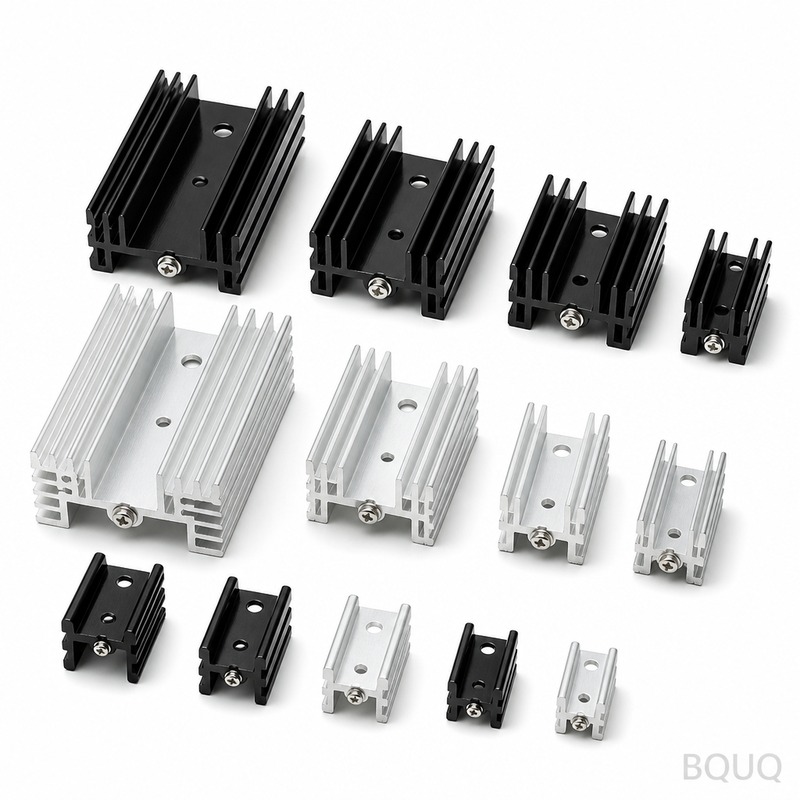
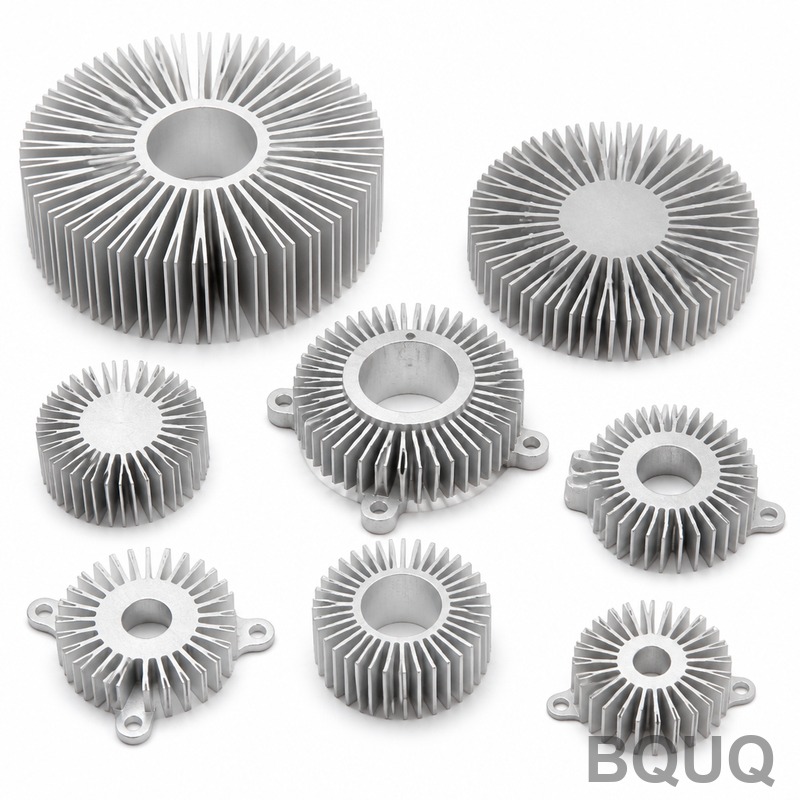
This Power Supply Heatsink is a CNC-machined aluminum or copper component that pulls heat away from IGBTs, MOSFETs, diodes, and voltage regulators. We hold flatness to 0.02mm acros
Power Supply Heatsink CNC Machining | BQUQ Precision Factory China
This Power Supply Heatsink is a CNC-machined aluminum or copper component that pulls heat away from IGBTs, MOSFETs, diodes, and voltage regulators. We hold flatness to 0.02mm across the base, surface
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This Power Supply Heatsink is a CNC-machined aluminum or copper component that pulls heat away from IGBTs, MOSFETs, diodes, and voltage regulators. We hold flatness to 0.02mm across the base, surface finish to Ra 1.6μm, and runout to 0.05mm TIR on all mounting bosses. You get a heatsink that mounts without shims, conducts heat uniformly, and ships from our Dongguan factory in 72 hours for prototypes.
Base Plate Flatness That Eliminates Thermal Paste Gaps
Most power supply failures start at the interface between the semiconductor and the heatsink base. If the base is warped by 0.1mm, the air gap acts as an insulator and the junction temperature rises by 15–20°C. We machine every Power Supply Heatsink base on a 3-axis CNC with a vacuum fixture, then verify flatness on a granite surface plate. Typical result: 0.01–0.02mm flatness on bases up to 300mm long. That means your thermal paste does its job—filling microscopic pores, not compensating for machining error.
Fin Geometry: We Cut Thinner, Tighter, and Faster Than Extrusion
Extruded heatsinks have fin thickness limits around 1.2mm and fin pitch that drifts over long lengths. We mill fins from solid bar stock. Minimum fin thickness is 0.8mm, minimum fin spacing is 2.0mm, and we hold fin height to ±0.05mm. For a 150mm long heatsink, that gives you 15% more surface area than a comparable extrusion. More surface area equals lower thermal resistance. We also deburr every fin edge with a robotic brush—no sharp slivers that cut your hands during assembly.
Material Selection: 6061-T6 for Cost, 6063-T5 for Anodizing, C1100 for Extreme Duty
We stock three grades for Power Supply Heatsinks. 6061-T6 is our default: 95 HB hardness, excellent machinability, good thermal conductivity (167 W/m·K). If you need a black anodized finish, we switch to 6063-T5—it produces a more uniform dye uptake and has a smoother surface. For high-current rectifier bridges that run hot continuously, we machine C1100 copper (390 W/m·K, 2.3x better than aluminum). For copper, we recommend a nickel-plated finish to prevent oxidation. Tell us your dissipation wattage and airflow, and we will recommend the material and fin density.
Mounting Holes, Threads, and Standoffs: Drilled and Tapped in One Setup
You do not want to drill mounting holes separately—that is how runout happens. We machine the base, fins, mounting holes, and tapped threads in a single CNC setup. Our tapping cycle holds thread depth to ±0.05mm, and we use form taps for aluminum to avoid chip clogging. Common thread sizes we cut: M3, M4, M5, and #6-32. We also machine pressed-in standoffs for PCB mounting, with a press-fit force of 10–20 kg per standoff. If your drawing specifies a shoulder or counterbore for a screw head, we hold that to ±0.02mm.
Specification
Value / Range
Material Options
6061-T6, 6063-T5, C1100 copper, 5052
Base Thickness
3mm – 25mm
Max Base Length
600mm (single setup)
Fin Thickness
0.8mm minimum
Fin Pitch
2.0mm – 8.0mm
Hardness (Aluminum)
95 HB (6061-T6), 80 HB (6063-T5)
Flatness (Base)
0.02mm over 300mm length
Surface Finish (Ra)
1.6μm standard, 0.8μm on request
Runout (TIR)
0.05mm on mounting bosses
Thread Tolerance
6H for metric, 2B for UNC
Prototype Lead Time
72 hours (single piece)
Production Lead Time
7 – 12 days (100–1000 pcs)
MOQ
No MOQ (1 piece accepted)
Surface Finish Options: From Bare Aluminum to Black Anodize Type II
Bare aluminum heatsinks oxidize naturally, which reduces emissivity. For passive convection, we recommend clear anodize (Type II, 8–12μm) to improve emissivity to 0.8 and protect against corrosion. For forced air, black anodize (Type II, sulfur dye) gives the same emissivity and looks professional. We also offer a chem-film (Alodine) finish for applications where electrical grounding is required. Each batch is tested for coating thickness using an eddy-current gauge, and we record the values in the inspection report. No anodize on copper—we use electroless nickel (5–8μm) instead.
Inspection Before Every Shipment: CMM Report Included
Every Power Supply Heatsink gets a full dimensional check before it leaves our floor. We use a Zeiss CMM for base flatness, fin pitch, and hole positions. A surface roughness tester checks Ra on the base. A thread plug gauge verifies every tapped hole. You receive a PDF inspection report with measured values against your drawing callouts. If we find any deviation beyond tolerance, that part is scrapped—we never ship "close enough" parts. For production batches over 100 pieces, we include an X-bar and R chart for flatness and finish.
What is the minimum order quantity for a Power Supply Heatsink?
No MOQ—we machine a single prototype for testing or a thousand units for production, and the unit price drops by roughly 30% at 500 pieces.
Can you match my existing heatsink drawing exactly?
Yes, send your 2D drawing or 3D STEP file; we run a DFM check within 4 hours and flag any features that need changes, such as fin thickness below 0.6mm or undercuts that require EDM.
How do you control quality for large production runs?
First article inspection on the CMM, then in-process checks every 30 minutes on critical dimensions (flatness, thread depth, and runout) with a final 100% visual and dimensional audit before packing.
What is the typical lead time for a custom Power Supply Heatsink?
Prototype (1–5 pieces) ships in 72 hours; production (up to 1000 pieces) ships in 7–12 days, and we can expedite to 5 days with a 10% surcharge.
Why Engineers Trust BQUQ for Power Supply Thermal Management
We are a precision manufacturing factory in Dongguan, China, with 20 years of experience in CNC machining, stamping, and spring manufacturing. Our heatsinks go into EV chargers, industrial inverters, medical power supplies, and telecom rectifiers. We do not outsource—every operation from raw bar stock to deburring to anodizing is in-house. That is why we can hold tolerances that job-shop brokers cannot match. For a deeper dive on tooling choices that affect fin quality, read our CNC cutting tool selection guide. To understand how we choose tolerances for your specific application, see our CNC machining tolerances guide.
Get a Firm Quote Within 12 Hours—Send Your Drawing
Email your STEP or PDF drawing to sc@bquq.com. We will respond within 12 hours with a firm quote, our DFM feedback, and a suggested material if you are unsure. For urgent needs, message us on WhatsApp at +86 13713157787. Include your target quantity and required finish (bare, anodized, or nickel). We will confirm pricing and lead time in the same working day. There is no MOQ, no tooling charge for standard sizes, and we can ship via DHL or FedEx for 3-day delivery to the US or EU.