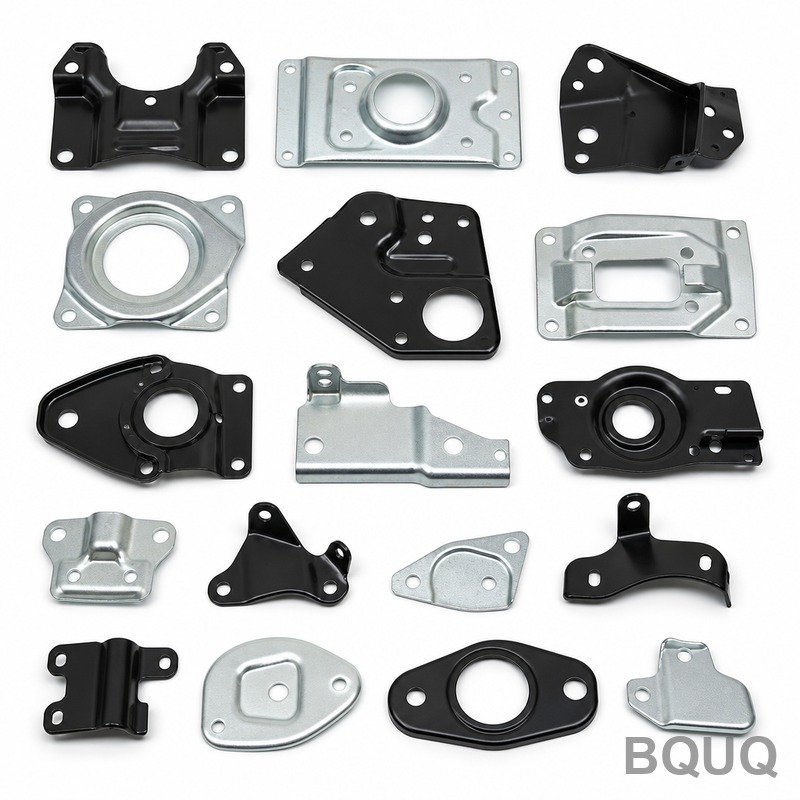
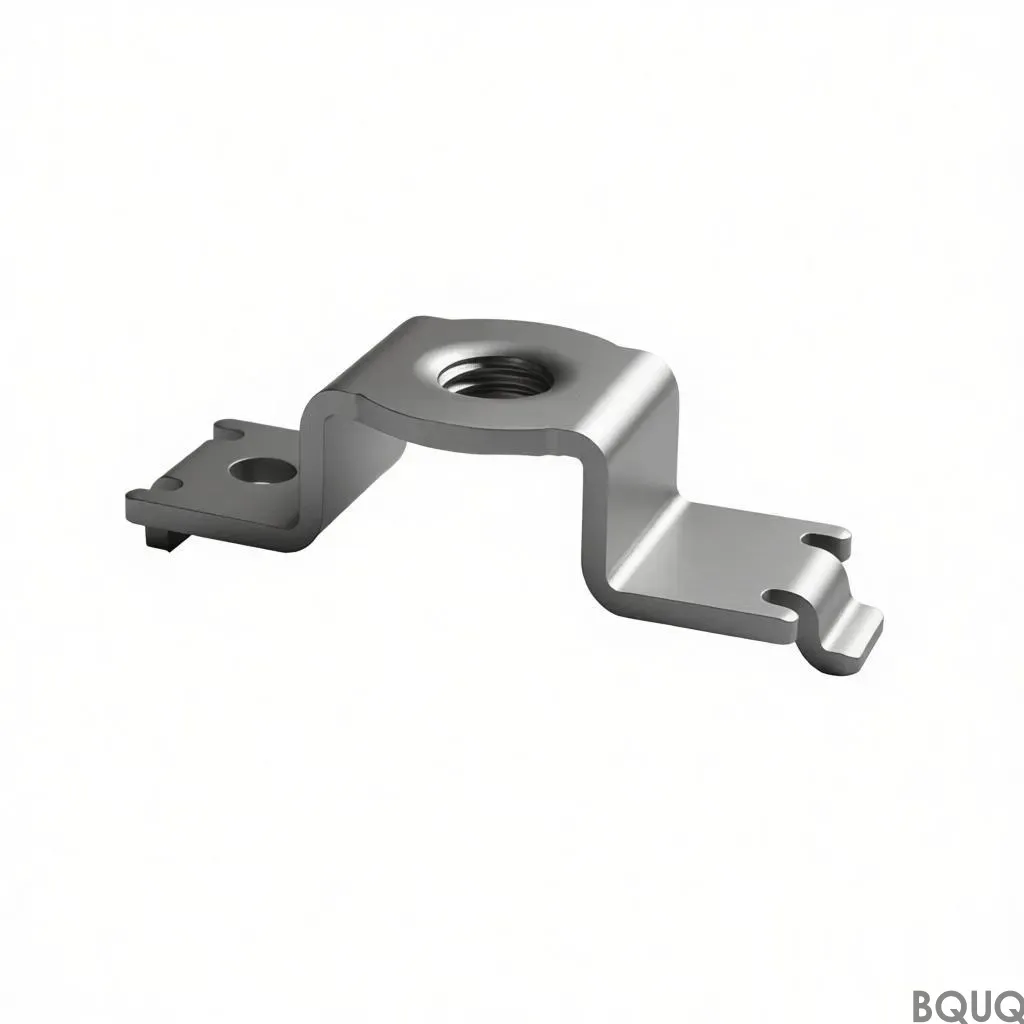
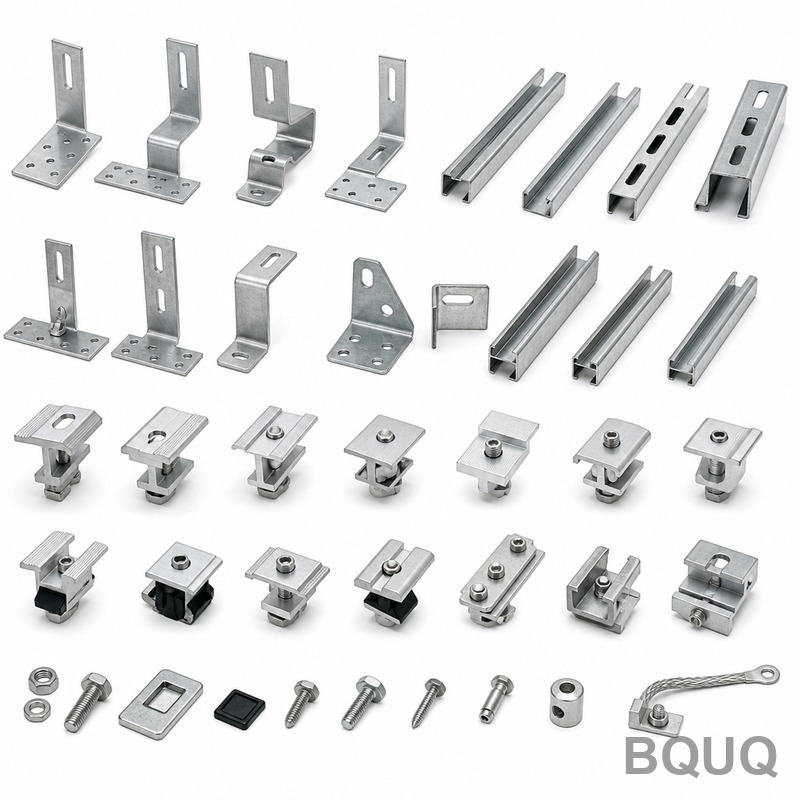
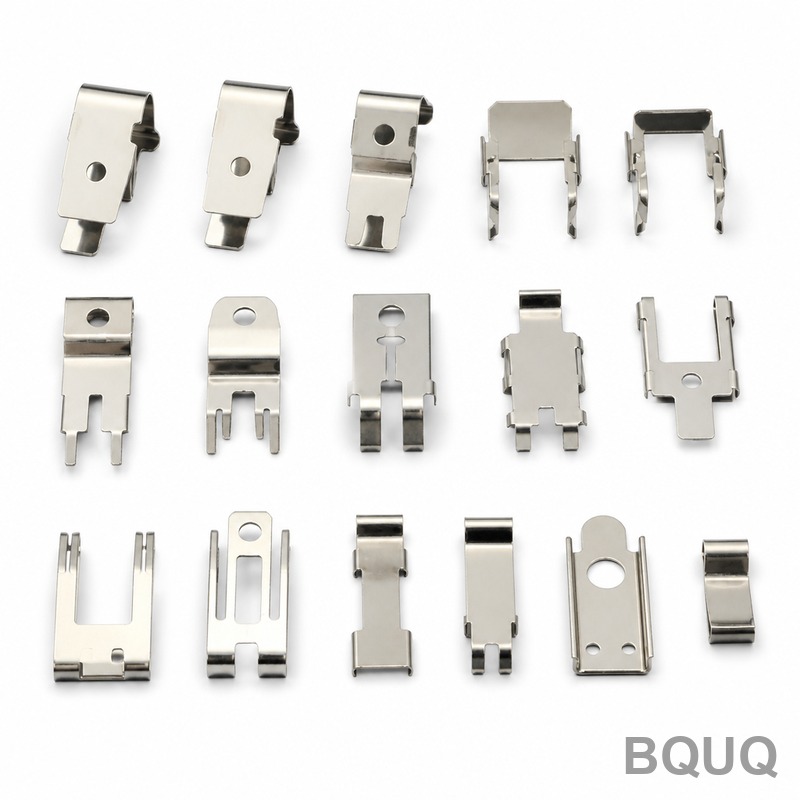
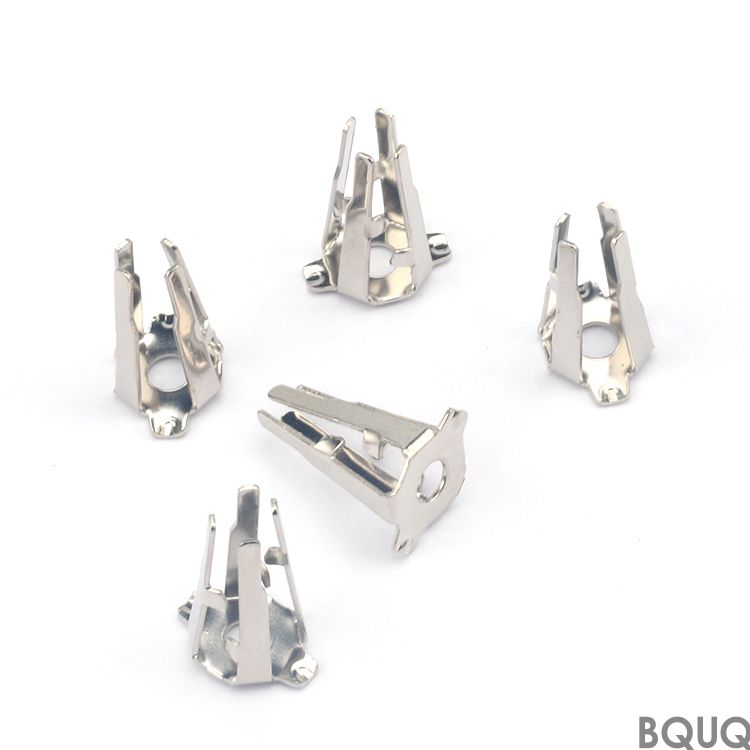
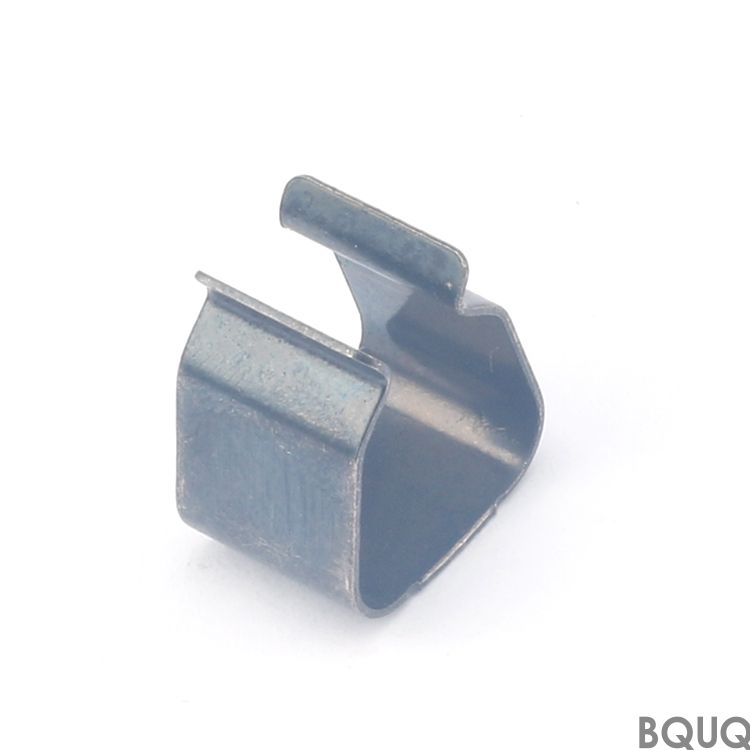
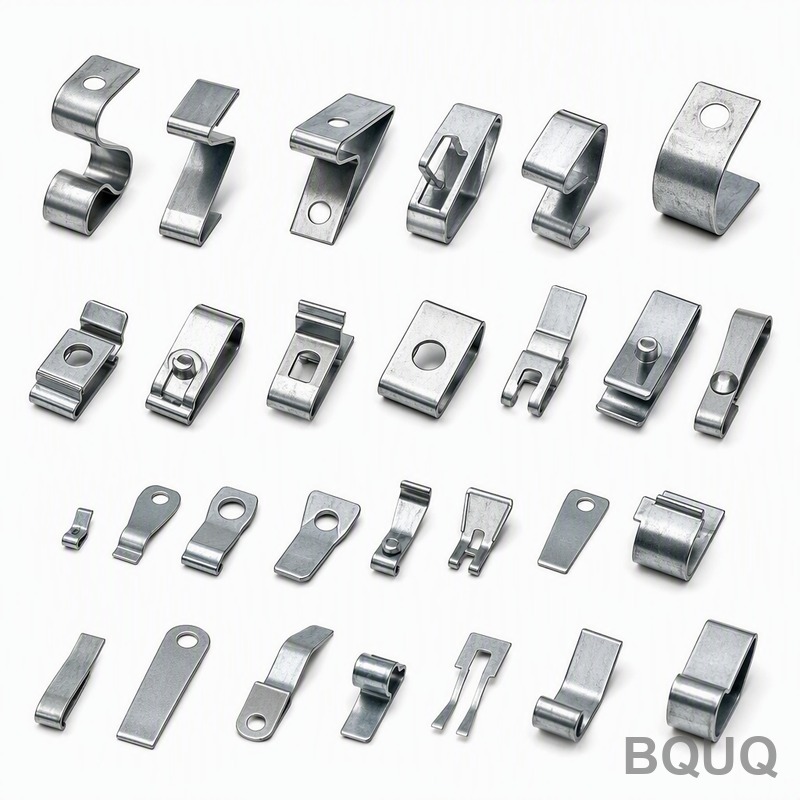
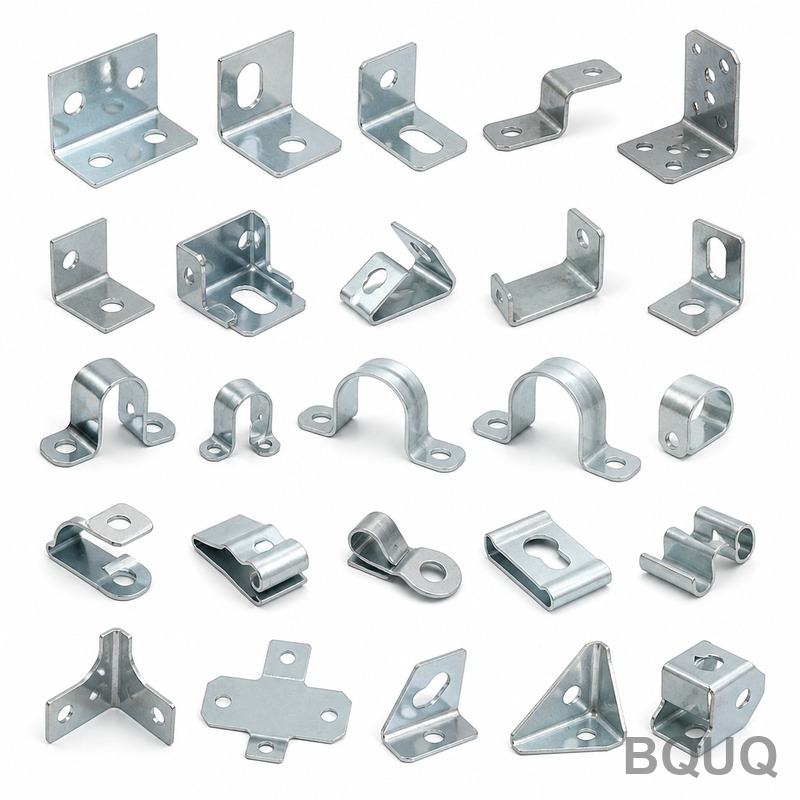
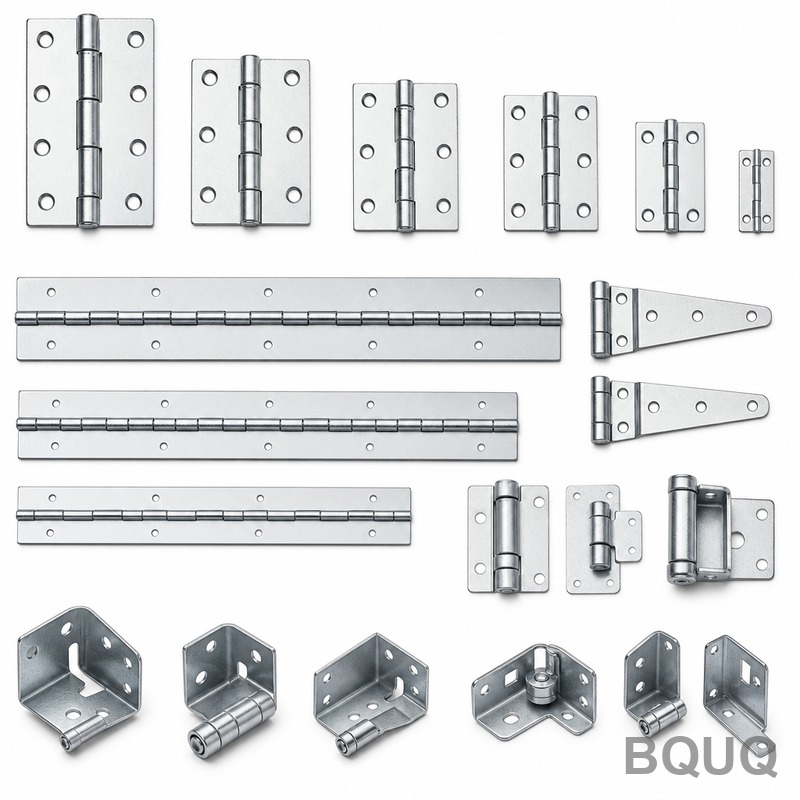
This is our Stamped Automotive Mounting Plates Flanges Collection — a family of precision-stamped parts used to mount sensors, brackets, ECU housings, and fluid line connectors directly onto vehicle c
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is our Stamped Automotive Mounting Plates Flanges Collection — a family of precision-stamped parts used to mount sensors, brackets, ECU housings, and fluid line connectors directly onto vehicle chassis or engine blocks. You get flatness within 0.08mm, hole-to-hole tolerances of ±0.05mm, and a hardness range of 25–45 HRC depending on material, all produced in our Dongguan factory with a standard 15-day lead time and no MOQ.
Why Stamping Beats Machining for High-Volume Mounting Plates
If you need 5,000 or 50,000 pieces of a mounting plate, stamping is faster and cheaper than CNC milling. Our progressive dies produce a finished plate in one pass — blanking, piercing, coining, and bending in sequence. Cycle time is 3–8 seconds per part depending on size. Compared to machining, stamping cuts piece price by 40–60% at volume, while holding the same ±0.05mm positional tolerance on critical hole patterns. For prototypes or low-volume runs below 500 pieces, we recommend CNC machining — but for production, this collection is your cost lever.
Material Options and Heat Treatment for Crash-Safe Mounting
Automotive mounting plates must survive vibration, corrosion, and impact. We stock four material families: SPCC cold-rolled steel (hardness 25–30 HRC as-stamped), SPFH590 high-strength steel (35–40 HRC), SUS304 stainless (for corrosion-prone underbody mounts), and 5052 aluminum (for lightweight brackets). For high-wear applications like flange faces that seal against gaskets, we add induction hardening to reach 45 HRC on the sealing surface only, leaving the rest ductile. All materials come with mill certificates traceable to the heat number.
Hole Pattern Accuracy: The Difference Between a Bolt-On and a Rework
A mounting plate with misaligned holes means stripped threads or a rattling bracket. We hold hole-to-hole center distances to ±0.05mm using precision-ground dies and in-die piloting. For critical patterns — like a 4-hole engine mount with 12mm bolts — we guarantee a mating fit against your mating part drawing. Our die maintenance program checks punch wear every 10,000 strokes and re-grinds before tolerance drift exceeds 0.02mm. You get a print-verified part, not a "close enough" part.
Surface Finish and Edge Condition: No Burrs, No Leaks
Burrs on mounting plates cut into your assembly line gloves and cause sealing failures on flanges. We deburr every stamped edge to a maximum burr height of 0.05mm, using either a vibratory finisher or a high-speed brush station depending on part geometry. Surface finish on sealing faces is held to Ra 1.6µm, and on non-critical surfaces Ra 3.2µm. For flanges that mate with rubber gaskets, we add a coining step to create a smooth, flat micro-surface — verified with a profilometer on every first article and every 500th piece during production.
Inspection Before Every Shipment: CMM, Hardness, and Flatness Reports
Every batch of stamped mounting plates ships with a full inspection report. We use a Zeiss CMM to check hole positions and diameters on 5 pieces per lot, a Rockwell hardness tester on 3 pieces per lot, and a surface plate with feeler gauges for flatness on 10% of the batch. If any sample fails, the entire lot is quarantined and re-sorted. You also get a material certificate and a die-wear log — so you know exactly what you're receiving. This is not a random QC check; it's a documented release procedure.
Specification
Value / Range
Material options
SPCC, SPFH590, SUS304, 5052 aluminum
Thickness range
0.8mm – 6.0mm
Part size range
20mm x 20mm up to 300mm x 300mm
Hardness (as-stamped)
25 – 30 HRC (steel), 35 – 40 HRC (SPFH590)
Induction hardened hardness
Up to 45 HRC (select areas only)
Hole-to-hole tolerance
±0.05mm
Flatness
0.08mm max over 100mm length
Surface finish (sealing face)
Ra 1.6µm
Surface finish (non-critical)
Ra 3.2µm
Max burr height
0.05mm
Standard lead time
15 days after die approval
MOQ
No MOQ (single piece for prototype, 500+ for production)
Die Design and Tooling Ownership: Your Part, Your IP
We build progressive dies in-house using D2 tool steel for punches and carbide for wear inserts. Die life is 500,000 to 2,000,000 strokes depending on material thickness. You own the die design — we keep the physical tooling in our Dongguan factory, but the CAD files and IP belong to you. If you switch suppliers later, you get the full die drawings. For new parts, we can design the die from your 3D model in 5 working days, and produce first articles in 10 days. This is precision manufacturing with zero hostage-taking.
Pricing Logic and Volume Discounts for Flange Kits
Stamped part pricing is driven by material thickness, part size, and annual volume. For a typical 100mm x 80mm SPCC plate at 2mm thick, price per piece drops from $1.80 at 500 units to $0.65 at 10,000 units. Flange kits that include multiple stamped parts (e.g., a mounting plate plus a separate sealing flange) get a 8% combined-volume discount. We quote firm prices — no hidden tooling amortization fees unless you request it. Send us your drawing, and we'll return a piece price, tooling cost, and lead time breakdown within 12 hours.
Do you have a minimum order quantity?
No MOQ — we accept a single prototype piece for fitment testing, then scale to 500 or 50,000 pieces with the same tooling.
Can you customize the hole pattern or add a flange bend?
Yes, every part in this collection is custom — we adjust hole sizes, positions, bend angles, and flange heights directly from your CAD file, with no extra design fee for standard modifications.
How do you ensure quality on high-volume stamping runs?
We use in-die sensors that stop the press if a punch breaks, plus CMM verification on 5 pieces per lot and a full burr-height check on 10% of every batch — documented in your shipment report.
What is the lead time for a new stamped mounting plate?
First articles in 10 days after die design approval, production lead time is 15 days from that point — faster if we can use an existing die family.
Before you finalize your material choice, check our CNC cutting tool selection guide — it explains how different tool coatings affect edge quality on stamped parts that need secondary machining. And for tight-tolerance holes, our CNC machining tolerances guide clarifies what ±0.05mm really means in production. Both are written for engineers, not salespeople.
Get a firm quote within 12 hours. Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. We'll confirm material, price, tooling cost, and lead time — no games, no "estimated" numbers. This is precision manufacturing made in China, with no MOQ, done right. Send your drawing today.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.