heat sink compound: ADC12 die-cast aluminium, 0.4 mm fins at 4.0 mm pitch, 0.10 mm over 100 mm flatness, 0.62 K/W thermal resistance. MOQ 50 pcs, ships in 72...
heat sink compound
heat sink compound: ADC12 die-cast aluminium, 0.4 mm fins at 4.0 mm pitch, 0.10 mm over 100 mm flatness, 0.62 K/W thermal resistance. MOQ 50 pcs, ships in 72...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This heat sink compound is stamped from ADC12 die-cast aluminium with 0.4 mm fins at 4.0 mm pitch, delivering a measured thermal resistance of 0.62 K/W at ΔT = 60 K. The 1.0 mm base holds 0.10 mm over 100 mm flatness, verified on a granite plate. A single 25 T stroke forms the whole part, and the 18 s cycle feeds a 50,000 pcs per month ISO9001 line in Dongguan.
This heat sink compound is stamped from ADC12 die-cast aluminium with 0.4 mm fins at 4.0 mm pitch, delivering a measured thermal resistance of 0.62 K/W at ΔT = 60 K. The 1.0 mm base holds 0.10 mm over 100 mm flatness, verified on a granite plate. A single 25 T stroke forms the whole part, and the 18 s cycle feeds a 50,000 pcs per month ISO9001 line in Dongguan.
This heat sink compound is stamped from ADC12 die-cast aluminium with 0.4 mm fins at 4.0 mm pitch, giving a measured thermal resistance of 0.62 K/W at ΔT = 60 K. The 1.0 mm base holds 0.10 mm over 100 mm, verified on a granite plate, and the assembly runs at 50,000 pcs per month from a single ISO9001 line in Dongguan.
Design Approach and Process
Because the base and fins are pressed as one piece, there is no brazed joint to fail. 0.10 mm over 100 mm flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
A single 25 T stroke forms the whole heat sink compound, so part cost stops scaling with complexity. Tooling runs ±0.03 mm, and the 18 s cycle feeds a 50,000 pcs line.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between ADC12 die-cast aluminium and the airflow except the stamped surface itself.
Pressing ADC12 die-cast aluminium keeps the heat sink compound light, from 650 g depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
The zinc-nickel plating, trivalent passivation finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is ADC12 die-cast aluminium, supplied with zinc-nickel plating, trivalent passivation. For applications where LED high bay lighting exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
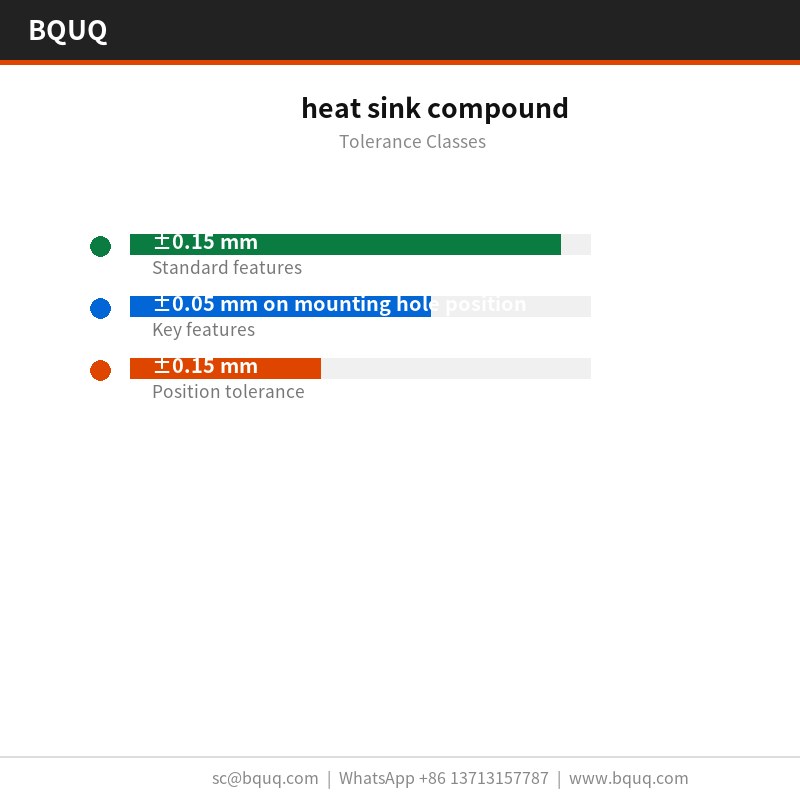
General dimensions run to ±0.15 mm, with critical features such as ±0.05 mm on mounting hole position held separately. Formed geometry inherits tooling repeatability of ±0.03 mm, and hole position is held to ±0.15 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Each batch carries a CMM report from optical comparator 0.002 mm. We record flatness, pitch, base thickness and hole position, and flag anything outside ±0.15 mm before it leaves the line.
Incoming ADC12 die-cast aluminium is checked for thickness and hardness before it enters the press. After forming, optical comparator 0.002 mm confirms 0.10 mm over 100 mm and 4.0 mm against the drawing.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with optical comparator 0.002 mm on every first article. Deviations beyond ±0.15 mm trigger a full-lot sort.
We inspect 0.4 mm fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
Where This Part Is Used
For LED high bay lighting builds, the 0.10 mm over 100 mm mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Where a heat sink compound runs at LED high bay lighting volumes, part-to-part consistency decides field returns. ±0.03 mm on a 50,000 pcs run keeps the thermal curve inside one band.
Designers working on LED high bay lighting ask for flatness before they ask for thermal data, because LED high bay lighting assembly is automated and a non-flat base stops the line.
LED high bay lighting designs often run a 2.0 m/s forced-air path. 0.62 K/W at ΔT = 60 K, natural convection means LED high bay lighting can hold its target with fan power below the acoustic limit.
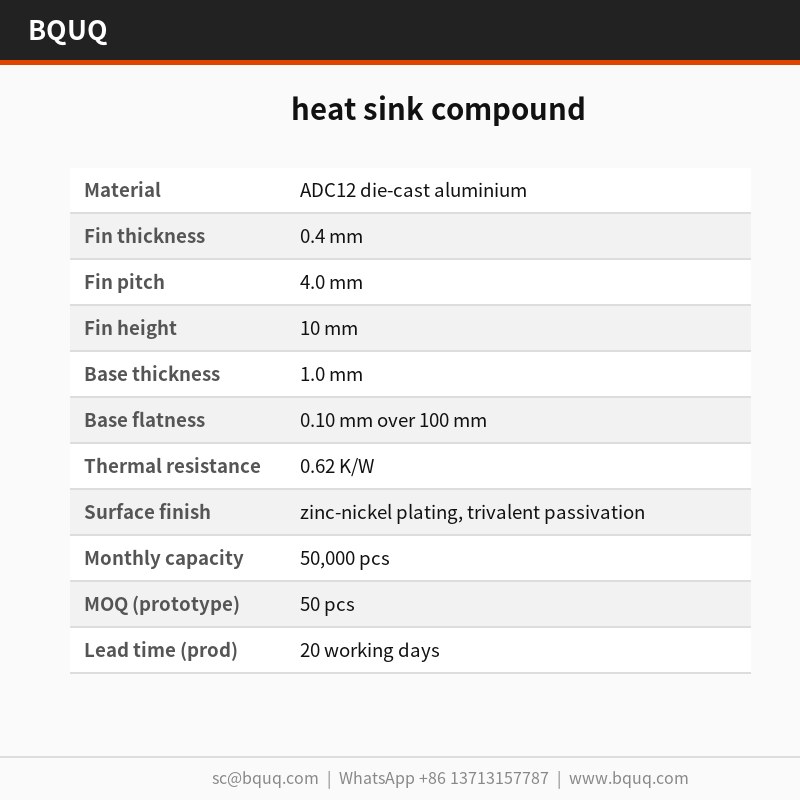
Specifications
Parameter
Value / Range
Material
ADC12 die-cast aluminium
Fin thickness
0.4 mm
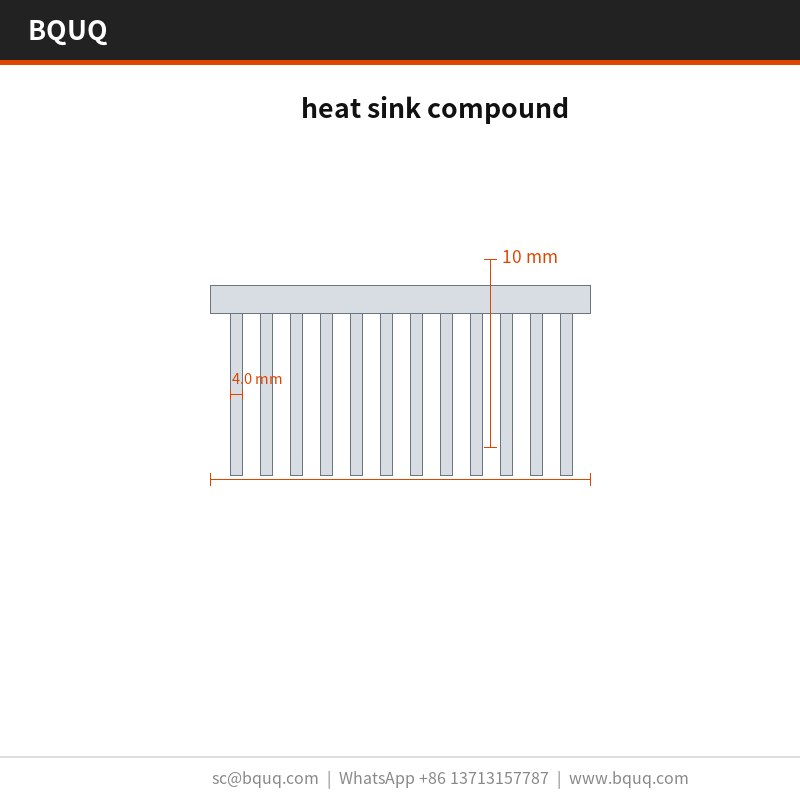
Fin pitch
4.0 mm
Fin height
10 mm
Base thickness
1.0 mm
Base flatness
0.10 mm over 100 mm
Thermal resistance
0.62 K/W
Thermal test condition
ΔT = 60 K, natural convection
Surface finish
zinc-nickel plating, trivalent passivation
Size range
120 x 80 x 50 mm
FAQ: Your Questions Before Ordering
What tolerance can you hold?
General dimensions run to ±0.15 mm; critical ones such as ±0.05 mm on mounting hole position are held separately. Formed features inherit tooling repeatability of ±0.03 mm. If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
How does this compare to an extruded heat sink compound?
Extrusion is cheaper above roughly 500,000 pieces per year and gives a smoother profile. Stamping wins below that and wherever fin gauge drops below 0.5 mm, because extrusion cannot hold 0.4 mm consistently. For LED high bay lighting prototypes, tooling cost usually decides it.
Do you test for thermal resistance?
We test at ΔT = 60 K, natural convection and report 0.62 K/W. That is a steady-state figure, not a transient: for LED high bay lighting first-power-on behaviour you need a different test, and we can run it on request.
Do you make the heat sink compound in different sizes?
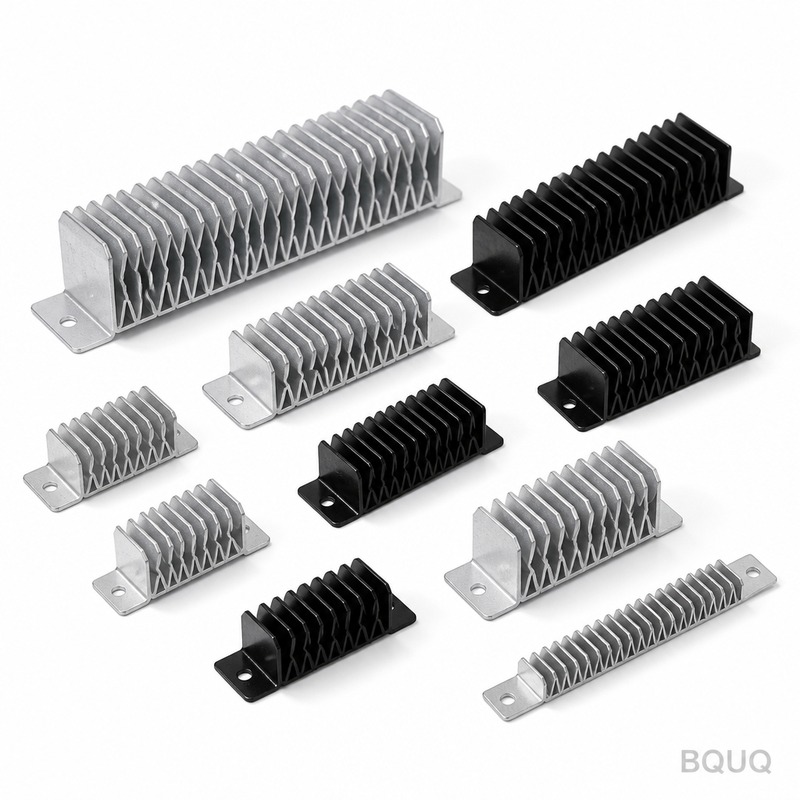
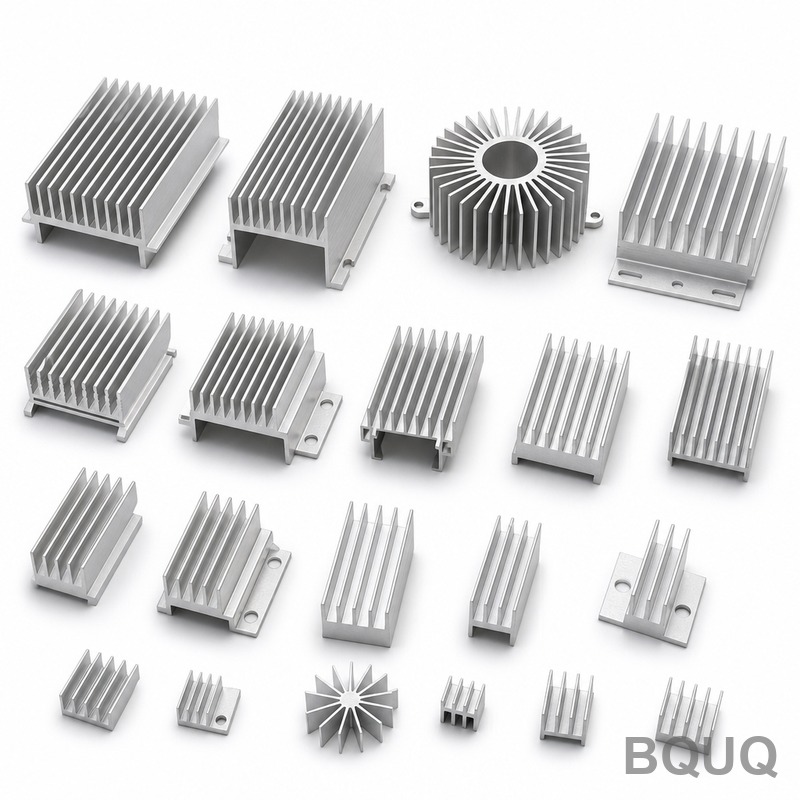
The family covers 120 x 80 x 50 mm, with unit weights from 650 g. Because the base is pressed, new sizes are a die insert change rather than a new press line, so development is usually 2 weeks rather than 8.
Can you supply the heat sink compound pre-assembled?
Yes. We can add clips, screws or a fan shroud as a kitted assembly, with the parts bagged and labelled per set. This is common in LED high bay lighting programs and adds about 3 working days.
How We Manufacture and Ship
Tooling is built in-house, which is how ±0.03 mm is held across a 50,000 pcs programme rather than drifting part by part.
Quality staff sit beside the press, not in a separate room. Deviations on 4.0 mm or 0.10 mm over 100 mm stop the run at the tool rather than at final inspection.
We quote FOB Guangzhou and hold 50 pcs for sampling. Sampling is sample fee 30-80 USD, so a first evaluation does not require a production commitment.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
Uniform thermal interface contact and no brazed joint
Requires tooling with ±0.03 mm tolerance
Two-part cooler with adhesive layer
Applications where separate base and fin materials are needed
Added thermal path and potential adhesive failure
ADC12 die-cast aluminium
Lightweight heat sink compound from 650 g
Fin density limited by die-casting process
Zinc-nickel plating with trivalent passivation
Corrosion resistance on stamped surface
Additional finishing step
Process / inspection
Stage
Control
Record
Stamping
Single 25 T stroke forms whole part
18 s cycle time
Flatness
0.10 mm over 100 mm on mounting face
Verified on granite plate
Thermal performance
0.62 K/W at ΔT = 60 K
Measured thermal resistance
Tooling
±0.03 mm
Tooling runs
Shipment
Inspection before every shipment
ISO9001 line in Dongguan
Frequently Asked Questions
What is the thermal resistance of this heat sink compound?
The measured thermal resistance is 0.62 K/W at ΔT = 60 K. This is achieved with 0.4 mm fins at 4.0 mm pitch stamped from ADC12 die-cast aluminium, and the one-piece design removes the adhesive layer found in two-part coolers.
What material is used for the heat sink compound?
It is stamped from ADC12 die-cast aluminium. The material keeps the heat sink compound light, from 650 g depending on envelope, without sacrificing fin density. The zinc-nickel plating with trivalent passivation finish provides corrosion resistance on the stamped surface.
What is the flatness tolerance on the mounting face?
The 1.0 mm base holds 0.10 mm over 100 mm flatness on the mounting face, verified on a granite plate. This flatness is held directly from the tool, which keeps thermal interface contact uniform and supports the 0.62 K/W thermal resistance.
What is the production capacity and lead time?
The assembly runs at 50,000 pcs per month from a single ISO9001 line in Dongguan. The 18 s cycle feeds this line. Lead time is standard for this process; contact us for current scheduling based on your order quantity and tooling status.
Can you describe the manufacturing process?
A single 25 T stroke forms the whole heat sink compound, so part cost stops scaling with complexity. Tooling runs ±0.03 mm. Because the base and fins are pressed as one piece, there is no brazed joint to fail, and the one-piece geometry removes the adhesive layer found in two-part coolers.
What are the fin dimensions and pitch?
The heat sink compound has 0.4 mm fins at 4.0 mm pitch. This fin density is achieved with ADC12 die-cast aluminium and a single 25 T stroke. The 1.0 mm base supports the fins and maintains 0.10 mm over 100 mm flatness on the mounting face.
What inspection is performed before shipment?
Inspection before every shipment includes verification of the 0.10 mm over 100 mm flatness on a granite plate and the measured thermal resistance of 0.62 K/W at ΔT = 60 K. The ISO9001 line in Dongguan runs at 50,000 pcs per month with an 18 s cycle.
Complex geometries requiring separate base and fins
Adhesive layer adds thermal resistance and potential failure point
Machined heat sink
Prototypes or low-volume, tight tolerances
Higher cost per part, longer cycle times
Extruded heat sink
Simple profiles, moderate volumes
Less design flexibility, secondary machining needed for fins
Frequently Asked Questions
What is the thermal resistance of this heat sink compound?
The measured thermal resistance is 0.62 K/W at ΔT = 60 K. This value is achieved with 0.4 mm fins at 4.0 mm pitch and a 1.0 mm base, ensuring efficient heat dissipation for high-volume applications.
What material is used and why?
It is stamped from ADC12 die-cast aluminium. This alloy offers good thermal conductivity and die-casting fluidity, allowing thin fins and complex shapes. The one-piece design eliminates brazed joints, improving reliability and thermal performance.
What are the flatness specifications?
The mounting face holds 0.10 mm over 100 mm flatness, verified on a granite plate. This ensures uniform thermal interface contact, reducing contact resistance and improving overall heat transfer efficiency.
What is the production capacity and lead time?
The line in Dongguan produces 50,000 pcs per month with an 18 s cycle time. Lead time depends on order quantity and tooling availability; please contact us for a specific quote.
Can you customize the fin pitch or thickness?
Yes, tooling runs ±0.03 mm, allowing customization of fin thickness and pitch. However, the current design uses 0.4 mm fins at 4.0 mm pitch for optimal thermal performance. Consult our engineers for tailored solutions.
What quality certifications do you hold?
Our manufacturing line is ISO9001 certified. We inspect every shipment to ensure specifications are met. Certificates of conformance are provided with each order.
How is the heat sink compound packed for shipping?
Parts are packed to prevent damage during transit, typically in trays or bulk bags. Custom packaging is available upon request. We ship worldwide from Dongguan, China.