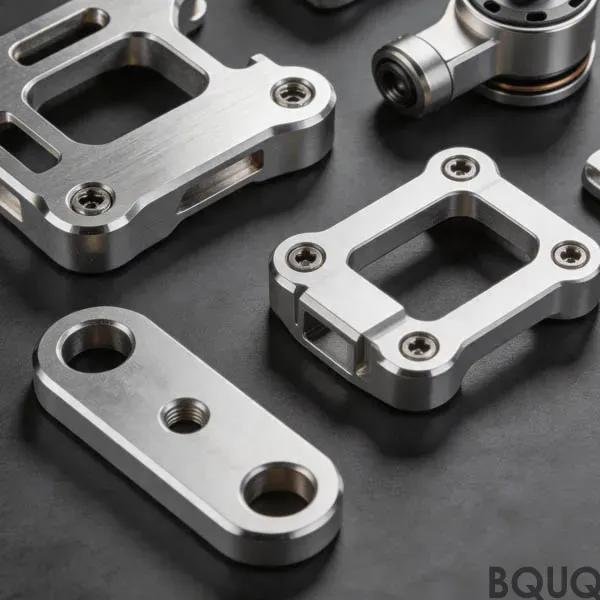
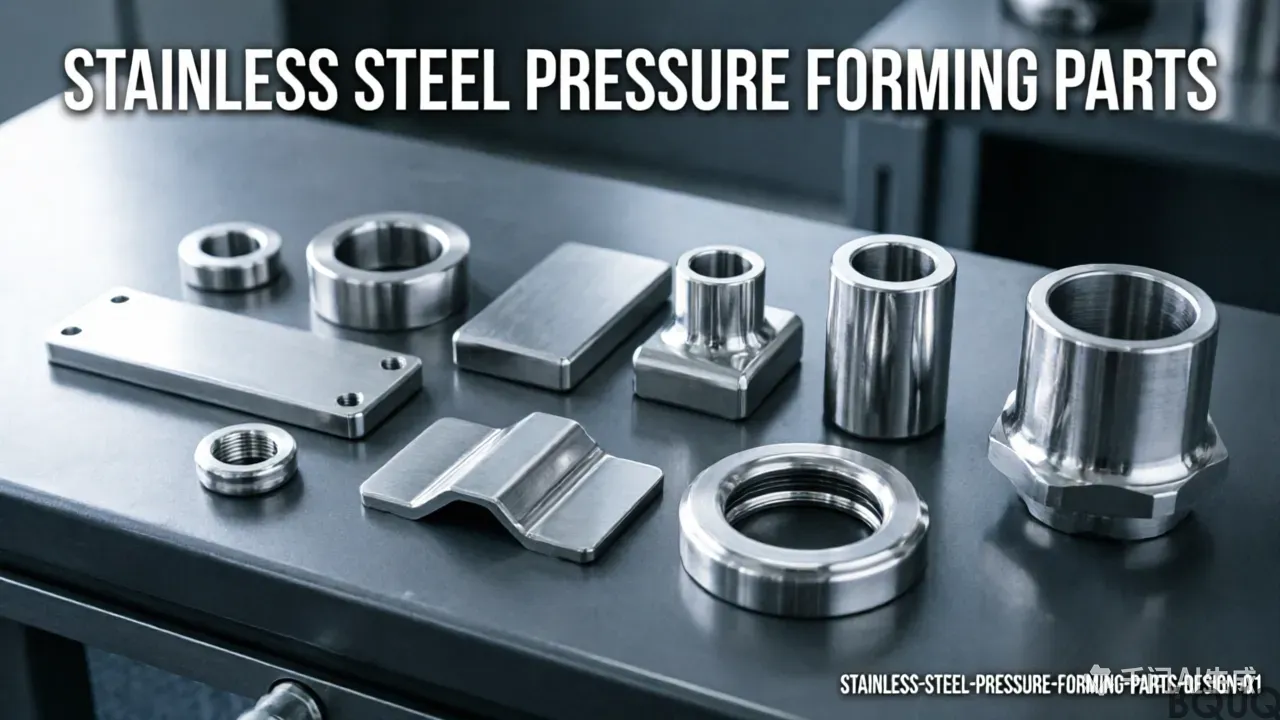
sheet metal parts manufacturer: POM / PEEK / nylon, tolerance 0.01 mm, surface hard chrome plate 0.025 mm, lead time 15 working days, MOQ 200 pcs. Capacity for medical device. Drawing review and first-article report included.
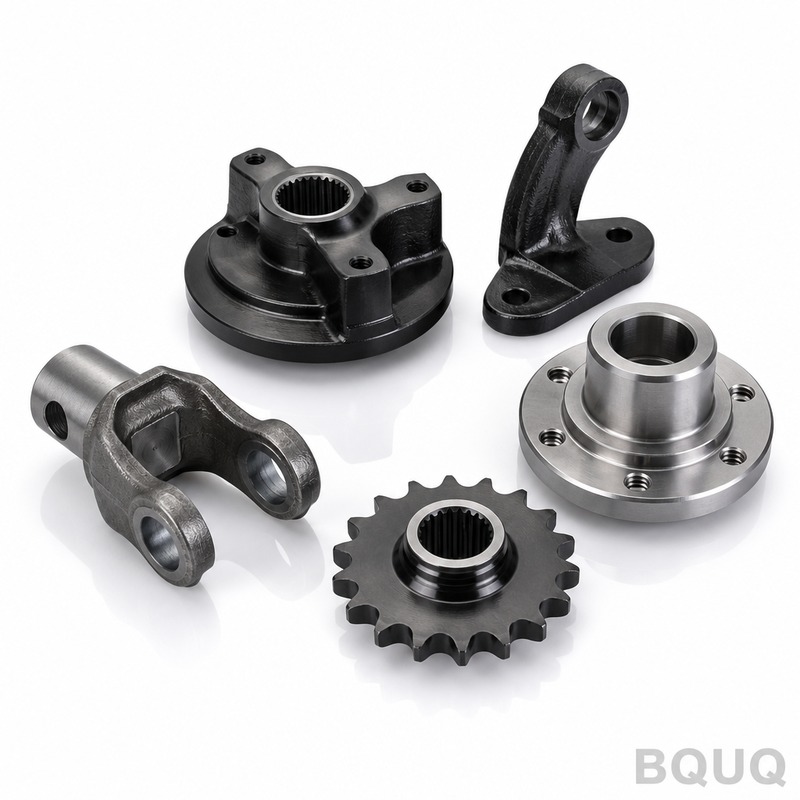
sheet metal parts manufacturer
Key Takeaway
Sheet metal parts manufacturer supply starts with a defined process window: aluminium 6061-T6, ±0.01 mm on critical features, Ra 0.4 on bore and Ra 0.8 external, 20 working days production lead time, and 500 pcs MOQ. Buyers facing tariff and logistics uncertainty increasingly require a second qualified source, so tolerances and tooling design are documented before production rather than verified only at final inspection.
There is no shortage of suppliers who can quote sheet metal parts manufacturer. The shortage is in suppliers who can explain why ±0.01 mm was chosen, what Ra 0.4 on bore, Ra 0.8 external does to service life, and how 20 working days is protected when tooling needs repair.
Related reading: Compression Spring vs Torsion Spring vs Extension Spring: What Is the Difference?.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | Aluminium 6061-T6 |
| Surface finish | Ra 0.4 on bore, Ra 0.8 external |
| Lead time (production) | 20 working days |
| MOQ (production) | 500 pcs |
Market and Technical Context
Tariff and logistics uncertainty has made regional qualification a priority in medical device. Buyers increasingly ask for a second qualified source, which changes how sheet metal parts manufacturer is specified and how tolerances are documented.
The technical bar keeps rising: assemblies that once accepted ±0.01 mm now specify tighter control on critical features, which pushes the decision to tooling design rather than to final inspection.
How We Manufacture It
The route for sheet metal parts manufacturer starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.01 mm is held at production speed rather than on a single slow part.
See also: Terminal Plating Thickness: Microns That Matter.
Tooling is designed around the measured capability of the process, so ±0.01 mm is a consequence of tooling geometry rather than an inspection filter. That is why 20 working days is realistic instead of optimistic.
In production, sheet metal parts manufacturer runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.01 mm.
Learn more about Oil-Tempered Wire Springs: Heavy-Duty Applications.
Material and Surface Finish
Material condition matters as much as grade. Aluminium 6061-T6 supplied in the wrong temper will drift after machining, which is why sheet metal parts manufacturer is stress-relieved before finishing when the geometry is asymmetric.
Where sheet metal parts manufacturer sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Further technical detail: What Is a Transfer Die? High-Speed Stamping for Complex Parts.
Substitution requests are common when Aluminium 6061-T6 goes on allocation. We qualify any substitute against the same ±0.01 mm and Ra 0.4 on bore, Ra 0.8 external criteria before shipping, and provide the certificate with the change.
Tolerance and Inspection
General dimensions on sheet metal parts manufacturer are held to ±0.01 mm; critical features are identified on the drawing and controlled separately with a tighter band.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on sheet metal parts manufacturer, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Recommended reading: BQUQ Cnc Machined Auto Lathe 20 Type Hex Bore Spring Collet.
Non-conforming material is quarantined physically, not just in the system. For sheet metal parts manufacturer, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
medical device is the largest application area for sheet metal parts manufacturer, where the part typically sees continuous load and a wide temperature range rather than laboratory conditions.
In assembly, sheet metal parts manufacturer is usually constrained by the mating part rather than by its own specification. Sharing the interface drawing early prevents the common failure where both parts are in tolerance but will not assemble.
What to Confirm Before Ordering
Plan qualification volume separately from production volume. For sheet metal parts manufacturer, 500 pcs is the point where the process is proven; everything before that is process development.
Confirm the reorder path. If sheet metal parts manufacturer is documented with tooling drawings and a first-article report on file, a repeat order years later reproduces the original part instead of approximating it.
FAQ: Your Questions Before Ordering
What is the minimum order quantity for sheet metal parts manufacturer?
General dimensions are held to ±0.01 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
How long does production take for sheet metal parts manufacturer?
Prototype quantities start well below production minimums. Production runs for sheet metal parts manufacturer start at 500 pcs, which is where the process window is proven and unit cost stabilises.
Compare it with Automotive High-Load Compression Spring: Oil-Tempered Wire, 5M-Cycle Fatigue, PPAP Documentation.
What surface finishes are available for sheet metal parts manufacturer?
Standard lead time for sheet metal parts manufacturer is 20 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Can you prototype before tooling?
Yes, and we recommend it. Prototyping sheet metal parts manufacturer without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of sheet metal parts manufacturer remains usable.
Capacity for sheet metal parts manufacturer is . That number is installed capability, not a sales figure, and it is what determines whether 20 working days holds when your volume increases.
Related reading: CNC Machining Aluminum vs Stainless Steel: Which Metal Is Right for Your Part?.
See also: Where to Buy Custom Metal Springs Online: Top 7 Suppliers.
Learn more about What Are the Manufacturing Differences Between Bonded Fin and Skived Fin Heat Sinks?.
Further technical detail: aluminum heat sinks passive cooling.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Aluminium 6061-T6 |
| Tolerance | ±0.01 mm on critical features |
| Lead time | 20 working days (production) |
| MOQ | 500 pcs (production) |
| Capacity | Production speed with tooling geometry fixed before run |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Single qualified source | Stable, low-risk programs with mature demand | No second-source coverage if tariffs or logistics disrupt supply |
| Second qualified source | Medical device and tariff-sensitive programs | Additional qualification and documentation effort |
| Tighter tolerance (±0.01 mm) | Critical features in rising technical-bar assemblies | Pushes cost and risk into tooling design rather than final inspection |
| Standard surface finish | Non-critical external surfaces | May not meet Ra 0.4 bore or Ra 0.8 external service-life requirements |
| Tooling repair protection | Programs with 20 working day lead time commitments | Requires planned maintenance windows and spare tooling strategy |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Process window definition | Fix material condition and tooling geometry first | Documented process window before machine selection |
| Tolerance validation | Confirm ±0.01 mm at production speed, not on a single slow part | Production-speed capability record |
| Surface finish | Ra 0.4 on bore, Ra 0.8 external | Surface finish measurement record |
| Tooling maintenance | Protect 20 working day lead time when tooling needs repair | Tooling repair and maintenance log |
| Final inspection | Verify critical features against documented tolerances | Inspection report tied to drawing requirements |
Frequently Asked Questions
What material and finish can you supply for sheet metal parts?
We supply aluminium 6061-T6 with Ra 0.4 on bore and Ra 0.8 external. These finishes support service life on critical features, and the material condition is fixed in the process window before production so ±0.01 mm is held at production speed.
What tolerance can you hold on critical features?
We hold ±0.01 mm on critical features. The decision is pushed to tooling design rather than final inspection, and we confirm the tolerance at production speed instead of on a single slow part.
What is the production lead time and MOQ?
Production lead time is 20 working days and MOQ is 500 pcs. We protect the 20 working day commitment when tooling needs repair by planning maintenance and spare tooling into the process window.
Why do buyers ask for a second qualified source?
Tariff and logistics uncertainty has made regional qualification a priority, especially in medical device. A second qualified source changes how sheet metal parts manufacturer is specified and how tolerances are documented, reducing supply risk.
Recommended reading: Certificate of honor.
How do you confirm ±0.01 mm at production speed?
We start with a process window, not a machine. Material condition and tooling geometry are fixed first, then we confirm ±0.01 mm is held at production speed rather than on a single slow part.
Compare it with Custom Mixed Type Industrial Springs.
What should I confirm before ordering sheet metal parts?
Confirm material condition, tooling geometry, critical-feature tolerances, surface finish Ra 0.4 bore and Ra 0.8 external, 20 working day lead time, and 500 pcs MOQ. Also confirm how tooling repair is protected and whether a second qualified source is required.
How does surface finish affect service life?
Ra 0.4 on bore and Ra 0.8 external are specified to support service life on critical features. These values are tied to the process window and tooling design, so they are documented before production rather than corrected at final inspection.