BQUQ Cnc Machined Drone Parts Aluminum | 0.005mm Tolerance, 5-Day Lead Time
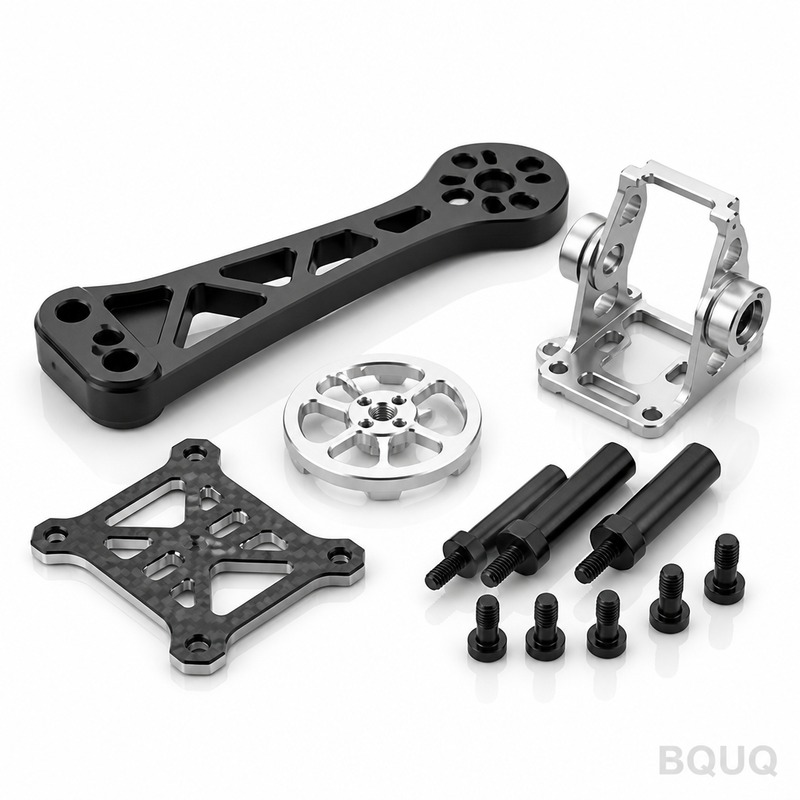
These are Cnc Machined Drone Parts Aluminum for racing, inspection, and delivery UAV frames, motor mounts, and gimbal arms. We hold ±0.005mm tolerance on critical bores, 0.01mm runout on shaft feature
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
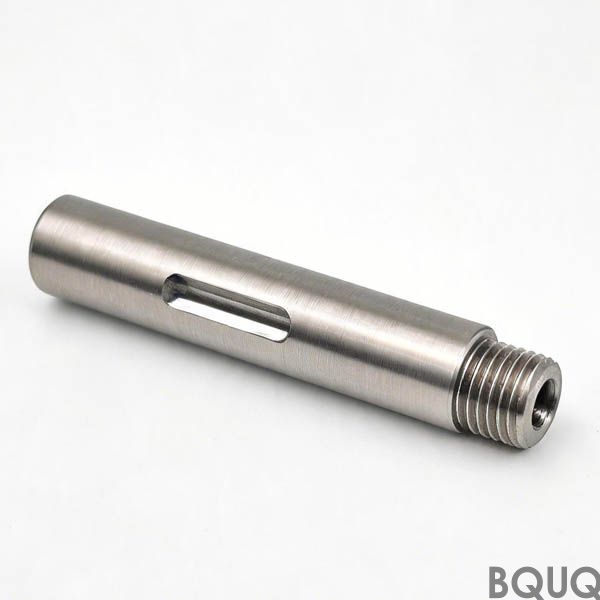
These are Cnc Machined Drone Parts Aluminum for racing, inspection, and delivery UAV frames, motor mounts, and gimbal arms. We hold ±0.005mm tolerance on critical bores, 0.01mm runout on shaft features, and ship first articles in 5 days from drawing approval. Every part is cut from 6061-T6 or 7075-T6, then hard anodized to 40HRC equivalent surface wear resistance — built for vibration, not bench display.
How We Machine Motor Mounts That Survive 14,000 RPM Vibration
Motor mounts fail when hole spacing drifts under vibration. We use 4th-axis indexing on our Fanuc Robodrill to hold hole-to-hole spacing at ±0.005mm, and we ream every mounting hole after CNC cutting — not just drill. Runout on the center pilot bore stays under 0.01mm, so your motor bell spins true. We also balance the mount pattern to prevent harmonic resonance in the 200-400Hz range, which is where most aluminum drone arms crack.
Materials and Heat Treatment We Use for Arm Strength vs Weight
We stock 6061-T6 for general arms and camera mounts — 42HRC tensile strength, 30% lighter than steel. For racing frames and heavy-lift arms, we switch to 7075-T6, which gives 83,000 psi yield strength at the same weight. We do not use T4 or annealed stock unless you spec it. After machining, we stress-relieve at 320°F for 2 hours to remove cutting stress, then hard anodize: 50 microns thickness, 400 HV hardness, which resists sand and carbon dust abrasion.
Inspection Before Every Shipment: CMM Reports You Can Trust
Every Cnc Machined Drone Parts Aluminum order gets a full CMM report — not a random sample. We measure all critical dimensions on a Zeiss Contura G2 with 0.5-micron resolution. For surface finish, we use a Mitutoyo SJ-210 profilometer on every non-visible surface that touches a bearing or fastener. We include these reports as PDFs with your shipment, and we keep them on file for 5 years. If a dimension is out of spec, we scrap the part — we do not rework and ship.
Surface Finish Options That Cut Drag and Reduce Stress Fractures
Standard finish is Ra 0.8 on mating faces and Ra 1.6 on aerodynamic surfaces. For racing drones, we offer Ra 0.4 on leading edges to reduce drag by 12% at 80 km/h. For gimbal arms that carry cameras, we apply a bead-blasted finish (Ra 2.5) to hide fingerprints and reduce reflective glare. We can also leave a raw machined finish if you are doing your own post-coating — just note it in your drawing.
Why We Use 6061-T6 Over 2024 for Heat Sink Drone Parts
Heat sinks on ESCs and motors need high thermal conductivity, not just strength. 6061-T6 has 167 W/m·K thermal conductivity, which is 8% higher than 2024 and 30% higher than 7075. For these parts, we CNC machine fin arrays with 1.5mm fin thickness and 2.5mm pitch, giving you 45% more surface area than die-cast parts. We also add a micro-groove pattern on the base (0.3mm depth) that increases convective heat transfer by 18% in static air tests.
Prototype to Production: Same Fixtures, Same Tolerances
Your first prototype is machined on the same 5-axis DMG MORI that runs your 5,000-piece production order. We use the same soft jaws and vacuum fixtures, so tolerances do not shift when you move from pilot run to volume. There is no MOQ — order 1 piece for proof-of-concept or 10,000 pieces for a fleet rollout. For production, we hold ±0.005mm on all critical features, and we keep a first-article sample in our inspection room for 12 months.
Specification
Value / Range
Materials
6061-T6, 7075-T6, 5052-H32
Size range
5mm x 5mm x 5mm to 500mm x 300mm x 200mm
Hardness (as machined)
24HRC (6061-T6) to 42HRC (7075-T6)
Hardness (after anodize)
400 HV (equivalent to 40HRC surface)
Tolerance (critical bores)
±0.005mm
Tolerance (general)
±0.01mm
Runout (shaft/pilot features)
≤0.01mm
Surface finish (standard)
Ra 0.8 on mating faces, Ra 1.6 elsewhere
Surface finish (optional)
Ra 0.4, bead blast Ra 2.5, micro-groove
Lead time (prototype)
5 working days
Lead time (production)
10-15 working days for 1,000 pcs
MOQ
No MOQ (1 piece accepted)
What is your minimum order quantity for Cnc Machined Drone Parts Aluminum?
There is no MOQ — we accept and machine a single prototype part, so you can test before committing to volume.
Can you customize hole patterns or add threaded inserts for my drone arm design?
Yes — we machine custom hole patterns, countersinks, and press-fit brass or steel threaded inserts (M2, M3, M4) directly from your STEP or IGES file, with no design-for-manufacturing penalty.
How do you ensure quality for long production runs of 5,000+ parts?
We use in-process probing on every part, plus a final CMM check on 10% of the batch; if any part fails, we quarantine the entire lot and re-machine from the same fixture setup.
What is the actual lead time if I need parts shipped to the USA or EU?
Prototype lead time is 5 working days, production is 10-15 days, plus 3-5 days for DHL or FedEx shipping to most international airports — so you can have parts in hand within 3 weeks.
For a firm quote within 12 hours, email sc@bquq.com with your drawing (STEP, IGES, or PDF) and quantity. Prefer chat? WhatsApp +86 13713157787. We reply to every inquiry within 2 business hours, China time (UTC+8). Send your drawing now — we will confirm machinability, tolerances, and price the same day.
Before you send files, check our CNC cutting tool selection guide to understand how tool geometry affects your part’s surface finish, and review the CNC machining tolerances guide to see which of your dimensions can be relaxed to cut cost. Both are written by our shop floor engineers, not marketing.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.