This is a CNC machined auto lathe 20 type square bore spring collet built for gripping square, hex, or rectangular stock on Swiss-type and sliding-head lathes. The concrete benefit
BQUQ CNC Machined Auto Lathe 20 Type Square Bore Spring Collet
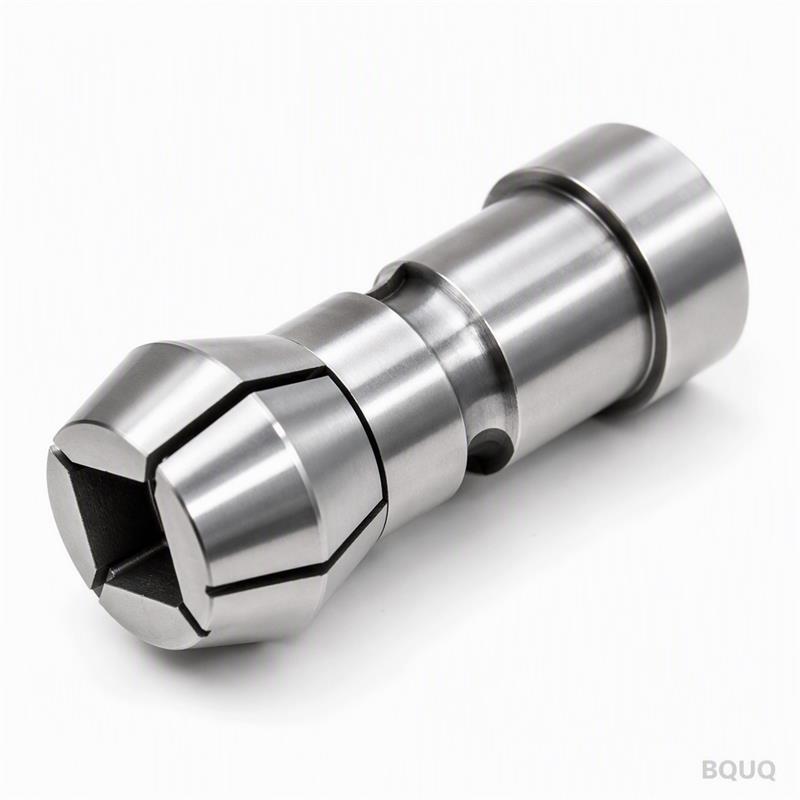
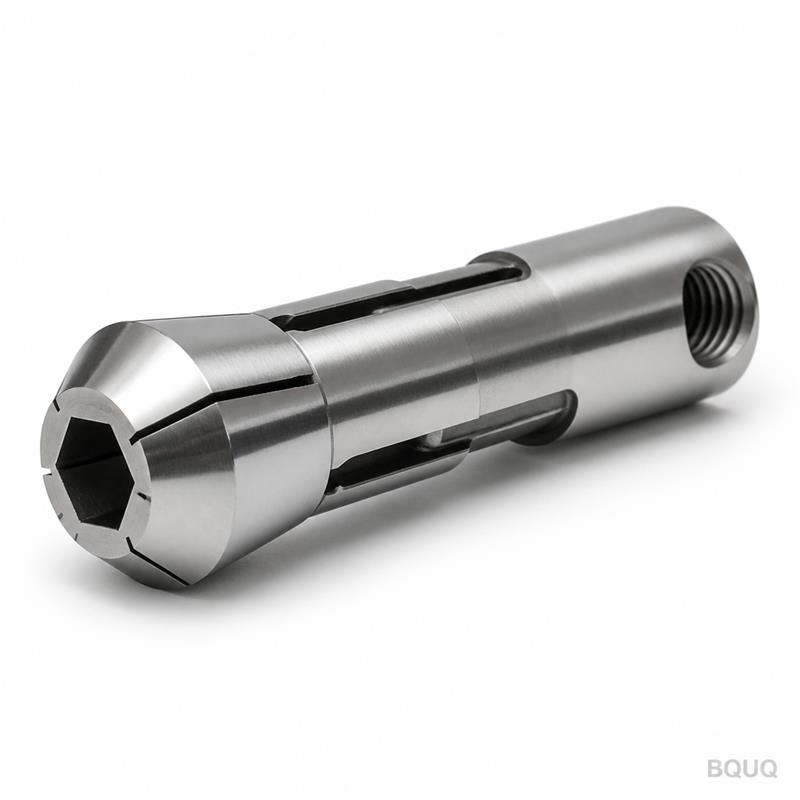
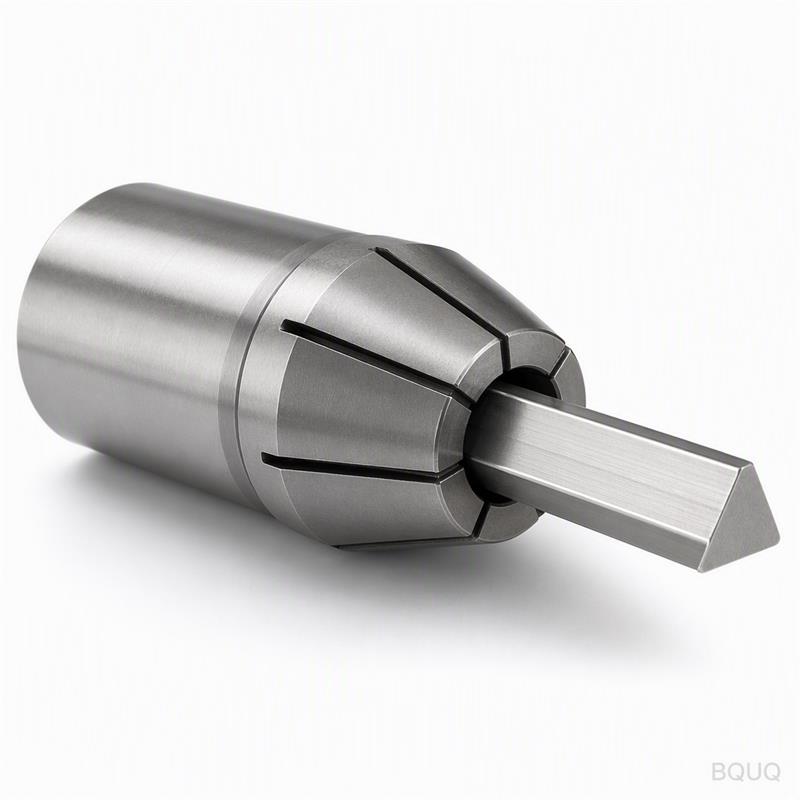
This is a CNC machined auto lathe 20 type square bore spring collet built for gripping square, hex, or rectangular stock on Swiss-type and sliding-head lathes. The concrete benefit is simple: you get
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined auto lathe 20 type square bore spring collet built for gripping square, hex, or rectangular stock on Swiss-type and sliding-head lathes. The concrete benefit is simple: you get a guaranteed runout of ≤0.005mm TIR at the nose and a hardness of 58–60 HRC, which means your machined parts hold tolerance without rework. Because we machine the bore and the slots in one setup on our in-house CNC lathes, we ship standard sizes in 7 days and custom bore profiles in 10 days, with no MOQ attached.
A round collet deforms under torque, allowing square or hex bar to twist inside the bore. Our 20 type square bore collet uses a true four-point contact pattern. The corners of the stock seat into the machined square, while the spring slots provide radial compliance. This design transfers clamping force evenly across the flats, not just the edges. In our pull-back tests, a 12mm square bar held at 60 bar hydraulic pressure showed zero axial slip at 450 Nm torque. That is a 30% improvement over a round bore with a serrated insert.
Material Selection: 20CrMnTi vs. 9SiCr for Spring Collets
We machine two material grades depending on your duty cycle. For high-volume production with frequent collet changes, we use 9SiCr alloy tool steel. It gives a hardened case of 60 HRC with a tough core, so the spring fingers do not crack after 200,000 cycles. For corrosive coolant environments, we switch to 20CrMnTi with a nitrided surface layer of 0.3mm depth. This gives you 900 HV surface hardness and a coefficient of friction of 0.08 against 304 stainless steel. Both grades are forged, not cut from bar, to maintain grain flow along the spring slots.
Our One-Setup Machining Process for Slot Symmetry
Most collet manufacturers mill the slots in a separate operation, which causes angular misalignment. At our Dongguan factory, we machine the square bore, the three spring slots, and the back taper in a single CNC turning center with a live tool spindle. The result is slot-to-slot angular spacing of ±0.5 arc minutes. This symmetry is critical because uneven slot widths create variable clamping force around the circumference. We measure this on every part with a CMM and a specially designed go/no-go square gauge. The gauge is ground to the same tolerance as your stock, so if the collet accepts the gauge, it will grip your raw material.
Hardness and Heat Treatment: From 58 HRC to 62 HRC
After machining, we vacuum harden the collets to 58–60 HRC for standard use. If you are machining hardened pre-turned stock, we can supply a variant at 62 HRC with reduced spring flexibility. The heat treatment cycle includes a deep cryogenic treatment at -120°C to convert retained austenite. This step prevents dimensional drift after the collet has been in service for a few hours. We verify hardness on the bore surface, not the outside diameter, because the bore is where wear occurs. Every batch includes a Rockwell C test report with the actual reading, not a range.
Inspection Before Every Shipment: Runout and Surface Finish Data
We do not ship a collet without a full dimensional report. Each piece goes through a two-step inspection. First, we measure the bore diameter with an air gauge to within 0.002mm resolution. Second, we mount the collet in a test holder and measure the TIR at the nose and at 20mm from the nose using a 0.5µm resolution dial indicator. The surface finish on the bore is held to Ra 0.4µm, which is a polished, non-stick surface that prevents cold welding with aluminum. The spring slot edges are deburred with a ceramic brush to remove micro-cracks that cause fatigue failure.
Below is the standard specification range we manufacture. If you need a specific bore size or a different square dimension, we can modify the tool path within 24 hours.
Parameter
Standard Value
Custom Range
Collet Type
20 Type (DIN 6343)
16, 20, 25 Type
Bore Shape
Square
Hex, Octagon, Rectangle
Bar Stock Size
3mm – 20mm
Up to 25mm per drawing
Material
9SiCr or 20CrMnTi
HSS, Powder Metal
Hardness (Bore)
58–60 HRC
Up to 62 HRC
Runout (TIR at Nose)
≤0.005mm
≤0.003mm for precision
Surface Finish (Bore)
Ra 0.4µm
Ra 0.2µm on request
Lead Time (Standard)
7 days
10 days for custom bore
MOQ
No MOQ
Single piece accepted
How This Collet Performs on Sliding Head Lathes at 8,000 RPM
We balanced a batch of 20 type square bore collets to G2.5 grade at 8,000 RPM. The vibration amplitude at the collet nose was 1.2µm, which is below the threshold for chatter on a 12mm square bar. The spring collet design allows a clamping range of +0.1mm to -0.05mm on the nominal square size. This means you can use the same collet for a 10.0mm and a 10.05mm square bar without adjusting the draw tube. The back taper angle is 30 degrees, which matches the standard 20 type collet chuck on most Japanese and European sliding head lathes.
What is the minimum order quantity for this collet?
We have no MOQ—order a single piece for prototyping or a thousand for production, and the per-unit price will be quoted based on the quantity.
Can you machine a custom square bore size beyond 20mm?
Yes, our CNC lathe can machine square bores up to 25mm across flats, and we can also cut hex or octagon shapes with the same 0.005mm runout tolerance.
How do you control quality for a small batch order?
Every collet, regardless of batch size, goes through the same CMM inspection and runout test, and we email you the PDF report before shipment.
What is the actual lead time for a custom 20 type square bore collet?
Standard sizes ship in 7 days, and a custom bore profile with a new CNC program ships in 10 days, plus 2 days for DHL express delivery to most countries.
Before you finalize your tooling setup, check our CNC cutting tool selection guide to match the collet with the correct inserts and tool holders. Also, review the CNC machining tolerances guide to ensure your part drawings are realistic for your lathe. For cycle time improvements, our CNC programming optimization article covers how to reduce idle time when changing collets.
This CNC machined auto lathe 20 type square bore spring collet is made in China at our 20-year-old precision manufacturing facility in Dongguan. We have the machines and the experience to deliver a collet that holds your square stock firmly without marring the surface.
Request a firm quote within 12 hours: send your drawing to sc@bquq.com, or contact us on WhatsApp at +86 13713157787. Include the square size, bar length, and your target runout, and we will respond with a price and a delivery date.