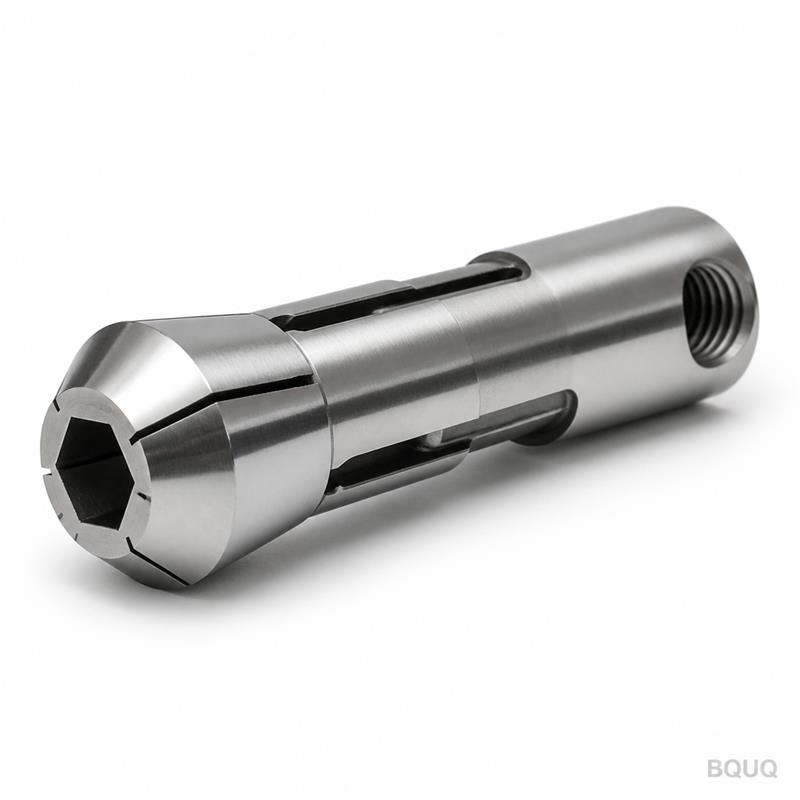
This is a CNC collet chuck built for auto lathe 46 type spindles, specifically machined to grip hex bar stock through an extended nose. You get a guaranteed runout of 0.008 mm TIR
BQUQ CNC Machined Auto Lathe 46 Type Hex Bore Extended Collet
This is a CNC collet chuck built for auto lathe 46 type spindles, specifically machined to grip hex bar stock through an extended nose. You get a guaranteed runout of 0.008 mm TIR (total indicated rea
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC collet chuck built for auto lathe 46 type spindles, specifically machined to grip hex bar stock through an extended nose. You get a guaranteed runout of 0.008 mm TIR (total indicated reading) and a bore tolerance of +0.005 / -0.000 mm, with a surface finish of Ra 0.4 on the gripping surface. Lead time is 7 working days for standard sizes, 12 days for custom hex bores—no MOQ, direct from BQUQ’s factory in Dongguan, China.
Why an Extended Nose Matters for Hex Bar Stock
Standard collets sit flush with the spindle nose, forcing you to cut hex stock close to the chuck face. That limits tool clearance and risks chatter. Our extended collet adds 25 mm of reach beyond the spindle face, letting you machine longer hex sections without re-chucking. This reduces setup time by roughly 30% on multi-step parts like valve stems and hex nuts. The extended bore is hardened and ground as one piece, so it does not flex under radial load.
Materials and Heat Treatment We Use
We make the body from 20CrMnTi carburizing steel. It gets carburized to a depth of 0.8–1.0 mm, then hardened to 58–60 HRC. The gripping surface is ground after heat treatment, not before—this removes decarburized layers and keeps the hex corners sharp. For stainless-tough jobs, we offer a variant in 9Cr18MoV hardened to 54–56 HRC with better corrosion resistance. Every collet is cryogenically treated at -80°C for 2 hours to stabilize the microstructure, preventing drift during high-speed auto lathe cycles.
Hex Bore Geometry: Sharp Corners, No Interference
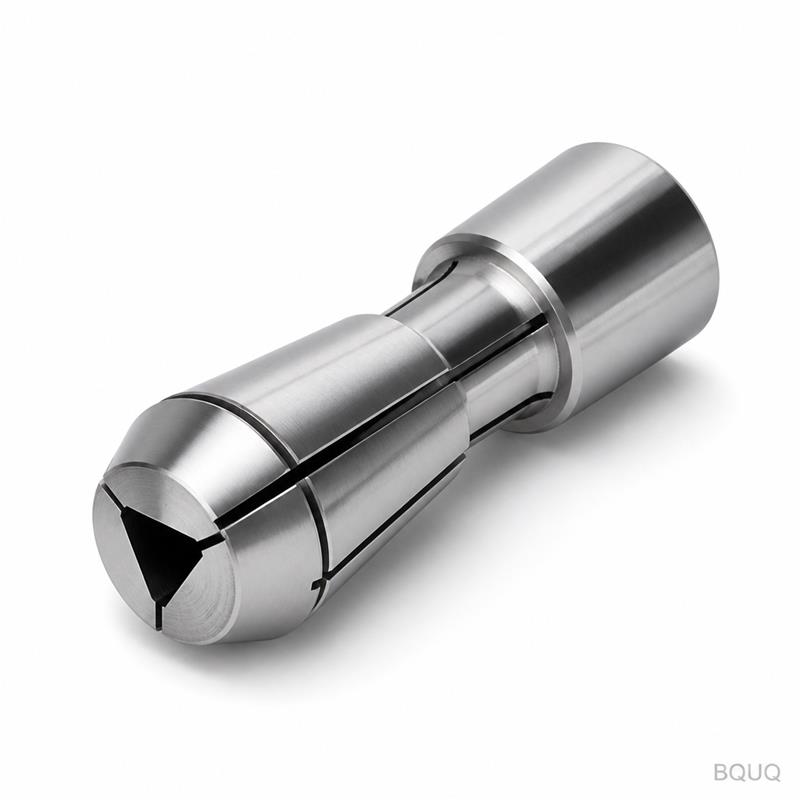
Your hex bar needs exact 60° internal angles. We machine each corner with a radius of 0.1 mm max, which supports the bar without stress risers. The bore is relieved by 0.02 mm over the last 5 mm of the nose to reduce binding when bars are fed through. We check every angle with a profile projector at 20x magnification. If you machine 1/4-inch hex, 3/8-inch hex, or metric equivalents (S6, S8, S10), we hold across-flats tolerance to ISO h8. For custom hex sizes, we cut the bore with a wire EDM before final grinding—this gives a mirror finish on the flanks, not just the outer surface.
Runout Control: How We Hold 0.008 mm TIR
Runout comes from two places: the collet’s own bore and its taper seat. We grind the 46 type taper (10° included angle) in the same setup as the bore, using a single-point diamond dresser on the machine. This eliminates the indexing error between operations. After grinding, we assemble the collet into a test spindle and measure TIR at three points: the nose tip, mid-bore, and rear taper. Only collets under 0.008 mm TIR pass. That is twice as tight as the 0.015 mm typical for off-the-shelf extended collets.
Inspection Before Every Shipment
Each collet gets a CMM (coordinate measuring machine) report with 12 measured points: hex across-flats, taper angle, bore runout, and surface finish. We also do a practical test—we load a 100 mm length of hex bar and check it for rotation under 2 N·m of torque. The report is attached to your shipment as a PDF, plus we keep it on file for 3 years. If you need PPAP Level 3 or a material certificate (EN 10204 3.1), we provide that at no extra cost.
Compatibility with Auto Lathe 46 Type Spindles
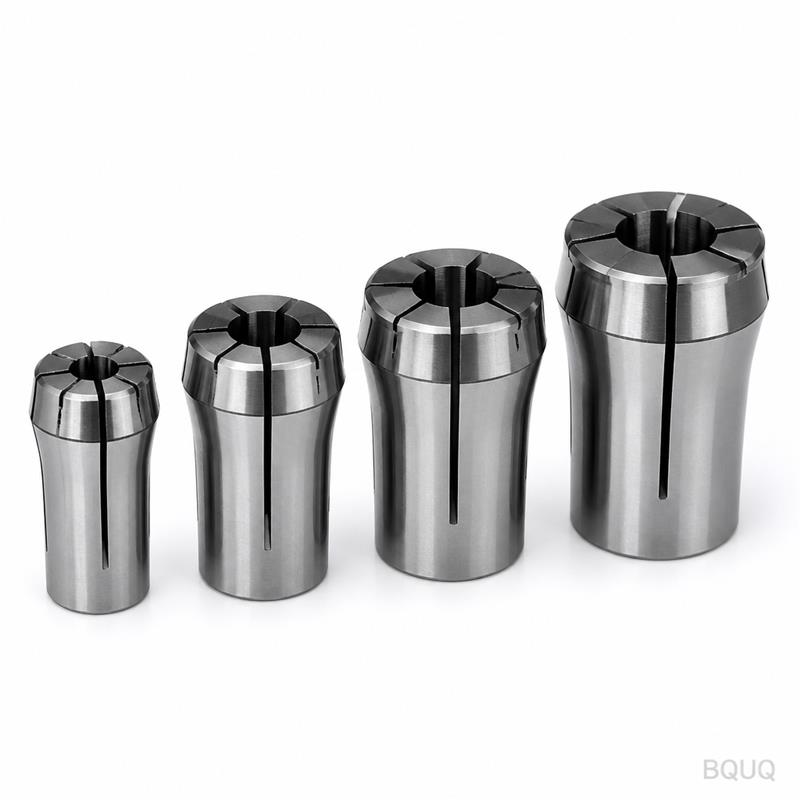
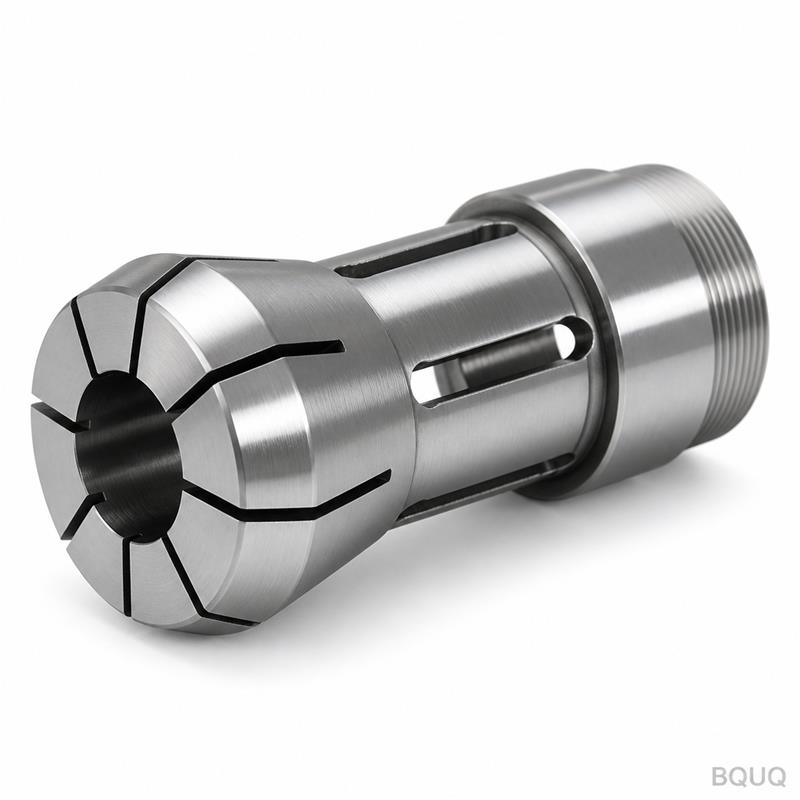
This collet fits the standard 46 type spindle nose—common on Tornos, Citizen, and Star sliding-head lathes that use a 10° taper mount. The outer diameter is 46.0 mm, with a length of 80 mm (standard) or 105 mm (extended reach). The thread at the rear is M16x1.5 for the draw tube. We stock blanks for 12 standard hex sizes: S4, S5, S6, S7, S8, S9, S10, S11, S12, S14, S16, S17. If your spindle uses a different thread, we can modify the rear thread in-house for a small setup fee. See our CNC cutting tool selection guide to match collet material with your workpiece hardness.
Pricing, MOQ, and Lead Time—Straight Numbers
No MOQ. You can order one piece for prototyping. Standard hex sizes start at $28 per piece for quantities of 1–10, dropping to $19 for 100+ pieces. Custom hex bores (non-standard across-flats) add $12 for wire EDM time. Lead time: 7 working days for standard sizes, 12 working days for custom bores. For urgent orders, we can rush a standard size in 3 days with a 30% expedite fee. We ship DHL or FedEx from Dongguan, China, and the packing is foam-lined plastic tubes to prevent edge damage.
Specification
Value
Body material
20CrMnTi (carburized) or 9Cr18MoV
Hardness
58–60 HRC (20CrMnTi) / 54–56 HRC (9Cr18MoV)
Carburizing depth
0.8–1.0 mm
Hex bore tolerance
ISO h8 (e.g., S8 = 8.000/7.964 mm)
Runout (TIR)
≤ 0.008 mm
Surface finish (bore)
Ra 0.4 µm
Taper angle
10° included, ground in one setup
Outer diameter
46.0 mm (+0.000/-0.010 mm)
Length (standard / extended)
80 mm / 105 mm
Rear thread
M16x1.5 (customizable)
Standard hex sizes
S4 to S17 (12 sizes)
Lead time
7 days (standard), 12 days (custom)
MOQ
1 piece (no MOQ)
FAQ
What is your minimum order quantity for this collet?
No MOQ—you can order a single piece for testing, and we keep the same unit price down to 1 piece.
Can you make a custom hex bore size not in your standard list?
Yes, we cut any hex size from S3 to S20 with wire EDM, and the lead time increases from 7 to 12 working days.
How do you verify runout before shipping?
We measure TIR on a test spindle at three points (nose, mid-bore, rear taper) using a 0.001 mm dial indicator, and only collets under 0.008 mm pass.
What is your typical lead time for a standard 46 type extended collet?
7 working days for any standard hex size, shipped via DHL or FedEx from our Dongguan factory.
If you need a collet that holds hex stock without vibration or re-chucking, send your drawing or hex size. We will reply with a firm quote within 12 hours, including the CMM inspection report template and shipping cost. Email sc@bquq.com or WhatsApp +86 13713157787. For more on how to select the right toolholder geometry, read our CNC cutting tool selection guide, and to understand tight tolerances in your part design, check the CNC machining tolerances guide.
BQUQ is a precision manufacturing company with 20 years of experience in CNC machining, stamping, springs, and heat sinks, based in Dongguan, China. All collets are 100% made in China and inspected before packing.