What This Chuck Does Differently: 0.005mm TIR Runout, 58 HRC, 15-Day Lead This is a CNC Machined Auto Lathe Synchronized Collet Chuck engineered for high-volume turning and grindi
What This Chuck Does Differently: 0.005mm TIR Runout, 58 HRC, 15-Day Lead This is a CNC Machined Auto Lathe Synchronized Collet Chuck engineered for high-volume turning and grinding operations where
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Chuck Does Differently: 0.005mm TIR Runout, 58 HRC, 15-Day Lead
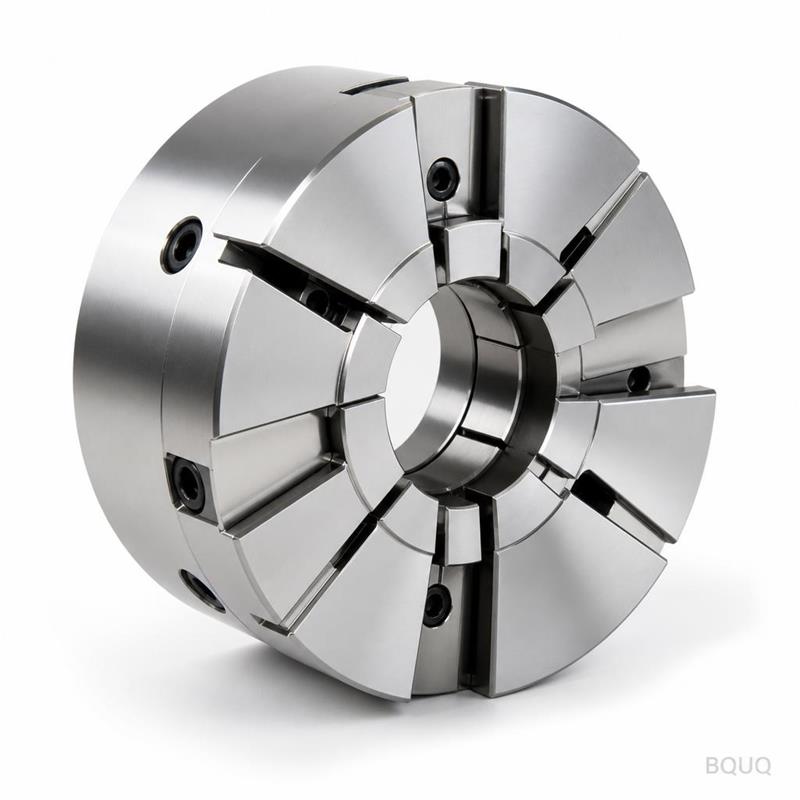
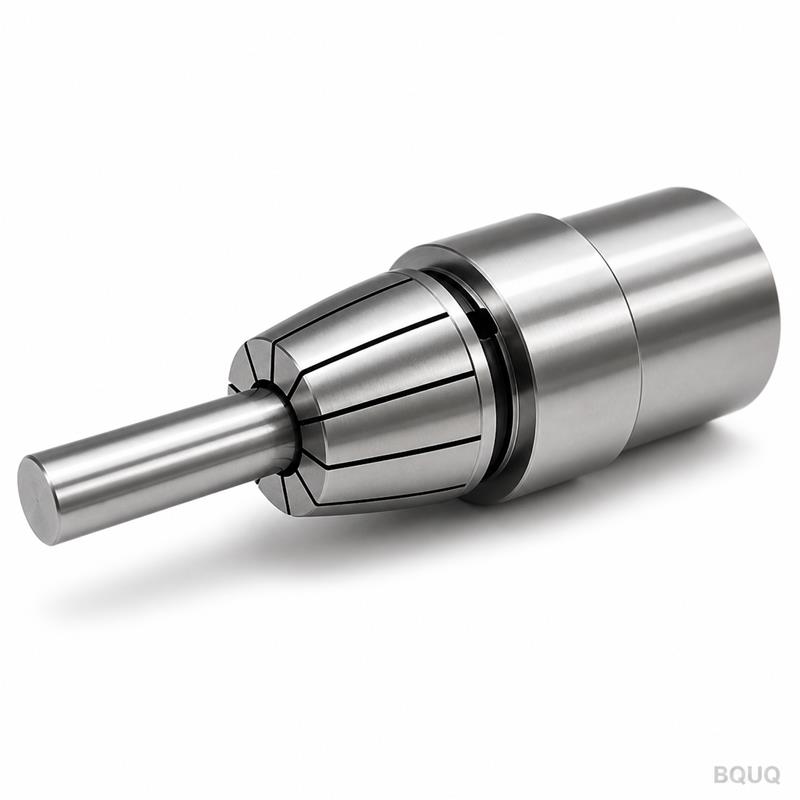
This is a CNC Machined Auto Lathe Synchronized Collet Chuck engineered for high-volume turning and grinding operations where concentricity cannot be compromised. The synchronized collet mechanism closes all segments evenly, holding round bar stock and pre-machined parts with a total indicated runout (TIR) of 0.005mm or better. You get repeatable clamping force without part distortion, and because we machine the body and collet seat in one clamping setup, you avoid the stacking tolerances found in multi-vendor assemblies. Typical lead time from drawing approval to shipment is 15 working days, with no MOQ for standard sizes.
Precision manufacturing in our Dongguan facility means every chuck body starts as 42CrMo steel, heat-treated to 58-60 HRC, then ground to a surface finish of Ra 0.4µm on the taper and gripping surfaces. That combination gives you tool life and part consistency that off-the-shelf import chucks cannot match.
How Synchronized Collet Segments Eliminate Uneven Gripping
Standard collet chucks rely on a single taper wedge, which can shift the workpiece if the collet is worn or the drawbar pulls unevenly. The synchronized design uses a ring gear and three or six slotted segments that move radially at identical speed and distance. Each segment travels the same amount per revolution of the actuation sleeve, so the gripping force vector stays perfectly centered on the spindle axis.
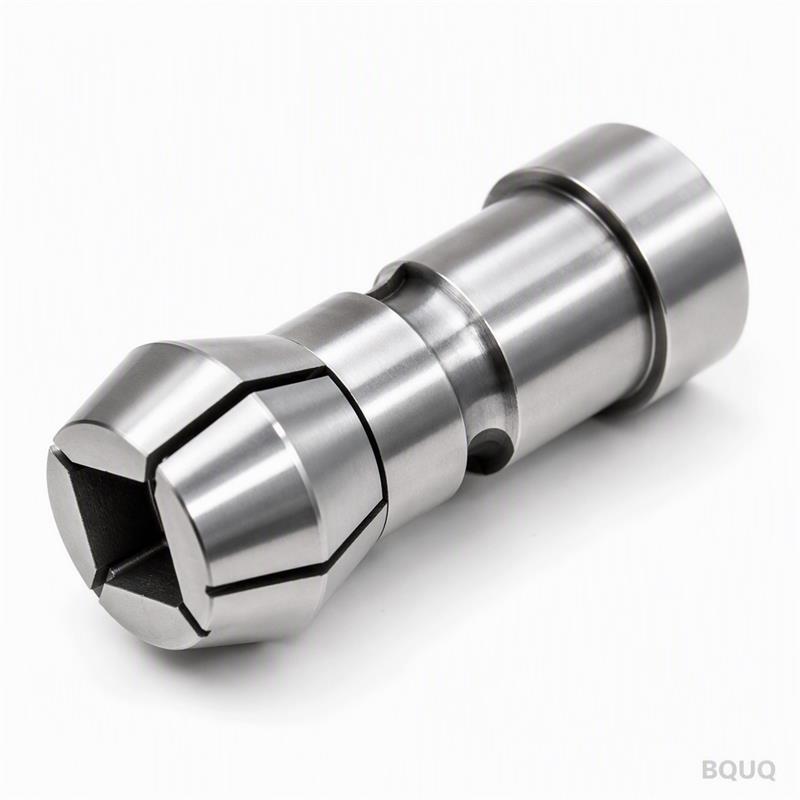
This matters when you are machining thin-walled parts or holding hex and square stock. Uneven clamping creates vibration marks and ovality. Our synchronized mechanism holds roundness within 0.003mm on a 25mm diameter bar, verified by a Marposs gauge before packing. The collet seat angle is 16 degrees, standard for DIN 6499, but we can customize the nose profile to match your spindle nose or existing drawtube.
Materials and Heat Treatment We Use for the Chuck Body and Collet
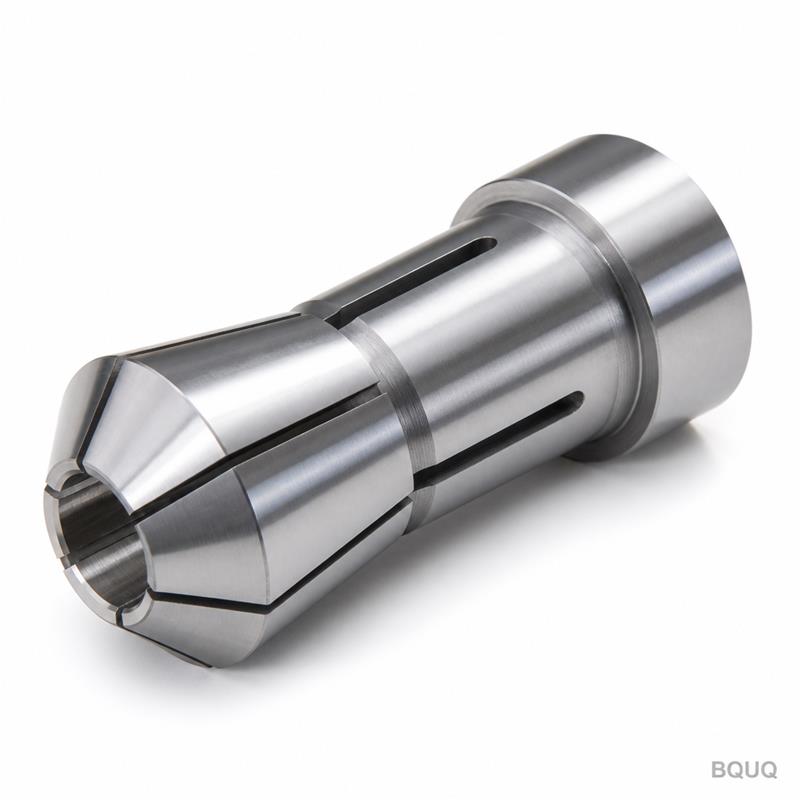
We do not cut corners on steel grade. The chuck body is 42CrMo (AISI 4140) quenched and tempered to 28-32 HRC for the base, then the gripping area is induction-hardened to 58-60 HRC. This dual hardness gives you a tough, shock-resistant body with a wear-resistant gripping surface. The collet itself is made from 65Mn spring steel, hardened to 45-50 HRC, then the slots are laser-cut and deburred to prevent burr transfer onto your workpiece.
For corrosive environments or stainless steel workpiece handling, we offer an optional electroless nickel plating on the entire body (thickness 0.02mm) that does not affect the taper accuracy. We have a full in-house heat treatment line, so the hardening and tempering cycles are logged with timestamps—not outsourced to a third party that might skip steps. Surface finish on the OD and taper is Ra 0.4µm, and the back plate mounting surface is lapped to Ra 0.2µm.
Inspection Before Every Shipment: Runout, Hardness, and Pull-Back Force
Every unit goes through a three-stage inspection. First, we measure the taper angle with a sine bar and dial indicator—must be within ±0.002mm over the full taper length. Second, we assemble the chuck on a test spindle and measure TIR at the nose using a 25mm ground test bar; we reject anything above 0.005mm. Third, we measure pull-back force with a load cell at 40 bar hydraulic actuation pressure and verify it matches your specified clamping force, typically 15-20 kN for a 25mm collet.
We also check the collet slot width with a pin gauge to ensure the slots do not close completely under force, which would cause permanent deformation. Each chuck ships with a signed inspection report, including runout values, hardness test results, and a photo of the final gauge reading. If you need a full material certificate (EN 10204 3.1), it is available at no extra cost.
Specifications: Sizes, Tolerances, and Delivery Terms
Parameter
Value / Range
Collet type
DIN 6499 ER16 / ER20 / ER25 / ER32 / ER40
Body material
42CrMo (AISI 4140), induction-hardened
Collet material
65Mn spring steel, 45-50 HRC
Body hardness
58-60 HRC (gripping area)
Runout TIR (at nose)
≤ 0.005mm (0.0002")
Concentricity repeatability
≤ 0.003mm over 20 clamp cycles
Surface finish (taper and OD)
Ra 0.4µm
Gripping range (ER32)
2.0 – 20.0mm
Max actuation pressure
60 bar
Lead time (standard sizes)
15 working days
MOQ
No MOQ for standard sizes (custom: 5 pcs)
For custom spindle nose mounting (e.g., A2-4, A2-5, or threaded nose), we adjust the back plate and can match your existing drawtube thread. The chuck body is balanced to G2.5 at 6000 RPM, suitable for most CNC lathe and auto lathe applications. If you are working with exotic materials, check our CNC cutting tool selection guide to pair this chuck with the right tooling.
What is your MOQ for a custom chuck size?
No MOQ for standard ER collet sizes (ER16-ER40); custom spindle nose or non-standard bore requires 5 pieces.
Can you customize the drawtube thread or back plate?
Yes, we machine the back plate and drawtube thread to match your lathe's spindle nose and actuator rod, with a tolerance of ±0.02mm on thread pitch.
How do you verify runout before shipment?
We use a Marposs gauge with a ground test bar; the signed inspection report is included in every shipment, and we reject anything above 0.005mm TIR.
What is your average lead time for a repeat order?
Repeat orders for standard sizes ship in 10 working days; first-time custom orders take 15 working days including drawing approval.
Why Precision Manufacturing in Our Dongguan Factory Beats Assembly-Based Suppliers
Many so-called collet chuck suppliers buy cast bodies and off-the-shelf collets, then assemble them without any machining. Our factory does the full cycle: CNC turning, milling, heat treatment, grinding, and assembly under the same roof. That means we control the taper angle, the slot geometry, and the heat treatment curve. We do not rely on a third-party collet that might have a different hardness or slot width.
This vertical integration also shortens your lead time. We have 40 CNC machines, including two 5-axis grinding centers, dedicated to chuck production. If you have a drawing, our engineers review it for manufacturability and send you a DFM report within 24 hours. We also make the springs and heat sinks in-house, so you can consolidate your vendor list for other precision parts. For tolerance fundamentals, refer to our CNC machining tolerances guide to understand how we hold these numbers.
Packing, Documentation, and Shipping for Global Orders
Each chuck is individually wrapped in anti-rust paper, placed in a foam-lined wooden box, and sealed with a desiccant bag. For orders over 10 pieces, we use a plywood crate with a shock-absorbing base. We ship via DHL, FedEx, or sea freight (FOB Shenzhen). Standard export packing includes the inspection report, a material certificate (if requested), and a part number label with your PO number.
We have shipped to engineering firms in Germany, the US, and Japan for the past 8 years, and our return rate is below 0.5% due to dimensional defects. If any unit fails your incoming inspection, we replace it within 7 days and cover the freight cost. That is our guarantee, not a marketing line.
Get a Firm Quote Within 12 Hours—Send Your Drawing Today
Send us your 2D drawing or 3D model (STEP, IGES, or PDF) for the CNC Machined Auto Lathe Synchronized Collet Chuck you need. We will respond with a firm quote, including unit price, tooling cost (if any), and delivery date, within 12 hours. For standard ER sizes, we can quote immediately from stock material without needing a drawing. We are a precision manufacturing source made in China, but we answer like a local supplier—fast, in English, with clear technical communication.
Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. No MOQ for standard sizes, and you will receive a DFM comment on any custom feature within 24 hours. Let us prove what a synchronized collet chuck should feel like.