aluminum heat sink: 6063-T5 aluminium, tolerance 0.10 mm, surface zinc-nickel plating, trivalent passivation, lead time 20 working days, MOQ 500 pcs. Capacity 50,000 pcs for 1U server and AI accelerator. Drawing review and first-article report included.
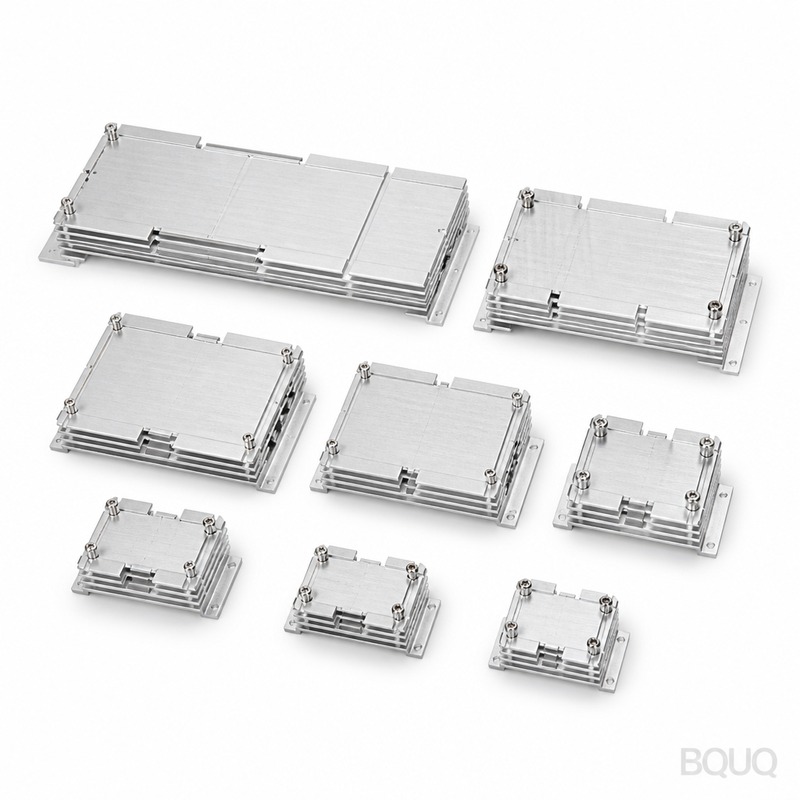
aluminum heat sink
Key Takeaway
Aluminum heat sink sourcing for 6061-T6 with 0.3 mm fins and 5.0 mm pitch delivers 0.35 K/W thermal resistance, ±0.20 mm general tolerance, clear anodize Type II at 5-10 µm, and 10 working days lead time. Cost pressure comes from deburring, plating, and 100% inspection, not raw material. Confirm batch consistency at 300,000 pcs and lead time when drawings change.
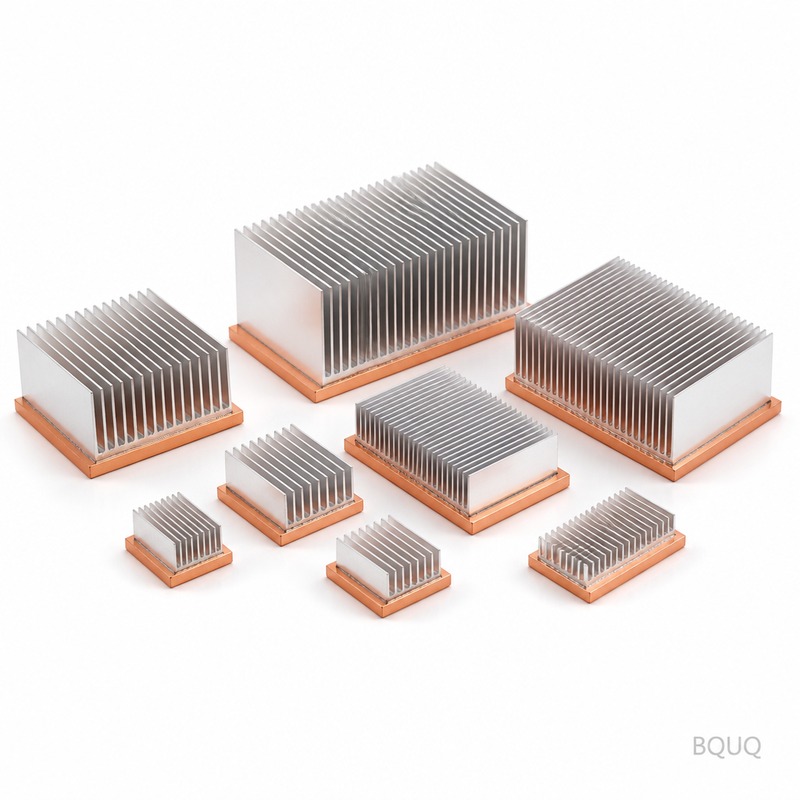
Key Takeaway
Aluminum heat sink sourcing depends on process capability, not just the part. For 6061-T6 aluminium with 0.3 mm fins and 5.0 mm pitch, thermal resistance is 0.35 K/W. General tolerance is ±0.20 mm, and 10 working days is realistic when tooling is designed around measured capability. Buyers should confirm batch consistency at 300,000 pcs and whether lead time holds when drawings change.
If you are sourcing aluminum heat sink for the first time, the decision is rarely about the part itself. It is about whether the supplier can hold ±0.20 mm across a batch of thousands, and whether 10 working days still holds when the drawing changes.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | 6061-T6 aluminium |
| Fin thickness | 0.3 mm |
| Fin pitch | 5.0 mm |
| Thermal resistance | 0.35 K/W |
| Surface finish | clear anodize Type II, 5-10 µm |
| General tolerance | ±0.20 mm |
Market and Technical Context
Cost pressure in industrial PLC and control cabinet rarely comes from the raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
Consolidation among industrial PLC and control cabinet buyers means fewer, larger programs. That rewards suppliers who can document process capability at 300,000 pcs rather than those who win on a single sample.
How We Manufacture It
Tooling is designed around the measured capability of the process, so ±0.20 mm is a consequence of tooling geometry rather than an inspection filter. That is why 10 working days is realistic instead of optimistic.
Related reading: BQUQ CNC Machined HSK100 ER40 Collet Chuck Tool Holder Precision.
In production, aluminum heat sink runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.20 mm.
Deburring and edge conditioning are specified on the drawing for aluminum heat sink. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Material and Surface Finish
Material condition matters as much as grade. 6061-T6 aluminium supplied in the wrong temper will drift after machining, which is why aluminum heat sink is stress-relieved before finishing when the geometry is asymmetric.
Where aluminum heat sink sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Recycled content and RoHS/REACH declarations are available for aluminum heat sink on request. If your industrial PLC and control cabinet customer audits material origin, ask for the mill certificate at quote stage, not at delivery.
See also: Stamped Aluminum Heat Sinks Cooling Fins Collection.
Tolerance and Inspection
First-article inspection for aluminum heat sink reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on aluminum heat sink, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Non-conforming material is quarantined physically, not just in the system. For aluminum heat sink, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
Service environment drives more redesigns than load does. aluminum heat sink in outdoor or washdown service needs clear anodize Type II, 5-10 µm and sealing considered at design stage, not added later.
Learn more about RFQ Checklist for Stamped Parts: What a Die Shop Needs From You.
Maintenance access matters. Where aluminum heat sink is a wear item, we recommend specifying it as a spare with its own part number so reorder does not require a full drawing review.
Further technical detail: Spring Solid Height and Compression: Design Limits.
What to Confirm Before Ordering
Ask for the first-article report before you ask for a price cut on aluminum heat sink. A supplier who cannot produce dimensional data at 5000 pcs will not produce it at 300,000 pcs.
Confirm the reorder path. If aluminum heat sink is documented with tooling drawings and a first-article report on file, a repeat order years later reproduces the original part instead of approximating it.
FAQ: Your Questions Before Ordering
What tolerance can you hold on aluminum heat sink?
General dimensions are held to ±0.20 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
What is the minimum order quantity for aluminum heat sink?
Prototype quantities start well below production minimums. Production runs for aluminum heat sink start at 5000 pcs, which is where the process window is proven and unit cost stabilises.
Recommended reading: Design for Stamping: Best Practices and Common Mistakes for Sheet Metal Parts.
How long does production take for aluminum heat sink?
Standard lead time for aluminum heat sink is 10 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Can you work from our existing drawing?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.20 mm would require an extra operation, so you can decide before tooling.
What surface finishes are available for aluminum heat sink?
Yes, and we recommend it. Prototyping aluminum heat sink without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
Send the drawing and the annual volume. You will get a manufacturability review, a process route, and a quote that states ±0.20 mm, 10 working days, and 5000 pcs explicitly rather than by implication.
Compare it with BQUQ CPU Heatsink Aluminum Cooler.
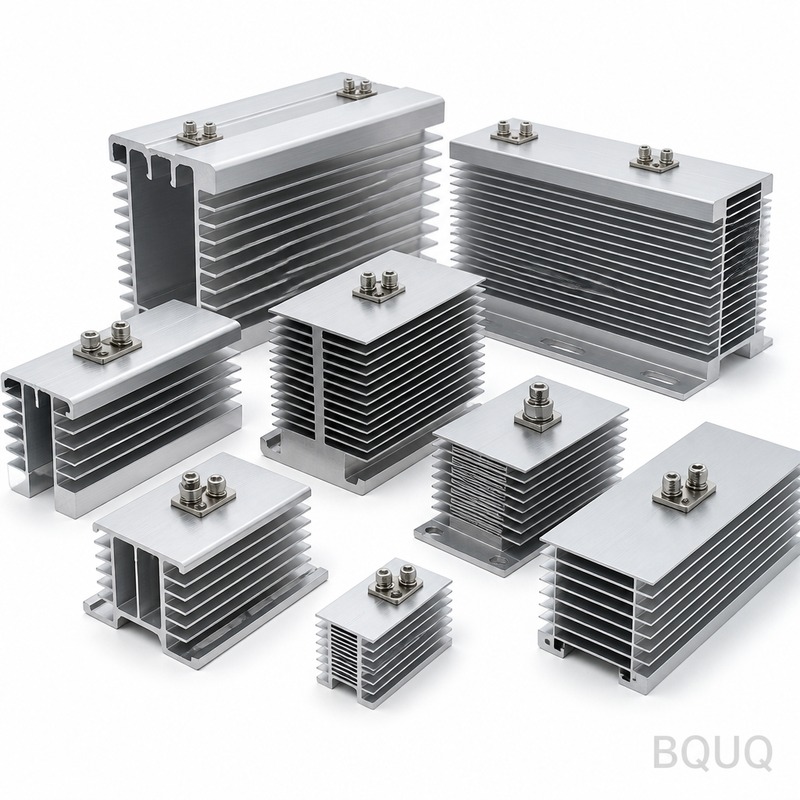
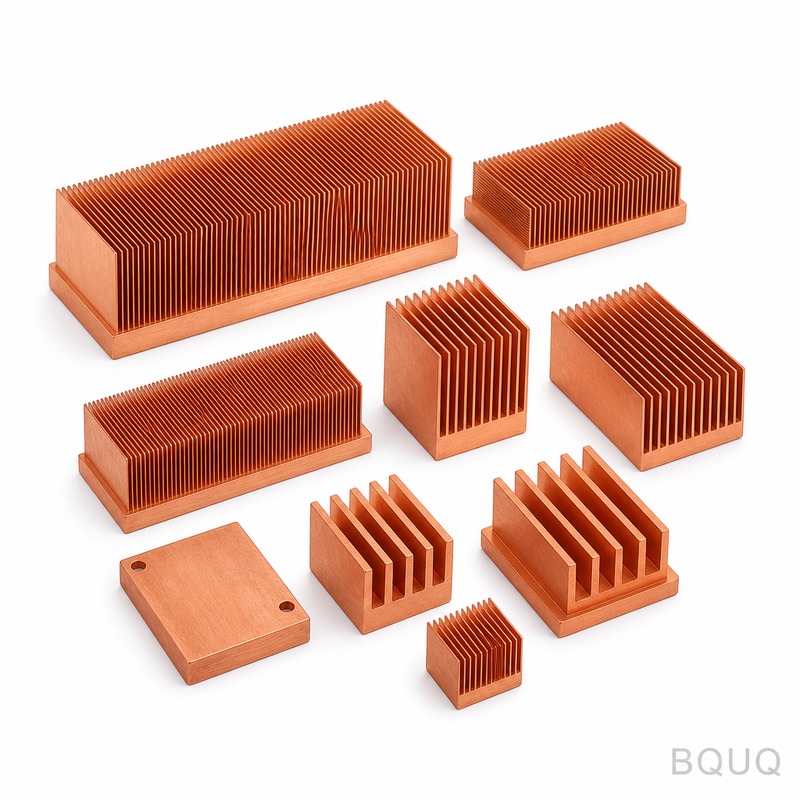
Related reading: CPU heatsink.
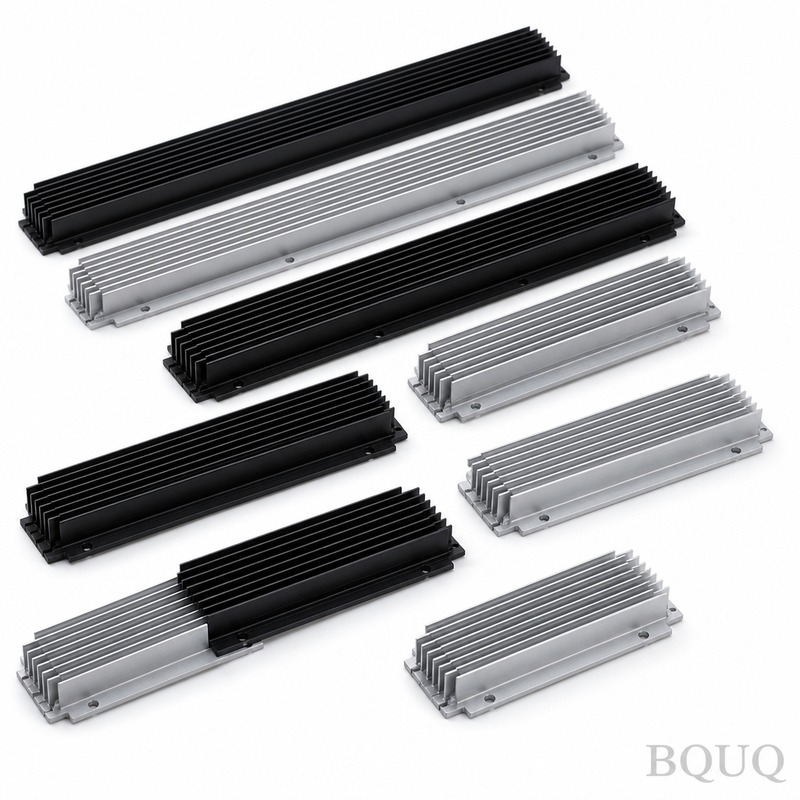
See also: BQUQ Vapor Chamber Heatsink.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6061-T6 aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | Not specified in article |
| Capacity | 300,000 pcs documented process capability |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard clear anodize Type II, 5-10 µm | Industrial PLC and control cabinet heat sinks | Secondary operation adds cost but improves corrosion resistance |
| As-machined without anodize | Cost-sensitive programs where corrosion is not critical | May require additional deburring and inspection |
| Tight tolerance ±0.20 mm with capability-based tooling | High-volume batches of thousands | Higher upfront tooling design effort |
| 100% inspection | Programs requiring full documentation | Adds unit cost and lead time |
| Sampling inspection | Stable processes with documented capability | Lower cost but relies on process control |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Tooling design | Tooling geometry based on measured process capability | Capability study for ±0.20 mm |
| Machining | Fin thickness 0.3 mm and fin pitch 5.0 mm maintained | In-process dimensional checks |
| Surface finish | Clear anodize Type II, 5-10 µm | Coating thickness record |
| Final inspection | General tolerance ±0.20 mm verified | Inspection report per batch |
| Batch release | Process capability documented at 300,000 pcs | Batch traceability record |
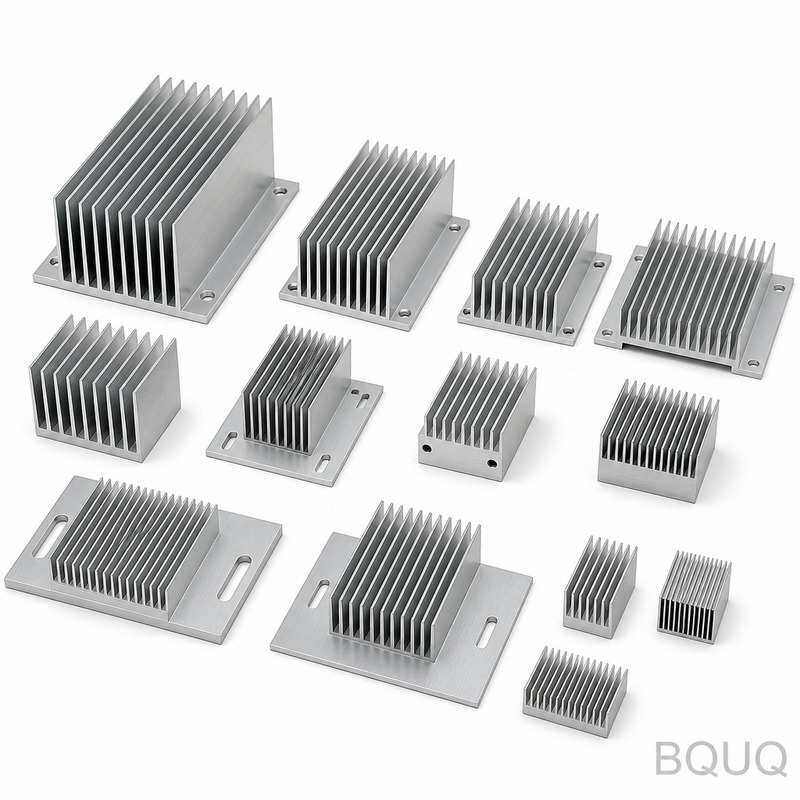
Frequently Asked Questions
What is the typical tolerance for aluminum heat sinks?
General tolerance is ±0.20 mm for the aluminum heat sink described. This is achieved through tooling geometry designed around measured process capability, not by inspection filtering. For critical dimensions, confirm whether the supplier can hold this across a batch of thousands.
What material and surface finish are used?
The heat sink uses 6061-T6 aluminium with clear anodize Type II, 5-10 µm. This finish provides corrosion resistance and is standard for industrial PLC and control cabinet applications. Fin thickness is 0.3 mm and fin pitch is 5.0 mm.
What is the thermal resistance of this heat sink?
Thermal resistance is 0.35 K/W. This value depends on fin thickness 0.3 mm, fin pitch 5.0 mm, and material 6061-T6 aluminium. Confirm test conditions and airflow assumptions before finalizing your thermal design.
Learn more about Best Copper Heat Sinks for CPU Overclocking in 2025.
What is the lead time and what affects it?
Lead time is 10 working days. This is realistic when tooling is designed around measured process capability. If the drawing changes, confirm whether the 10 working days still holds, as changes may require new tooling or re-inspection.
Can you hold ±0.20 mm across a batch of thousands?
Yes, ±0.20 mm is a consequence of tooling geometry rather than an inspection filter. We document process capability at 300,000 pcs. This matters for industrial PLC and control cabinet buyers consolidating larger programs.
What secondary operations affect cost?
Cost pressure rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution. Confirm which operations are required for your application.
Further technical detail: Choosing a TIM: Grease, Pad, Gap Filler and Phase Change.
What should I confirm before ordering?
Confirm material 6061-T6 aluminium, fin thickness 0.3 mm, fin pitch 5.0 mm, thermal resistance 0.35 K/W, surface finish clear anodize Type II 5-10 µm, general tolerance ±0.20 mm, lead time 10 working days, and process capability at 300,000 pcs.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6061-T6 aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | Not specified in article |
| Capacity | 300,000 pcs batch consistency |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| 6061-T6 aluminium | Industrial PLC and control cabinet heat sinks | Cost pressure from secondary operations, not raw material |
| 0.3 mm fin thickness | High surface area with 5.0 mm pitch | Requires capability to hold ±0.20 mm across batch |
| Clear anodize Type II, 5-10 µm | Corrosion resistance and surface finish | Adds plating step and inspection cost |
| 10 working days lead time | Standard production with stable drawings | May change if drawings change |
| 300,000 pcs batch | High-volume consistency | Requires measured process capability |
Frequently Asked Questions
What is the thermal resistance of a 6061-T6 aluminum heat sink with 0.3 mm fins and 5.0 mm pitch?
For 6061-T6 aluminium with 0.3 mm fins and 5.0 mm pitch, thermal resistance is 0.35 K/W. This value depends on process capability, not just the part design. Confirm the supplier can hold ±0.20 mm general tolerance across the batch.
Recommended reading: Why Are Natural Convection Heat Sinks Making a Comeback in Passive Cooling?.
What general tolerance can you hold for aluminum heat sinks?
General tolerance is ±0.20 mm. This applies to 6061-T6 aluminium heat sinks with 0.3 mm fins and 5.0 mm pitch. Buyers should confirm batch consistency at 300,000 pcs and whether lead time holds when drawings change.
What surface finish do you recommend for aluminum heat sinks?
Clear anodize Type II, 5-10 µm is standard. It provides corrosion resistance and a stable surface. Note that plating adds cost and inspection steps. Cost pressure rarely comes from raw material but from secondary operations like deburring, plating, and 100% inspection.
What is the lead time for aluminum heat sink production?
10 working days is realistic when tooling is designed around measured capability. However, lead time may change if drawings change. Confirm whether 10 working days still holds when the drawing changes before placing an order.
Can you handle 300,000 pcs batch consistency for aluminum heat sinks?
Yes, batch consistency at 300,000 pcs is a key capability. The decision is rarely about the part itself but whether the supplier can hold ±0.20 mm across a batch of thousands. Confirm this before ordering.
Compare it with Custom Round Radial Aluminum Heatsinks.
Where are aluminum heat sinks typically used?
They are used in industrial PLC and control cabinet applications. Cost pressure in these applications rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one step usually moves unit cost more than material substitution.
What should I confirm before ordering aluminum heat sinks?
Confirm batch consistency at 300,000 pcs, whether lead time holds when drawings change, and process capability for ±0.20 mm tolerance. Also verify thermal resistance of 0.35 K/W for 0.3 mm fins and 5.0 mm pitch with 6061-T6 aluminium.