ssd heat sink: copper-alloy CuZn37, tolerance 0.20 mm, surface black anodize Type II, 10-15 µm, lead time 15 working days, MOQ 1000 pcs. Capacity 120,000 pcs for IGBT power module. Drawing review and first-article report included.
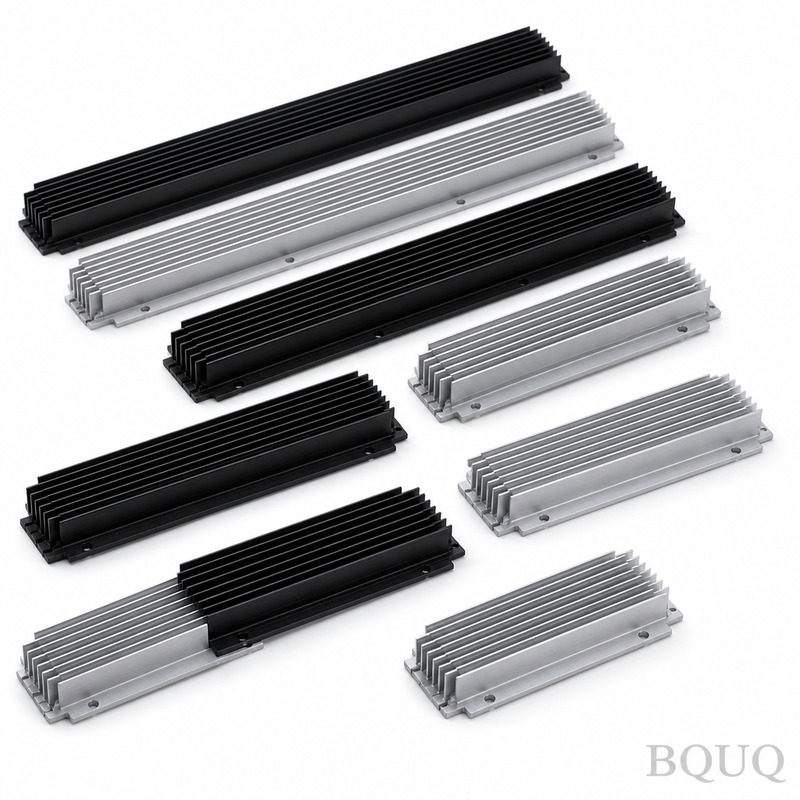
ssd heat sink
Key Takeaway
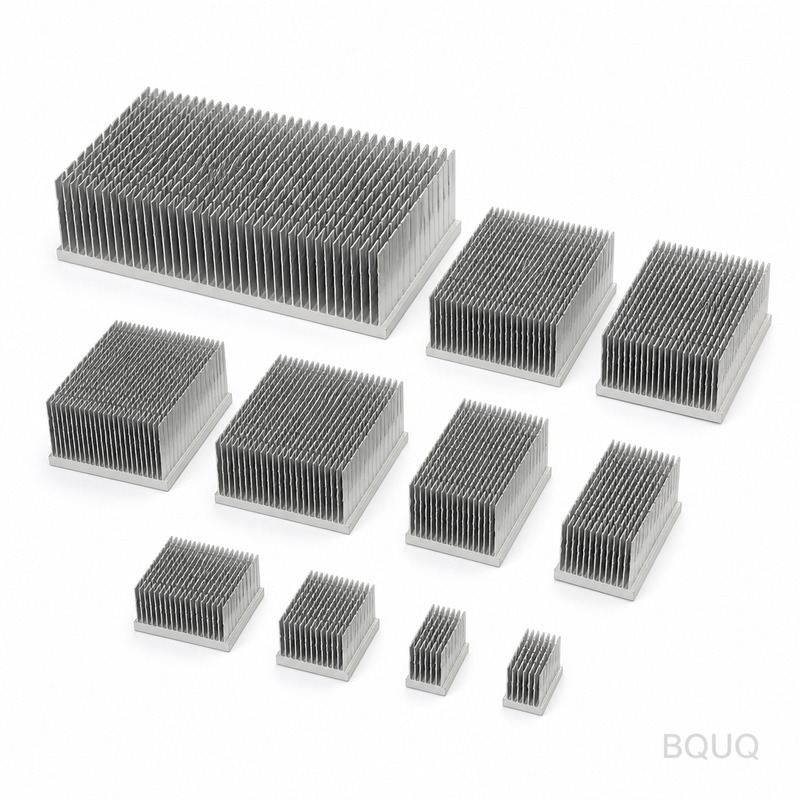
For ssd heat sink, BQUQ starts with survival conditions: load cycling, thermal swing, or corrosive VFD and inverter environments. The 6063-T5 aluminium part uses 1.0 mm fins at 5.0 mm pitch, delivering 0.85 K/W thermal resistance with zinc-nickel plating and trivalent passivation. General tolerance is ±0.20 mm, and lead time is quoted at 10 working days when tooling design and process validation run in parallel.
Most buyers start with a drawing and a target price. We start with ssd heat sink and ask what the part actually has to survive: load cycling, thermal swing, or a corrosive environment in VFD and inverter.
Related reading: High Power IGBT Heat Sink.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | 6063-T5 aluminium |
| Fin thickness | 1.0 mm |
| Fin pitch | 5.0 mm |
| Thermal resistance | 0.85 K/W |
| Surface finish | zinc-nickel plating, trivalent passivation |
| General tolerance | ±0.20 mm |
Market and Technical Context
Lead time pressure has compressed across VFD and inverter. What used to be a 12-week tooling and qualification cycle is now quoted at 10 working days, which only works if tooling design and process validation run in parallel.
The technical bar keeps rising: assemblies that once accepted ±0.20 mm now specify tighter control on critical features, which pushes the decision to tooling design rather than to final inspection.
How We Manufacture It
The route for ssd heat sink starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.20 mm is held at production speed rather than on a single slow part.
Deburring and edge conditioning are specified on the drawing for ssd heat sink. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Final inspection for ssd heat sink is sampling-based for general dimensions and 100% for critical features. The split is agreed before tooling, because moving a feature from general to critical changes cost and 10 working days.
See also: Ordering Custom Springs: The Info a Factory Needs for an Accurate Quote.
Material and Surface Finish
Surface specification for ssd heat sink is zinc-nickel plating, trivalent passivation, chosen for the service environment in VFD and inverter. Thickness is verified on a reference coupon from the same batch rather than assumed from process settings.
Learn more about Passive vs Active Heat Sinks: How to Choose the Right Cooling Solution for Your Electronics.
Where ssd heat sink sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Further technical detail: Spring MOQ and Pricing: Why Small Orders Cost More.
Substitution requests are common when 6063-T5 aluminium goes on allocation. We qualify any substitute against the same ±0.20 mm and zinc-nickel plating, trivalent passivation criteria before shipping, and provide the certificate with the change.
Recommended reading: BQUQ Cnc Machined Surgical Instruments.
Tolerance and Inspection
First-article inspection for ssd heat sink reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Traceability is kept by heat lot and production date. If a field issue ever appears with ssd heat sink, we can identify which batch, which tooling set, and which inspection record applies.
Compare it with Stamping Die Costs: 2024 Tooling Price Breakdown and Engineering Guide.
Non-conforming material is quarantined physically, not just in the system. For ssd heat sink, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
In assembly, ssd heat sink is usually constrained by the mating part rather than by its own specification. Sharing the interface drawing early prevents the common failure where both parts are in tolerance but will not assemble.
Retrofit requests are common: an existing assembly needs ssd heat sink in a slightly different size. Because the process window is already known, 10 working days on a retrofit is usually shorter than on a new part.
What to Confirm Before Ordering
Ask for the first-article report before you ask for a price cut on ssd heat sink. A supplier who cannot produce dimensional data at 500 pcs will not produce it at 800,000 pcs.
Compare quotes on the same basis: material grade, zinc-nickel plating, trivalent passivation, inspection scope, and packaging. A lower unit price that drops 100% inspection is not a lower total cost.
See also: How Does AI Server Liquid Cooling Adoption Impact Heat Sink Design?.
FAQ: Your Questions Before Ordering
What tolerance can you hold on ssd heat sink?
Prototype quantities start well below production minimums. Production runs for ssd heat sink start at 500 pcs, which is where the process window is proven and unit cost stabilises.
How long does production take for ssd heat sink?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.20 mm would require an extra operation, so you can decide before tooling.
Learn more about Aluminum vs Copper Heat Sink: Which Should You Choose for CNC Machining?.
Do you provide material and inspection certificates?
Yes. Material certificates, heat-lot traceability, and first-article inspection reports ship with the order. If your VFD and inverter customer requires additional documentation, specify it at quote stage.
Further technical detail: Custom High Power LED Heatsink.
Can you prototype before tooling?
zinc-nickel plating, trivalent passivation is standard for ssd heat sink. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of ssd heat sink remains usable.
Capacity for ssd heat sink is 800,000 pcs. That number is installed capability, not a sales figure, and it is what determines whether 10 working days holds when your volume increases.
Key Specifications and Selection Guide
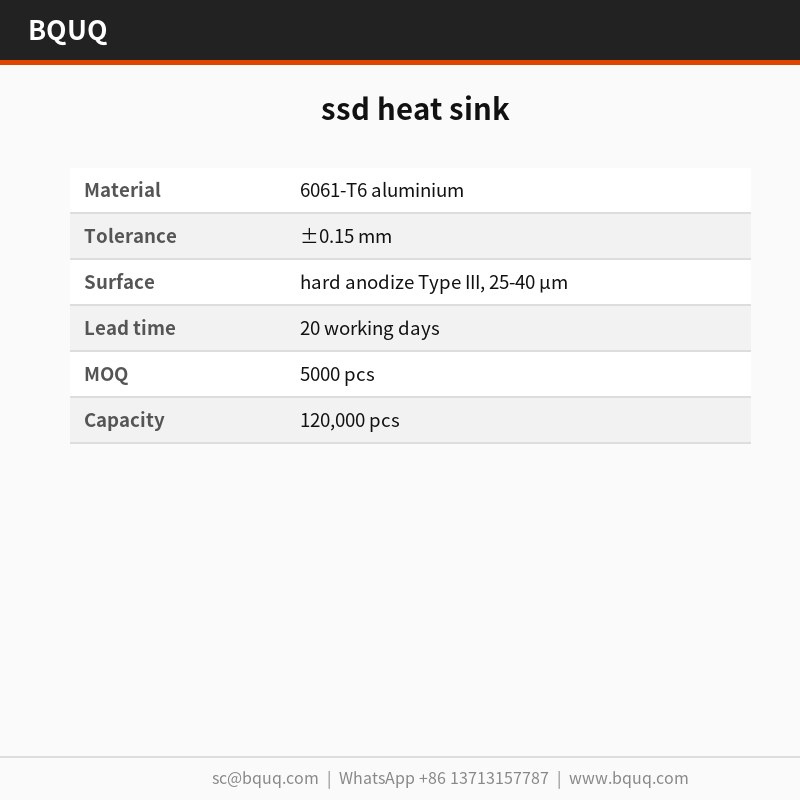
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6063-T5 aluminium |
| Tolerance | ±0.20 mm general |
| Lead time | 10 working days |
| MOQ | Not specified in article |
| Capacity | Production speed with ±0.20 mm held |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| 6063-T5 aluminium | Thermal swing and load cycling | Requires corrosion protection in harsh environments |
| Zinc-nickel plating + trivalent passivation | Corrosive VFD and inverter environments | Added process step versus bare aluminium |
| 1.0 mm fin thickness at 5.0 mm pitch | 0.85 K/W thermal resistance | Tighter tooling design for production speed |
| ±0.20 mm general tolerance | Standard assembly fit | Critical features may need tighter control |
| Parallel tooling design and process validation | 10 working day lead time | Requires early process window definition |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Tooling design | Fix material condition and tooling geometry first | Process window definition |
| Production | Confirm ±0.20 mm at production speed, not single slow part | In-process inspection data |
| Deburring and edge conditioning | Specified on drawing for ssd heat sink | Drawing compliance record |
| Surface finish | Zinc-nickel plating, trivalent passivation | Plating and passivation record |
| Final inspection | General tolerance ±0.20 mm | Inspection report |
Frequently Asked Questions
What is the thermal resistance of this ssd heat sink?
The ssd heat sink delivers 0.85 K/W thermal resistance with 1.0 mm fin thickness and 5.0 mm fin pitch. This is based on 6063-T5 aluminium and is intended for load cycling and thermal swing conditions in VFD and inverter applications.
Recommended reading: Precision Stamped Crimp Terminals Collection.
What material and surface finish do you use?
We use 6063-T5 aluminium with zinc-nickel plating and trivalent passivation. This finish supports corrosive environments in VFD and inverter use. General tolerance is ±0.20 mm, and deburring and edge conditioning are specified on the drawing.
What is the general tolerance for the ssd heat sink?
The general tolerance is ±0.20 mm. We confirm this tolerance at production speed rather than on a single slow part. Critical features may require tighter control, which pushes the decision to tooling design rather than final inspection.
What is the lead time for ssd heat sink orders?
Lead time is quoted at 10 working days. This is possible when tooling design and process validation run in parallel. The route starts with a process window, not a machine, so material condition and tooling geometry are fixed first.
Can you hold tighter tolerances on critical features?
Assemblies that once accepted ±0.20 mm now specify tighter control on critical features. We address this in tooling design rather than final inspection. The general tolerance remains ±0.20 mm, but critical features can be reviewed for tighter capability.
What should I confirm before ordering an ssd heat sink?
Confirm the survival conditions: load cycling, thermal swing, or corrosive VFD and inverter environment. Also confirm material 6063-T5, fin thickness 1.0 mm, fin pitch 5.0 mm, thermal resistance 0.85 K/W, surface finish zinc-nickel plating with trivalent passivation, and general tolerance ±0.20 mm.
Compare it with 5G RRU Heat Sink: 300mm Extruded Profile, CNC-Machined, Black Anodized.
How do you ensure quality during production?
We fix material condition and tooling geometry first, then confirm ±0.20 mm is held at production speed rather than on a single slow part. Deburring and edge conditioning are specified on the drawing. Surface finish uses zinc-nickel plating with trivalent passivation.