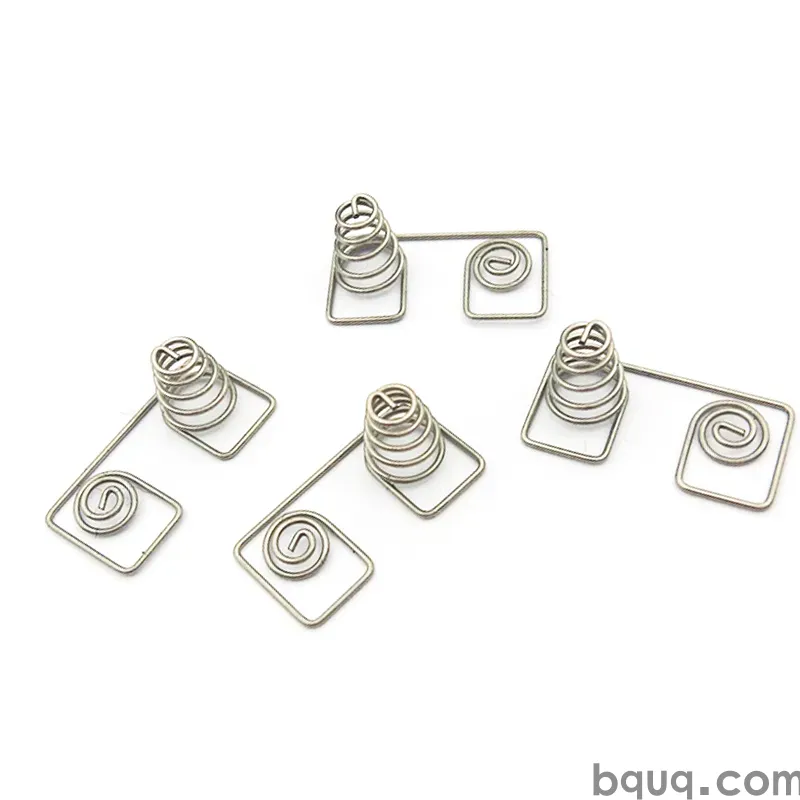
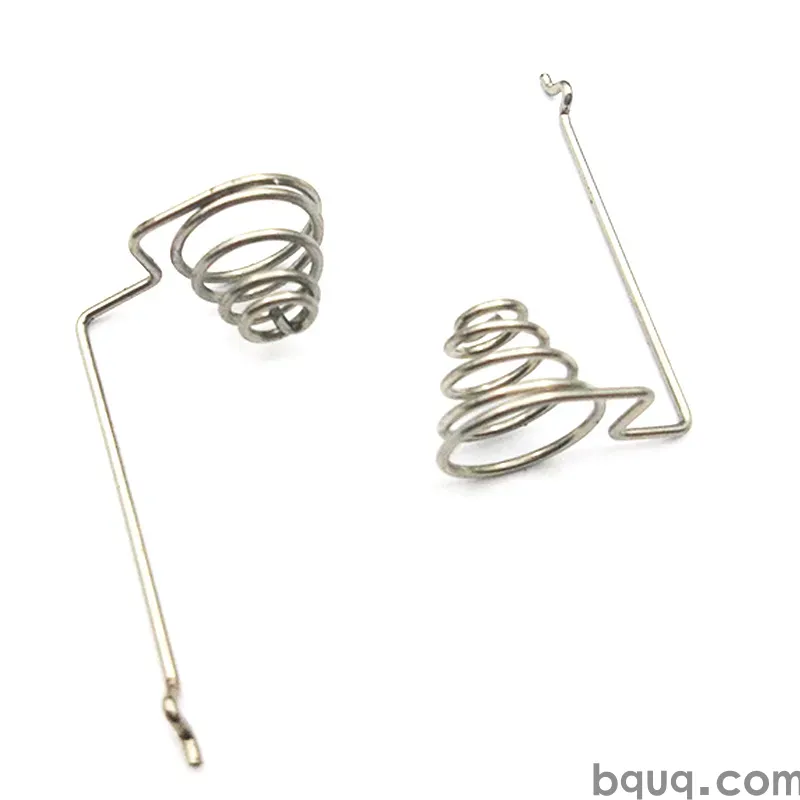
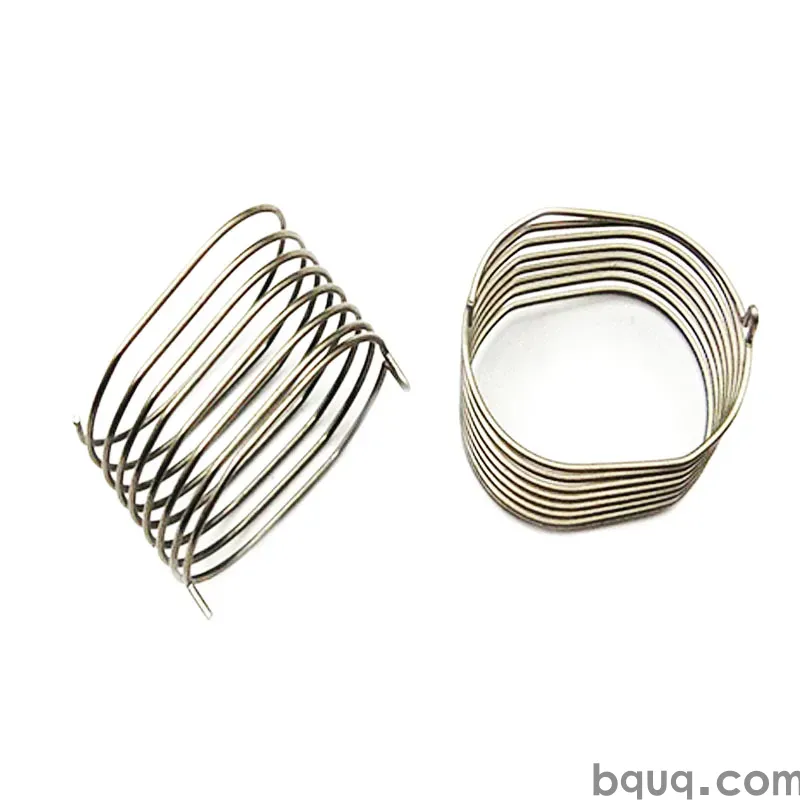
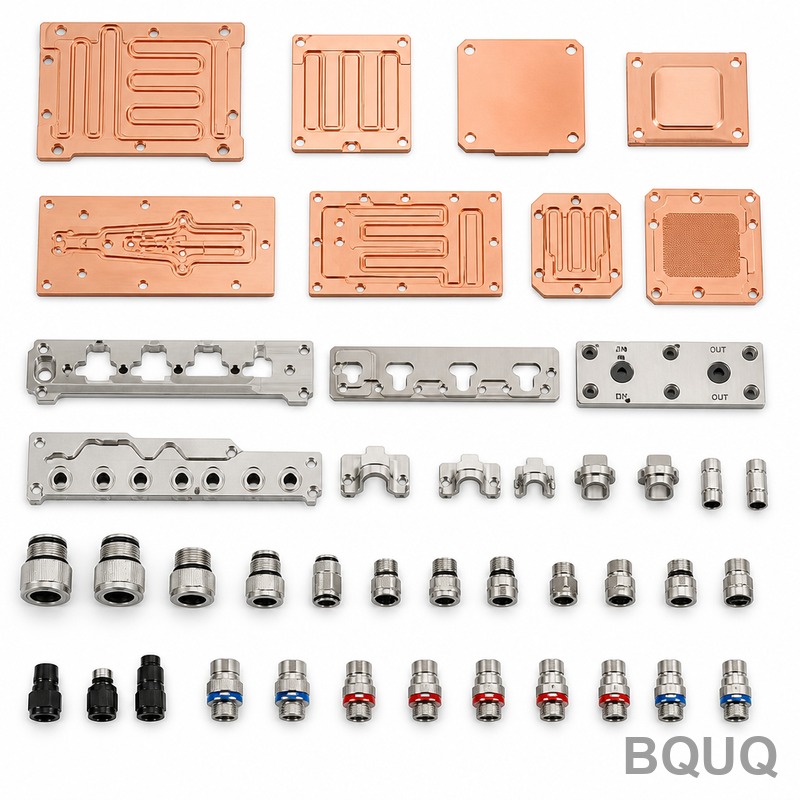
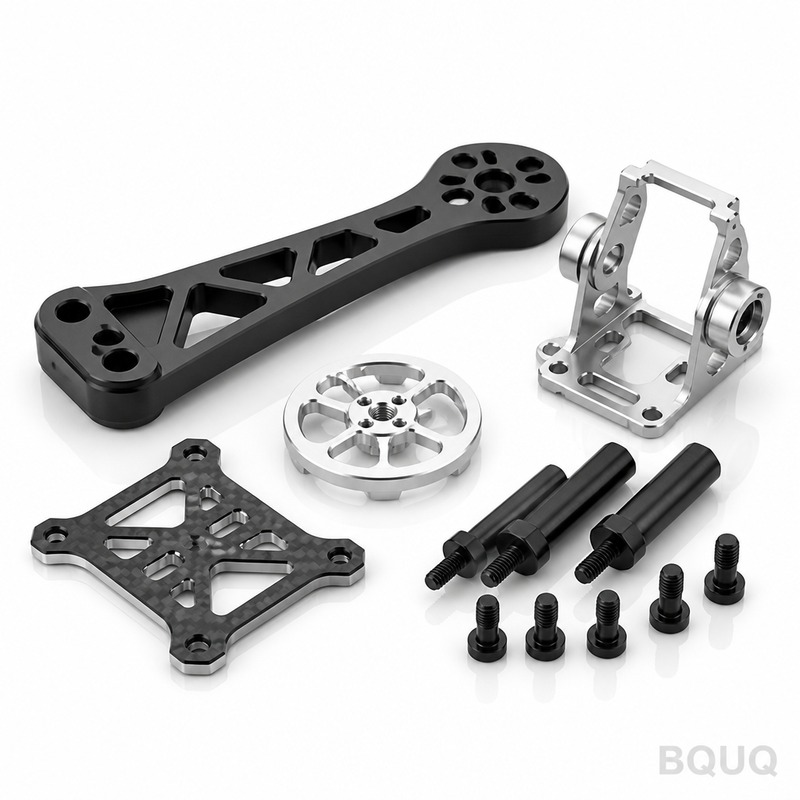
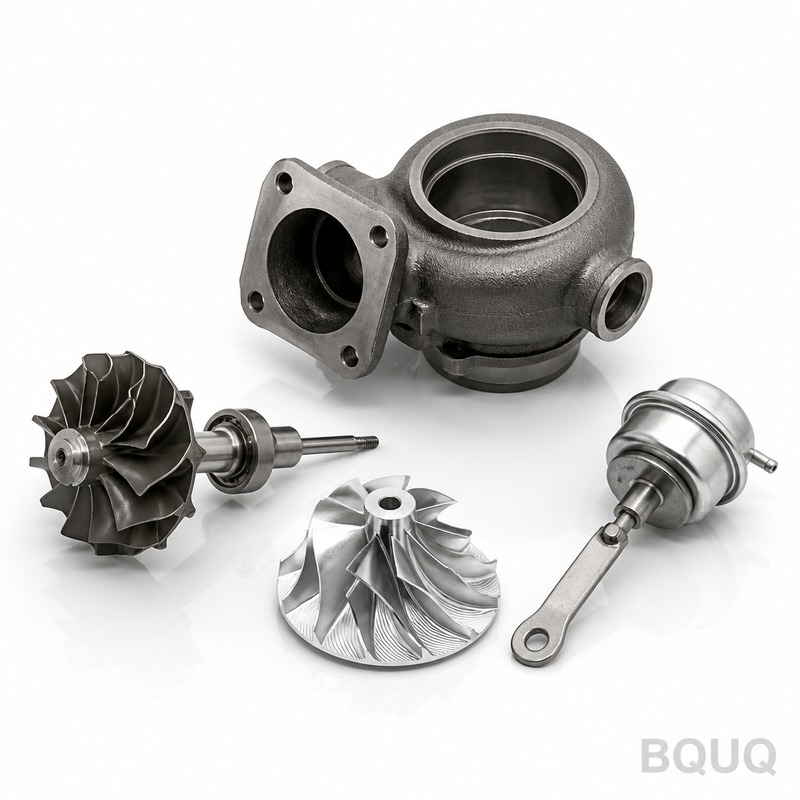
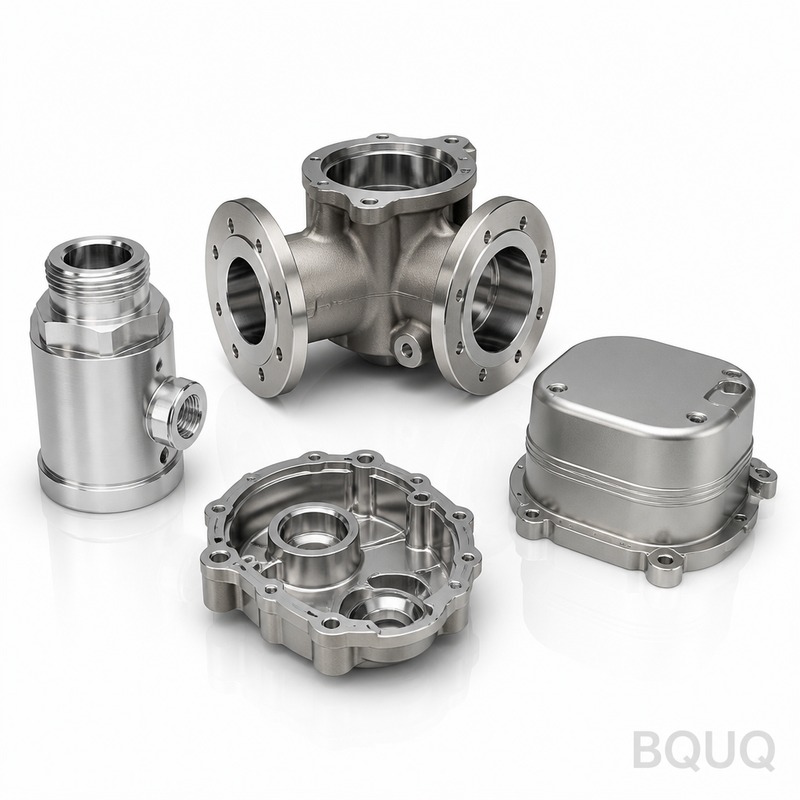
precision metal parts: Titanium Grade 5, tolerance 0.003 mm, surface bead blast + passivate, lead time 20 working days, MOQ 500 pcs. Capacity for aerospace. Drawing review and first-article report included.
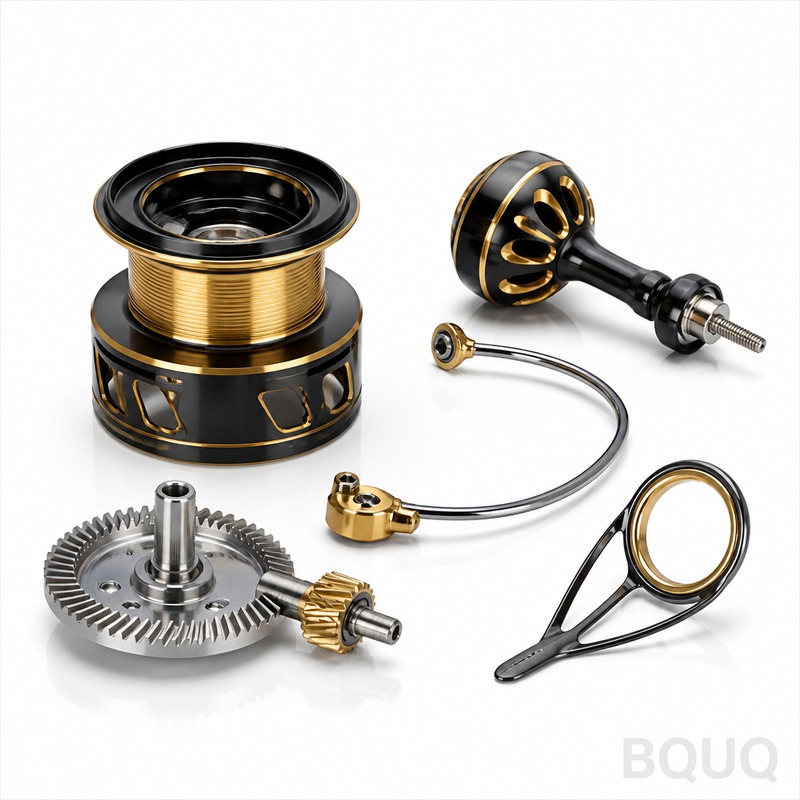
precision metal parts
Key Takeaway
Precision metal parts balance dimensional stability, unit cost, and delivery time. In our production, material options include POM, PEEK, and nylon, with a surface finish of bead blast plus passivate. Production lead time is 10 working days at a MOQ of 200 pcs, and tolerances are held to ±0.005 mm at production speed. Documentation such as material certificates and first-article reports is available from 200 pcs.
precision metal parts sits at the intersection of three constraints that rarely agree: dimensional stability, unit cost, and delivery time. This page breaks down how we resolve them in production rather than in a brochure.
Related reading: Stamped Metal Grommets Eyelets Ferrules Collection.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | POM / PEEK / nylon |
| Surface finish | bead blast + passivate |
| Lead time (production) | 10 working days |
| MOQ (production) | 200 pcs |
Market and Technical Context
Demand in robotics has shifted from single-source standard parts toward qualified custom parts, which pushes documentation requirements upstream. Material certificates, first-article reports, and PPAP-style records are now requested at 200 pcs rather than at mass production.
Tariff and logistics uncertainty has made regional qualification a priority in robotics. Buyers increasingly ask for a second qualified source, which changes how precision metal parts is specified and how tolerances are documented.
See also: cnc turning parts.
How We Manufacture It
The route for precision metal parts starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.005 mm is held at production speed rather than on a single slow part.
In production, precision metal parts runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.005 mm.
Final inspection for precision metal parts is sampling-based for general dimensions and 100% for critical features. The split is agreed before tooling, because moving a feature from general to critical changes cost and 10 working days.
Material and Surface Finish
Material condition matters as much as grade. POM / PEEK / nylon supplied in the wrong temper will drift after machining, which is why precision metal parts is stress-relieved before finishing when the geometry is asymmetric.
Where precision metal parts sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Substitution requests are common when POM / PEEK / nylon goes on allocation. We qualify any substitute against the same ±0.005 mm and bead blast + passivate criteria before shipping, and provide the certificate with the change.
Learn more about Surface Roughness Ra vs Rz: Key Differences and Selection Guide.
Tolerance and Inspection
First-article inspection for precision metal parts reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on precision metal parts, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Traceability is kept by heat lot and production date. If a field issue ever appears with precision metal parts, we can identify which batch, which tooling set, and which inspection record applies.
Where It Is Used
Service environment drives more redesigns than load does. precision metal parts in outdoor or washdown service needs bead blast + passivate and sealing considered at design stage, not added later.
Further technical detail: BQUQ Corrugated Fin Heatsink Precision CNC Machining & Stamping.
Maintenance access matters. Where precision metal parts is a wear item, we recommend specifying it as a spare with its own part number so reorder does not require a full drawing review.
What to Confirm Before Ordering
Compare quotes on the same basis: material grade, bead blast + passivate, inspection scope, and packaging. A lower unit price that drops 100% inspection is not a lower total cost.
Recommended reading: Stamped Aluminum Heat Sinks Cooling Fins Collection.
Confirm the reorder path. If precision metal parts is documented with tooling drawings and a first-article report on file, a repeat order years later reproduces the original part instead of approximating it.
FAQ: Your Questions Before Ordering
What is the minimum order quantity for precision metal parts?
Prototype quantities start well below production minimums. Production runs for precision metal parts start at 200 pcs, which is where the process window is proven and unit cost stabilises.
How long does production take for precision metal parts?
Standard lead time for precision metal parts is 10 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Compare it with Hydraulic vs Pneumatic Power Chucks: Which Is the 2026 Trend?.
Can you work from our existing drawing?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.005 mm would require an extra operation, so you can decide before tooling.
Related reading: BQUQ Cnc Machined Auto Lathe 34 Type Round Bore Spring Collet Chuck.
Do you provide material and inspection certificates?
bead blast + passivate is standard for precision metal parts. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
See also: Plating for Stamped Spring Contacts: Gold, Tin and Nickel.
Can you prototype before tooling?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of precision metal parts remains usable.
If precision metal parts is already in production elsewhere, send a sample and the current drawing. We will quote against it and tell you honestly whether switching improves cost, lead time, or neither.
Learn more about Metal Stamping Die Design for CNC Finishing: Best Practices.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | POM / PEEK / nylon |
| Tolerance | ±0.005 mm |
| Lead time | 10 working days |
| MOQ | 200 pcs |
| Capacity | Production speed with documented first-article and PPAP-style records |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| POM | General precision parts needing dimensional stability | Lower temperature resistance than PEEK |
| PEEK | High-temperature or chemically demanding applications | Higher material cost |
| Nylon | Parts needing toughness and wear resistance | Moisture absorption can affect stability |
| Bead blast + passivate | Clean, corrosion-resistant surface | Additional processing step and cost |
| Single qualified source | Fast initial sourcing | Risk if tariffs or logistics disrupt supply |
| Second qualified source | Supply chain resilience | Extra qualification time and documentation |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Material conditioning | Fix material condition before machining | Material certificate |
| Tooling setup | Fix tooling geometry first | Tooling record |
| Production | Hold ±0.005 mm at production speed | First-article report |
| Inspection | Verify dimensional stability | PPAP-style records |
| Final finish | Bead blast + passivate | Surface finish record |
Frequently Asked Questions
What materials are available for precision metal parts?
We machine precision metal parts from POM, PEEK, and nylon. Each material offers different balances of dimensional stability, temperature resistance, and cost. POM is common for general precision use, PEEK for high-temperature or chemical exposure, and nylon for toughness. Material certificates are available from 200 pcs.
What is the production lead time and MOQ?
Production lead time is 10 working days, and the minimum order quantity is 200 pcs. At this MOQ, we can provide material certificates, first-article reports, and PPAP-style records. This supports robotics buyers who need qualified custom parts rather than single-source standard parts.
Further technical detail: How to Choose Metal Stamping Material Thickness: What Is the Right Gauge?.
What tolerance can you hold at production speed?
We hold ±0.005 mm at production speed, not just on a single slow part. The process starts with a fixed process window: material condition and tooling geometry are set first. This ensures dimensional stability across the production run, with first-article and PPAP-style records documenting the result.
Recommended reading: Heat Sink Fin Spacing: Calculate Optimal Fin Pitch for Natural and Forced Air Cooling in 2025.
What surface finish is applied to precision metal parts?
The standard surface finish is bead blast plus passivate. Bead blasting creates a uniform matte texture, while passivation improves corrosion resistance. This combination is suitable for many robotics and industrial applications. Additional finishes may be available on request, but the documented standard is bead blast + passivate.
Compare it with 'Stamped Grounding Hardware for Electronics'.
Why is a second qualified source important for precision metal parts?
Tariff and logistics uncertainty has made regional qualification a priority in robotics. Buyers increasingly ask for a second qualified source to reduce supply risk. This changes how precision metal parts are specified and how tolerances are documented, since both sources must meet the same records and inspection requirements.
What documentation is available at 200 pcs?
At 200 pcs, we provide material certificates, first-article reports, and PPAP-style records. These documents support qualified custom parts and are now requested at 200 pcs rather than at mass production. They help buyers verify material condition, tooling geometry, and tolerance compliance.
How do you ensure dimensional stability during production?
We start with a process window, not a machine. Material condition and tooling geometry are fixed first, then we confirm that ±0.005 mm is held at production speed. Inspection records, including first-article reports and PPAP-style documentation, verify stability across the 200 pcs minimum order quantity.