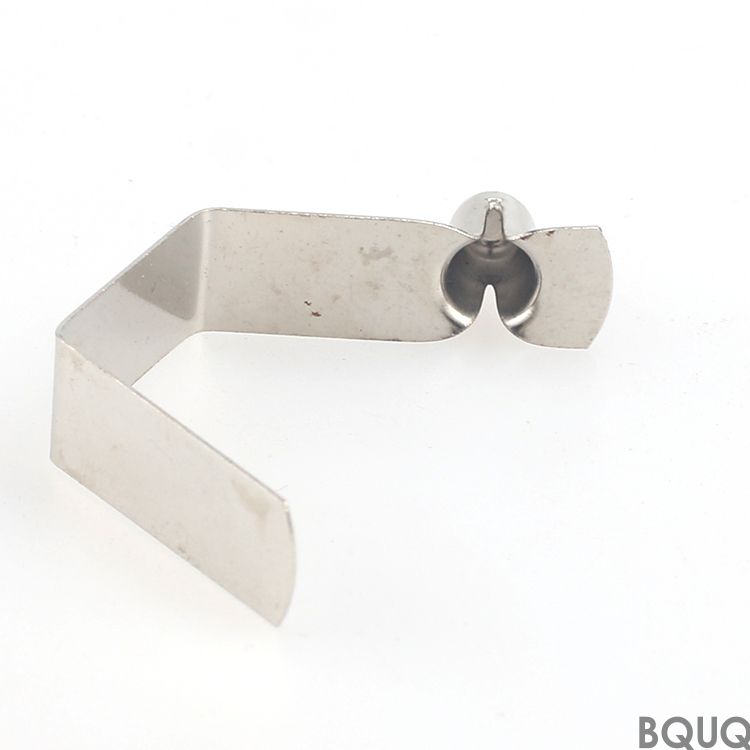
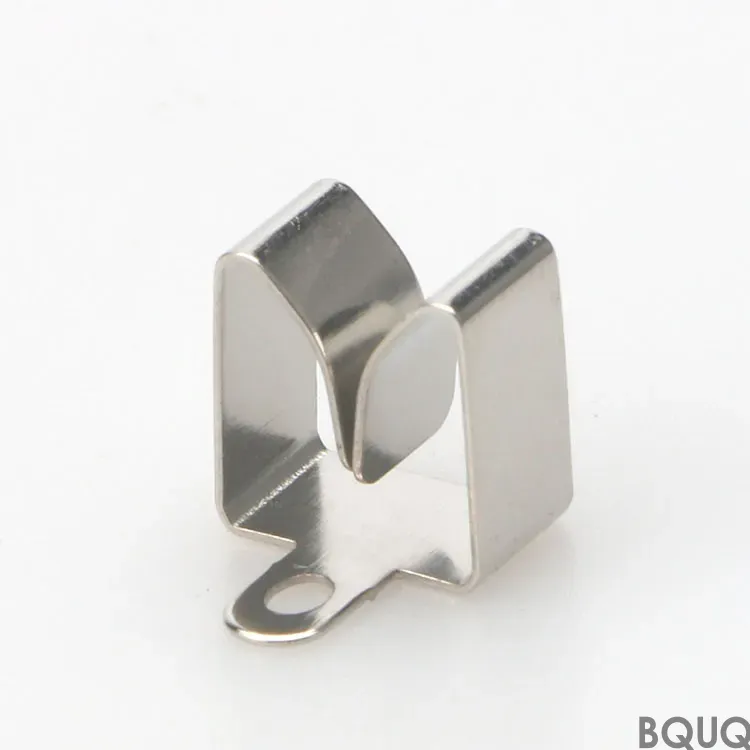
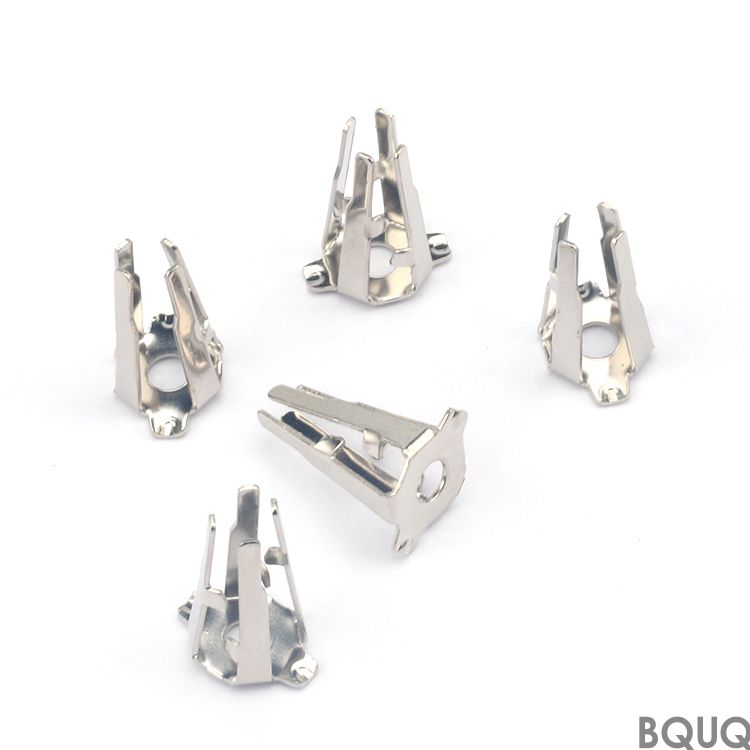
This is a small batch progressive die stamping metal clip prototype built for engineers who need functional validation parts before full production. You get 0.01 mm positional tol
Small Batch Progressive Die Stamping Metal Clip Prototype | BQUQ Precision
This is a small batch progressive die stamping metal clip prototype built for engineers who need functional validation parts before full production. You get ±0.01 mm positional tolerance, surface fini
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a small batch progressive die stamping metal clip prototype built for engineers who need functional validation parts before full production. You get ±0.01 mm positional tolerance, surface finish down to Ra 0.8, and a guaranteed 7-day lead time from drawing approval, with hardness up to 52 HRC after heat treatment.
We run 20 CNC machining centers and 15 high-speed stamping presses in our Dongguan factory, so your prototype is not a lab sample—it is a production-representative part made on the same tooling path as your future volume order. No MOQ, no tooling surprises, no vague delivery promises.
How a Progressive Die Produces Your Clip in One Continuous Strip
Your metal clip prototype moves through a single progressive die in a continuous strip, not as a standalone blank. Each station performs one operation: pilot hole piercing, edge trimming, bending, coining, and final cutoff. This means your prototype has the same dimensional consistency as a 100,000-piece run because the strip is indexed with a ±0.005 mm pilot pin system.
For small batches, we use a modular die base that cuts tooling cost by 40% compared to a dedicated die. You get the geometry accuracy of progressive stamping without paying for a full production die upfront. The strip width is calculated to minimize material waste, so your prototype cost per piece stays flat even at 50 pieces.
Materials and Heat Treatment We Use for Spring-Like Clips
We stock 12 common stamping alloys in our Dongguan warehouse, all with mill certificates traceable to the melt. For clips that need spring-back resistance, we recommend 301 stainless steel (full hard, 480–520 MPa yield) or C17200 beryllium copper (aged to 38–42 HRC). For general retention clips, SPCC cold-rolled steel with a 48–52 HRC quench and temper cycle works best.
Heat treatment is done in-house in a vacuum furnace, which prevents surface decarburization—a common defect in small clips that ruins fatigue life. We can also apply a 0.5–1.0 µm electroless nickel plating for corrosion resistance, measured with a calibrated X-ray fluorescence gauge.
Inspection Before Every Shipment: CMM, Profile Projector, and Hardness Test
Every small batch progressive die stamping metal clip prototype goes through a 3-step inspection before it leaves the factory. First, a Zeiss CMM measures critical dimensions—hole positions, bend angles, and clip gap width—against your 2D drawing. Second, a profile projector at 20× magnification checks edge condition and burr height, which we hold under 0.03 mm.
Third, a Rockwell hardness tester verifies the heat treatment result on a sacrificial part from the same strip. We send you a PDF inspection report with actual measured values, not just a pass/fail note. If any dimension is out of tolerance, we re-run the tooling before shipping—never a "close enough" approval.
Tooling Costs for Small Batches: Die Sharing and Modular Inserts
Most stamping shops charge you a full die cost even for 100 pieces. We do not. For your metal clip prototype, we use a modular die frame with interchangeable inserts, so the die cost is 30–50% lower than a custom die. If your clip design changes after testing, we replace only the affected insert—not the whole die—saving you another 20% on revision costs.
For truly tiny quantities (under 200 pieces), we can also use a wire-cut blanking method that skips the die entirely, but the part will have a slightly rougher edge (Ra 1.6 vs Ra 0.8). We will tell you honestly if this fits your application, so you are never paying for a die you do not need.
Why Lead Time Is 7 Days, Not 20: In-House Tool Room and CNC Backup
The industry average for a stamping prototype is 15–20 days because most shops outsource die making. We have a 6-person tool room with 3 wire EDM machines and 2 CNC mills on-site, so your progressive die inserts are cut, hardened, and assembled in 3 days. The remaining 4 days cover material cutting, stamping setup, inspection, and shipping.
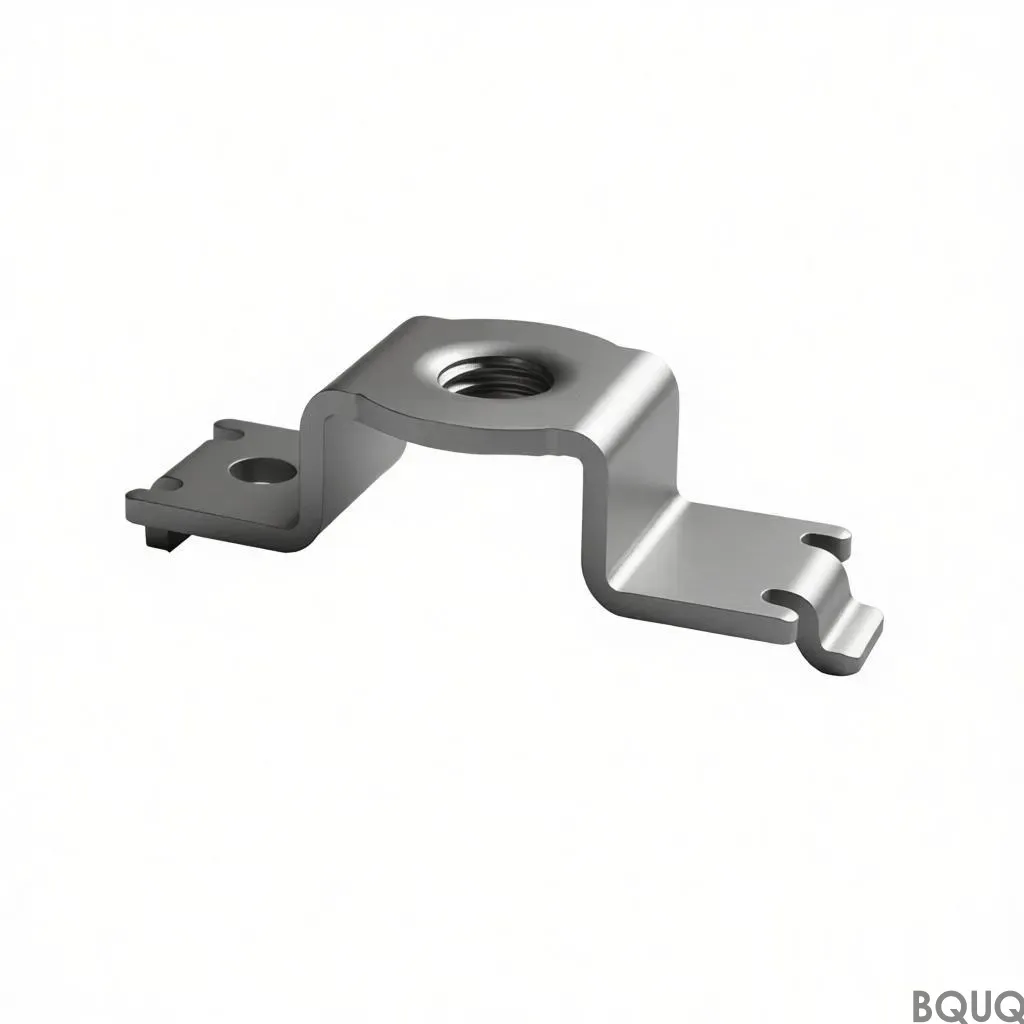
If your clip is too complex for stamping alone—for example, it needs a threaded hole or a precision-machined slot—we switch to CNC machining for those features after stamping. This hybrid approach keeps the 7-day lead time intact. You can also refer to our CNC cutting tool selection guide to see how we match tooling to your material.
Real Tolerances for a Metal Clip Prototype: What We Guarantee
We guarantee the following on every small batch progressive die stamping metal clip prototype, verified by our CMM and documented in the inspection report. These numbers are not "best case"—they are the contract values we sign off on.
Parameter
Specification
Material options
301 SS, SPCC, C17200 BeCu, 5052 Al, 65Mn spring steel
Strip thickness range
0.1 mm – 3.0 mm
Positional tolerance (holes)
±0.01 mm
Bend angle tolerance
±0.5°
Burr height
≤ 0.03 mm
Surface finish (stamped)
Ra 0.8 – 1.6 µm
Hardness (after heat treat)
38 – 52 HRC depending on alloy
Flatness (per 25 mm length)
≤ 0.05 mm
Lead time (from drawing approval)
7 working days
MOQ
No MOQ (1 piece accepted)
If you need tighter tolerances than these, we have the equipment to go to ±0.005 mm on critical features, but we will first check your design—sometimes a looser tolerance saves 30% on cost without affecting function. Read our CNC machining tolerances guide to understand how we balance precision with cost.
Packaging and Shipping: No Rust, No Bent Clips, No Customs Delays
Small clips are easy to lose or damage in transit. We pack each prototype in anti-static bubble wrap, then in a rigid ESD tray, then in a double-wall carton with foam inserts. For stainless and beryllium copper clips, we add VCI (vapor corrosion inhibitor) paper to prevent any surface oxidation during sea freight.
We ship via DHL, FedEx, or UPS from Shenzhen airport, 30 minutes from our factory. Typical delivery to the US is 3–4 days, to Europe 4–5 days. All export documents—commercial invoice, packing list, and certificate of origin—are prepared by our shipping team, so your customs clearance has zero surprises.
Do you really have no MOQ for a stamping prototype?
Yes, we accept orders from 1 piece for a small batch progressive die stamping metal clip prototype, though the per-piece price for 1 piece will be higher than for 50 pieces due to setup time.
Can I make design changes after receiving my prototype?
Yes, if you change a bend angle or hole position, we modify only the affected die insert—this costs 20% of a new die and takes 2 extra days.
How do you handle quality control for a single prototype?
We still run the full inspection routine—CMM, profile projector, and hardness test—on the single piece, and we include the measured data in your shipment.
What is your fastest possible lead time?
If you approve the 3D model and material by 10 AM China time, we can ship a simple clip (no heat treatment) in 4 working days.
Send your drawing for a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. We will confirm material, tolerance, and price based on your exact part geometry—no guesswork, no hidden tooling fees.