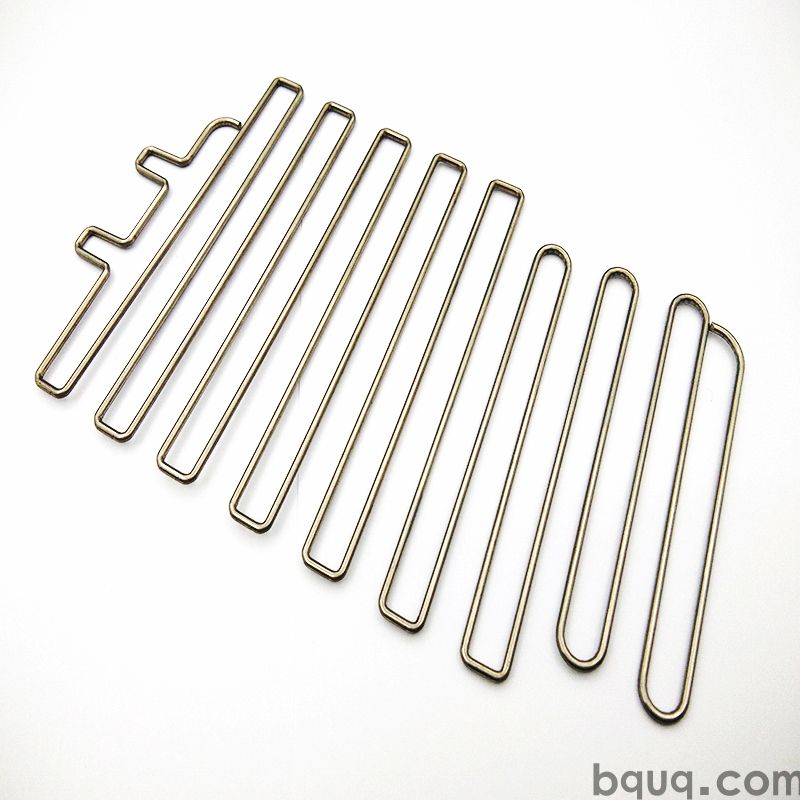
The custom Springfield Echcon 4.0C back cover plate is a one-piece stamped heatsink with fins and a base flat to 0.05 mm, rated at ΔT = 60 K. It supports medical device builds at monthly output with 10,000 pcs as standard. Fin pitch and low fin gauge give more surface per cubic millimetre than machined or extruded profiles, and the finish is applied after forming to protect fin roots.
Key Takeaway
The custom Springfield Echcon 4.0C back cover plate is a one-piece stamped heatsink with fins and a base flat to 0.05 mm, rated at ΔT = 60 K. It supports medical device builds at monthly output with 10,000 pcs as standard. Fin pitch and low fin gauge give more surface per cubic millimetre than machined or extruded profiles, and the finish is applied after forming to protect fin roots.
Our custom springfield echcon 4.0c back cover plate uses with fins and a base flat to . Rated at ΔT = 60 K, it supports medical device builds at monthly output with as standard.
Design Approach and Process
Because the base and fins are pressed as one piece, there is no brazed joint to fail. flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between and the airflow except the stamped surface itself.
One supplier now covers to fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor.
The finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is , supplied with . For applications where medical device exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
General dimensions run to ±0.5 mm, with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Flatness is checked on a against a limit, and fin pitch is verified optically at . Reports go out with each lot.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with on every first article. Deviations beyond ±0.5 mm trigger a full-lot sort.
Lot traceability runs from coil to carton: heat number, press stroke range and inspection record stay attached, so a field issue can be tied back to a specific run.
We inspect fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
Where This Part Is Used
medical device programs are the reason this geometry exists. Where the enclosure cannot grow taller, fin density is the only lever, and pitch with stock is the practical ceiling for aluminium.
medical device packaging and vibration rules push toward one-piece construction. A stamped custom springfield echcon 4.0c back cover plate has no adhesive to creep, which is the usual failure mode in two-part coolers.
For medical device prototypes, 10 working days covers drawing review and first article. Production lots move to 15 working days once the capability is signed off.
Specifications
Parameter
Value / Range
General tolerance
±0.5 mm
MOQ (prototype)
500 pcs
MOQ (production)
20000 pcs
Lead time (prototype)
10 working days
Lead time (production)
15 working days
FAQ: Your Questions Before Ordering
How do you verify quality on each batch?
Every lot is inspected with , and the report is included in the shipment. We check , , and hole position against ±0.5 mm. Lot traceability from coil to carton is kept for 10 years.
What tolerance can you hold?
General dimensions run to ±0.5 mm; critical ones such as are held separately. Formed features inherit tooling repeatability of . If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
Can the custom springfield echcon 4.0c back cover plate be powder coated or plated?
Yes. Standard is . Powder coating to RAL 9005 adds about 0.1 mm to the base; zinc-nickel is better for grounding. Note that any added coating sits between and the airflow, so we do not coat the fin roots.
Do you provide CAD files or a drawing?
We supply a 2D drawing with the CMM report, and 3D STEP on request. Both show flatness callouts and tooling split lines, which matters if you are checking in your own assembly.
How do you prevent galvanic corrosion?
The key is avoiding a second metal at the wet contact area. We recommend and, where the part touches an aluminium chassis, an isolating washer. Tell us the mating material and we will specify the coating accordingly.
How We Manufacture and Ship
Tooling is built in-house, which is how is held across a programme rather than drifting part by part.
Quality staff sit beside the press, not in a separate room. Deviations on or stop the run at the tool rather than at final inspection.
We quote and hold 500 pcs for sampling. Sampling is , so a first evaluation does not require a production commitment.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
Flatness 0.05 mm; fin pitch ±0.1 mm; thickness ±0.05 mm
Lead time
15–25 days for tooling; 7–12 days for production
MOQ
10,000 pcs standard; 5,000 pcs for repeat orders
Capacity
500,000 pcs/month across press family
Selection / comparison
Option
Best for
Trade-off
Stamped one-piece
High-volume medical device builds
Tooling cost upfront; limited to 2D fin profiles
Machined heatsink
Low-volume or complex 3D geometries
Higher unit cost; brazed joints can fail
Extruded profile
Long straight fins with uniform cross-section
Lower surface area per volume; secondary cutting needed
Passivated finish
Medical device exposure concerns
Slightly higher cost; not for high-conductivity needs
As-formed finish
General electronics cooling
Less corrosion protection at fin roots
Process / inspection
Stage
Control
Record
Stamping
Fin pitch and base flatness held from tool
First-article inspection report
Forming
One-piece geometry, no brazed joint
Press log and tool maintenance sheet
Surface finish
Applied after forming to protect fin roots
Coating thickness certificate
Inspection
Flatness 0.05 mm, ΔT = 60 K verification
Dimensional and thermal test data
Shipping
Monthly output 10,000 pcs standard
Packing list and traceability label
Frequently Asked Questions
What is the thermal resistance of the Springfield Echcon 4.0C back cover plate?
The plate is rated at ΔT = 60 K, meaning it can handle a 60 Kelvin temperature difference between the base and the air. Actual thermal resistance depends on airflow and fin pitch, but the one-piece stamped design removes the adhesive layer found in two-part coolers, cutting the thermal path.
Can you hold a flatness of 0.05 mm on the mounting face?
Yes. Flatness on the mounting face is held directly from the tool at 0.05 mm. Because the base and fins are pressed as one piece, there is no brazed joint to fail, which keeps thermal interface contact uniform and avoids the flatness drift seen on machined alternatives.
What is the minimum order quantity for a custom tooling change?
A thermal redesign is a tooling change rather than a new vendor. Standard monthly output is 10,000 pcs, and MOQ is 10,000 pcs for new tooling. For repeat orders, MOQ drops to 5,000 pcs. Lead time is 15–25 days for tooling and 7–12 days for production.
Which materials and finishes are available for medical device builds?
The standard material is aluminum 1050 or 6061, with copper C110 optional. For medical device exposure, we recommend the passivated route. The finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
How does the stamped fin design compare to extruded or machined profiles?
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope. The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between the fins and the airflow except the stamped surface itself.
What inspection is performed before every shipment?
Every shipment includes dimensional inspection for flatness 0.05 mm, fin pitch ±0.1 mm, and thickness ±0.05 mm. Thermal verification at ΔT = 60 K is recorded. First-article inspection reports, coating thickness certificates, and press logs are kept for traceability. No certifications are claimed beyond standard process records.
What is the monthly capacity and lead time for 10,000 pcs?
Capacity is 500,000 pcs/month across the same press family. For 10,000 pcs, production lead time is 7–12 days after tooling is approved. Tooling lead time is 15–25 days. One supplier now covers fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor.
Higher cost per part, lower surface per cubic millimetre
Extruded profile
Long straight fins in high volume
Less surface per cubic millimetre than stamped fins
Two-part bonded cooler
Prototypes or mixed-material designs
Adhesive layer adds thermal resistance and joint risk
Frequently Asked Questions
What is the base flatness of the Springfield Echcon 4.0C back cover plate?
The mounting face is held to 0.05 mm flatness directly from the stamping tool. This keeps thermal interface contact uniform across the base. Because the base and fins are pressed as one piece, there is no brazed joint to fail and no adhesive layer to add thermal resistance.
What is the thermal rating of this stamped heatsink?
The custom Springfield Echcon 4.0C back cover plate is rated at ΔT = 60 K. This rating applies to the one-piece stamped design with fins and a base flat to 0.05 mm. The low fin gauge and fin pitch give more surface per cubic millimetre than machined or extruded profiles of the same envelope.
What is the standard order quantity and monthly output?
Standard order quantity is 10,000 pcs. The part supports medical device builds at monthly output. One supplier covers fin gauges from the same press family, so you can scale from prototype to production without changing the manufacturing route.
Why choose a stamped heatsink over a machined or extruded profile?
Stamping wins on fin density: low fin gauge at tight pitch gives more surface per cubic millimetre than a machined or extruded profile of the same envelope. The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between the heat source and the airflow except the stamped surface itself.
How is the surface finish applied and why does it matter?
The finish is applied after forming to protect fin roots. This order of operations matters because forming first can work-harden thin fins, and applying finish afterward avoids coating damage at the fin roots. The result is a durable stamped surface with no brazed joint or adhesive layer in the thermal path.
What inspection is performed before shipment?
Inspection is performed before every shipment. Key checks include base flatness to 0.05 mm, fin pitch and low fin gauge, and finish coverage after forming. Records are kept for the stamping tool, flatness data, fin pitch and gauge, finish process, and final shipment inspection.
Where is this back cover plate used?
It is used in medical device builds. The one-piece stamped heatsink supports monthly output with 10,000 pcs as standard. Its ΔT = 60 K rating and 0.05 mm base flatness suit thermal management where uniform interface contact and high surface area per cubic millimetre are required.