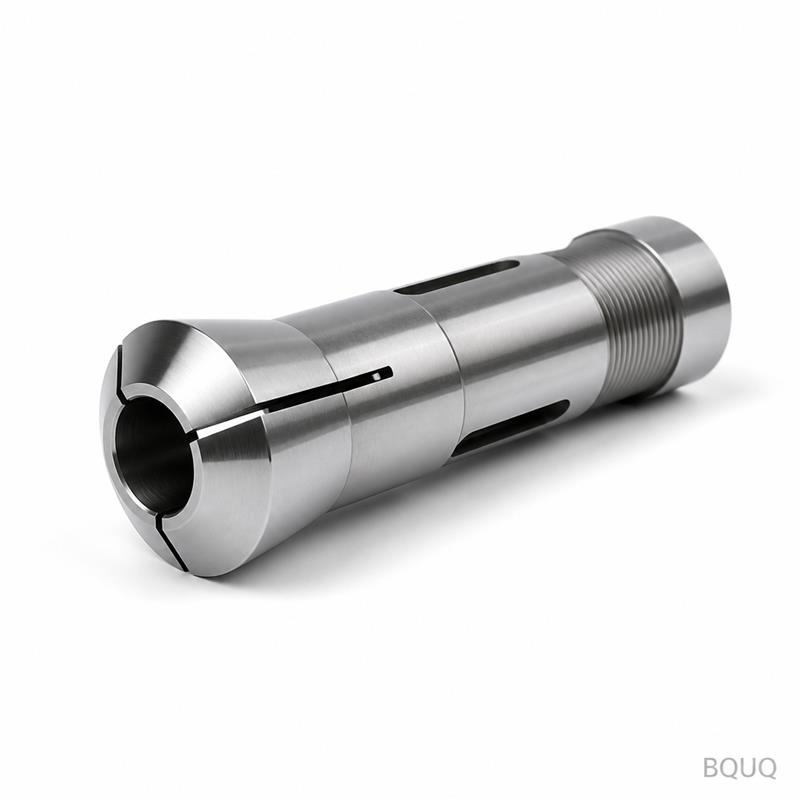
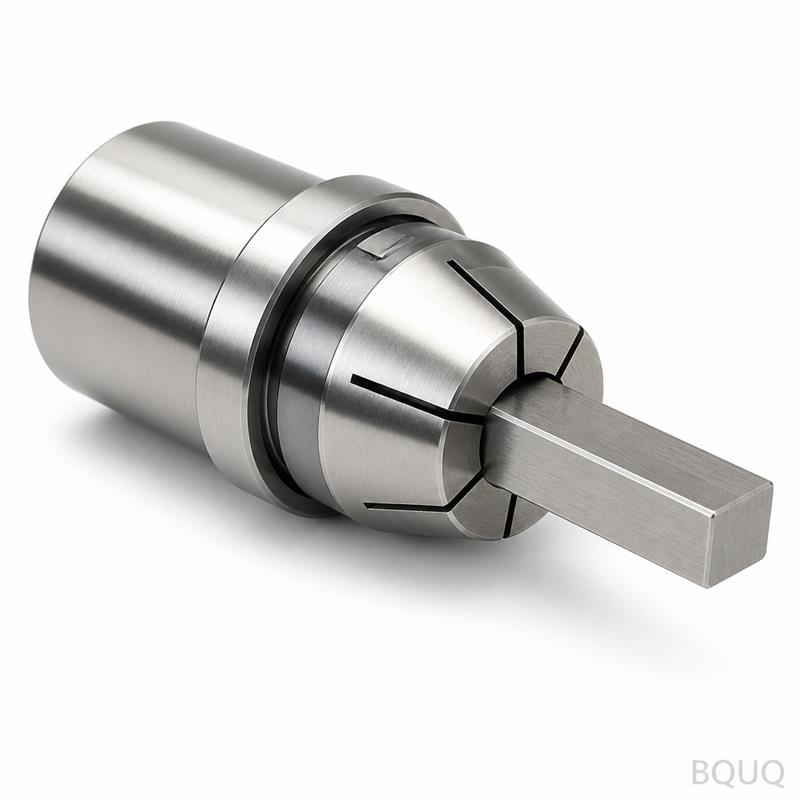
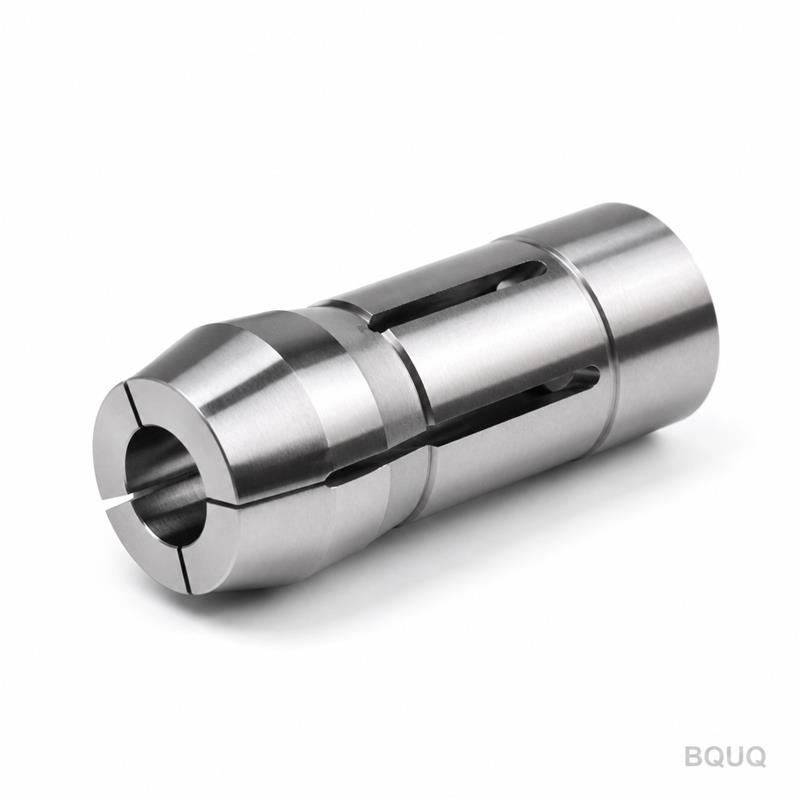
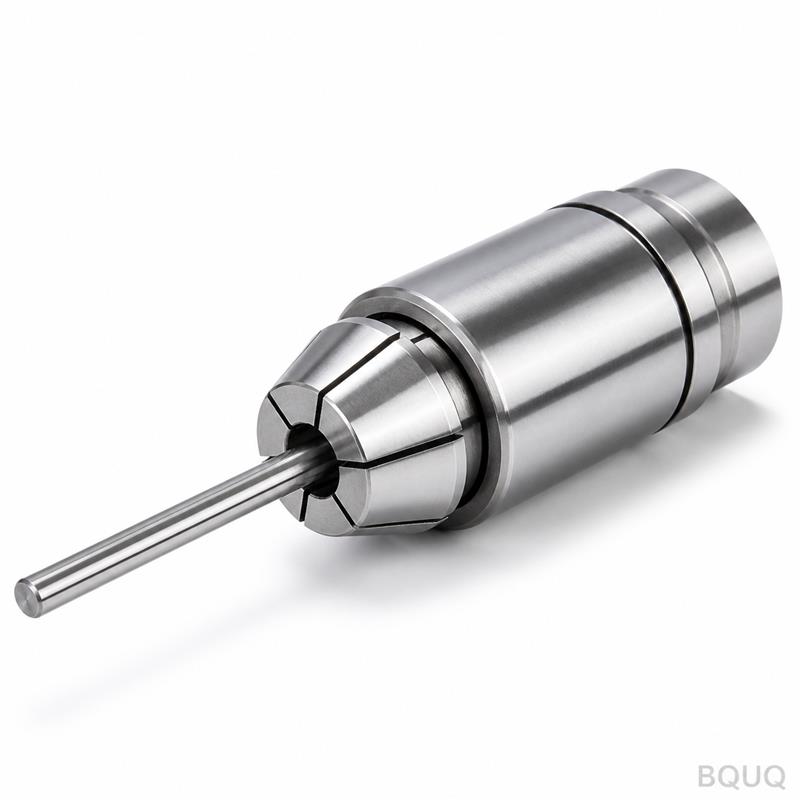
This is a CNC machined auto lathe 630 type round bore spring collet chuck, built to grip round stock from 3 mm to 30 mm on sliding-head and fixed-head auto lathes. You get 0.005 mm
BQUQ CNC Machined Auto Lathe 630 Type Round Bore Spring Collet Chuck
This is a CNC machined auto lathe 630 type round bore spring collet chuck, built to grip round stock from 3 mm to 30 mm on sliding-head and fixed-head auto lathes. You get 0.005 mm total indicated run
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined auto lathe 630 type round bore spring collet chuck, built to grip round stock from 3 mm to 30 mm on sliding-head and fixed-head auto lathes. You get 0.005 mm total indicated runout (TIR) at the nose, a hardness of 58–60 HRC across the gripping surface, and a standard lead time of 7 working days for any size in our standard range.
Why 630 Type Geometry Matters for Round Stock
The 630 type collet uses a single tapered outer cone and a round bore, not a hexagonal or square bore. That round bore contacts the workpiece along a full 360-degree circumference. This eliminates the three-point pressure marks you get with spring collets that have slotted relief cuts. For bar stock feeding, the 630 series maintains concentricity because the slots are cut at a 15-degree helix angle, which allows even radial compression without distorting the bore. We machine the taper to a 30-minute included angle, matching the spindle nose on most Japanese and European auto lathes (Citizen, Star, Tsugami, Tornos).
Steel Selection and Heat Treatment Sequence
We start with either GCr15 (equivalent to AISI 52100) or 65Mn spring steel, depending on your run size and wear requirements. GCr15 gives you higher hardness retention after 100,000 cycles; 65Mn gives you more elastic recovery for thin-wall tubes. The bore is ground after heat treatment, not before. That sequence matters: we harden to 60 HRC, then grind the bore and taper on a CNC internal grinder with a CBN wheel. Final surface finish on the bore is Ra 0.2 µm, which reduces friction and prevents galling on soft aluminum or brass stock.
Hardness, Runout, and Surface Finish – Measured, Not Claimed
Every collet is checked on a Mitutoyo CMM for taper angle and bore diameter. We measure runout by mounting the collet in a precision test holder with a 10 mm ground pin, then rotating the assembly on a pair of V-blocks. We reject anything above 0.005 mm TIR. Hardness is tested on a Rockwell C scale at three points around the bore: front, middle, and rear. We do not spot-check; we inspect 100% of production. The table below shows what you can expect from a standard order.
Parameter
Value / Range
Collet Type
630 Type Round Bore Spring Collet
Bore Diameter Range
3.0 mm – 30.0 mm (0.118" – 1.181")
Material Options
GCr15 (52100) or 65Mn spring steel
Heat Treatment Hardness
58–60 HRC (surface), 55 HRC (core)
Total Indicated Runout (TIR)
≤ 0.005 mm at nose
Bore Surface Finish
Ra 0.2 µm (ground after hardening)
Taper Angle Accuracy
± 0.0005 mm over taper length
Slot Width
0.8 mm ± 0.05 mm (helix 15°)
Standard Lead Time
7 working days (standard sizes)
MOQ
No MOQ – single piece accepted
Slots Cut by Wire EDM, Not Milling
Most collet manufacturers cut the relief slots on a milling machine, which leaves burrs and micro-tears at the slot edges. We cut all slots with a wire EDM after heat treatment. That gives a recast layer under 0.01 mm and a slot edge radius of 0.05 mm. The result is a collet that flexes evenly without stress risers. You will see longer service life on high-speed spindles running at 8,000 RPM or above. If you are working with thin-walled tubing, ask for our 65Mn version with a wider slot opening – it closes more gently on delicate parts.
Inspection Before Every Shipment – The 5-Point Check
We do not ship without a final inspection report. Each collet goes through a 5-point check: (1) taper angle measured with a sine bar, (2) bore diameter verified with a bore gauge to ±0.002 mm, (3) runout test with a 10 mm master pin, (4) hardness reading on the Rockwell C scale, and (5) visual inspection under 5x magnification for surface cracks or grinding burns. You receive a digital copy of the report with your shipment. If you need a full material certificate with heat lot traceability, we provide that for free – just request it on your PO.
How to Match the Collet to Your Spindle Nose
The 630 type collet is not universal. The taper angle and thread pitch on the draw tube must match your machine. Before you order, measure the draw tube thread pitch (metric or imperial) and the taper angle on your existing collet. We machine the back thread to any pitch you specify – from M16x1.5 to 1/2"-20. We also offer a 2 mm or 3 mm pad for clamping pre-machined parts without marking the surface. If you are unsure, send us a photo of your current collet and the spindle nose drawing. We will tell you within 24 hours if we can match it.
Frequently Asked Questions
Do you accept an order for just one collet?
Yes, we have no MOQ – you can order a single piece for prototype testing, and the unit price only drops if you buy 20 or more.
Can you make a collet with a non-standard bore diameter?
Absolutely – we machine any bore size between 3 mm and 30 mm in 0.1 mm increments, and we keep the same 0.005 mm TIR guarantee.
How do you ensure quality on a batch of 500 pieces?
We use a SPC process on the bore grinding step, sampling every 10th piece during production and then doing a 100% final inspection for runout and hardness.
What is the fastest lead time for a custom size?
For a custom bore diameter, we can ship in 5 working days using a pre-hardened blank; standard sizes ship in 7 working days.
Raw Material Sourcing and Traceability
We buy GCr15 and 65Mn steel from certified mills in China, and each batch arrives with a mill certificate. The steel is spheroidized annealed before machining, which makes the slots cut cleanly and the taper grind without chatter. We keep a sample from each heat for 24 months. If you have a critical application – like medical device components – we can supply a full traceability package, including the heat number and chemical composition report.
This collet is precision manufacturing made in China, but with a 0.005 mm runout guarantee that matches or beats your current supplier. We are a 20-year factory in Dongguan, running 40 CNC lathes and 15 grinding machines under one roof. No trading company in between – you talk directly to the engineers who make the parts.
Get a firm quote within 12 hours. Send your drawing or collet specification to sc@bquq.com or WhatsApp us at +86 13713157787. Include your bore size, machine model, and desired quantity – we will reply with a price and a delivery date. No MOQ, no hidden tooling costs.