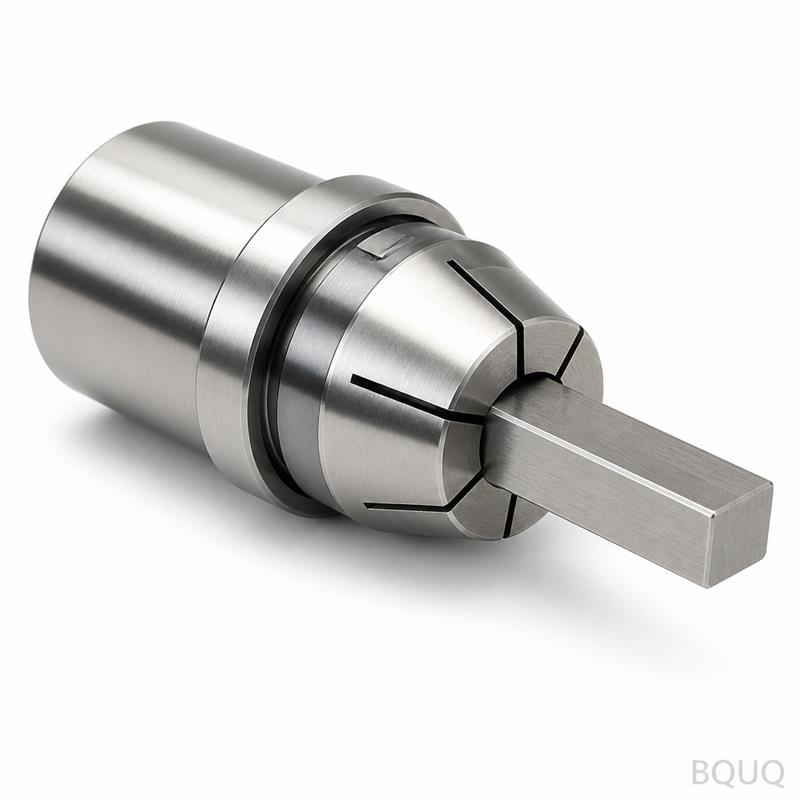
What This Collet Does for Your Auto Lathe This is a CNC machined auto lathe 38 type collet with square bar stock, built to grip square, rectangular, and hexagonal bar material tigh
BQUQ CNC Machined Auto Lathe 38 Type Collet With Square Bar Stock
What This Collet Does for Your Auto Lathe This is a CNC machined auto lathe 38 type collet with square bar stock, built to grip square, rectangular, and hexagonal bar material tightly during high-spee
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined auto lathe 38 type collet with square bar stock, built to grip square, rectangular, and hexagonal bar material tightly during high-speed turning. You get consistent 0.005 mm total indicated runout (TIR) at the nose, which means your finished parts hold tolerance without rework. We ship standard sizes within 10 working days, and every unit is hardened to 58-60 HRC for long clamping life.
Why Square Bar Stock Needs a Dedicated 38 Type Collet
Round collets crush square stock corners. The 38 type collet has a machined square bore that matches your bar exactly, distributing clamping force evenly across four flat faces. This prevents bar rotation under heavy cutting loads and eliminates surface marks on your material. Our square bore is wire-cut, not broached, so the corners are sharp and the flat faces stay parallel within 0.003 mm.
Materials and Heat Treatment We Use
We start with 8620 alloy steel, then carburize and harden to 58-60 HRC. The case depth is 0.8-1.2 mm, giving a wear-resistant surface while the core stays tough for repeated spring-back. For custom orders, we also offer 4140 pre-hardened steel or stainless 17-4PH. All collets are cryogenically treated after hardening to stabilize the microstructure and prevent dimensional drift over months of use.
How We Machine the Slots and Spring Action
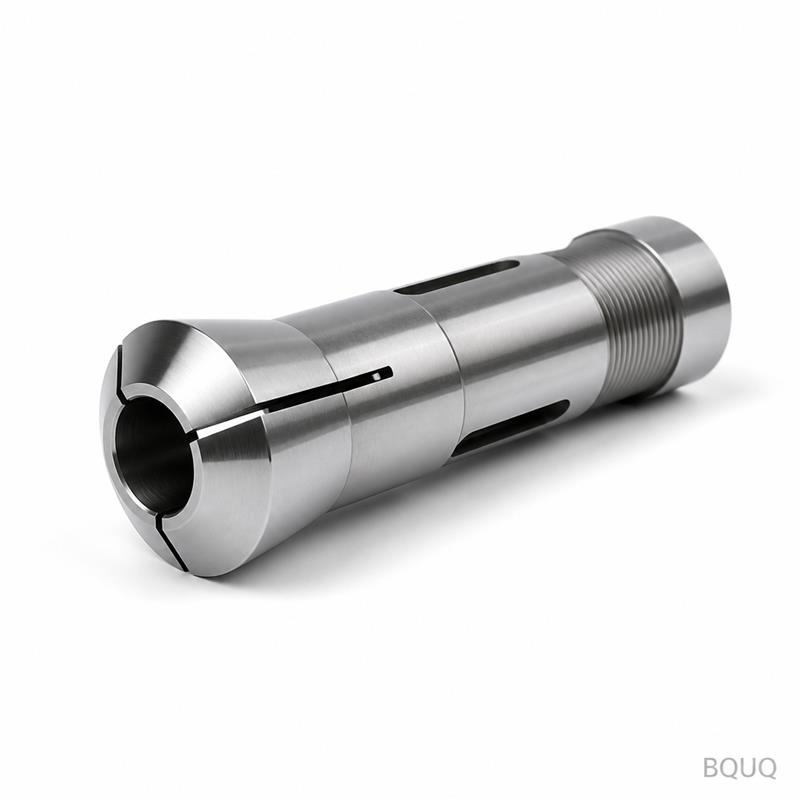
The 38 type collet has three relief slots cut by wire EDM, not milled. This gives a slot width of 0.4 mm with no burrs and no stress raisers. The spring action is tuned to close 0.2 mm under pneumatic pressure, which is the sweet spot for gripping square bar from 6 mm to 38 mm. We test each collet for opening and closing force at 0.3 MPa air pressure before packing.
Inspection Before Every Shipment
Every collet goes through a 100% dimensional check using a Zeiss CMM. We measure bore size, concentricity, and slot width on each unit. Runout is verified on a precision test arbor with a 0.001 mm indicator. We also do a hardness test on the nose and the taper. If any collet fails, it goes to scrap, not to a customer. You get a traceable inspection report with each order.
Compatibility and Fitting Notes for Your Machine
This collet matches standard 38 type auto lathe spindles from brands like Citizen, Star, and Tsugami. The taper angle is 16 degrees, and the head diameter is 38.0 mm with a -0.02 mm tolerance for a snug fit. We also offer a pull-back style and a dead-length style. If your machine uses a different pull tube thread, we can machine the back end to match your drawbar within 3 days.
Ordering Custom Sizes Without the Minimum Quantity Penalty
We do not force you to buy 100 pieces. Our standard MOQ is 1 piece for sizes between 6 mm and 38 mm. For custom bore shapes (like hex or keyway), we ask for 5 pieces to cover setup time. All custom collets are machined from solid stock in our Dongguan factory, so you get the same 10-day lead time as standard sizes. No MOQ on our catalog sizes, ever.
Hard Numbers for Your Drawing Review
| Parameter | Value | |---|---| | Material | 8620 alloy steel (case-hardened) | | Hardness | 58-60 HRC (case depth 0.8-1.2 mm) | | Bore size range | 6 mm - 38 mm square, hex, or round | | TIR (runout) at nose | 0.005 mm max | | Taper angle | 16 degrees | | Head diameter | 38.0 mm (-0.02 mm) | | Surface finish | Ra 0.4 µm on bore, Ra 0.8 µm on taper | | Slot width | 0.4 mm (wire EDM) | | Lead time (standard) | 10 working days | | Lead time (custom bore) | 12 working days | | MOQ | 1 piece (standard), 5 pieces (custom shape) |
Quality Control from Raw Bar to Finished Collet
We start with certified material that has mill test reports. After CNC turning and wire EDM slotting, each collet is stress-relieved at 190°C for 2 hours. Final grinding on the taper and bore is done in one setup to avoid concentricity errors. Before shipment, we do a 100% air-gauge check on the bore size. If your drawing calls for tighter runout than 0.005 mm, we can get to 0.003 mm with lapping, but that adds 3 days to lead time.
What is your MOQ for this collet?
No MOQ on standard sizes—you can order one piece for prototype or maintenance needs.
Can you make a collet for a non-standard square bar size?
Yes, we machine custom bore sizes from 6 mm to 38 mm in any square, hex, or rectangular profile, with a 5-piece minimum for custom shapes.
How do you verify runout on the finished collet?
We mount each collet on a precision test arbor and measure TIR with a 0.001 mm dial indicator, recording the value on your inspection report.
What is the typical lead time for a custom 38 type collet?
Standard sizes ship in 10 working days; custom bore shapes take 12 working days from drawing approval.
Get a Firm Quote Within 12 Hours
Send us your drawing or just your bar size and machine model. We will send a firm price and lead time within 12 hours, not a vague estimate. Our team in Dongguan, China handles your RFQ directly—no sales agents, no markup. Email your drawing to sc@bquq.com or reach us on WhatsApp at +86 13713157787. For more context on matching this collet to your cutting tools, read our CNC cutting tool selection guide. And if you are setting tolerances for your next job, check our CNC machining tolerances guide.