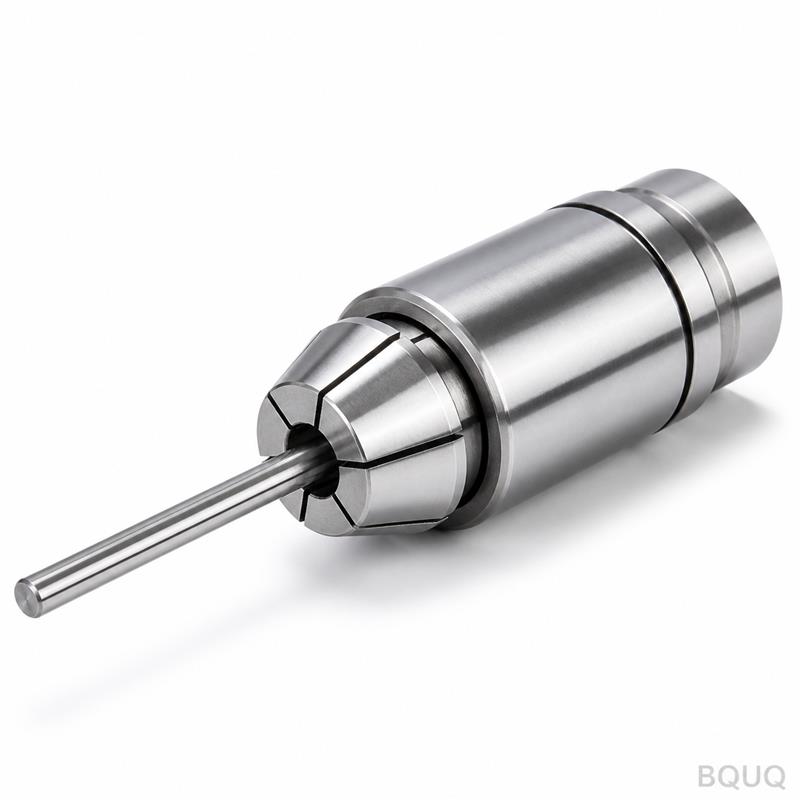
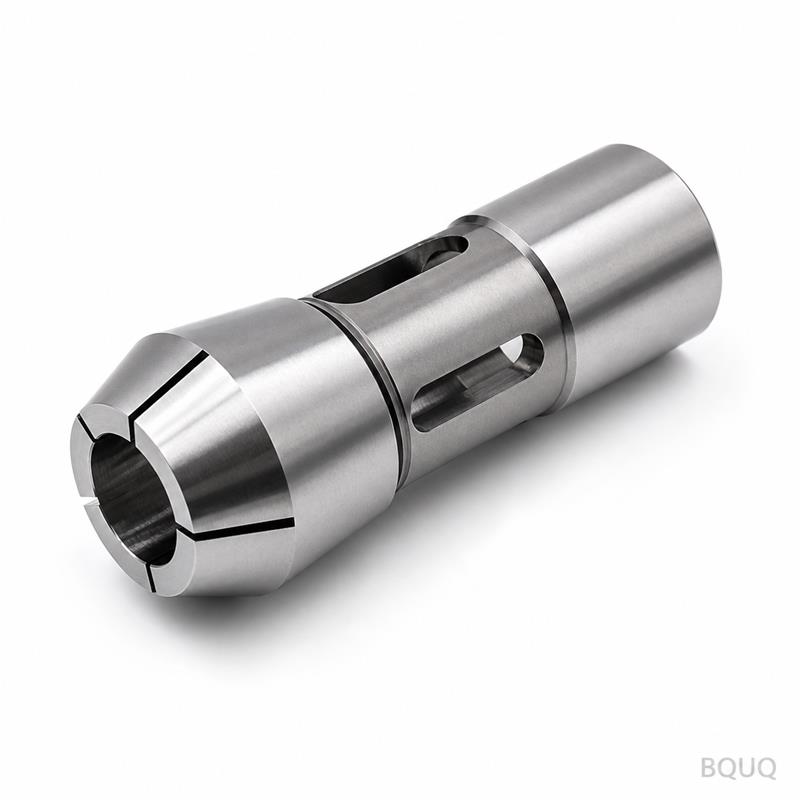
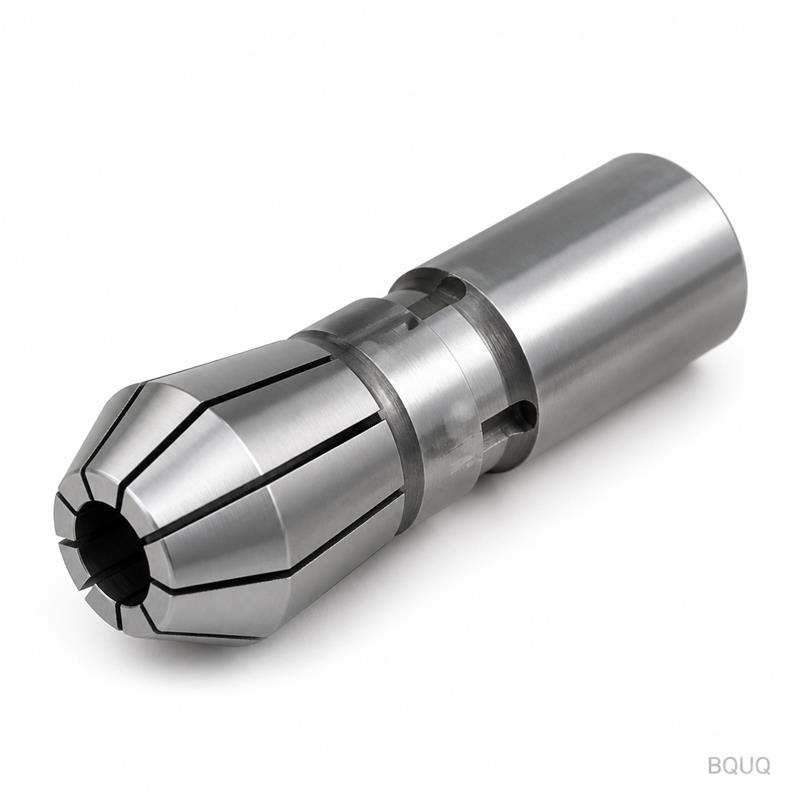
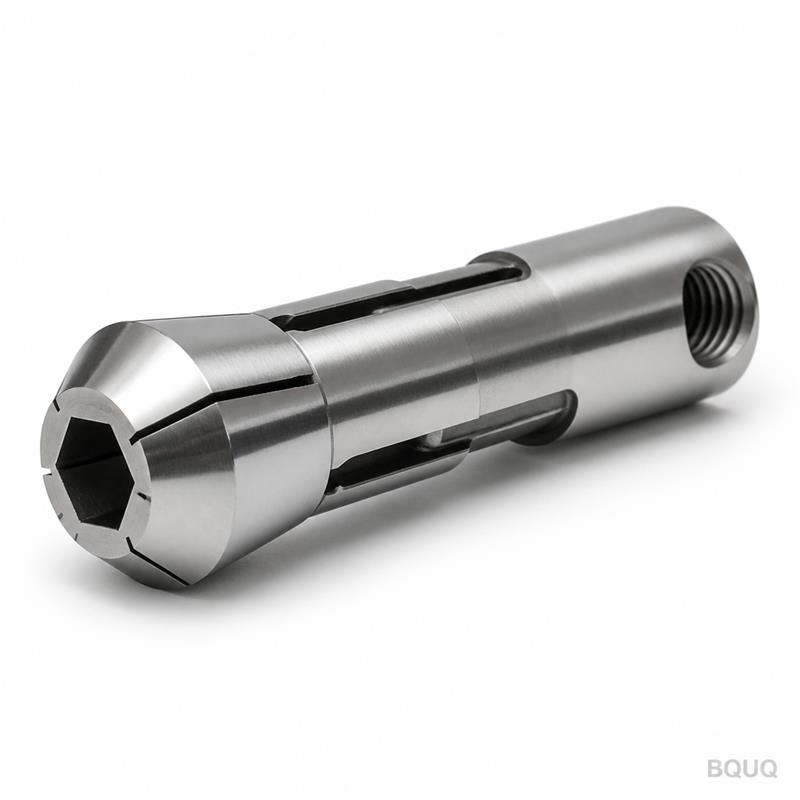
What This Collet Does and Why It Matters for Your Auto Lathe This is a CNC machined auto lathe 15 type collet designed specifically for gripping small round bars from 1.0 mm to 15.
BQUQ CNC Machined Auto Lathe 15 Type Collet With Small Round Bar
What This Collet Does and Why It Matters for Your Auto Lathe This is a CNC machined auto lathe 15 type collet designed specifically for gripping small round bars from 1.0 mm to 15.0 mm in diameter. Yo
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Collet Does and Why It Matters for Your Auto Lathe
This is a CNC machined auto lathe 15 type collet designed specifically for gripping small round bars from 1.0 mm to 15.0 mm in diameter. You get a guaranteed runout of 0.005 mm TIR (total indicated reading) at the nose, which means your turned parts stay concentric even at 8,000 RPM spindle speeds. Hardness is held at 58-60 HRC across the full gripping surface, so the collet survives over 100,000 clamping cycles without losing springback accuracy. Lead time is 7 working days for standard sizes, and we ship from our Dongguan factory with no MOQ—order one piece or one thousand.
Why the 15 Type Geometry Is Built for Small Round Bar Stock
The 15 type collet uses a 15-degree tapered seat and a single-slot relief cut, which is the optimal geometry for round bar stock under 15 mm. Unlike ER collets that use multiple slots, this design maintains a continuous cylindrical grip over 80% of the clamping length. That contact area prevents bar pushback during heavy turning passes. The internal bore is honed to a 0.4 µm Ra finish, so the bar slides in freely but locks without marring the material surface. For stainless steel or pre-hardened bar, the edge break is 0.1 mm x 45°, reducing notch stress at the grip line.
Materials and Heat Treatment We Use for 100K+ Cycles
We machine every collet from 8620 case-hardening steel, not cheap 1045. After CNC turning and slot milling, we carburize at 925°C for 4 hours to reach a case depth of 0.8-1.0 mm. The core stays tough at 32-36 HRC, while the surface hits 58-60 HRC. We then deep-freeze treat at -75°C for 2 hours to eliminate retained austenite. This is what prevents the slots from spreading open after repeated clamping. The final OD grind is done on a Studer cylindrical grinder, holding the taper to 0.003 mm over the full 30 mm seat length.
Runout Control: How We Hold 0.005 mm TIR on the Taper
Runout on a collet is not about the bore—it is about the taper that seats into the spindle. We grind the 15-degree taper and the internal bore in a single setup on a CNC grinder with a hydrostatic spindle. This eliminates any re-chucking error. Each collet is then assembled into a test holder and checked with a dial indicator at 5 mm from the nose. If the TIR exceeds 0.005 mm, we reject it. The max acceptable value for our own QC is 0.003 mm, so the parts you receive are always better than spec. For comparison, standard DIN 6499 collets allow 0.015 mm.
Inspection Before Every Shipment: Not a Sampling Plan
We do not use AQL sampling. Every single collet is inspected individually before packaging. The checks are: taper angle via air gauge (tolerance ±30 arc-seconds), bore diameter via go/no-go plug gauge, runout via a 3-jaw test fixture, and hardness via Rockwell C tester. We also do a 100-cycle load test on each lot to verify slot recovery. The inspection report is included with your shipment, showing the actual measured values for each collet. If you ask for a material certificate, it is available for every heat number.
Specification
Value
Collet Type
Auto Lathe 15 Type (15° taper)
Gripping Range
1.0 mm – 15.0 mm round bar
Material
AISI 8620 case-hardened steel
Hardness (Surface)
58-60 HRC
Hardness (Core)
32-36 HRC
Runout (TIR at nose)
0.005 mm max (typical 0.003 mm)
Surface Finish (Bore)
0.4 µm Ra
Case Depth
0.8 – 1.0 mm
Max RPM
8,000
Lead Time
7 working days (standard sizes)
MOQ
No MOQ – order 1 piece
Custom Bore Sizes for Non-Standard Bar Diameters
If your bar stock is 3.175 mm, 6.35 mm, or 12.7 mm, we can machine the bore to your exact diameter without changing the 15-type taper. Custom bores are ground to the same 0.005 mm runout and 0.4 µm Ra finish. The only difference is the bore dimension on the drawing. We can also add a coolant hole through the back face if you run through-coolant on your auto lathe. This modification takes 2 extra days on the lead time. Send us your bar OD and tolerance, and we will confirm the bore size within 24 hours.
What is the MOQ for this collet?
There is no MOQ—we accept an order for a single piece, though we offer a 5% discount for quantities over 50 pieces.
Can you machine a custom bore for my odd bar diameter?
Yes, we can grind any bore from 1.0 mm to 15.0 mm to your exact tolerance, typically within ±0.002 mm, and we just need your bar OD and material type.
How do you ensure quality on each collet?
We perform 100% inspection on taper angle, bore diameter, runout, and hardness for every piece, not a random sample, and we include the actual measured report with your shipment.
What is the actual lead time for a custom size?
Standard sizes ship in 7 working days, and custom bore sizes add 2-3 days, so the maximum lead time is 10 working days from drawing approval.
Why This Collet Works With Your CNC Cutting Tool Selection
Gripping the bar is only half the job. The other half is choosing the right insert and holder for your material. If you are cutting 303 stainless or 12L14 free-machining steel, the tool geometry changes your cycle time and surface finish. Read our CNC cutting tool selection guide to match your inserts with the rigidity this collet provides. A stiff grip means you can push feed rates higher without chatter, but only if the tool nose radius and rake angle are correct for your bar.
How This Collet Fits Into Your Overall Precision Manufacturing System
Your auto lathe is only as accurate as the weakest link in the spindle-to-tool chain. This collet holds the bar at 0.005 mm runout, but your spindle taper and draw tube also affect the final part. If you are chasing tolerances tighter than ±0.01 mm on turned diameters, check our CNC machining tolerances guide to understand how thermal expansion and tool wear stack up against your print. We make the collet to spec, but you need to control the rest of the machine environment to hit those numbers every cycle.
Shipping and Packaging for International Orders
We pack each collet in a VCI (vapor corrosion inhibitor) paper wrap, then in a foam-lined plastic tube to prevent edge damage during transit. Standard export cartons hold 20 pieces. We ship via DHL, FedEx, or UPS for small orders—delivery to the US or EU takes 3-5 days. For larger orders, we use sea freight with wooden crates that meet ISPM-15 standards. Every package includes the inspection report and a packing list. If you need a specific shipper account number, just provide it, and we will use your rate.
Get a firm quote within 12 hours. Email your drawing or bar size to sc@bquq.com, or message us on WhatsApp at +86 13713157787. We will confirm the collet type, bore size, and price for your exact requirement. No MOQ, no minimum order value, made in China. Send your drawing today.