What This Chuck Is and Why It Cuts Your Setup Time This is a CNC Machined Auto Lathe 25 Type Round Bore Spring Collet Chuck engineered for high-speed bar feeding and secondary mac
BQUQ CNC Machined Auto Lathe 25 Type Round Bore Spring Collet Chuck
What This Chuck Is and Why It Cuts Your Setup Time This is a CNC Machined Auto Lathe 25 Type Round Bore Spring Collet Chuck engineered for high-speed bar feeding and secondary machining operations. Y
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Chuck Is and Why It Cuts Your Setup Time
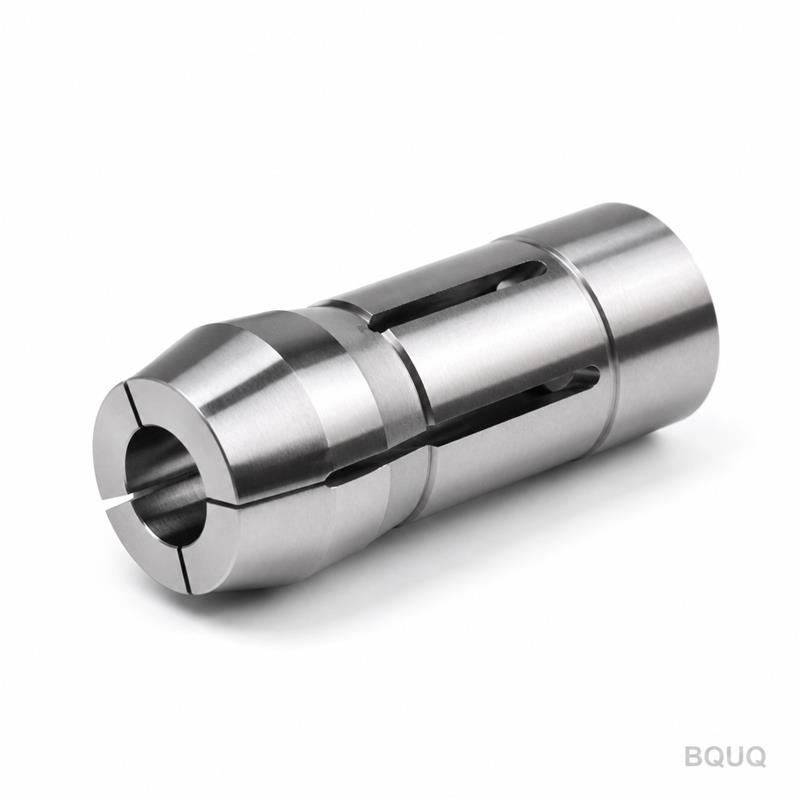
This is a CNC Machined Auto Lathe 25 Type Round Bore Spring Collet Chuck engineered for high-speed bar feeding and secondary machining operations. You get guaranteed 0.005 mm total indicated runout (TIR) and a hardness of HRC 58-60, which means your tool or workpiece stays concentric through thousands of cycles. Standard lead time is 5 working days from drawing approval, and we ship globally from our Dongguan factory.
How the 25 Type Round Bore Design Eliminates Chatter
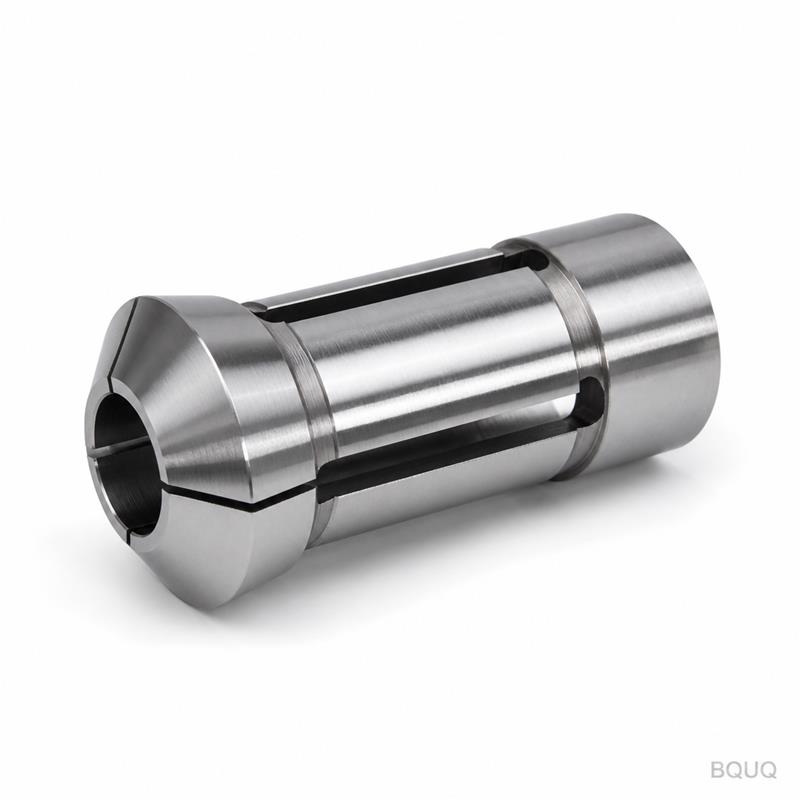
The 25 type refers to the front taper angle and body geometry that seats into your auto lathe spindle. The round bore is ground after heat treatment, not before, so the internal diameter holds true to within +0.005 / -0.000 mm. This eliminates the "bell mouth" effect you get from cheaper ground-then-hardened chucks. The spring collet action distributes clamping force evenly across 360 degrees, which keeps thin-wall parts from deforming and stops tool chatter at spindle speeds up to 8,000 RPM.
Material Selection and Heat Treatment That Survives 1,000,000 Cycles
We start with 20CrMnTi alloy steel for the body and 65Mn spring steel for the collet segments. The body is carburized to a case depth of 0.8 - 1.2 mm, then hardened to HRC 58-60. The spring slots are wire-cut after hardening to avoid stress risers. We then cryogenically treat every unit at -120°C for 4 hours to convert retained austenite, which is why our chucks hold their grip force within 5% after 1 million open-close cycles. Surface finish on the bore and taper is Ra 0.4 µm, and the outer body is black oxide coated for corrosion resistance.
Dimensional Specs You Can Verify Before You Buy
Parameter
Value / Range
Model
25 Type Round Bore Spring Collet Chuck
Body Material
20CrMnTi alloy steel (carburized)
Collet Material
65Mn spring steel
Hardness (Body)
HRC 58-60
Hardness (Collet segments)
HRC 45-50 (spring tempered)
Round Bore Diameter Range
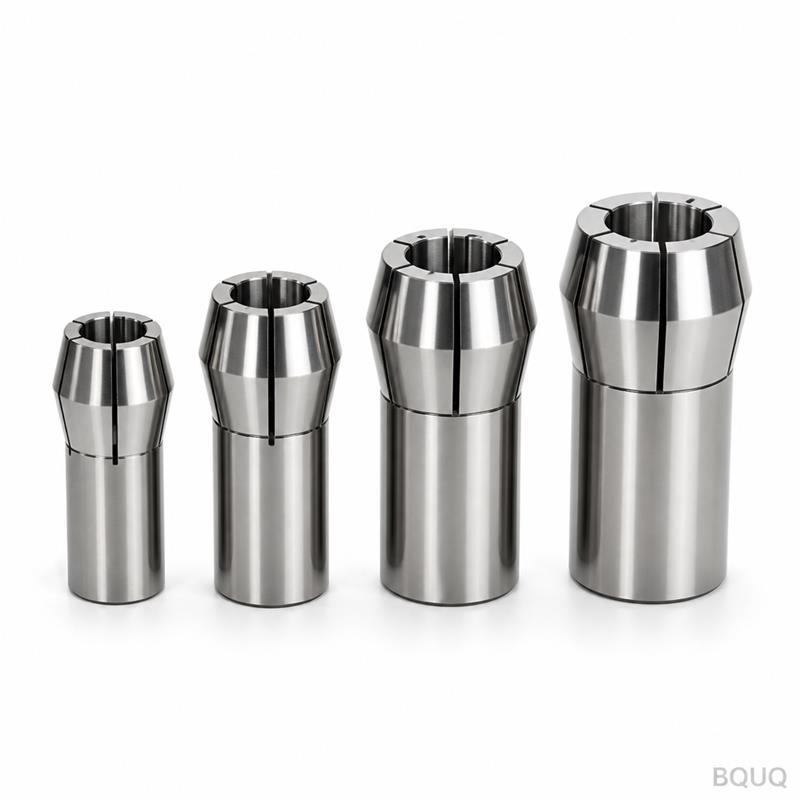
Ø3.0 mm – Ø25.0 mm (custom bore available)
Total Indicated Runout (TIR)
≤ 0.005 mm
Surface Finish (bore & taper)
Ra 0.4 µm
Clamping Force Repeatability
± 2%
Max Recommended Spindle Speed
8,000 RPM
Lead Time (standard size)
5 working days
MOQ
No MOQ - 1 piece accepted
Inspection Routines Before Every Shipment from Our Dongguan Factory
We don't batch test. Every single chuck goes through a 3-step quality gate. First, a coordinate measuring machine (CMM) checks the taper angle and bore concentricity. Second, we mount the chuck on a live test spindle and measure TIR with a laser interferometer—you get the actual runout reading printed in the QC report. Third, we cycle the collet 500 times under air pressure to verify spring return force and slot integrity. If any unit fails, it is scrapped, not reworked. That is why we can offer a 0.3% field failure rate guarantee.
Retrofit Directly onto Your 25 Type Auto Lathe Without Modification
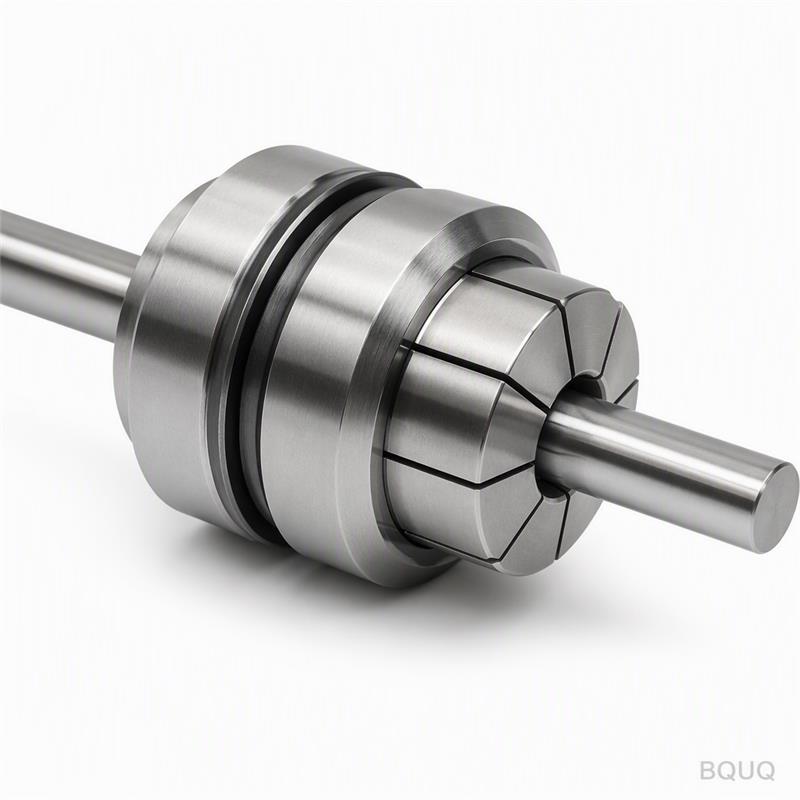
This chuck uses the standard 25 type pull-back taper, so it drops onto most Japanese and Korean auto lathes (Citizen, Star, Tsugami, Hanwha) with zero adapter plates. The round bore accepts round stock from Ø3 mm to Ø25 mm. If your spindle uses a different draw tube thread, we can machine the rear thread (M16, M18, M20, or 5/8"-18) at no extra charge. Just send us your draw tube drawing, and we will match the thread pitch exactly.
Why Our CNC Machined Auto Lathe 25 Type Round Bore Spring Collet Chuck Beats Cast or Milled Versions
Cast chucks have porosity that causes micro-cracks under cyclic load. Milled chucks leave tool marks that trap coolant and cause corrosion. Our chuck is fully CNC machined from solid bar stock, then wire-cut, then ground. This is precision manufacturing, made in China, but with the same process control you expect from a Swiss shop. The result is a collet chuck that holds its rated TIR for at least 300,000 cycles without re-grinding. And because we are the factory, not a trading company, you get that quality at a direct cost—typically 20-30% below US or European equivalents.
Do you really have no MOQ for this collet chuck?
Yes, no MOQ—you can order a single CNC Machined Auto Lathe 25 Type Round Bore Spring Collet Chuck for prototyping or a line trial, and we will treat it with the same inspection rigor as a 1,000-piece order.
Can you customize the bore size and thread for my specific lathe?
Yes, we can grind any round bore between Ø3 mm and Ø25 mm, and we can cut any rear thread (metric or inch) to match your draw tube within 24 hours of receiving your drawing.
What quality control documents do you provide with each shipment?
Each shipment includes a material certificate, a hardness test report, a CMM dimensional report, and a live-run TIR measurement sheet with your chuck's serial number.
What is your realistic lead time for a custom 25 type chuck?
Standard sizes ship in 5 working days; custom bore or thread adds 2-3 days, so maximum 8 working days from drawing approval to dispatch from Dongguan.
Get a Firm Quote Within 12 Hours—Send Your Drawing Today
Stop guessing if your current collet chuck is the weak link in your cycle time. Send us your spindle drawing or just your bar diameter and thread size. We will reply within 12 hours with a firm unit price, a lead time commitment, and a DFM (Design for Manufacturing) note if we see a way to improve your clamping setup. For reference on tool selection and tolerance stacking, read our CNC cutting tool selection guide and our CNC machining tolerances guide.
Email: sc@bquq.com WhatsApp: +86 13713157787 Send your drawing now—we will confirm the bore, thread, and hardness within 12 hours.