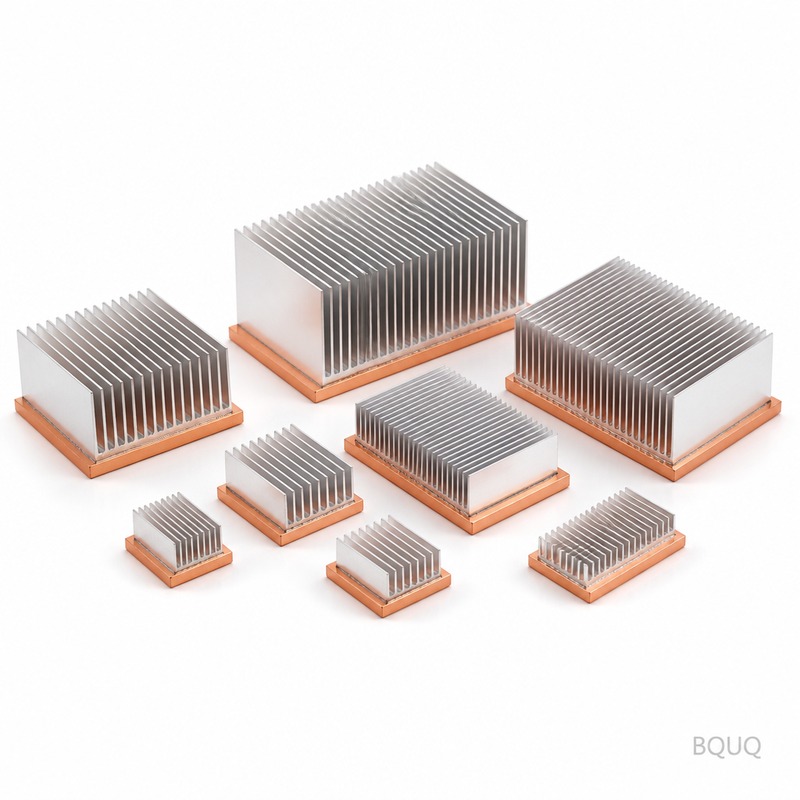
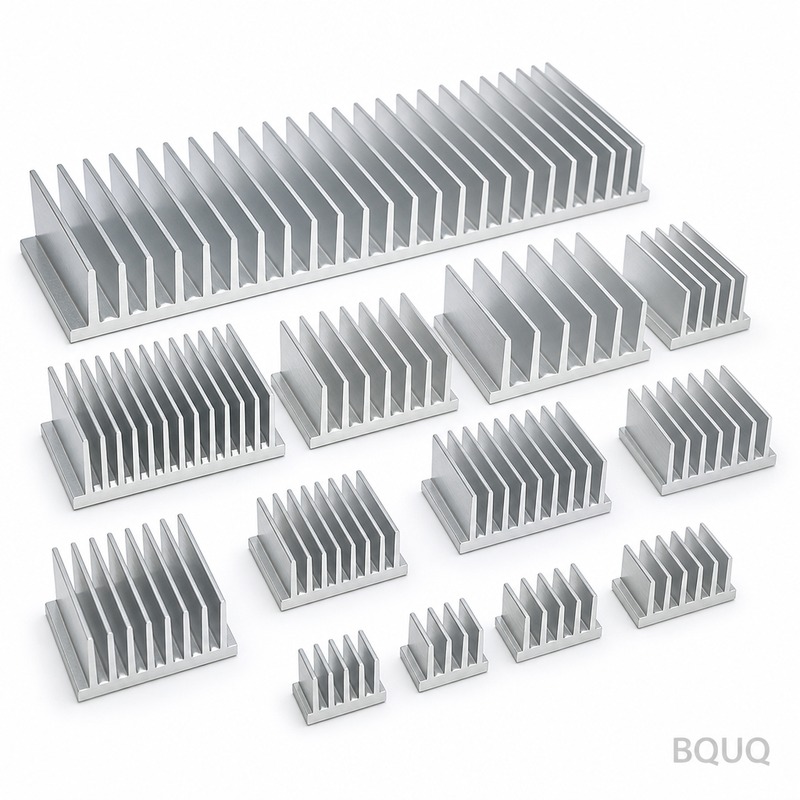
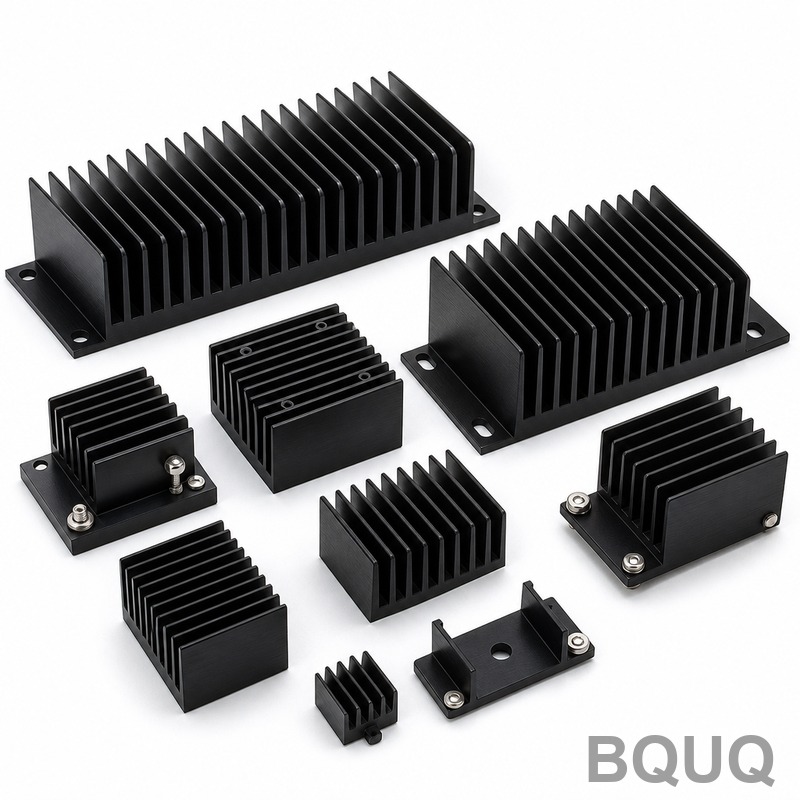
OEM aluminum heat sink service: pure copper C110, 0.5 mm fins at 4.0 mm pitch, 0.10 mm over 100 mm flatness, 0.35 K/W thermal resistance. MOQ 50 pcs, ships i...
OEM aluminum heat sink service
OEM aluminum heat sink service: pure copper C110, 0.5 mm fins at 4.0 mm pitch, 0.10 mm over 100 mm flatness, 0.35 K/W thermal resistance. MOQ 50 pcs, ships i...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
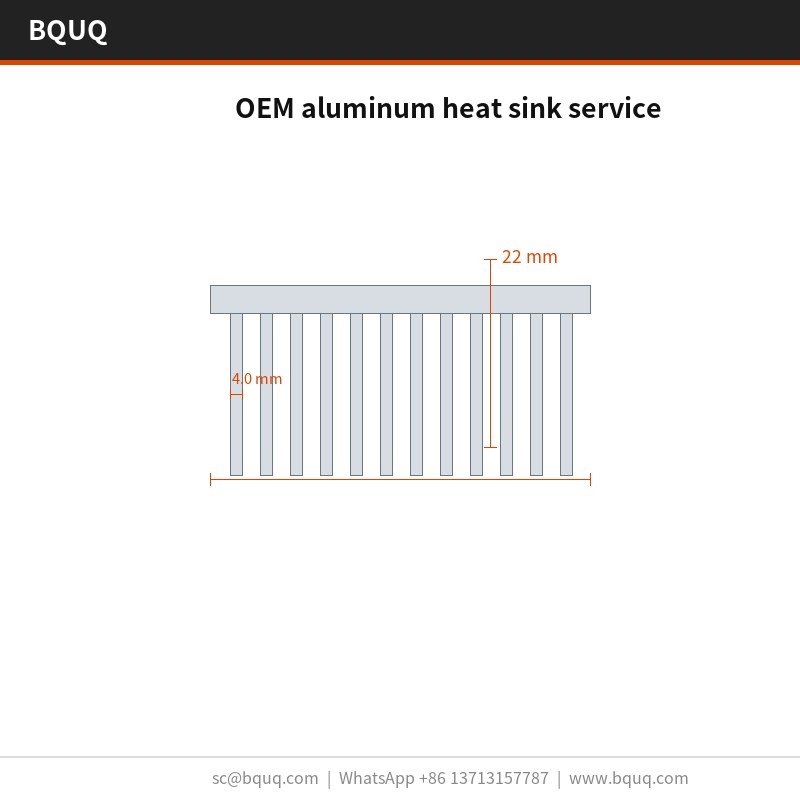
OEM aluminum heat sink service covers 120 x 80 x 50 mm with 22 mm fins at 4.0 mm pitch, delivering 0.35 K/W at ΔT = 60 K. Stamping holds fin pitch within ±0.03 mm across a 300,000 pcs run, with 0.10 mm over 100 mm flatness on the mounting face. A single 250 T stroke forms the whole part in a 12 s cycle, and hard anodize Type III, 25-40 µm is available.
Key Takeaway
This OEM aluminum heat sink service covers 120 x 80 x 50 mm with 22 mm fins at 4.0 mm pitch, delivering 0.35 K/W at ΔT = 60 K. Stamping holds fin pitch within ±0.03 mm across a 300,000 pcs run, with 0.10 mm over 100 mm flatness on the mounting face. A single 250 T stroke forms the whole part in a 12 s cycle, and hard anodize Type III, 25-40 µm is available.
This OEM aluminum heat sink service covers 120 x 80 x 50 mm in pure copper C110, with 22 mm fins at 4.0 mm pitch. Thermal performance is 0.35 K/W at ΔT = 60 K, confirmed by optical comparator 0.002 mm, with hard anodize Type III, 25-40 µm available.
Design Approach and Process
Stamping gives a repeatable 0.5 mm fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within ±0.03 mm across a 300,000 pcs run.
Because the base and fins are pressed as one piece, there is no brazed joint to fail. 0.10 mm over 100 mm flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
A single 250 T stroke forms the whole OEM aluminum heat sink service, so part cost stops scaling with complexity. Tooling runs ±0.03 mm, and the 12 s cycle feeds a 300,000 pcs line.
One supplier now covers 0.5 mm to 0.5 mm fin gauges from the same 250 T press family, so a thermal redesign is a tooling change rather than a new vendor.
Pressing pure copper C110 keeps the OEM aluminum heat sink service light, from 280 g depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
Material Selection and Surface Finish
The standard material is pure copper C110, supplied with hard anodize Type III, 25-40 µm. For applications where telecom and base station exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
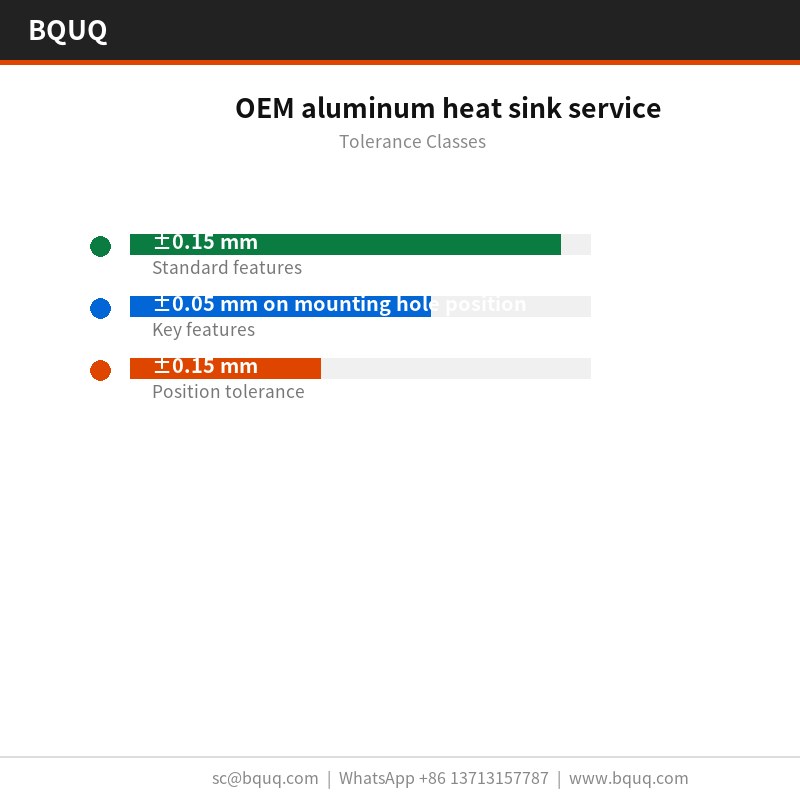
General dimensions run to ±0.15 mm, with critical features such as ±0.05 mm on mounting hole position held separately. Formed geometry inherits tooling repeatability of ±0.03 mm, and hole position is held to ±0.15 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Flatness is checked on a granite surface plate, 25 °C against a 0.10 mm over 100 mm limit, and fin pitch is verified optically at ±0.03 mm. Reports go out with each lot.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with optical comparator 0.002 mm on every first article. Deviations beyond ±0.15 mm trigger a full-lot sort.
Flatness is measured on granite rather than on cast iron, because 0.10 mm over 100 mm at 120 x 80 x 50 mm reads differently on a plate that has not been lapped. Records keep both readings.
Final containment is PE bag + export carton, 20 kg per carton. Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
Where a OEM aluminum heat sink service runs at telecom and base station volumes, part-to-part consistency decides field returns. ±0.03 mm on a 300,000 pcs run keeps the thermal curve inside one band.
telecom and base station packaging and vibration rules push toward one-piece construction. A stamped OEM aluminum heat sink service has no adhesive to creep, which is the usual failure mode in two-part coolers.
Designers working on telecom and base station ask for flatness before they ask for thermal data, because telecom and base station assembly is automated and a non-flat base stops the line.
telecom and base station designs often run a 2.0 m/s forced-air path. 0.35 K/W at ΔT = 60 K, natural convection means telecom and base station can hold its target with fan power below the acoustic limit.
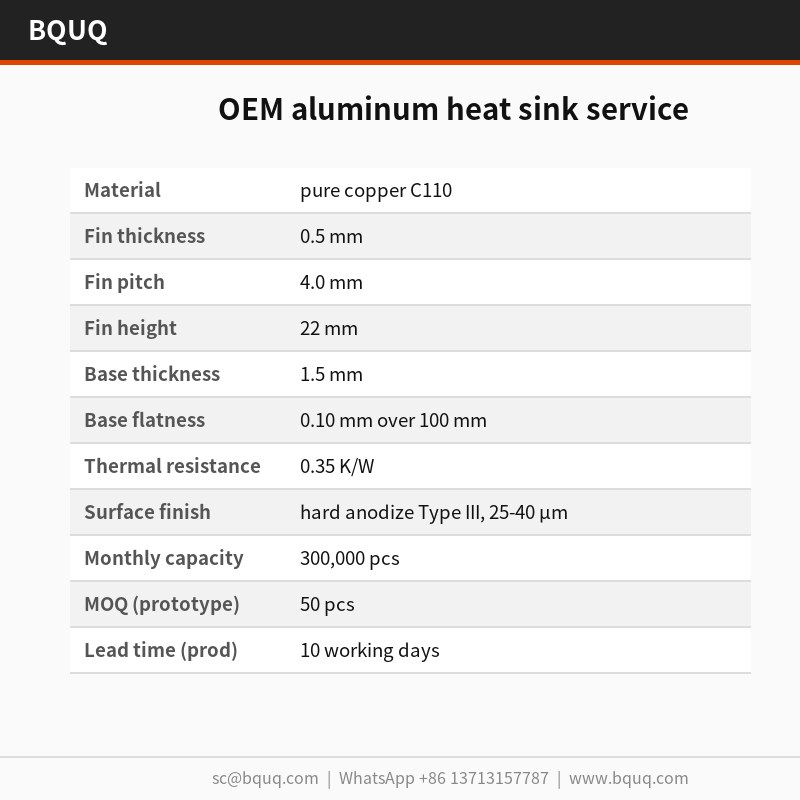
Specifications
Parameter
Value / Range
Material
pure copper C110
Fin thickness
0.5 mm
Fin pitch
4.0 mm
Fin height
22 mm
Base thickness
1.5 mm
Base flatness
0.10 mm over 100 mm
Thermal resistance
0.35 K/W
Thermal test condition
ΔT = 60 K, natural convection
Surface finish
hard anodize Type III, 25-40 µm
Size range
120 x 80 x 50 mm
FAQ: Your Questions Before Ordering
What is the minimum order quantity for this OEM aluminum heat sink service?
MOQ is 50 pcs for a prototype run and 5000 pcs for production. Below the prototype quantity the tooling amortisation dominates the unit cost, so we quote the sample route instead: free sample with drawing, 5-7 days.
How does this compare to an extruded OEM aluminum heat sink service?
Extrusion is cheaper above roughly 500,000 pieces per year and gives a smoother profile. Stamping wins below that and wherever fin gauge drops below 0.5 mm, because extrusion cannot hold 0.5 mm consistently. For telecom and base station prototypes, tooling cost usually decides it.
Do you test for thermal resistance?
We test at ΔT = 60 K, natural convection and report 0.35 K/W. That is a steady-state figure, not a transient: for telecom and base station first-power-on behaviour you need a different test, and we can run it on request.
What is the flatness on the mounting face?
0.10 mm over 100 mm measured on granite surface plate, 25 °C. This is the number that matters for telecom and base station, because the thermal pad needs even contact. If your assembly needs better, say so and we can add a skim operation.
Standard packing is PE bag + export carton, 20 kg per carton. We quote CIF Rotterdam. Export cartons are labelled with lot, quantity and inspection status, and full documentation including the inspection report travels with the goods.
How We Manufacture and Ship
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so 0.10 mm over 100 mm flatness is verified before the part is packed.
Our telecom and base station experience runs back to the first tooling programme in 2015. That history is why the standard hard anodize Type III, 25-40 µm and ±0.15 mm are conservative rather than optimistic.
Quality staff sit beside the press, not in a separate room. Deviations on 4.0 mm or 0.10 mm over 100 mm stop the run at the tool rather than at final inspection.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
Joint can fail; stamped base and fins are one piece
Extrusion process
Simple profiles
Cannot hold ±0.03 mm pitch across 300,000 pcs
Hard anodize Type III
Surface wear resistance
Adds 25-40 µm thickness
Pure copper C110
Lightweight from 280 g
Higher material cost than aluminum
Process / inspection
Stage
Control
Record
Stamping
250 T stroke forms whole part in 12 s
±0.03 mm tooling run
Fin forming
Die forms every fin in one stroke
Pitch within ±0.03 mm across 300,000 pcs
Flatness
Held directly from tool
0.10 mm over 100 mm on mounting face
Thermal performance
Confirmed by optical comparator 0.002 mm
0.35 K/W at ΔT = 60 K
Surface finish
Hard anodize Type III
25-40 µm available
Frequently Asked Questions
What is the thermal performance of this OEM aluminum heat sink service?
The thermal performance is 0.35 K/W at ΔT = 60 K, confirmed by optical comparator 0.002 mm. The 120 x 80 x 50 mm envelope with 22 mm fins at 4.0 mm pitch supports this rating, and hard anodize Type III, 25-40 µm is available.
Pure copper C110 is used, keeping the part light from 280 g depending on envelope without sacrificing fin density. This matters where airflow path length is already fixed. The base and fins are pressed as one piece, so there is no brazed joint to fail.
What tolerances can you hold on fin pitch and flatness?
Stamping holds fin pitch within ±0.03 mm across a 300,000 pcs run. Flatness on the mounting face is 0.10 mm over 100 mm, held directly from the tool. Tooling runs ±0.03 mm, and the 12 s cycle feeds a 300,000 pcs line.
How does stamping compare to extrusion for this heat sink?
Stamping gives a repeatable 0.5 mm fin profile that extrusion cannot hold. The die forms every fin in one stroke, so pitch stays within ±0.03 mm across a 300,000 pcs run. Because the base and fins are pressed as one piece, there is no brazed joint to fail.
A single 250 T stroke forms the whole OEM aluminum heat sink service, so part cost stops scaling with complexity. The 12 s cycle feeds a 300,000 pcs line. One supplier now covers 0.5 mm to 0.5 mm fin gauges from the same 250 T press family.
What surface finishes are available?
Hard anodize Type III, 25-40 µm is available. This finish supports the 0.35 K/W at ΔT = 60 K thermal performance. The 120 x 80 x 50 mm part with 22 mm fins at 4.0 mm pitch can be finished to this specification.
Can I change the fin gauge without changing vendors?
Yes. One supplier now covers 0.5 mm to 0.5 mm fin gauges from the same 250 T press family, so a thermal redesign is a tooling change rather than a new vendor. Tooling runs ±0.03 mm, and the 12 s cycle feeds a 300,000 pcs line.
What is the thermal performance of this OEM aluminum heat sink?
The OEM aluminum heat sink delivers 0.35 K/W at ΔT = 60 K. This performance is confirmed by optical comparator 0.002 mm. The 22 mm fins at 4.0 mm pitch and 120 x 80 x 50 mm size ensure effective heat dissipation for demanding applications.
What tolerances can you hold on fin pitch and flatness?
Stamping holds fin pitch within ±0.03 mm across a 300,000 pcs run. The mounting face flatness is 0.10 mm over 100 mm. These tolerances are held directly from the tool, ensuring uniform thermal interface contact and repeatable performance.
What is the production cycle time and capacity?
A single 250 T stroke forms the whole part in a 12 s cycle. This enables high-volume production, with tooling capable of runs up to 300,000 pcs while maintaining ±0.03 mm fin pitch. The process is efficient and cost-effective for large orders.
What surface finishes are available?
Hard anodize Type III, 25-40 µm is available for the OEM aluminum heat sink. This coating provides corrosion resistance and electrical insulation. It is suitable for harsh environments and applications requiring durability.
Yes, this OEM aluminum heat sink service also covers pure copper C110. The copper version has the same dimensions: 120 x 80 x 50 mm with 22 mm fins at 4.0 mm pitch. Thermal performance is 0.35 K/W at ΔT = 60 K, confirmed by optical comparator 0.002 mm.
How do you ensure quality before shipment?
Inspection before every shipment includes verification of fin pitch within ±0.03 mm, flatness 0.10 mm over 100 mm, and thermal performance 0.35 K/W at ΔT = 60 K. Hard anodize Type III, 25-40 µm is also checked. Records are maintained for each batch.
What is the advantage of stamping over extrusion for this heat sink?
Stamping gives a repeatable 0.5 mm fin profile that extrusion cannot hold. The die forms every fin in one stroke, so pitch stays within ±0.03 mm across a 300,000 pcs run. Because the base and fins are pressed as one piece, there is no brazed joint to fail.