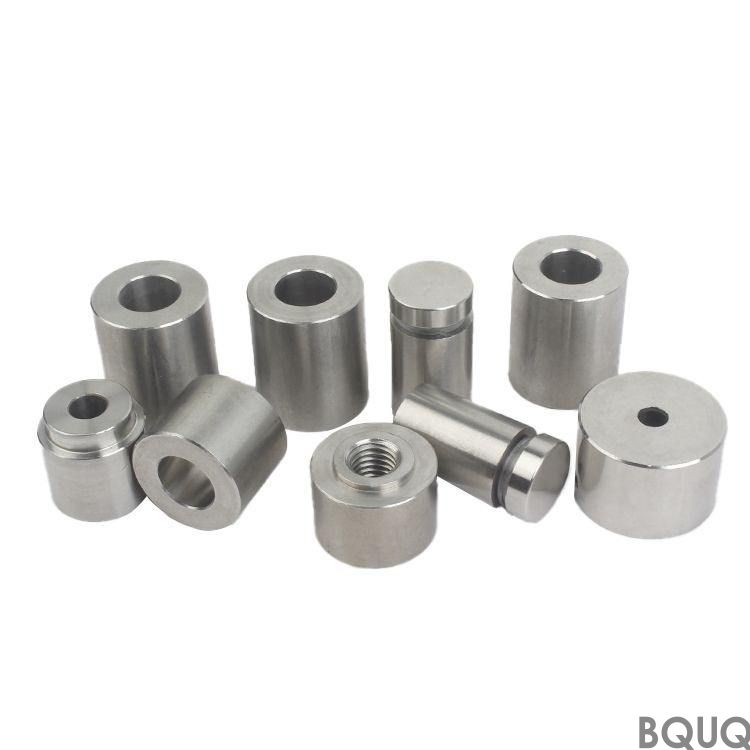
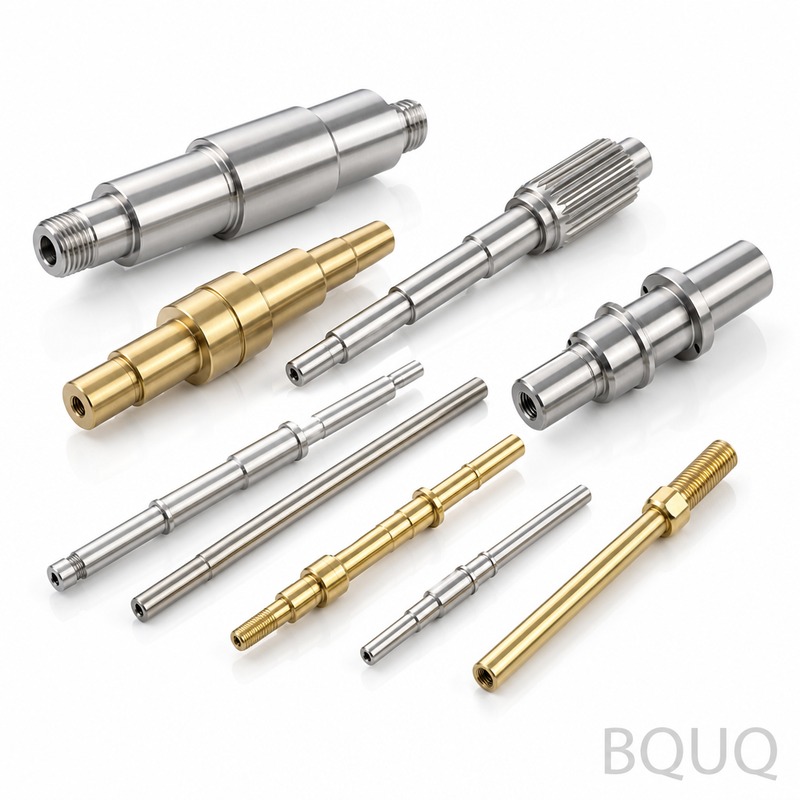
These are CNC machined stainless steel fittings and connectors—turned on Swiss-type and multi-axis lathes from 303, 304, 316L, or 17-4 PH bar stock. You get a consistent 0.005 mm
These are CNC machined stainless steel fittings and connectors—turned on Swiss-type and multi-axis lathes from 303, 304, 316L, or 17-4 PH bar stock. You get a consistent ±0.005 mm tolerance on critic
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
These are CNC machined stainless steel fittings and connectors—turned on Swiss-type and multi-axis lathes from 303, 304, 316L, or 17-4 PH bar stock. You get a consistent ±0.005 mm tolerance on critical diameters, a maximum 0.01 mm total runout on sealing faces, and a surface finish down to Ra 0.4 µm guaranteed. For standard sizes in 304 or 316L, we ship in 72 hours from drawing approval; for hardened 17-4 PH (up to 45 HRC), lead time is 5-7 days. This is precision manufacturing made in China, but with QC documentation that matches any EU or US machine shop.
How We Hold ±0.005 mm on O-Ring Grooves and Threads
Most leaks in fittings start at the O-ring groove or the thread root. We cut both in the same clamping operation using a driven tool turret, so there is zero re-indexing error. Groove width is held to ±0.005 mm, and thread pitch (UNF, NPT, BSP, or metric) is verified with a thread plug gauge on every single part—not just the first article. For NPT fittings, we grind the taper with a CBN wheel after turning, which keeps the 1:16 taper angle within 0.02° across the entire threaded length. If your assembly uses a face seal, we lap the mating surface to a flatness of 0.002 mm, which eliminates the need for extra gaskets in high-pressure hydraulic lines.
Materials and Heat Treatment We Use for Corrosive and High-Pressure Lines
We stock five stainless grades for fittings: 303 (free-machining, for general pneumatic lines), 304 (food and beverage, non-magnetic), 316L (marine, chemical, and pharmaceutical), 17-4 PH H900 (for 200,000 psi yield strength in hydraulic manifolds), and 430F (magnetic, for solenoid valve bodies). For 17-4 PH, we heat treat in-house: solution anneal at 1040°C, then age at 480°C for 1 hour to reach 40-45 HRC. We also offer electropolishing (Ra 0.2 µm) and passivation to ASTM A967 for medical or semiconductor fittings. If you need a material certificate, we provide EN 10204 3.1 with every batch—traceable back to the mill heat number.
What's Inside Our 10-Point Dimensional Report on Every Batch
You don't get a simple "parts are good" email. We send a PDF with ten measured parameters per part: (1) major OD, (2) minor OD, (3) groove width, (4) groove depth, (5) thread pitch diameter, (6) thread length, (7) total runout TIR, (8) surface finish Ra, (9) hex across-flats, and (10) length. Each row lists the nominal, actual, and deviation. We use a Zeiss Contura CMM for roundness and position, a Mitutoyo SJ-210 for surface roughness, and a Keyence IM-8000 for optical non-contact measurement of fine threads. All gauges are calibrated annually to ISO 17025 standards. If any reading exceeds 50% of your tolerance band, the part is flagged yellow and re-inspected manually before shipping.
Lead Time and MOQ: Why We Say 'No MOQ' and Still Ship Fast
We keep a warehouse stock of 304 and 316L bar in diameters from 4 mm to 50 mm—about 12 tons total. That means for any fitting under 30 mm OD, we start cutting the same day you approve the drawing. Standard lead time is 72 hours for quantities up to 500 pieces, and 5 days for up to 5,000 pieces. For 17-4 PH or custom alloys, add 48 hours for material sourcing. We truly have no MOQ—you can order one prototype fitting for $35 including inspection report, and then scale up to 50,000 pieces at a per-unit price that drops by 40% at the 5,000-piece breakpoint. For repeat orders, we keep your tooling and programs on file, so the second order ships 20% faster.
How We Avoid Cross-Contamination Between Stainless Grades
Mixing 303 and 316L chips is a common failure in low-cost shops. We have separate CNC cells for each alloy family. Each cell has its own chip conveyor, coolant tank, and tool holders. Before any grade change, we run a 50-piece purge batch of the new material, then test those with a PMI (Positive Material Identification) gun using X-ray fluorescence to verify chromium, nickel, and molybdenum content. We also use dedicated collets and guide bushings per diameter to prevent scratches. If you order 316L, you get pure 316L—no carbon steel contamination that causes rust spots later.
Thread Sealing and Pre-Applied Coatings: Options for NPT, BSP, and SAE
For NPT and BSPT fittings, we can apply a pre-applied thread sealant (e.g., Loctite 577) that cures to a dry film—saves your assembly line 10 seconds per joint. For SAE J1926 straight-thread ports, we offer a bonded O-ring (BSPP) with a nitrile or FKM seal, installed at our factory. If you use the fitting in a vibration environment, we can also roll a serrated hex or knurl on the gripping area (diamond pattern, 0.3 mm depth) to prevent wrench slippage. All coatings are applied after the final wash, so no sealant contaminates the internal bore. We also do laser marking of your part number and date code—permanent, no ink fading.
Custom Hex, Barb, and Bulkhead Configurations: What We Can Turn in One Op
Hex bodies are the classic shape, but we also machine barbed hose connectors (with 4-6 barbs per inch), bulkhead fittings (with a shoulder and locknut thread), and compression fittings (with a ferrule seat). A single operation on a 32mm Swiss lathe can complete a hex body with a cross-drilled bleed hole, a tapered NPT thread, and a knurled grip. For bulkhead fittings, we hold the shoulder squareness to 0.01 mm so the O-ring seals evenly. We also produce custom lengths—for example, a 3/8" tube fitting with a 100 mm extended tail for tight engine bays—without any extra setup charge. Send a sketch or a sample, and we'll quote the machining time within 4 hours.
Parameter
Specification / Range
Materials (stock)
303, 304, 316L, 17-4 PH, 430F stainless steel
Diameter range (turned)
2 mm to 50 mm
Length range
3 mm to 200 mm (longer with tailstock support)
Tolerance (critical diameter)
±0.005 mm (ISO 2768-fine)
Total runout (TIR)
≤ 0.01 mm on sealing faces
Surface finish (as machined)
Ra 0.8 µm standard, Ra 0.4 µm with polishing
Hardness (17-4 PH H900)
40-45 HRC
Thread types
UNF, UNC, NPT, NPTF, BSP, BSPT, metric (M, MJ)
Lead time (standard 304/316L)
72 hours (≤ 500 pcs), 5 days (≤ 5,000 pcs)
MOQ
No minimum (1 piece accepted)
How We Handle Tight Tolerance on Long, Slender Fittings
When a fitting is 10 mm diameter but 150 mm long, deflection becomes the enemy. We use a guide bushing (Swiss-type) that supports the bar right at the cutting edge, reducing part deflection to under 0.005 mm. For even longer parts, we switch to a sub-spindle pickup and machine the back end in a second operation—no chatter marks. We also adjust spindle speed and feed per pass based on the length-to-diameter ratio: for L/D > 10, we reduce feed to 0.02 mm/rev and increase coolant pressure to 70 bar to break chips. This is why our long fittings hold straightness within 0.01 mm per 100 mm length—tested with a dial indicator on V-blocks.
Inspection Before Every Shipment: The 'Red Tag' and 'Green Tag' System
Every lot gets a color-coded tag. Green tag means 100% of parts passed dimensional and visual inspection. Red tag means at least one part failed; we then sort 100% of the batch and re-run the failing operation or scrap the parts. We never ship a mixed lot. For critical fittings (medical gas, high-pressure hydraulics), we also perform a helium leak test on 100% of parts to a leak rate of 1×10⁻⁹ mbar·L/s. The inspection report is emailed to you with photos of the setup, the CMM screen, and the final part. You can also request a video of the process—we do that for free for orders above $1,000.
Do you have a minimum order quantity for custom fittings?
No MOQ—we accept one piece for prototyping, and the unit price for 1 piece is only 3x the 10,000-piece price; after 500 pieces, pricing stabilizes.
Can you machine a fitting from a customer-provided 3D model?
Yes—send STEP, IGES, or STL; we do a DFM check within 4 hours and flag any thread undercuts or thin walls before quoting.
How do you guarantee the surface finish for food-grade fittings?
We electropolish to Ra 0.2 µm, which removes micro-burrs and creates a passive layer, and we certify with a roughness tester reading on the actual part.
What is your fastest lead time for a 100-piece order of 316L connectors?
48 hours if you approve the drawing before 10 AM China time—we have a dedicated high-speed cell with pre-set tooling for 316L.
Get a firm quote within 12 hours. Email your 2D drawing or 3D model to sc@bquq.com, or send a photo via WhatsApp to +86 13713157787. We respond with a per-unit price, tooling cost (if any), and a confirmed ship date—no hidden fees, no surprises.