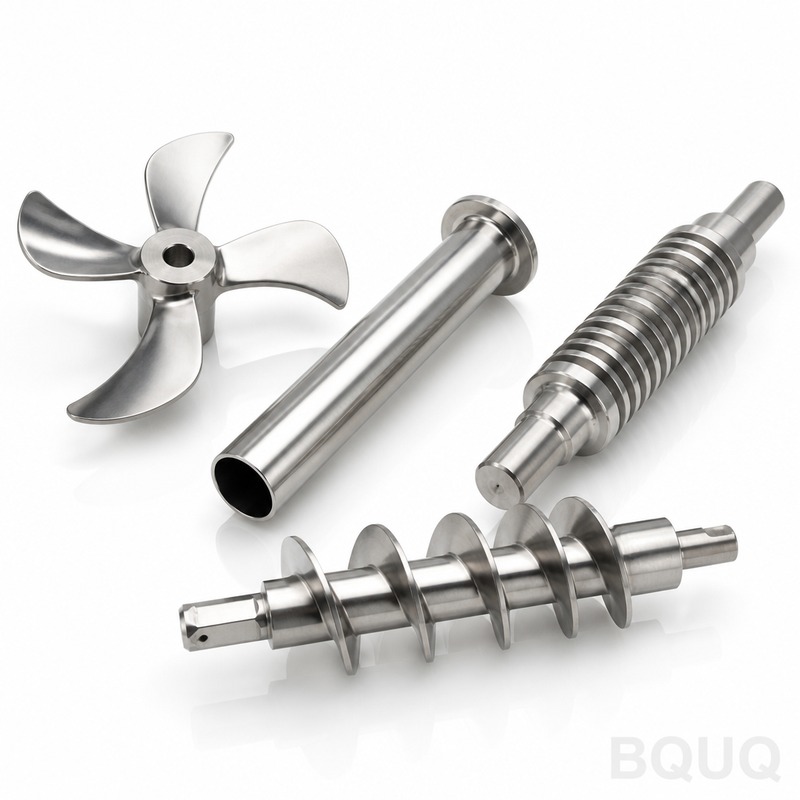
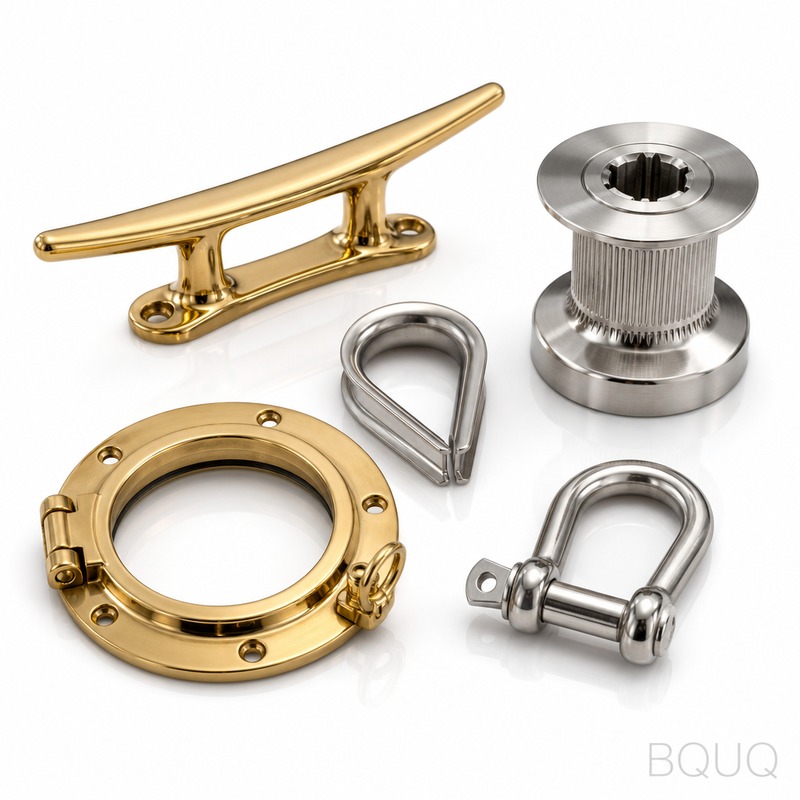
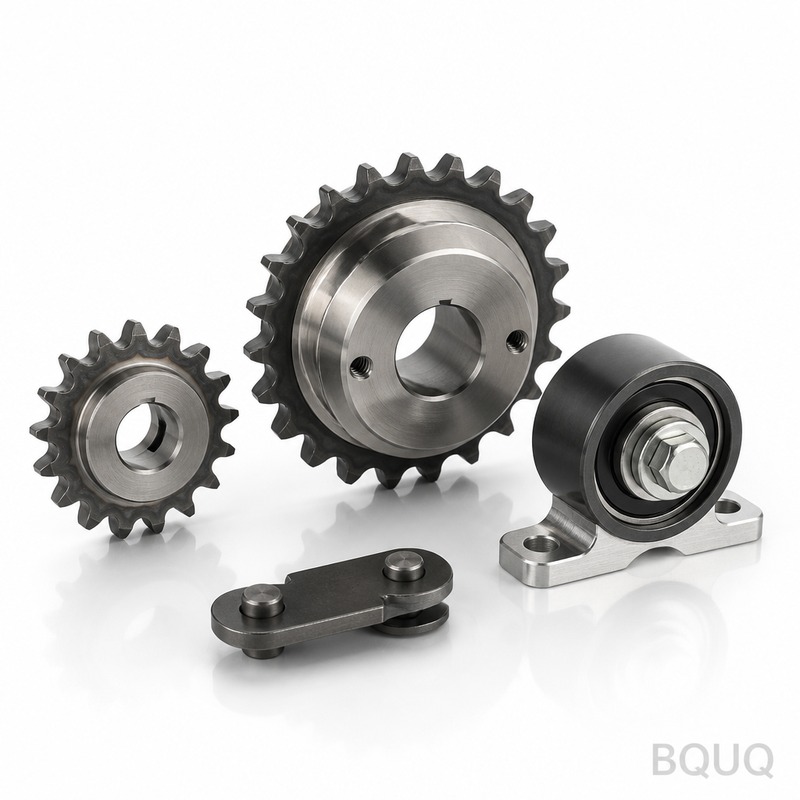
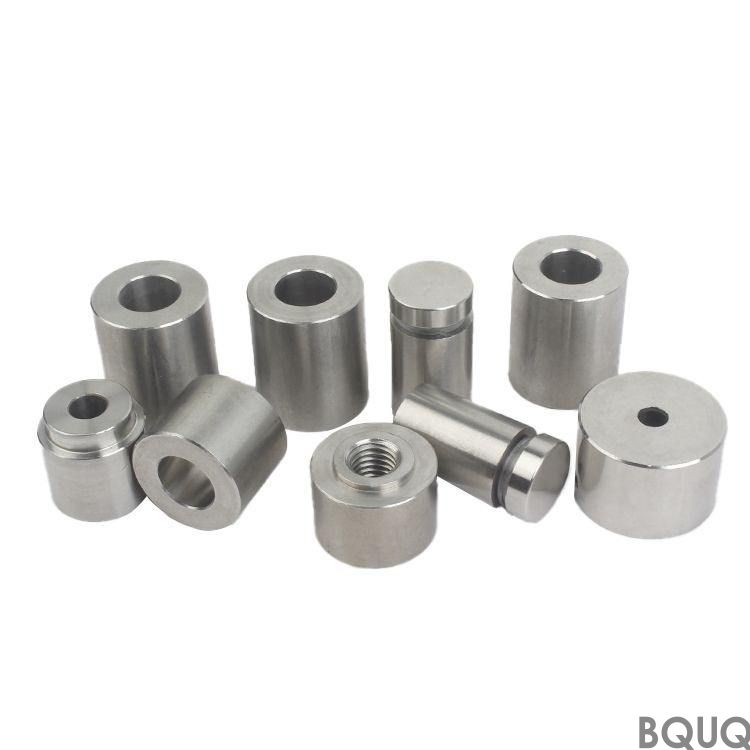
precision machined parts for industrial equipment: Stainless 303 / 304 / 316L, fins at pitch, flatness, thermal resistance. MOQ 10 pcs, ships in 72 hours.
precision machined parts for industrial equipment
precision machined parts for industrial equipment: Stainless 303 / 304 / 316L, fins at pitch, flatness, thermal resistance. MOQ 10 pcs, ships in 72 hours.
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Precision machined parts for industrial equipment in Stainless 303 / 304 / 316L deliver thermal resistance with fins at pitch and a base verified flat before dispatch. Hard chrome plate 0.025 mm is applied after forming, protecting fin roots. Stamped construction holds fin pitch across batches, so hole position carries across the batch for repeatable aerospace volume programs.
Engineered for aerospace, the precision machined parts for industrial equipment in Stainless 303 / 304 / 316L reaches thermal resistance. Fins measure at pitch; the base is verified flat to before dispatch.
Design Approach and Process
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at rather than in the field.
The hard chrome plate 0.025 mm finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
The standard material is Stainless 303 / 304 / 316L, supplied with hard chrome plate 0.025 mm. For applications where aerospace exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to , with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Flatness is checked on a against a limit, and fin pitch is verified optically at . Reports go out with each lot.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with on every first article. Deviations beyond trigger a full-lot sort.
We inspect fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
Final containment is . Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
In aerospace, the rating determines how much airflow the enclosure still needs. At aerospace junction temperatures, fins at pitch keep the delta-T inside the sensor budget.
For aerospace builds, the mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Where a precision machined parts for industrial equipment runs at aerospace volumes, part-to-part consistency decides field returns. on a run keeps the thermal curve inside one band.
In aerospace, the base usually doubles as the mounting interface. with flat gives a stable surface for the aerospace thermal pad.
Specifications
Parameter
Value / Range
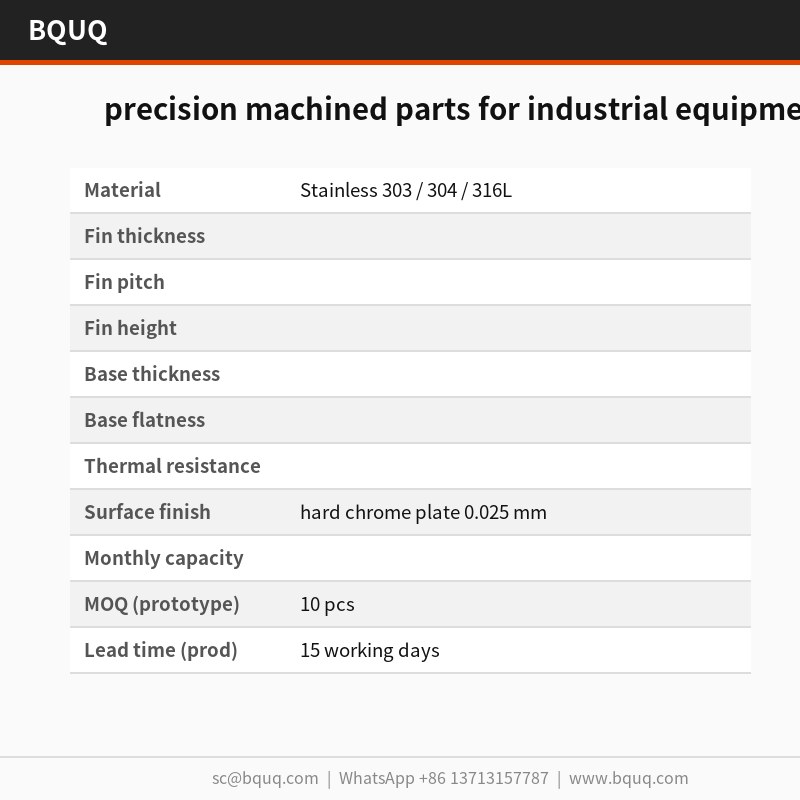
Material
Stainless 303 / 304 / 316L
Surface finish
hard chrome plate 0.025 mm
Size range
Ø2 mm to Ø500 mm
MOQ (prototype)
10 pcs
MOQ (production)
1000 pcs
Lead time (prototype)
72 hours
Lead time (production)
15 working days
FAQ: Your Questions Before Ordering
Which materials do you recommend?
Stainless 303 / 304 / 316L is the standard choice. For aerospace in a corrosive environment we specify 6063-T5 with hard chrome plate 0.025 mm; for the highest conductivity we move to copper C110, which raises cost and weight but drops thermal resistance by roughly half at the same envelope.
Can the precision machined parts for industrial equipment be powder coated or plated?
Yes. Standard is hard chrome plate 0.025 mm. Powder coating to RAL 9005 adds about 0.1 mm to the base; zinc-nickel is better for grounding. Note that any added coating sits between Stainless 303 / 304 / 316L and the airflow, so we do not coat the fin roots.
How long does tooling last before replacement?
On Stainless 303 / 304 / 316L at normal press tonnage, expect a tooling life of roughly . At that is 6 to 12 months. We keep spare die sets on site for aerospace programs, which removes the wait if wear shows up in the flatness record.
Do you make the precision machined parts for industrial equipment in different sizes?
The family covers Ø2 mm to Ø500 mm, with unit weights from . Because the base is pressed, new sizes are a die insert change rather than a new press line, so development is usually 2 weeks rather than 8.
Can you supply the precision machined parts for industrial equipment pre-assembled?
Yes. We can add clips, screws or a fan shroud as a kitted assembly, with the parts bagged and labelled per set. This is common in aerospace programs and adds about 3 working days.
How We Manufacture and Ship
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so flatness is verified before the part is packed.
Fin pitch and base flatness verified; hole position carries across batch
Lead time
Standard for this process: quoted per project, tooling change may affect schedule
MOQ
Standard for this process: batch production, aerospace volume programs
Capacity
Same press family covers multiple fin gauges; every stroke dimensionally identical
Selection / comparison
Option
Best for
Trade-off
Stamped construction
High surface area per cubic millimetre with fins at pitch
Die wear shows as measurable fin pitch shift, caught by inspection
Machined profile
Simple geometries and low volume
Corrosion protection can be cut through at fin roots after plating
Extruded profile
Continuous lengths with uniform cross-section
Tolerates batch variation less than stamping; redesign needs new tooling
Hard chrome plate 0.025 mm
Corrosion protection after forming
Applied post-forming, so fin roots remain protected
Process / inspection
Stage
Control
Record
Forming
Every stroke dimensionally identical; fin pitch monitored
Fin pitch measurement
Plating
Hard chrome plate 0.025 mm applied after forming
Plating thickness record
Base flatness
Verified flat before dispatch
Flatness verification
Hole position
Carries across the batch
Batch dimensional report
Final inspection
Catches die wear shift at inspection rather than in the field
Inspection before every shipment
Frequently Asked Questions
What materials are used for precision machined parts for industrial equipment?
The standard material is Stainless 303 / 304 / 316L, supplied with hard chrome plate 0.025 mm. This combination reaches thermal resistance and protects fin roots after forming. The material choice suits aerospace exposure and industrial equipment duty.
How is fin pitch controlled during production?
Low fin gauge is where stamping wins: fins at pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope. Die wear shows up first as a measurable shift in fin pitch, which inspection catches at inspection rather than in the field.
What tolerance can you hold on base flatness and hole position?
The base is verified flat before dispatch. Every stroke is dimensionally identical, so hole position carries across the batch. Fin pitch is measured as a control. These checks support repeatable aerospace volume programs without field failures.
Is hard chrome plating applied before or after forming?
The hard chrome plate 0.025 mm finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives. This preserves protection at critical fin root geometry.
How does stamping compare with extrusion for finned parts?
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches. One supplier now covers multiple fin gauges from the same press family, so a thermal redesign is a tooling change rather than a new vendor.
What inspection is performed before every shipment?
Inspection before every shipment includes fin pitch measurement, base flatness verification, and hole position checks. The base is verified flat before dispatch. These records confirm every stroke is dimensionally identical and hole position carries across the batch.
Can you support aerospace volume programs with repeatable quality?
Yes. Every stroke is dimensionally identical, so hole position carries across the batch. That is what makes aerospace volume programs repeatable. Stamped construction with hard chrome plate 0.025 mm and inspection before every shipment supports this repeatability.