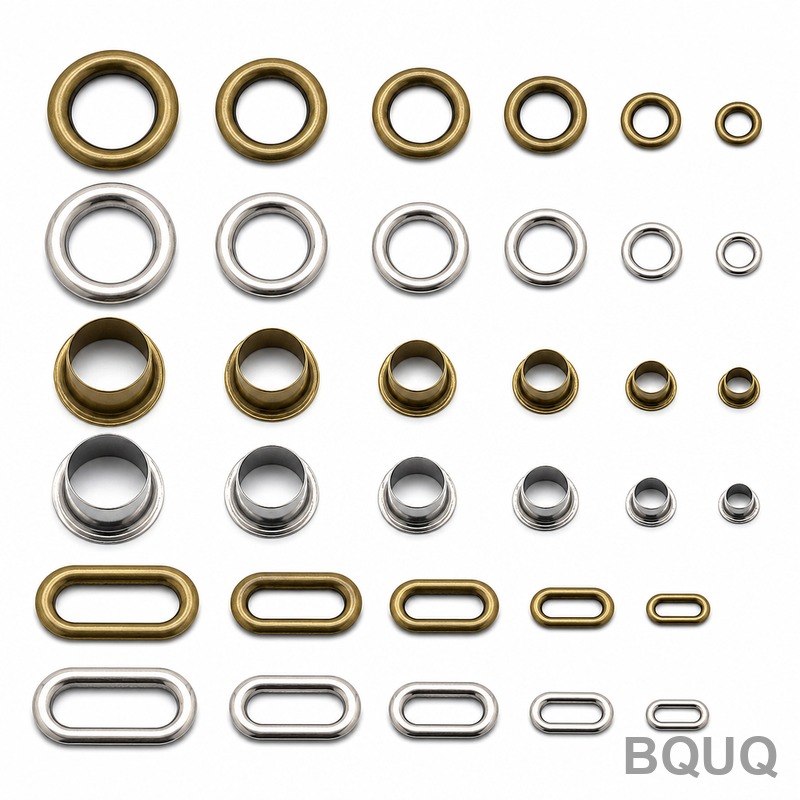
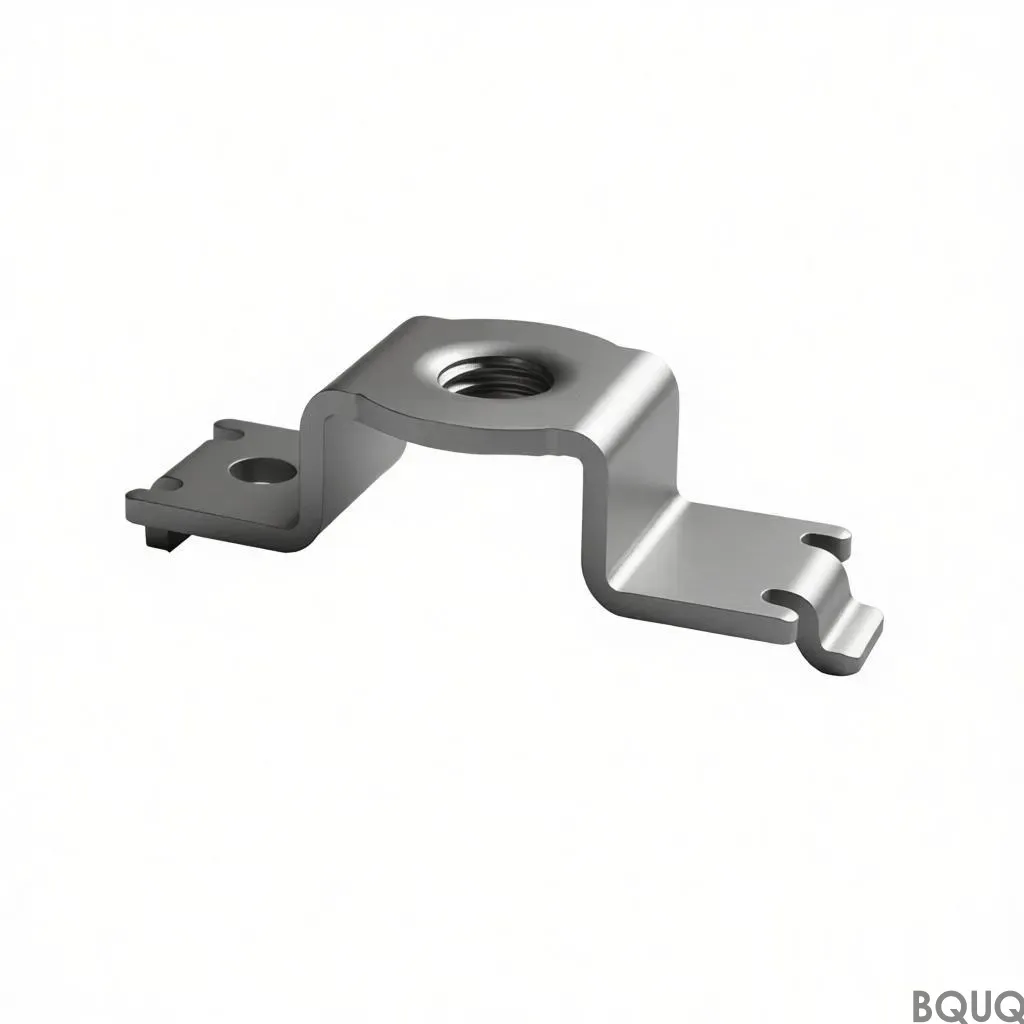
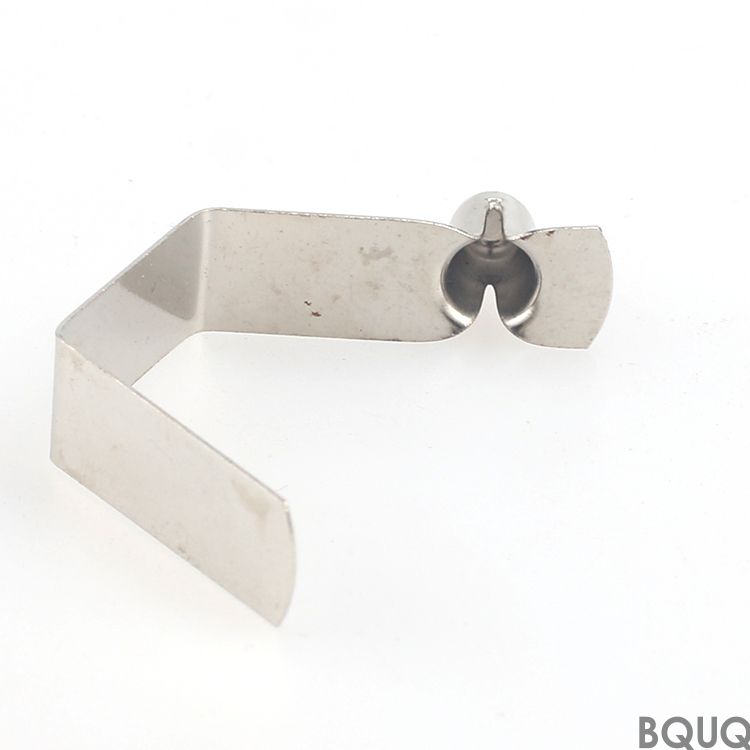
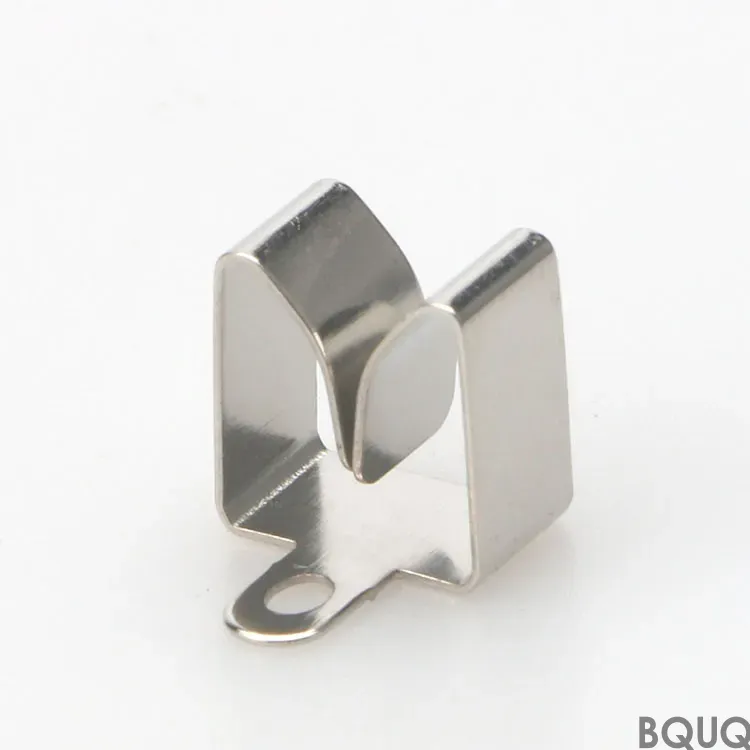
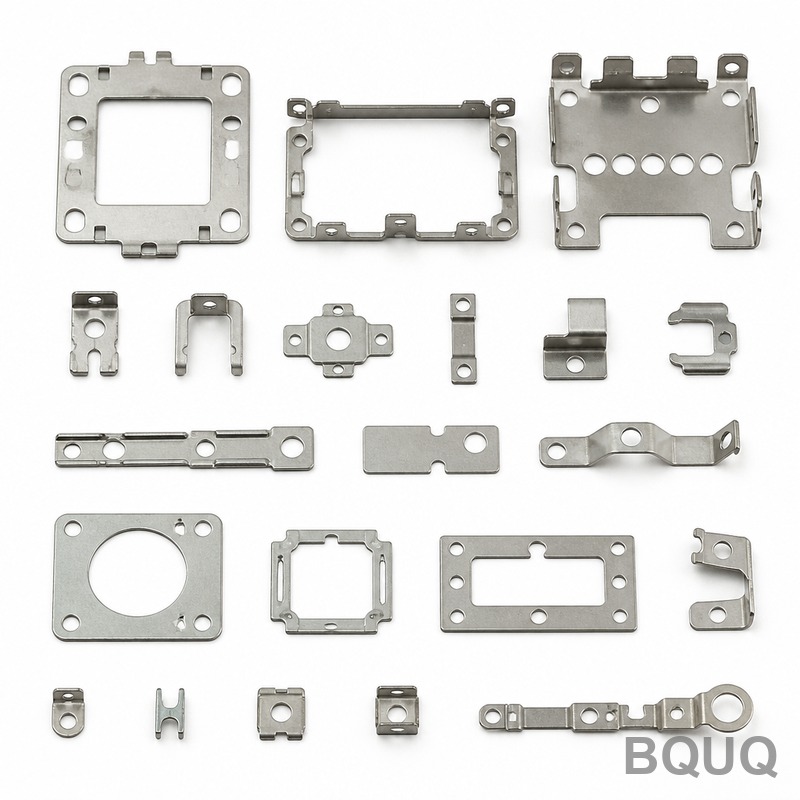
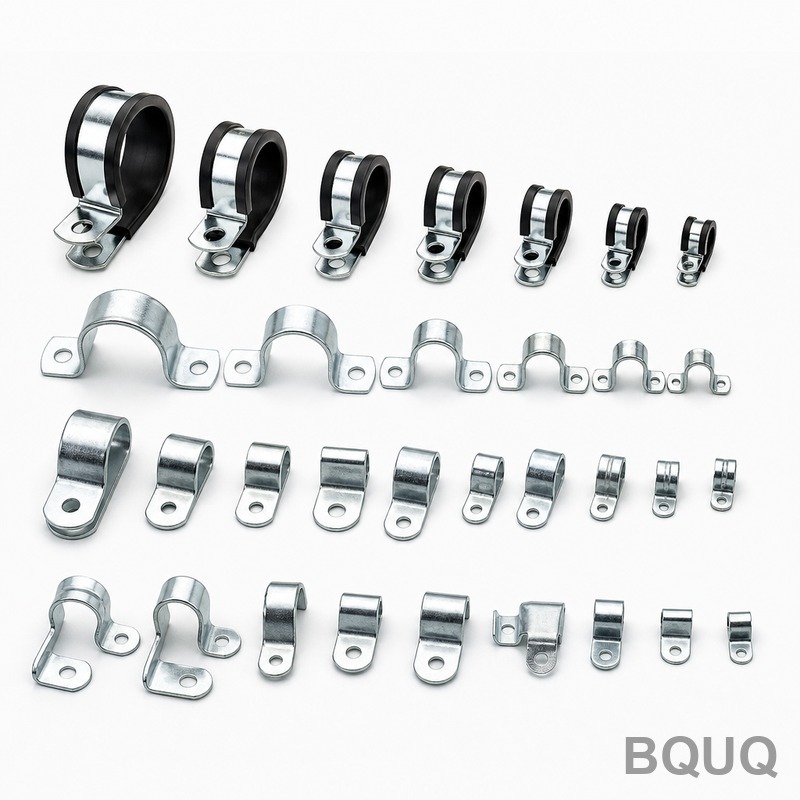
This is BQUQ’s Stamped Metal Grommets Eyelets Ferrules Collection — a family of precision-stamped components for cable pass-throughs, fabric reinforcement, PCB standoffs, and fl
Stamped Metal Grommets Eyelets Ferrules Collection | BQUQ Precision
This is BQUQ’s Stamped Metal Grommets Eyelets Ferrules Collection — a family of precision-stamped components for cable pass-throughs, fabric reinforcement, PCB standoffs, and fluid-sealing ferrules
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is BQUQ’s Stamped Metal Grommets Eyelets Ferrules Collection — a family of precision-stamped components for cable pass-throughs, fabric reinforcement, PCB standoffs, and fluid-sealing ferrules. You get ±0.01 mm dimensional tolerance, 0.02 mm maximum runout on concentric features, and a 7-day lead time for standard sizes. Hardness reaches 45 HRC after optional heat treatment, so these parts survive repeated assembly torque and vibration without cracking.
How We Hold ±0.01 mm Across High-Volume Stamping Runs
Our 20-year-old factory in Dongguan runs 25-ton to 250-ton high-speed presses with servo-driven feed accuracy of ±0.005 mm per stroke. Progressive dies are ground in-house to a 0.002 mm step tolerance, and we use optical comparators on every first article. For grommets with a rolled rim, we control the curl radius within 0.03 mm — that prevents cable insulation from chafing. Eyelets for fabric use get a burr-free backside (max 0.05 mm burr height) because that is where sharp edges cut thread and skin.
Materials and Heat Treatment We Use for Grommets and Ferrules
We stock 12 raw material grades, but three cover 90% of requests. Brass C2680 (half-hard) for electrical conductivity and corrosion resistance. Stainless steel 304 (annealed) for medical and marine environments. Spring steel C75 (hardened to 42–45 HRC) for ferrules that must clamp and hold without loosening. For aluminum grommets, we use 5052-H32 — it bends without micro-cracking at the flange. Heat treatment is done in a vacuum furnace (no oxidation scale), and we can add a matte nickel plating (3–5 µm) for solderability.
Rolled Rims, Flared Tops, and Flanged Bases — What We Can Shape
This collection covers three main geometries. First, rolled-rim grommets for rubber seals or wire harnesses: inner diameter from 2.0 mm to 30.0 mm, wall thickness 0.3–1.5 mm. Second, flared-top eyelets for lacing or ventilation grills: flare angle up to 45°, with a smooth countersink to guide the lace. Third, compression ferrules with a hexagonal or knurled outer surface: knurl pitch 0.8 mm, depth 0.2 mm, for hand-tightened fittings. We also do a hybrid part — a grommet with an integrated spring washer lip, which eliminates a separate assembly step.
Runout and Concentricity — The Numbers That Matter for Rotating Assemblies
If your grommet or ferrule sits on a rotating shaft or aligns a sensor, runout is your enemy. Our stamped parts hold ≤0.02 mm total indicated runout (TIR) between the inner bore and outer diameter. That is achieved by a two-stage forming process: first we blank the disc, then we use a coining die to true the bore before curling the rim. We verify runout on a 3-axis CMM with a 0.5 µm resolution, and we report the actual values on every inspection certificate. For non-rotating parts, we still hold concentricity to 0.05 mm — better than most industry standards for stamped eyelets.
Inspection Before Every Shipment — Not Just a Sampling Check
We do not ship based on AQL 1.0 sampling alone. For this collection, we run a 100% dimensional check on critical features (inner diameter, rim height, and burr height) using a vision system with 0.01 mm resolution. Then we pull 5 pieces per lot for a destructive test: we crush the grommet with a 500 N load and measure how much the inner diameter deforms — it must return within 0.03 mm of its original size. This is especially important for spring steel ferrules. Every shipment includes a lot report with raw material mill certificates and plating thickness measurements.
Surface Finish and Plating Options for Corrosion and Friction
Standard stamped surface finish is Ra 1.6 µm on flat areas and Ra 3.2 µm on curled rims. If you need lower friction for sliding cables, we add a PTFE-impregnated anodize (for aluminum) or a dry-film lubricant (for steel) that cuts friction coefficient from 0.3 to 0.1. For outdoor use, we offer trivalent clear zinc (8–12 µm) with a salt spray resistance of 120 hours. For electronics, we do bright tin plating (5–8 µm) on brass or phosphor bronze — this maintains solderability after 6 months of storage. All plating is RoHS and REACH compliant, verified with a third-party XRF test.
Lead Time, MOQ, and How We Handle Custom Sizes
Standard sizes (2–10 mm inner diameter) ship in 7 days from our stock of 40 pre-made die sets. Custom sizes need a new die — that takes 10–12 days for a simple round grommet, 15 days for a flared or knurled ferrule. MOQ is zero — we accept your first order as a single piece for prototype validation. After you approve, we scale to 10,000 pieces per day. Tooling cost is amortized over the first 20,000 pieces, then we return the tooling drawings to you. For a full breakdown of how we control tolerances during stamping, see our CNC machining tolerances guide. And if you are pairing these parts with a cutting tool, check our CNC cutting tool selection guide to avoid die wear issues.
Specification
Value / Range
Materials
Brass C2680, SS 304, C75 spring steel, Al 5052-H32
Inner Diameter Range
2.0 mm – 30.0 mm
Wall Thickness
0.3 mm – 1.5 mm
Hardness (as stamped)
80–90 HRB (brass), 140–180 HV (SS304)
Hardness (heat-treated)
42–45 HRC (C75 spring steel)
Dimensional Tolerance
±0.01 mm on ID/OD, ±0.03 mm on flange width
Runout (TIR)
≤0.02 mm
Surface Finish (Ra)
1.6 µm flat, 3.2 µm rolled rims
Burr Height (max)
0.05 mm
Lead Time (standard)
7 days
Lead Time (custom die)
10–15 days
MOQ
No minimum (prototype = 1 piece)
What is the MOQ for custom sizes in this collection?
There is no MOQ — we produce a single prototype for your validation, then scale to high volume without extra setup fees.
Can you match a specific material or plating that is not in the table?
Yes, we work with 12 stock grades and 5 plating options; send your spec and we will confirm availability within 24 hours.
How do you guarantee quality on a large production run?
We use 100% vision inspection on critical dimensions, plus a 5-piece destructive crush test per lot, and we ship the full inspection report with your parts.
What is the actual lead time for a custom ferrule with a knurled surface?
Custom knurled ferrules take 15 days from drawing approval to first article, then 7 days for repeat orders with the same die.
Send your drawing for a firm quote within 12 hours — include material, dimensions, and quantity. Email sc@bquq.com or WhatsApp +86 13713157787. We are a precision manufacturing partner based in Dongguan, China, with 20 years of stamping and CNC experience — no MOQ, no minimum order, just exact parts.