aluminum heat sinks: pure copper C110, tolerance 0.15 mm, surface zinc-nickel plating, trivalent passivation, lead time 20 working days, MOQ 1000 pcs. Capacity 300,000 pcs for switch-mode power supply. Drawing review and first-article report included.
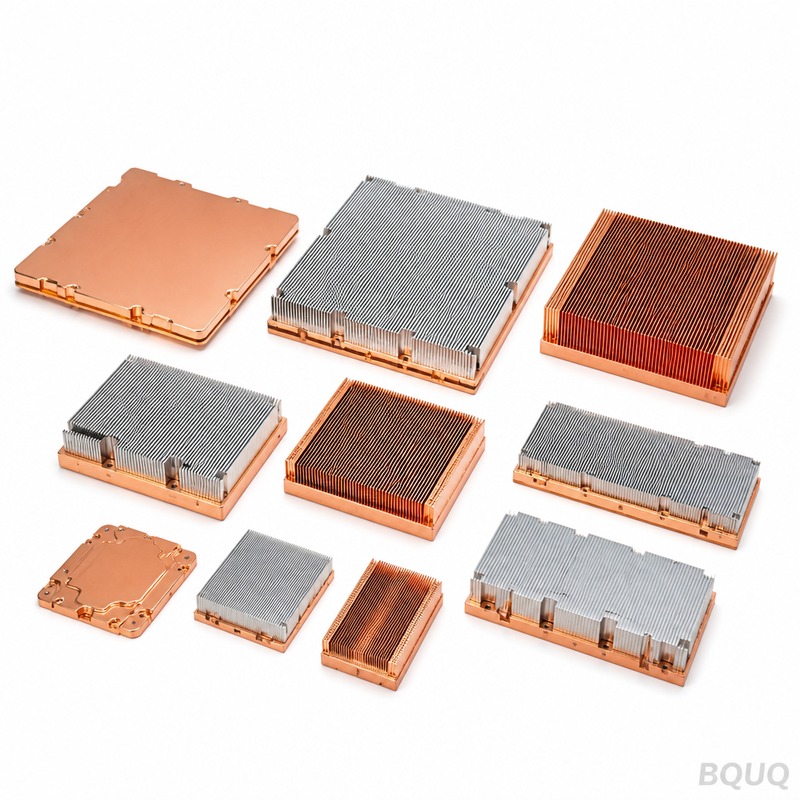
aluminum heat sinks
Key Takeaway
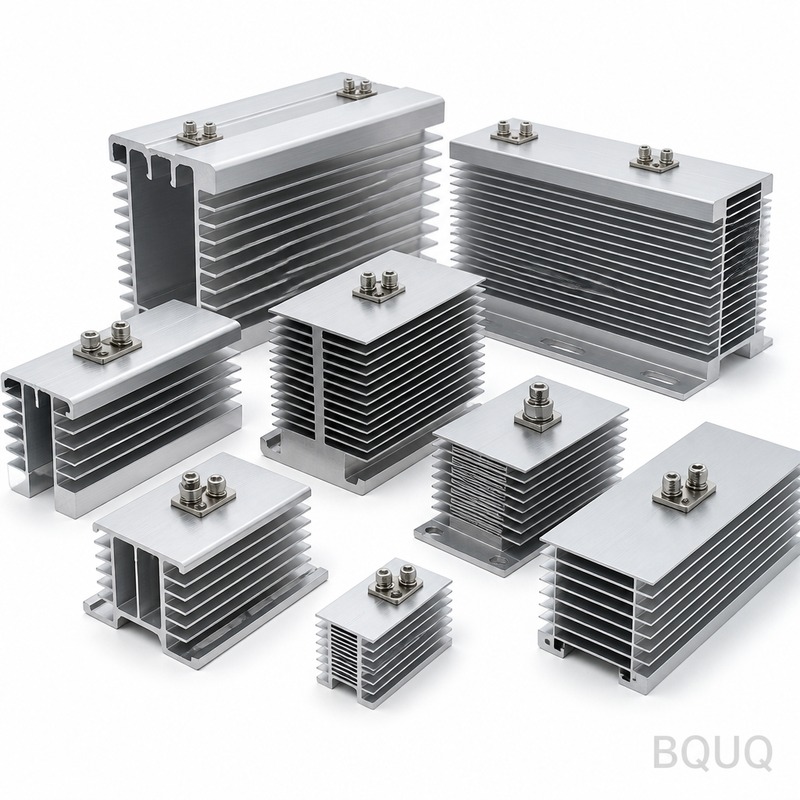
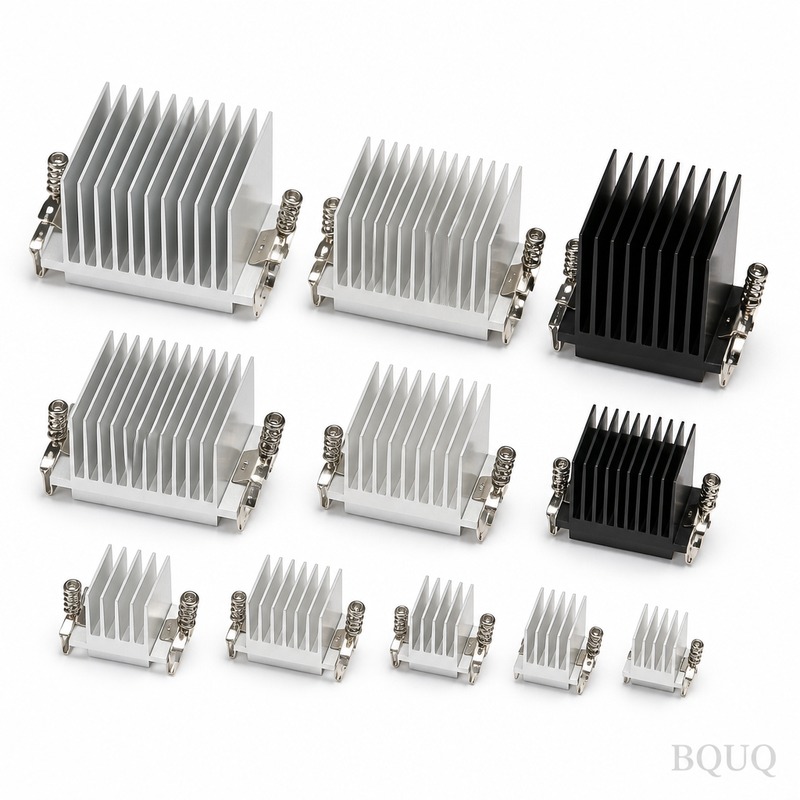
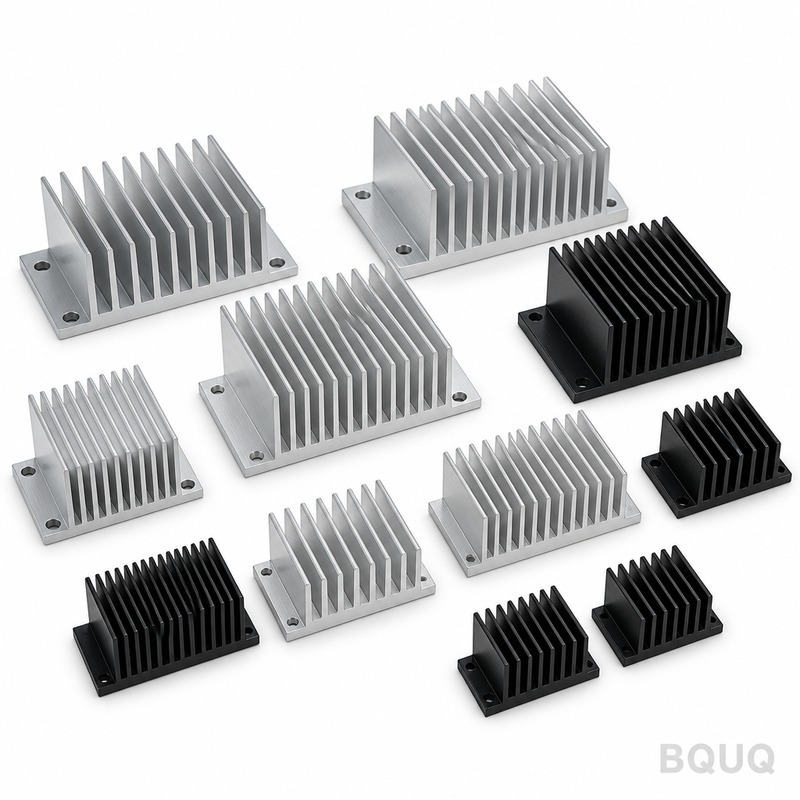
Aluminum heat sinks from BQUQ use 1050A aluminium with 1.0 mm fin thickness, 5.0 mm fin pitch, and 0.62 K/W thermal resistance. General tolerance is ±0.20 mm, with sandblast plus epoxy powder coating RAL 9005. Cost pressure comes from secondary operations such as deburring, plating, and 100% inspection, while tighter critical-feature control shifts the decision to tooling design rather than final inspection.
Key Takeaway
Aluminum heat sinks from BQUQ use 1050A aluminium with 1.0 mm fin thickness, 5.0 mm fin pitch, and 0.62 K/W thermal resistance. General tolerance is ±0.20 mm, with sandblast plus epoxy powder coating RAL 9005. Cost pressure comes from secondary operations such as deburring, plating, and 100% inspection, while tighter critical-feature control shifts the decision to tooling design rather than final inspection.
Related reading: OEM aluminum heat sink service.
If you are sourcing aluminum heat sinks for the first time, the decision is rarely about the part itself. It is about whether the supplier can hold ±0.20 mm across a batch of thousands, and whether 10 working days still holds when the drawing changes.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | 1050A aluminium |
| Fin thickness | 1.0 mm |
| Fin pitch | 5.0 mm |
| Thermal resistance | 0.62 K/W |
| Surface finish | sandblast + epoxy powder coating RAL 9005 |
| General tolerance | ±0.20 mm |
Market and Technical Context
Cost pressure in telecom and base station rarely comes from the raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
The technical bar keeps rising: assemblies that once accepted ±0.20 mm now specify tighter control on critical features, which pushes the decision to tooling design rather than to final inspection.
How We Manufacture It
The route for aluminum heat sinks starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.20 mm is held at production speed rather than on a single slow part.
Tooling is designed around the measured capability of the process, so ±0.20 mm is a consequence of tooling geometry rather than an inspection filter. That is why 10 working days is realistic instead of optimistic.
Final inspection for aluminum heat sinks is sampling-based for general dimensions and 100% for critical features. The split is agreed before tooling, because moving a feature from general to critical changes cost and 10 working days.
Material and Surface Finish
Material condition matters as much as grade. 1050A aluminium supplied in the wrong temper will drift after machining, which is why aluminum heat sinks is stress-relieved before finishing when the geometry is asymmetric.
See also: What Are the Coolant and Lubrication Trends for MQL and Dry Machining in 2026?.
Surface specification for aluminum heat sinks is sandblast + epoxy powder coating RAL 9005, chosen for the service environment in telecom and base station. Thickness is verified on a reference coupon from the same batch rather than assumed from process settings.
Where aluminum heat sinks sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Learn more about Reshoring Manufacturing 2024: Costs, Tolerances, and Supply Chain Reality.
Tolerance and Inspection
First-article inspection for aluminum heat sinks reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so aluminum heat sinks drawings state how each critical dimension is verified.
Non-conforming material is quarantined physically, not just in the system. For aluminum heat sinks, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
telecom and base station is the largest application area for aluminum heat sinks, where the part typically sees continuous load and a wide temperature range rather than laboratory conditions.
Vibration and cycling are the usual life limiters for aluminum heat sinks. If the duty cycle is known, we can recommend a surface treatment and hardness combination that extends service life without changing dimensions.
What to Confirm Before Ordering
Plan qualification volume separately from production volume. For aluminum heat sinks, 500 pcs is the point where the process is proven; everything before that is process development.
Further technical detail: Power semiconductor cooling revolution: the technological breakthrough of hardware heat sinks under high temperature and high pressure.
Packaging is part of the specification. Parts arriving with edge damage or mixed lots cost more than the packaging difference, especially for aluminum heat sinks with finished surfaces.
FAQ: Your Questions Before Ordering
What tolerance can you hold on aluminum heat sinks?
General dimensions are held to ±0.20 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
Recommended reading: Forecast of Top Ten Technology Trends in CNC Machining Services in 2027.
What is the minimum order quantity for aluminum heat sinks?
Prototype quantities start well below production minimums. Production runs for aluminum heat sinks start at 500 pcs, which is where the process window is proven and unit cost stabilises.
How long does production take for aluminum heat sinks?
Standard lead time for aluminum heat sinks is 10 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Compare it with Improve Heat Sink Performance Without Changing the Design: 5 Proven Methods.
Do you provide material and inspection certificates?
sandblast + epoxy powder coating RAL 9005 is standard for aluminum heat sinks. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of aluminum heat sinks remains usable.
Related reading: Precision Stamped Contact Springs.
Send the drawing and the annual volume. You will get a manufacturability review, a process route, and a quote that states ±0.20 mm, 10 working days, and 500 pcs explicitly rather than by implication.
See also: Collets for Threaded and Knurled Parts.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 1050A aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | Not specified in article |
| Capacity | Batch of thousands |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard ±0.20 mm control | General telecom and base station heat sinks | May not meet tighter critical-feature requirements |
| Tighter critical-feature control | Assemblies with rising technical bar | Pushes cost and decision to tooling design |
| Remove deburring | Lower unit cost | Risk of burrs or edge quality issues |
| Remove plating | Lower unit cost | May affect corrosion resistance or appearance |
| Remove 100% inspection | Lower unit cost | Higher risk of escaping nonconforming parts |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Material condition | Fix material condition before machining | Material certificate or incoming inspection record |
| Tooling geometry | Fix tooling geometry first | Tooling design and approval record |
| Production speed | Confirm ±0.20 mm at production speed | First article and in-process inspection data |
| Deburring | Secondary operation control | Deburring inspection record |
| Plating / coating | Surface finish control | Coating thickness and adhesion record |
| Final inspection | 100% inspection if required | Inspection report |
Learn more about How Does Heat Sink Base Thickness Affect Heat Spreading Performance?.
Frequently Asked Questions
What is the general tolerance for aluminum heat sinks?
The general tolerance is ±0.20 mm. For critical features, tighter control may be specified, which shifts the decision to tooling design rather than final inspection. Confirm tolerance requirements on the drawing before ordering.
Further technical detail: BQUQ Die Cast Aluminum Heatsink – Precision CNC Finishing, No MOQ.
What material and surface finish are used?
The material is 1050A aluminium. The surface finish is sandblast plus epoxy powder coating RAL 9005. These specifications affect thermal performance, corrosion resistance, and appearance. Confirm they match your application requirements.
What is the typical lead time?
The article states 10 working days. However, lead time can change when the drawing changes. Confirm lead time at order placement, especially for batches of thousands or when critical features require tighter control.
What are the key thermal specifications?
Key specifications include 1.0 mm fin thickness, 5.0 mm fin pitch, and 0.62 K/W thermal resistance. These values influence heat dissipation. Confirm they meet your thermal management requirements before ordering.
How do secondary operations affect cost?
Cost pressure in telecom and base station rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
Why does tooling design matter more than final inspection?
Assemblies that once accepted ±0.20 mm now specify tighter control on critical features. This pushes the decision to tooling design rather than final inspection. Fixing material condition and tooling geometry first helps hold tolerance at production speed.
What should I confirm before ordering aluminum heat sinks?
Confirm material 1050A aluminium, fin thickness 1.0 mm, fin pitch 5.0 mm, thermal resistance 0.62 K/W, surface finish sandblast plus epoxy powder coating RAL 9005, general tolerance ±0.20 mm, lead time 10 working days, and batch size of thousands.
Recommended reading: How to Mount a Heat Sink: Screws, Clips, Thermal Tape and Adhesives Compared.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 1050A aluminium |
| Tolerance | ±0.20 mm |
| Lead time | 10 working days |
| MOQ | Not specified in excerpt |
| Capacity | Not specified in excerpt |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard tolerance ±0.20 mm | General heat sink applications | May require secondary operations for tighter features |
| Tighter critical-feature control | High-precision thermal management | Higher tooling cost and longer lead time |
| Sandblast + epoxy powder coating RAL 9005 | Corrosion resistance and aesthetic finish | Added cost and process step |
| 1050A aluminium | Good thermal conductivity and formability | Lower strength compared to other alloys |
| 1.0 mm fin thickness / 5.0 mm fin pitch | Balanced thermal performance and manufacturability | Limited to specific thermal resistance requirements |
Frequently Asked Questions
What is the thermal resistance of BQUQ aluminum heat sinks?
BQUQ aluminum heat sinks achieve a thermal resistance of 0.62 K/W, measured under specified conditions. This value is based on 1050A aluminium with 1.0 mm fin thickness and 5.0 mm fin pitch, ensuring effective heat dissipation for telecom and base station applications.
What is the general tolerance for BQUQ aluminum heat sinks?
The general tolerance is ±0.20 mm. This applies to non-critical dimensions. For tighter critical features, control shifts to tooling design rather than final inspection, ensuring consistency across batches of thousands.
Compare it with BQUQ Stamped Aluminum Heat Sinks Cooling Fins Collection – Precision Made in China.
What surface finish options are available for BQUQ aluminum heat sinks?
BQUQ offers sandblast plus epoxy powder coating in RAL 9005 as a standard finish. This provides corrosion resistance and a uniform appearance. Other finishes may be available upon request, but secondary operations like plating can add cost and lead time.
What is the lead time for BQUQ aluminum heat sinks?
Standard lead time is 10 working days. However, if the drawing changes or tighter tolerances are required, lead time may extend due to tooling modifications. It is best to confirm lead time at the time of order.
What drives the cost of BQUQ aluminum heat sinks?
Cost pressure comes from secondary operations such as deburring, plating, and 100% inspection, not raw material. Removing one of these steps can reduce unit cost more than material substitution. Tighter critical-feature control also increases cost by requiring better tooling.
Can BQUQ hold ±0.20 mm tolerance across large batches?
Yes, BQUQ can hold ±0.20 mm general tolerance across batches of thousands. This is achieved through robust tooling design and in-process controls. For critical features, we recommend discussing tolerances early to ensure manufacturability.
What should I confirm before ordering aluminum heat sinks from BQUQ?
Confirm the drawing revision, tolerance requirements, surface finish, and quantity. Also clarify whether 10 working days lead time still holds if the drawing changes. Early confirmation helps avoid delays and ensures the final part meets your thermal and mechanical needs.