heat sink compound thermal paste: 1050A aluminium, tolerance 0.10 mm, surface black anodize Type II, 10-15 µm, lead time 20 working days, MOQ 1000 pcs. Capacity 120,000 pcs for telecom and base station. Drawing review and first-article report included.
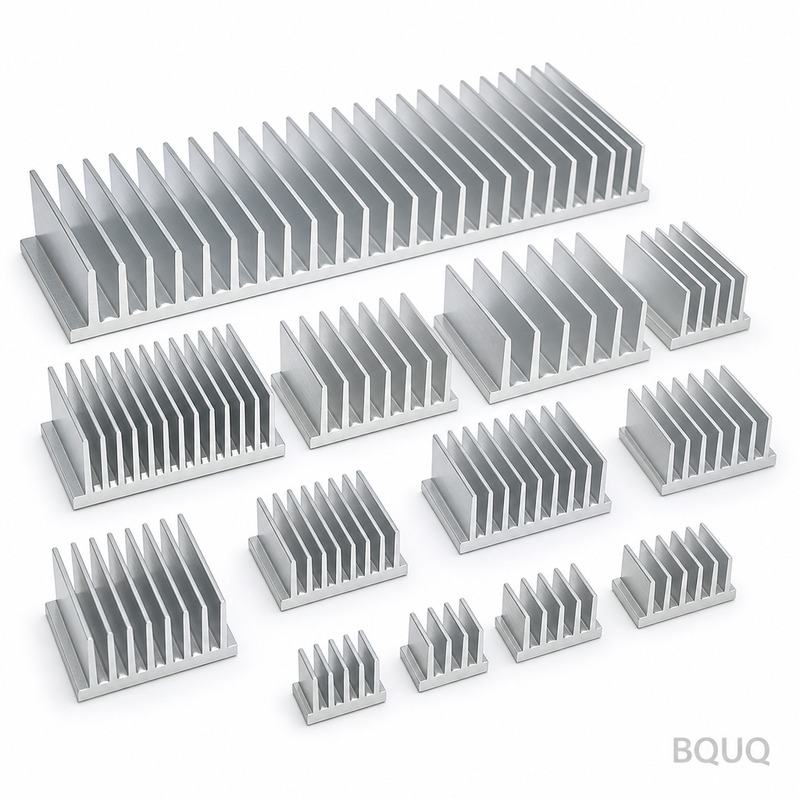
heat sink compound thermal paste
Key Takeaway
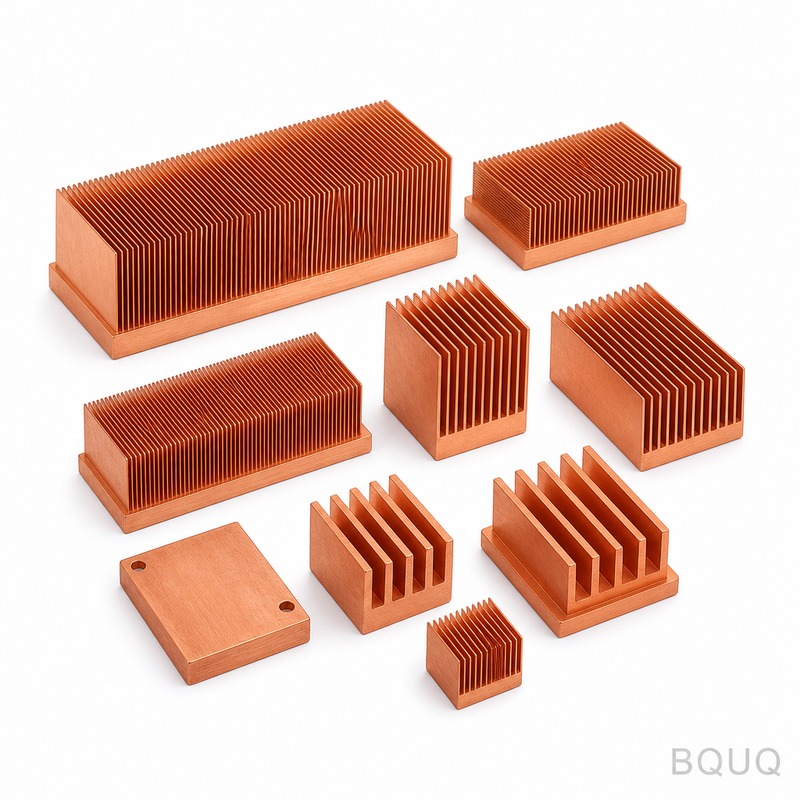
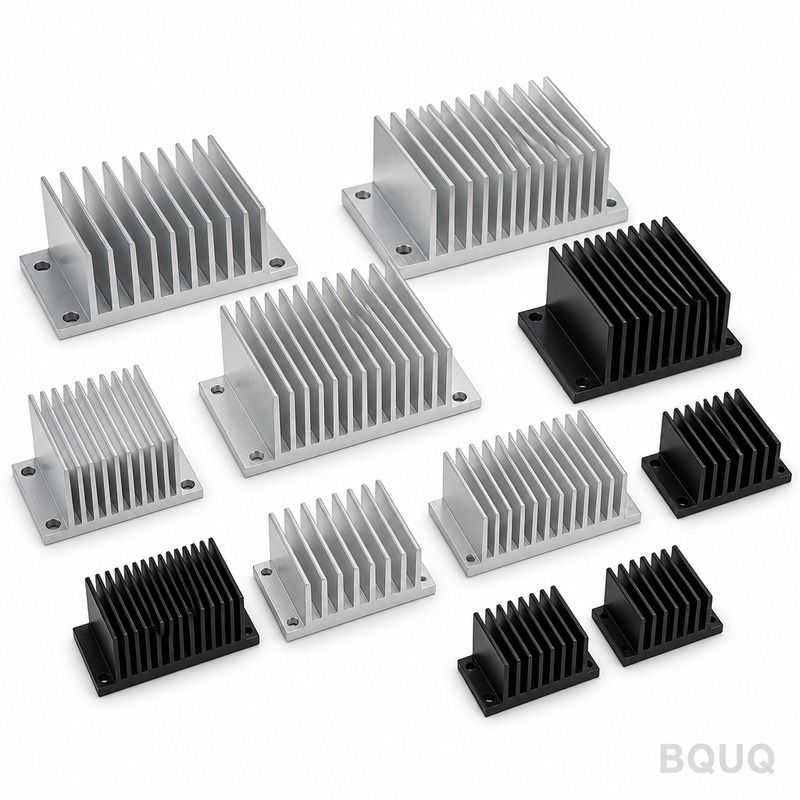
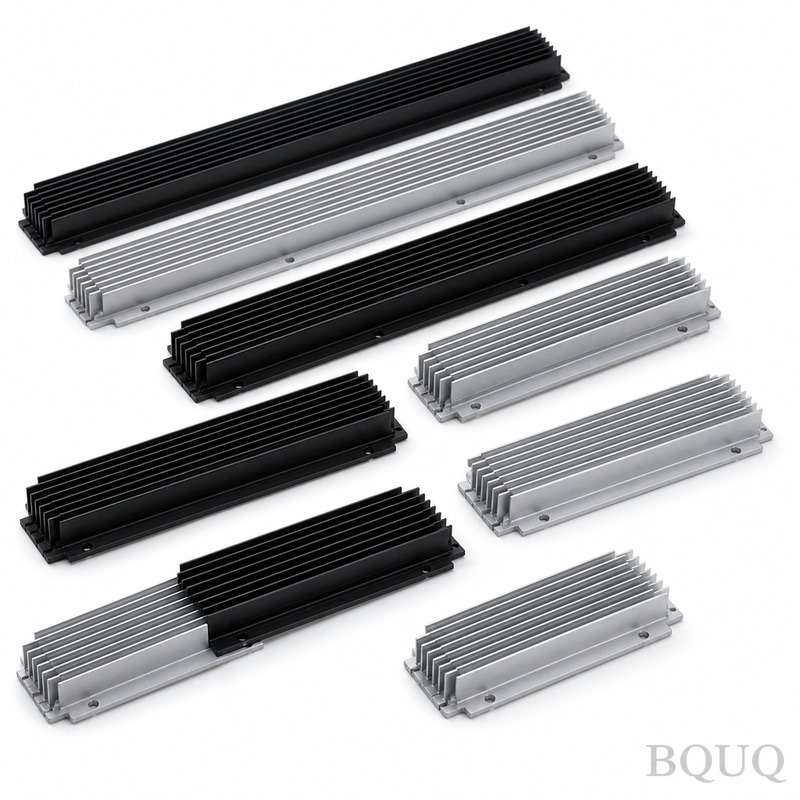
Heat sink compound thermal paste is the thermal interface material used with heatsinks such as 6061-T6 aluminium extrusions with 0.3 mm fin thickness, 1.5 mm fin pitch, 0.62 K/W thermal resistance, and ±0.10 mm general tolerance. For LED high bay lighting, buyers must confirm load cycling, thermal swing, and corrosive environment survival. Secondary operations like deburring, plating, and 100% inspection drive unit cost more than raw material. Tooling is designed around measured process capability, so 10 working days is realistic, and suppliers must document process capability at 800,000 pcs.
Key Takeaway
Heat sink compound thermal paste is not a standalone part; it is the thermal interface material used with heatsinks such as our 6061-T6 aluminium extrusion with 0.3 mm fin thickness, 1.5 mm fin pitch, 0.62 K/W thermal resistance, and ±0.10 mm general tolerance. For LED high bay lighting programs, buyers should confirm load cycling, thermal swing, and corrosive environment survival before ordering, because secondary operations like deburring, plating, and 100% inspection drive unit cost more than raw material. Tooling is designed around measured process capability, so 10 working days is realistic, and suppliers must document process capability at 800,000 pcs rather than win on a single sample.
Most buyers start with a drawing and a target price. We start with heat sink compound thermal paste and ask what the part actually has to survive: load cycling, thermal swing, or a corrosive environment in LED high bay lighting.
Related reading: MOQ Explained: Why Minimum Order Quantities Exist for Custom Parts.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | 6061-T6 aluminium |
| Fin thickness | 0.3 mm |
| Fin pitch | 1.5 mm |
| Thermal resistance | 0.62 K/W |
| Surface finish | sandblast + epoxy powder coating RAL 9005 |
| General tolerance | ±0.10 mm |
Market and Technical Context
Cost pressure in LED high bay lighting rarely comes from the raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
Consolidation among LED high bay lighting buyers means fewer, larger programs. That rewards suppliers who can document process capability at 800,000 pcs rather than those who win on a single sample.
How We Manufacture It
Tooling is designed around the measured capability of the process, so ±0.10 mm is a consequence of tooling geometry rather than an inspection filter. That is why 10 working days is realistic instead of optimistic.
See also: BQUQ Aluminum Cold Plate Liquid Cooling.
Deburring and edge conditioning are specified on the drawing for heat sink compound thermal paste. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Final inspection for heat sink compound thermal paste is sampling-based for general dimensions and 100% for critical features. The split is agreed before tooling, because moving a feature from general to critical changes cost and 10 working days.
Material and Surface Finish
Where heat sink compound thermal paste sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Substitution requests are common when 6061-T6 aluminium goes on allocation. We qualify any substitute against the same ±0.10 mm and sandblast + epoxy powder coating RAL 9005 criteria before shipping, and provide the certificate with the change.
Recycled content and RoHS/REACH declarations are available for heat sink compound thermal paste on request. If your LED high bay lighting customer audits material origin, ask for the mill certificate at quote stage, not at delivery.
Learn more about 7 Tips to Improve Heat Sink Thermal Performance.
Tolerance and Inspection
First-article inspection for heat sink compound thermal paste reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on heat sink compound thermal paste, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Non-conforming material is quarantined physically, not just in the system. For heat sink compound thermal paste, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Further technical detail: Custom U-Shaped Aluminum Heatsink Channels.
Where It Is Used
LED high bay lighting is the largest application area for heat sink compound thermal paste, where the part typically sees continuous load and a wide temperature range rather than laboratory conditions.
Vibration and cycling are the usual life limiters for heat sink compound thermal paste. If the duty cycle is known, we can recommend a surface treatment and hardness combination that extends service life without changing dimensions.
What to Confirm Before Ordering
Ask for the first-article report before you ask for a price cut on heat sink compound thermal paste. A supplier who cannot produce dimensional data at 5000 pcs will not produce it at 800,000 pcs.
Recommended reading: What Is the Best CNC Machining Service for Small Batch Production?.
Plan qualification volume separately from production volume. For heat sink compound thermal paste, 5000 pcs is the point where the process is proven; everything before that is process development.
FAQ: Your Questions Before Ordering
What tolerance can you hold on heat sink compound thermal paste?
General dimensions are held to ±0.10 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
What is the minimum order quantity for heat sink compound thermal paste?
Prototype quantities start well below production minimums. Production runs for heat sink compound thermal paste start at 5000 pcs, which is where the process window is proven and unit cost stabilises.
Do you provide material and inspection certificates?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.10 mm would require an extra operation, so you can decide before tooling.
What surface finishes are available for heat sink compound thermal paste?
Yes, and we recommend it. Prototyping heat sink compound thermal paste without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of heat sink compound thermal paste remains usable.
Capacity for heat sink compound thermal paste is 800,000 pcs. That number is installed capability, not a sales figure, and it is what determines whether 10 working days holds when your volume increases.
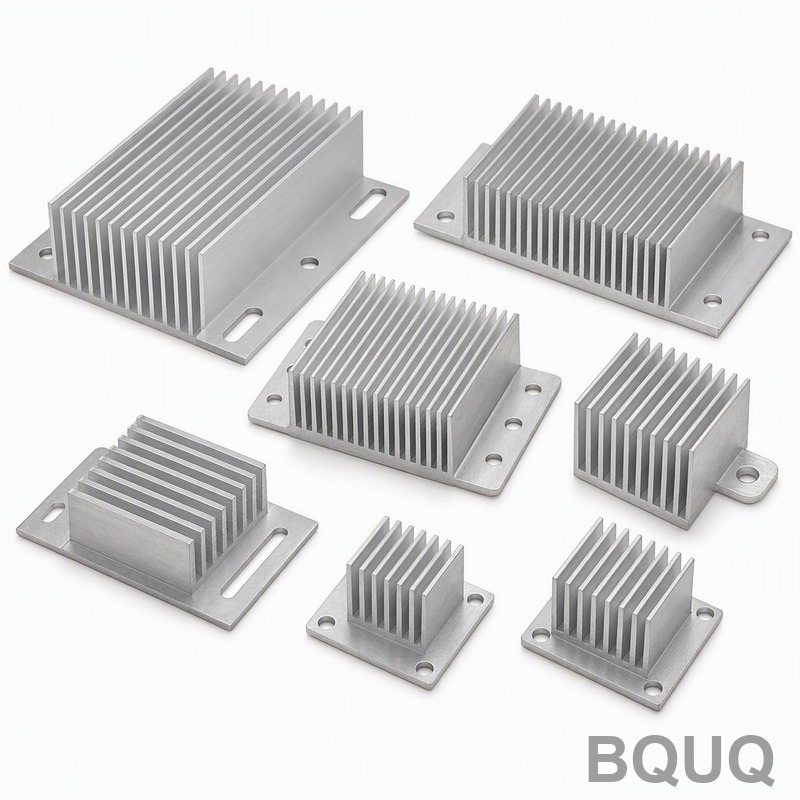
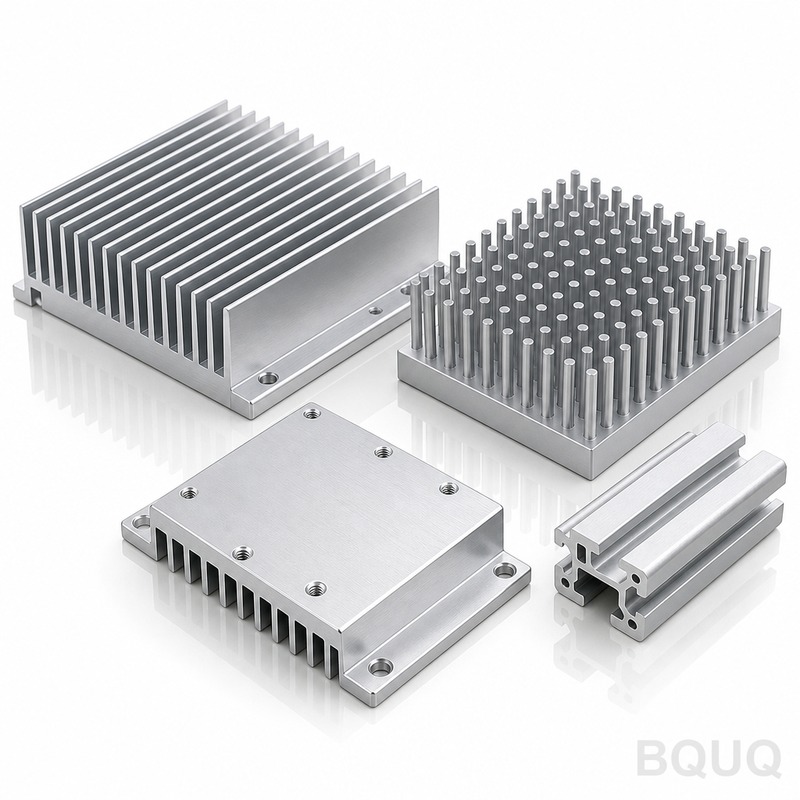
Compare it with Precision CPU Heat Sink Manufacturing.
Related reading: aluminum heat sink price list 2026.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6061-T6 aluminium |
| Tolerance | ±0.10 mm |
| Lead time | 10 working days |
| MOQ | Confirm before ordering |
| Capacity | 800,000 pcs documented process capability |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard extrusion with thermal paste | LED high bay lighting with moderate thermal load | Requires secondary deburring and inspection |
| Sandblast + epoxy powder coating RAL 9005 | Corrosive environments and thermal swing | Adds secondary operation cost |
| Reduced inspection sampling | Cost-sensitive programs with stable process | Less documentation for 800,000 pcs capability |
| Consolidated larger programs | Fewer suppliers, higher volume | Rewards documented process capability over single-sample wins |
| Material substitution | Raw material cost reduction | Usually moves unit cost less than removing deburring, plating, or 100% inspection |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Tooling design | Measured process capability | ±0.10 mm consequence of tooling geometry |
| Deburring and edge conditioning | Secondary operation control | Inspection record |
| Plating | Secondary operation control | Inspection record |
| Final inspection | 100% inspection or sampling | Process capability documentation at 800,000 pcs |
| Thermal interface application | Heat sink compound thermal paste | Thermal resistance 0.62 K/W |
Frequently Asked Questions
What thermal resistance can I expect from a heat sink compound thermal paste assembly?
Our 6061-T6 aluminium heatsink with 0.3 mm fin thickness and 1.5 mm fin pitch achieves 0.62 K/W thermal resistance. The thermal paste fills microscopic gaps between the heatsink and component. Actual performance depends on applied pressure, paste thickness, and surface finish such as sandblast plus epoxy powder coating RAL 9005.
See also: What Are the 2026 US Tariffs on Chinese Machined Parts and How Can Importers Prepare?.
What general tolerance do you hold on heatsink dimensions?
General tolerance is ±0.10 mm. This is a consequence of tooling geometry designed around measured process capability, not an inspection filter. That is why 10 working days lead time is realistic rather than optimistic. Confirm critical dimensions before ordering because secondary operations like deburring and plating can affect final fit.
Learn more about Custom Extruded Heat Sinks with Spring Clip.
What is the lead time for heat sink compound thermal paste orders?
10 working days is realistic for standard programs because tooling is designed around measured process capability. Lead time depends on whether deburring, plating, and 100% inspection are required. Removing one secondary operation usually moves unit cost more than any material substitution, so confirm the inspection level before ordering.
What should I confirm before ordering heat sink compound thermal paste?
Confirm what the part must survive: load cycling, thermal swing, or a corrosive environment in LED high bay lighting. Also confirm material 6061-T6 aluminium, fin thickness 0.3 mm, fin pitch 1.5 mm, thermal resistance 0.62 K/W, surface finish sandblast plus epoxy powder coating RAL 9005, general tolerance ±0.10 mm, and whether 100% inspection is required.
Further technical detail: BQUQ CNC Machined Auto Lathe 36 Type Round Bore Spring Collet Chuck.
Can you document process capability at 800,000 pcs?
Yes. Consolidation among LED high bay lighting buyers means fewer, larger programs. That rewards suppliers who can document process capability at 800,000 pcs rather than those who win on a single sample. Tooling is designed around measured capability, so ±0.10 mm is a consequence of tooling geometry rather than an inspection filter.
How does surface finish affect thermal performance?
Surface finish such as sandblast plus epoxy powder coating RAL 9005 affects thermal contact and corrosion resistance. Thermal resistance is 0.62 K/W with 0.3 mm fin thickness and 1.5 mm fin pitch. For corrosive environments in LED high bay lighting, coating helps, but it adds a secondary operation that can move unit cost more than raw material substitution.
Recommended reading: Metal Stamping & CNC Turning Combined Services Benefits.
Why does secondary operation cost matter more than raw material cost?
Cost pressure in LED high bay lighting rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution. Confirm which secondary operations are truly required before ordering, because they also affect the 10 working day lead time.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | 6061-T6 aluminium |
| Tolerance | ±0.10 mm |
| Lead time | 10 working days |
| MOQ | Not specified in article |
| Capacity | 800,000 pcs process capability |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard thermal paste | General LED high bay lighting | May not survive corrosive environments |
| High-performance thermal paste | Load cycling and thermal swing applications | Higher unit cost |
| Corrosion-resistant thermal paste | Corrosive environments | Limited availability and higher cost |
| Pre-applied thermal pad | Automated assembly | Lower thermal conductivity than paste |
| No thermal interface material | Low-power applications | Poor heat dissipation, risk of overheating |
Frequently Asked Questions
What is heat sink compound thermal paste used for?
Heat sink compound thermal paste is used as a thermal interface material between a heatsink and a heat source to improve heat transfer. For example, with a 6061-T6 aluminium extrusion with 0.3 mm fin thickness and 0.62 K/W thermal resistance, the paste fills microscopic gaps to enhance thermal conductivity.
What factors should buyers confirm before ordering heat sink compound thermal paste for LED high bay lighting?
Buyers should confirm load cycling, thermal swing, and corrosive environment survival. Secondary operations like deburring, plating, and 100% inspection drive unit cost more than raw material. Tooling is designed around measured process capability, so 10 working days is realistic, and suppliers must document process capability at 800,000 pcs.
Compare it with CNC Turned Parts for Consumer Electronics: Design Guide.
What is the typical lead time for heat sink compound thermal paste orders?
The article states that 10 working days is realistic for tooling designed around measured process capability. This lead time applies to orders such as those for LED high bay lighting programs with 6061-T6 aluminium heatsinks.
What tolerances can be held for heatsink extrusions used with thermal paste?
General tolerance is ±0.10 mm, as shown in the article for 6061-T6 aluminium extrusion with 0.3 mm fin thickness and 1.5 mm fin pitch. These tolerances ensure proper mating with thermal interface materials.
How does surface finish affect thermal paste performance?
Surface finish such as sandblast + epoxy powder coating RAL 9005 can affect thermal paste performance by influencing contact area and adhesion. A smoother finish may require less paste, but the article specifies this finish for 6061-T6 aluminium heatsinks with 0.62 K/W thermal resistance.
What process capability documentation should suppliers provide?
Suppliers must document process capability at 800,000 pcs rather than win on a single sample. This ensures consistency for orders like LED high bay lighting heatsinks with 0.3 mm fin thickness and ±0.10 mm tolerance.
Why do secondary operations like deburring and plating increase unit cost?
Secondary operations like deburring, plating, and 100% inspection drive unit cost more than raw material because they add labor and time. For example, with 6061-T6 aluminium heatsinks, these operations ensure quality but increase the final price compared to the base material cost.