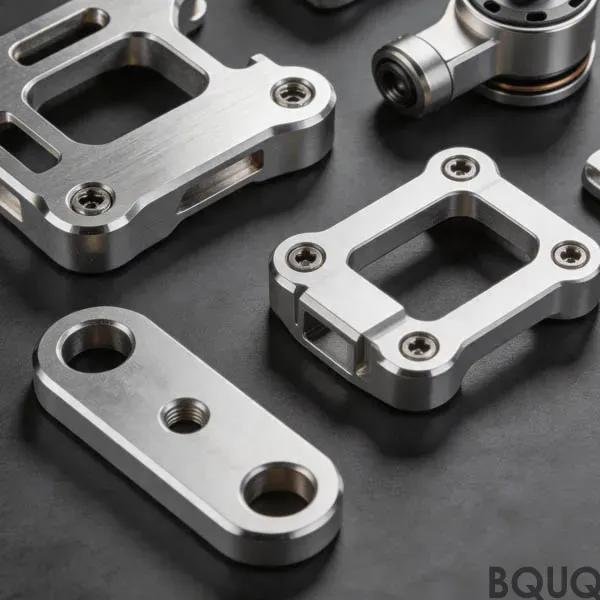
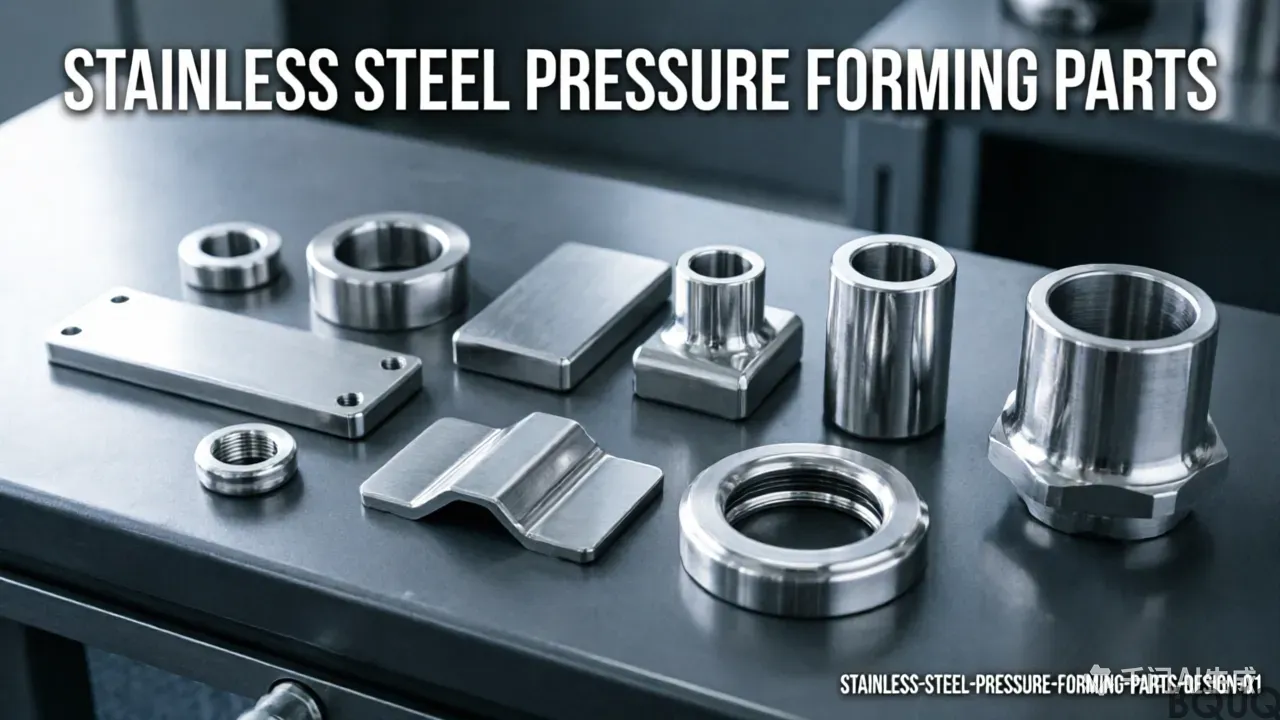
sheet metal parts hs code: Copper C110, tolerance 0.01 mm, surface hard chrome plate 0.025 mm, lead time 10 working days, MOQ 200 pcs. Capacity for semiconductor equipment. Drawing review and first-article report included.
sheet metal parts hs code
Key Takeaway
Sheet metal parts HS code classification depends on material and function, not the machining route. For aluminium 7075-T6 parts with electropolish Ra 0.2, production runs at 1000 pcs MOQ and 20 working days lead time, with ±0.005 mm tolerance held across batches. Buyers should confirm material certificates, first-article reports, and PPAP-style records at 1000 pcs, since robotics programs now require documented process capability rather than single-sample results.
Key Takeaway
Sheet metal parts HS code classification depends on material and function, not on the machining route. For aluminium 7075-T6 parts with electropolish Ra 0.2, production runs at 1000 pcs MOQ and 20 working days lead time, with ±0.005 mm tolerance held across batches. Buyers should confirm material certificates, first-article reports, and PPAP-style records at 1000 pcs, since robotics programs now require documented process capability rather than single-sample results.
Related reading: Custom Round LED Bulb Heatsink.
If you are sourcing sheet metal parts hs code for the first time, the decision is rarely about the part itself. It is about whether the supplier can hold ±0.005 mm across a batch of thousands, and whether 20 working days still holds when the drawing changes.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | Aluminium 7075-T6 |
| Surface finish | electropolish Ra 0.2 |
| Lead time (production) | 20 working days |
| MOQ (production) | 1000 pcs |
Market and Technical Context
Demand in robotics has shifted from single-source standard parts toward qualified custom parts, which pushes documentation requirements upstream. Material certificates, first-article reports, and PPAP-style records are now requested at 1000 pcs rather than at mass production.
Consolidation among robotics buyers means fewer, larger programs. That rewards suppliers who can document process capability at rather than those who win on a single sample.
Learn more about Progressive vs Transfer Stamping: Key Differences Explained.
How We Manufacture It
The route for sheet metal parts hs code starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.005 mm is held at production speed rather than on a single slow part.
Tooling is designed around the measured capability of the process, so ±0.005 mm is a consequence of tooling geometry rather than an inspection filter. That is why 20 working days is realistic instead of optimistic.
Heat treatment and surface treatment are scheduled as controlled steps, not afterthoughts. electropolish Ra 0.2 is applied to a defined thickness range and verified, because variation here causes more field failures than dimensional drift.
Material and Surface Finish
Surface specification for sheet metal parts hs code is electropolish Ra 0.2, chosen for the service environment in robotics. Thickness is verified on a reference coupon from the same batch rather than assumed from process settings.
Where sheet metal parts hs code sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Recycled content and RoHS/REACH declarations are available for sheet metal parts hs code on request. If your robotics customer audits material origin, ask for the mill certificate at quote stage, not at delivery.
Tolerance and Inspection
First-article inspection for sheet metal parts hs code reports every dimension on the drawing, not a sample of them. That report is the reference for the rest of the batch and for any future reorder.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on sheet metal parts hs code, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Non-conforming material is quarantined physically, not just in the system. For sheet metal parts hs code, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
Service environment drives more redesigns than load does. sheet metal parts hs code in outdoor or washdown service needs electropolish Ra 0.2 and sealing considered at design stage, not added later.
Vibration and cycling are the usual life limiters for sheet metal parts hs code. If the duty cycle is known, we can recommend a surface treatment and hardness combination that extends service life without changing dimensions.
What to Confirm Before Ordering
Ask for the first-article report before you ask for a price cut on sheet metal parts hs code. A supplier who cannot produce dimensional data at 1000 pcs will not produce it at .
Confirm the reorder path. If sheet metal parts hs code is documented with tooling drawings and a first-article report on file, a repeat order years later reproduces the original part instead of approximating it.
FAQ: Your Questions Before Ordering
What tolerance can you hold on sheet metal parts hs code?
General dimensions are held to ±0.005 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
Further technical detail: Toy Battery Contact Spring Power Terminal Custom Mold Making.
What is the minimum order quantity for sheet metal parts hs code?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.005 mm would require an extra operation, so you can decide before tooling.
What surface finishes are available for sheet metal parts hs code?
electropolish Ra 0.2 is standard for sheet metal parts hs code. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
Recommended reading: CNC Spring Coiling Machine Guide: Precision, Tolerances, and Process Control.
Can you prototype before tooling?
Yes, and we recommend it. Prototyping sheet metal parts hs code without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
How do you handle a design change mid-program?
Changes are documented against the original first-article report. We identify which dimensions are affected, requote only the affected operations, and tell you whether existing stock of sheet metal parts hs code remains usable.
If sheet metal parts hs code is already in production elsewhere, send a sample and the current drawing. We will quote against it and tell you honestly whether switching improves cost, lead time, or neither.
Compare it with Stamping Die Manufacturing Time: Lead Times, Cost Drivers, and Process Breakdown.
Related reading: About BQUQ.
See also: What Are the Key Benefits of CNC Machined Components for Automotive Applications?.
Learn more about Plating for Stamped Spring Contacts: Gold, Tin and Nickel.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Aluminium 7075-T6 |
| Tolerance | ±0.005 mm |
| Surface finish | electropolish Ra 0.2 |
| Lead time | 20 working days |
| MOQ | 1000 pcs |
| Capacity | batch production at 1000 pcs |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Standard single-source part | Low-volume or non-critical robotics builds | Limited documentation; may not meet PPAP-style records at 1000 pcs |
| Qualified custom part | Robotics programs needing material certificates and first-article reports | Higher upfront documentation and process validation effort |
| Single slow sample | Design verification only | Does not prove ±0.005 mm at production speed |
| Production-speed batch | 1000 pcs orders with 20 working days lead time | Requires fixed material condition and tooling geometry first |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Material conditioning | Fix material condition before machining | Material certificates |
| Tooling setup | Fix tooling geometry around the process window | Tooling design records |
| Production run | Hold ±0.005 mm at production speed, not on a single slow part | First-article reports |
| Batch documentation | Confirm process capability at 1000 pcs | PPAP-style records |
| Final inspection | Verify electropolish Ra 0.2 and batch consistency | Inspection records |
Frequently Asked Questions
What HS code applies to aluminium 7075-T6 sheet metal parts?
HS code depends on the specific part function and material composition, not on the machining route. For aluminium 7075-T6 parts with electropolish Ra 0.2 and ±0.005 mm tolerance, confirm the code with your customs broker using the material certificate and part drawing before ordering 1000 pcs.
Can you hold ±0.005 mm across a 1000 pcs production run?
Yes, provided material condition and tooling geometry are fixed first. We confirm ±0.005 mm at production speed rather than on a single slow part. This is documented through first-article reports and PPAP-style records at the 1000 pcs MOQ, with a 20 working days lead time.
What documentation is included at 1000 pcs?
At 1000 pcs, documentation includes material certificates, first-article reports, and PPAP-style records. These are now requested at 1000 pcs rather than at mass production because robotics buyers need process capability evidence. The 20 working days lead time covers production after drawing approval.
What is the lead time if the drawing changes?
The standard production lead time is 20 working days. If the drawing changes, the process window, material condition, and tooling geometry must be re-confirmed before production restarts. We recommend freezing the drawing before the 1000 pcs run to protect the 20 working days schedule.
What surface finish can you achieve on aluminium 7075-T6 sheet metal parts?
We achieve electropolish Ra 0.2 on aluminium 7075-T6 sheet metal parts. This finish is verified alongside the ±0.005 mm tolerance and documented in first-article reports. For 1000 pcs orders, surface finish consistency is checked as part of the PPAP-style record set.
Why do robotics buyers request PPAP-style records at 1000 pcs?
Robotics demand has shifted from single-source standard parts to qualified custom parts, pushing documentation upstream. Buyers now request material certificates, first-article reports, and PPAP-style records at 1000 pcs rather than at mass production. This rewards suppliers who can document process capability at ±0.005 mm across batches.
What should I confirm before ordering sheet metal parts?
Confirm material condition, tooling geometry, and that ±0.005 mm is held at production speed. Verify electropolish Ra 0.2, 20 working days lead time, and 1000 pcs MOQ. Also confirm material certificates, first-article reports, and PPAP-style records are available at 1000 pcs before releasing the order.
Further technical detail: OEM aluminum heat sink service.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Aluminium 7075-T6 |
| Tolerance | ±0.005 mm |
| Lead time | 20 working days |
| MOQ | 1000 pcs |
| Capacity | Production runs at 1000 pcs MOQ |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Aluminium 7075-T6 | High-strength robotics parts | Higher cost than common alloys |
| Electropolish Ra 0.2 | Smooth surface, corrosion resistance | Added process time and cost |
| ±0.005 mm tolerance | Precision assemblies | Requires capable supplier and inspection |
| 1000 pcs MOQ | Production scale programs | Higher upfront commitment |
| 20 working days lead time | Planned robotics builds | May extend if drawing changes |
Frequently Asked Questions
What HS code applies to aluminium 7075-T6 sheet metal parts?
HS code classification depends on material and function, not the machining route. For aluminium 7075-T6 parts, the code is typically under aluminium articles, but the exact heading depends on the part's function and whether it is a finished or semi-finished product. Confirm with a customs broker using the part drawing and material cert.
Does electropolish Ra 0.2 change the HS code?
No. Surface finish like electropolish Ra 0.2 does not change the HS code. Classification is based on material and function. The code remains tied to the aluminium 7075-T6 part and its end use, not the surface treatment.
What documentation is required for 1000 pcs orders?
At 1000 pcs, buyers should confirm material certificates, first-article reports, and PPAP-style records. These documents verify process capability and traceability. Robotics programs now require documented process capability rather than single-sample results, so ensure these records are included.
Can you hold ±0.005 mm tolerance across batches?
Yes. Production runs at 1000 pcs MOQ with ±0.005 mm tolerance held across batches. This requires capable processes and inspection. Confirm the supplier's process capability records and first-article reports to ensure consistency across the entire order.
Recommended reading: Custom CNC Machined ER40 Spring Collet Chuck for End Mill Milling.
What is the lead time for 1000 pcs of aluminium 7075-T6 parts?
Lead time is 20 working days for production. However, if the drawing changes, the lead time may be affected. Confirm the final drawing before production to avoid delays. The 20 working days applies to standard production runs at 1000 pcs MOQ.
What is the MOQ for sheet metal parts with electropolish Ra 0.2?
The MOQ is 1000 pcs for production runs. This applies to aluminium 7075-T6 parts with electropolish Ra 0.2 and ±0.005 mm tolerance. For smaller quantities, consult the supplier for feasibility and pricing.
Compare it with Metal Stamping Die Design for CNC Finishing: Best Practices.
Why do robotics programs require PPAP-style records at 1000 pcs?
Robotics programs require documented process capability rather than single-sample results. At 1000 pcs, PPAP-style records, material certificates, and first-article reports ensure the supplier can hold ±0.005 mm across batches. This reduces risk and ensures consistency for qualified custom parts.