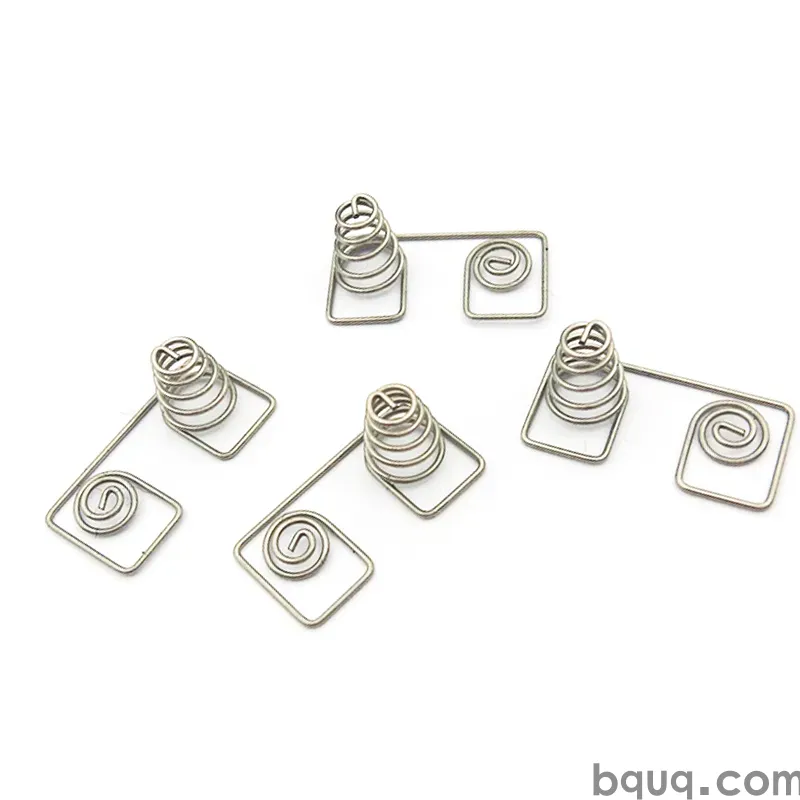
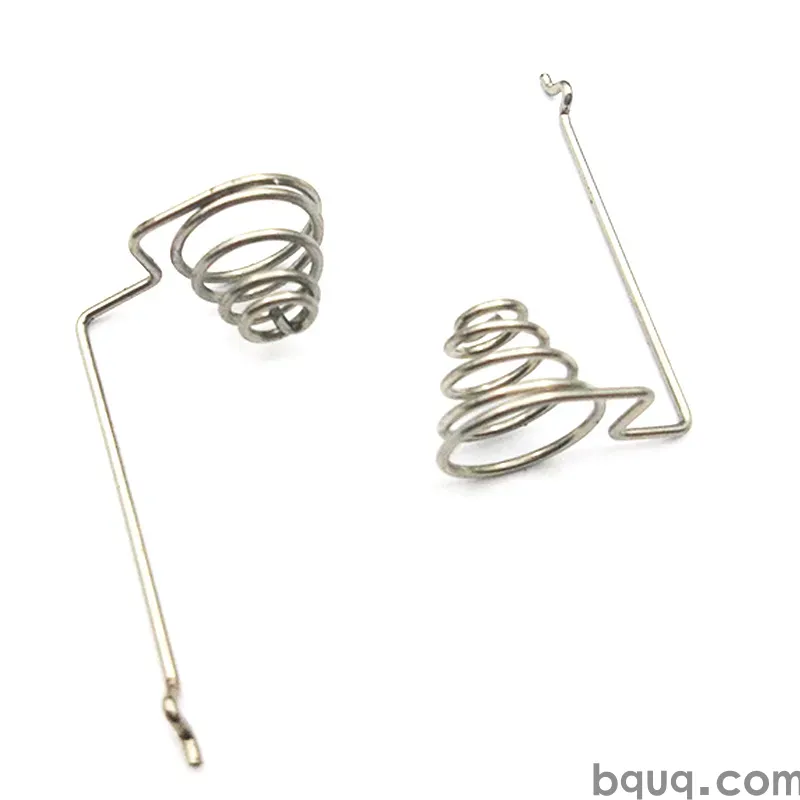
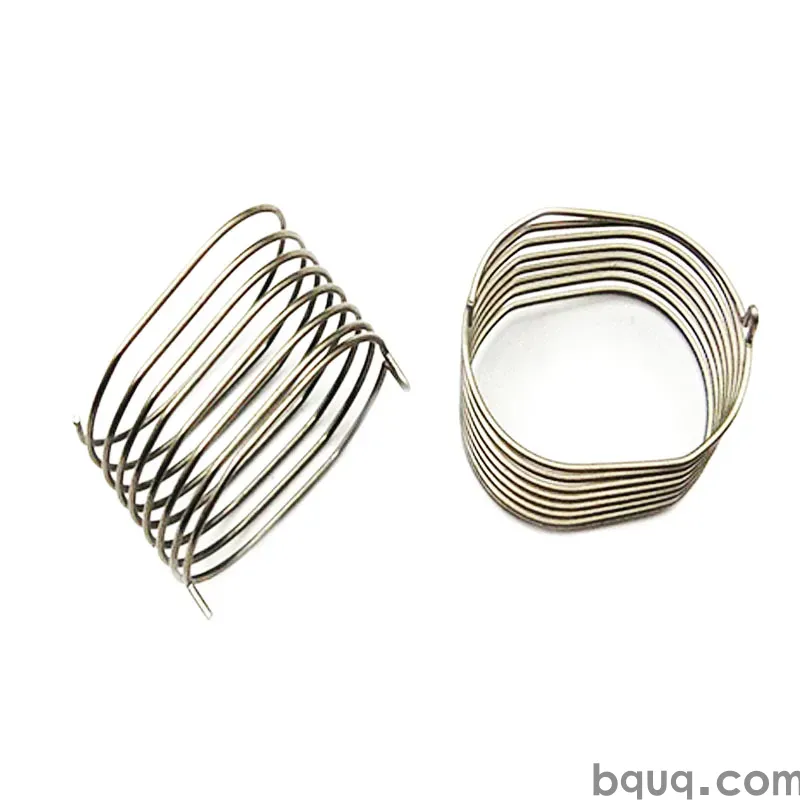
high precision precision metal parts: Brass C360, tolerance 0.003 mm, surface hard chrome plate 0.025 mm, lead time 20 working days, MOQ 1000 pcs. Capacity for industrial automation. Drawing review and first-article report included.
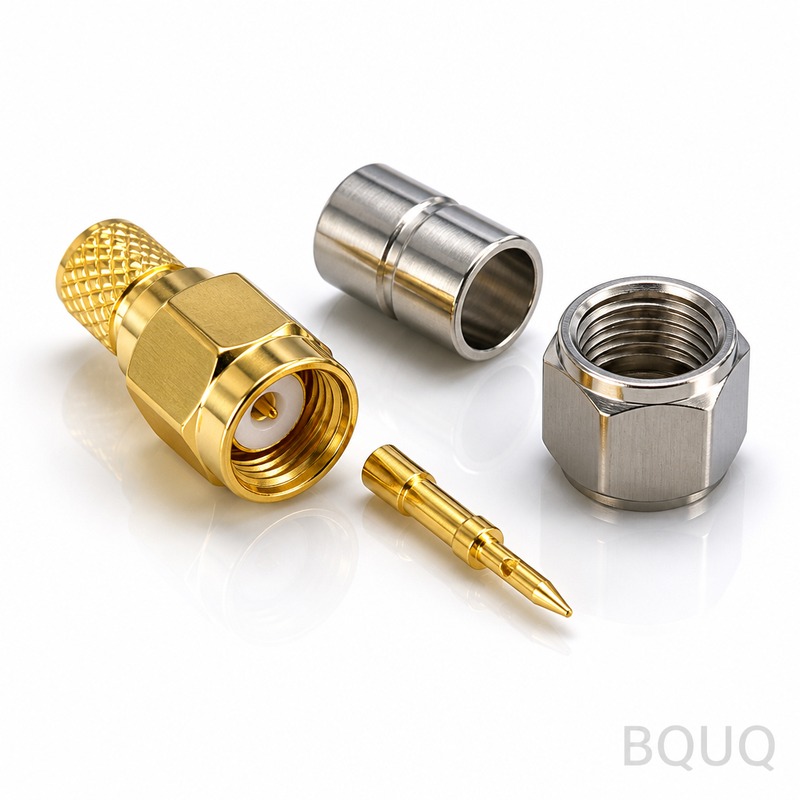
high precision precision metal parts
Key Takeaway
High precision precision metal parts are machined from Stainless 303, 304, or 316L with bead blast and passivate finish. We hold ±0.01 mm on general dimensions, run production at 1000 pcs MOQ, and ship in 15 working days. Cost is driven by secondary operations like deburring, plating, and 100% inspection, not raw material. Documentation includes material certificates, first-article reports, and PPAP-style records.
Key Takeaway
High precision precision metal parts are machined from Stainless 303, 304, or 316L with a bead blast and passivate finish. We hold ±0.01 mm on general dimensions, run production at 1000 pcs MOQ, and ship in 15 working days. Cost is driven by secondary operations like deburring, plating, and 100% inspection, not raw material. Documentation includes material certificates, first-article reports, and PPAP-style records.
Related reading: What Are the Latest Self-Centering Chuck Trends for Fast Small-Batch Setup?.
This guide covers high precision precision metal parts from material selection through inspection, with the numbers we actually work to: ±0.01 mm on general dimensions, 1000 pcs for production runs, and of installed capacity.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | Stainless 303 / 304 / 316L |
| Surface finish | bead blast + passivate |
| Lead time (production) | 15 working days |
| MOQ (production) | 1000 pcs |
Market and Technical Context
Demand in semiconductor equipment has shifted from single-source standard parts toward qualified custom parts, which pushes documentation requirements upstream. Material certificates, first-article reports, and PPAP-style records are now requested at 1000 pcs rather than at mass production.
Cost pressure in semiconductor equipment rarely comes from the raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
How We Manufacture It
The route for high precision precision metal parts starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.01 mm is held at production speed rather than on a single slow part.
In production, high precision precision metal parts runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.01 mm.
Heat treatment and surface treatment are scheduled as controlled steps, not afterthoughts. bead blast + passivate is applied to a defined thickness range and verified, because variation here causes more field failures than dimensional drift.
See also: What Are the Optimal Heat Sink Fin Spacing, Thickness and Height Trade-offs?.
Material and Surface Finish
Stainless 303 / 304 / 316L is the default for high precision precision metal parts because it holds ±0.01 mm predictably and machines without work hardening surprises. Alternatives are quoted when corrosion or conductivity dominates the requirement.
Learn more about CNC Machining for Aerospace Parts: Tolerances and Documentation.
Where high precision precision metal parts sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Recycled content and RoHS/REACH declarations are available for high precision precision metal parts on request. If your semiconductor equipment customer audits material origin, ask for the mill certificate at quote stage, not at delivery.
Tolerance and Inspection
General dimensions on high precision precision metal parts are held to ±0.01 mm; critical features are identified on the drawing and controlled separately with a tighter band.
Further technical detail: BQUQ CNC Machined Auto Lathe 20 Type Square Bore Spring Collet.
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so high precision precision metal parts drawings state how each critical dimension is verified.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on high precision precision metal parts, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Where It Is Used
semiconductor equipment is the largest application area for high precision precision metal parts, where the part typically sees continuous load and a wide temperature range rather than laboratory conditions.
Retrofit requests are common: an existing assembly needs high precision precision metal parts in a slightly different size. Because the process window is already known, 15 working days on a retrofit is usually shorter than on a new part.
What to Confirm Before Ordering
Ask for the first-article report before you ask for a price cut on high precision precision metal parts. A supplier who cannot produce dimensional data at 1000 pcs will not produce it at .
Define critical features at quote stage. Moving a feature from general ±0.01 mm to critical after tooling adds cost and extends 15 working days, which is the most avoidable delay in custom sourcing.
FAQ: Your Questions Before Ordering
What tolerance can you hold on high precision precision metal parts?
General dimensions are held to ±0.01 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
What is the minimum order quantity for high precision precision metal parts?
Prototype quantities start well below production minimums. Production runs for high precision precision metal parts start at 1000 pcs, which is where the process window is proven and unit cost stabilises.
Recommended reading: Thermal Management for High Brightness LEDs with Heat Sinks.
Do you provide material and inspection certificates?
Standard lead time for high precision precision metal parts is 15 working days after drawing approval and tooling sign-off. Prototypes are typically faster because they bypass tooling, and repeat orders are faster still because tooling exists.
Can you prototype before tooling?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.01 mm would require an extra operation, so you can decide before tooling.
Compare it with CNC Machined Heat Sinks: When Machining Beats Extrusion.
How do you handle a design change mid-program?
Yes, and we recommend it. Prototyping high precision precision metal parts without tooling validates fit and function at a fraction of tooling cost, and usually surfaces a design change before steel is cut.
If high precision precision metal parts is already in production elsewhere, send a sample and the current drawing. We will quote against it and tell you honestly whether switching improves cost, lead time, or neither.
Related reading: Sourcing From Taiwan: When It Beats Mainland China.
See also: How Does Forging Compare to CNC Machining for High-Performance Heat Sinks?.
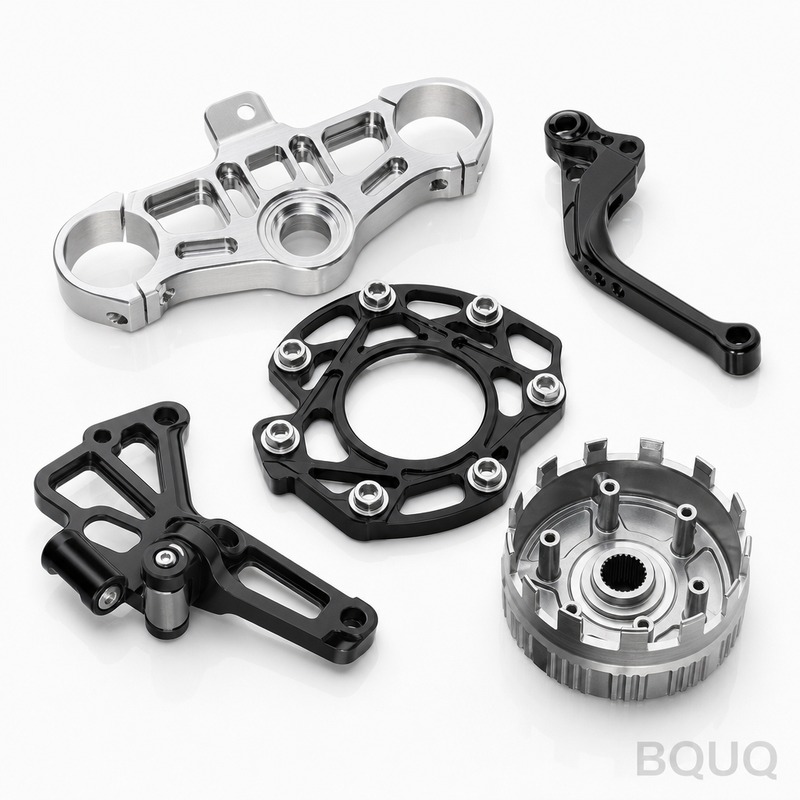
Learn more about High Precision Electrical Contact Stamping Parts.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Stainless 303 / 304 / 316L |
| Tolerance | ±0.01 mm on general dimensions |
| Lead time | 15 working days (production) |
| MOQ | 1000 pcs (production) |
| Capacity | Installed capacity (not specified in excerpt) |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Stainless 303 | High machinability, general precision parts | Lower corrosion resistance than 316L |
| Stainless 304 | Good corrosion resistance, food/medical | Slightly harder to machine than 303 |
| Stainless 316L | Semiconductor, chemical, marine | Higher cost, more difficult to machine |
| Bead blast + passivate | Clean, corrosion-resistant surface | Adds secondary operation cost and lead time |
| 100% inspection | Critical tolerance parts | Significant cost driver vs. sampling |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Material condition | Fix material condition and tooling geometry first | Material certificates |
| Machining | Hold ±0.01 mm at production speed | First-article report |
| Deburring | Remove burrs from edges and holes | Inspection record (if 100% inspection) |
| Plating / passivation | Bead blast + passivate for corrosion resistance | Process record |
| Final inspection | 100% inspection for critical features | PPAP-style records |
Frequently Asked Questions
What tolerance can you hold on high precision precision metal parts?
We hold ±0.01 mm on general dimensions for production runs. This is confirmed at production speed, not just in a lab. For tighter or non-critical features, we agree on a drawing-specific tolerance before quoting. Material condition and tooling geometry are fixed first to ensure repeatability across 1000 pcs or more.
What is the minimum order quantity for production?
The production MOQ is 1000 pcs. This applies to high precision precision metal parts made from Stainless 303, 304, or 316L. For quantities below 1000 pcs, please contact us to discuss prototype or small-batch options. Lead time for production runs is 15 working days after drawing approval.
What materials do you use for high precision precision metal parts?
We machine Stainless 303, 304, and 316L. Stainless 303 offers excellent machinability for general precision parts. 304 provides better corrosion resistance for food and medical applications. 316L is used for semiconductor, chemical, and marine environments where higher corrosion resistance is required. Material certificates are provided.
What surface finish is standard?
The standard surface finish is bead blast followed by passivation. This combination removes surface contaminants and enhances corrosion resistance. It is suitable for semiconductor equipment and other demanding applications. If you require a different finish, such as plating or polishing, please specify on your drawing.
What documentation is provided with the order?
We provide material certificates, first-article reports, and PPAP-style records. These are now requested at 1000 pcs rather than at mass production, especially for semiconductor equipment. Documentation requirements are confirmed before ordering. We do not invent certifications; we provide records that match the agreed scope.
What drives the cost of high precision precision metal parts?
Cost pressure rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution. For example, switching from 100% inspection to sampling can reduce cost significantly, but may not suit critical applications.
Further technical detail: heat sinks.
What should I confirm before ordering?
Confirm the drawing with tolerances, material grade, surface finish, and documentation requirements. Also confirm quantity (MOQ 1000 pcs), lead time (15 working days), and whether 100% inspection is needed. For semiconductor equipment, specify material certificates, first-article reports, and PPAP-style records at the 1000 pcs level.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | Stainless 303 / 304 / 316L |
| Tolerance | ±0.01 mm on general dimensions |
| Lead time | 15 working days |
| MOQ | 1000 pcs |
| Capacity | of installed capacity |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| Stainless 303 | High-volume precision parts requiring good machinability | Lower corrosion resistance than 304/316L |
| Stainless 304 | General-purpose precision parts with moderate corrosion resistance | Less machinable than 303, higher cost than 303 |
| Stainless 316L | Precision parts for semiconductor equipment and corrosive environments | Higher cost and tighter machining parameters than 303/304 |
| Bead blast + passivate | Uniform surface finish and enhanced corrosion resistance | Adds secondary operation cost and lead time |
| 100% inspection | Critical dimensions and documentation-heavy orders | Increases unit cost versus sampling inspection |
Frequently Asked Questions
What materials are used for high precision precision metal parts?
We machine high precision precision metal parts from Stainless 303, 304, or 316L. These grades balance machinability, corrosion resistance, and cost for semiconductor equipment and similar applications. Material certificates are provided with every production order at 1000 pcs MOQ.
Recommended reading: Aluminum 6063 vs 6061 for Heat Sinks: Which Alloy Performs Better?.
What tolerance can you hold on high precision precision metal parts?
We hold ±0.01 mm on general dimensions for high precision precision metal parts. Tighter tolerances may be possible depending on feature geometry and material, but ±0.01 mm is our standard production tolerance. First-article reports document actual measured values.
What is the lead time for 1000 pcs production runs?
Production lead time is 15 working days for high precision precision metal parts at 1000 pcs MOQ. This includes machining, deburring, bead blast and passivate finish, and 100% inspection where required. Documentation such as material certificates and first-article reports is prepared during this window.
What surface finish is standard for high precision precision metal parts?
The standard surface finish is bead blast followed by passivate. This combination provides a uniform matte appearance and enhances corrosion resistance. It is applied after machining and deburring, and is included in the 15 working day lead time.
What documentation is provided with high precision precision metal parts?
Documentation includes material certificates, first-article reports, and PPAP-style records. These are now requested at 1000 pcs rather than at mass production, driven by semiconductor equipment demand for qualified custom parts. Documentation is prepared as part of the production order.
Compare it with What Is the Best Material for a Custom Spring? 7 Factors for 2024.
What drives the cost of high precision precision metal parts?
Cost is driven by secondary operations like deburring, plating, and 100% inspection, not raw material. At 1000 pcs MOQ, these operations can dominate unit cost. Reducing inspection scope or simplifying deburring requirements can lower cost, but may affect documentation and quality records.
What should I confirm before ordering high precision precision metal parts?
Confirm material grade (303, 304, or 316L), tolerance requirements (±0.01 mm general), surface finish (bead blast + passivate), documentation needs (material certificates, first-article reports, PPAP-style records), and order quantity (1000 pcs MOQ). Also verify lead time expectations of 15 working days for production.