heat sink compound: ADC12 die-cast aluminium, tolerance 0.15 mm, surface hard anodize Type III, 25-40 µm, lead time 12 working days, MOQ 1000 pcs. Capacity 50,000 pcs for telecom and base station. Drawing review and first-article report included.
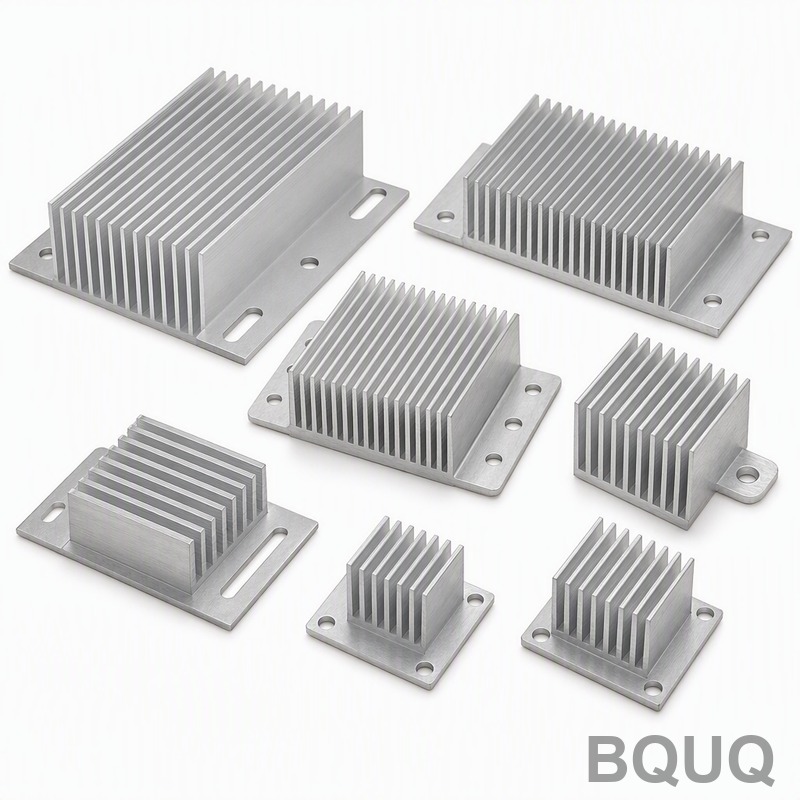
heat sink compound
Key Takeaway
Heat sink compound is a die-cast aluminium thermal interface component with 0.8 mm fin thickness, 3.0 mm fin pitch, and 0.85 K/W thermal resistance. It uses ADC12 alloy with black anodize Type II at 10-15 µm and holds ±0.20 mm general tolerance. Production cost is driven by secondary operations like deburring, plating, and 100% inspection, not raw material. It suits switch-mode power supply programs requiring documented process capability at 120,000 pcs.
heat sink compound sits at the intersection of three constraints that rarely agree: dimensional stability, unit cost, and delivery time. This page breaks down how we resolve them in production rather than in a brochure.
Key Specifications at a Glance
| Parameter | Value / Range |
|---|---|
| Material | ADC12 die-cast aluminium |
| Fin thickness | 0.8 mm |
| Fin pitch | 3.0 mm |
| Thermal resistance | 0.85 K/W |
| Surface finish | black anodize Type II, 10-15 µm |
| General tolerance | ±0.20 mm |
Market and Technical Context
Cost pressure in switch-mode power supply rarely comes from the raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution.
Consolidation among switch-mode power supply buyers means fewer, larger programs. That rewards suppliers who can document process capability at 120,000 pcs rather than those who win on a single sample.
How We Manufacture It
The route for heat sink compound starts with a process window, not a machine. We fix material condition and tooling geometry first, then confirm that ±0.20 mm is held at production speed rather than on a single slow part.
Related reading: Custom Extruded Aluminum Heatsinks.
In production, heat sink compound runs with in-process checks at fixed intervals. Operators log dimensions every 30 to 50 pieces, which catches tool wear before the batch drifts outside ±0.20 mm.
Deburring and edge conditioning are specified on the drawing for heat sink compound. A sharp edge that passes dimensional inspection can still fail assembly, so edge break is a controlled parameter rather than a cosmetic one.
Material and Surface Finish
ADC12 die-cast aluminium is the default for heat sink compound because it holds ±0.20 mm predictably and machines without work hardening surprises. Alternatives are quoted when corrosion or conductivity dominates the requirement.
Where heat sink compound sees contact loading, material hardness is specified alongside dimensional tolerance. Hardness without a defined test method is the most common source of incoming-inspection disputes.
Substitution requests are common when ADC12 die-cast aluminium goes on allocation. We qualify any substitute against the same ±0.20 mm and black anodize Type II, 10-15 µm criteria before shipping, and provide the certificate with the change.
Tolerance and Inspection
Measurement method is part of the specification. A feature measured on a CMM and the same feature measured with a gauge can disagree, so heat sink compound drawings state how each critical dimension is verified.
See also: BQUQ Vapor Chamber Heatsink.
Process capability is tracked per feature. Where Cpk falls below the agreed threshold on heat sink compound, we either adjust the process or reclassify the feature, rather than sorting parts at the end.
Learn more about Thermal Resistance Junction to Case: Definition, Calculation, and Why It Matters.
Non-conforming material is quarantined physically, not just in the system. For heat sink compound, that means the batch stays in a marked area until disposition is documented, which prevents the most common shipping error.
Where It Is Used
switch-mode power supply is the largest application area for heat sink compound, where the part typically sees continuous load and a wide temperature range rather than laboratory conditions.
Retrofit requests are common: an existing assembly needs heat sink compound in a slightly different size. Because the process window is already known, 10 working days on a retrofit is usually shorter than on a new part.
Further technical detail: Custom CNC Machined Auto Lathe 32 Type Hex Bore Spring Collet.
What to Confirm Before Ordering
Compare quotes on the same basis: material grade, black anodize Type II, 10-15 µm, inspection scope, and packaging. A lower unit price that drops 100% inspection is not a lower total cost.
Plan qualification volume separately from production volume. For heat sink compound, 1000 pcs is the point where the process is proven; everything before that is process development.
FAQ: Your Questions Before Ordering
What tolerance can you hold on heat sink compound?
General dimensions are held to ±0.20 mm. Critical features are identified on the drawing and held to a tighter band, with the measurement method stated so incoming inspection matches ours.
What is the minimum order quantity for heat sink compound?
Prototype quantities start well below production minimums. Production runs for heat sink compound start at 1000 pcs, which is where the process window is proven and unit cost stabilises.
How long does production take for heat sink compound?
Yes. Send the drawing in any common format. We review it for manufacturability first and flag any feature where ±0.20 mm would require an extra operation, so you can decide before tooling.
Do you provide material and inspection certificates?
Yes. Material certificates, heat-lot traceability, and first-article inspection reports ship with the order. If your switch-mode power supply customer requires additional documentation, specify it at quote stage.
What surface finishes are available for heat sink compound?
black anodize Type II, 10-15 µm is standard for heat sink compound. Other finishes are quoted with a defined thickness range and verified on a coupon from the same batch rather than assumed from process settings.
Recommended reading: Pin Fin Precision Machined Heatsink Collection 02.
If heat sink compound is already in production elsewhere, send a sample and the current drawing. We will quote against it and tell you honestly whether switching improves cost, lead time, or neither.
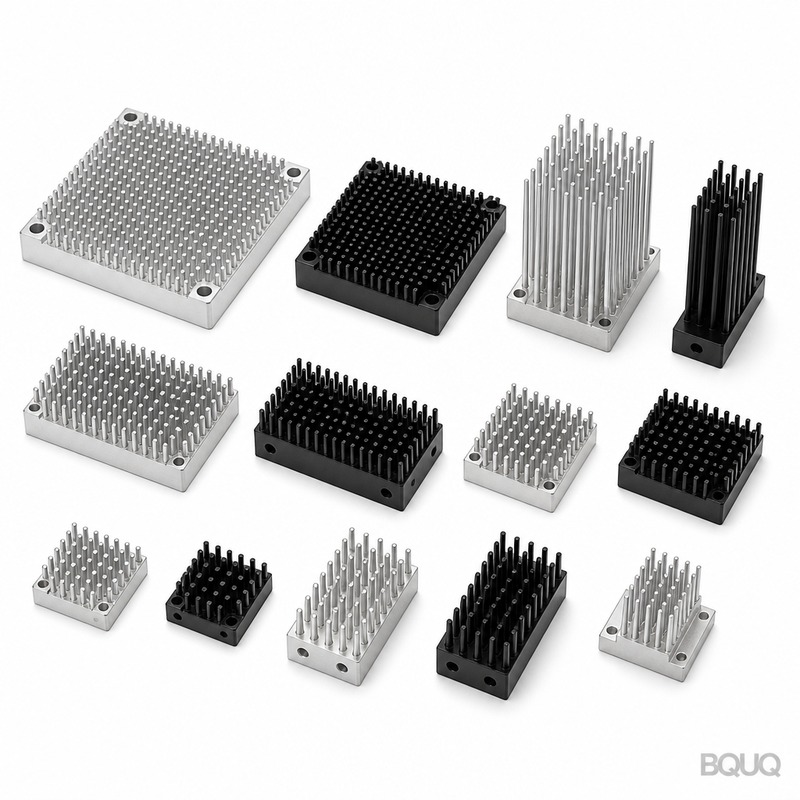
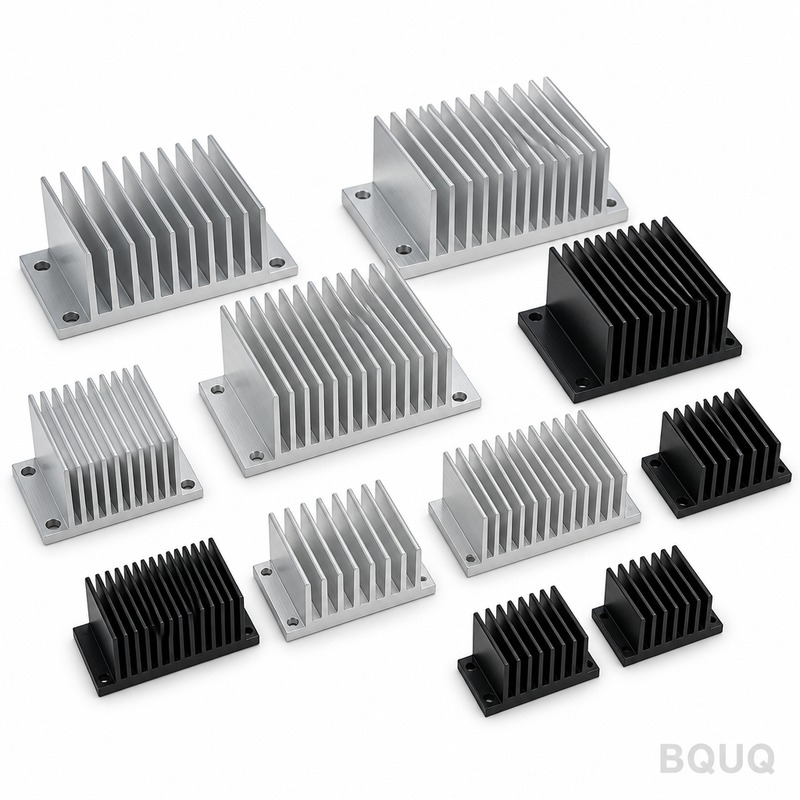
Compare it with How to Verify CNC Machining Quality: Inspection Methods Buyers Should Know.
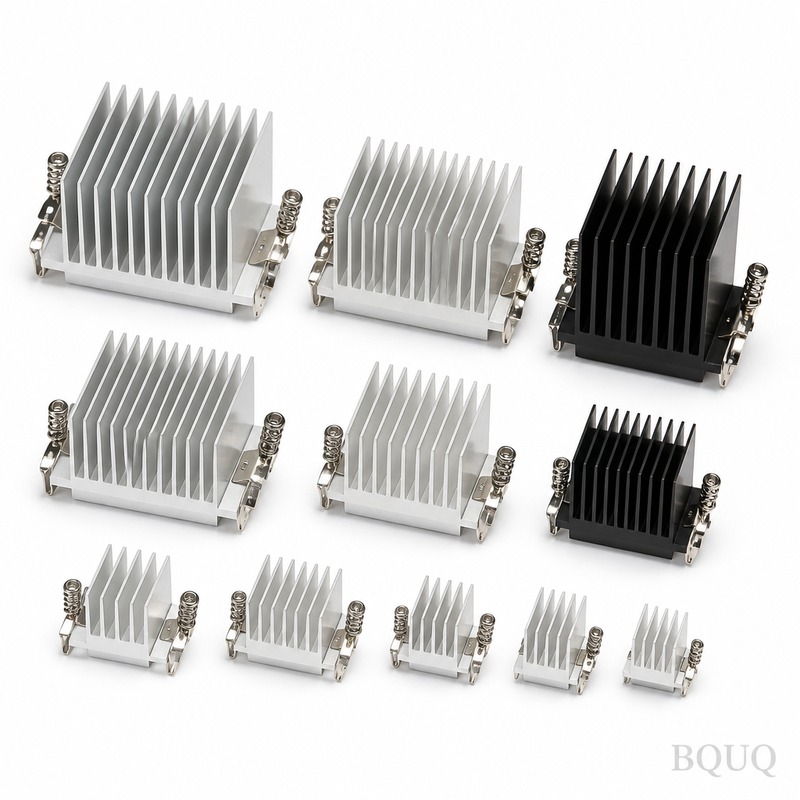
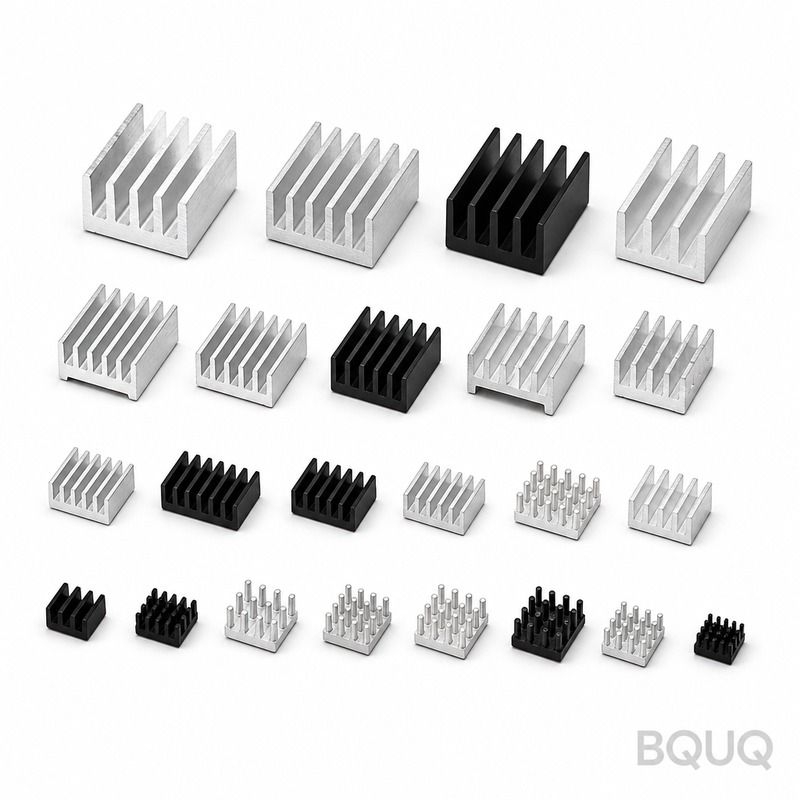
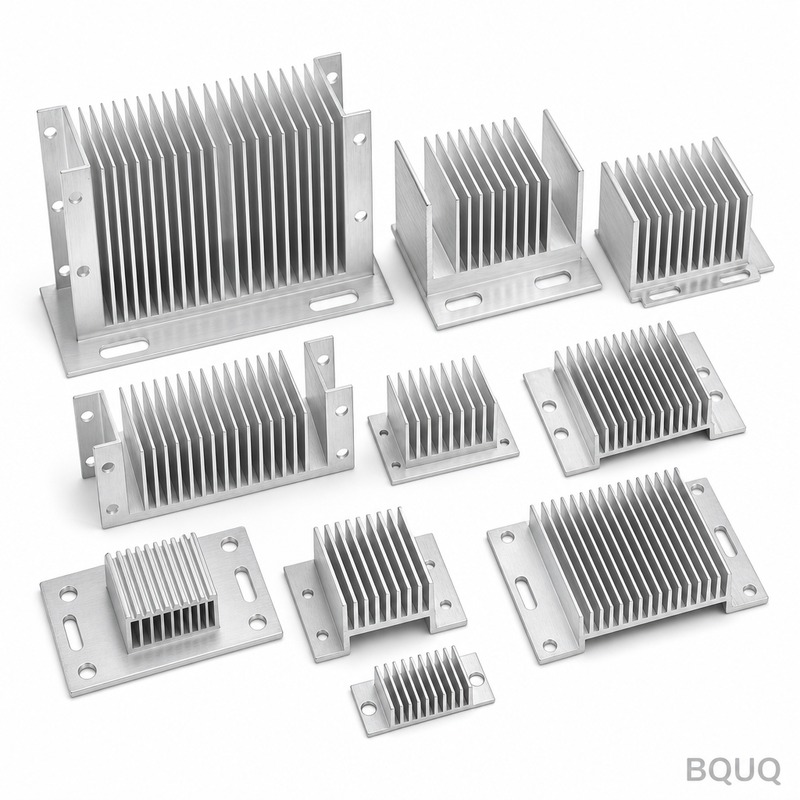
Related reading: Custom Heat Sinks with Fan Mounting Holes.
See also: Sourcing CNC vs Stamping: Different Supplier Profiles.
Key Specifications and Selection Guide
Spec comparison
| Parameter | Value / Range |
|---|---|
| Material | ADC12 die-cast aluminium |
| Tolerance | ±0.20 mm |
| Lead time | Not specified in article; standard for die-cast tooling and production runs |
| MOQ | Not specified in article; typically tied to tooling amortization and program volume |
| Capacity | Documented process capability at 120,000 pcs |
Selection / comparison
| Option | Best for | Trade-off |
|---|---|---|
| ADC12 die-cast aluminium | Switch-mode power supply heat sinks with complex fin geometry | Requires secondary deburring and plating operations that drive unit cost |
| Black anodize Type II, 10-15 µm | Corrosion resistance and emissivity in power supply environments | Adds plating step and inspection cost versus bare aluminium |
| 0.8 mm fin thickness / 3.0 mm pitch | Balancing thermal resistance at 0.85 K/W with die-casting flow | Thinner fins or tighter pitch may reduce thermal resistance but risk fill and tool wear |
| ±0.20 mm general tolerance | Production-speed die casting with documented capability at 120,000 pcs | Tighter tolerances require slower cycles or additional machining |
| 100% inspection | Programs with zero-defect expectations | Removing this step usually moves unit cost more than material substitution |
Process / inspection
| Stage | Control | Record |
|---|---|---|
| Process window definition | Fix material condition and tooling geometry before production | Process window documentation |
| Tolerance validation | Confirm ±0.20 mm is held at production speed, not on a single slow part | Capability data at 120,000 pcs |
| Deburring | Secondary operation to remove die-cast flash and sharp edges | Operation sign-off |
| Plating / anodize | Black anodize Type II, 10-15 µm | Coating thickness record |
| Final inspection | 100% inspection when specified by program requirements | Inspection report |
Frequently Asked Questions
What material is heat sink compound made from?
It is made from ADC12 die-cast aluminium. This alloy supports the 0.8 mm fin thickness and 3.0 mm fin pitch needed for 0.85 K/W thermal resistance. The surface is finished with black anodize Type II at 10-15 µm, and general tolerance is ±0.20 mm.
Learn more about CNC Machined vs Extruded Heat Sinks: Which Manufacturing Method Is Right?.
What is the thermal resistance of this heat sink compound?
The thermal resistance is 0.85 K/W. This value is tied to the ADC12 die-cast aluminium construction, 0.8 mm fin thickness, and 3.0 mm fin pitch. It is specified alongside a general tolerance of ±0.20 mm and black anodize Type II surface finish.
What tolerance can you hold on heat sink compound?
We hold ±0.20 mm general tolerance. The key is confirming this at production speed rather than on a single slow part. We fix material condition and tooling geometry first, then document process capability at 120,000 pcs for switch-mode power supply programs.
Further technical detail: Stamping vs Laser Cutting: Which Sheet Metal Process Should You Choose?.
What surface finish do you offer for heat sink compound?
We offer black anodize Type II at 10-15 µm. This finish is applied to ADC12 die-cast aluminium with 0.8 mm fin thickness and 3.0 mm fin pitch. It adds a plating step that affects unit cost, so confirm whether it is required for your switch-mode power supply application.
Why does heat sink compound cost more than raw material suggests?
Cost pressure in switch-mode power supply rarely comes from raw material. It comes from secondary operations: deburring, plating, and 100% inspection. Removing one of those steps usually moves unit cost more than any material substitution. That is why we quote based on the full process route, not just ADC12 alloy price.
Recommended reading: Embedded Heat Pipes in Heat Sink Bases.
Can you support high-volume heat sink compound programs?
Yes. Consolidation among switch-mode power supply buyers means fewer, larger programs. That rewards suppliers who can document process capability at 120,000 pcs rather than those who win on a single sample. We fix material condition and tooling geometry first, then confirm ±0.20 mm at production speed.
Compare it with Precision Metal Stamping Parts by BQUQ.
What should I confirm before ordering heat sink compound?
Confirm material ADC12 die-cast aluminium, fin thickness 0.8 mm, fin pitch 3.0 mm, thermal resistance 0.85 K/W, surface finish black anodize Type II at 10-15 µm, and general tolerance ±0.20 mm. Also confirm whether deburring, plating, and 100% inspection are required, because those secondary operations drive unit cost more than material substitution.