OpeningThis is a 52-type round bore extended collet, machined to your exact drawing. We do not sell off-the-shelf approximations. Every unit is cut, heat-treated, and ground in our
OpeningThis is a 52-type round bore extended collet, machined to your exact drawing. We do not sell off-the-shelf approximations. Every unit is cut, heat-treated, and ground in our Dongguan factory, t
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
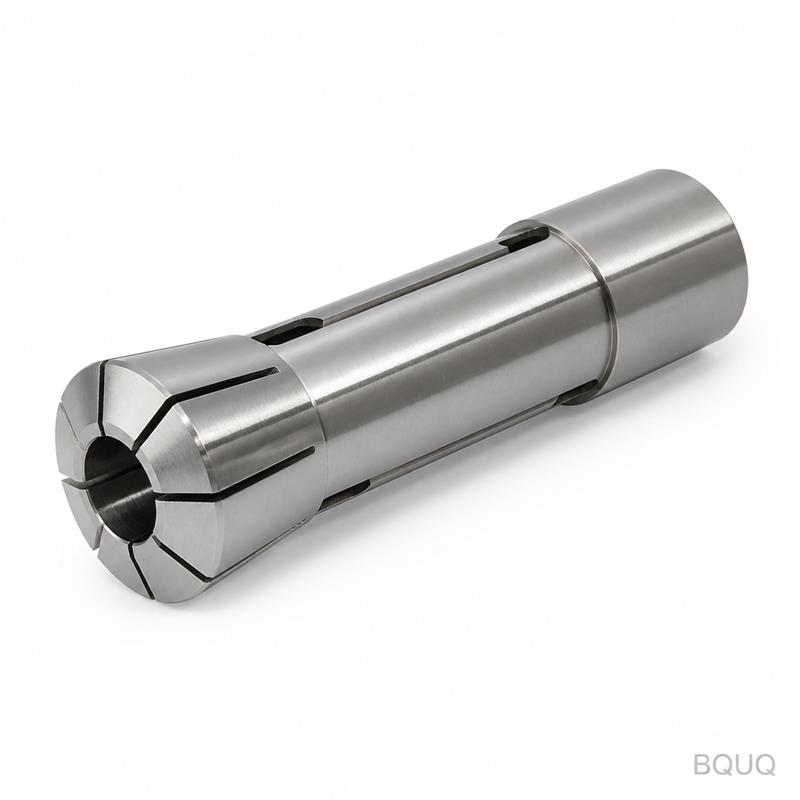
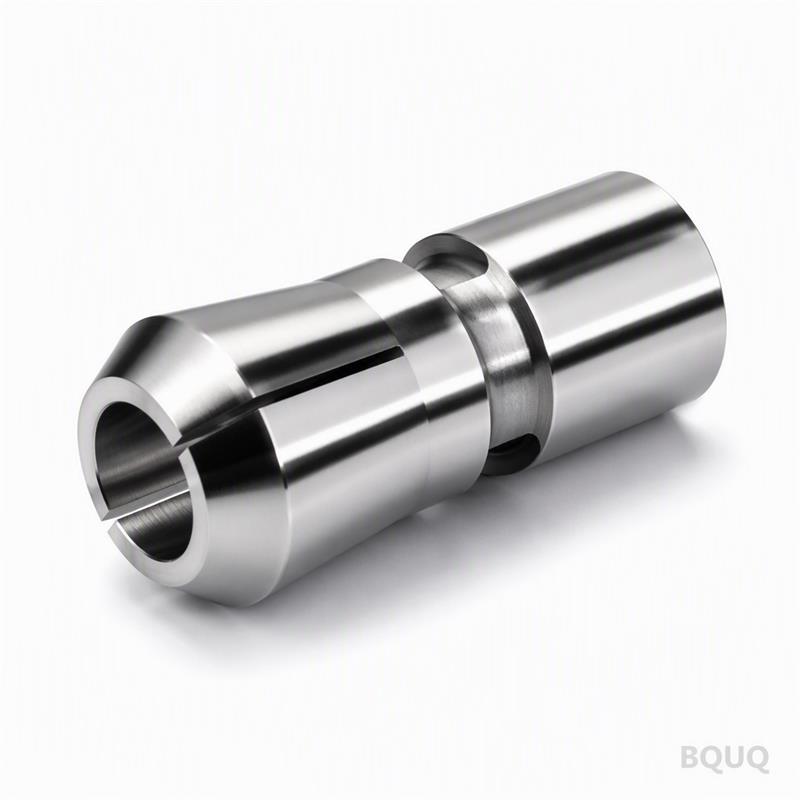
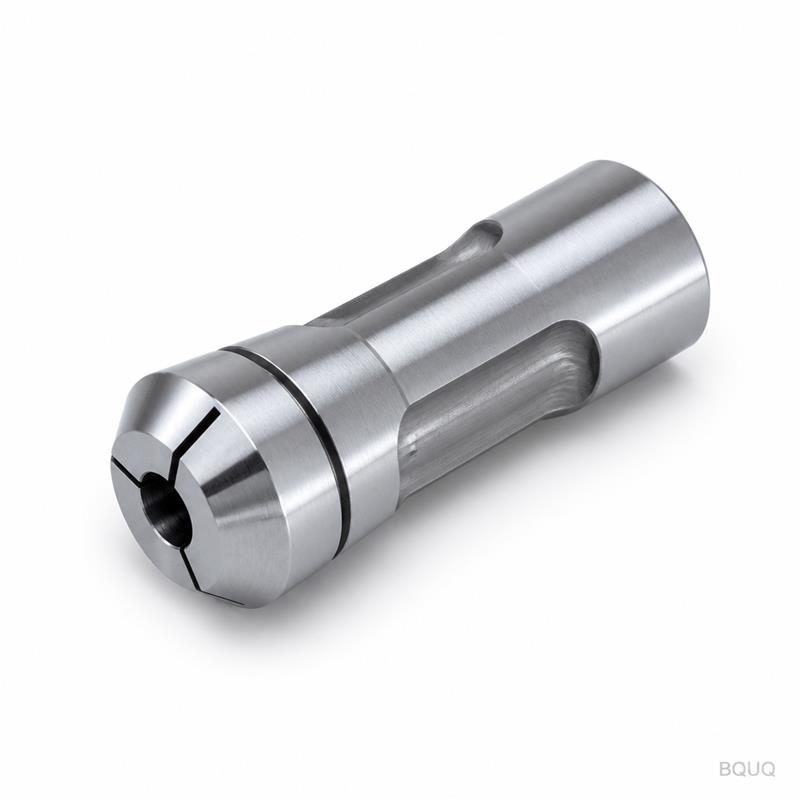
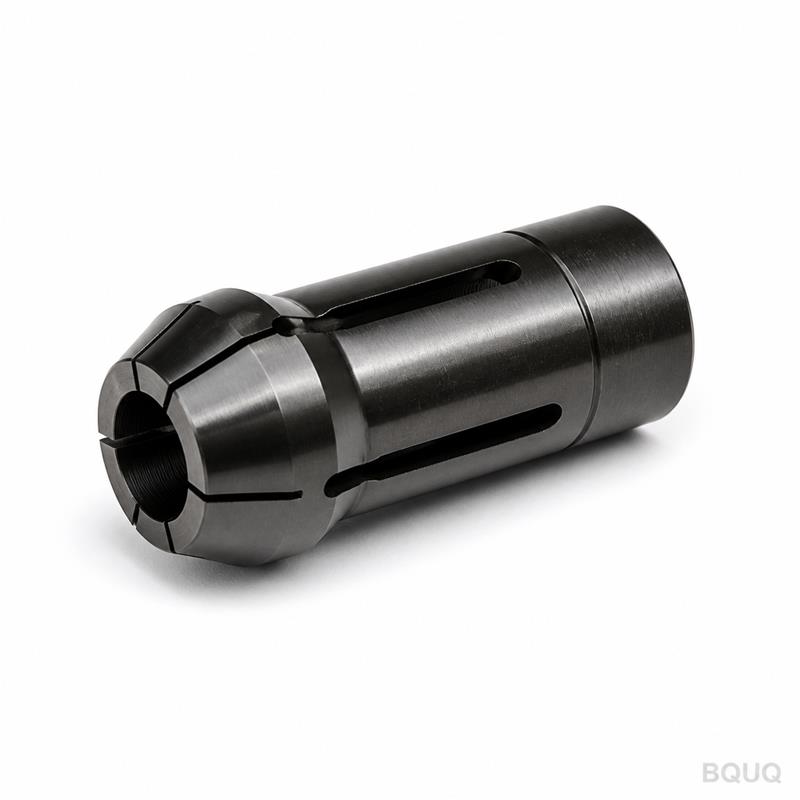
This is a 52-type round bore extended collet, machined to your exact drawing. We do not sell off-the-shelf approximations. Every unit is cut, heat-treated, and ground in our Dongguan factory, then verified for concentricity and bore tolerance before shipment. If the print says ±0.005 mm, that is what you get.
At a glance: Tolerance ±0.005 mm on bore and taper, surface finish Ra 0.4 µm, lead time 7–10 working days, no MOQ. One prototype or 5,000 pieces—same process control.
1. Batch-traceable quality. Each heat lot gets a unique code. We record material cert, heat treatment parameters, and final grind data. If a part fails in your spindle, we can trace it back to the exact furnace cycle. No guesswork.
2. Inspection report per batch. You do not have to ask. Every shipment includes a dimensional report with measured values for bore ID, taper angle, and concentricity. For critical runs, we add a CMM report and material cert. This is standard, not a paid extra.
3. One factory for CNC + stamping + springs + heat sinks. Your collet chuck is not an isolated part. If your assembly also needs a stamped retainer, a spring pusher, or a heat sink for the drive, we make all of it under one roof. Fewer vendors, fewer handoffs, fewer tolerance stack-ups. You send one drawing package; we coordinate the rest.
Where these parts are used
This 52-type extended collet is for CNC lathes and Swiss-type automatic lathes with a 52 mm spindle nose. The extended length reaches deeper into the workpiece, so you can grip longer bar stock or parts with recessed features without losing rigidity.
Bar feeding for automotive shafts and pins
Secondary operations on turned parts with long overhang
Precision gripping for hydraulic valve spools
Medical implant blanks (titanium, stainless) where surface finish and concentricity are critical
Aerospace fasteners requiring repeatable grip force across thousands of cycles
The round bore design handles solid round stock. If you need hex, square, or custom profiles, we can wire-cut the bore to match—just send the drawing.
Q: What is your MOQ?
A: No MOQ. We run one piece for prototypes and 5,000+ for production. Tooling is standard for 52-type collets, so there is no setup penalty for small batches.
Q: How do you guarantee tolerance and quality?
A: We grind the bore and taper on a CNC internal grinder, then check every part with a bore gauge and a taper ring. Concentricity is verified on a precision mandrel. The inspection report is included with your shipment. If a part is out of spec, we replace it at no cost.
Q: What is your lead time?
A: 7–10 working days for standard materials and heat treatment. If you need 3-day rush, we can do it for an additional 20% expedite fee, subject to material availability.
Q: Can you provide material certificates and heat treatment reports?
A: Yes. We supply mill certs for raw material and a heat treatment report with hardness values and case depth. These are included for every batch, no extra charge.
Send your drawing
Email your PDF or STEP file to sc@bquq.com or WhatsApp +86 13713157787. We reply with a firm quote within 12 hours—including price, lead time, and a review of any critical tolerances. No MOQ, no obligation. If you want a second opinion on your collet design, our engineers will tell you straight if something can be made cheaper or faster. That is precision manufacturing, done the way we have done it for 20 years in Dongguan.