OpeningYour drawing defines the part. We make it exactly to that geometry, then verify every critical dimension before the box leaves our floor. This is not a catalog product. It i
Custom CNC Collet Chuck Precision Auto Lathe Dark Collet Series | BQUQ
OpeningYour drawing defines the part. We make it exactly to that geometry, then verify every critical dimension before the box leaves our floor. This is not a catalog product. It is a custom CNC colle
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
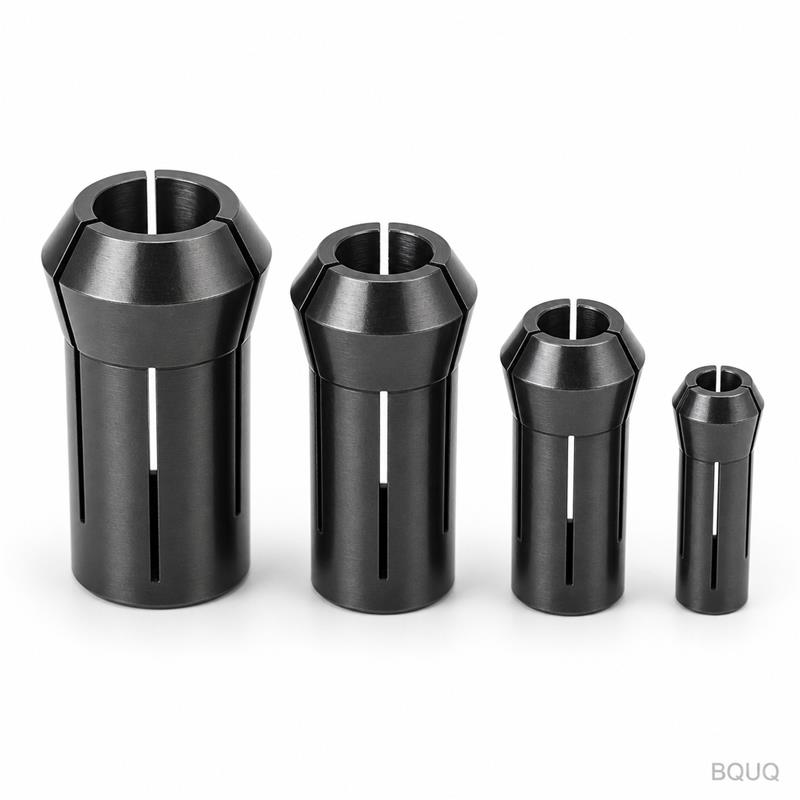
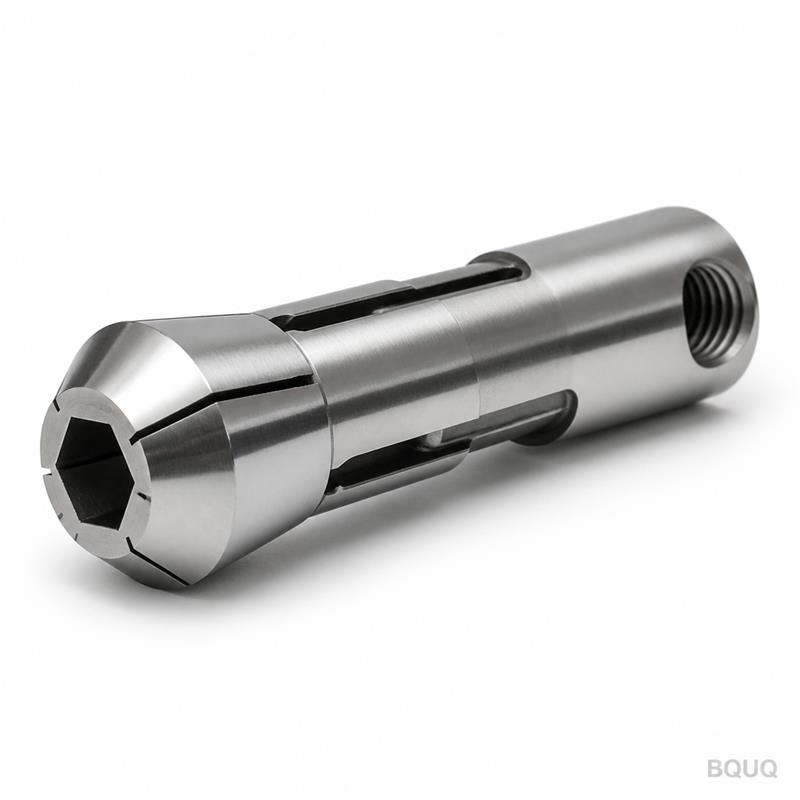
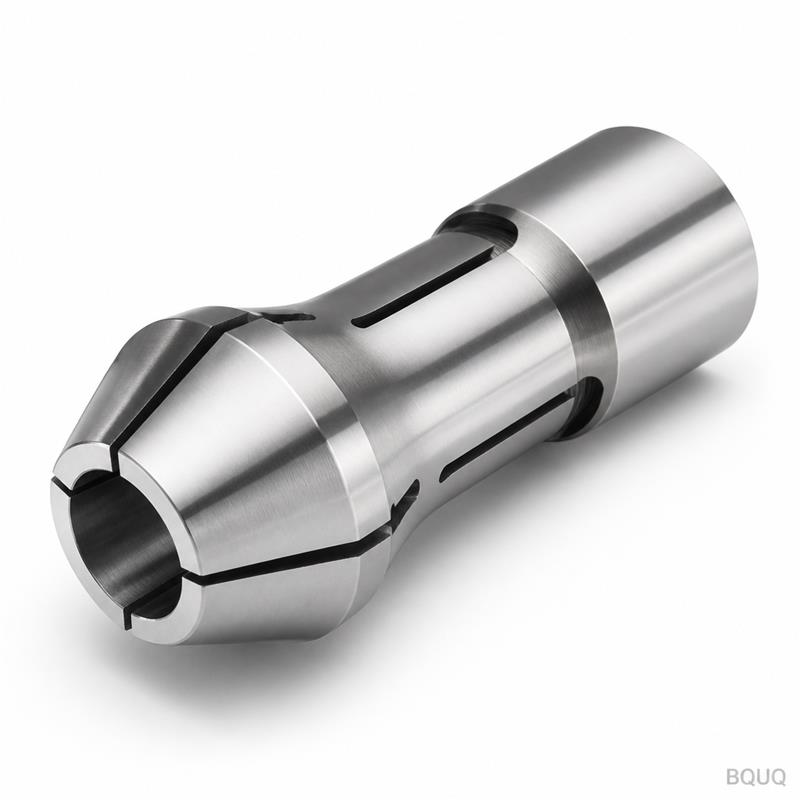
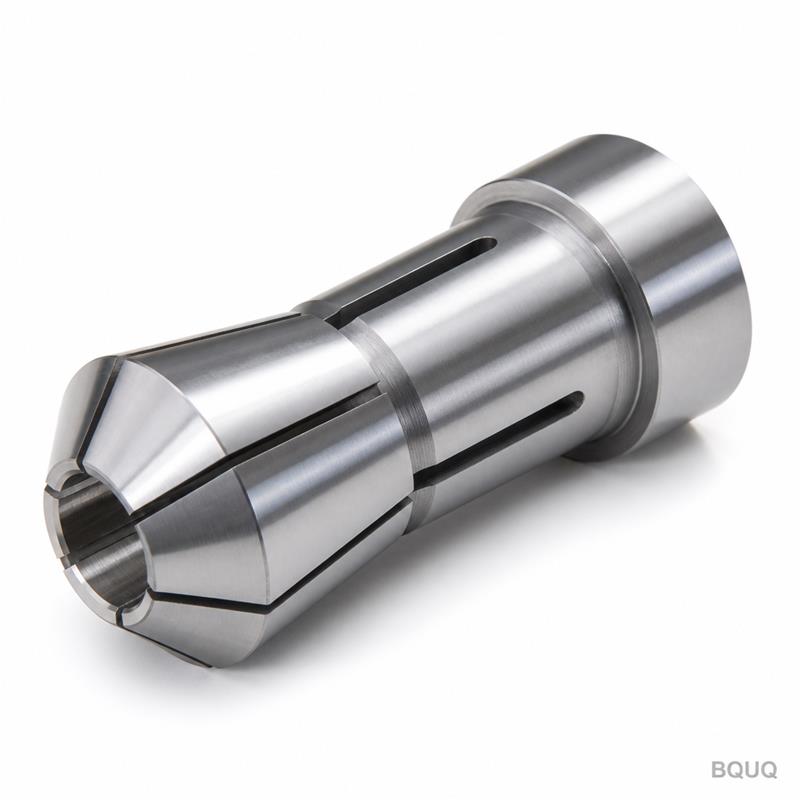
Your drawing defines the part. We make it exactly to that geometry, then verify every critical dimension before the box leaves our floor. This is not a catalog product. It is a custom CNC collet chuck machined from your spec, with a hardened dark oxide finish for wear resistance and chip shedding.
Tolerance: ±0.005 mm on bore and taper
Lead time: 7–12 working days for prototypes, 15–20 days for production runs
No MOQ: order one piece or ten thousand
Material: 65Mn, GCr15, or 20CrMnTi, hardened to HRC 58–62
Finish: quenched dark (black oxide) or as-machined
Inspection: 100% dimensional check, report included per batch
Specifications
Parameter
Value
Material options
65Mn spring steel, GCr15 bearing steel, 20CrMnTi carburizing steel
Hardness
HRC 58–62 (through-hardened or case-hardened)
Tolerance (bore)
±0.005 mm
Tolerance (taper angle)
±0.5 arcmin
Surface finish
Ra 0.4 µm on bore, Ra 0.8 µm on OD
Surface treatment
Quenched dark (black oxide), thickness 1–3 µm
Machining process
CNC Swiss-type auto lathe, then centerless grind
Grinding allowance
0.15–0.25 mm on bore and taper
Roundness
≤0.003 mm
Concentricity (bore to taper)
≤0.005 mm
Batch size
1–50,000 pcs
Inspection equipment
CMM, optical comparator, air gauge
Documentation
Material cert, dimensional report, hardness report
Every collet starts as a precision ground blank. We turn the profile on a CNC auto lathe, then grind the bore and taper on a dedicated internal grinder. The dark oxide layer is applied after hardening, which adds corrosion resistance without changing critical dimensions. For high-volume orders, we use multi-spindle autos to keep cycle times under 30 seconds per piece.
Three reasons buyers send us their drawings
1. Batch-traceable quality.
Each heat of material gets a unique lot number. That lot number follows the steel from the incoming inspection to the final hardness test. If you ever need to trace a failed part back to its raw material, we can show you the exact mill cert and heat treatment curve. No guesswork.
2. Inspection report per batch.
You do not have to ask for quality data. We send it automatically. Every batch ships with a dimensional report covering bore size, taper angle, roundness, and concentricity. Hardness readings from three positions on each sample are included. If you need full 100% inspection with SPC charts, we do that too—just mark it on the PO.
3. One factory for CNC, stamping, springs, and heat sinks.
Your collet chuck does not exist in isolation. It sits in a spindle, often with a spring pusher or a stamped retainer. We make all of those parts under one roof. That means one purchase order, one shipping date, one quality standard. You avoid the headache of coordinating three suppliers who do not talk to each other.
Where these parts are used
Custom CNC collet chucks from this series are specified for high-speed, high-precision workholding in:
Swiss-type lathes for medical bone screws, dental implants, and watch pinions—where runout below 0.005 mm is mandatory.
Automatic bar feeders in fastener production, holding hex, square, and round bar stock from 1 mm to 42 mm diameter.
Grinding spindles for tool holders and guide bushings, where the dark oxide layer prevents galling on the collet OD.
Spring coilers and wire forming machines, where the collet must grip wire without marking the surface.
Heat sink machining lines for electronics, where frequent tool changes demand a collet that holds position after thousands of cycles.
The quenched dark finish is not cosmetic. It reduces friction between the collet and the spindle taper, which prevents seizure during high-speed indexing. It also sheds coolant and chips better than a plain ground surface, extending the life of your spindle nose.
Q: Is there really no MOQ?
A: Yes, no MOQ. We regularly ship single prototype pieces for fit testing. The price per piece is higher for one-off orders because setup and inspection time dominate. But if you send us a drawing, we will quote it honestly—whether you need one piece or fifty thousand.
Q: How do you guarantee tolerance on a custom collet?
A: We machine to your drawing, but we also check the part against the actual spindle taper you specify. If you give us the taper angle and the mating part number, we verify our bore and taper with an air gauge and a CMM. The inspection report shows the measured values, not just a pass/fail stamp.
Q: What is your typical lead time?
A: For a standard material like GCr15 with a dark oxide finish, prototypes ship in 7–12 working days. Production runs of 500+ pieces take 15–20 working days. If you need faster, we can expedite with a 3-day prototype service at a 20% surcharge.
Q: Do you provide material certificates?
A: Yes. Every batch includes a mill certificate for the raw steel, plus our own hardness and chemical composition test results. For aerospace or medical orders, we can provide full traceability documentation with lot numbers and heat treatment records.
Send your drawing
Stop comparing quotes from suppliers who cannot hold a tenth. Send us your part drawing and we will respond with a firm price and lead time within 12 hours. We are a precision manufacturing factory in Dongguan, China, with 20 years of experience in CNC machining, stamping, springs, and heat sinks. Custom CNC collet chucks are our daily work, not a side project.
Email your drawing to sc@bquq.com
WhatsApp: +86 13713157787
We reply within 12 hours, Monday to Saturday, China time.