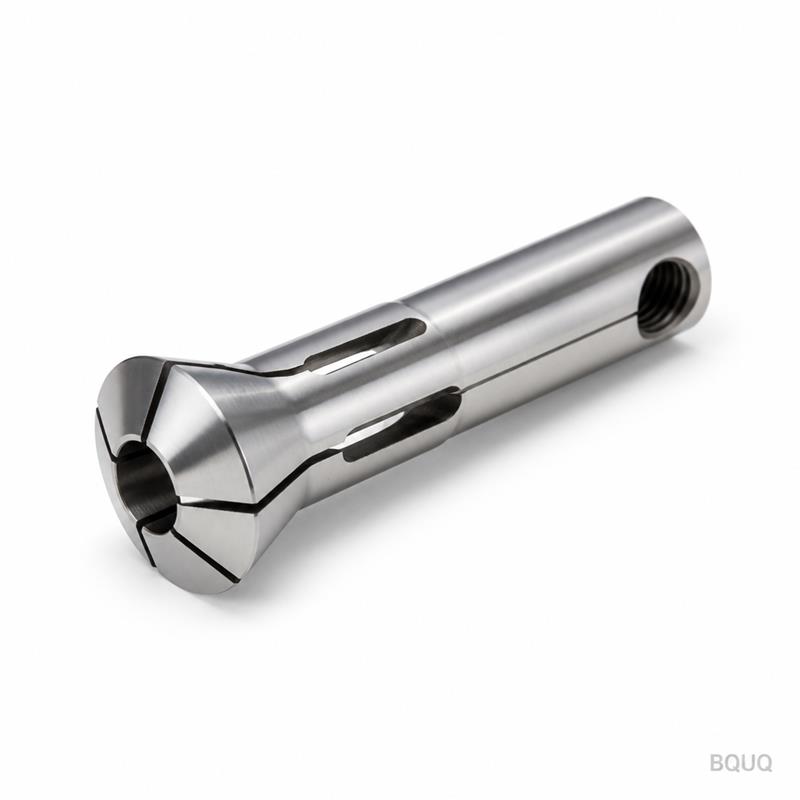
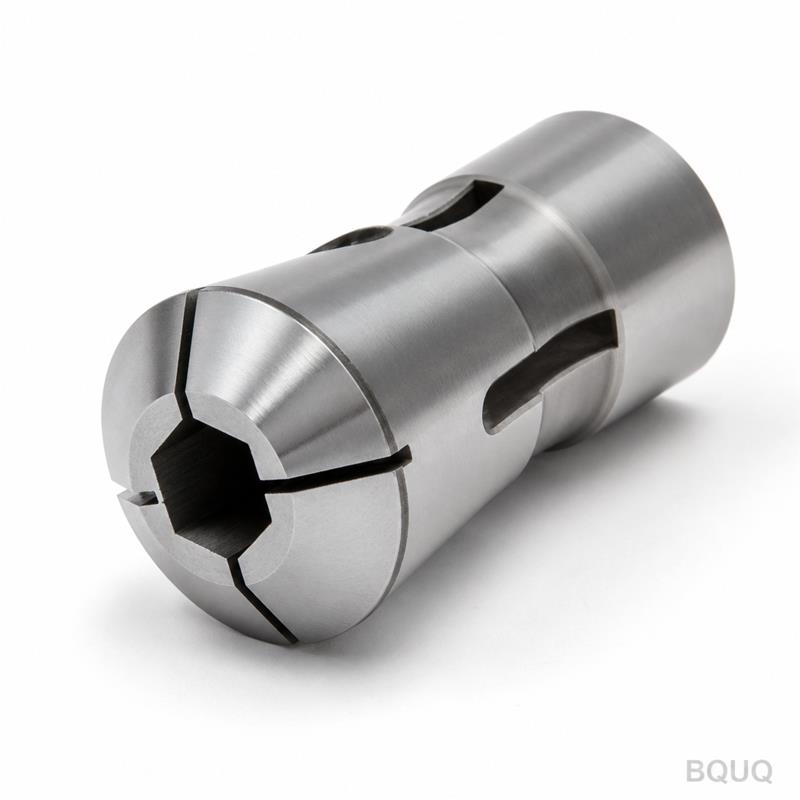
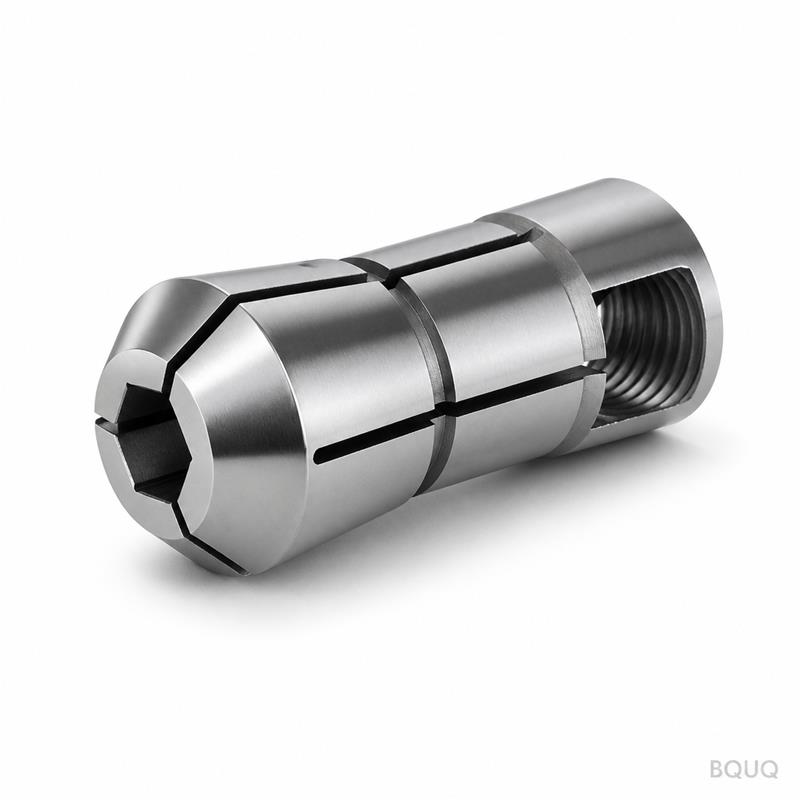
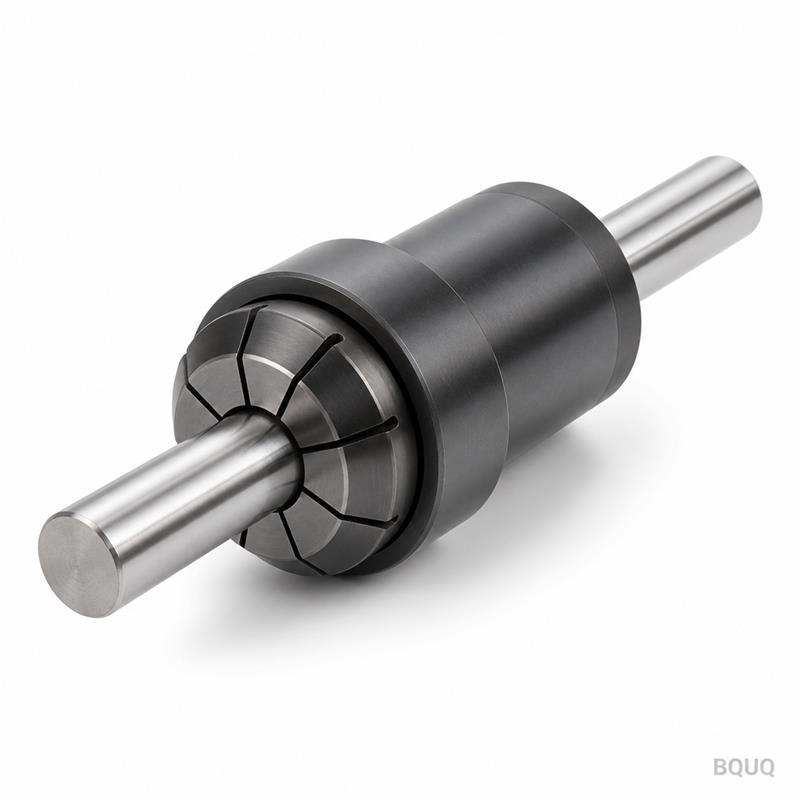
Why This Extended Collet Exists This is a CNC machined Auto Lathe 15 Type Round Bore Extended Collet. It grips long, small-diameter round stock on sliding-head (Swiss-type) auto la
BQUQ CNC Machined Auto Lathe 15 Type Round Bore Extended Collet
Why This Extended Collet Exists This is a CNC machined Auto Lathe 15 Type Round Bore Extended Collet. It grips long, small-diameter round stock on sliding-head (Swiss-type) auto lathes. The extended n
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined Auto Lathe 15 Type Round Bore Extended Collet. It grips long, small-diameter round stock on sliding-head (Swiss-type) auto lathes. The extended nose reaches deep into tight spindle clearances without flexing. You get 0.005 mm total indicated runout (TIR) at the nose, 58 HRC core hardness, and a 5-day production lead time. That means fewer rejected parts, longer tool life, and less downtime on your high-speed machining line.
How the Extended Nose Solves Deep-Reach Gripping
Standard collets stop short. When your workpiece sticks out 40 mm or more, a regular collet loses grip rigidity. This 15 Type Round Bore Extended Collet adds 25 mm of precision-machined extension. The bore stays concentric to the taper within 0.005 mm. You can machine longer components in one pass, eliminating secondary operations and re-chucking errors. Hardinge-compatible thread and taper geometry mean it drops into your existing spindle without modifications.
Materials and Heat Treatment We Use
We start with AISI 4140 alloy steel, pre-treated to 28-32 HRC for machinability. After CNC turning and milling, we through-harden to 56-58 HRC. Then we temper twice to relieve internal stress. The final grind brings the bore to H5 tolerance and surface finish of Ra 0.4 µm. No coatings. No shortcuts. This heat treatment cycle gives you a collet that holds its shape after 100,000+ cycles.
Inspection Before Every Shipment
Every single collet, not a sample batch, goes through a 4-step check. Step 1: bore diameter verified with an air gauge (resolution 0.001 mm). Step 2: TIR measured at the nose and at 25 mm from nose using a 0.5 µm dial indicator. Step 3: hardness test on the taper surface using a Rockwell C tester. Step 4: visual check under 10x magnification for edge burrs or grinding burns. If any parameter fails, the collet is scrapped. We do not rework. You get a test report with each shipment.
Bore Sizes, Tolerances, and Hardness Data
Below are the standard specifications for the CNC Machined Auto Lathe 15 Type Round Bore Extended Collet. Custom bore diameters are available at no extra tooling cost.
Specification
Value
Collet Type
Auto Lathe 15 Type (Hardinge 15-style taper)
Nose Extension Length
25 mm (standard), up to 40 mm on request
Bore Diameter Range
Ø1.0 mm to Ø15.0 mm
Bore Tolerance
H5 (+0.008 / 0 mm for Ø3-6 mm)
Total Indicated Runout (TIR)
0.005 mm max at nose
Surface Finish (bore)
Ra 0.4 µm
Hardness (core)
56-58 HRC
Material
AISI 4140 (equivalent 42CrMo4)
Concentricity (taper to bore)
0.003 mm
Lead Time
5 working days (standard sizes), 10 days (custom bore)
MOQ
No MOQ – order 1 piece or 1000
Inspection Report
Included with every order (CMM + air gauge)
Why Our Heat Treatment Beats Cheap Alternatives
Low-cost collets are case-hardened only to 0.3 mm depth. The soft core flexes under heavy feed rates. Our 4140 is through-hardened to 58 HRC. The hardness is uniform from surface to center. This gives you spring-back resistance and consistent grip force over the full clamping range. For deep cuts on stainless or titanium, this is the difference between holding tolerance and scrapping parts. We also grind the relief behind the bore to prevent stress concentration cracks.
Cost Per Part vs. Cheaper Imports
A $15 collet that fails after 5,000 cycles costs you more than a $45 collet that runs 50,000 cycles. Calculate your real cost: machine rate ($80-120/hr), operator time, scrap parts. Our collet holds 0.005 mm TIR for at least 50,000 cycles under normal coolant conditions (flood or oil mist). We have customers in Germany and Japan running these 24/7 on Citizen and Star machines. They reorder every 2-3 months because the collet outlasts their tooling inserts.
Frequently Asked Questions
What is the minimum order quantity (MOQ)?
There is no MOQ – we ship a single piece to the same quality standard as a bulk order.
Can you make a custom bore diameter for my specific part?
Yes, we can bore to any diameter between 1.0 mm and 15.0 mm in 0.1 mm increments, with no extra tooling charge and only 5 additional days of lead time.
How do you ensure quality control on each collet?
We perform 100% inspection using an air gauge for bore size, a dial indicator for TIR, and a Rockwell tester for hardness, issuing a certified report with every shipment.
What is the typical lead time for a standard collet?
Standard sizes ship in 5 working days from our Dongguan factory, and custom bore sizes ship in 10 working days.
Choosing the Right Collet for Your Machine
Before you order, confirm your spindle taper spec. The Auto Lathe 15 Type matches Hardinge 15-style receivers, common on older BNF, Tsugami, and Star models. If you are unsure about your spindle interface, check our CNC cutting tool selection guide for a breakdown of taper types and grip force calculations. Also review our CNC machining tolerances guide to match bore tolerance to your part’s real requirement – you may not need H5 for every job.
This collet is manufactured in our 20-year-old precision manufacturing facility in Dongguan, China. We operate 32 CNC lathes and 12 grinding machines, all with thermal compensation. Our quality system is ISO 9001:2015 certified. Every order, including single pieces, gets the same inspection protocol.
Ready to cut your runout and scrap rate? Send your drawing or just your bore size and machine model. We will confirm fitment and send a firm quote within 12 hours.
Email: sc@bquq.com WhatsApp: +86 13713157787 Send your drawing today – no MOQ, no minimum order value.