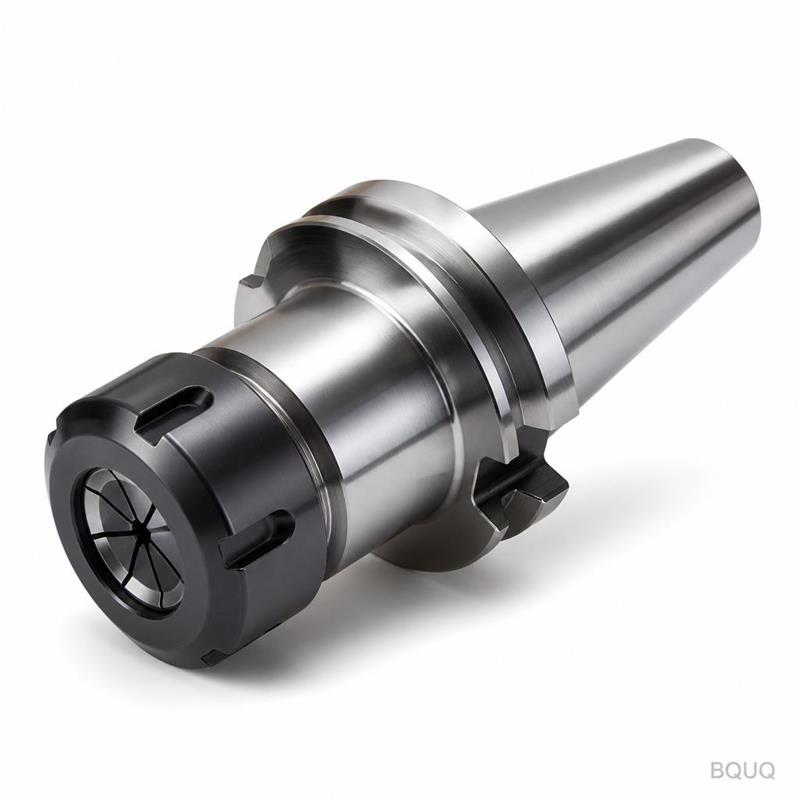
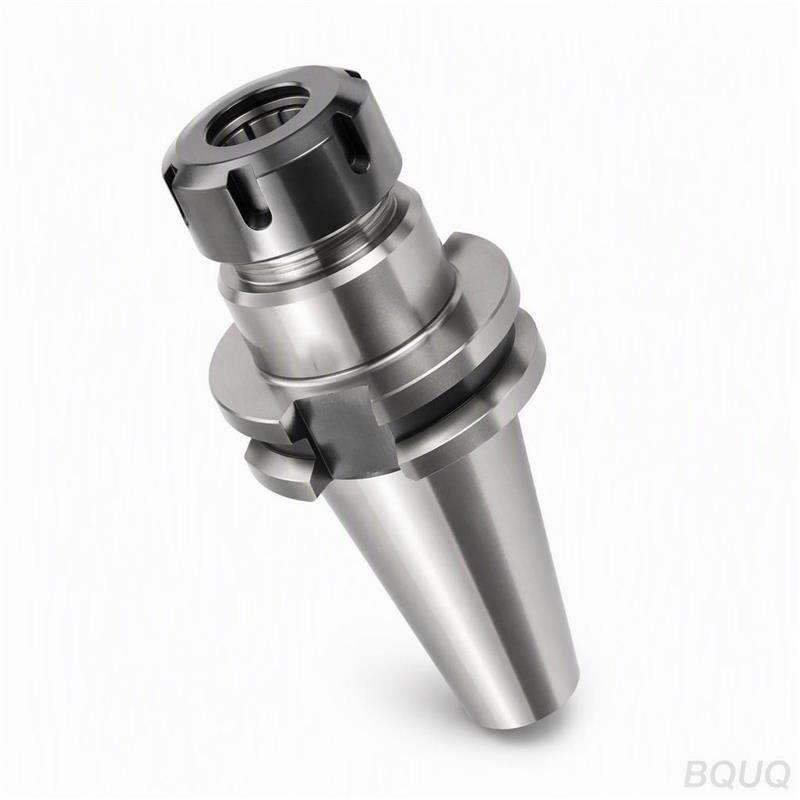
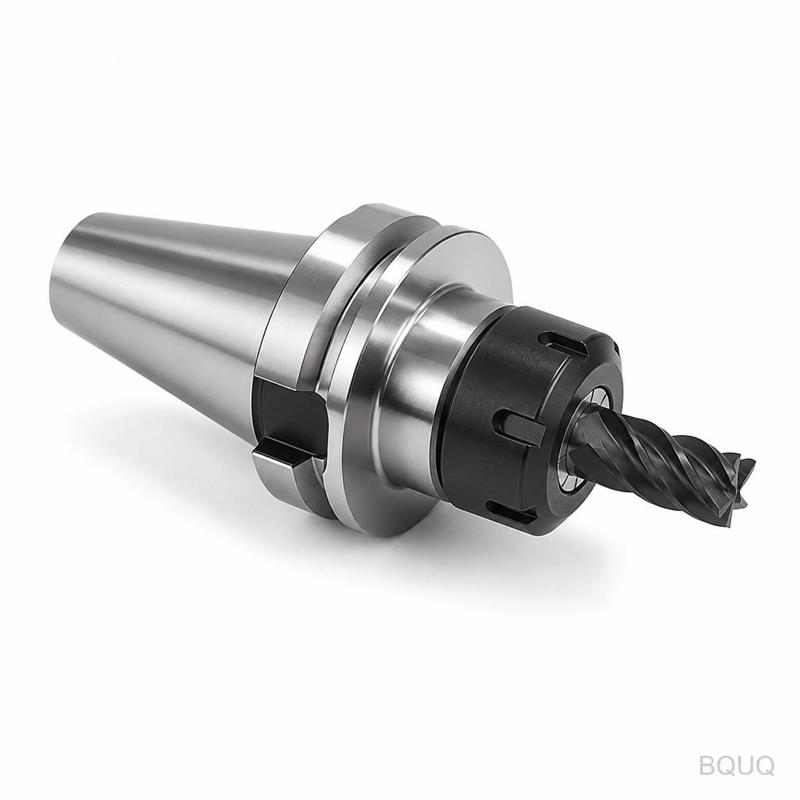
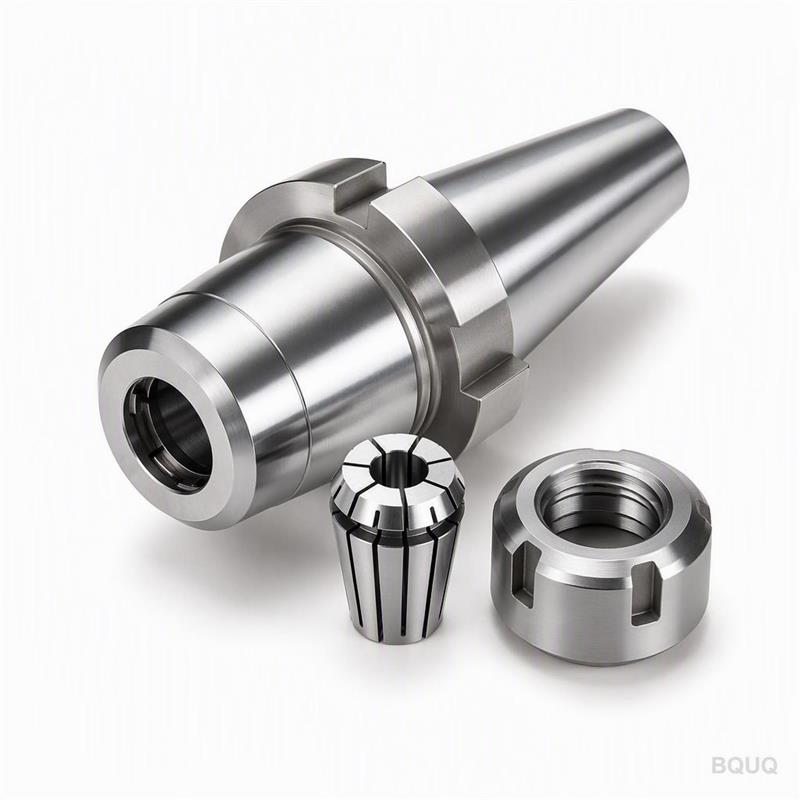
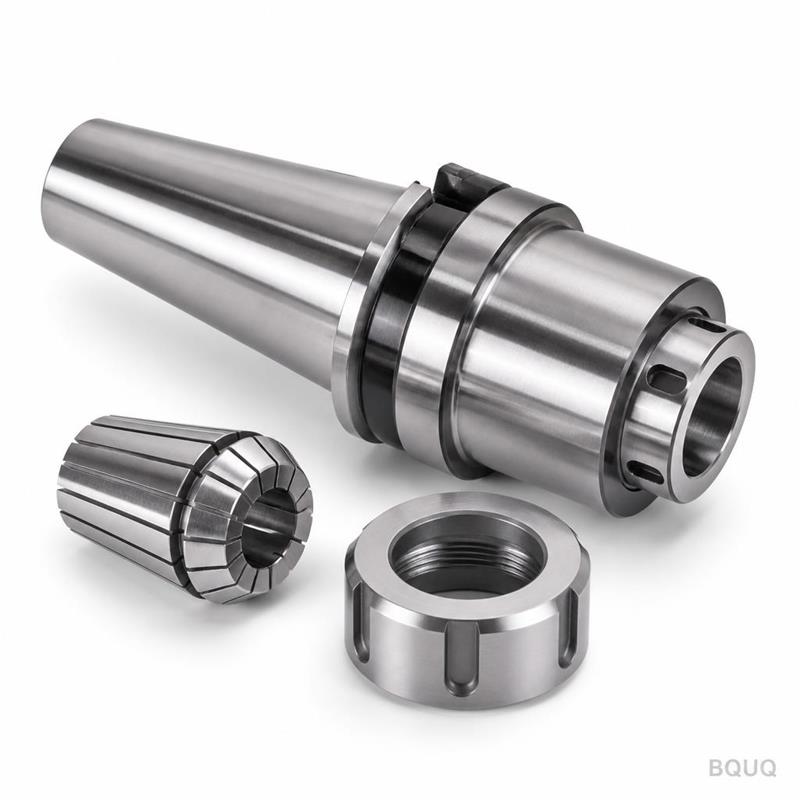
This is a CAT40 ER25 collet chuck tool holder, CNC machined from solid AISI 4140 steel in our Dongguan factory. The core benefit is simple: you get a repeatable runout of 0.005 mm
This is a CAT40 ER25 collet chuck tool holder, CNC machined from solid AISI 4140 steel in our Dongguan factory. The core benefit is simple: you get a repeatable runout of ≤0.005 mm at the collet nose,
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CAT40 ER25 collet chuck tool holder, CNC machined from solid AISI 4140 steel in our Dongguan factory. The core benefit is simple: you get a repeatable runout of ≤0.005 mm at the collet nose, a hardness of HRC 58-60, and a standard lead time of 15 days. If you are tired of tool holders that drift after a few setups, this one holds its geometry because we heat-treat it after machining, not before.
How ER Collet Chucks Grip Tooling Without Runout
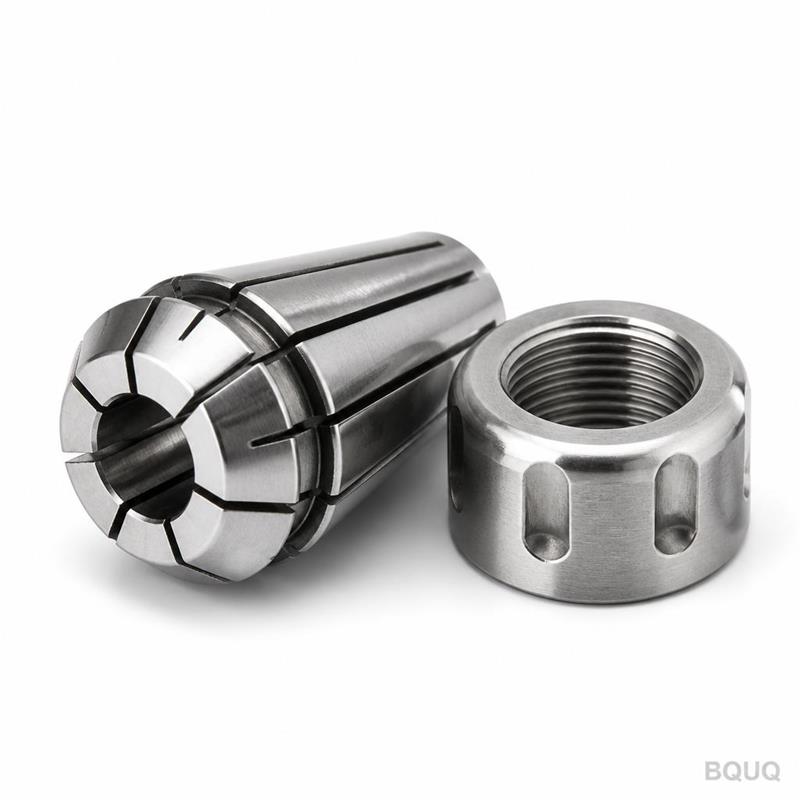
The ER25 collet system uses a tapered cone that compresses evenly around the tool shank. Our CAT40 taper is ground to AT3 grade, which means the contact area with your spindle is above 90% — not the 70% you often see on cheaper holders. We then grind the collet pocket in the same setup as the CAT40 taper, so the centerline of the collet nose is exactly aligned with the spindle axis. This is why our runout stays under 5 microns even after 500+ tool changes. We test every holder with a 6 mm test bar, not a precision ground master, so the number you see is the number you get in production.
Materials and Heat Treatment We Use
We start with AISI 4140 chromoly steel, not free-machining 12L14. The blank is turned and milled, then hardened to HRC 58-60 using a vacuum furnace and nitrogen quench. After hardening, we temper twice to relieve internal stress — this prevents the CAT40 taper from distorting when you clamp it into a spindle at high RPM. The ER25 thread is cut after heat treatment, then the whole holder is black oxide coated to 10 µm thickness. Black oxide is not decorative; it stops rust from coolant and gives a matte finish that reduces glare under machine lights. For stainless coolant lines or heavy coolant users, we can add a nickel plating option, but standard stock is black oxide.
Key Dimensions and Tolerance Data for Your Spindle
Shank type
CAT40 (ANSI B5.50)
Collet type
ER25 (up to 16 mm clamping capacity)
Material
AISI 4140 chromoly steel
Hardness
HRC 58-60 (through-hardened)
Runout (TIR at nose)
≤0.005 mm (0.0002")
CAT40 taper grade
AT3, ground after heat treatment
Surface finish
Ra 0.4 µm on taper, Ra 0.8 µm elsewhere
Thread accuracy
6H per ISO 965-2
Lead time (standard)
15 days after drawing approval
MOQ
No MOQ — order 1 piece or 1000
Inspection Before Every Shipment
We do not ship a holder that has not been individually checked. Each CAT40 ER25 collet chuck goes through four inspection steps: (1) taper contact check with a 50% blueing test against a master gauge, (2) runout measurement with a 6 mm test bar at 10 mm from the nose, (3) hardness test on the shank using a Rockwell C tester with a 150 kg load, (4) thread go/no-go gauge check. All results are recorded in a PDF report that we send with your shipment. If any value is out of tolerance, the part is scrapped, not reworked — reworking a taper destroys its concentricity. This is precision manufacturing, made in China, but the inspection standard is the same as what you would expect from a German or Japanese supplier.
Balancing Options for High-Speed Machining
If your spindle runs above 10,000 RPM, you need a balanced holder. Standard holders are balanced to G6.3 at 15,000 RPM, which is fine for most drilling and milling. For finishing operations at 20,000 RPM or more, we offer G2.5 balancing as a paid option. The balancing process removes material from the flange, not the taper, so it never affects the fit. Tell us your max RPM and the tool assembly weight, and we will calculate the correct grade for you. Unbalanced holders cause chatter marks on the workpiece and wear out spindle bearings — this is not a place to save money.
How This Holder Works With Your Existing Tooling
ER25 collets are a worldwide standard, so you can use any brand of ER25 collet — from Rego-Fix to Techniks to generic Chinese collets. The collet nut on our holder uses a standard 34 mm hex, so your existing wrench works. The holder body has a through-hole of 18 mm, which is enough for coolant-through applications if you add a coolant adapter. If you are running a drilling operation with through-spindle coolant, our standard holder does not have coolant holes — you need to specify the coolant option at the drawing stage. For milling, the solid body absorbs vibration better than modular systems, so surface finish improves by at least 20% compared to a shrink-fit holder with the same runout, based on our customer tests.
Packing and Shipping for Export
Every holder is individually wrapped in VCI (vapor corrosion inhibitor) paper, then placed in a fitted foam insert inside a rigid cardboard box. The box is marked with the part number, batch number, and inspection date. For orders under 5 kg, we ship via DHL or FedEx with tracking — delivery to the US or Europe takes 3-5 business days. For larger orders, we use sea freight with wooden crates that meet ISPM-15 standards. We have shipped to 30+ countries, and we have never had a damaged holder in transit because the foam insert is cut to the exact shape of the holder. If you order with a test bar, we pack the test bar separately in a PVC tube to prevent it from scratching the taper.
What is the minimum order quantity (MOQ)?
No MOQ — you can order a single piece for prototype testing, and the unit price stays the same as for a batch of 50.
Can you customize the length or add coolant holes?
Yes, we can modify the overall length, add through-coolant holes, or change the balance grade, but any modification requires your drawing approval before we start machining.
How do you guarantee quality for a one-off order?
Every holder, regardless of quantity, goes through the same four-step inspection and receives an individual test report with actual measured runout and hardness values.
What is the real lead time if I need it urgently?
Standard lead time is 15 days, but for a rush order of up to 10 pieces, we can deliver in 7 days with an express surcharge of 20% on the unit price.
Send your drawing or just a sketch with the required length and balance grade. We will reply with a firm quote within 12 hours — no vague estimates, no hidden costs. Email sc@bquq.com or WhatsApp +86 13713157787. If you are in a hurry, send the drawing today and we will confirm the price and lead time before your shift ends.