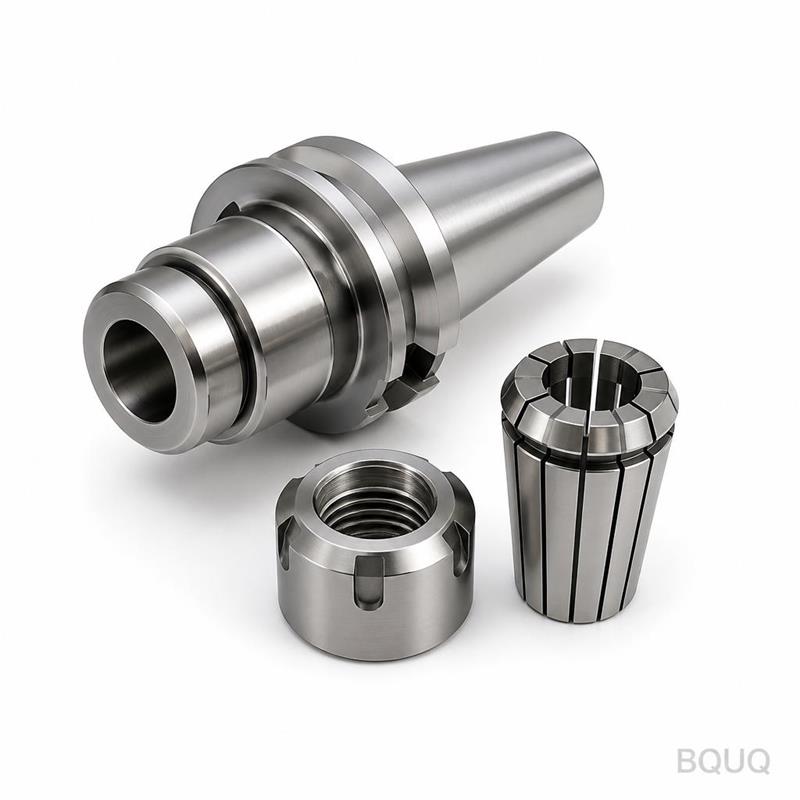
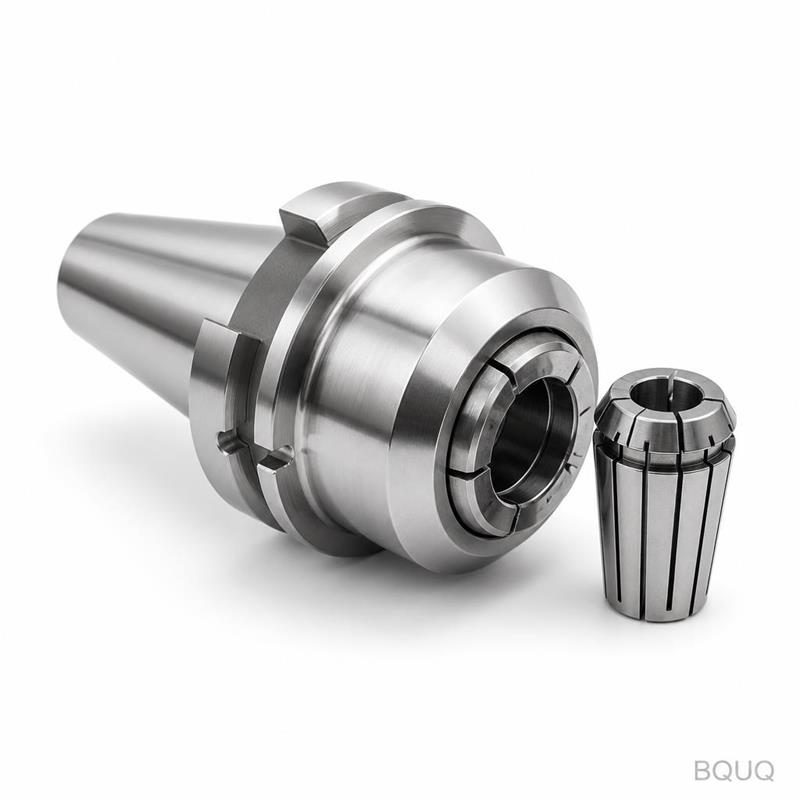
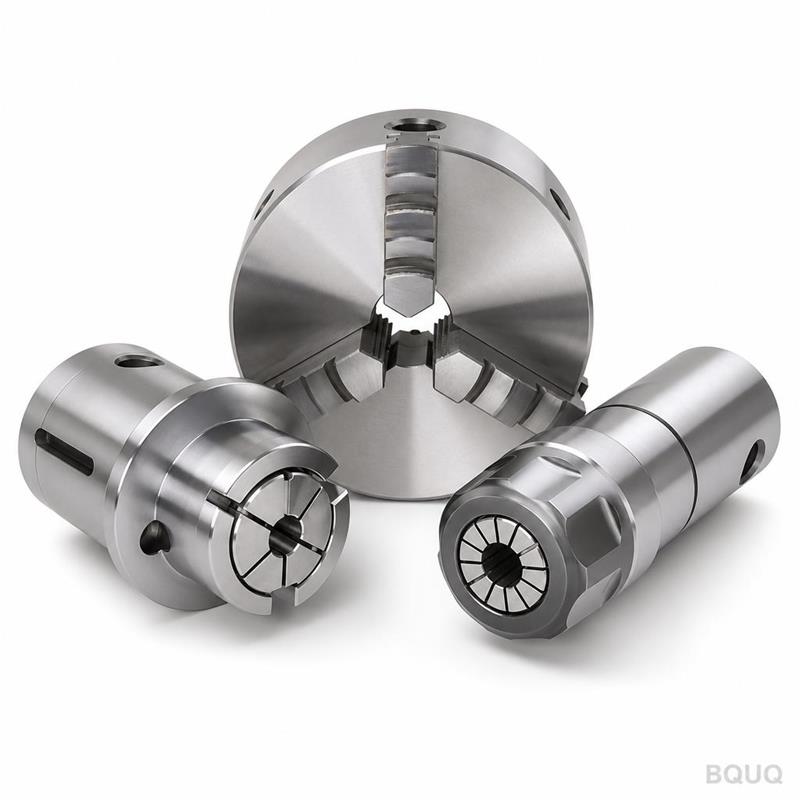
What This DA Collet Chuck Delivers in Real Numbers This is a CNC machined DA collet chuck with a matching collet nut, manufactured to DIN6388 for ER-style tool clamping. You get
What This DA Collet Chuck Delivers in Real Numbers This is a CNC machined DA collet chuck with a matching collet nut, manufactured to DIN6388 for ER-style tool clamping. You get a guaranteed runout
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This DA Collet Chuck Delivers in Real Numbers
This is a CNC machined DA collet chuck with a matching collet nut, manufactured to DIN6388 for ER-style tool clamping. You get a guaranteed runout of ≤0.005 mm at the nose, a hardness of 58–62 HRC on the gripping surfaces, and a surface finish of Ra 0.4 µm on the taper. Lead time is 15 days for standard sizes, and we ship from our Dongguan factory with no MOQ. This is precision manufacturing made in China, but with inspection reports you can trust.
How the DA Collet System Grips Without Introducing Runout
The DA collet chuck uses a 8-degree taper angle (per DIN6388) that collapses the collet evenly around the tool shank. Unlike cheap chucks where the nut deforms the collet unevenly, our collet nut is machined with a precision-ground thread (class 6H) and a hardened thrust face. This distributes clamping force radially, keeping the tool centerline within 0.005 mm of the spindle axis. You will not see the “wobble” common in generic collet chucks when you tighten the nut past 30 Nm.
Materials and Heat Treatment We Use for Long-Term Rigidity
The chuck body is made from 20CrMnTi (case-hardening steel), carburized to a depth of 0.8–1.2 mm, then hardened to 58–62 HRC. The collet nut is made from 40CrMo, quenched and tempered to 45–50 HRC, then nitrided to 900 HV on the thread flanks. This combination resists wear from repeated tool changes and prevents thread galling, a common failure point on DIN6388 nuts. We do not use 1214 free-cutting steel or any low-cost substitute that sacrifices rigidity.
Inspection Before Every Shipment: Not Just a Paper Certificate
Every DA collet chuck and collet nut is 100% inspected, not sampled. We use a CMM (coordinate measuring machine) to verify the 8° taper angle, a laser micrometer for the bore concentricity, and a Rockwell tester for hardness on three points. Runout is checked with a dial indicator at 50 mm from the nose. You receive a digital inspection report with serial numbers matching your parts. If any dimension is outside tolerance, the part is scrapped—not reworked.
DIN6388 Compliance and Interchangeability With Your Existing Tooling
DIN6388 defines the critical dimensions: the collet taper, nut thread (M20x1.0 for DA-100 series, M25x1.5 for DA-200), and the collet slot width. Our chucks and nuts are made to these exact standards, so they fit any standard DA collet from brands like Rego-Fix, Techniks, or Lyndex. The thread is cut with a CNC lathe using a single-point insert, achieving a pitch error of less than 0.01 mm over the full thread length. You can mix our nut with another brand’s chuck—but you won’t need to.
Sizes, Tolerances, and Surface Finish—What You Can Specify
We keep a stock of 20CrMnTi blanks and 40CrMo bar stock in our Dongguan warehouse. For standard DA sizes (100, 200, 300), we start machining the day you place the order. CNC lathe cycle time is 12 minutes per chuck body, 8 minutes per nut. Heat treatment takes 48 hours in our in-house vacuum furnace—no outsourcing delays. Inspection adds 2 hours. Total process: 15 days door-to-door, including surface finishing and packaging. For prototype orders (1–5 pieces), we can ship in 7 days by air.
Customizing the Collet Nut for Non-Standard Tool Holders
If your spindle has a non-standard thread or you need a longer nut for reach, we can modify the nut’s outer diameter, length, or thread. We have cut custom nuts with hex flats for torque wrenches, with through-holes for coolant, and with extended noses for deep pocket milling. The minimum order for a custom nut is 10 pieces, but the tooling charge is zero if you accept our standard blank. Send your drawing—we will reply with a DFM (design for manufacturability) comment within 24 hours.
What is the minimum order quantity (MOQ) for this DA collet chuck?
No MOQ—you can order a single DA-100 collet chuck with one nut, and we will treat it with the same inspection rigor as a 1,000-piece order.
Can you customize the collet nut for a non-standard thread or length?
Yes, we can modify the thread class, outer diameter, length, and add features like coolant holes or torque flats, with a 10-piece minimum and free DFM feedback.
How do you ensure the runout stays under 0.005 mm after heat treatment?
We grind the taper and bore after heat treatment using a CNC internal grinder, and then verify with a laser micrometer on a 50 mm gauge arbor—every part, not a sample.
What is the typical lead time for a custom DA collet chuck order?
Standard sizes ship in 15 days; custom nuts with new thread profiles take 20 days because we add one extra inspection step for thread pitch accuracy.
Request a Firm Quote With Inspection Data—Within 12 Hours
Send your drawing or just the DA series and shank size. We will reply within 12 hours with a firm unit price, lead time, and a sample inspection report from a similar part we have shipped. Email sc@bquq.com or WhatsApp +86 13713157787. No MOQ, no negotiation games—just precision manufacturing with numbers you can verify. For more context on tool selection, read our CNC cutting tool selection guide. If you are pushing tolerances beyond 0.005 mm, check our CNC machining tolerances guide to see what we can hold on your specific geometry.