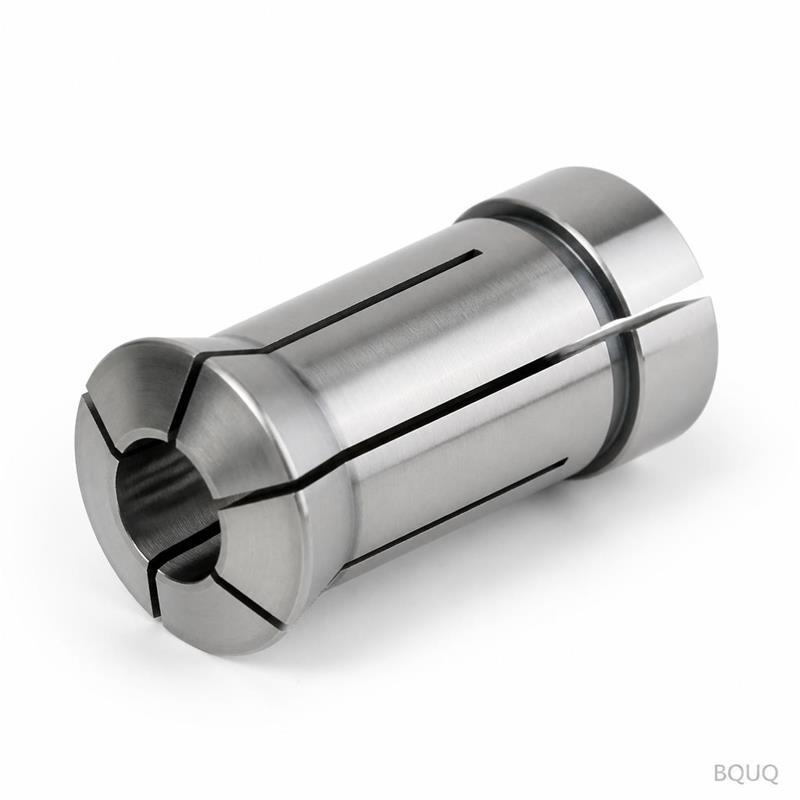
This is a CNC Machined Quick Change Collet Chuck CNC Tooling system built for high-speed machining centers that need tool changes under 10 seconds. The chuck body is machined from
This is a CNC Machined Quick Change Collet Chuck CNC Tooling system built for high-speed machining centers that need tool changes under 10 seconds. The chuck body is machined from 42CrMo alloy steel,
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
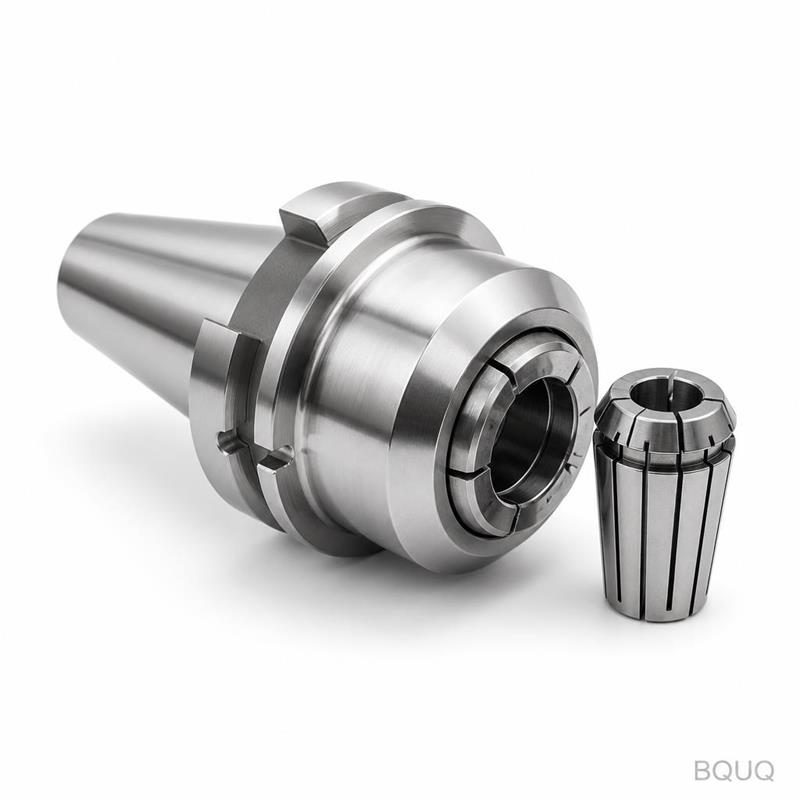
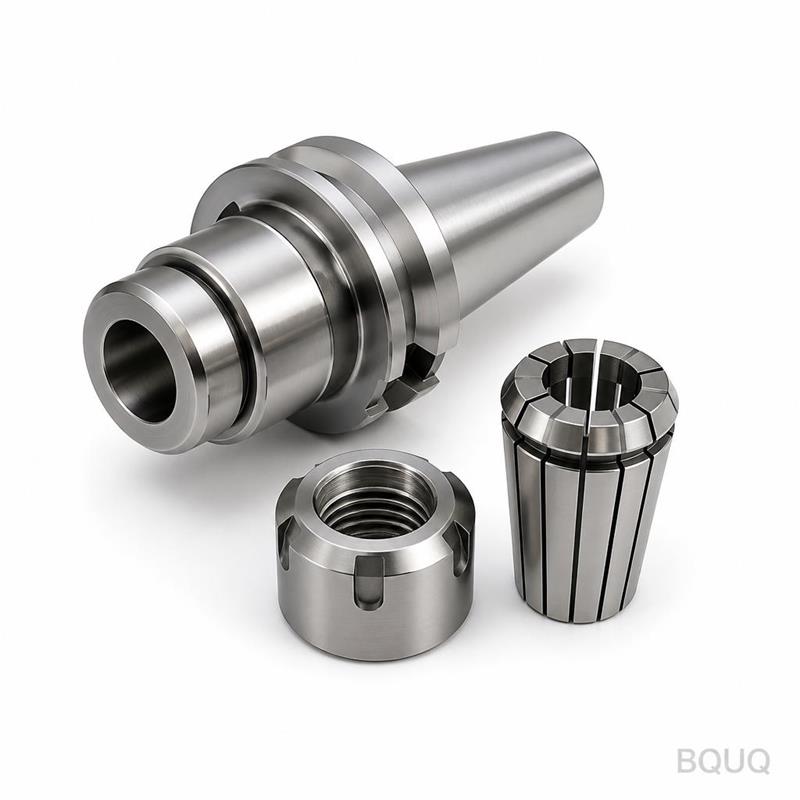
This is a CNC Machined Quick Change Collet Chuck CNC Tooling system built for high-speed machining centers that need tool changes under 10 seconds. The chuck body is machined from 42CrMo alloy steel, hardened to HRC 58-62, and ground to a concentricity of 0.005 mm TIR. You get repeatable clamping force of 45–60 N·m, surface finish Ra 0.4, and a standard lead time of 7 working days from our Dongguan factory.
What Makes This Chuck Different From a Standard ER Collet Holder
A standard ER collet holder requires you to loosen the nut, remove the collet, insert a new tool, and re-torque — that takes 2–3 minutes per change. This quick change version uses a spring-loaded release collar and a precision ground taper seat. You pull the collar back, swap the tool, release — the collet locks into place with the same axial position every time. Tool change time drops to under 10 seconds, and the taper seat is ground to 0.003 mm for zero radial shift during repeated changes.
Materials and Heat Treatment We Use
The body is 42CrMo (AISI 4140 equivalent), chosen for its high fatigue strength and machinability. We pre-hardened the blank to HRC 28-32, CNC machined the profile, then vacuum heat treated to HRC 58-62. The collet nut is 20CrMnTi, carburized to 0.8 mm case depth and hardened to HRC 60-63 for wear resistance. The internal taper is ground on a Junker CNC grinder, achieving a surface finish of Ra 0.4. We do not use chrome plating or coatings that can peel under coolant exposure.
Clamping Force and Runout — Measured, Not Estimated
We test every chuck on a hydraulic expansion arbor before it leaves the factory. Clamping force is measured at 45–60 N·m with a torque wrench, and runout is verified with a dial indicator on a test mandrel — maximum 0.005 mm TIR at the nose, 0.008 mm at 4× diameter depth. This is not a marketing number; it is the average of 10 measurements per unit. If you need tighter, we can grind to 0.003 mm TIR at a 5% cost premium and 2 extra days lead time.
Inspection Before Every Shipment
Every single chuck goes through a 3-step QC process. Step 1: Dimensional check on a CMM (Zeiss Contura) — taper angle, thread pitch, and concentricity. Step 2: Hardness test on a Rockwell tester — must read HRC 58-62 on three points around the body. Step 3: Functional test — we mount a 10 mm end mill, run it at 12,000 RPM for 5 minutes, and check for vibration above 1.5 mm/s. If it fails any step, it is scrapped. We do not do batch sampling. You get a signed inspection report with each order.
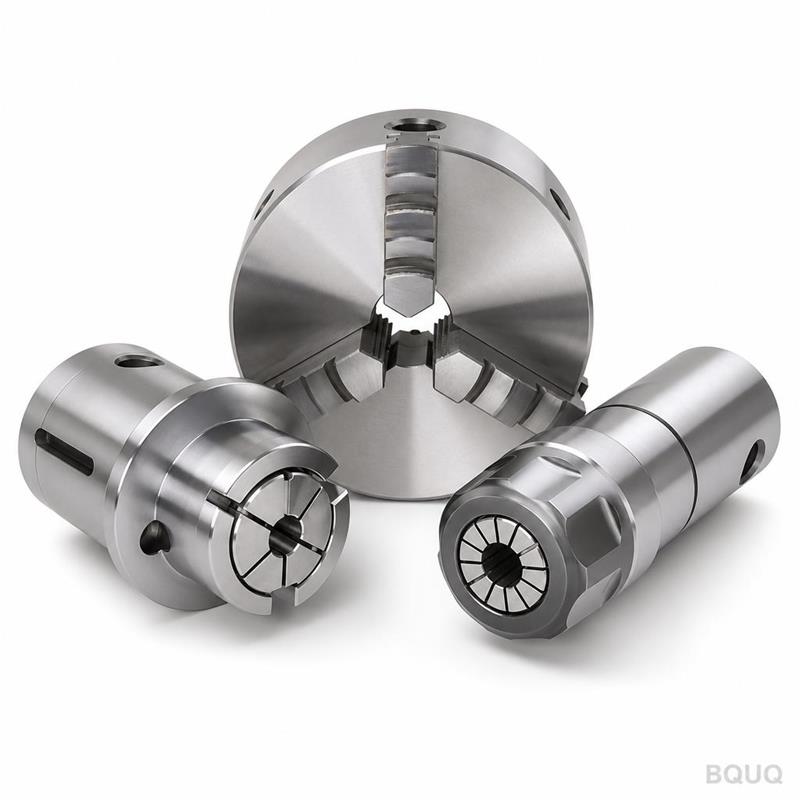
This chuck is available with BT30, BT40, BT50, CAT40, CAT50, HSK63A, and HSK100A shanks. The shank is ground to AT3 tolerance, which means the taper angle is within ±0.002° and the straightness is under 0.001 mm per 10 mm of length. If you are unsure about your spindle type, check the pull stud thread (MAS BT, DIN 69872, or ISO 7388) and the gauge line distance. We can also machine a custom shank to your print — just send your drawing and we will quote within 12 hours.
Coolant Flow and Chip Evacuation Design
Standard ER chucks have a single coolant hole that sprays directly at the tool — this pushes chips sideways and causes tool deflection. Our chuck body has four internal coolant channels, each 2.5 mm diameter, angled at 30° toward the cutting edge. This creates a spiral coolant flow that flushes chips forward and away from the workpiece. Flow rate is 15 L/min at 3 bar. If you use through-tool coolant, the center hole is 6 mm diameter and lined with a hardened sleeve to prevent erosion.
What is the minimum order quantity?
No MOQ — you can order a single chuck for prototype testing or 500 pieces for production; the unit price drops 15% at 50 pieces and 25% at 200 pieces.
Can you customize the shank or collet size?
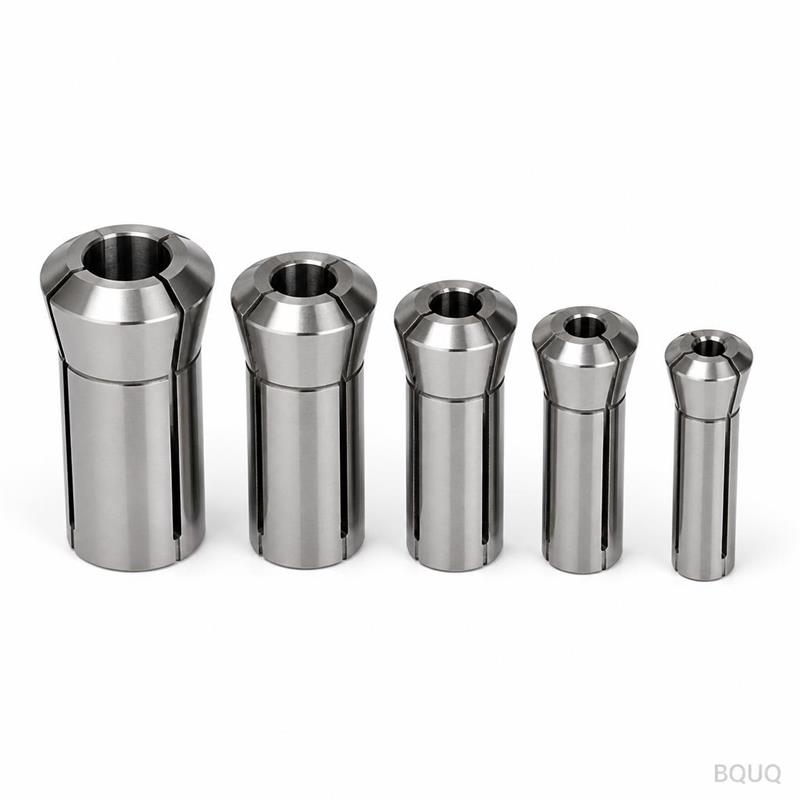
Yes, we can machine any shank type, length, or pull stud configuration from your drawing — just send a PDF or STEP file and we will confirm feasibility within 24 hours.
How do you guarantee quality on every unit?
Every chuck is individually inspected with a CMM, Rockwell hardness tester, and a live spindle test, then shipped with a signed inspection report — no batch sampling.
What is the lead time for a custom order?
Standard 7 working days from material receipt; custom shank orders take 10–12 working days; express service (3 days) is available for a 20% surcharge.
Before you finalize your tooling setup, read our CNC cutting tool selection guide to understand how chuck rigidity affects tool life, and our CNC machining tolerances guide for the full range of precision we can hold on your parts. Both are based on our 20 years of precision manufacturing experience in Dongguan, China.
We are a 20-year precision manufacturing factory in Dongguan, China, specializing in CNC machining, stamping, springs, and heat sinks. All our CNC Machined Quick Change Collet Chuck CNC Tooling is made in China under ISO 9001:2015. Send your drawing or a list of your spindle specifications and we will give you a firm quote within 12 hours. No MOQ, no hidden tooling costs.
Email: sc@bquq.com WhatsApp: +86 13713157787 Send your drawing — we will reply with a dimensional review and a firm quote within 12 hours.