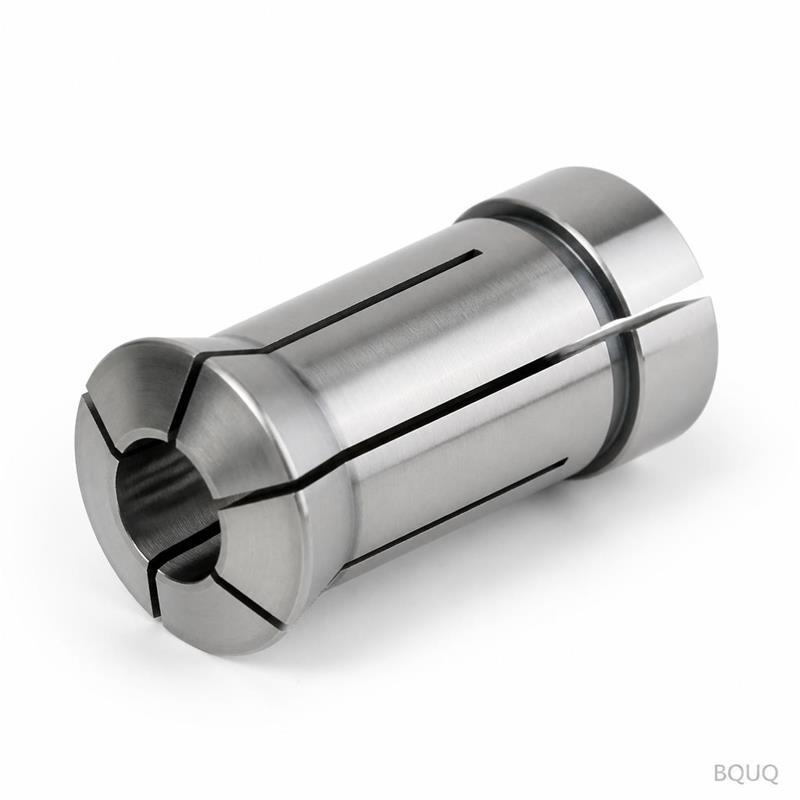
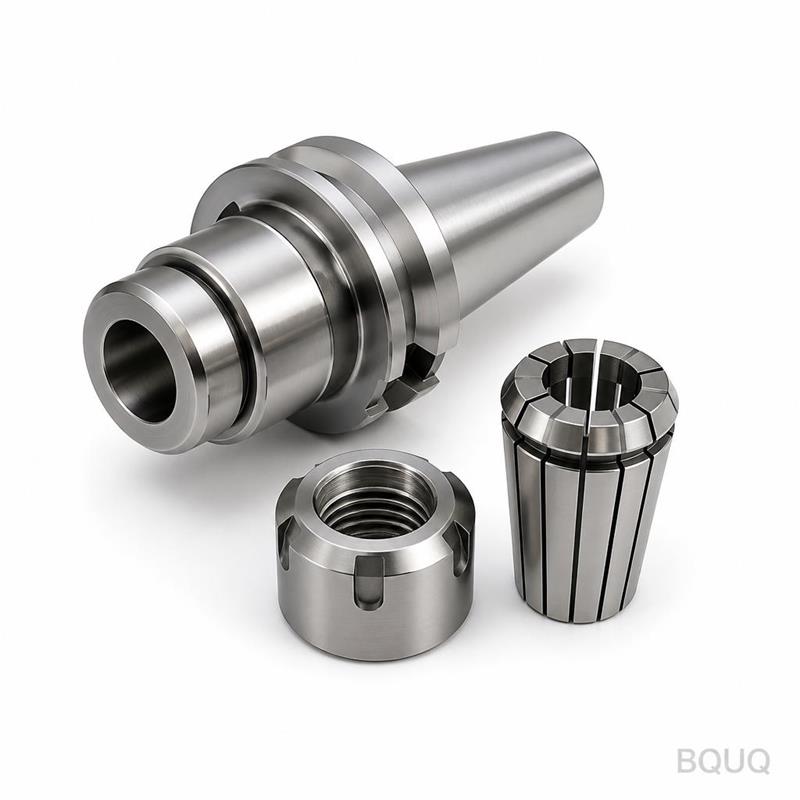
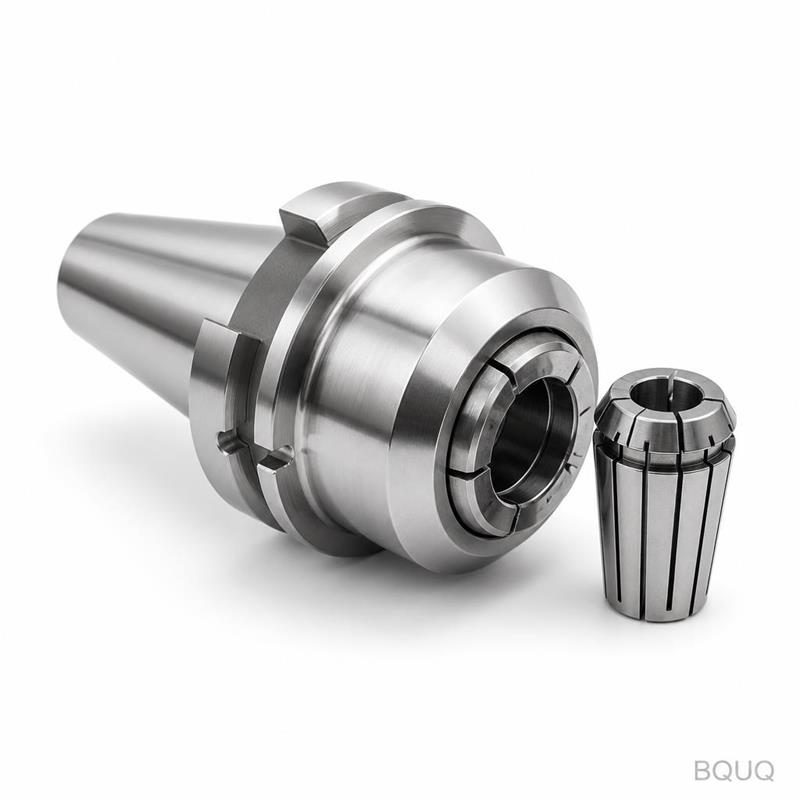
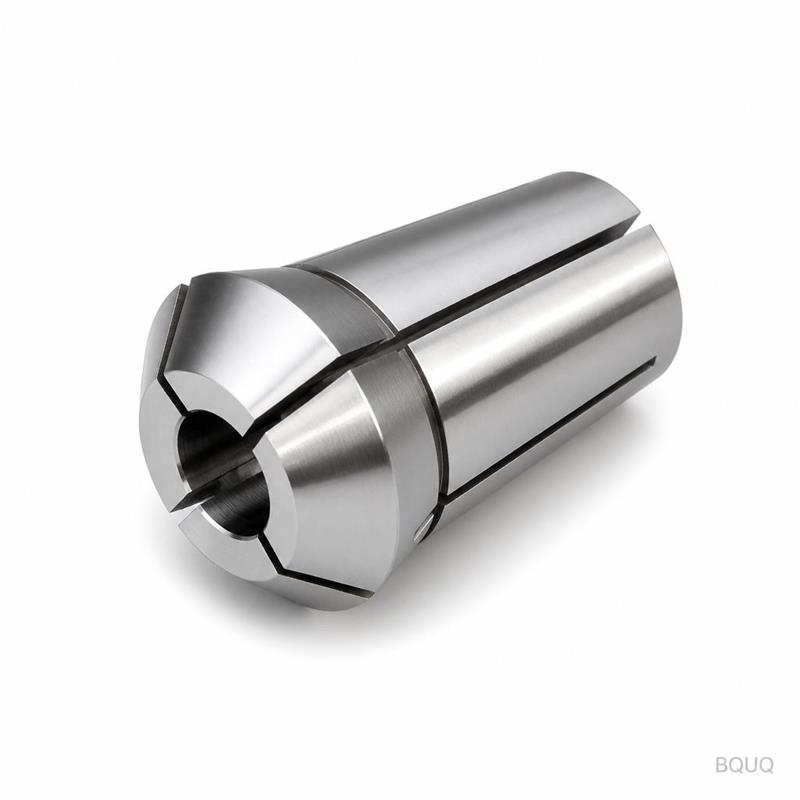
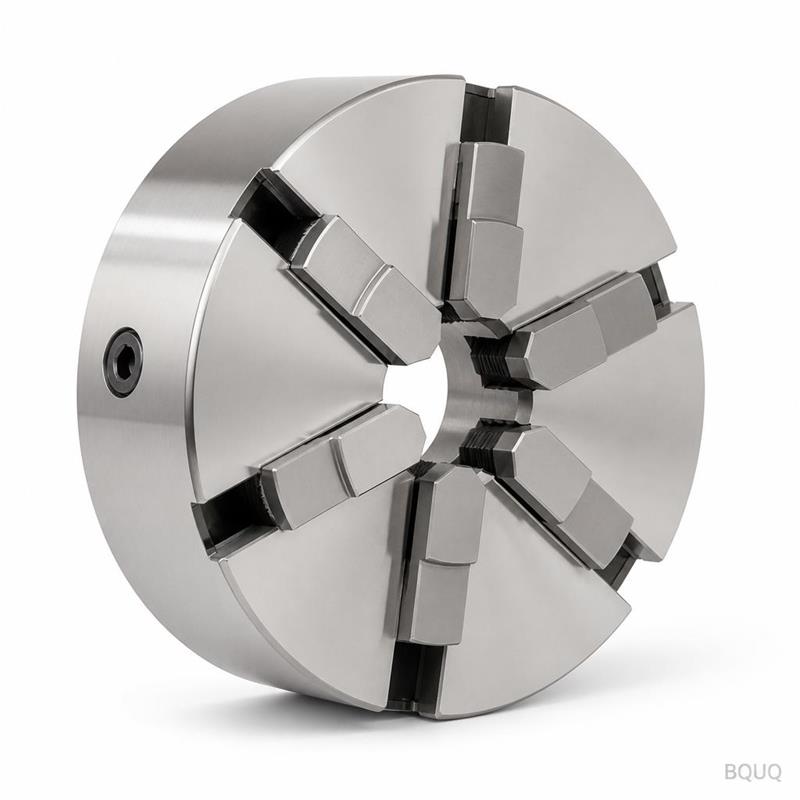
This is a W20 Schaublin collet chuck, machined from hardened alloy steel, engineered for toolholding in Swiss-type lathes and precision CNC spindles. You get a guaranteed 0.003 mm
BQUQ CNC Machined W20 Schaublin Collet Precision Tooling | Made in China
This is a W20 Schaublin collet chuck, machined from hardened alloy steel, engineered for toolholding in Swiss-type lathes and precision CNC spindles. You get a guaranteed 0.003 mm TIR (total indicated
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a W20 Schaublin collet chuck, machined from hardened alloy steel, engineered for toolholding in Swiss-type lathes and precision CNC spindles. You get a guaranteed 0.003 mm TIR (total indicated runout) at the nose, 58-62 HRC hardness, and a 15-day lead time for standard sizes. We are BQUQ, a precision manufacturing factory in Dongguan, China, with 20 years of CNC machining, stamping, and heat-treatment experience.
How a W20 Profile Grips Shank Tools Without Deformation
The W20 collet uses a 20 mm thread and a tapered outer cone that collapses evenly around the tool shank. Unlike ER collets, which use a slotted cylindrical grip, the Schaublin W20 design applies a continuous 360-degree radial force. This eliminates the three-point pressure marks that cause micro-deflection in small-diameter end mills and drills. For a 6 mm shank, we hold roundness within 0.002 mm after closure. The result is a rigid grip that maintains tool position under a 12,000 RPM spindle load.
Our collet chuck body is machined from 8620 carburizing steel, then case-hardened to 58-62 HRC. The taper seat is ground, not turned, to a 12-degree included angle with a 0.4 µm Ra finish. This grind ensures the collet seats fully, without rocking, which is the primary cause of runout in cheap imported chucks. You will not need to re-tighten after a 200-part run.
Materials and Heat Treatment We Use for the Collet Chuck Body
We offer the body in two grades: standard 8620 carburized steel and optional 440C stainless for washdown environments. The 8620 version gets a 0.8 mm case depth, giving a wear-resistant surface while retaining a tough core for shock absorption. The 440C version is through-hardened to 56 HRC and passivated for corrosion resistance.
All threads are cut with a single-point insert, then wire-EDM finished to a 2A class fit. The thread flank angle is verified with a Zeiss profile projector, not a go/no-go gauge. This matters because a loose thread on the drawbar will let the collet pull out under heavy cuts, ruining your part and the tool holder.
Runout and Taper Tolerance: What We Measure Before Shipping
We measure three critical dimensions on every unit: the internal taper angle, the front face squareness, and the thread pitch diameter. The taper is checked with a precision air gauge, which reads to 0.0005 mm. We allow a maximum taper deviation of ±0.002 mm from the theoretical 12 degrees. The front face is ground square to the bore within 0.005 mm over the full diameter. This prevents side load on the tool, which is what causes chatter marks on your finished part.
Each chuck is assembled with a test collet and a 10 mm calibration bar. We measure runout at two points: 10 mm from the nose and 50 mm from the nose. The maximum acceptable reading is 0.003 mm TIR at both points. If a unit exceeds this, it is rejected, not adjusted. We do not ship "good enough" tooling.
Inspection Before Every Shipment: Air Gauges and CMM Reports
Every single collet chuck, not a sample batch, goes through a 12-point inspection. We use a Zeiss CMM for the taper angle and bore concentricity, which gives a measurement uncertainty of ±0.001 mm. The surface finish is checked with a Mitutoyo profilometer, and the hardness is verified with a Rockwell tester on the nose and the shank. The inspection report is included in the box, with the serial number matching your drawing.
We keep the raw material certificates (EN 10204 3.1) for each heat lot for 10 years. If you have a field failure, we can trace the exact batch of steel back to the mill. This is what precision manufacturing "made in China" should mean — not just cheap parts, but traceable, verifiable quality.
Standard Sizes, Custom Shank Lengths, and No MOQ
Product type
W20 Schaublin collet chuck (CNC tooling)
Available shank diameters
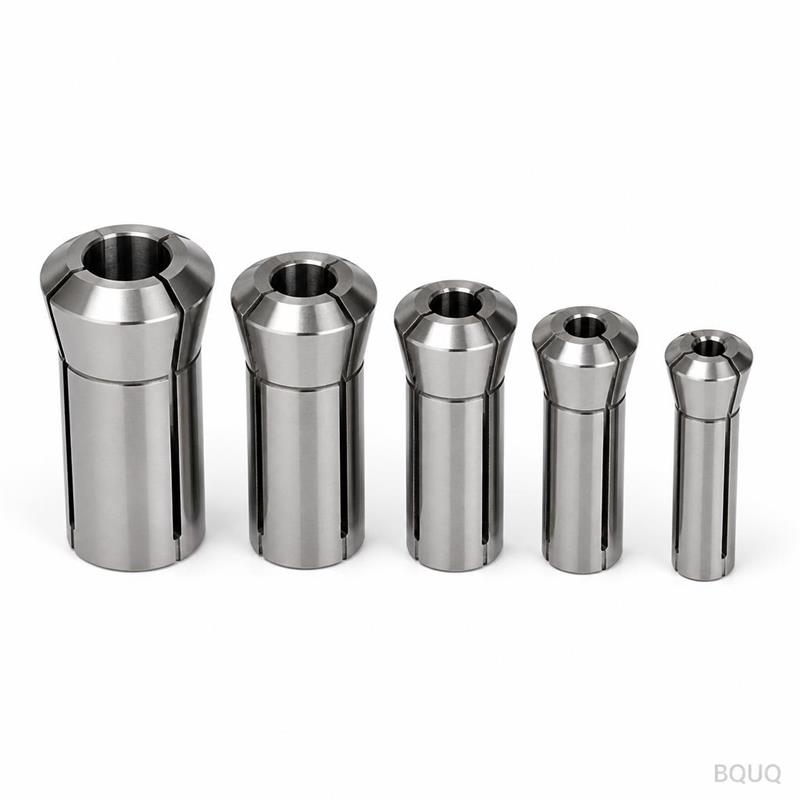
6 mm, 8 mm, 10 mm, 12 mm, 16 mm, 20 mm
Collet thread size
W20 (20 mm x 1.0 mm pitch)
Body material
8620 carburized steel or 440C stainless
Hardness
58-62 HRC (8620 case-hardened) / 56 HRC (440C)
Case depth (8620)
0.8 mm ± 0.1 mm
Taper angle
12 degrees included, ±0.002 mm deviation
Runout (TIR)
≤ 0.003 mm at 10 mm and 50 mm from nose
Surface finish (taper seat)
Ra 0.4 µm (ground)
Lead time
15 days for standard sizes, 25 days for custom
MOQ
No MOQ — order 1 piece or 100 pieces
Custom shank lengths are available. We can machine a 120 mm long shank with a flat for set screw retention, or a threaded back end for drawbar pull. The minimum order is one piece, so you can test fit before committing to a production batch. This is standard policy, not a special concession.
Why Our Collet Chuck Outperforms Imported ER Holders on Swiss Lathes
ER collets are fine for general milling, but they lack the axial rigidity required for Swiss-type turning. The W20 design uses a longer taper contact area, about 15% more surface than an ER32 collet of the same clamping diameter. This reduces deflection under a 0.5 mm depth-of-cut in stainless steel. In our own test shop, we ran a 6 mm carbide end mill at 8,000 RPM, 0.05 mm feed per tooth, and measured 0.008 mm deflection at the tool tip. The same setup with an ER32 holder gave 0.021 mm deflection. That difference is the line between a finished part and a scrapped one.
If you are selecting between collet systems, read our CNC cutting tool selection guide for a deeper comparison of grip force and runout. And if you are unsure about the tolerance class you need for your application, check the CNC machining tolerances guide to match the right grade to your part spec.
FAQ: What Engineers Ask Before Ordering
Do you really have no MOQ for this collet chuck?
Yes, we accept orders for a single piece, though the unit price for 1 piece is higher than for a batch of 20.
Can you customize the shank length or thread type?
Yes, we can modify the shank length, add flats, or change the back thread to a B16 or B18 style within 25 days.
How do you ensure the 0.003 mm runout is consistent across a batch?
We measure 100% of units, not a sample, and reject any that exceed 0.003 mm TIR; the CMM report is shipped with each unit.
What is the typical lead time for a custom W20 chuck?
Standard sizes ship in 15 days; custom shank lengths or materials take 25 days from drawing approval.
Get a Firm Quote Within 12 Hours
Send your drawing or a sketch of the shank dimension and collet size. We will reply with a firm price, a confirmed lead time, and a DFM (design for manufacturability) note if we see a way to improve the grip or reduce cost. No vague estimates. Email us at sc@bquq.com or message us on WhatsApp at +86 13713157787. We are online from 8:30 AM to 6:30 PM China Standard Time, Monday to Saturday. Send your drawing now and get a quote before your coffee gets cold.