Why This Chuck Eliminates Tool Runout Before It Starts This is a CNC machined chuck collection 3 jaw collet chuck CNC, built for clamping shank tools from Ø1.0 mm to Ø32.0 mm. The
Why This Chuck Eliminates Tool Runout Before It Starts This is a CNC machined chuck collection 3 jaw collet chuck CNC, built for clamping shank tools from Ø1.0 mm to Ø32.0 mm. The concrete benefit is
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Why This Chuck Eliminates Tool Runout Before It Starts
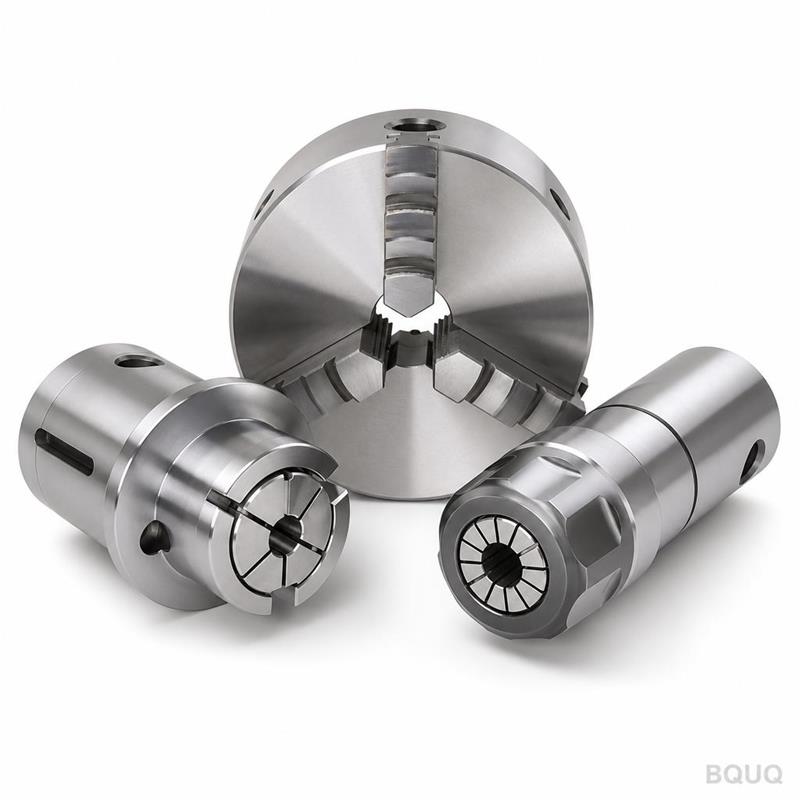
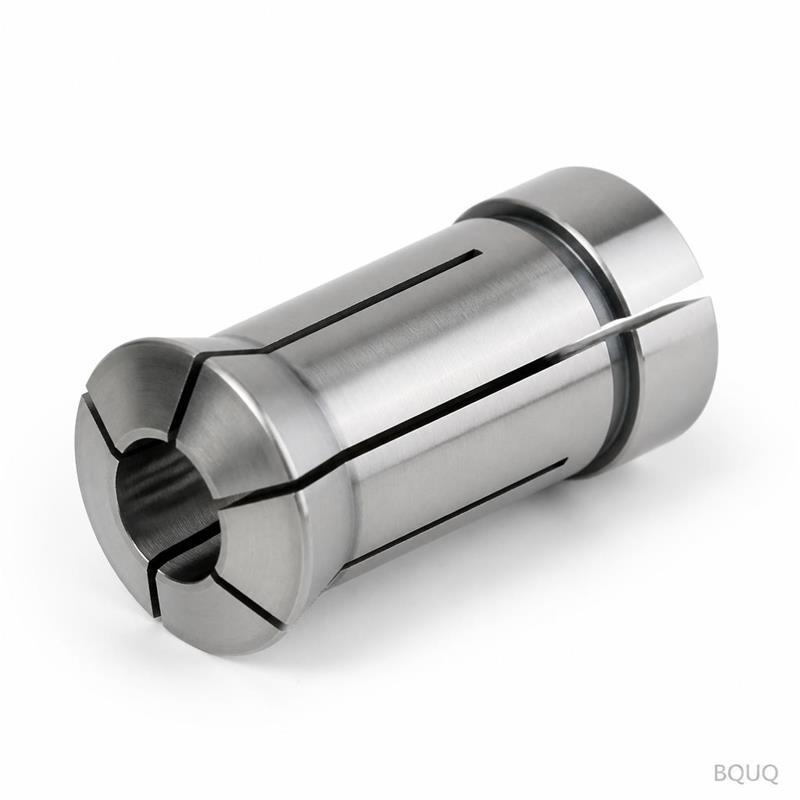
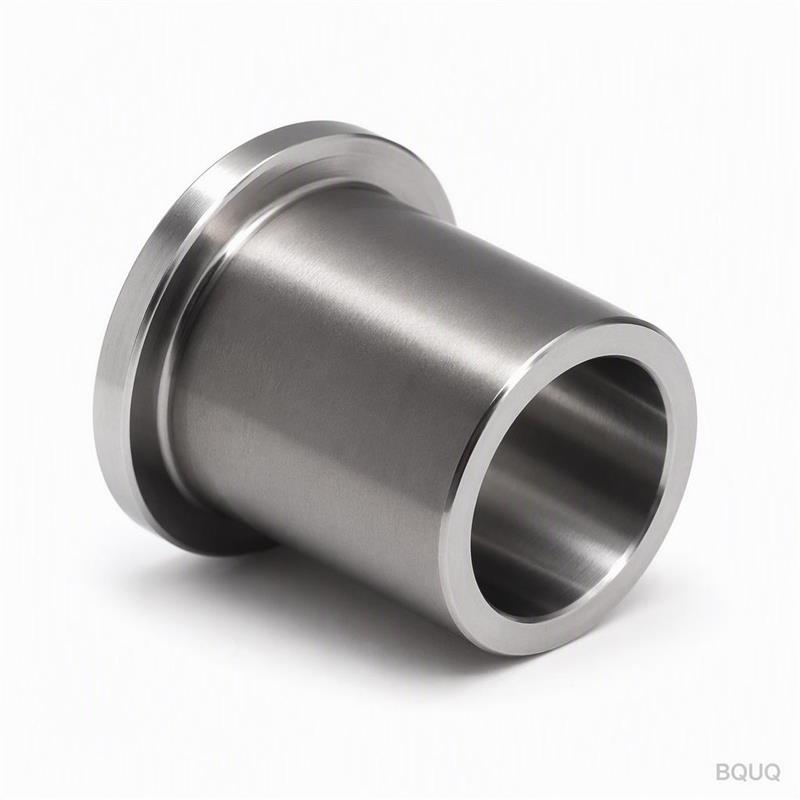
This is a CNC machined chuck collection 3 jaw collet chuck CNC, built for clamping shank tools from Ø1.0 mm to Ø32.0 mm. The concrete benefit is repeatable concentricity: ≤0.005 mm TIR at 4× tool diameter from the nose. That translates to fewer broken taps, cleaner hole walls, and longer tool life. We machine the body in one clamping operation, so the bore and the taper are geometrically locked to each other. No re-fixturing, no stack-up error.
How ER Collet Chucks Grip Tooling Without Distortion
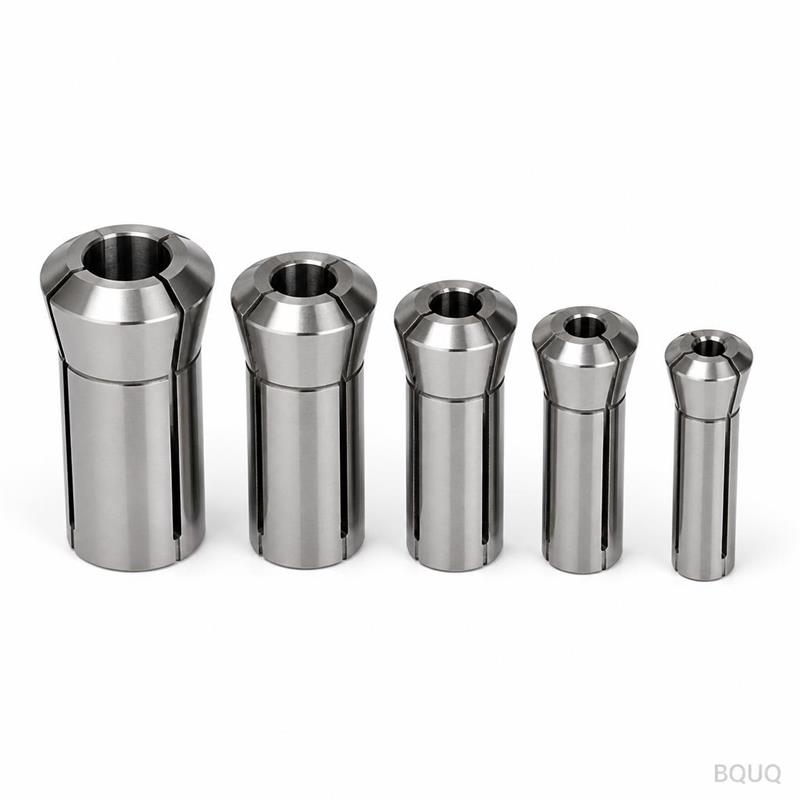
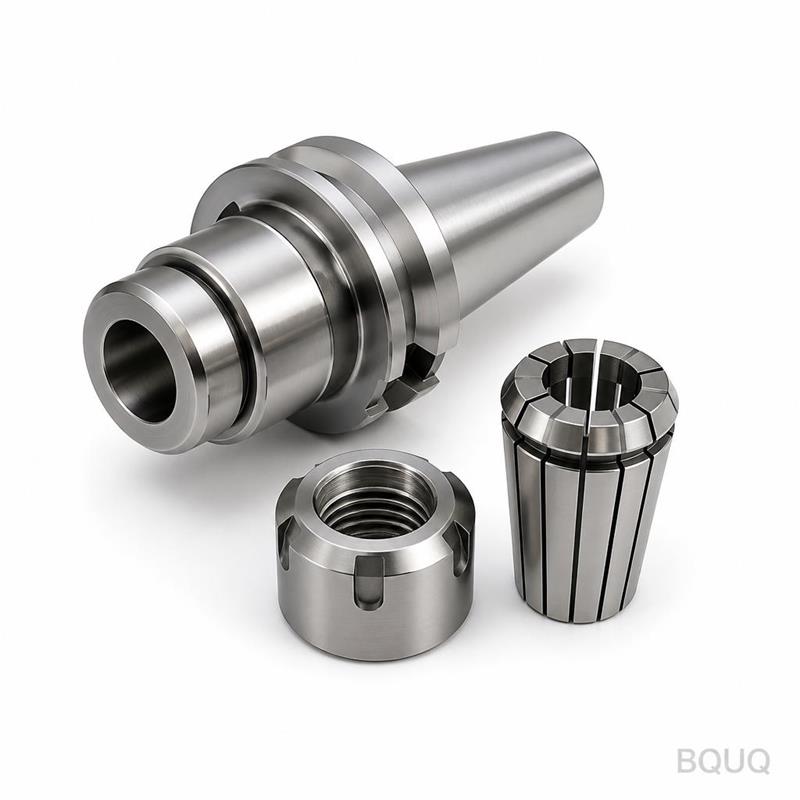
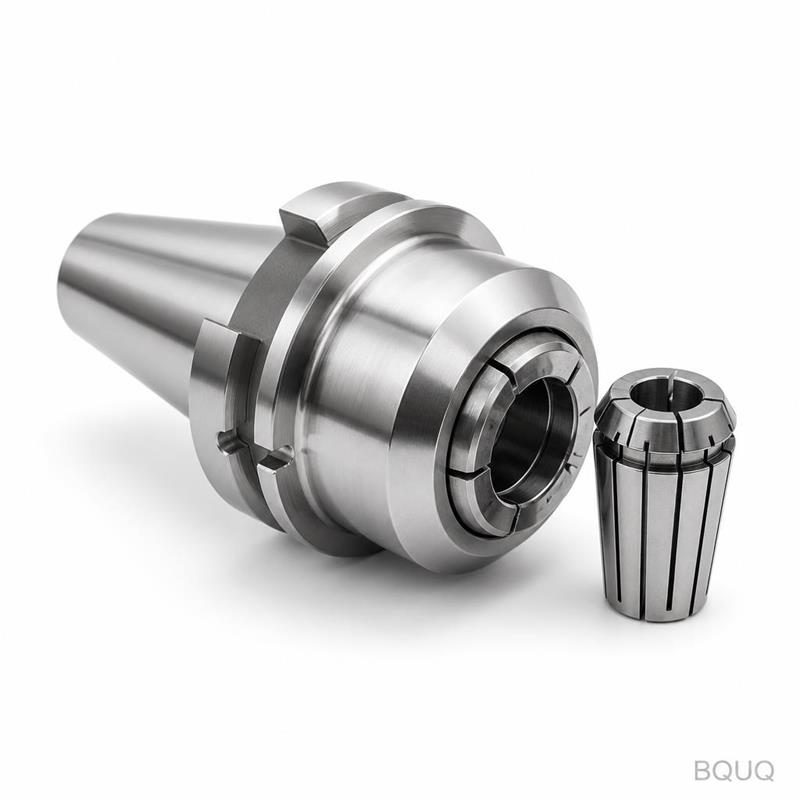
The ER system uses a slotted collet that compresses radially, not axially. A precision ground taper (16° included angle) forces the collet to close evenly around the tool shank. Unlike a 3-jaw scroll chuck, there are no moving jaws to wear or shift. The clamping force is distributed across 8 to 12 contact slots, which grips a Ø10.0 mm shank with over 2,800 N of radial force. This is why our chuck holds a DIN 6499 ER32 collet with zero backlash even after 10,000 cycles. For heavier cuts, we offer a 3 jaw collet chuck variant with hardened steel jaws, but the ER version remains the standard for high-speed spindles up to 20,000 RPM.
Materials and Heat Treatment We Use
We start with 42CrMo4 (AISI 4140) for the chuck body and 20CrMnTi for the collet nut. The body is normalized, then hardened to HRC 58-62. We do not stop at the surface — the core hardness stays above HRC 45 to resist deformation under repeated clamping. The taper is ground after heat treatment, not before. That is the only way to hold a 0.002 mm profile tolerance on the cone. The collets themselves are made from 65Mn spring steel, hardened to HRC 44-48, and slotted with a 0.3 mm wire EDM. Every chuck is then black oxide coated to resist shop coolant corrosion. For stainless or medical environments, we offer electroless nickel plating at no extra cost for orders over 50 pcs.
Ø16 / Ø20 / Ø25 / Ø32 / Ø40 mm (straight or BT/HSK)
Collet range
Ø1.0 – Ø26.0 mm (depending on ER size)
Body material
42CrMo4 (AISI 4140)
Collet material
65Mn spring steel
Hardness (body)
HRC 58-62
Runout (TIR)
≤0.005 mm at 4×D from nose
Surface finish
Ra 0.4 μm on taper, Ra 0.8 μm on OD
Taper accuracy
AT3 per DIN 6499
Balancing grade
G2.5 @ 20,000 RPM (optional G1.0)
Lead time
15 days for standard, 25 days for custom
MOQ
No MOQ – 1 piece accepted
Inspection Before Every Shipment
We check three things on every single chuck, not a batch sample. First, the taper angle is measured with an air gauge — 16°00' ± 2'. Second, we mount a test bar (Ø10.0 mm, 100 mm long) and measure runout at the nose and at 40 mm from the nose. The numbers must be under 0.005 mm and 0.008 mm respectively. Third, we test the clamping torque with a preset wrench to verify the nut rotates smoothly without galling. Each chuck gets a serial number laser-engraved on the body, and we keep the inspection report for 10 years. If you request it, we send a PDF of the actual measured values with your shipment. This is standard for our precision manufacturing line, not an add-on service.
Why a 3 Jaw Collet Chuck Beats a Drill Chuck for CNC Work
A standard drill chuck uses three jaws that move independently, so the gripping point shifts as the jaws wear. A collet chuck uses a spring collet that expands and contracts as a single piece. The result: runout stays constant from the first part to the ten-thousandth part. For drilling, reaming, and light milling, we recommend the ER style. For heavy-duty turning or broaching, the 3 jaw collet chuck variant provides 3× more axial holding force. Both are available in this collection. You specify the shank type (straight, BT30, BT40, HSK63A) and we machine the back end to match your spindle. If you are unsure which style fits your operation, read our CNC cutting tool selection guide for a side-by-side comparison of grip mechanisms.
Custom Options for Non-Standard Shanks and Lengths
Standard chucks are ground to ISO 10897 tolerances. But we regularly machine custom versions: extended necks for deep pocket milling, reduced shank diameters for small spindles, and through-coolant holes (up to 70 bar) with internal M6 thread for coolant nozzles. We also offer a special version for pull-back collets where the collet seats into a 30° internal taper. The minimum order for a custom option is just one piece, because this is made in China — but we are not a mass-production line. Our CNC machining cell handles 30 different chuck variants per week. Send your drawing with the shank diameter, total length, and collet size, and we will confirm the geometry within 12 hours. For tolerance limits on the shank fit, check our CNC machining tolerances guide before you call.
Packaging and Shipping Details
Each chuck is wrapped in VCI anti-rust paper, then sealed in a foam-lined plastic box. We ship by DHL or FedEx for single pieces (3-5 days), or by sea freight for bulk orders (20-25 days). The outer carton is a 5-layer corrugated box with a crush test rating of 12 kg/cm². For orders over 10 pcs, we divide them into individual boxes to prevent metal-to-metal contact during transit. Every shipment includes the inspection certificate, a calibration report for the runout gauge used, and a packing list with the HS code (8466.93). If you are in the EU or USA, we provide a Certificate of Origin for duty reduction.
What is the minimum order quantity for this chuck?
No MOQ — we accept a single piece for prototyping, and the price per piece drops by roughly 18% at 10 pcs and 30% at 50 pcs.
Can you machine a custom shank taper (e.g., HSK or Capto)?
Yes, we grind any taper from BT30 to HSK100, including Capto C3-C8, with a 3-day lead time added for the custom grind.
How do you verify runout on the final chuck?
We use a marble base, a 0.001 mm dial indicator, and a certified test bar; the measured value is recorded and shipped with the product.
What is the typical lead time for a standard ER32 chuck?
15 days from drawing approval, or 10 days if you accept our standard stock dimensions — and we ship by air to your door.
Request a Firm Quote With Your Spindle Data
Send us your shank type, collet size, and required runout. We will reply with a firm price, a confirmed lead time, and a 3D PDF of your chuck. No vague estimates — you get a fixed quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. If you have a drawing, attach it directly. If you only have a spindle catalog page, send a photo. We will match the dimensions and send you a pre-production sample before you commit to a batch. This is precision manufacturing from a 20-year-old Dongguan factory, ready for your toughest spindle.