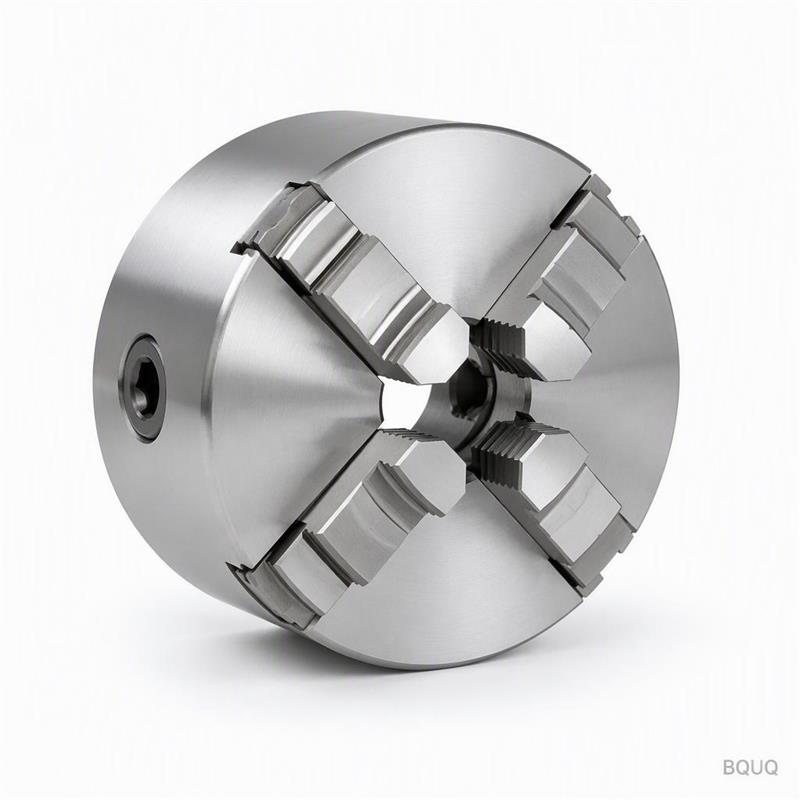
What This C Style Collet Chuck Holder Does for Your Spindle This is a C style collet chuck holder — a precision CNC tooling component that grips ER collets to hold cutting tools fi
C Style Collet Chuck Holder CNC Tooling | BQUQ Precision Made in China
What This C Style Collet Chuck Holder Does for Your Spindle This is a C style collet chuck holder — a precision CNC tooling component that grips ER collets to hold cutting tools firmly in your machini
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This C Style Collet Chuck Holder Does for Your Spindle
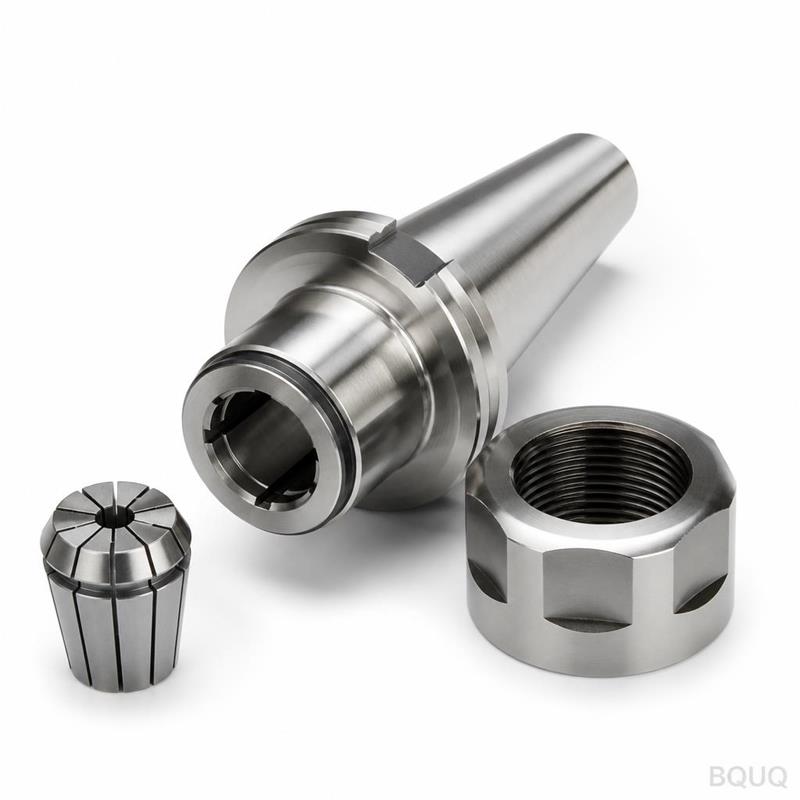
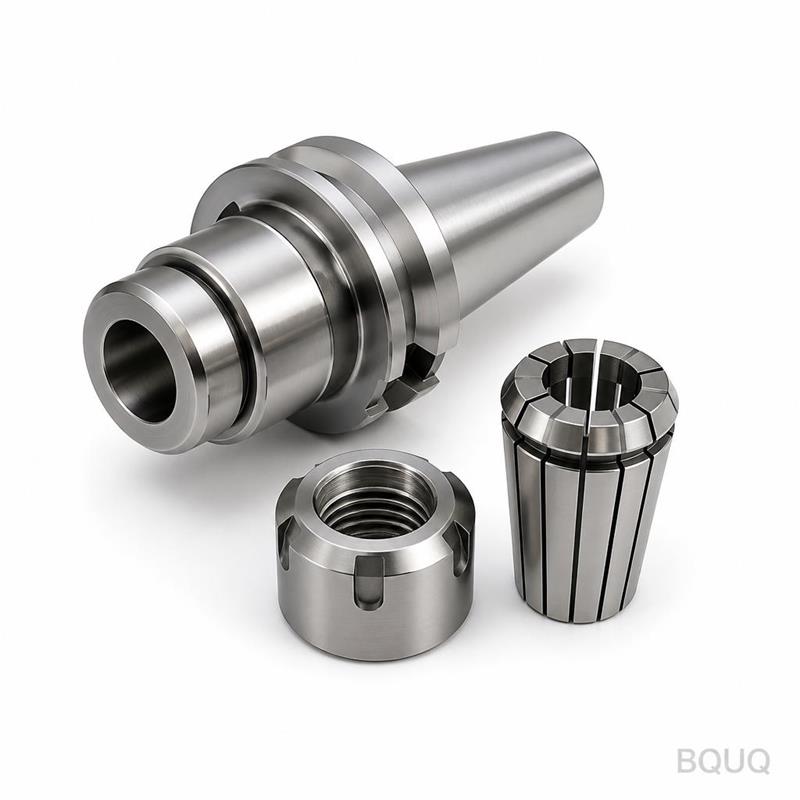
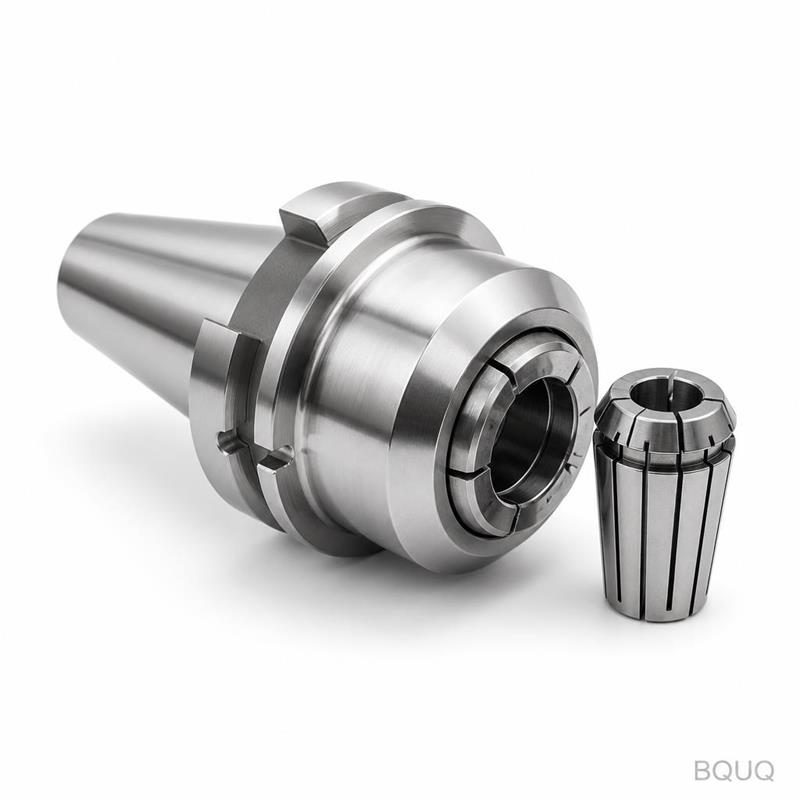
This is a C style collet chuck holder — a precision CNC tooling component that grips ER collets to hold cutting tools firmly in your machining center or lathe. You get a guaranteed runout of 0.005 mm TIR at the nose, a hardness of HRC 58-62 on the gripping surfaces, and a lead time of 10 days for standard sizes. That means less tool deflection, longer tool life, and repeatable part accuracy on every cycle.
Why a C Style Chuck Beats a Straight Shank for High-Speed Machining
C style collet chucks are designed with a tapered nose and a threaded retaining nut, which pulls the collet inward as you tighten. This creates a stronger, more concentric grip than a straight shank holder, especially above 10,000 RPM. For your high-speed milling or drilling operations, this design reduces vibration and prevents tool pullout — so you can push feed rates up to 20% higher without losing finish quality.
Materials and Heat Treatment We Use for the Chuck Body
We machine the chuck body from 42CrMo alloy steel, then through-harden it to HRC 58-62. The hardened layer reaches 1.5 mm deep, so the taper won't deform even after repeated collet changes. The retaining nut is made from 20CrMnTi, carburized to HRC 58-62 for wear resistance on the threads. We grind the inner taper to a surface finish of Ra 0.4 µm, which ensures the collet seats evenly and holds runout at 0.005 mm TIR.
Inspection Before Every Shipment — Not Just a Spot Check
Every single C style collet chuck holder goes through a 100% inspection, not a sampling plan. We measure the taper angle with a CMM, check the runout with a precision mandrel, and test the thread fit with a go/no-go gauge. You also get a printed inspection report with the actual measured values, signed by our QC engineer. If any unit exceeds 0.005 mm TIR, it goes back to the grinding machine — it never ships.
How We Match Your Tooling Setup with the Right ER Collet Series
We make C style chucks for ER11, ER16, ER20, ER25, ER32, and ER40 collets. The shank diameter can be 1/8" to 1-1/4" (3.175 mm to 31.75 mm), and the overall length ranges from 50 mm to 150 mm. If you use a CAT, BT, or HSK spindle, we can machine the back end to your exact pull stud or retention knob specification. Just tell us your collet series and shank size — we'll match the taper geometry precisely to the collet manufacturer's standard.
Surface Finish and Coating Options for Corrosion Resistance
Standard finish is a black oxide coating, which protects against rust and reduces friction when inserting the collet. For coolant-heavy environments, we offer an electroless nickel plating that adds 25 µm of corrosion resistance without changing the dimensions. If you need high-temperature stability above 200°C, we can apply a TiN coating on the taper. All coatings are applied after final grinding, so the dimensional accuracy stays within tolerance.
Why You Should Compare Our Price Against Local Suppliers in the USA or EU
You might think a made in China tool holder costs less but sacrifices quality. That's not true with our precision manufacturing process. Our C style collet chuck holders are ground on the same Japanese and Swiss machines used by premium brands, but our overhead in Dongguan is lower. You typically pay 30-40% less than a comparable German or American product, and we ship DDP to your door with no hidden customs fees. The tolerance and hardness are identical — we publish them, and we stand behind them.
Technical Specifications for C Style Collet Chuck Holder
Parameter
Value
Material (body)
42CrMo alloy steel
Material (nut)
20CrMnTi, carburized
Hardness (body)
HRC 58-62
Hardness (nut threads)
HRC 58-62
Runout (TIR at nose)
0.005 mm
Taper surface finish
Ra 0.4 µm
Collet series
ER11, ER16, ER20, ER25, ER32, ER40
Shank diameter
3.175 mm – 31.75 mm (1/8" – 1-1/4")
Overall length
50 mm – 150 mm
Lead time (standard sizes)
10 days
MOQ
No MOQ — order 1 piece
Inspection
100% CMM + runout test, report included
FAQ: What Engineers Ask Before Ordering
What is the minimum order quantity for a custom C style chuck?
There is no MOQ — you can order a single prototype piece for testing, and we will apply the same full inspection process as a bulk order.
Can you machine the back end to fit a CAT40 or BT30 spindle taper?
Yes, we can turn, grind, and thread the back end to match any standard spindle taper (CAT, BT, HSK) or your custom pull stud design — just include the drawing with your inquiry.
How do you guarantee the 0.005 mm runout on every unit?
We grind the inner taper and nose in a single setup on a cylindrical grinder, then verify each unit with a precision test mandrel and record the actual TIR on the inspection report.
What is the lead time if I need a non-standard length or coating?
Standard sizes ship in 10 days; custom lengths or special coatings (TiN, nickel) add 3-5 days, so expect 13-15 days total — we will confirm the exact date in your quote.
Get a Firm Quote Within 12 Hours — Send Your Drawing Now
Stop waiting for vague estimates. Send us your drawing or just your spindle and collet specs, and we will return a firm quote with unit price, tooling cost, and delivery date within 12 hours. For a full reference on choosing toolholders, check our CNC cutting tool selection guide. To confirm your tolerance requirements, read our CNC machining tolerances guide. Email your drawing to sc@bquq.com or reach us on WhatsApp at +86 13713157787 — we are ready to machine your first piece this week.