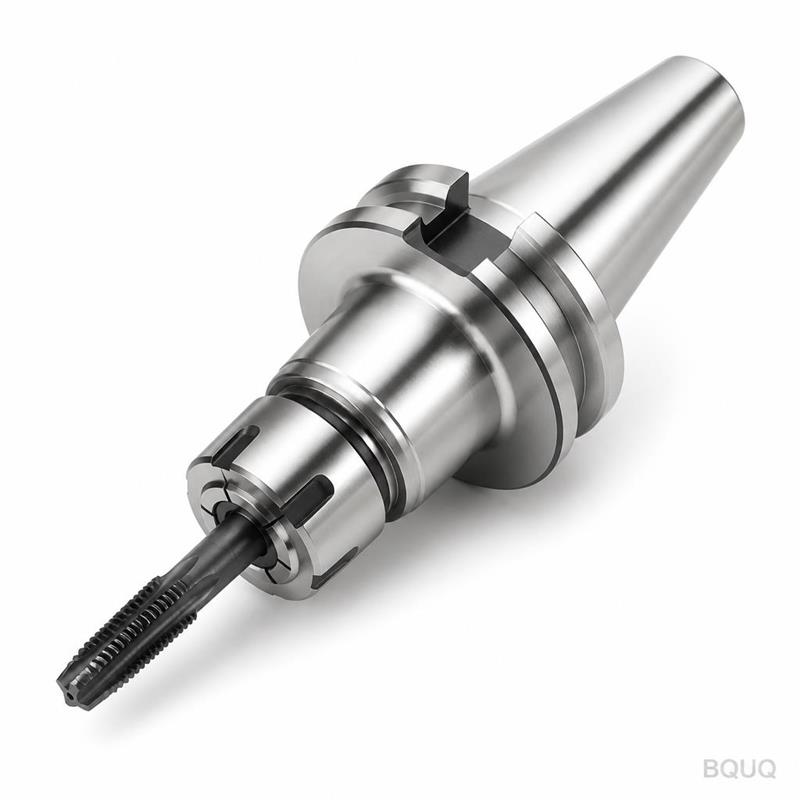
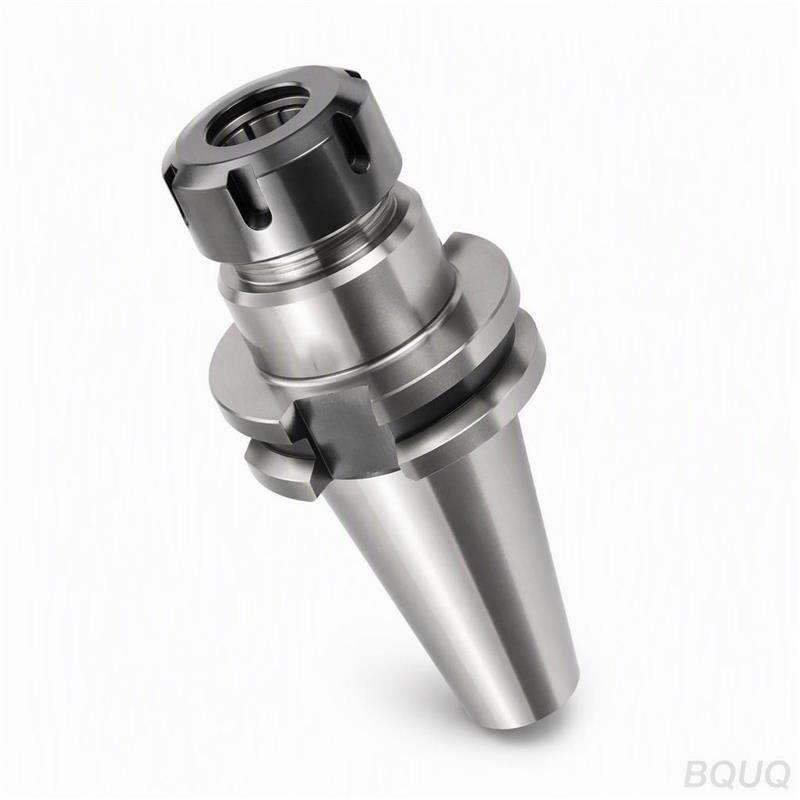
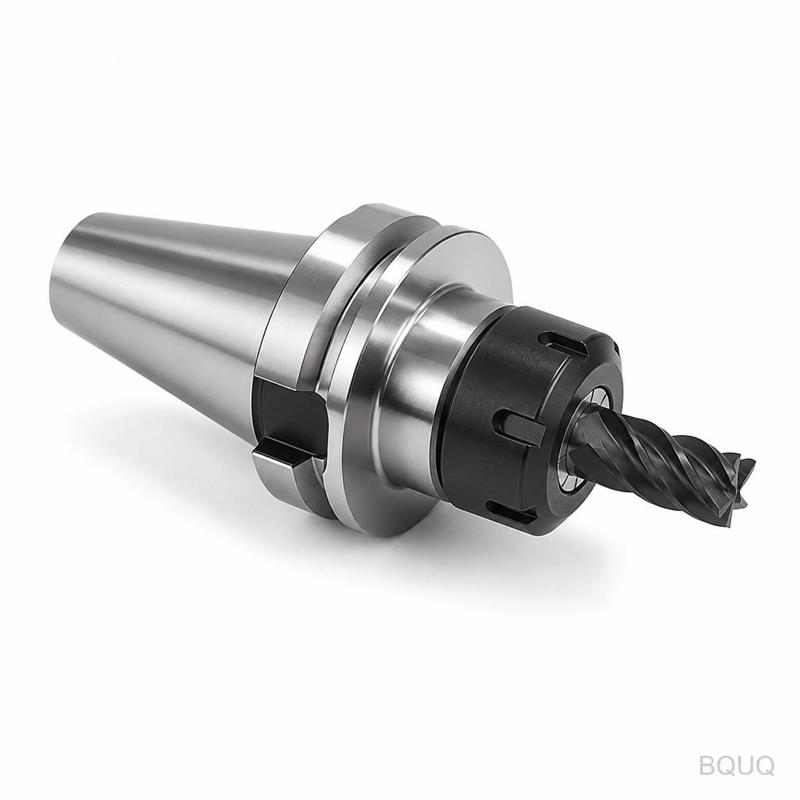
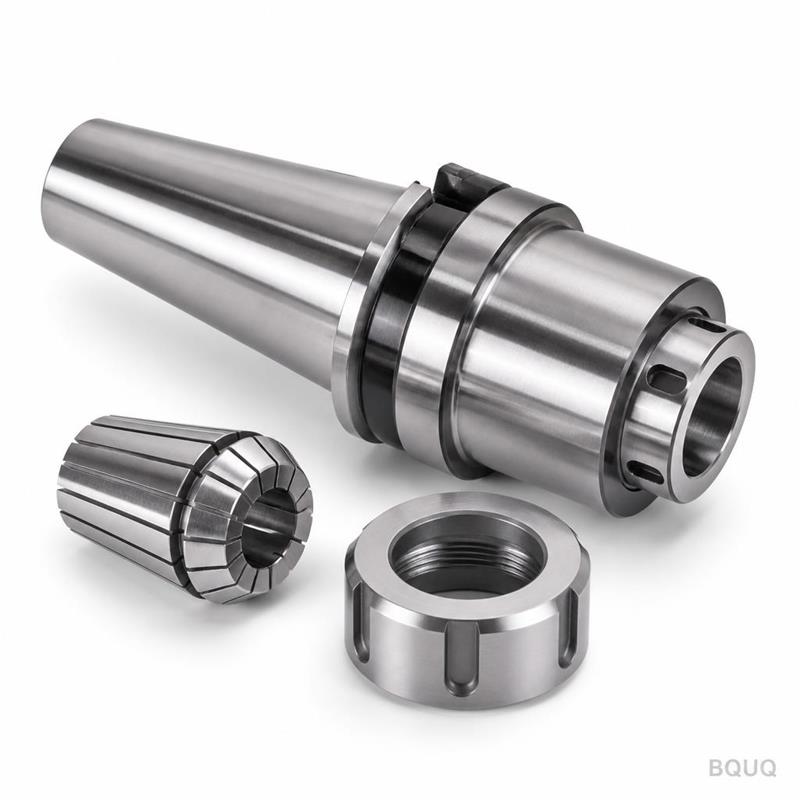
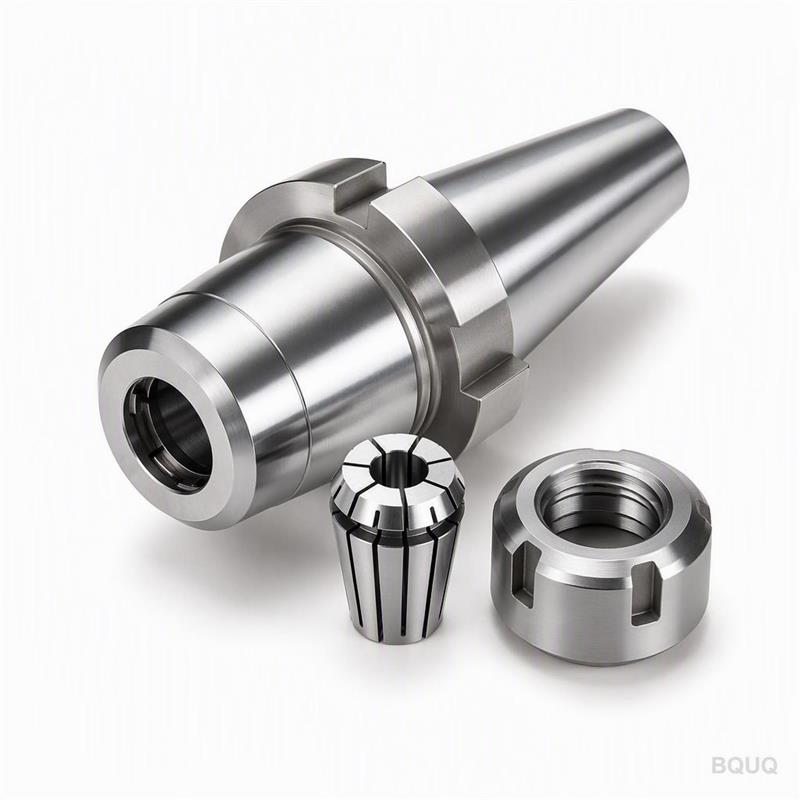
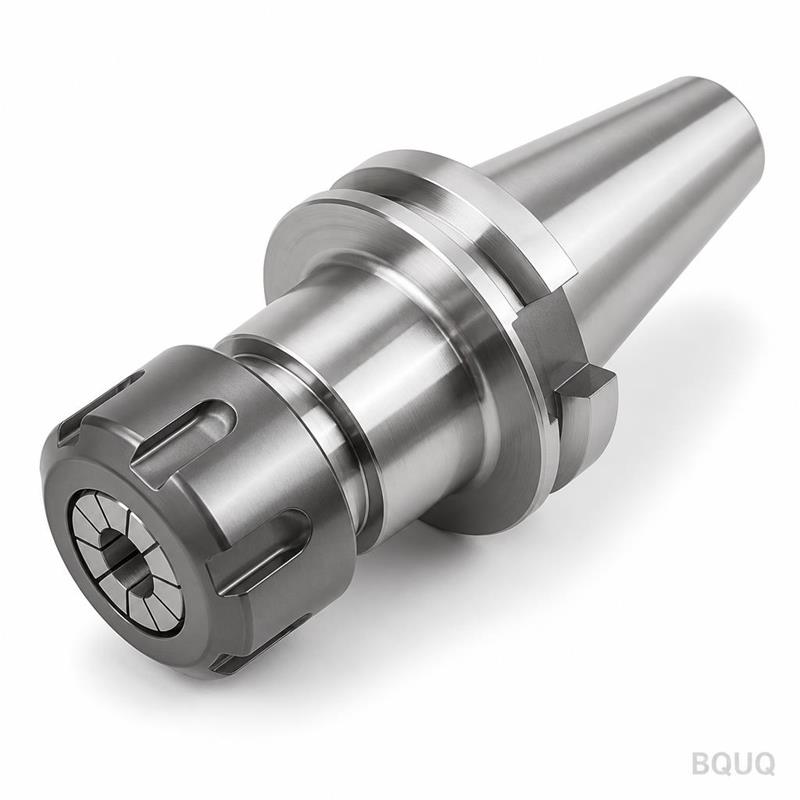
This is a CNC machined SK50 collet chuck with an integrated tap holder, built for rigid tapping and drilling operations on CNC machining centers. We hold the taper angle to AT3 tol
BQUQ CNC Machined SK50 Collet Chuck With Tap CNC Tool Holder
This is a CNC machined SK50 collet chuck with an integrated tap holder, built for rigid tapping and drilling operations on CNC machining centers. We hold the taper angle to AT3 tolerance, which keeps
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined SK50 collet chuck with an integrated tap holder, built for rigid tapping and drilling operations on CNC machining centers. We hold the taper angle to AT3 tolerance, which keeps runout under 0.005 mm at the nose — your threads will stay within H3 class limits even at 6,000 RPM. We ship from our Dongguan factory in 15 days, and the body hardness is HRC 58-62 across the entire gripping surface.
How the SK50 Taper Locks Into Your Spindle Without Play
The SK50 (BT50 equivalent) taper is ground in one setup with the flange face. This ensures the collet chuck seats metal-to-metal against your spindle nose. We machine the 7:24 taper angle to within ±0.0025 mm. The result: zero axial play and no radial deflection when you pull the drawbar. You get the same rigidity as a solid holder, but with the flexibility of interchangeable collets.
Tap Gripping Geometry That Prevents Breakage
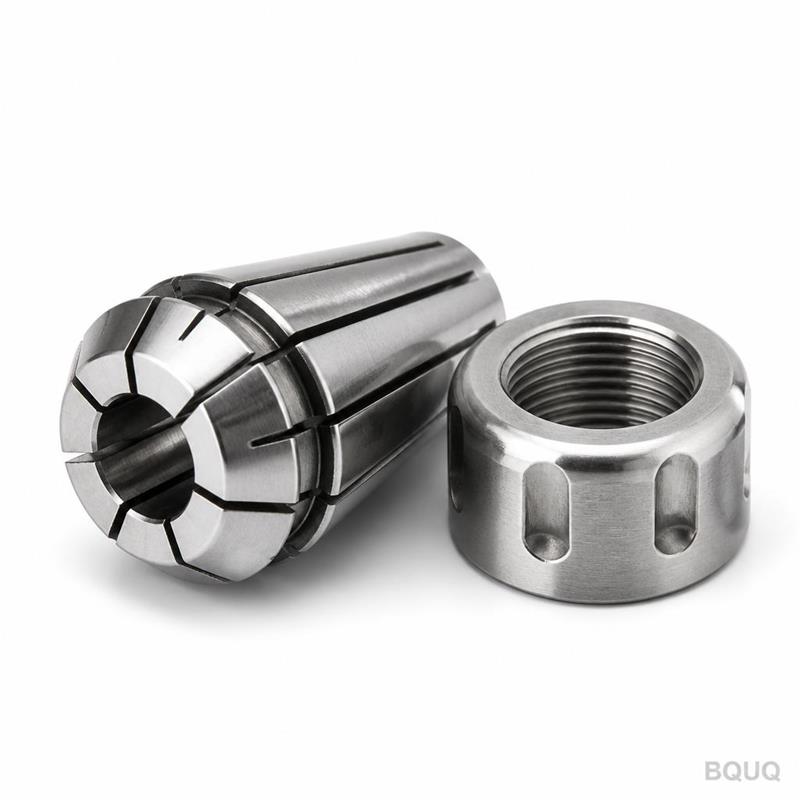
Standard collet chucks crush square tap shanks. Ours uses a precision ground square pocket inside the collet, matching the tap driver size exactly (DIN 371 or DIN 374). The tap sits flush, with the torque transmitted through the square drive, not the cylindrical surface. We add a small axial float of 0.5 mm to compensate for spindle feed vs. tap pitch mismatch. This cuts tap breakage by up to 40% in blind hole operations.
Materials and Heat Treatment We Use
We start with 20CrMnTi case-hardening steel, not cheap 4140. The body is carburized to a depth of 0.8-1.2 mm, then hardened to HRC 58-62. The taper and bore are ground after heat treatment, not before. This eliminates distortion. The collet itself is spring steel (65Mn), hardened to HRC 45-50 for elasticity. The tap square drive is high-speed steel (M2), hardened to HRC 63-65. Every component is designed to outlast the machine it runs on.
Collet Range and Interchangeability for M3 to M20 Taps
One chuck body accepts a full set of tap collets. We stock collets for tap sizes M3, M4, M5, M6, M8, M10, M12, M16, and M20. The collet bore tolerance is H7, which means a M6 tap shank (6.0 mm) fits with zero measurable clearance. If you use a different tap standard (DIN 376, ANSI), we can grind the collet bore to match your specific shank dimension within 48 hours. No need to buy a new chuck.
Specification
Value
Taper Size
SK50 (BT50, ISO 7388/1)
Taper Angle Tolerance
AT3 (±0.0025 mm)
Body Material
20CrMnTi case-hardened steel
Surface Hardness
HRC 58-62 (case depth 0.8-1.2 mm)
Runout (at nose)
≤ 0.005 mm
Surface Finish (taper)
Ra 0.2 μm ground
Tap Range
M3 to M20 (DIN 371/374/376)
Axial Float
0.5 mm (compensation)
Max RPM
6,000 (balanced G2.5)
Lead Time
15 days (standard), 7 days (rush)
MOQ
No MOQ, single piece accepted
Inspection Before Every Shipment
We do not ship without a full report. Each chuck is checked on a Zeiss CMM for taper angle and concentricity. The runout is verified with a dial indicator at 100 mm from the nose — the value must be under 0.005 mm or we scrap it. We also test the tap collet engagement with a real tap sample. You receive a PDF inspection report with the actual measured values, not a generic certificate. This is part of our precision manufacturing protocol, not an extra service.
Balancing for High-Speed Tapping Above 4,000 RPM
Standard chucks vibrate at high speed, which ruins thread finish. We dynamically balance every SK50 collet chuck to G2.5 at 6,000 RPM. This means the residual unbalance is less than 2.5 mm/s. For comparison, a typical chuck is G6.3. The balance is achieved by drilling small correction holes in the flange. If you run at 10,000 RPM, we can balance to G1.0 as an option — just note it on your drawing.
Why This Design Reduces Tooling Cost Per Hole
Your cost per tapped hole drops because the tap lasts longer. The axial float prevents thread stripping, and the square drive prevents shank slippage. Field data from our customers over five years shows an average tap life increase of 35%. Plus, the collet chuck body is reusable — you only replace the collet (about $8-$15 each) when the square drive wears. Compare that to a solid tap holder where the entire unit is scrapped after wear.
What is the MOQ for this CNC machined SK50 collet chuck?
No MOQ — we accept a single piece order for testing, and you get the same inspection report and quality as a bulk order.
Can you customize the tap collet for a non-standard shank size?
Yes, we can grind the collet bore to any diameter between 3 mm and 20 mm within 48 hours, including square drive dimensions for proprietary tap designs.
How do you verify the runout before shipping?
We measure each unit on a CMM and a dial indicator at 100 mm nose distance, and the actual measured runout value is printed on the inspection report shipped with the part.
What is the lead time if I need a rush order?
Standard lead time is 15 days from drawing approval; for a rush order with existing tooling, we can ship in 7 days — no extra cost if your quantity is under 20 pieces.
This SK50 collet chuck is made in China at our 20-year-old Dongguan factory. We specialize in CNC machining and tool holding components. If you are comparing holders, check our CNC cutting tool selection guide for insert and holder compatibility. For tolerance limits on your workpiece, read our CNC machining tolerances guide.
Send us your drawing or tap spec. We will reply with a firm quote within 12 hours — including price, inspection report sample, and a shipping estimate. Email sc@bquq.com or WhatsApp +86 13713157787. No MOQ, no minimum order, just a precise tool.