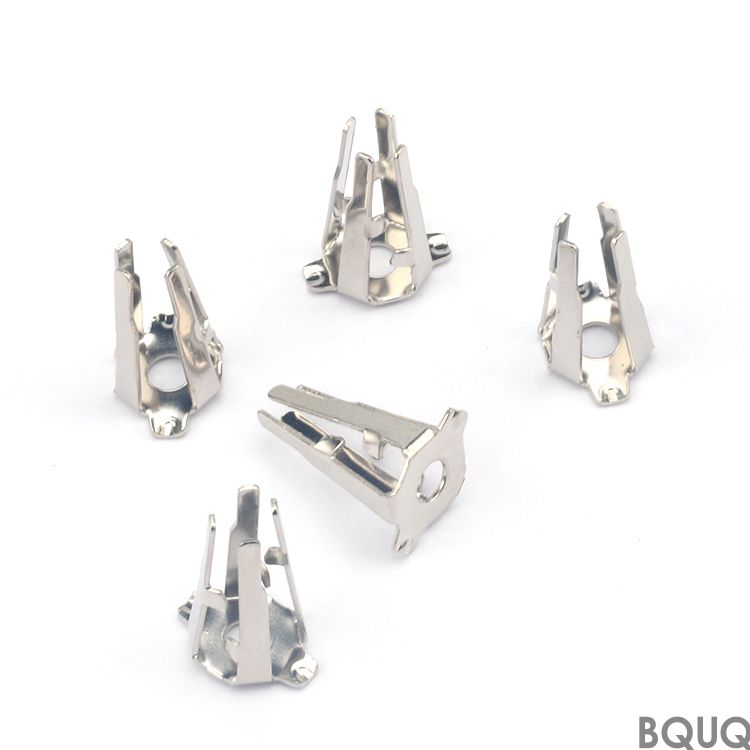
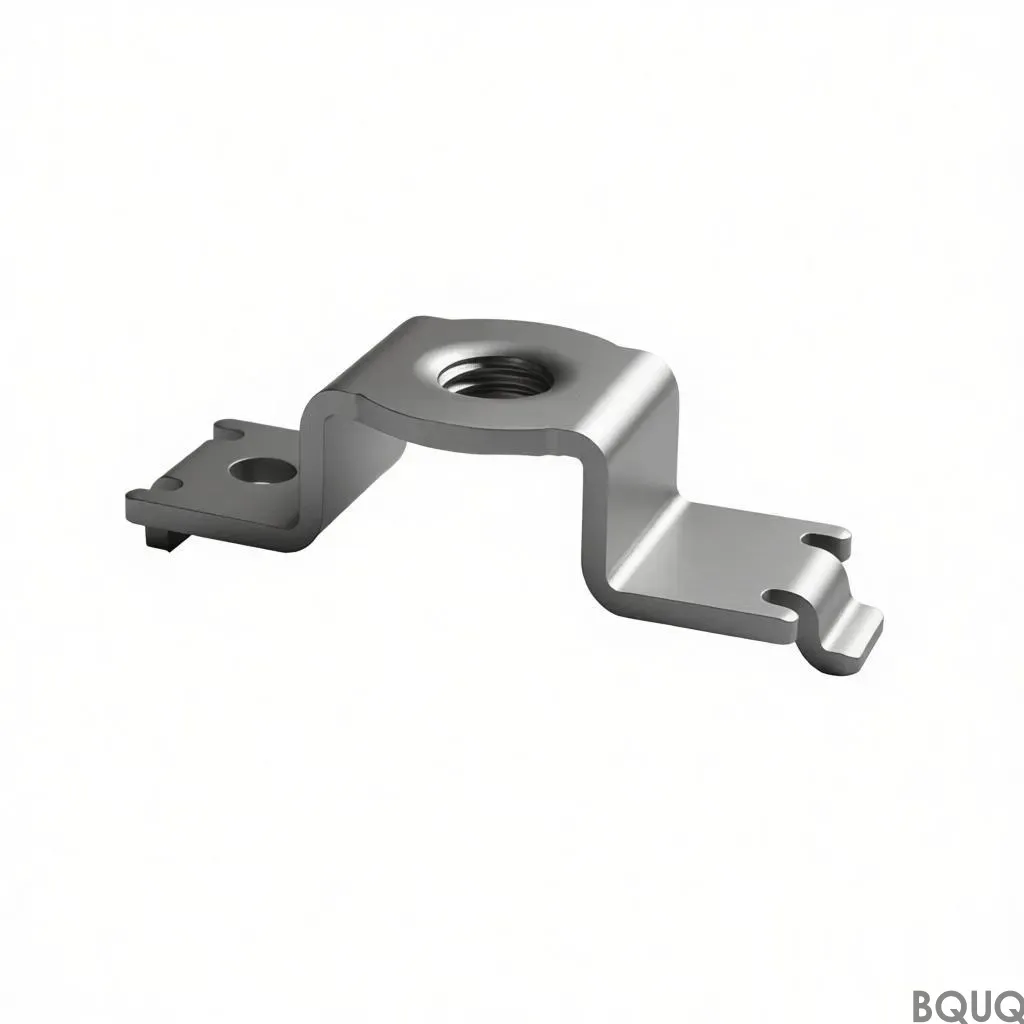
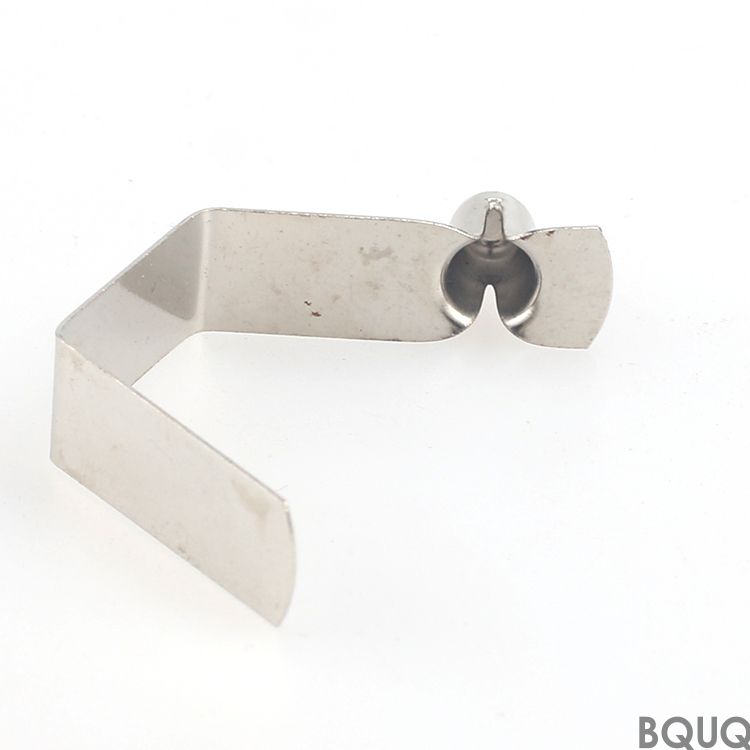
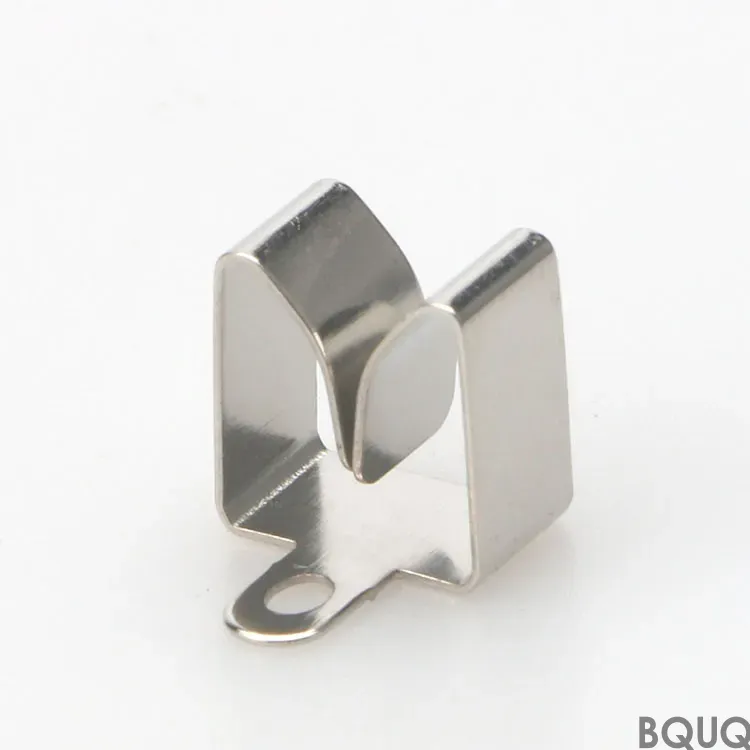
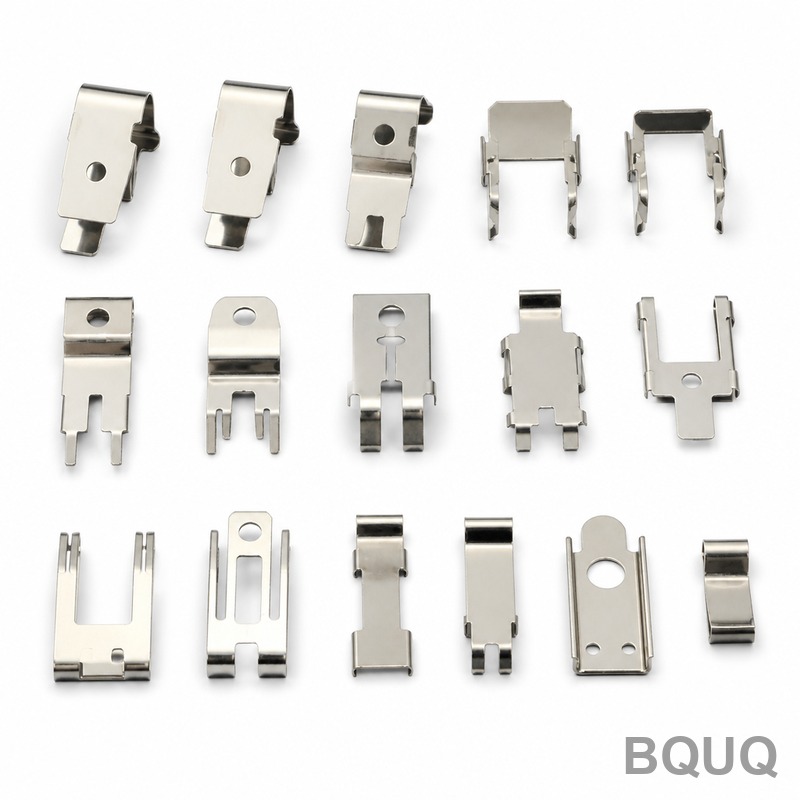
This is a progressive die stamped elastic clamp — a spring-steel clip formed in a continuous die strip, not a bent wire or machined block. You get repeatable clamping force across
Progressive Die Stamping Elastic Clamp | BQUQ Precision Metal Stamping Parts
This is a progressive die stamped elastic clamp — a spring-steel clip formed in a continuous die strip, not a bent wire or machined block. You get repeatable clamping force across 100,000 parts, dime
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a progressive die stamped elastic clamp — a spring-steel clip formed in a continuous die strip, not a bent wire or machined block. You get repeatable clamping force across 100,000 parts, dimensional tolerance of ±0.01 mm on critical surfaces, and a surface finish of Ra 0.8 µm without secondary polishing. BQUQ ships these clamps from our Dongguan factory in 7 days for standard tooling, with hardness held at 45–50 HRC for spring-grade 65Mn or 301 stainless.
How Progressive Die Tooling Locks in Clamp Geometry
A progressive die (also called a continuous die) feeds a metal strip through 12 to 18 stations. Each station performs one operation — pilot hole piercing, blanking, coining, bending, and final cutoff — while the strip remains indexed to ±0.005 mm. This means every elastic clamp comes off the line with identical bend radii and leg angles. No secondary hand forming. No operator judgment. The die sets we build for elastic clamps use D2 tool steel punches and carbide inserts, giving you a tool life of 500,000 to 1,000,000 strokes before resharpening.
Spring Steel Grades and Heat Treatment for Elastic Clamps
An elastic clamp must return to shape after deflection. We stock three materials for this product line: 65Mn carbon spring steel (cost-effective, 45–50 HRC), SK5 high-carbon steel (better fatigue life, 48–52 HRC), and SUS301 stainless (corrosion resistant, 40–45 HRC after full hardening). All strips are oil-quenched and tempered in continuous furnaces. We control tempering time within ±5 minutes to keep hardness uniform across the strip. If your application needs a specific finish — zinc plating, nickel plating, or passivation — we apply it after heat treatment so the plating does not crack under flexing.
Holding Clamping Force Tolerance at ±10%
Clamping force is a function of material thickness, bend angle, and leg length. Our progressive die stamping holds material thickness to ±0.02 mm, and we verify bend angles with optical comparators on every first article. The result: clamp force varies less than ±10% from part to part. For a typical elastic clamp with a 10 mm opening, this means a consistent 8–12 N insertion force across your assembly line. We measure this on a custom test fixture using a digital force gauge (resolution 0.01 N) before any batch ships.
Surface Finish and Burr Control on Stamped Edges
Die clearance is set at 5–8% of material thickness per side. This is the sweet spot that produces a clean shear zone and minimizes burr height to under 0.05 mm. For edges that will contact wires or hoses, we add a coining station to push a 0.2 mm radius onto the cut edge. Surface finish on the flat faces is Ra 0.8 µm as-stamped. If you need Ra 0.4 µm for a sealing surface, we can add a micro-brush deburring pass — this adds one day to lead time but removes all microscopic edge fracture.
Inspection Before Every Shipment: Force, Hardness, and Dimensional Reports
Every batch of elastic clamps gets a sampling inspection per ISO 2859-1, Level II. We check the critical dimensions — leg opening width, inside diameter, and overall length — with a CMM (accuracy ±0.002 mm). Hardness is tested on a Rockwell tester on the flat section of the clamp. Clamping force is verified with the same fixture used in your assembly. You receive a full inspection report with each shipment, including SPC charts if your order is over 10,000 pieces. If any part fails, the entire batch is quarantined and re-sorted.
Tooling Ownership and Fast Ramp-Up for Custom Clamps
We keep the progressive die tooling in our own tool room, which means you do not pay tooling maintenance fees. For a custom elastic clamp, we deliver the first article in 15 days and production parts in 20 days. Tooling cost is quoted separately and amortized into your piece price — we can also offer a tooling buy-back agreement if you stop production within 24 months. Because we run our own wire EDM and CNC machining centers, we modify existing dies for new clamp sizes in 5 days, not weeks.
Material Certifications and Traceability for Regulated Industries
We issue mill certificates for every coil of spring steel used in your order, traceable back to the original steel mill. This is critical if your elastic clamps go into automotive braking systems, medical device handles, or electrical connectors. Each heat number is recorded in our ERP system, and we can provide full traceability reports for up to 10 years after shipment. Our ISO 9001:2015 and IATF 16949 certifications cover this product line — we are audited twice a year by third-party registrars.
Specification
Value / Range
Material grades
65Mn, SK5, SUS301, C75S
Thickness range
0.2 mm – 3.0 mm
Clamp opening diameter
3 mm – 50 mm
Overall length
5 mm – 80 mm
Hardness (as-tempered)
40 – 52 HRC depending on grade
Dimensional tolerance
±0.01 mm on critical features
Surface finish Ra
0.8 µm standard, 0.4 µm optional
Burr height max
0.05 mm
Clamping force consistency
±10% of nominal
Lead time (standard tool)
7 days for 100k pcs
MOQ
No MOQ — 1 piece to 1 million
Packaging
Anti-rust paper, plastic trays, export cartons
What is the minimum order quantity for custom elastic clamps?
We have no MOQ — you can order 10 pieces for prototyping or 1 million for production, and the piece price adjusts accordingly.
Can you modify an existing progressive die for a different clamp size?
Yes, our in-house tool room can change pilot holes, bend stations, or cutoff inserts in 5 days, and we only charge for the actual material and machining time.
How do you verify clamping force before shipment?
We use a digital force gauge with a custom anvil that simulates your assembly condition, testing 5 parts per batch and recording data in the inspection report.
What is the typical lead time for a new progressive die stamping tool?
First article in 15 days, production in 20 days from approved drawing — this includes die design, wire EDM cutting, assembly, and tryout on our 25-ton to 160-ton presses.
For clamping force requirements beyond our standard range, we recommend reviewing our CNC cutting tool selection guide to understand how mating components affect your assembly. If your design has tight dimensional callouts, our CNC machining tolerances guide explains what we can hold on stamped vs. machined features.
Send your drawing or a sketch of the elastic clamp you need — our engineers will quote the progressive die and piece price within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. We are a precision manufacturing factory in Dongguan, China, with 20 years of progressive die stamping experience, and we ship worldwide.