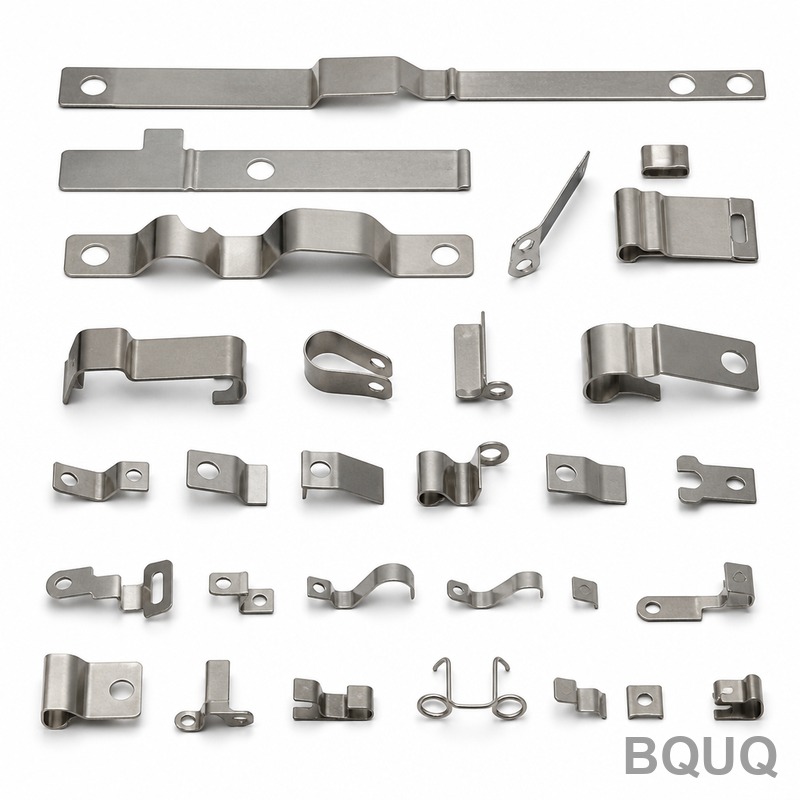
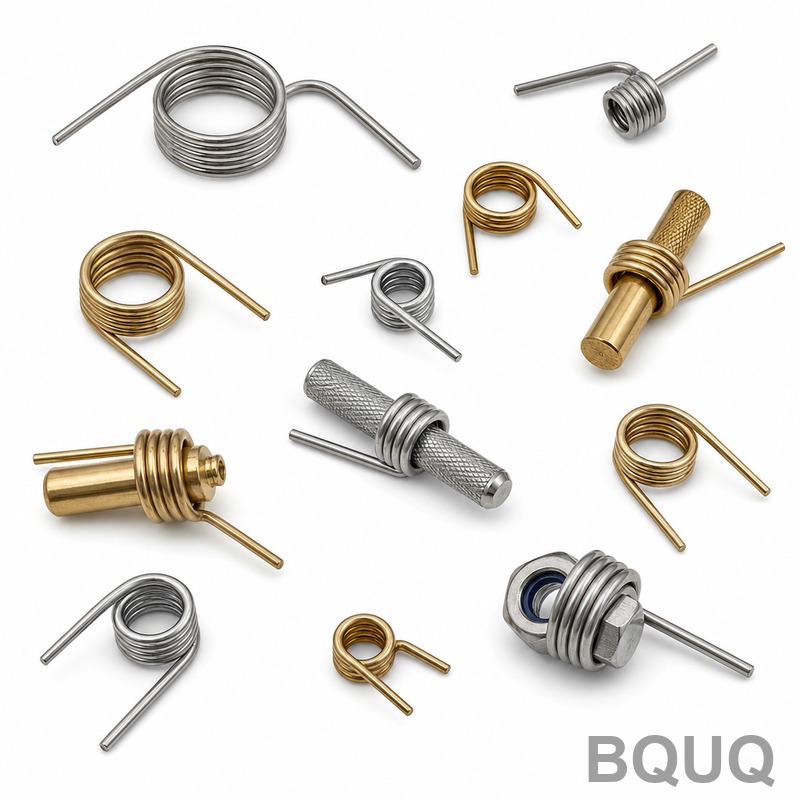
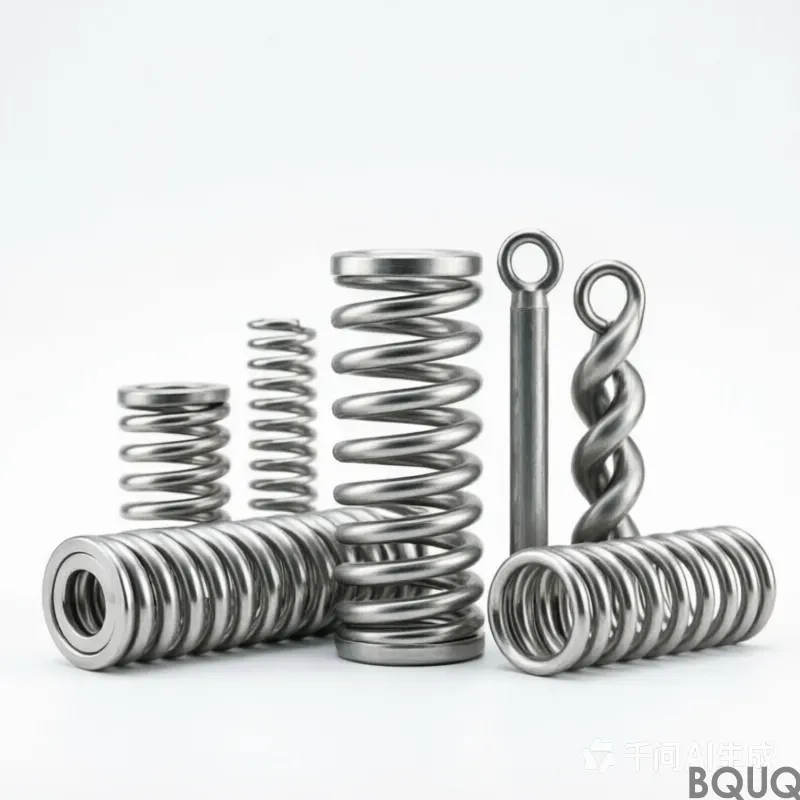
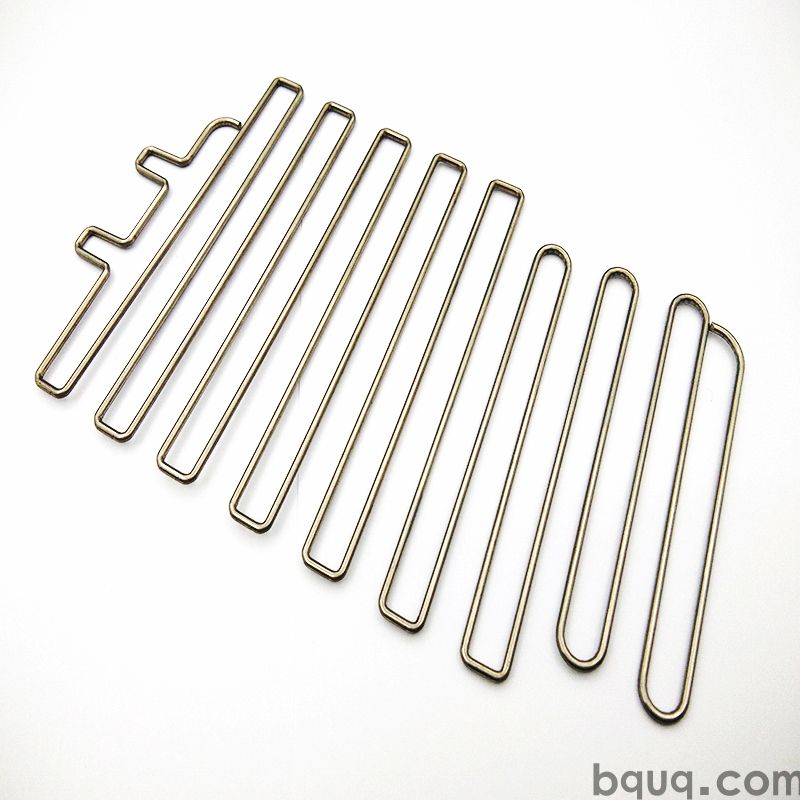
Custom spring headbands are stamped as a one-piece base-and-fin geometry, so the die forms every fin in one stroke and fin pitch stays within tolerance across a run. Flatness on the mounting face is held directly from the tool, and every batch ships with a CMM report. Tooling runs and the cycle feeds a line, with hole position carrying across the batch for repeatable volume programs.
Key Takeaway
Custom spring headbands are stamped as a one-piece base-and-fin geometry, giving repeatable fin pitch within a run and flatness held directly from the tool. The die forms every fin in one stroke, so part cost stops scaling with complexity, and every batch ships with a CMM report. Tooling runs and the cycle feeds a line, with hole position carrying across the batch for repeatable volume programs.
A custom spring headbands in delivers thermal resistance under . Fins are thick at pitch over a base, and every batch ships with a CMM report at .
Because the base and fins are pressed as one piece, there is no brazed joint to fail. flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between and the airflow except the stamped surface itself.
Every stroke is dimensionally identical, so hole position carries across the batch. That is what makes safety lanyard volume programs repeatable.
Material Selection and Surface Finish
The standard material is , supplied with . For applications where safety lanyard exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to ±0.5 mm, with critical features such as held separately. Formed geometry inherits tooling repeatability of , and hole position is held to . Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Each batch carries a CMM report from . We record flatness, pitch, base thickness and hole position, and flag anything outside ±0.5 mm before it leaves the line.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with on every first article. Deviations beyond ±0.5 mm trigger a full-lot sort.
Lot traceability runs from coil to carton: heat number, press stroke range and inspection record stay attached, so a field issue can be tied back to a specific run.
Final containment is . Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
In safety lanyard, the rating determines how much airflow the enclosure still needs. At safety lanyard junction temperatures, fins at pitch keep the delta-T inside the sensor budget.
safety lanyard customers typically specify for corrosion reasons and then hold the drawing to ±0.5 mm. The line absorbs the volume without a second source.
In safety lanyard, the base usually doubles as the mounting interface. with flat gives a stable surface for the safety lanyard thermal pad.
safety lanyard designs often run a 2.0 m/s forced-air path. at means safety lanyard can hold its target with fan power below the acoustic limit.
Specifications
Parameter
Value / Range
General tolerance
±0.5 mm
MOQ (prototype)
1000 pcs
MOQ (production)
5000 pcs
Lead time (prototype)
7 working days
Lead time (production)
20 working days
FAQ: Your Questions Before Ordering
What tolerance can you hold?
General dimensions run to ±0.5 mm; critical ones such as are held separately. Formed features inherit tooling repeatability of . If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
How does this compare to an extruded custom spring headbands?
Extrusion is cheaper above roughly 500,000 pieces per year and gives a smoother profile. Stamping wins below that and wherever fin gauge drops below 0.5 mm, because extrusion cannot hold consistently. For safety lanyard prototypes, tooling cost usually decides it.
Can you deliver without surface treatment?
Yes, we ship as-pressed for customers who do their own finishing. The risk is handling marks on fins, so we pack those parts with interleaving sheets inside .
Is there any risk of the fins bending in transit?
With fins and standard , damage is rare. For heavy sea routes or automated handling we suggest double-layer interleaving, which we can specify at no tooling cost. We have shipped per month this way without a transit claim in the last 3 years.
Can you supply the custom spring headbands pre-assembled?
Yes. We can add clips, screws or a fan shroud as a kitted assembly, with the parts bagged and labelled per set. This is common in safety lanyard programs and adds about 3 working days.
How We Manufacture and Ship
Source-direct from Dongguan: coil stock, forming, surface treatment and inspection happen in one building, so flatness is verified before the part is packed.
Our safety lanyard experience runs back to the first tooling programme in 2015. That history is why the standard and ±0.5 mm are conservative rather than optimistic.
We quote and hold 1000 pcs for sampling. Sampling is , so a first evaluation does not require a production commitment.
Single-stroke die forms whole part; every stroke dimensionally identical
Selection / comparison
Option
Best for
Trade-off
Stamped one-piece
Repeatable fin profile and uniform thermal interface contact
Requires tooling; best for volume programs
Extrusion
Simple continuous profiles
Cannot hold fin pitch as consistently as stamping
Two-part cooler with adhesive
Lower tooling complexity
Adds adhesive layer, lengthens thermal path, brazed joint can fail
Passivated finish
Exposure concerns
May trade off conductivity versus weight-sensitive applications
Conductivity-focused finish
Conductivity matters more than weight
May not prioritize exposure resistance
Process / inspection
Stage
Control
Record
Stamping
Die forms every fin in one stroke; pitch stays within across a run
Dimensional identity stroke to stroke
Base and fin forming
Pressed as one piece; no brazed joint to fail
One-piece geometry documented
Flatness
Mounting face flatness held directly from the tool
Keeps thermal interface contact uniform
Hole position
Carries across the batch
Supports safety lanyard volume programs
Final inspection
Every batch ships with a CMM report
CMM report at
Frequently Asked Questions
What makes stamped custom spring headbands more repeatable than extruded profiles?
Stamping forms every fin in one stroke, so pitch stays within across a run. Extrusion cannot hold that fin profile as consistently. Because the base and fins are pressed as one piece, there is no brazed joint to fail, and flatness on the mounting face is held directly from the tool for uniform thermal interface contact.
How does the one-piece design affect thermal performance?
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between the base and the airflow except the stamped surface itself. That direct path supports thermal resistance under the specified target while keeping flatness on the mounting face held directly from the tool.
What material and surface finish options are available for custom spring headbands?
The standard material is supplied with a passivated route recommended where exposure is a concern. Where conductivity matters more than weight, an alternative finish can be selected. Both routes are compatible with the stamped one-piece geometry and the CMM report supplied with every batch.
Can hole position be held consistently across a volume program?
Yes. Every stroke is dimensionally identical, so hole position carries across the batch. That is what makes safety lanyard volume programs repeatable. The die forms every fin in one stroke, and the cycle feeds a line, so batch-to-batch variation is controlled without secondary hole operations.
What inspection documentation ships with each batch?
Every batch ships with a CMM report at the specified tolerance. Inspection covers the stamped fin profile, pitch within across a run, flatness on the mounting face, and hole position across the batch. This record supports repeatable safety lanyard volume programs and confirms the one-piece geometry.
Does part cost scale with fin complexity in this process?
No. A single stroke forms the whole custom spring headbands, so part cost stops scaling with complexity. Tooling runs and the cycle feeds a line. Because the base and fins are pressed as one piece, there is no brazed joint to fail and no adhesive layer to add cost or thermal resistance.
Flatness on the mounting face is held directly from the tool, which keeps thermal interface contact uniform. The die forms every fin in one stroke, so pitch stays within across a run. Every batch ships with a CMM report at the specified tolerance to verify the mounting face and fin profile.
Key Specifications and Selection Guide
Spec comparison
Parameter
Value / Range
Material
Stamped metal base and fin, one-piece construction
Tolerance
Fin pitch held within tolerance across a run; flatness held directly from the tool
Lead time
Tooling runs and the cycle feeds a line; batch timing depends on tooling and run schedule
MOQ
Not specified in the article; volume programs are supported
Capacity
Repeatable volume programs with hole position carrying across the batch
Selection / comparison
Option
Best for
Trade-off
Stamped one-piece base-and-fin
Repeatable fin pitch and flatness from the tool
Requires tooling; geometry is set by the die
Extruded fin profile
Simpler profiles where extrusion can hold shape
Cannot hold the repeatable fin profile that stamping gives
Two-part cooler with adhesive layer
Applications where a bonded joint is acceptable
Adds an adhesive layer and a brazed joint that can fail
Brazed joint construction
When a joined assembly is required
There is a brazed joint to fail and an extra thermal path layer
One-piece stamped headband
Thermal interface contact uniformity and volume programs
Part cost stops scaling with complexity, but tooling is needed
Frequently Asked Questions
What makes custom spring headbands different from extruded fin profiles?
Stamping gives a repeatable fin profile that extrusion cannot hold. The die forms every fin in one stroke, so pitch stays within tolerance across a run. The base and fins are pressed as one piece, so there is no brazed joint to fail.
Flatness on the mounting face is held directly from the tool. Because the base and fins are stamped as a one-piece geometry, the die sets the flatness, which keeps thermal interface contact uniform across the batch.
Does part cost increase with fin complexity?
A single stroke forms the whole custom spring headbands, so part cost stops scaling with complexity. The die forms every fin in one stroke, and tooling runs and the cycle feeds a line for repeatable volume programs.
What inspection documentation ships with each batch?
Every batch ships with a CMM report. Flatness on the mounting face is held directly from the tool, and hole position carries across the batch for repeatable volume programs, so the report reflects the tooled geometry.
Why is a one-piece stamped headband better for thermal contact?
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between the base and the fin, and there is no brazed joint to fail, which keeps thermal interface contact uniform.
Can hole position be held repeatably across a production batch?
Yes. Hole position carries across the batch for repeatable volume programs. Tooling runs and the cycle feeds a line, and the die forms every fin in one stroke, so pitch stays within tolerance across a run.
What should I specify when ordering custom spring headbands?
Specify the one-piece base-and-fin geometry, fin pitch within tolerance across a run, flatness on the mounting face held directly from the tool, and hole position for your volume program. Every batch ships with a CMM report.