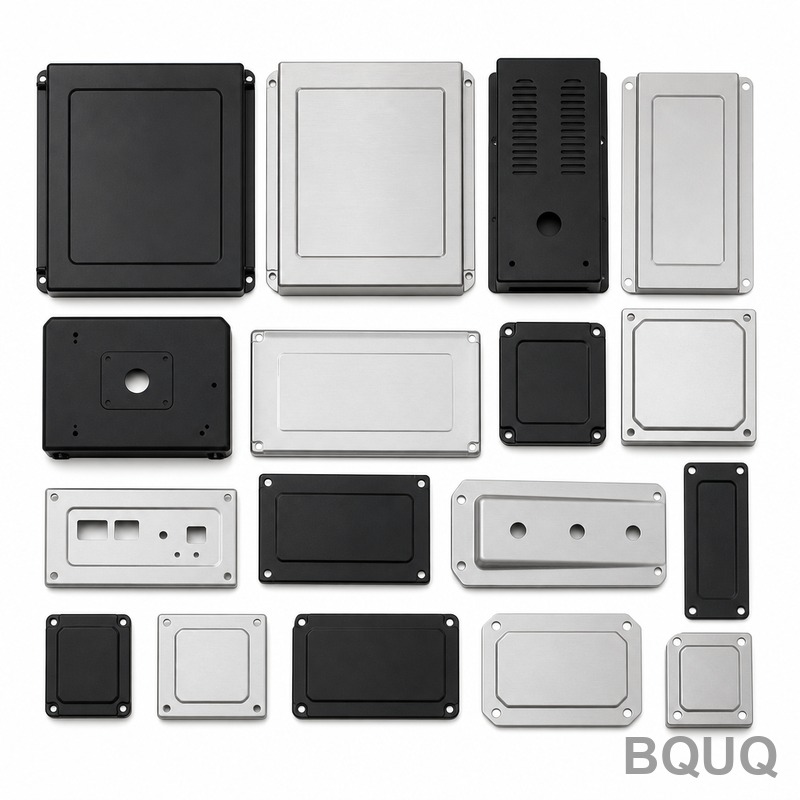
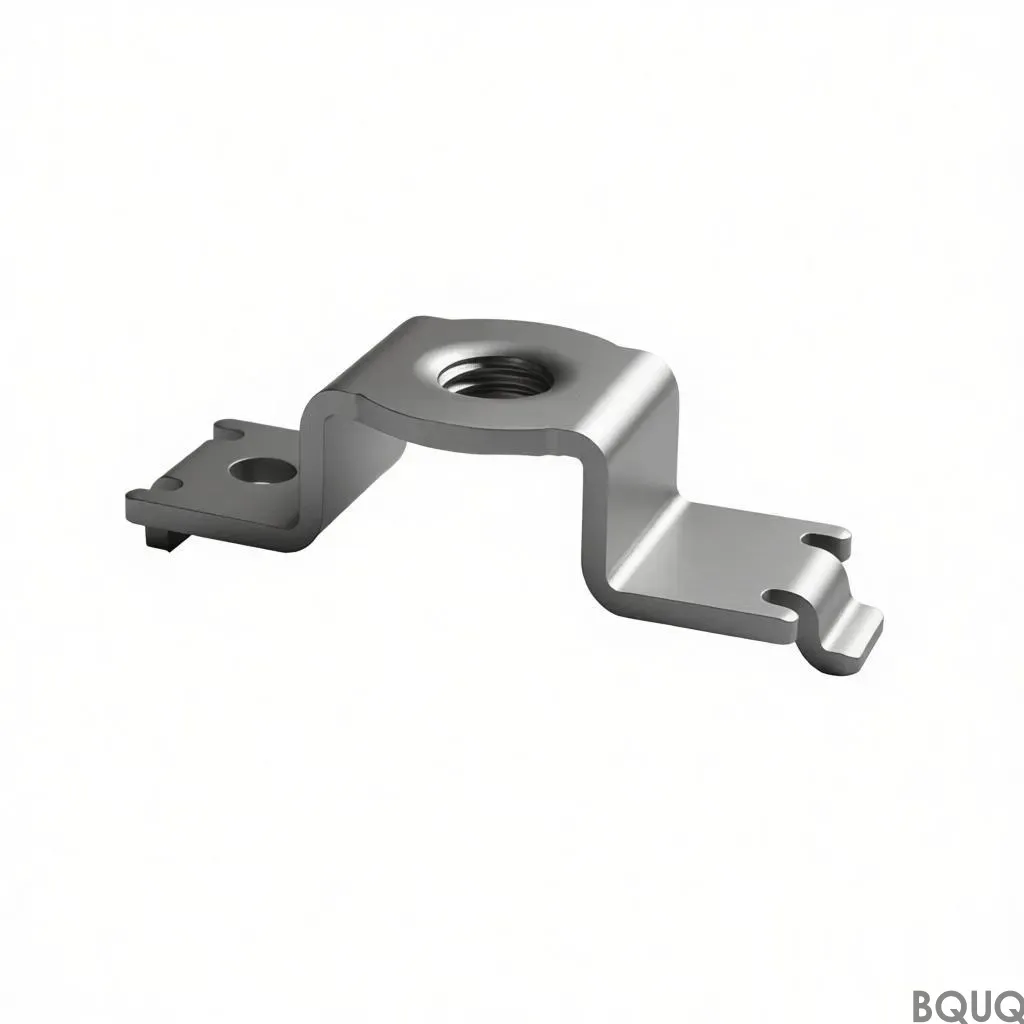
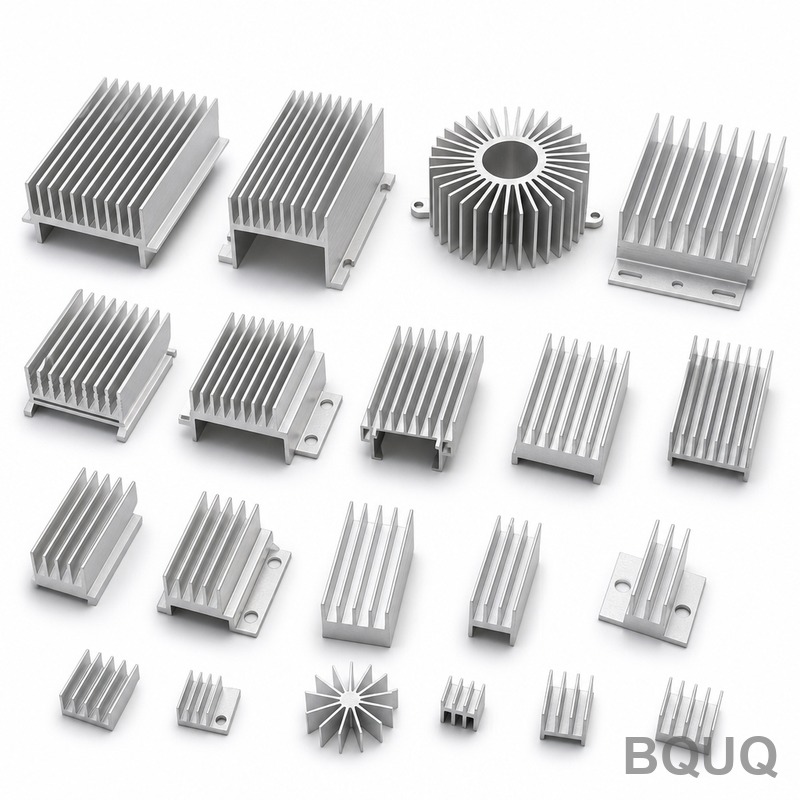
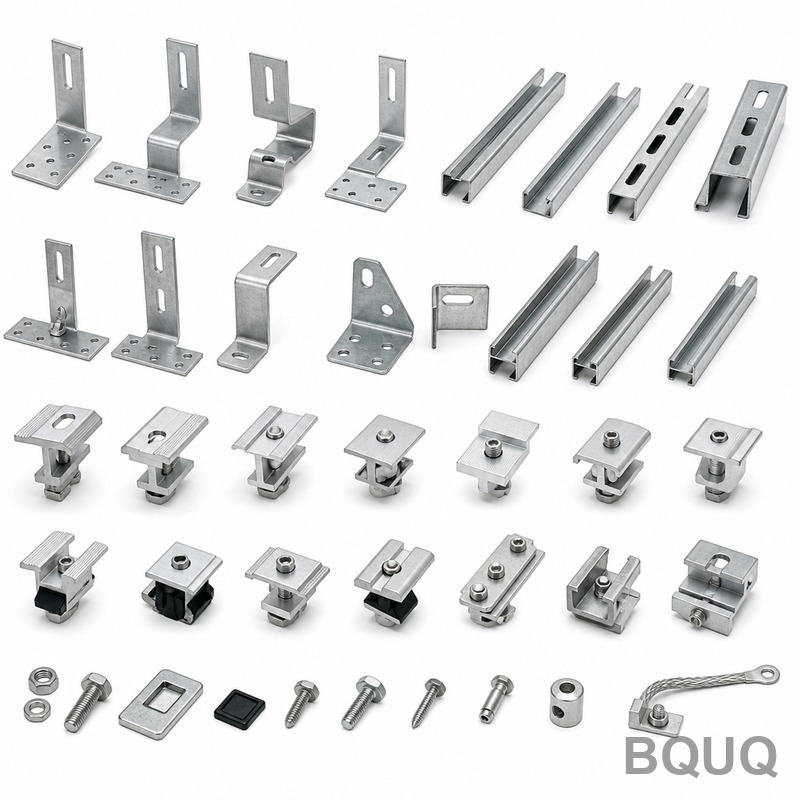
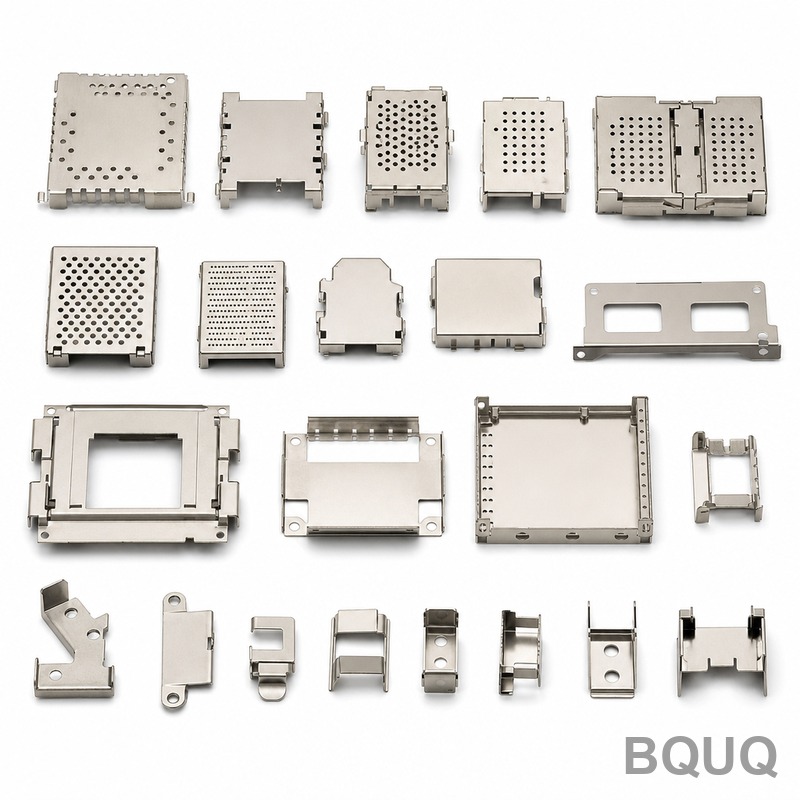
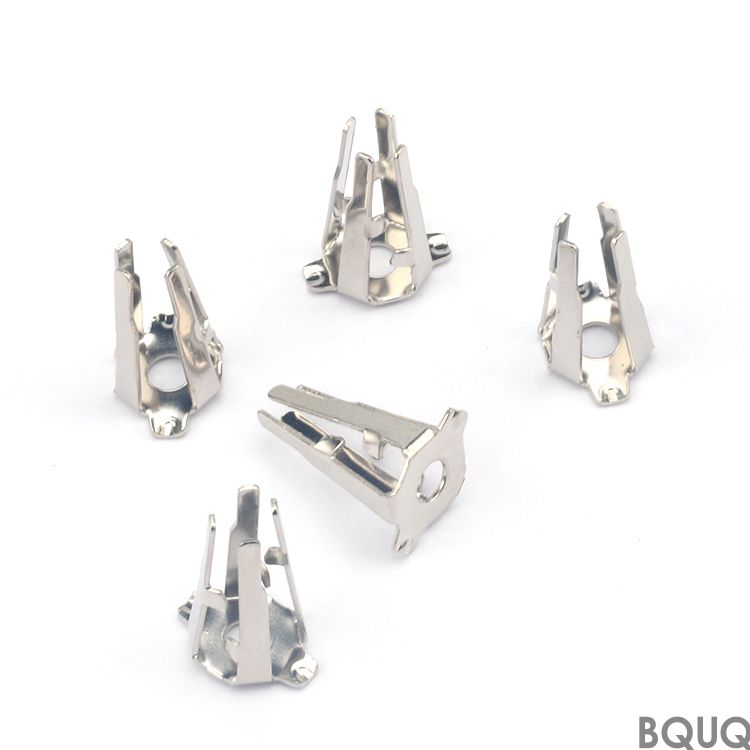
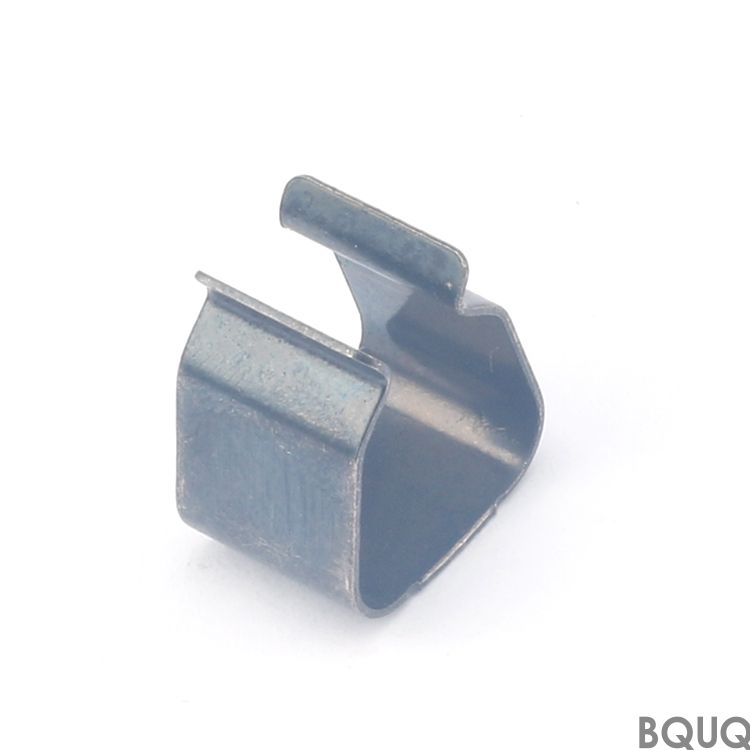
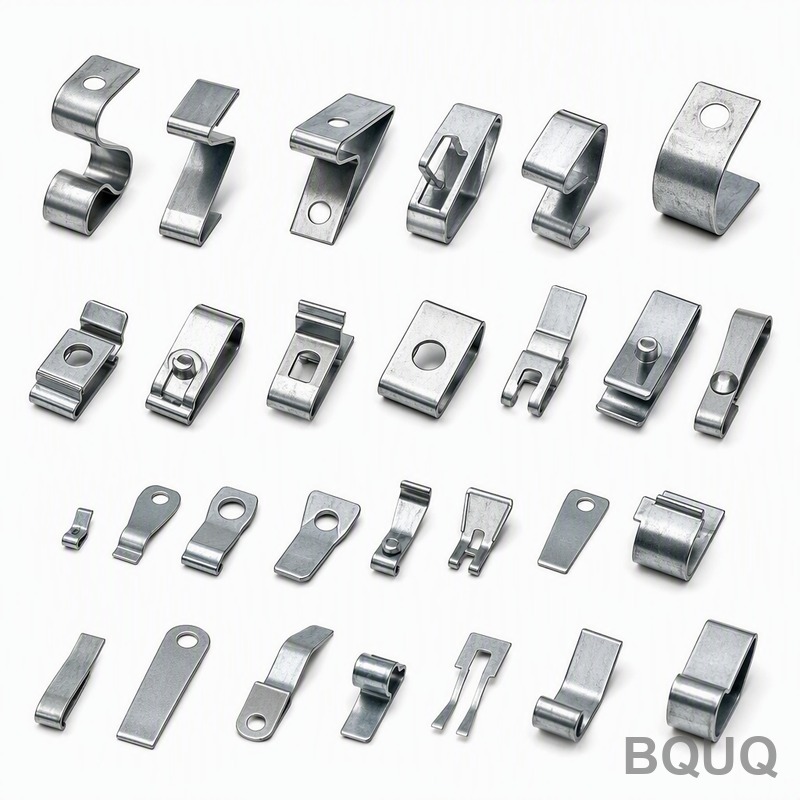
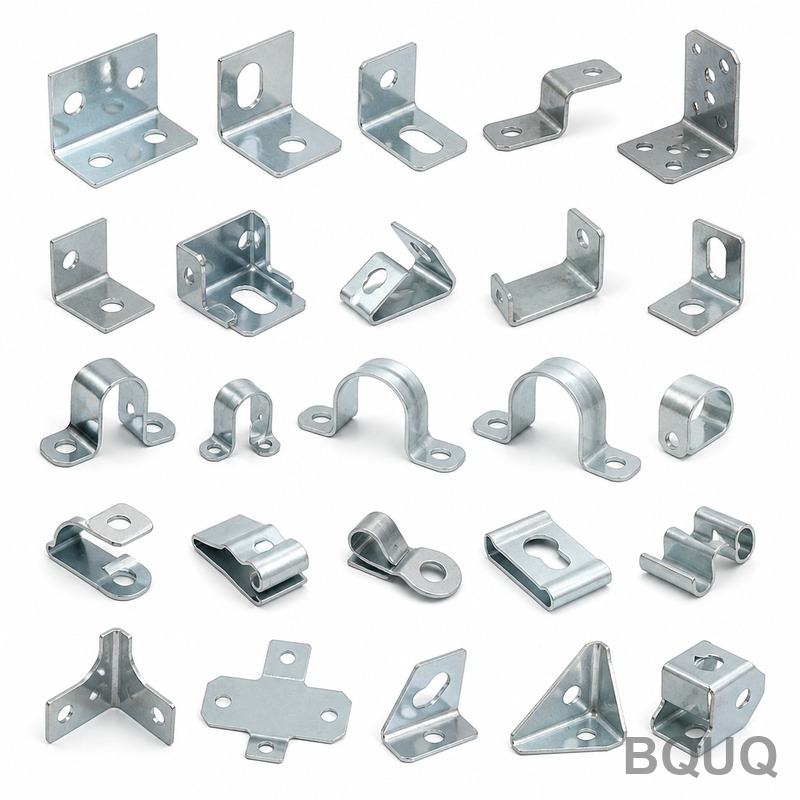
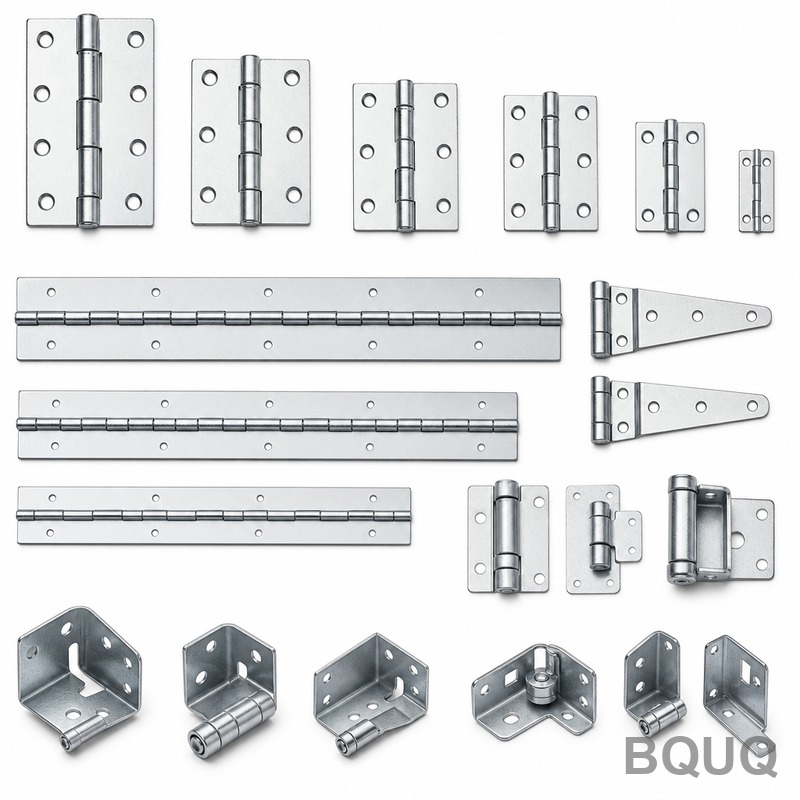
This is a stamped sheet metal enclosures covers collection built for brackets and mounts that must hold alignment under vibration and thermal cycling. You get stamped parts with ±0.05 mm positional t
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a stamped sheet metal enclosures covers collection built for brackets and mounts that must hold alignment under vibration and thermal cycling. You get stamped parts with ±0.05 mm positional tolerance, flatness within 0.1 mm per 100 mm, and surface finish down to Ra 0.8 µm — without waiting for CNC cycles. Typical lead time is 7 days for standard tooling, and we run hardness up to 45 HRC on spring steel variants.
Why Stamped Brackets Beat Machined Mounts at Volume
Stamping is a shear-and-form process, not a cutting process. For brackets and mounts with wall thicknesses from 0.3 mm to 6.0 mm, stamping produces identical parts at 40 to 60 strokes per minute. Compare that to CNC machining at 1 to 3 minutes per piece. At 10,000 pieces, stamping saves you roughly 80% of the per-unit cost. Tooling amortization breaks even at 2,000 units for most geometries. We hold burr height under 0.05 mm on all cut edges — that is the number that kills assembly line fit.
Die Design Rules That Prevent Springback Distortion
Springback is the enemy of stamped brackets. After the punch withdraws, the metal relaxes and the bend angle opens up by 1 to 3 degrees. We counter this with coining steps in the die — a secondary squeeze that sets the grain structure. For 90-degree bends in 1.5 mm cold-rolled steel, we hold angle tolerance to ±0.5 degrees. For high-strength alloys like 301 stainless, we add a 2-degree overbend in the tool. Every die is validated with a 50-piece first article before production. That first article goes to you with a full CMM report.
Materials and Heat Treatment We Use for Mounts
| Spec | Value | |------|-------| | Material options | SPCC, SECC, SUS301, SUS304, 5052 aluminum, 65Mn spring steel | | Thickness range | 0.3 mm to 6.0 mm | | Hardness (as stamped) | 80-90 HRB (SPCC), 140-180 HV (SUS301) | | Hardness (after heat treat) | 40-45 HRC (65Mn spring steel) | | Positional tolerance | ±0.05 mm | | Flatness | 0.1 mm per 100 mm | | Surface finish Ra | 0.8 µm (stamped), 0.4 µm (on request) | | Burr height | ≤0.05 mm | | Lead time (standard tooling) | 7 working days | | MOQ | No MOQ — 1 piece to 1 million pieces |
We stock coil steel in 12 standard gauges. For outdoor enclosures, we offer SECC (electro-galvanized) with a 72-hour salt spray rating. For high-temperature mounts near motors, use SUS304 with a 800°C continuous service limit. If you need spring-back resistance in a latch or clip, 65Mn with oil quenching hits 45 HRC without losing ductility.
Secondary Operations: Tapping, Riveting, and Heat Sink Bonding
A stamped bracket is rarely the final part. We integrate secondary operations in-house to cut your supply chain. We tap holes from M2 to M12 with a 6H thread class — that is a snug fit for standard bolts. We press-in PEM nuts at 5,000 parts per hour with pull-out force verified to spec. For power electronics mounts, we bond aluminum heat sinks to stamped steel brackets using thermally conductive epoxy, achieving 2.0 W/mK thermal interface. This is where our 20 years of heat sink manufacturing pays off — you get a structural mount that also dissipates 30% more heat than a bare bracket.
Inspection Before Every Shipment: CMM and Hardness Reports
Every lot gets a sampling per ISO 2859-1, Level II. We measure critical bend angles with a digital protractor to 0.1 degrees. We check hole positions with a CMM (Coordinate Measuring Machine) accurate to ±0.002 mm. For spring steel parts, we run a Rockwell hardness test on every 100th piece. You receive a digital inspection report with each shipment — no extra charge. If a dimension drifts, we stop the press, re-shim the die, and re-run the first article. That is how we keep a 99.2% first-pass yield across our stamped product line.
Packaging and Delivery for Stamped Parts
Small brackets under 50 mm go into anti-static bags, 500 pieces per bag, then into double-wall cartons. Larger mounts over 200 mm are separated by corrugated dividers to prevent surface scratches. We laser-mark each part with a batch code if you need traceability for automotive or medical audits. Shipping is via DHL or FedEx for orders under 50 kg. For container loads, we use palletized export crates with a 500 kg capacity. Standard delivery is 7 days for tooled parts, 15 days for new dies. We quote freight at cost — no markup.
Why Our Dongguan Factory Keeps Your Tolerances Tight
We are a precision manufacturing facility in Dongguan, China, with 20 years of continuous operation. Our press shop runs 16 machines from 25 tons to 250 tons. We make our own dies in-house, so tooling modifications take 48 hours, not weeks. Because we also do CNC machining and springs, we can combine stamped brackets with machined pins or custom coil springs in one assembly — one purchase order, one quality system. This is the difference between buying a stamped part and buying a solved mounting problem.
What is the minimum order quantity for stamped brackets?
There is no MOQ — we prototype a single stamped part and scale to one million pieces without changing the die.
Can you stamp parts from my existing CAD file without a factory drawing?
Yes — send your STEP or DXF file, and our tooling engineers will design the die and add bend reliefs within 24 hours.
How do you guarantee quality on high-volume stamping runs?
We use in-die sensors that measure strip thickness and punch wear every stroke, and we perform CMM verification on the first article plus hourly patrol inspections.
What is the fastest lead time for a custom stamped mount?
For a simple bracket with existing tooling, we ship in 7 days; for a new die with complex bends, we quote 15 days including tool tryout.
Send your drawing today for a firm quote within 12 hours. Email sc@bquq.com or WhatsApp +86 13713157787. We will reply with a unit price, tooling cost, and a DFM (Design for Manufacturing) review — free of charge.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.