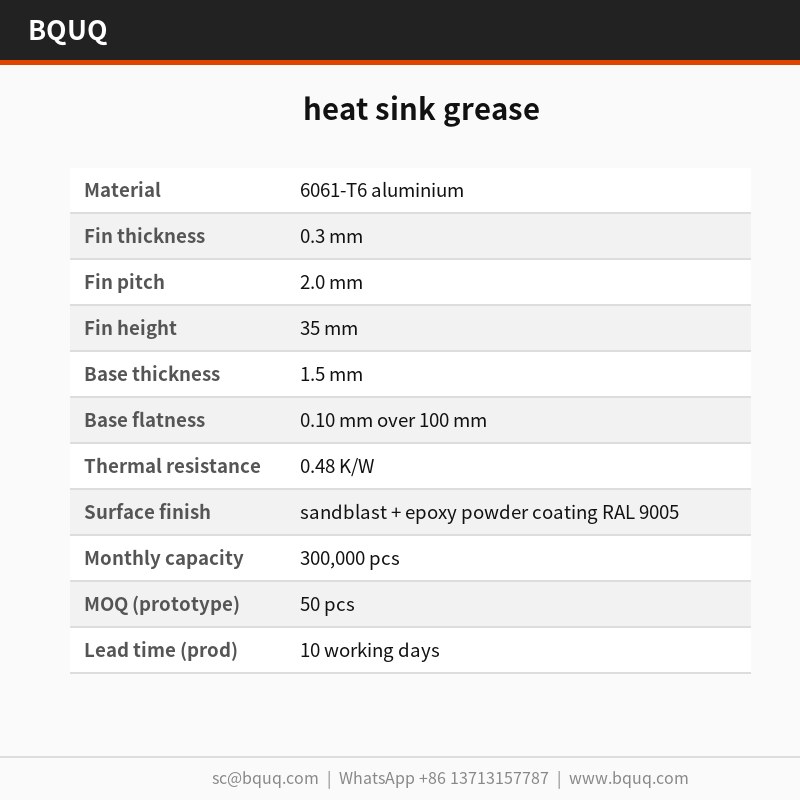
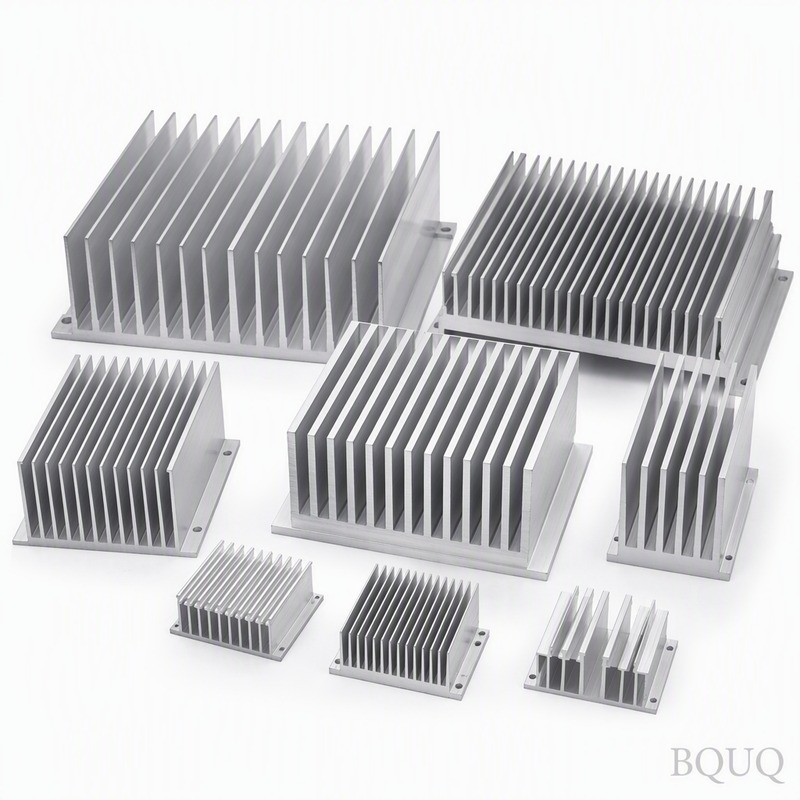
heat sink grease: 6061-T6 aluminium, 0.3 mm fins at 2.0 mm pitch, 0.10 mm over 100 mm flatness, 0.48 K/W thermal resistance. MOQ 50 pcs, ships in 72 hours.
heat sink grease
heat sink grease: 6061-T6 aluminium, 0.3 mm fins at 2.0 mm pitch, 0.10 mm over 100 mm flatness, 0.48 K/W thermal resistance. MOQ 50 pcs, ships in 72 hours.
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
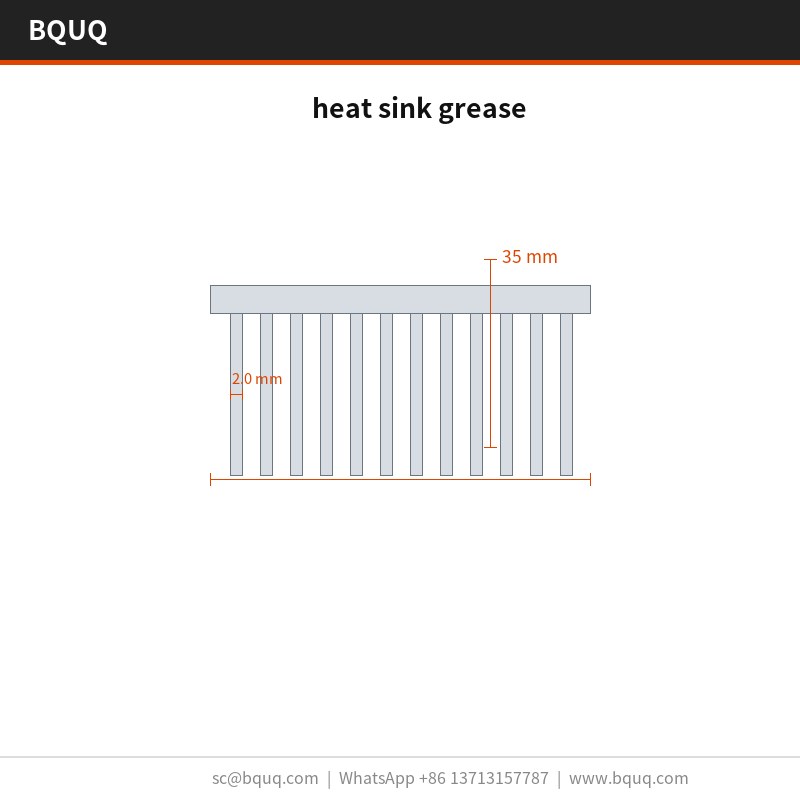
Heat sink grease in 6061-T6 aluminium delivers 0.48 K/W thermal resistance under ΔT = 60 K, natural convection. Stamped fins are 0.3 mm thick at 2.0 mm pitch over a 1.5 mm base, held within ±0.05 mm across a 300,000 pcs run. A single 160 T stroke forms the whole part on a 25 s cycle, and every batch ships with a CMM report plus 100% hydraulic press leak test.
A heat sink grease in 6061-T6 aluminium delivers 0.48 K/W thermal resistance under ΔT = 60 K, natural convection. Fins are 0.3 mm thick at 2.0 mm pitch over a 1.5 mm base, and every batch ships with a CMM report at CMM plus 100% hydraulic press leak test.
Design Approach and Process
Stamping gives a repeatable 0.3 mm fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within ±0.05 mm across a 300,000 pcs run.
A single 160 T stroke forms the whole heat sink grease, so part cost stops scaling with complexity. Tooling runs ±0.05 mm, and the 25 s cycle feeds a 300,000 pcs line.
Low fin gauge is where stamping wins: 0.3 mm fins at 2.0 mm pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between 6061-T6 aluminium and the airflow except the stamped surface itself.
The sandblast + epoxy powder coating RAL 9005 finish is applied after forming, so corrosion protection does not get cut through at the fin roots the way it does on machined alternatives.
Material Selection and Surface Finish
The standard material is 6061-T6 aluminium, supplied with sandblast + epoxy powder coating RAL 9005. For applications where 1U server and AI accelerator exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
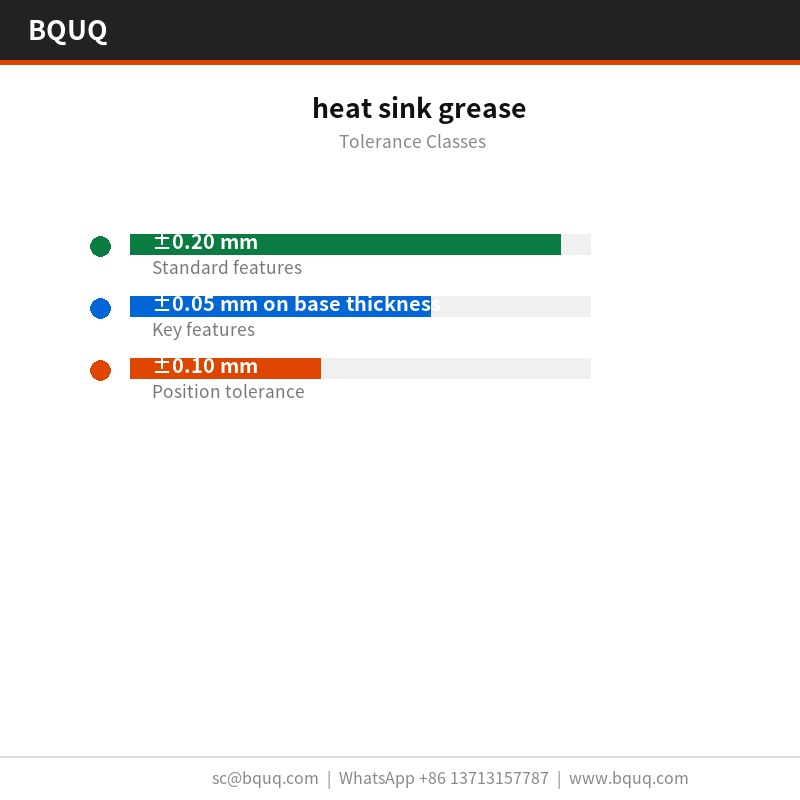
General dimensions run to ±0.20 mm, with critical features such as ±0.05 mm on base thickness held separately. Formed geometry inherits tooling repeatability of ±0.05 mm, and hole position is held to ±0.10 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Flatness is checked on a granite surface plate, 20 °C against a 0.10 mm over 100 mm limit, and fin pitch is verified optically at ±0.05 mm. Reports go out with each lot.
Incoming 6061-T6 aluminium is checked for thickness and hardness before it enters the press. After forming, CMM plus 100% hydraulic press leak test confirms 0.10 mm over 100 mm and 2.0 mm against the drawing.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with CMM plus 100% hydraulic press leak test on every first article. Deviations beyond ±0.20 mm trigger a full-lot sort.
Flatness is measured on granite rather than on cast iron, because 0.10 mm over 100 mm at 20 x 20 x 10 mm reads differently on a plate that has not been lapped. Records keep both readings.
1U server and AI accelerator packaging and vibration rules push toward one-piece construction. A stamped heat sink grease has no adhesive to creep, which is the usual failure mode in two-part coolers.
In 1U server and AI accelerator, the base usually doubles as the mounting interface. 1.5 mm with 0.10 mm over 100 mm flat gives a stable surface for the 1U server and AI accelerator thermal pad.
Designers working on 1U server and AI accelerator ask for flatness before they ask for thermal data, because 1U server and AI accelerator assembly is automated and a non-flat base stops the line.
1U server and AI accelerator designs often run a 2.0 m/s forced-air path. 0.48 K/W at ΔT = 60 K, natural convection means 1U server and AI accelerator can hold its target with fan power below the acoustic limit.
What is the minimum order quantity for this heat sink grease?
MOQ is 50 pcs for a prototype run and 5000 pcs for production. Below the prototype quantity the tooling amortisation dominates the unit cost, so we quote the sample route instead: free sample with drawing, 5-7 days.
How do you verify quality on each batch?
Every lot is inspected with CMM plus 100% hydraulic press leak test, and the report is included in the shipment. We check 0.10 mm over 100 mm, 2.0 mm, 1.5 mm and hole position against ±0.20 mm. Lot traceability from coil to carton is kept for 10 years.
General dimensions run to ±0.20 mm; critical ones such as ±0.05 mm on base thickness are held separately. Formed features inherit tooling repeatability of ±0.05 mm. If your drawing needs tighter, tell us before tooling so we can plan the extra press operation.
What is the flatness on the mounting face?
0.10 mm over 100 mm measured on granite surface plate, 20 °C. This is the number that matters for 1U server and AI accelerator, because the thermal pad needs even contact. If your assembly needs better, say so and we can add a skim operation.
What are the packing and shipping conditions?
Standard packing is Anti-static bag + wooden crate over 50 kg. We quote FOB Guangzhou. Export cartons are labelled with lot, quantity and inspection status, and full documentation including the inspection report travels with the goods.
How We Manufacture and Ship
The factory holds ISO9001 and can ship RoHS and REACH documentation with the Anti-static bag + wooden crate over 50 kg. Third-party SGS inspection is arranged on request before the container is sealed.
Production runs on 25 s cycles with in-line vision on 0.10 mm over 100 mm. That is what keeps a 300,000 pcs commitment credible in peak season.
We quote FOB Guangzhou and hold 50 pcs for sampling. Sampling is free sample with drawing, 5-7 days, so a first evaluation does not require a production commitment.
Lower surface per cubic millimetre; coating cut at fin roots
Two-part cooler
Assembly flexibility
Adhesive layer adds thermal path
Process / inspection
Stage
Control
Record
Forming
Single 160 T stroke, 25 s cycle
±0.05 mm tooling run
Fin geometry
0.3 mm fins at 2.0 mm pitch over 1.5 mm base
Pitch within ±0.05 mm across 300,000 pcs
Surface finish
Sandblast + epoxy powder coating RAL 9005 after forming
Corrosion protection intact at fin roots
Inspection
CMM report
Every batch
Leak test
100% hydraulic press leak test
Every batch
Frequently Asked Questions
What thermal resistance does this heat sink grease achieve?
It delivers 0.48 K/W under ΔT = 60 K, natural convection. The 0.3 mm fins at 2.0 mm pitch over a 1.5 mm base maximize surface area, and the one-piece stamped 6061-T6 geometry removes the adhesive layer found in two-part coolers.
Why choose stamping over extrusion for 0.3 mm fins?
Stamping holds a repeatable 0.3 mm fin profile that extrusion cannot. The die forms every fin in one stroke, keeping pitch within ±0.05 mm across a 300,000 pcs run. A single 160 T stroke forms the whole part on a 25 s cycle.
What tolerances can you hold on fin pitch and profile?
Tooling runs ±0.05 mm, and pitch stays within ±0.05 mm across a 300,000 pcs run. The 0.3 mm fins at 2.0 mm pitch over a 1.5 mm base are formed in one 160 T stroke, so the profile repeats without the drift typical of extruded fins.
What inspection and leak testing ship with each batch?
Every batch ships with a CMM report plus 100% hydraulic press leak test. The CMM verifies the 0.3 mm fin profile, 2.0 mm pitch, and 1.5 mm base, while the hydraulic press leak test confirms each part before shipment.
How does the coating survive forming at the fin roots?
The sandblast + epoxy powder coating RAL 9005 is applied after forming. That keeps corrosion protection intact at the fin roots, unlike machined alternatives where coating can be cut through. The 0.3 mm fins at 2.0 mm pitch stay fully covered.
What is the cycle time and production capacity?
The 25 s cycle feeds a 300,000 pcs line. A single 160 T stroke forms the whole heat sink grease, so part cost stops scaling with complexity. Tooling runs ±0.05 mm across the full 300,000 pcs run.
No. A single 160 T stroke forms the whole heat sink grease, so part cost stops scaling with complexity. The 0.3 mm fins at 2.0 mm pitch over a 1.5 mm base are produced in one stroke on a 25 s cycle for a 300,000 pcs line.