OpeningYour drawing defines the part. We machine it. Before shipment, every collet chuck is verified on a CMM and a runout tester. You get a part that fits your spindle and holds y
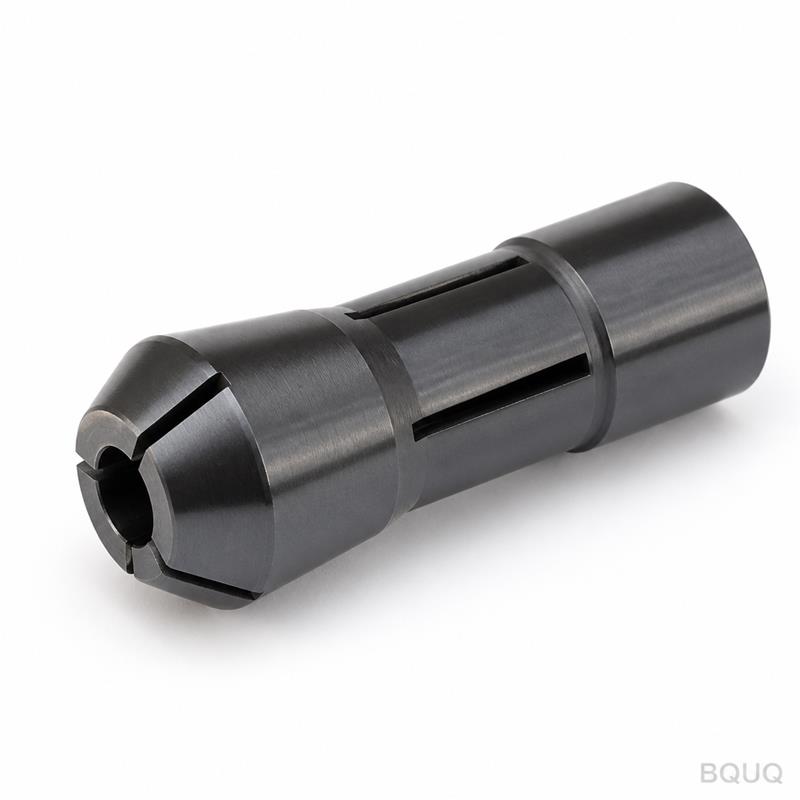
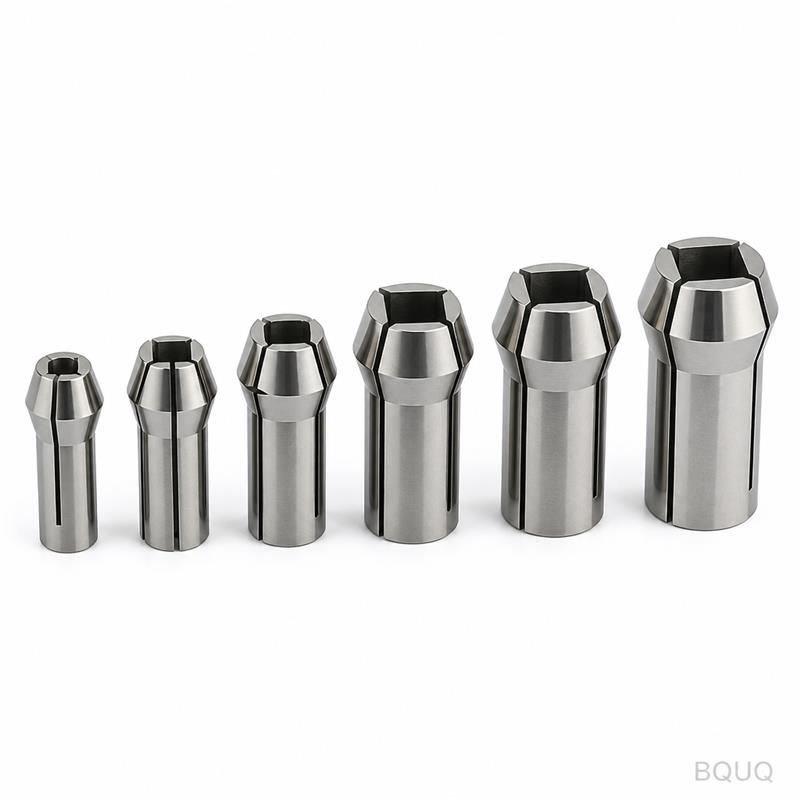
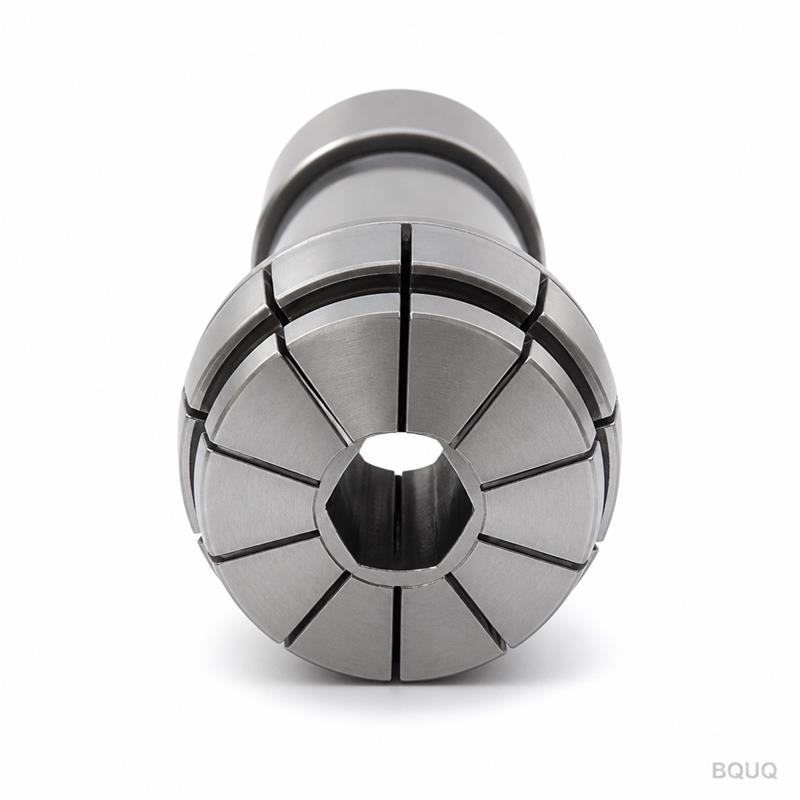
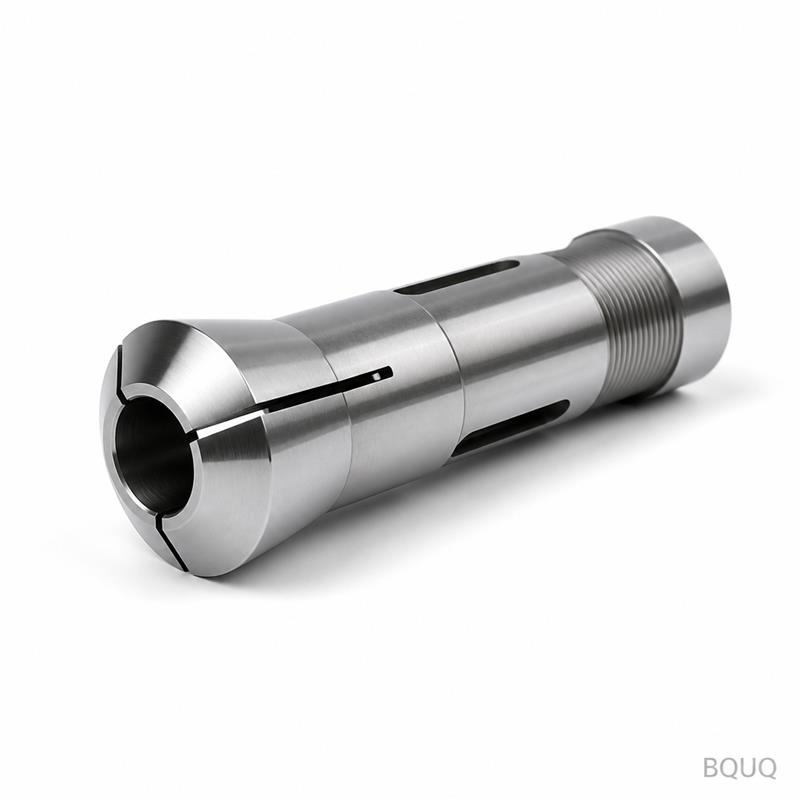
Custom CNC Collet Chuck 36 Type Quenched Dark, Made to Drawing
OpeningYour drawing defines the part. We machine it. Before shipment, every collet chuck is verified on a CMM and a runout tester. You get a part that fits your spindle and holds your workpiece true.T
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
Your drawing defines the part. We machine it. Before shipment, every collet chuck is verified on a CMM and a runout tester. You get a part that fits your spindle and holds your workpiece true.
Tolerance: 0.005 mm on bore and taper
Runout: ≤ 0.008 mm TIR at nose
Lead time: 15–20 working days after drawing approval
No MOQ: one piece or one thousand, same process control
This is a 36-type auto lathe collet chuck, hardened and quenched to a dark finish. The dark oxide layer reduces glare and adds mild corrosion resistance. It is built for high-speed, high-repeatability clamping in sliding-head and fixed-head automatic lathes.
Specifications
Parameter
Value
Material
AISI 4140 or 8620, or per your spec
Hardness
58–62 HRC (quenched and tempered)
Surface finish
Dark oxide (black) or plain ground
Bore tolerance
+0.005 / 0 mm
Taper accuracy
AT3 or better per DIN 55026
Runout (TIR)
≤ 0.008 mm at nose, ≤ 0.005 mm at bore
Roundness
≤ 0.003 mm
Surface roughness
Ra 0.4 µm on taper, Ra 0.8 µm elsewhere
Machining
CNC turning, internal grinding, OD grinding
Inspection
100% CMM, runout test, hardness test per batch
Batch size
1–10,000 pcs, no MOQ
Lead time
15 days for prototypes, 20 days for production
Country of origin
Made in China, Dongguan factory
We use precision manufacturing methods: CNC turning for the blank, then heat treatment, then finish grinding on the taper and bore. The quenched dark finish is applied after grinding, so it does not affect dimensional accuracy.
Three reasons buyers send us their drawings
1. Batch-traceable quality.
Every heat lot is logged. Every part gets a serial number. If you need to trace a batch back to raw material, heat treatment furnace, and operator, we have the records. No guesswork.
2. Inspection report per batch.
You get a dimensional report with actual measured values, not just a pass/fail stamp. We include runout, taper angle, bore diameter, hardness, and surface roughness. For critical orders, we can add a video of the CMM measurement.
3. One factory for CNC, stamping, springs, and heat sinks.
Your collet chuck is not an isolated part. If your assembly also needs a stamped washer, a compression spring, or a heat sink for the drive electronics, we make all of them under one roof. One purchase order, one quality system, one shipping date.
Where these parts are used
A 36-type collet chuck is common in Swiss-type and automatic lathes. Typical applications:
Medical device components: Small titanium and stainless parts that need repeatable clamping without marking.
Watch and jewelry production: Pinion gears, stems, and cases where runout below 0.01 mm is mandatory.
Electronic connectors: Brass and copper pins, sockets, and terminals produced at high spindle speeds.
Automotive fuel injectors: Needle valves and nozzle bodies that require concentric clamping over long production runs.
Aerospace fasteners: Small-diameter bolts and inserts made from heat-treated alloys.
The dark quenched finish is often specified for toolroom environments where light reflection interferes with optical inspection. It also helps the chuck resist light rust during storage.
Q: Is there a minimum order quantity?
No. We machine one prototype or a full production batch with the same setup discipline. Many buyers start with one piece to verify fit and runout, then scale up.
Q: How do you guarantee tolerance and quality?
We grind the taper and bore after heat treatment. Then we measure every part on a CMM and a runout tester. The inspection report is included with the shipment. If a part is out of spec, we replace it at no cost.
Q: What is the lead time for a custom CNC collet chuck?
Standard lead time is 15 working days for a prototype, 20 working days for production quantities. If you need a rush, we can often compress to 10 days for a small batch.
Q: Can you provide material certificates and heat treatment reports?
Yes. We supply mill certificates for the raw material and a heat treatment report with hardness values and furnace logs. All documents are in English.
Send your drawing
Send us your 2D drawing or 3D model. We will review the taper, bore, and material spec, then send you a firm quote within 12 hours.
Email: sc@bquq.com
WhatsApp: +86 13713157787
No MOQ. No minimum order value. Just a precise, quenched dark collet chuck made to your drawing, verified before shipment.