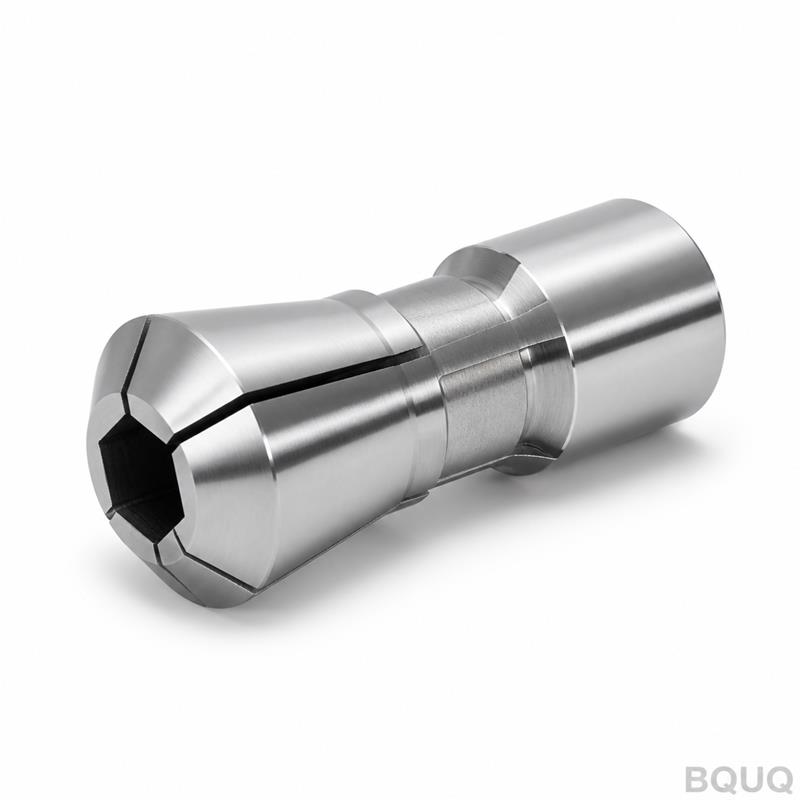
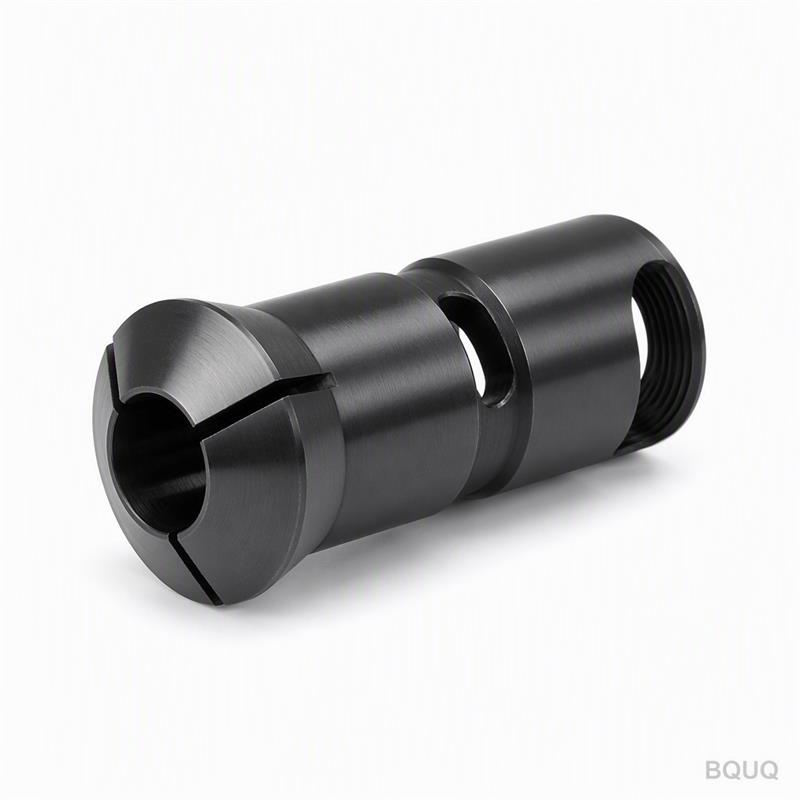
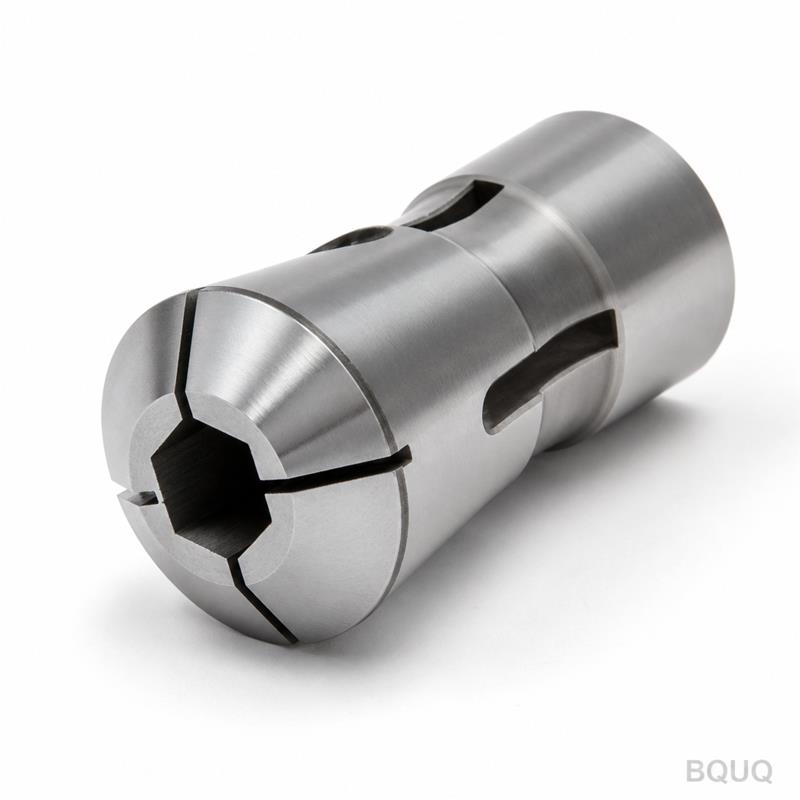
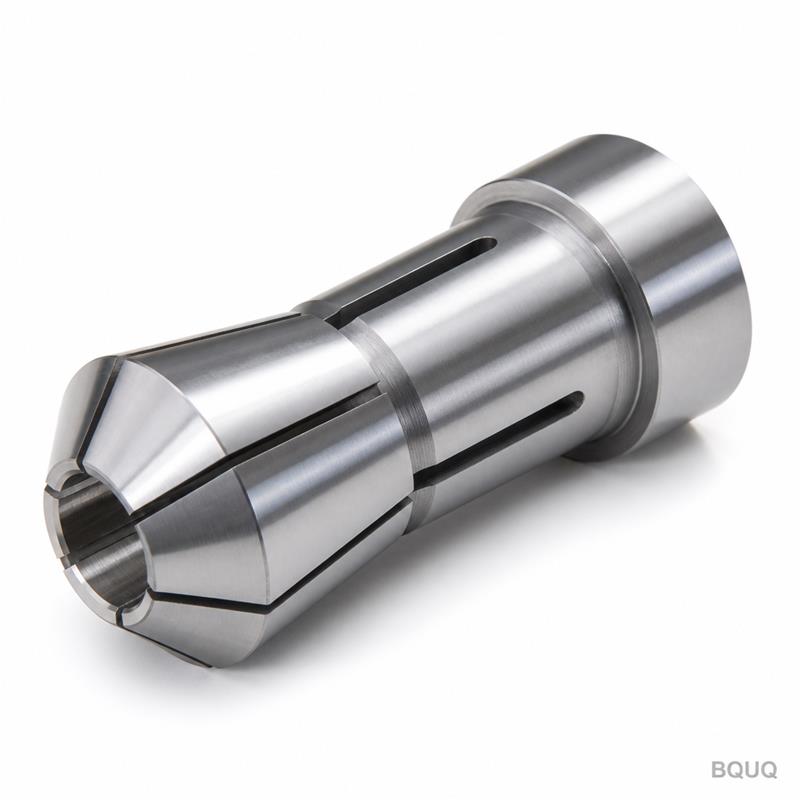
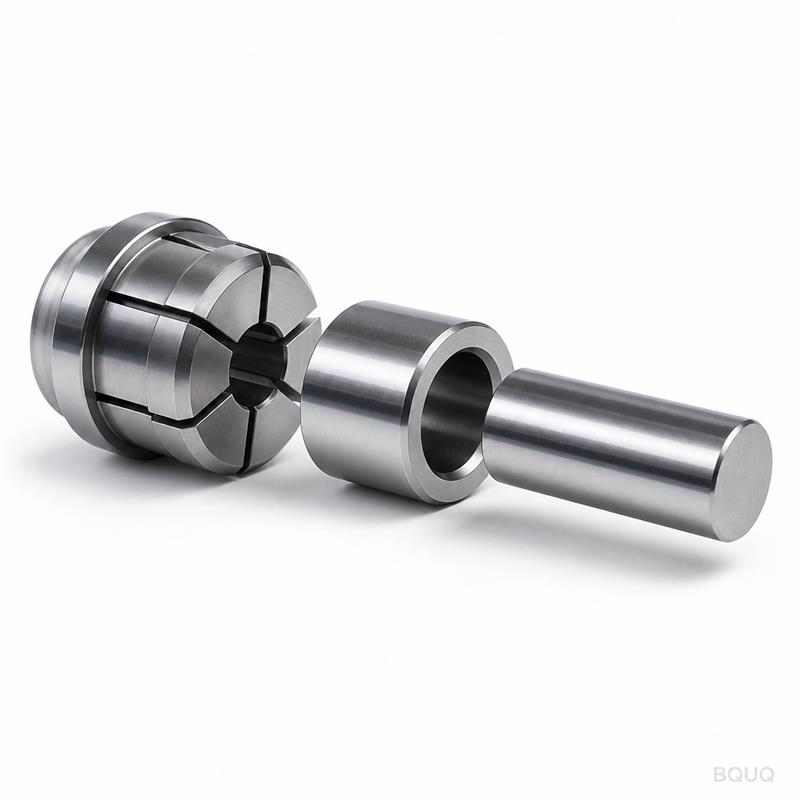
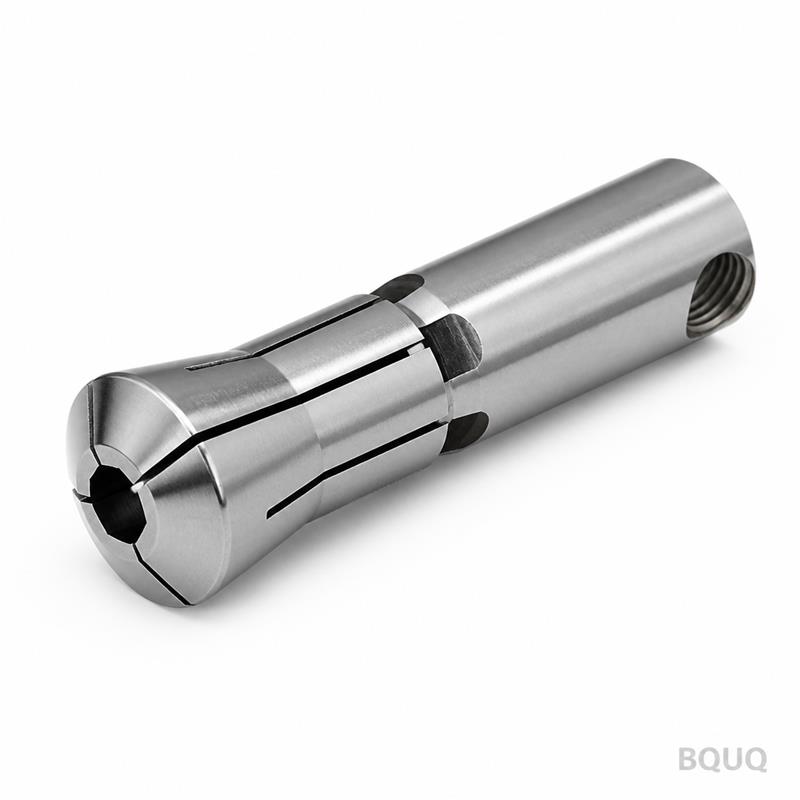
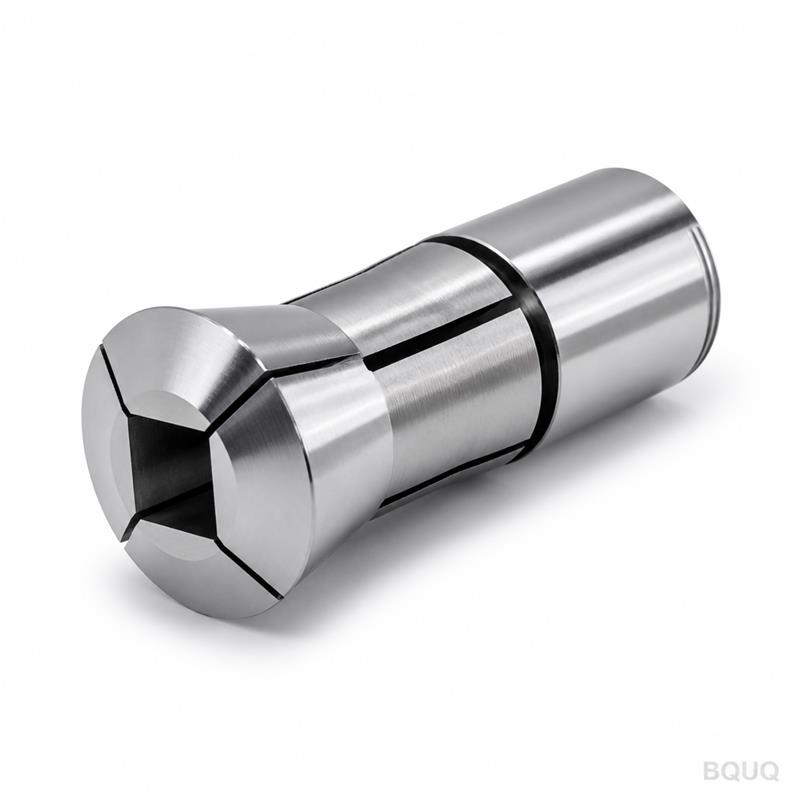
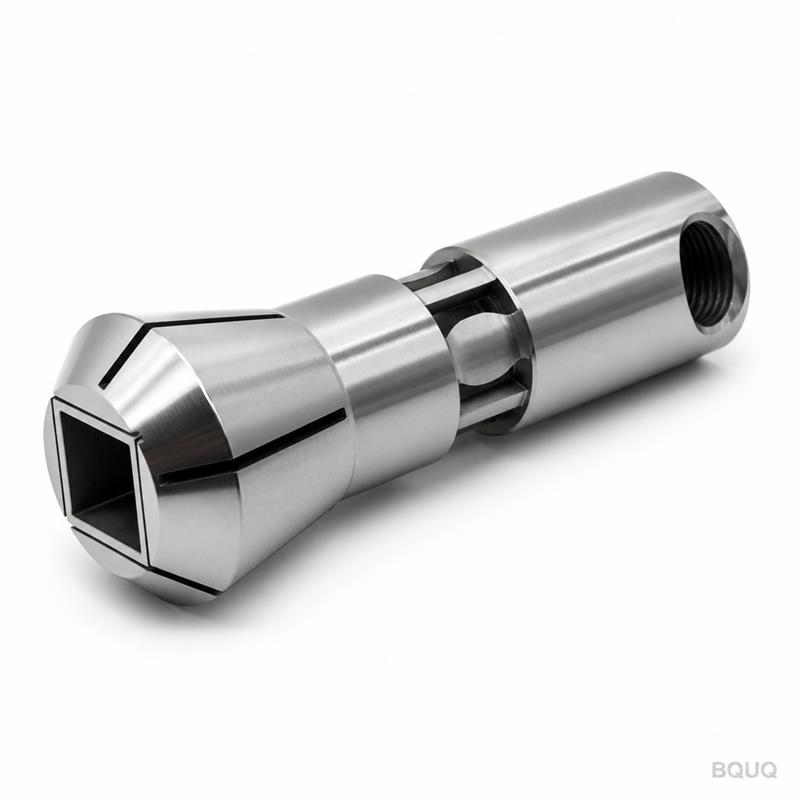
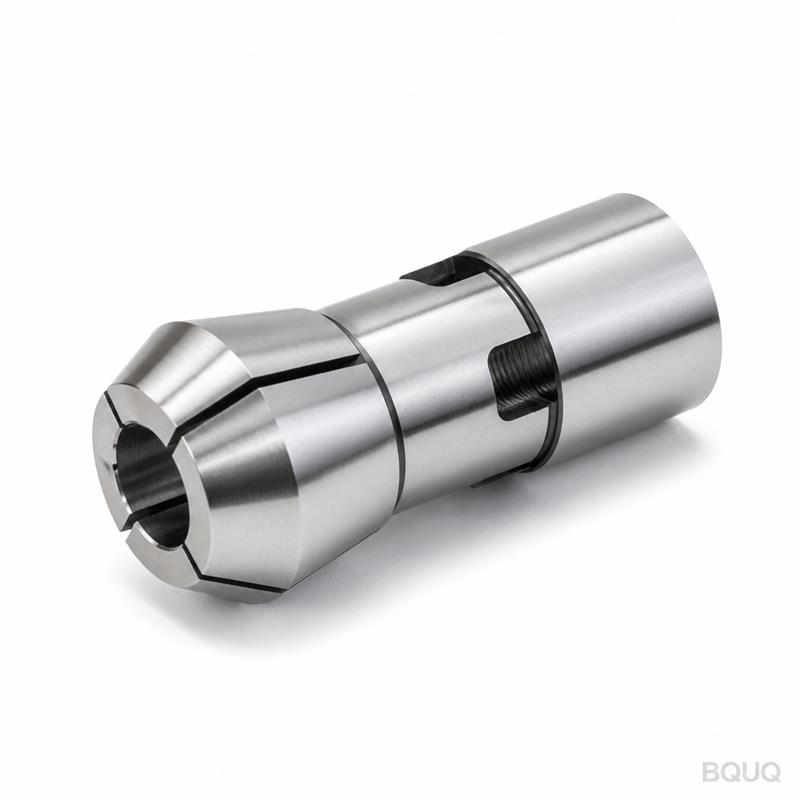
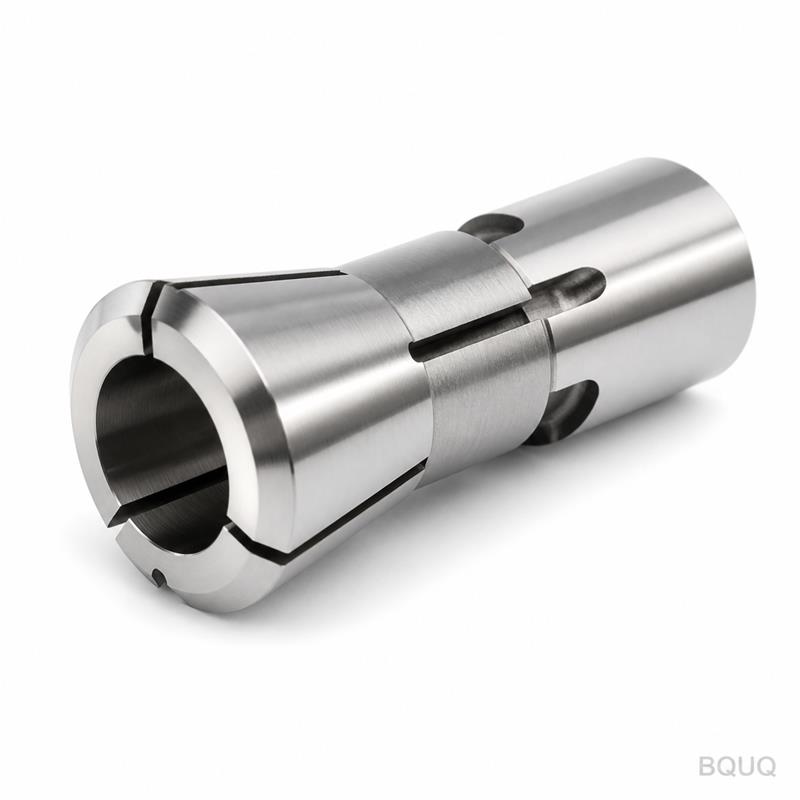
BQUQ CNC Machined Auto Lathe 36 Type Quenched Dark Collet Chuck
What This Chuck Is and Why It Cuts Your Reject Rate This is a CNC machined auto lathe 36 type collet chuck, hardened and finished in a dark oxide (quenched dark) surface. You get 0.005 mm total runout
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
What This Chuck Is and Why It Cuts Your Reject Rate
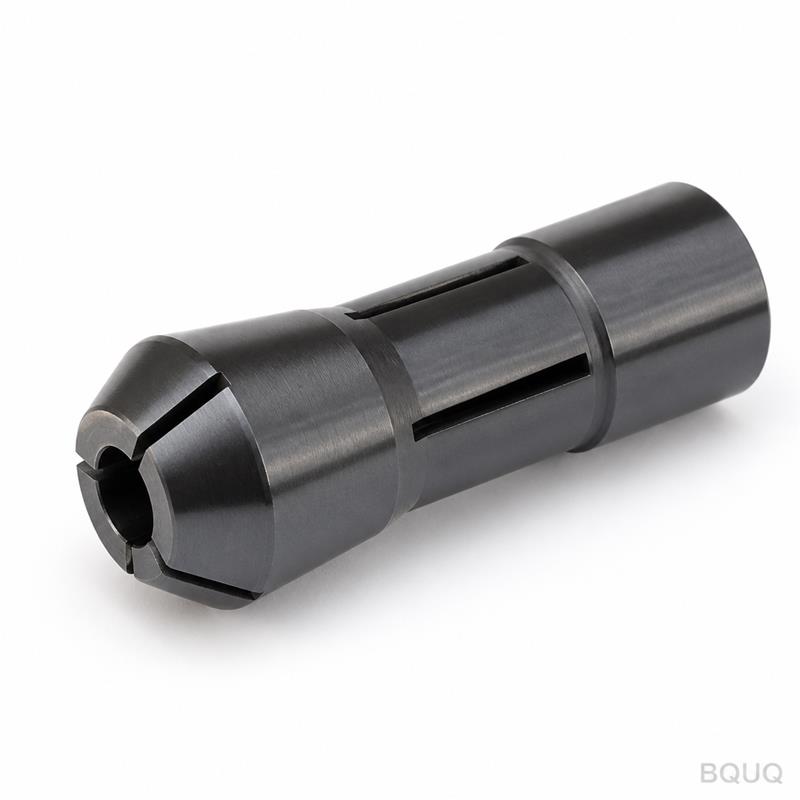
This is a CNC machined auto lathe 36 type collet chuck, hardened and finished in a dark oxide (quenched dark) surface. You get 0.005 mm total runout at the nose and 0.008 mm at 3× diameter from the face. Hardness is locked at HRC 58-62 across the gripping bore. Lead time for standard sizes is 7 working days. That means your spindle stops wobbling, your parts stop drifting, and your scrap bin stays empty.
How the 36 Type Profile Matches Your Auto Lathe Spindle Nose
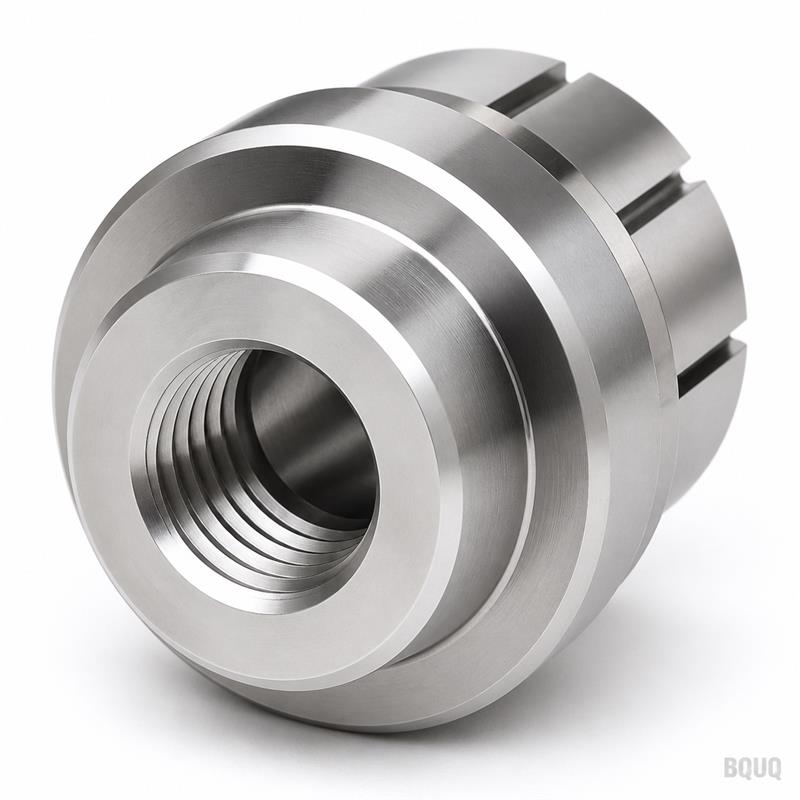
The 36 type refers to the DIN 6343-36 mounting profile, which fits common auto lathes (Citizen, Star, Tsugami, and many Taiwanese clones). The taper angle is 16° included, the thread is M36×1.5, and the back face registers flat against your spindle with a 0.002 mm perpendicularity check. We machine the taper and the thread in one clamping on a DMG MORI NTX 2000, so there is no transfer error between the two critical features. If your spindle is not exactly 36 type, send us your drawing—we can modify the back end without changing the gripping geometry.
Quenched Dark Finish vs. Plain Hardened Steel
The dark finish is not paint. It is a black oxide conversion coating applied after heat treatment and final grinding. This layer is 0.5 to 1.5 microns thick, which does not change the bore dimension. Benefits are real: it holds a thin film of oil for rust prevention, reduces galling when you slide the collet into a warm spindle, and makes surface inspection easier under shop lights because glare drops. We do not skip the quench step—the entire body is vacuum hardened and then double tempered, not just case hardened. Core hardness is HRC 58-62, and the gripping slots are wire-cut after hardening so the spring fingers keep their elasticity.
Gripping Bore Tolerance and Surface Finish You Can Measure
The gripping bore is ground to a H6 tolerance. For a 10 mm collet, that means the bore is 10.000 to 10.009 mm. Surface finish on the bore is Ra 0.2 μm, and the taper is Ra 0.4 μm. Runout between the bore and the taper is held to 0.005 mm TIR. We do not round these numbers up. Every collet is measured on a Zeiss Contura CMM with a 0.1 μm resolution probe, and the report is attached to your shipment. If you need a tighter bore for a specific material (brass, aluminum, steel), we can grind to H5 on request, but that adds 2 days to the lead time.
Specification
Value / Range
Type
DIN 6343-36 (auto lathe 36 type)
Material
GCR15 (AISI 52100) bearing steel
Hardness (core)
HRC 58-62
Gripping bore tolerance
H6 (e.g., 10.000–10.009 mm for Ø10)
Bore surface finish
Ra 0.2 μm
Taper surface finish
Ra 0.4 μm
Total runout (at nose)
0.005 mm TIR
Total runout (3×D from face)
0.008 mm TIR
Gripping range
Ø3 mm to Ø42 mm (depending on collet bore)
Lead time (standard sizes)
7 working days
MOQ
No MOQ (single piece accepted)
Surface finish (external)
Quenched dark oxide, 0.5–1.5 μm
Heat Treatment Cycle That Prevents Slot Fatigue
We start with GCR15 (AISI 52100) bar stock, which is spheroidize annealed before machining. After turning the OD and boring the taper, we vacuum harden at 1030°C, then quench in 5 bar nitrogen. Tempering is done twice at 180°C for 2 hours each. This gives a martensitic structure with retained austenite below 3%. The gripping slots are wire-cut after hardening, and then the fingers are stress-relieved at 150°C for 1 hour. This sequence is why our collets do not crack at the slot root after 100,000 cycles. We test every heat treatment batch with a Rockwell C tester and a microsection sample—no exceptions.
Inspection Before Every Shipment—Not a Random Sample
Every single collet gets a full dimensional check, not a batch sample. We measure the taper angle with a precision sine bar (error < 0.001 mm over 50 mm length), the bore diameter with an air gauge (resolution 0.0005 mm), and the runout on a custom spindle fixture with a 0.0001 mm indicator. The dark oxide thickness is verified with a coating thickness gauge. If any number is outside the table above, the collet is scrapped, not reworked. You get a signed inspection sheet with each part number. For your own records, we also send a PDF of the CMM report via email within 24 hours of shipping.
FAQ: Your First Order, Custom Bores, and QC
Is there a minimum order quantity?
No MOQ—you can order a single collet for a prototype run, and the price per piece only drops slightly at 10+ because we set up the grinding wheel once.
Can you make a custom bore size for a non-standard bar diameter?
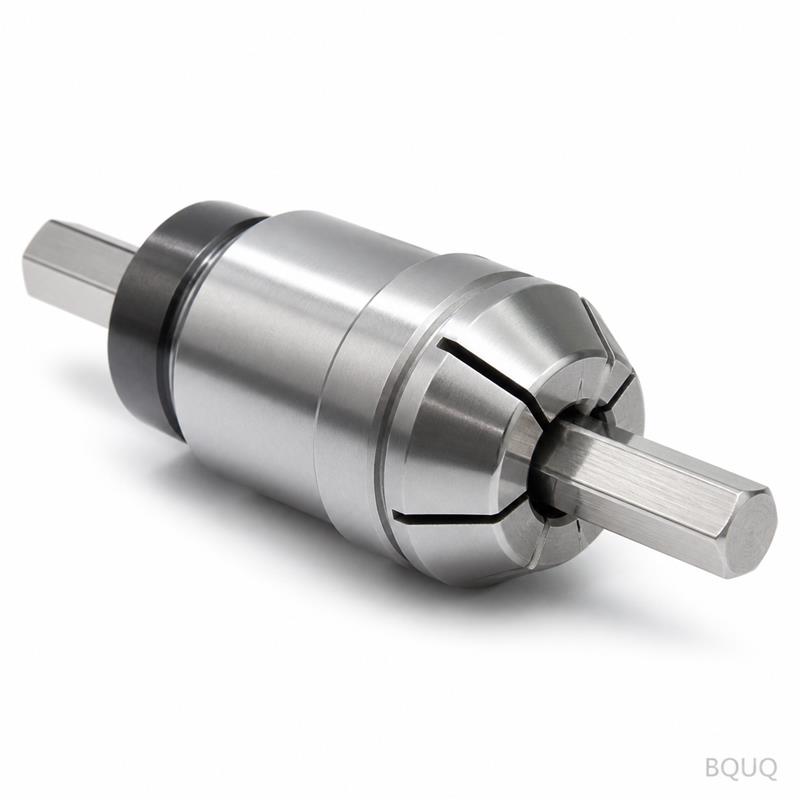
Yes, we can grind any bore from Ø3 mm to Ø42 mm in 0.5 mm increments, and we can also make a stepped bore for hex or square stock, but that requires a 3-day tooling adjustment.
How do you verify runout before shipping?
We mount the collet on a test mandrel with the same taper as your spindle, then rotate it at 300 rpm and measure TIR at the nose and at 3×D with a capacitive sensor.
What is your lead time for a rush order?
Standard is 7 working days, but if you need a collet in 48 hours, we can pull one from our semi-finished stock (25% oversize blank) and finish grind it for an extra 15% rush fee.
How This Collet Fits Your Tooling and Workholding System
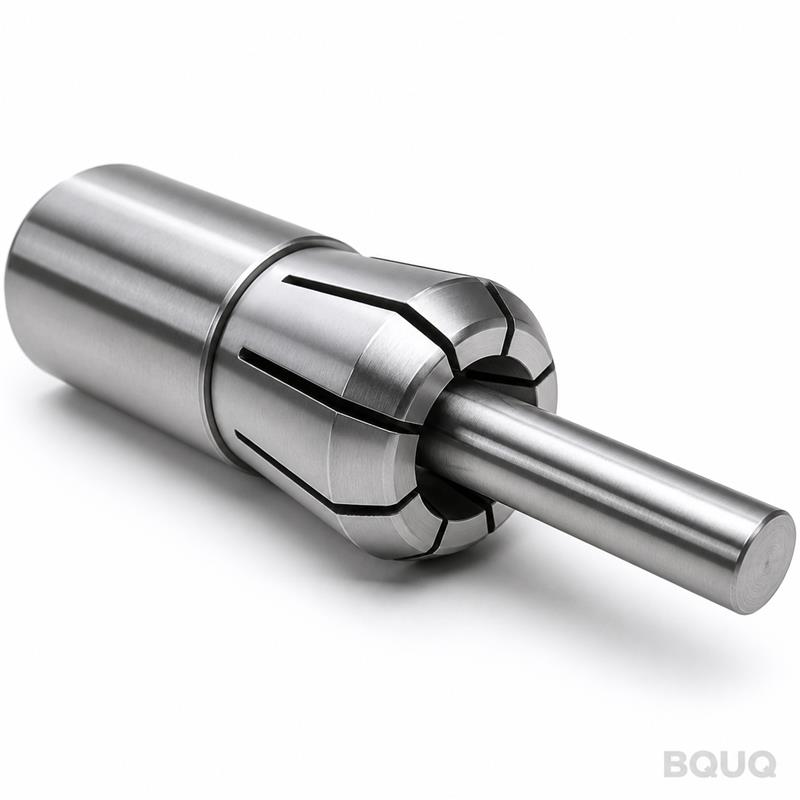
Pair this chuck with a CNC lathe or Swiss-type machine using a 36 type spindle nose. It grips round bar stock, ground pins, and pre-machined parts with a concentricity that eliminates secondary operations. For cutting tool selection, see our CNC cutting tool selection guide to match your insert grades with the low runout this chuck provides. If you are designing a new fixture, our CNC machining tolerances guide explains how to budget for the 0.005 mm runout in your stack-up analysis. This chuck is part of our precision manufacturing line, made in China with full export documentation.
Order This Collet and Get a Quote in 12 Hours
Send us your drawing or just tell us the bar diameter and spindle model. We will reply with a firm quote within 12 hours—not a range, not a "depending on," a real number. Email your drawing to sc@bquq.com, or send a photo or PDF via WhatsApp at +86 13713157787. If you are not sure about the 36 type fit, include your spindle taper drawing and we will check it for free. We ship worldwide with DHL or FedEx, and customs paperwork is included. No MOQ, no haggling, just a collet that holds 0.005 mm.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.