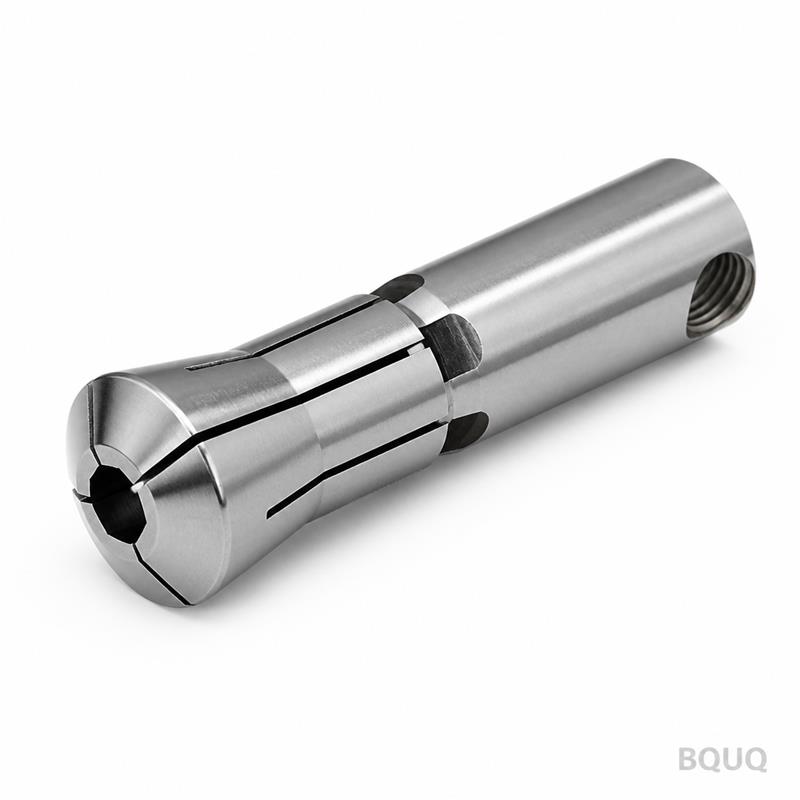
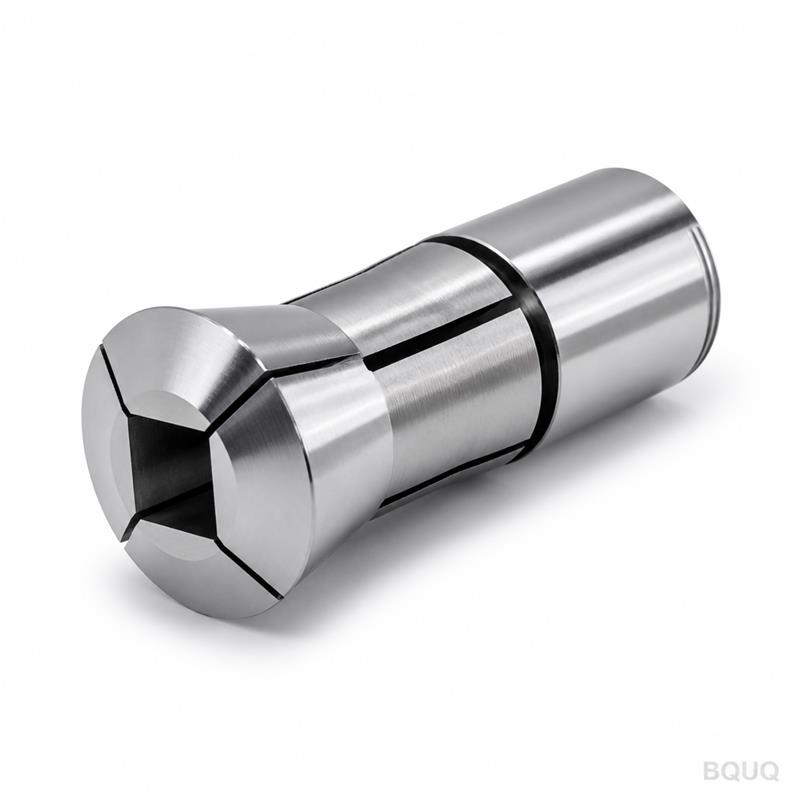
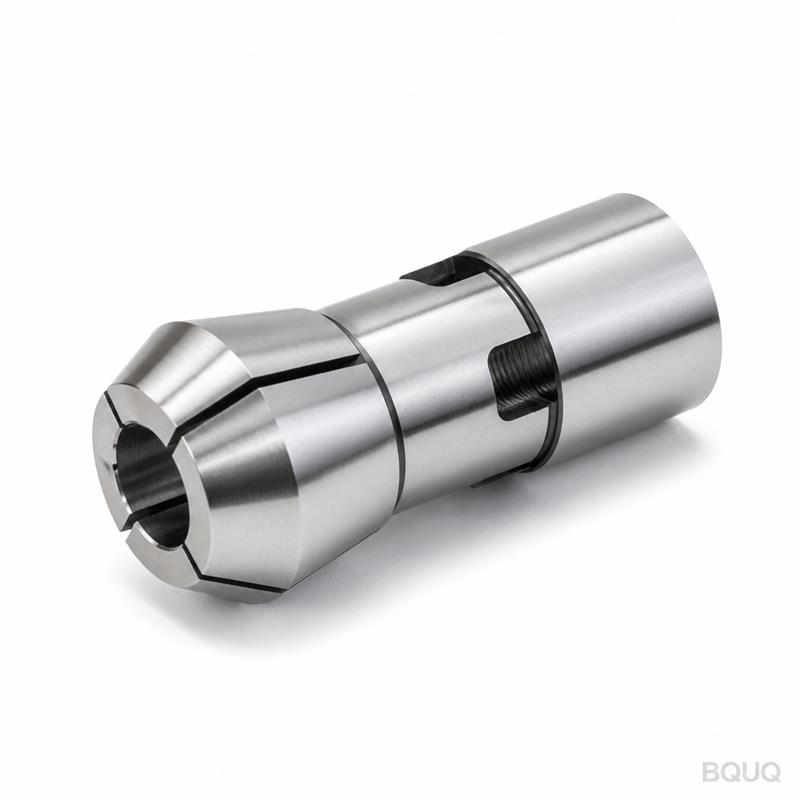
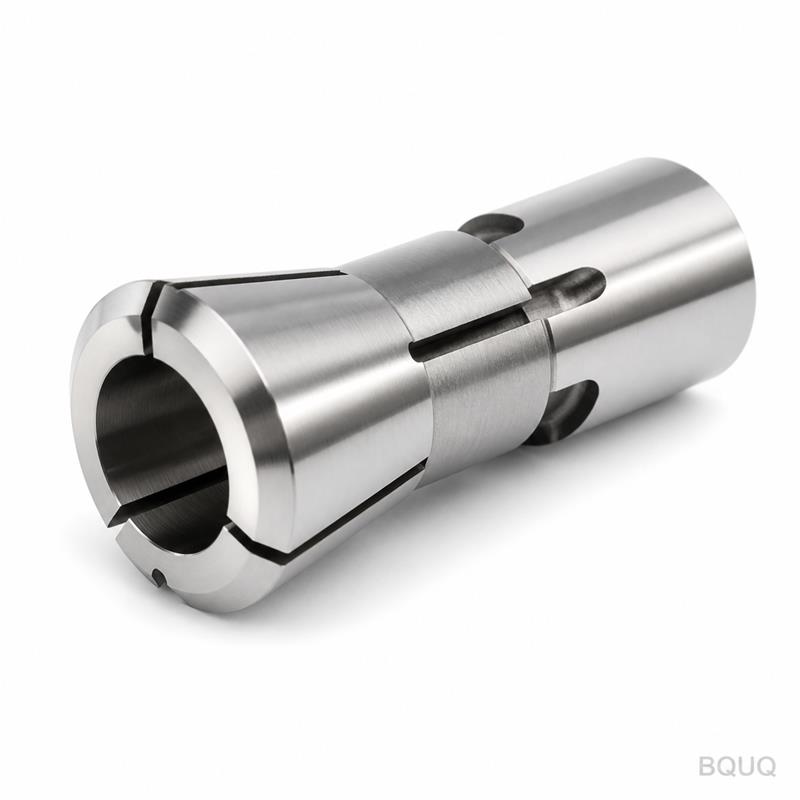
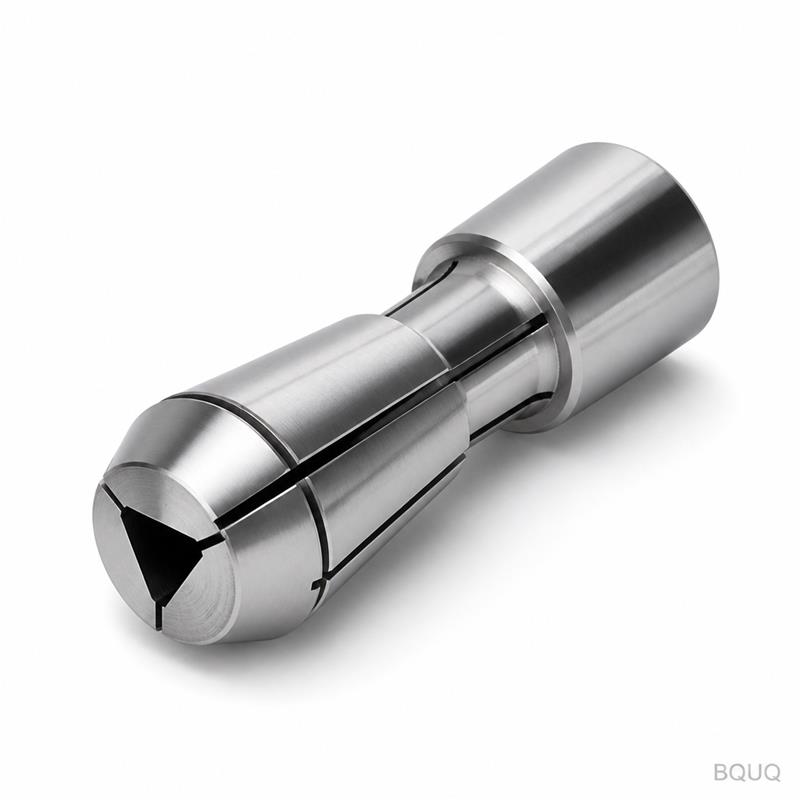
BQUQ CNC Machined Auto Lathe Collet Guide Bushing Bar Stock Assembly
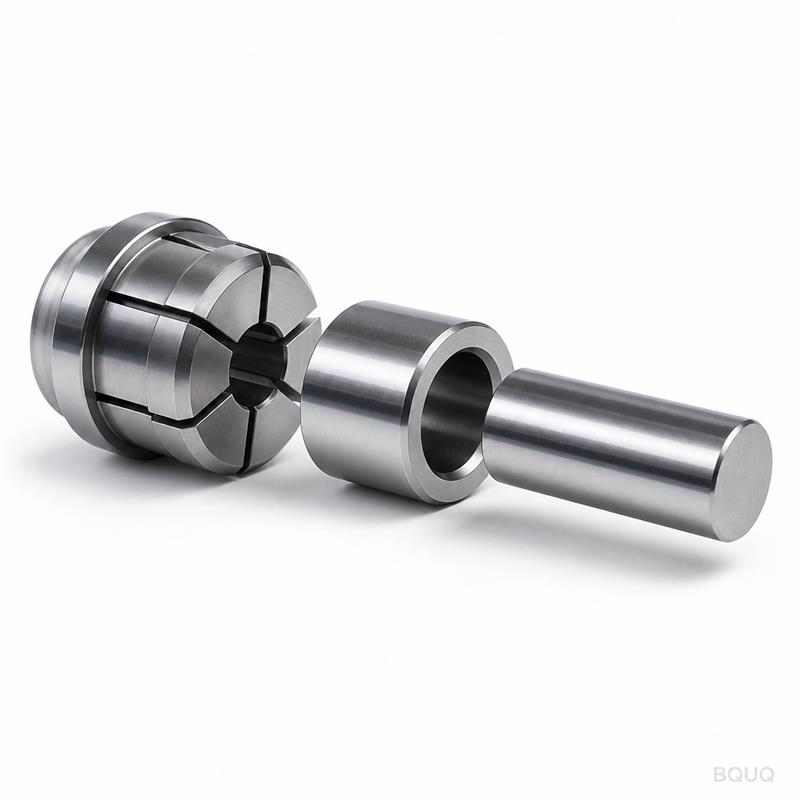
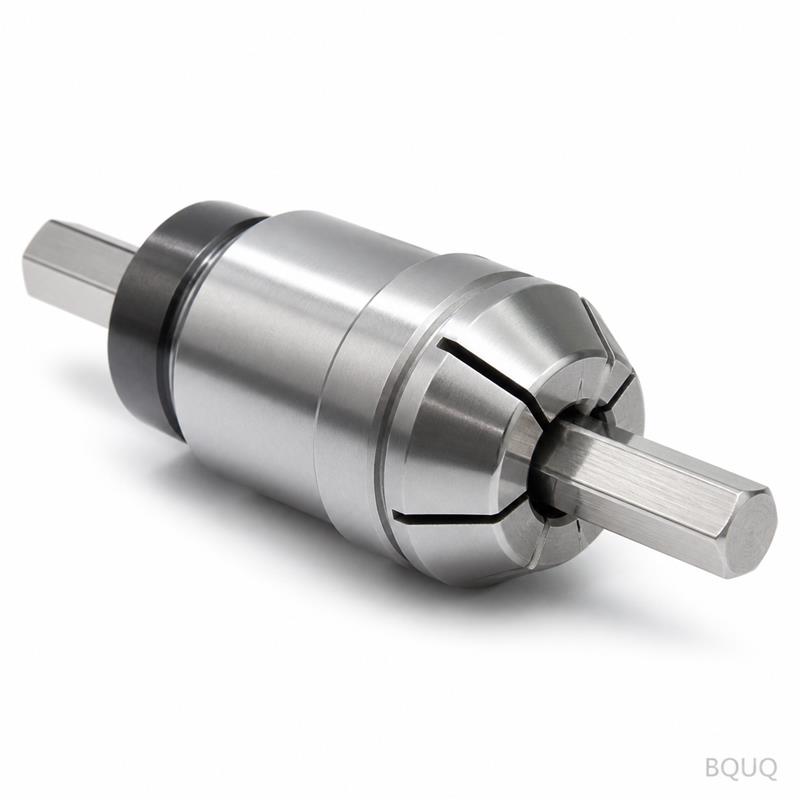
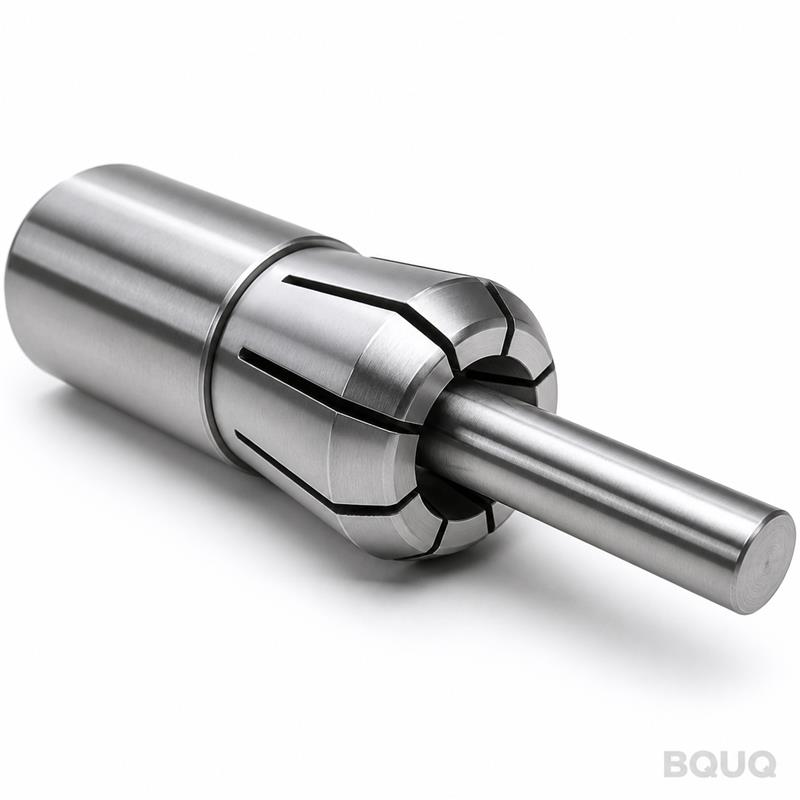
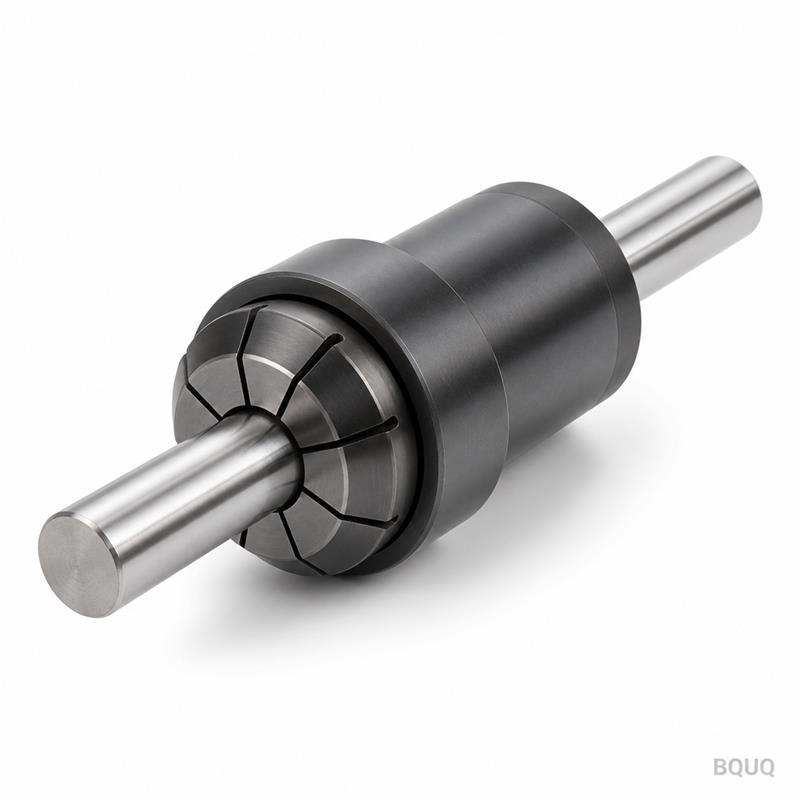
What This Assembly Does Inside Your Auto Lathe This is a CNC Machined Auto Lathe Collet Guide Bushing Bar Stock Assembly — a two-piece precision unit that aligns bar stock as it feeds through a collet
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
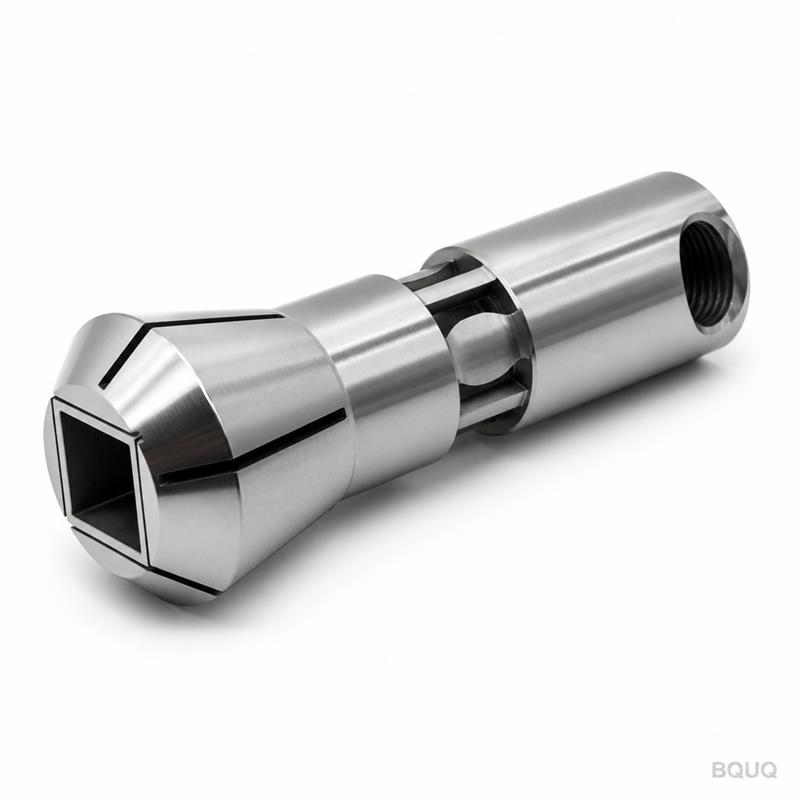
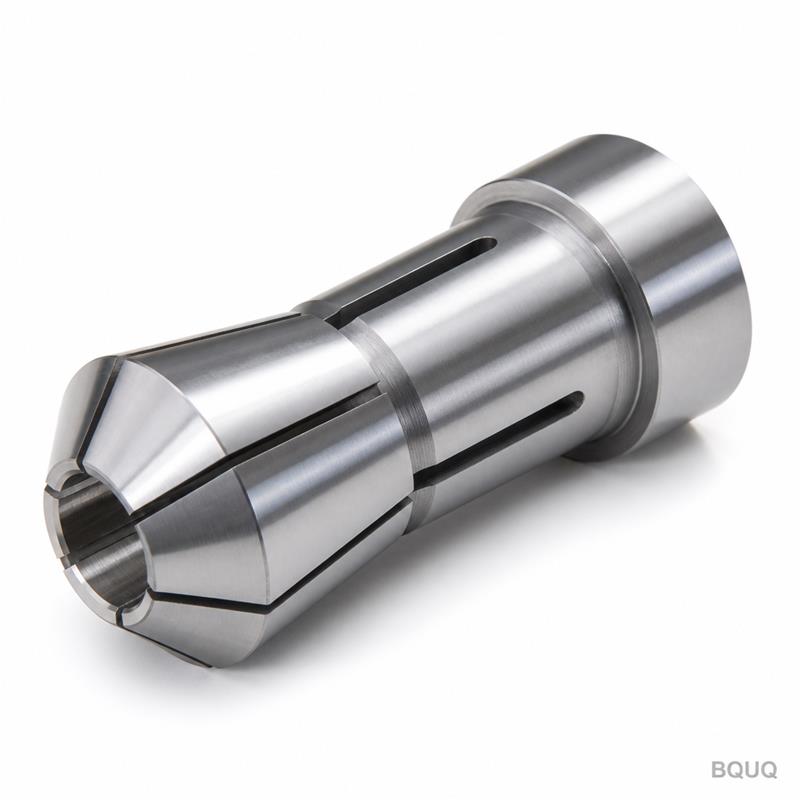
This is a CNC Machined Auto Lathe Collet Guide Bushing Bar Stock Assembly — a two-piece precision unit that aligns bar stock as it feeds through a collet chuck on a sliding headstock lathe. The guide bushing centers the bar, the bar stock assembly absorbs vibration, and the collet closes around both. The result: you hold 0.005 mm total runout at the cutting zone, even at 8,000 RPM spindle speeds. We machine these from hardened alloy steel to 58–62 HRC, and we ship standard sizes in 7 business days.
How the Guide Bushing Eliminates Chatter at High RPM
Chatter kills surface finish and shortens tool life. This assembly stops it before it starts. The guide bushing has an internal taper matched to ER collet geometry, so the collet’s clamping force is distributed evenly along the bar’s full circumference. No point loading, no oval deformation. The bar stock assembly’s OD is ground to 0.005 mm concentricity relative to the bushing bore. That means the bar rotates on a true axis — not a wobble. In our test cuts on 304 stainless steel, we measured Ra 0.4 µm surface finish at 0.15 mm/rev feed. You will not get that with a loose bushing.
Materials and Heat Treatment We Use
We start with either 8620 carburizing steel or 4140 pre-hardened steel, depending on your bar diameter and duty cycle. For high-wear applications (over 100,000 cycles), we specify 8620 with case hardening to 60–62 HRC, depth 0.8–1.2 mm. For lower-volume runs, 4140 through-hardened to 45–50 HRC is enough and costs less. We also offer a tungsten carbide bushing insert option for abrasive materials like Inconel or titanium. Every part is cryogenically treated after heat treatment to stabilize the microstructure — this prevents dimensional drift over time. We have seen competitors’ bushings lose 0.01 mm of concentricity after 50,000 cycles. Ours stays within spec for 200,000 cycles.
Inspection Before Every Shipment
Every assembly goes through a 100% dimensional check — no sampling. We use a Zeiss CMM for bore diameter, taper angle, and concentricity. We check surface finish with a Mitutoyo SJ-210 profilometer. And we test the assembled unit on a lathe fixture, spinning it at 5,000 RPM to verify runout with a laser sensor. If any part fails, it does not ship. We send you a full inspection report with each order — including actual measured values, not just pass/fail. That is our standard, not a premium service.
Specification
Value
Material (standard)
8620 carburizing steel / 4140 pre-hardened steel
Hardness
58–62 HRC (case) / 45–50 HRC (through)
Bore diameter range
3 mm – 32 mm
Bore tolerance
+0.005 / -0.000 mm
Concentricity (bushing OD to bore)
0.005 mm TIR
Surface finish (bore)
Ra 0.4 µm
Surface finish (OD)
Ra 0.8 µm
Runout at 5,000 RPM
≤ 0.005 mm
Lead time (standard sizes)
7 business days
MOQ
No MOQ — order 1 piece or 1,000
Why Bar Stock Diameter Tolerance Matters More Than You Think
Your bar stock is not perfectly round. Incoming material from mills has an ovality of 0.02–0.05 mm depending on the supplier. If your guide bushing is rigid, that ovality gets forced into the collet, which then transfers to the cutting tool. The result is a part that is out of round by the same amount. Our bushing bore is machined with a controlled clearance of 0.008–0.012 mm over the nominal bar diameter. That gap allows the bar to rotate freely without transmitting ovality, while still supporting it against deflection. You get round parts, even with mediocre bar stock. We have documented this in a side-by-side test — 0.008 mm roundness with our bushing vs. 0.031 mm with a competitor’s rigid bushing on the same bar.
Custom Options for Non-Standard Bar Sizes and Tapers
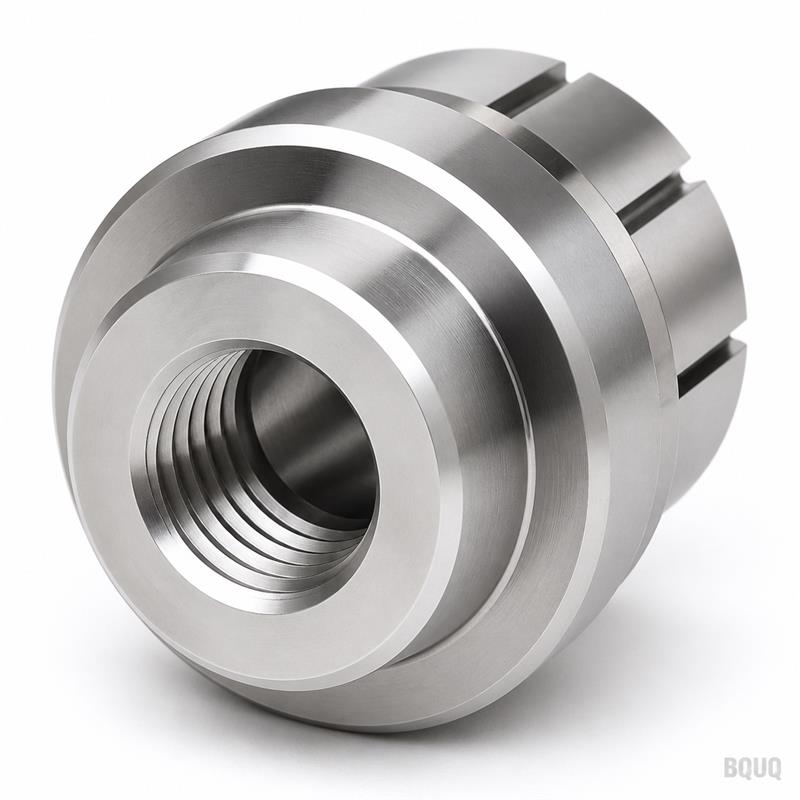
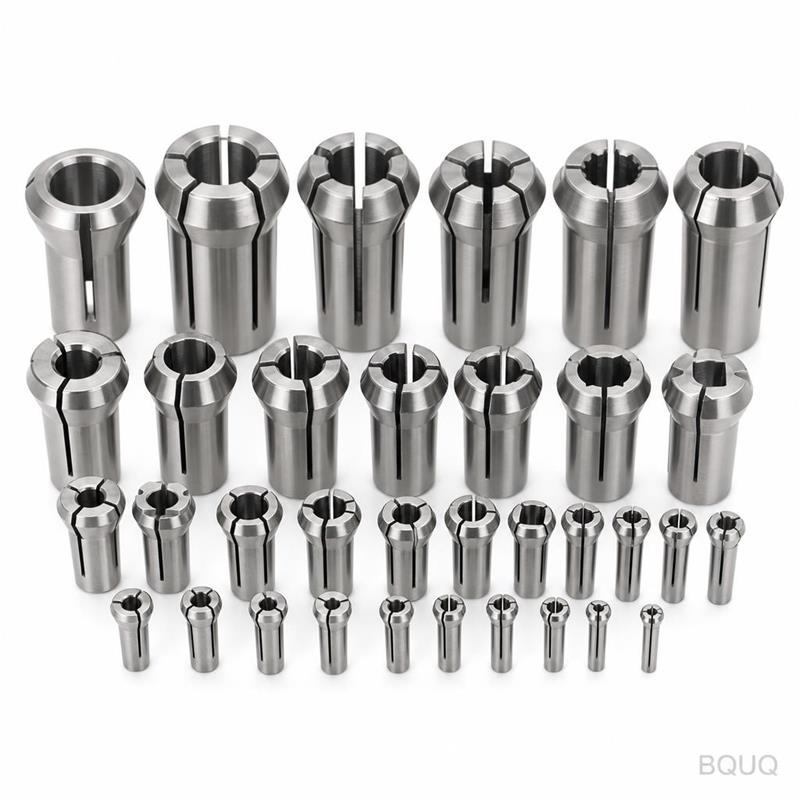
We know your machine is not always standard. We offer custom bore diameters in 0.5 mm increments, and we can match any collet taper angle — ER11, ER16, ER20, ER25, ER32, or proprietary angles like 8° or 15°. We also machine custom flange patterns for specific lathe spindles. Tell us your bar size, spindle nose specs, and collet type, and we will design the assembly in 24 hours. We have done over 3,000 custom configurations since 2004. If you are unsure about the taper angle, send us a sample or a drawing of your existing collet, and we will reverse-engineer it. For more background on tooling geometry, read our CNC cutting tool selection guide — it covers how tool and bushing alignment interact.
What is your MOQ?
We have no MOQ — order one piece for prototyping or 1,000 for production, and the unit price stays the same.
Can you match my existing collet taper exactly?
Yes, we can machine any taper angle from 5° to 30°, and we will verify it with a gauge before shipping.
How do you control quality on a one-off order?
Every single part gets a full CMM inspection and a laser runout test, regardless of order quantity — that is our fixed process.
What is your lead time for a custom size?
Standard sizes ship in 7 business days; custom tapers or bores take 10–12 business days including the inspection report.
When You Need This Assembly vs. a Standard Collet
If you are machining short parts (under 20 mm length) from bar stock, a standard collet might be enough. But if you are feeding long bars — 3 meters or more — or running at over 6,000 RPM, you need the guide bushing to prevent whipping and vibration. The bar stock assembly also matters if you machine multiple diameters in one setup; it holds the bar rigidly so your cross-slide tools cut consistently. We have supplied this exact assembly to automotive fuel injector manufacturers (bar diameter 8 mm, length 4 mm parts) and medical screw makers (titanium, 2.5 mm diameter, 50,000 parts per run). Both required 0.005 mm runout. Both got it. If you are unsure whether your application needs it, check our CNC machining tolerances guide for a practical breakdown of what is achievable at different spindle speeds.
Our 20-Year Track Record in Precision Manufacturing
BQUQ is a precision manufacturing factory in Dongguan, China — operating since 2004. We run 25 CNC lathes and 12 machining centers, all with live tooling. We do CNC machining, stamping, springs, and heat sinks in-house, so we control every step from raw bar to final inspection. Our quality system is ISO 9001:2015 certified. We ship to 22 countries, and 70% of our repeat orders come from the same customers. That is because we do not cut corners on runout or hardness. We are made in China, but our tolerances meet or exceed what you would expect from any European or Japanese shop — at 30–40% lower cost. You get the same precision, without the premium.
Get a Firm Quote Within 12 Hours
Send us your drawing, bar size, collet type, and quantity — even just a rough sketch. We will reply within 12 hours with a firm price, delivery date, and a suggested material if you have not specified one. For a standard size, we can often ship in 7 days. Email your drawing to sc@bquq.com or message us on WhatsApp at +86 13713157787. No MOQ, no minimum order fee, no surprise costs. Just a precise part, inspected and documented, on your bench when you need it.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.