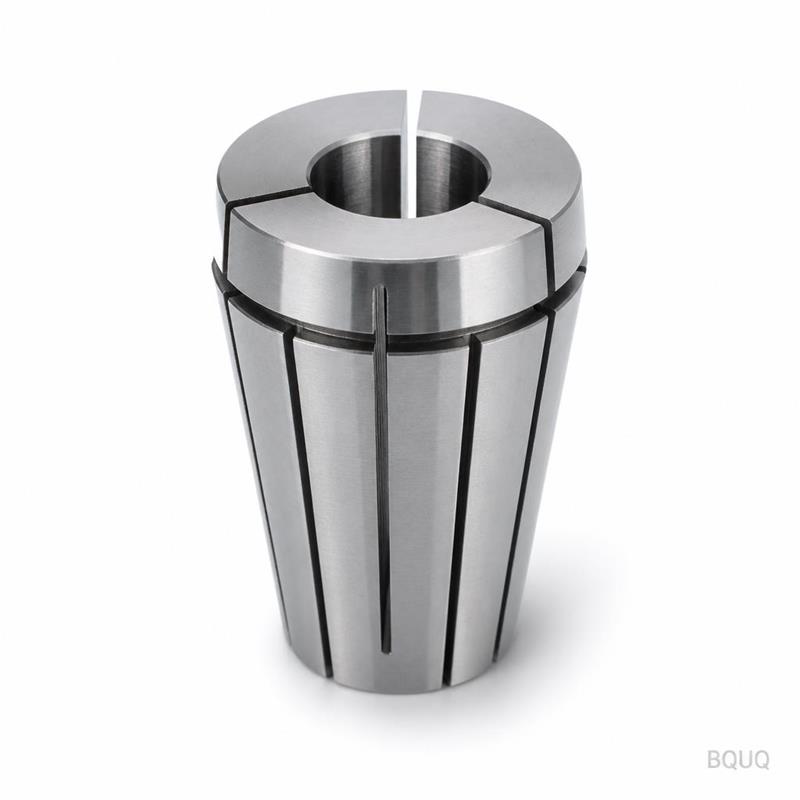
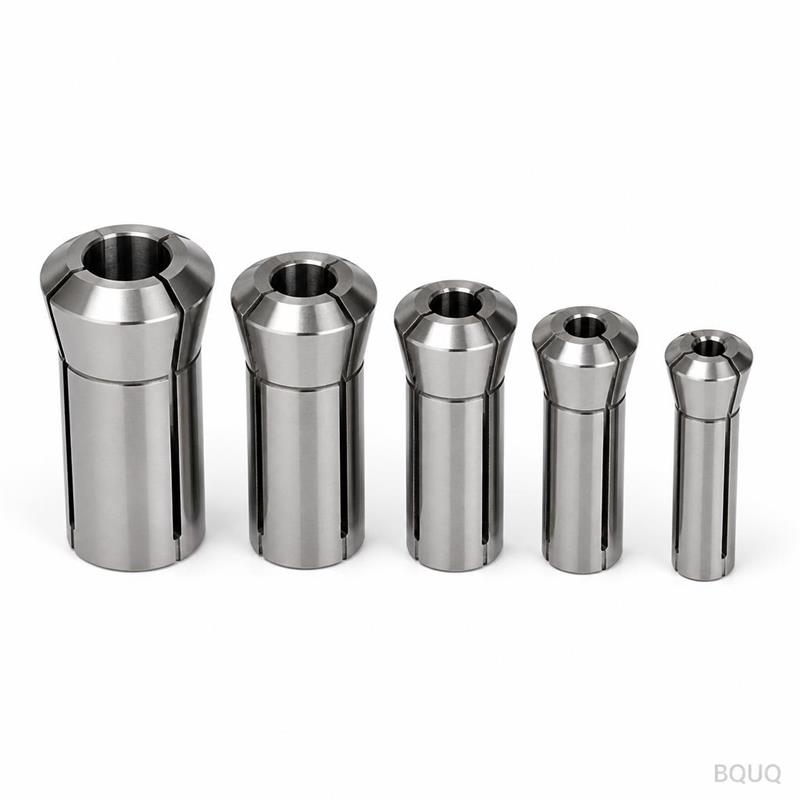
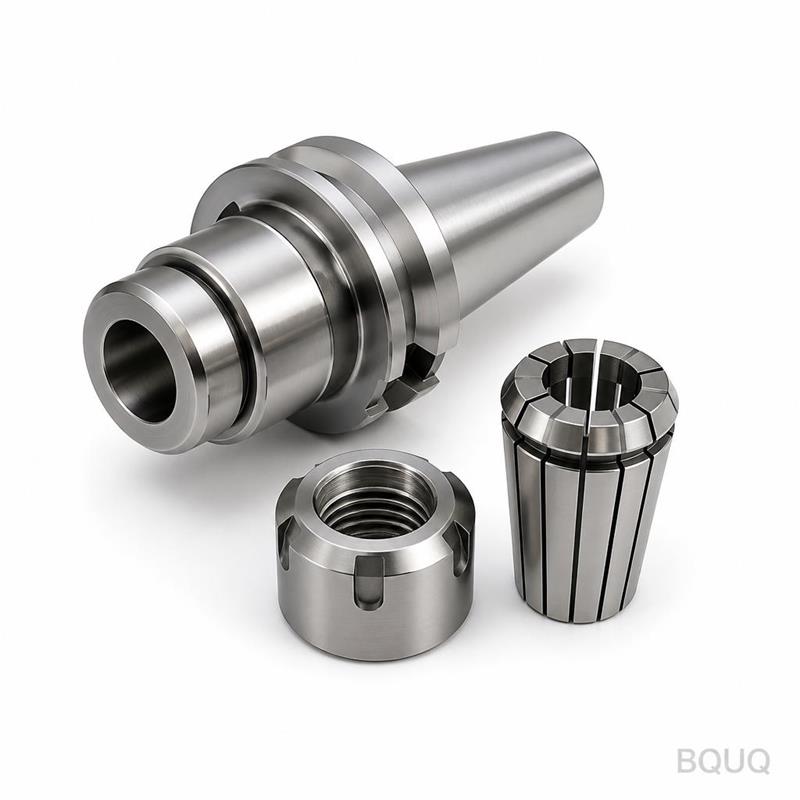
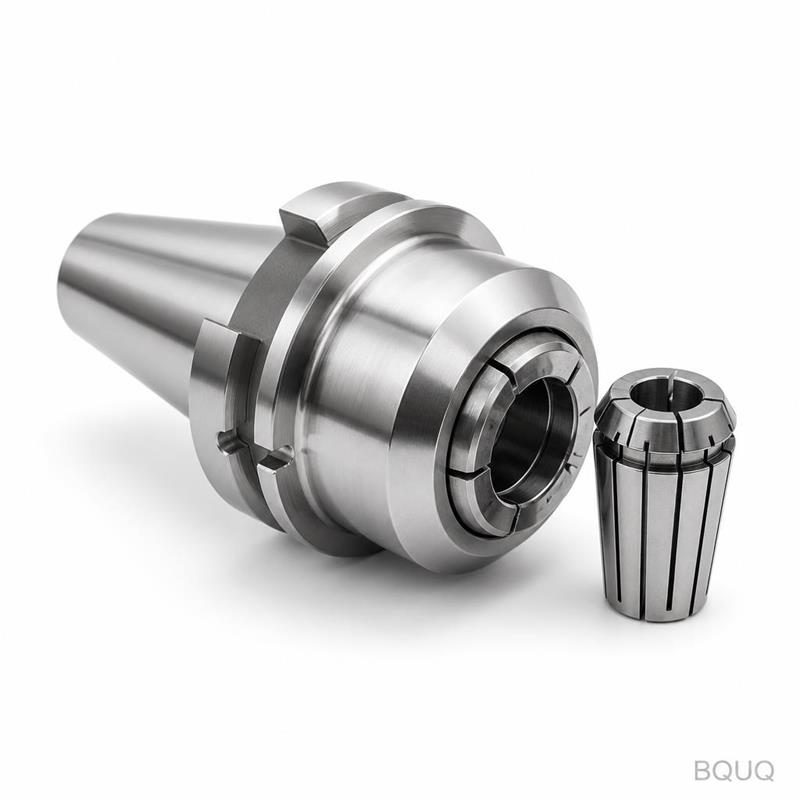
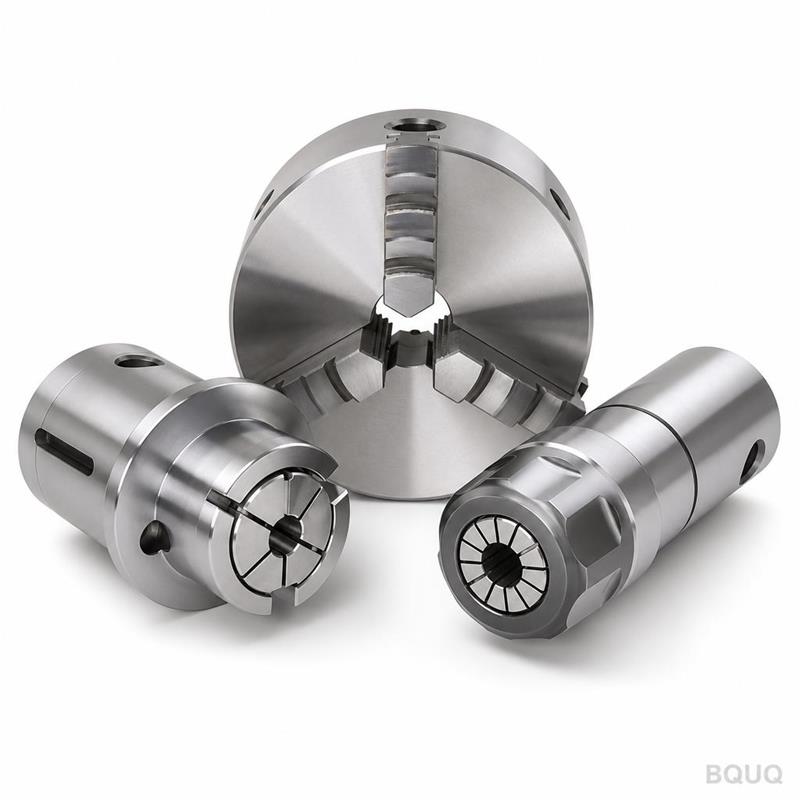
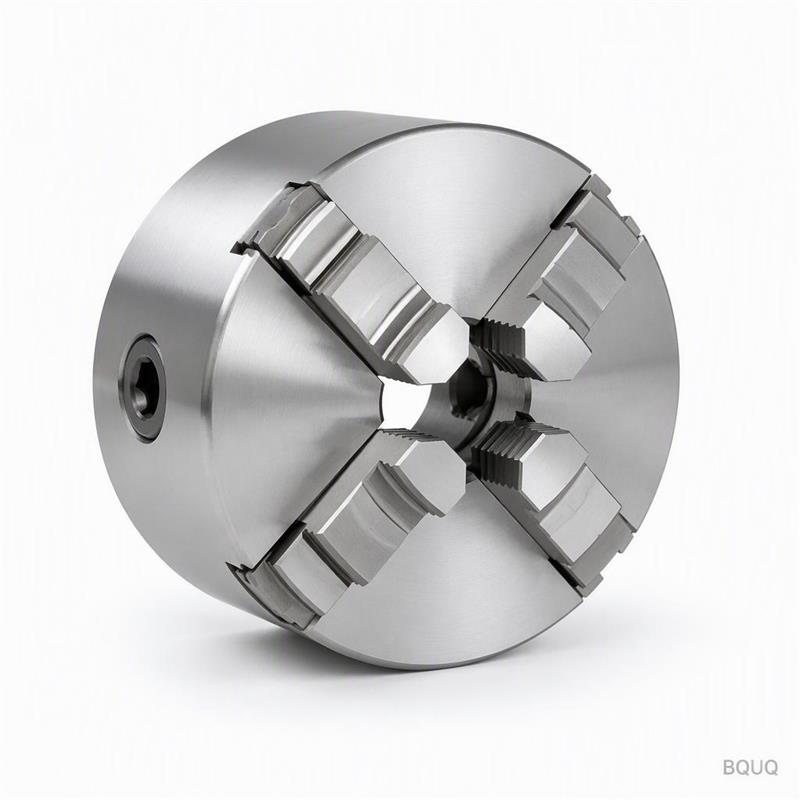
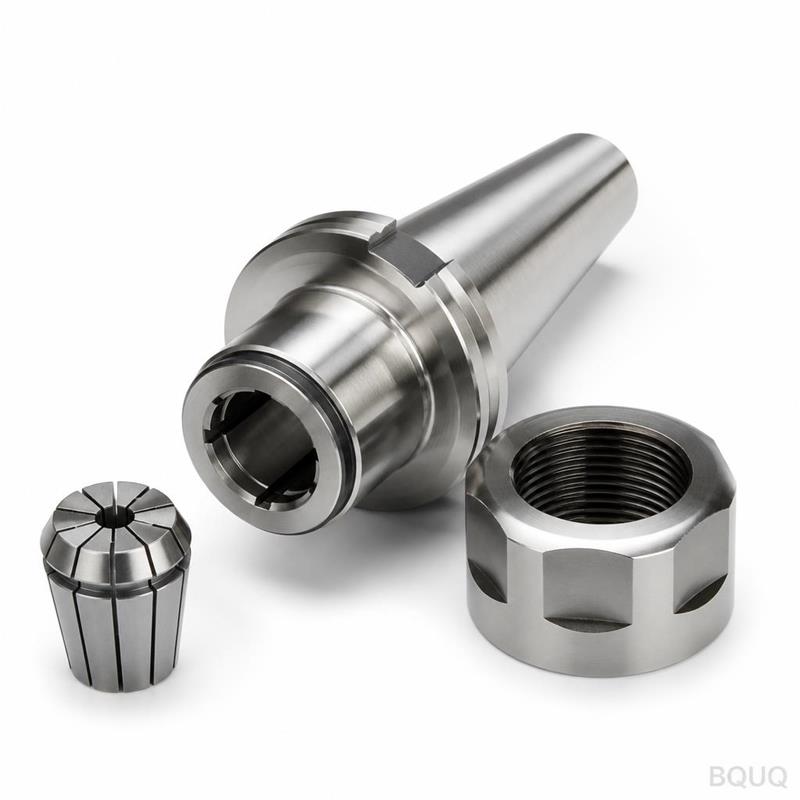
What This 2J Collet Chuck Does Differently This is a CNC machined 2J collet chuck for lathes. It grips your bar stock or tool shank with 0.003 mm total indicated runout (TIR). That is not a marketing
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
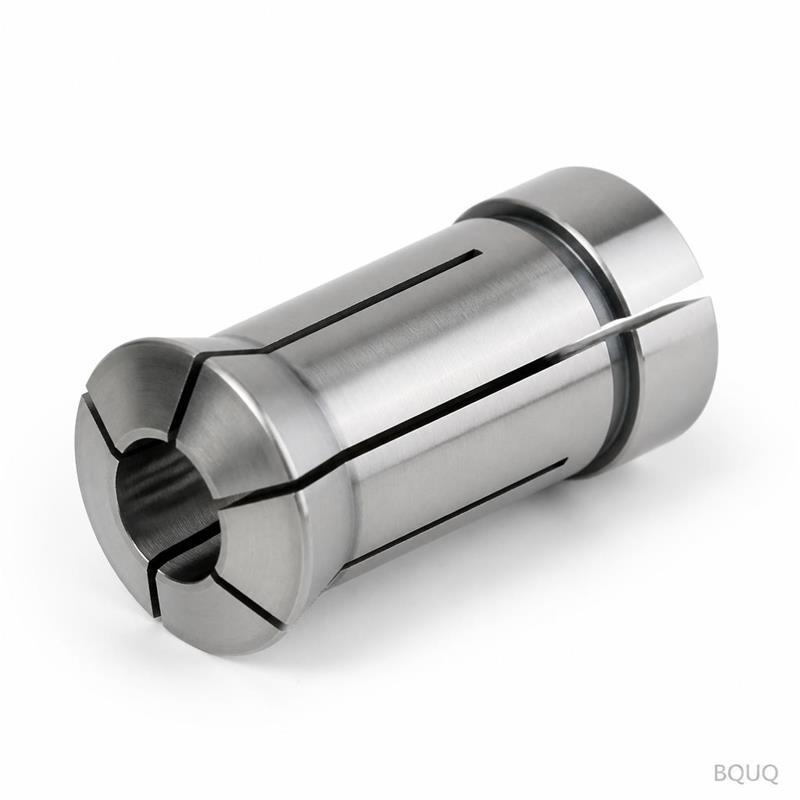
This is a CNC machined 2J collet chuck for lathes. It grips your bar stock or tool shank with 0.003 mm total indicated runout (TIR). That is not a marketing number. That is what we measure on every unit before it leaves our Dongguan factory. Hardness is 58–60 HRC on the gripping surface. Surface finish is Ra 0.4 µm. Lead time for standard sizes is 7–10 days. For custom bores, add 3 days. No MOQ. One piece or one thousand — same price per unit.
How the 2J Profile Eliminates Chatter and Slippage
The 2J collet uses a 20-degree tapered seat. Unlike ER collets that rely on a thin slit, the 2J design uses a full-length slot with a hardened steel body. This gives you 0.02 mm radial flexibility. That is enough to absorb bar stock diameter variation up to ±0.05 mm without losing grip force. The gripping force at the nose is 12 kN at 40 N·m torque. You get repeatable clamping for second-operation work. No bell-mouthing. No tool pull-out. That is why this collet chuck is the standard for Swiss-type and gang-tool lathes.
Materials and Heat Treatment We Use
We start with AISI 8620 alloy steel. This is not off-the-shelf stock. We buy from certified mills in China with mill certificates. After CNC machining to the 2J profile, we carburize the collet at 920°C for 4 hours. Case depth is 0.8–1.2 mm. Then we quench and temper to 58–60 HRC. The bore is then ground on a jig grinder to achieve the 0.003 mm TIR. The taper is ground last, in the same setup as the bore. That is the only way to guarantee concentricity between the taper and the gripping surface. If you specify a through-coolant version, we add a 1.5 mm cross-hole before heat treat. No secondary drilling after hardening.
Specifications You Can Verify
Workholding Type
2J collet chuck (dead length)
Available Bore Diameters
3 mm to 25 mm (in 0.5 mm increments)
Shank Options
Straight shank (20 mm, 25 mm), or custom thread mount
Hardness (Gripping Surface)
58–60 HRC
Runout (TIR) at Nose
0.003 mm
Surface Finish on Bore
Ra 0.4 µm
Grip Force at 40 N·m
12 kN
Max Recommended RPM
8,000 RPM (balanced)
Lead Time (Standard)
7–10 days
MOQ
No MOQ (1 piece accepted)
Inspection Before Every Shipment
Every 2J collet gets a full inspection report. We do not sample. We check 100% of units. The report includes: bore diameter measured with a bore gauge to 0.001 mm, TIR measured on a precision spindle with a 0.0005 mm indicator, hardness check on a Rockwell tester, and surface roughness on a profilometer. The report is signed by our QC engineer and shipped with the parts. If you request, we also include a video of the runout test. We have done this for 20 years. We do not skip it for small orders.
Customizing the 2J Collet for Non-Standard Workpieces
Your part is not always round. We machine custom bore profiles: hex, square, or stepped. The 2J body stays the same. We just change the bore geometry. For hex stock, we grind a 60-degree internal relief to prevent corner stress. For stepped parts, we add a rear pilot bore to locate the workpiece axially. Tolerances for custom bores are ±0.005 mm. We need your drawing in DXF or STEP format. If you have a sample part, we can measure it here and match the profile. Typical custom bore lead time is 10–12 days. No tooling charge for bores under 20 mm.
When to Use a 2J Collet vs an ER Collet
Use a 2J collet when you need dead-length accuracy for second-op work. ER collets pull the tool back as you tighten. The 2J collet does not move axially. That is why it holds length tolerance to ±0.01 mm. Use ER for drilling or milling where axial movement does not matter. If you are cutting threads or grooving, the 2J is the correct choice. For more on matching tooling to your cut, see our CNC cutting tool selection guide. For a deeper look at what tolerances are realistic, read our CNC machining tolerances guide.
What is your MOQ for this 2J collet chuck?
No MOQ. You can order a single collet for prototyping or a thousand for production — the unit price stays the same.
Can you make a custom bore for my non-standard bar stock?
Yes, we machine custom bore profiles (hex, square, stepped) to ±0.005 mm tolerance; send your DXF or STEP file and we will quote within 12 hours.
How do you ensure the 0.003 mm runout is consistent?
We grind the taper and bore in one setup, then 100% inspect every unit with a 0.0005 mm indicator and send you the signed report.
What is your lead time for a standard 2J collet order?
Standard sizes ship in 7–10 days; custom bores add 3 days, and we ship worldwide via DHL or FedEx.
Get a Firm Quote Within 12 Hours
Send your drawing or just your bore size and shank type. We will reply with a firm price and lead time within 12 hours — no guessing, no hidden tooling charges. This is precision manufacturing made in China, with 20 years of CNC machining experience. Email your drawing to sc@bquq.com or WhatsApp us at +86 13713157787. We are online 7 days a week.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.