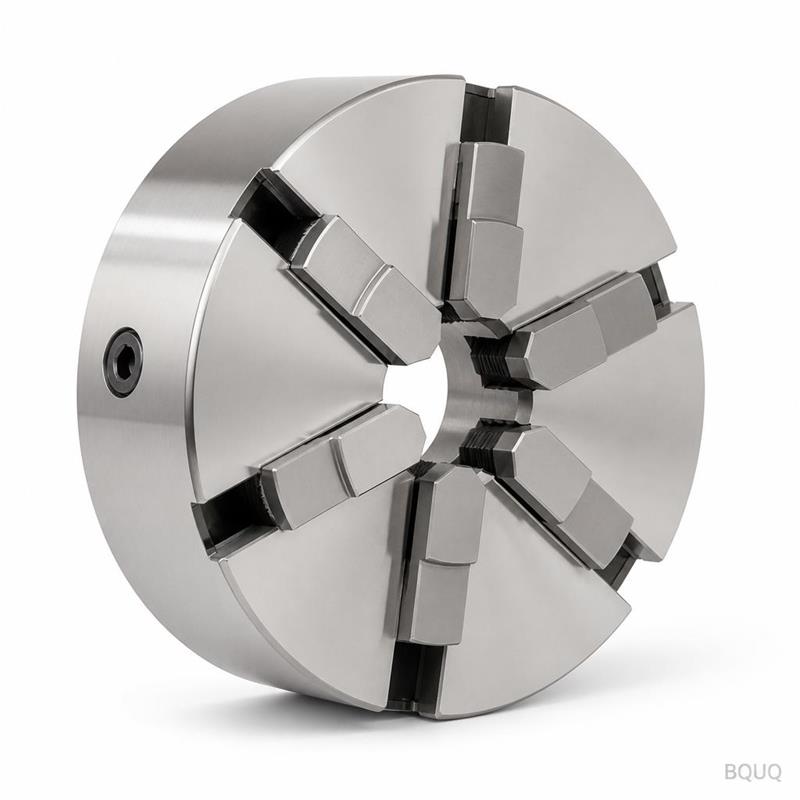
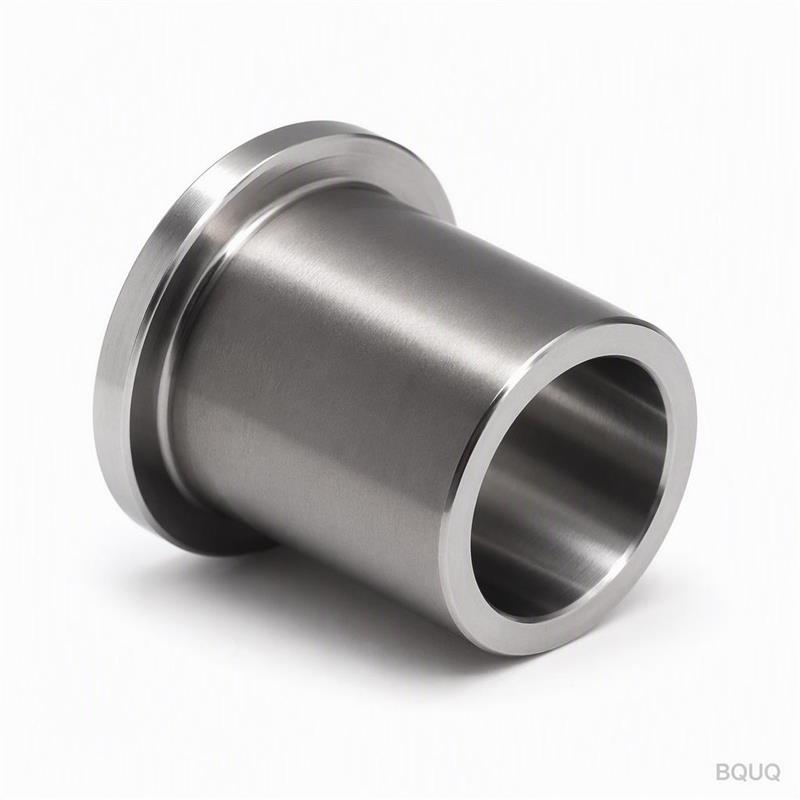
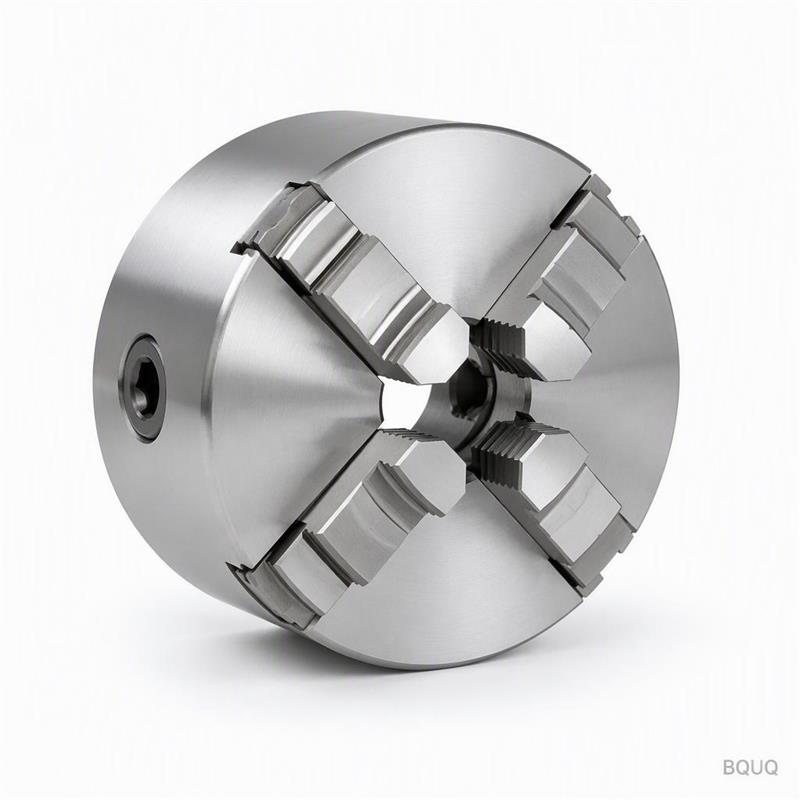
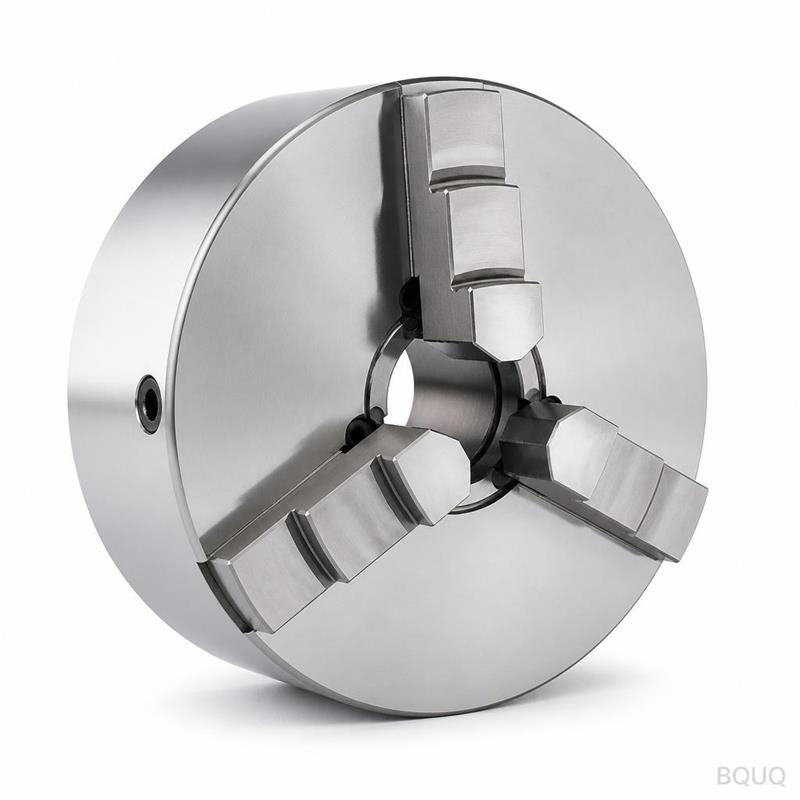
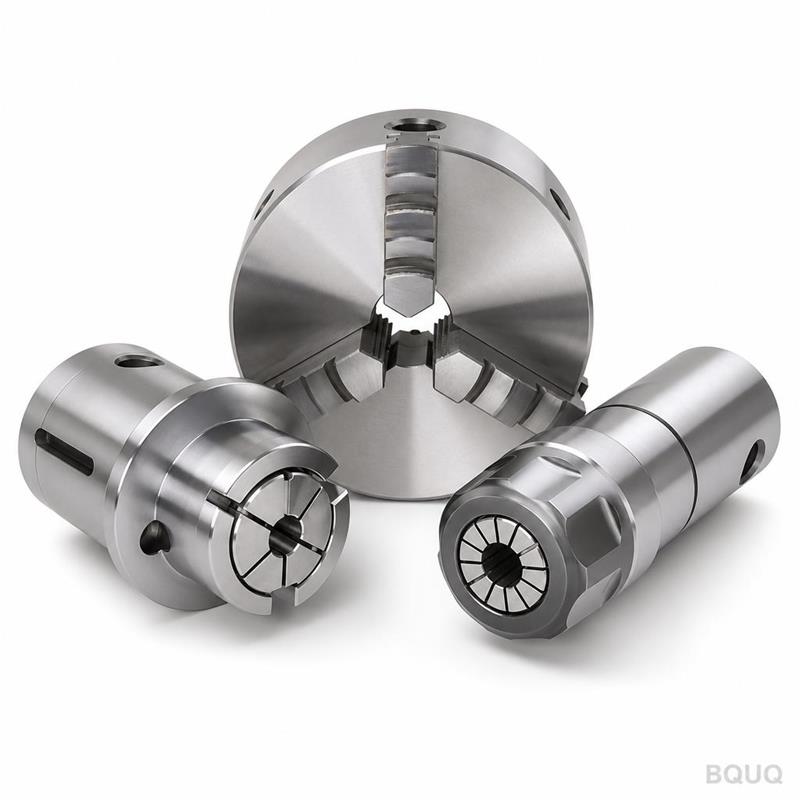
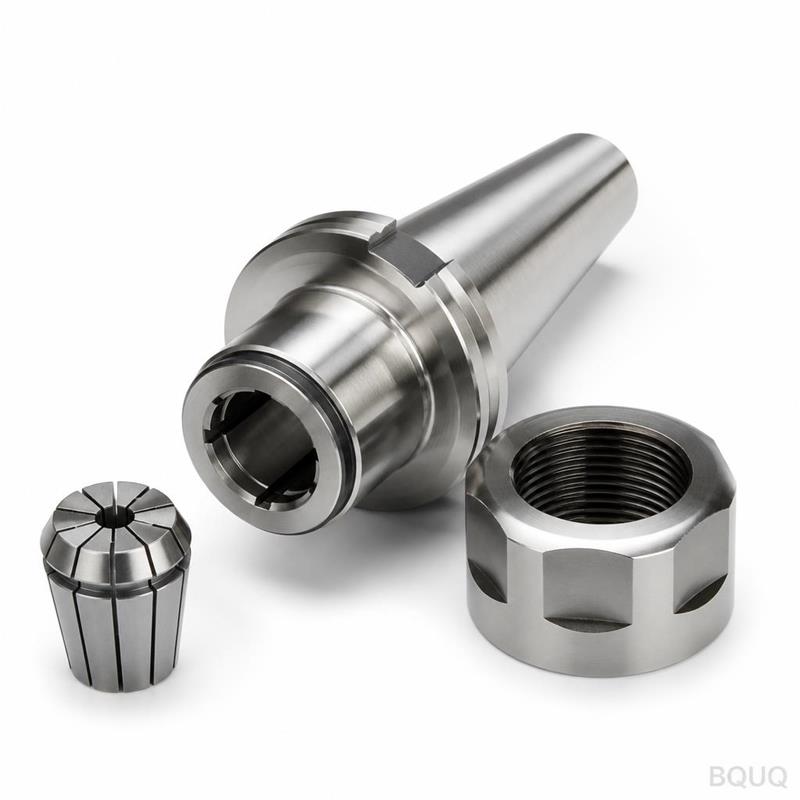
This is a CNC machined 6 jaw precision chuck for CNC lathes. It grips hex, square, and round stock with 0.005 mm concentricity and 58 HRC jaw hardness. You get a rigid, repeatable workholding solution
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
This is a CNC machined 6 jaw precision chuck for CNC lathes. It grips hex, square, and round stock with 0.005 mm concentricity and 58 HRC jaw hardness. You get a rigid, repeatable workholding solution with a 10-day lead time and no minimum order quantity.
Why Six Jaws Beat Three Jaws for Thin-Walled Parts
Standard three-jaw chucks deform thin-walled tubes and soft aluminum parts due to point loading. The six-jaw design distributes clamping force over twice the contact area. This reduces radial distortion by up to 40% on parts with wall thickness below 2 mm. You can machine to final tolerance without a second finishing pass.
The jaws are machined from 20CrMnTi alloy steel, case-hardened to 58–60 HRC. Each jaw is ground to a 0.002 mm profile tolerance. The chuck body is 45# steel, hardened to 42 HRC for wear resistance in high-volume production.
Grip Range and Jaw Geometry for Hex and Square Stock
The 6 jaw chuck accepts bar stock from 3 mm to 60 mm diameter. Jaw options include hard stepped jaws for roughing and soft machinable jaws for custom profiles. The jaw seat angle is 15 degrees, giving a self-centering action that pulls the workpiece back against the locating face.
For hex stock, the six jaws align perfectly with the flats. For square stock, every other jaw grips the corners. This eliminates the need for custom soft jaws on standard shapes. Runout remains under 0.005 mm across the full gripping range.
Materials and Heat Treatment We Use
We start with 20CrMnTi for jaws and 45# steel for the body. Both are forged, not cut from bar stock, to align the grain structure for maximum strength. After rough machining, we carburize the jaws to 0.8–1.2 mm case depth. Final grinding brings the hardness to 58 HRC with a surface finish of Ra 0.4.
The chuck body is induction hardened to 42 HRC on the taper and mounting surfaces. This prevents fretting and galling when the chuck is mounted and removed repeatedly. All critical dimensions are machined on a 5-axis CNC center with a CMM inspection report included with every unit.
Inspection Before Every Shipment
Every chuck is inspected individually before packaging. We measure runout at three positions: front face, mid-grip, and rear bore. We test clamping force with a torque wrench at 25 Nm, 50 Nm, and 75 Nm. The results are recorded on a serialized inspection sheet that ships with the chuck.
We also perform a 200-cycle grip test on a live CNC lathe. This verifies that the jaw movement remains smooth and the self-centering action stays within 0.003 mm after repeated actuation. No chuck leaves our floor without passing this test.
Mounting Options for Common CNC Lathe Spindles
We offer three mounting types: A2-4, A2-5, and A2-6 with corresponding back plates. The chuck body has a precision-ground taper that matches the spindle nose. For customers with a custom spindle, we machine the back plate to your drawing at no extra cost.
Each mounting option includes a draw tube thread of M16, M18, or M20. We can also supply a hydraulic actuation kit if your lathe does not have a through-hole drawbar. The total chuck weight ranges from 8 kg to 25 kg depending on the jaw size.
Specification
Detail
Product Type
CNC Machined 6 Jaw Precision Chuck for CNC Lathe
Jaw Material
20CrMnTi alloy steel, carburized
Body Material
45# steel, induction hardened
Jaw Hardness
58–60 HRC
Body Hardness
42 HRC
Concentricity (Runout)
0.005 mm TIR
Surface Finish
Ra 0.4 on jaws, Ra 0.8 on body
Grip Range
3 mm – 60 mm diameter
Mounting Options
A2-4, A2-5, A2-6 with back plate
Lead Time
10 days for standard, 20 days for custom
MOQ
No MOQ, single piece accepted
Inspection
100% CMM report with serial number
How Our Six-Jaw Chuck Handles High-Speed Spindle Loads
At 4000 RPM, centrifugal force can cause three-jaw chucks to lose grip. Our six-jaw design uses a shorter jaw stroke and a steeper wedge angle to maintain clamping force at speed. We balance each chuck to G2.5 at 4000 RPM, which means vibration stays under 0.5 mm/s.
The jaw guides are hardened to 60 HRC and coated with a low-friction treatment. This reduces heat buildup during long production runs. You can run continuous cutting cycles for 8 hours without thermal drift affecting part dimensions.
Does this chuck require special lubrication?
No, we apply a lithium-based grease at the factory that lasts for 10,000 cycles, and you can use standard spindle oil for replenishment.
Can you machine the jaws to my specific part profile?
Yes, we can machine soft jaws to any profile within 48 hours after receiving your part drawing, and we include this service free with your first order.
What is your quality control process for custom orders?
For custom orders, we send a pre-production sample with a full CMM report, and we only ship the batch after you approve the sample dimensions.
What is the typical lead time for a single chuck order?
Standard sizes ship in 10 days, custom back plates add 5 days, and we can expedite to 5 days for urgent tooling needs.
We are BQUQ, a precision manufacturing factory in Dongguan, China, with 20 years of experience in CNC machining, stamping, springs, and heat sinks. We ship worldwide with no MOQ. Send your drawing for a firm quote within 12 hours.
Straight answers from the factory, not a sales brochure.
How do I get a quote for this part?
Send your drawing (STEP, IGES, DWG, DXF or PDF) with quantity and target material to sc@bquq.com or WhatsApp +86 137 1315 7787. Our engineers review the drawing and reply with price, lead time and tooling cost.
What is your MOQ?
We do not set a fixed MOQ. The minimum is decided per part and per process, so tell us your target quantity and we quote against it. Small trial batches are accepted for new parts.
What is the lead time?
Lead time is agreed per order, based on the date you need, the quantity, the material and whether tooling is required. Send your target date with the drawing and we confirm what is achievable before you commit.
What tolerance can you hold?
CNC machining holds ±0.005 mm. Stamping, spring and extrusion parts are made to the tolerances marked on your drawing, and we confirm achievable values at quotation so there are no surprises at inspection.
Can you manufacture parts to my drawing?
Yes. Every order is made to the customer drawing or sample. We run CNC machining, metal stamping, spring coiling and aluminium heat sink extrusion in-house in Dongguan, so one supplier covers the whole part.
STEP, IGES, DWG, DXF and PDF. A 2D drawing with tolerances and surface finish requirements is preferred alongside the 3D model. Hand sketches can be quoted after our engineers redraw them.
How is quality controlled?
Inspection runs through the process, not only at the end: first article approval, in-process checks and a final report per batch, measured with CMM and optical equipment. Material certificates are available on request.
Where is the factory and do you ship worldwide?
Our factory is in Dongguan, Guangdong, China, operating since 2005. We ship worldwide by express, air and sea, and work with the forwarder nominated by the buyer.