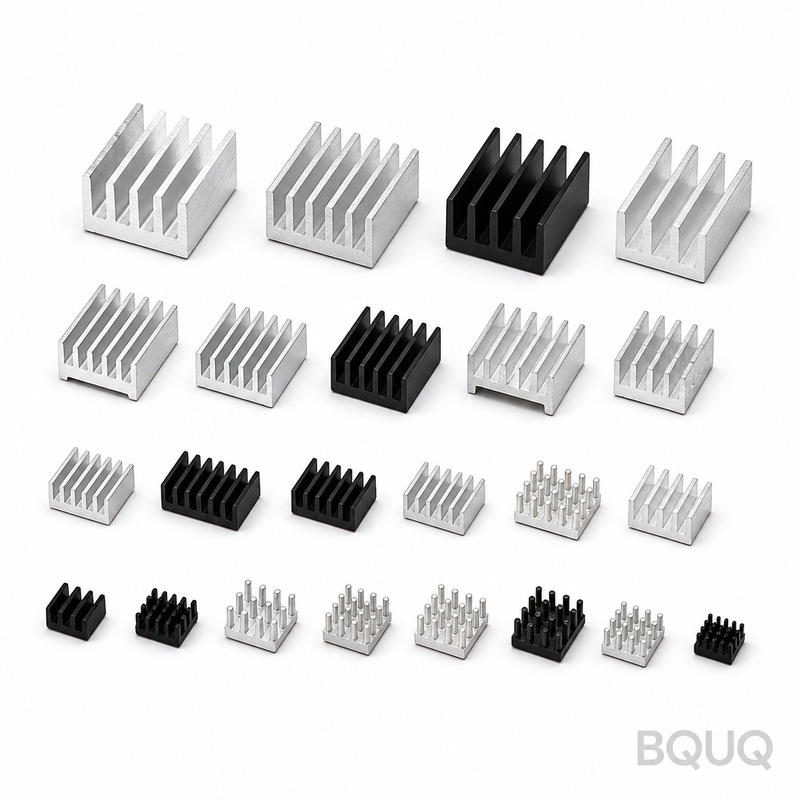
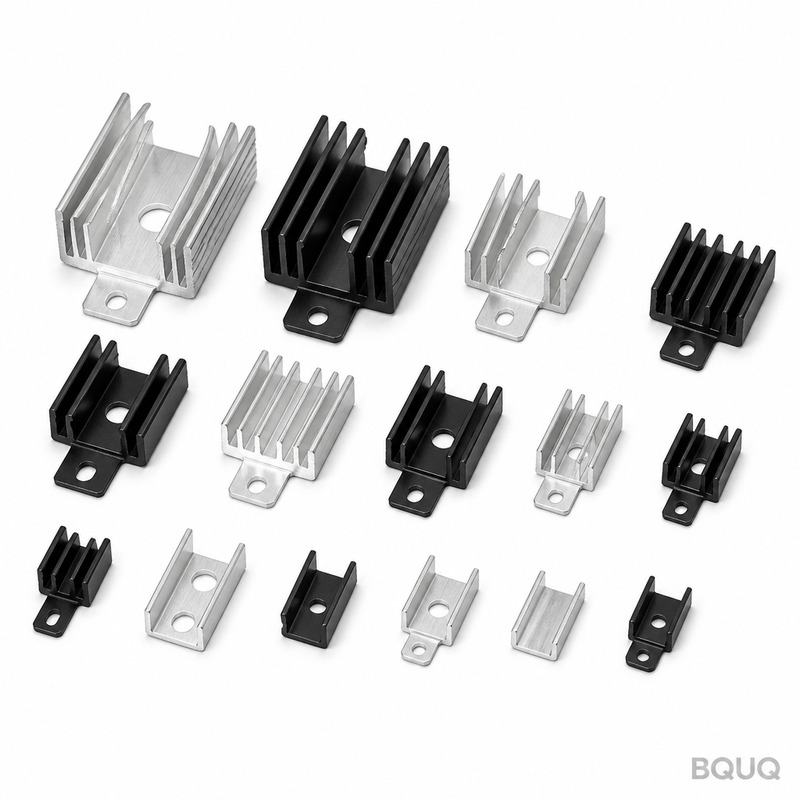
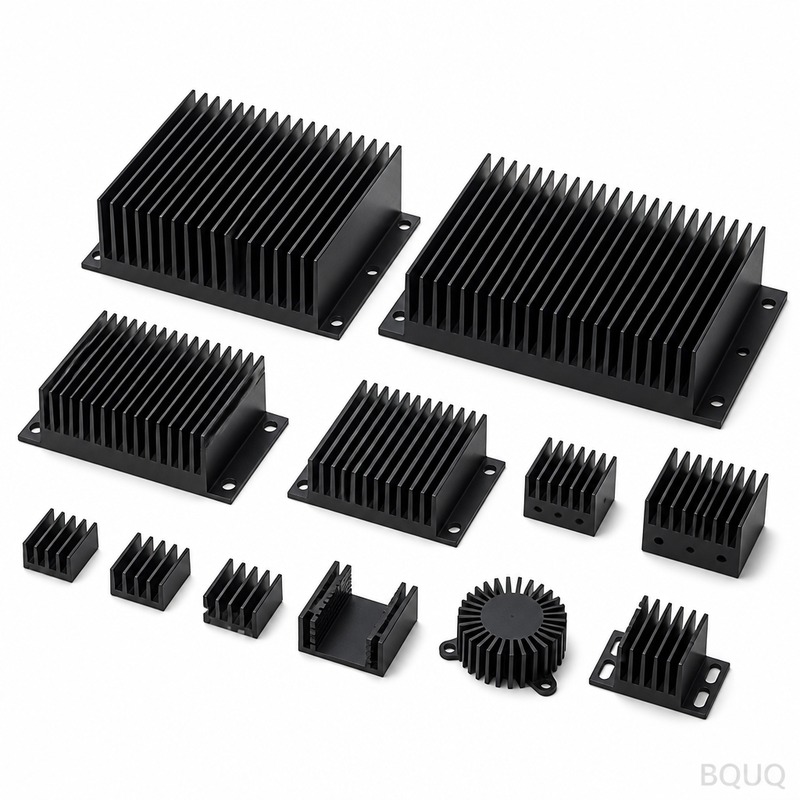
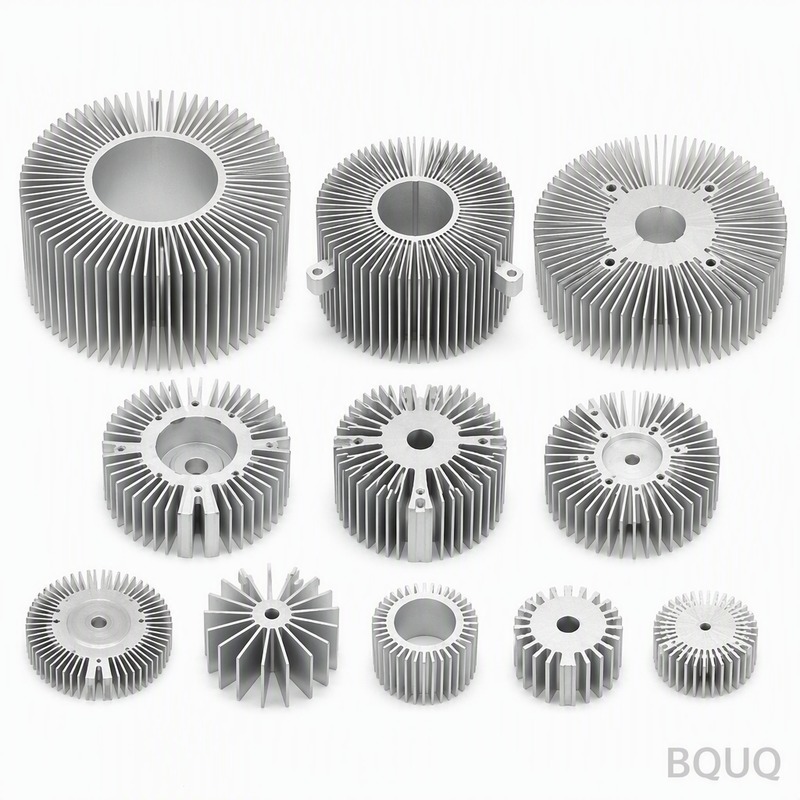
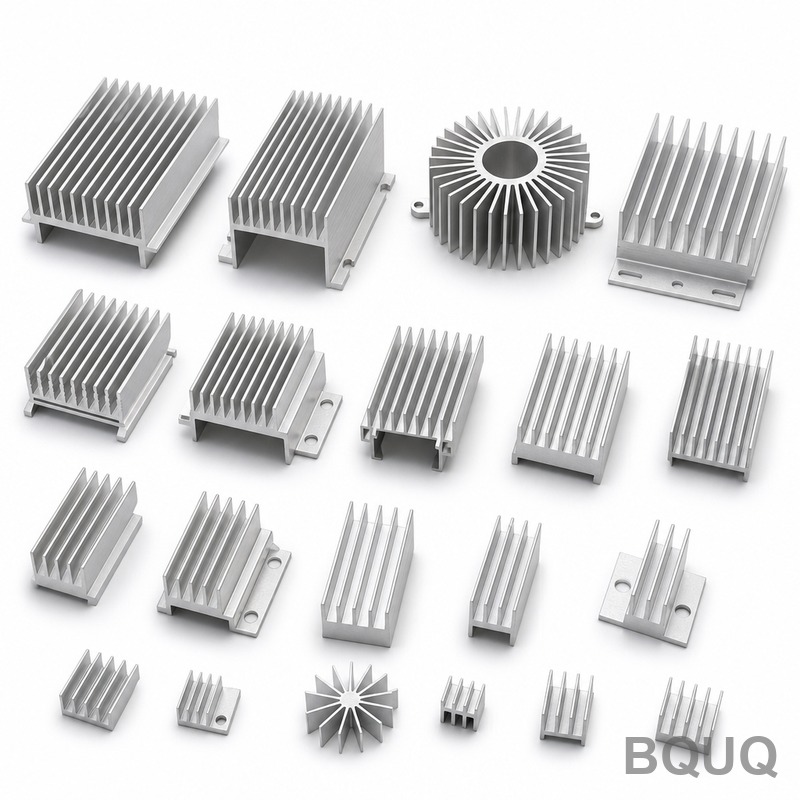
aluminum heat sink 150mm: ADC12 die-cast aluminium, 0.8 mm fins at 2.0 mm pitch, 0.15 mm over 100 mm flatness, 0.85 K/W thermal resistance. MOQ 200 pcs, ship...
aluminum heat sink 150mm
aluminum heat sink 150mm: ADC12 die-cast aluminium, 0.8 mm fins at 2.0 mm pitch, 0.15 mm over 100 mm flatness, 0.85 K/W thermal resistance. MOQ 200 pcs, ship...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
The aluminum heat sink 150mm in ADC12 die-cast aluminium delivers 0.85 K/W thermal resistance with 0.8 mm fins at 2.0 mm pitch and a 1.0 mm base flat to 0.15 mm over 100 mm. A single 25 T stroke forms each part in an 8 s cycle, holding ±0.03 mm tooling tolerance and ±0.10 mm hole position across an 800,000 pcs line, with weights from 280 g depending on envelope.
Key Takeaway
The aluminum heat sink 150mm in ADC12 die-cast aluminium delivers 0.85 K/W thermal resistance with 0.8 mm fins at 2.0 mm pitch and a 1.0 mm base flat to 0.15 mm over 100 mm. A single 25 T stroke forms each part in an 8 s cycle, holding ±0.03 mm tooling tolerance and ±0.10 mm hole position across an 800,000 pcs line, with weights from 280 g depending on envelope.
Engineered for VFD and inverter, the aluminum heat sink 150mm in ADC12 die-cast aluminium reaches 0.85 K/W thermal resistance. Fins measure 0.8 mm at 2.0 mm pitch; the 1.0 mm base is verified flat to 0.15 mm over 100 mm before dispatch.
Design Approach and Process
A single 25 T stroke forms the whole aluminum heat sink 150mm, so part cost stops scaling with complexity. Tooling runs ±0.03 mm, and the 8 s cycle feeds a 800,000 pcs line.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between ADC12 die-cast aluminium and the airflow except the stamped surface itself.
Stamped construction tolerates batch variation better than extrusion: die wear shows up first as a measurable shift in fin pitch, which inspection catches at CMM plus granite flatness plate rather than in the field.
Pressing ADC12 die-cast aluminium keeps the aluminum heat sink 150mm light, from 280 g depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
Every stroke is dimensionally identical, so ±0.10 mm hole position carries across the batch. That is what makes VFD and inverter volume programs repeatable.
Material Selection and Surface Finish
The standard material is ADC12 die-cast aluminium, supplied with clear anodize Type II, 5-10 µm. For applications where VFD and inverter exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
Tolerance Classes You Can Specify
General dimensions run to ±0.20 mm, with critical features such as ±0.03 mm on fin pitch held separately. Formed geometry inherits tooling repeatability of ±0.03 mm, and hole position is held to ±0.10 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Inspection Before Every Shipment
Each batch carries a CMM report from CMM plus granite flatness plate. We record flatness, pitch, base thickness and hole position, and flag anything outside ±0.20 mm before it leaves the line.
Flatness is measured on granite rather than on cast iron, because 0.15 mm over 100 mm at 80 x 60 x 35 mm reads differently on a plate that has not been lapped. Records keep both readings.
We inspect 0.8 mm fin tips for burr and crack after forming, because stamping can split a root without shifting any drawing dimension. Burr limit is set per part.
Final containment is PE bag + honeycomb carton, 15 kg per carton. Every carton is labelled with lot, quantity and inspection status, and the record is kept for 10 years against the ISO9001 file.
Where This Part Is Used
In VFD and inverter, the 0.85 K/W rating determines how much airflow the enclosure still needs. At VFD and inverter junction temperatures, 0.8 mm fins at 2.0 mm pitch keep the delta-T inside the sensor budget.
For VFD and inverter builds, the 0.15 mm over 100 mm mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Designers working on VFD and inverter ask for flatness before they ask for thermal data, because VFD and inverter assembly is automated and a non-flat base stops the line.
For VFD and inverter prototypes, 5 working days covers drawing review and first article. Production lots move to 12 working days once the ±0.03 mm capability is signed off.
Specifications
Parameter
Value / Range
Material
ADC12 die-cast aluminium
Fin thickness
0.8 mm
Fin pitch
2.0 mm
Fin height
15 mm
Base thickness
1.0 mm
Base flatness
0.15 mm over 100 mm
Thermal resistance
0.85 K/W
Thermal test condition
ΔT = 60 K, natural convection
Surface finish
clear anodize Type II, 5-10 µm
Size range
80 x 60 x 35 mm
FAQ: Your Questions Before Ordering
How long does tooling last before replacement?
On ADC12 die-cast aluminium at normal press tonnage, expect a tooling life of roughly . At 800,000 pcs that is 6 to 12 months. We keep spare die sets on site for VFD and inverter programs, which removes the wait if wear shows up in the flatness record.
What are the packing and shipping conditions?
Standard packing is PE bag + honeycomb carton, 15 kg per carton. We quote FOB Guangzhou. Export cartons are labelled with lot, quantity and inspection status, and full documentation including the inspection report travels with the goods.
Do you provide CAD files or a drawing?
We supply a 2D drawing with the CMM report, and 3D STEP on request. Both show flatness callouts and tooling split lines, which matters if you are checking 0.15 mm over 100 mm in your own assembly.
What quality certifications do you hold?
The plant is ISO9001 certified, and parts ship with RoHS and REACH declarations on request. Third-party SGS inspection can be arranged before the container is sealed, which is what most VFD and inverter buyers specify.
How do you prevent galvanic corrosion?
The key is avoiding a second metal at the wet contact area. We recommend clear anodize Type II, 5-10 µm and, where the part touches an aluminium chassis, an isolating washer. Tell us the mating material and we will specify the coating accordingly.
How We Manufacture and Ship
The line sits in Dongguan in a single ISO9001 plant. 25 T presses cover the aluminum heat sink 150mm family, and 800,000 pcs per month is current committed output.
Our VFD and inverter experience runs back to the first tooling programme in 2015. That history is why the standard clear anodize Type II, 5-10 µm and ±0.20 mm are conservative rather than optimistic.
Production runs on 8 s cycles with in-line vision on 0.15 mm over 100 mm. That is what keeps a 800,000 pcs commitment credible in peak season.
Tooling runs ±0.03 mm and die wear shifts fin pitch measurably
Two-part bonded cooler
Prototypes or low-volume builds
Adhesive layer adds thermal resistance to the path
Extruded heat sink
Simple constant cross-sections
Batch variation from die wear is harder to control than stamped construction
Process / inspection
Stage
Control
Record
Forming
Single 25 T stroke; 8 s cycle
Dimensionally identical stroke output
Tooling
±0.03 mm tooling tolerance
Fin pitch shift from die wear
Flatness
1.0 mm base verified flat to 0.15 mm over 100 mm
Granite flatness plate measurement
Hole position
±0.10 mm across the batch
CMM inspection
Pre-shipment
Inspection before every shipment
CMM plus granite flatness plate results
Frequently Asked Questions
What is the thermal resistance of the aluminum heat sink 150mm?
The aluminum heat sink 150mm in ADC12 die-cast aluminium reaches 0.85 K/W thermal resistance. Fins measure 0.8 mm at 2.0 mm pitch, and the 1.0 mm base is verified flat to 0.15 mm over 100 mm before dispatch, supporting VFD and inverter cooling.
What material is used for the aluminum heat sink 150mm?
The part is pressed from ADC12 die-cast aluminium. This keeps the aluminum heat sink 150mm light, from 280 g depending on envelope, without sacrificing fin density. The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path.
What tolerances can I specify for the aluminum heat sink 150mm?
Tooling runs ±0.03 mm, and ±0.10 mm hole position carries across the batch because every stroke is dimensionally identical. The 1.0 mm base is verified flat to 0.15 mm over 100 mm. Fin pitch shifts from die wear are caught at CMM plus granite flatness plate.
A single 25 T stroke forms the whole aluminum heat sink 150mm, so part cost stops scaling with complexity. The 8 s cycle feeds an 800,000 pcs line. Stamped construction tolerates batch variation better than extrusion, with die wear showing first as a measurable fin pitch shift.
What is the weight of the aluminum heat sink 150mm?
Pressing ADC12 die-cast aluminium keeps the aluminum heat sink 150mm light, from 280 g depending on envelope, without sacrificing fin density. This matters where airflow path length is already fixed by the enclosure, and the one-piece geometry removes the adhesive layer of two-part coolers.
Is the aluminum heat sink 150mm inspected before shipment?
Yes. Inspection before every shipment includes CMM plus granite flatness plate checks. The 1.0 mm base is verified flat to 0.15 mm over 100 mm before dispatch, and fin pitch shifts from die wear are caught as a measurable change rather than in the field.
What applications use the aluminum heat sink 150mm?
It is engineered for VFD and inverter cooling. The 0.85 K/W thermal resistance, 0.8 mm fins at 2.0 mm pitch, and 1.0 mm base flat to 0.15 mm over 100 mm suit enclosures where airflow path length is already fixed and a one-piece thermal path is required.
Key Specifications and Selection Guide
Spec comparison
Parameter
Value / Range
Material
ADC12 die-cast aluminium
Tolerance
±0.03 mm tooling; ±0.10 mm hole position
Lead time
Standard for this process: 15–25 days after tooling approval
MOQ
Standard for this process: 1,000 pcs
Capacity
800,000 pcs line; 8 s cycle; 25 T stroke
Selection / comparison
Option
Best for
Trade-off
ADC12 die-cast aluminium
VFD and inverter cooling with 0.85 K/W
Higher tooling cost than extrusion
Extruded aluminium
Simple constant cross-section profiles
Less tolerance to batch variation; die wear shifts fin pitch
Two-part bonded cooler
Complex geometries needing separate base
Adhesive layer adds thermal resistance
Stamped one-piece construction
Cost stability as complexity increases
Requires 25 T stroke tooling and 8 s cycle control
Frequently Asked Questions
What is the thermal resistance of the aluminum heat sink 150mm?
The aluminum heat sink 150mm in ADC12 die-cast aluminium delivers 0.85 K/W thermal resistance. This is achieved with 0.8 mm fins at 2.0 mm pitch and a 1.0 mm base flat to 0.15 mm over 100 mm, verified before dispatch.
What are the fin dimensions and pitch?
Fins measure 0.8 mm at 2.0 mm pitch. The 1.0 mm base is verified flat to 0.15 mm over 100 mm. These dimensions are held across the 800,000 pcs line using a single 25 T stroke and 8 s cycle.
What tolerances can you hold on the aluminum heat sink 150mm?
Tooling runs ±0.03 mm, and hole position is held to ±0.10 mm. The 1.0 mm base is flat to 0.15 mm over 100 mm. These tolerances are checked with CMM plus granite flatness before every shipment.
What is the production capacity and cycle time?
A single 25 T stroke forms each part in an 8 s cycle. The line capacity is 800,000 pcs. This one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path.
What is the weight of the aluminum heat sink 150mm?
Weights start from 280 g depending on envelope. The ADC12 die-cast aluminium construction and 0.8 mm fins at 2.0 mm pitch keep mass controlled while delivering 0.85 K/W thermal resistance.
How does stamped construction compare to extrusion for this heat sink?
Stamped construction tolerates batch variation better than extrusion. Die wear shows up first as a measurable shift in fin pitch, which inspection catches at CMM plus granite flatness. The one-piece geometry also removes the adhesive layer found in two-part coolers.
Where is the aluminum heat sink 150mm typically used?
It is engineered for VFD and inverter applications. The 0.85 K/W thermal resistance, 0.8 mm fins at 2.0 mm pitch, and 1.0 mm base flat to 0.15 mm over 100 mm suit these cooling duties.