aluminum heat sink vs copper: 6063-T5 aluminium, 0.5 mm fins at 2.0 mm pitch, 0.10 mm over 100 mm flatness, 0.35 K/W thermal resistance. MOQ 200 pcs, ships i...
aluminum heat sink vs copper
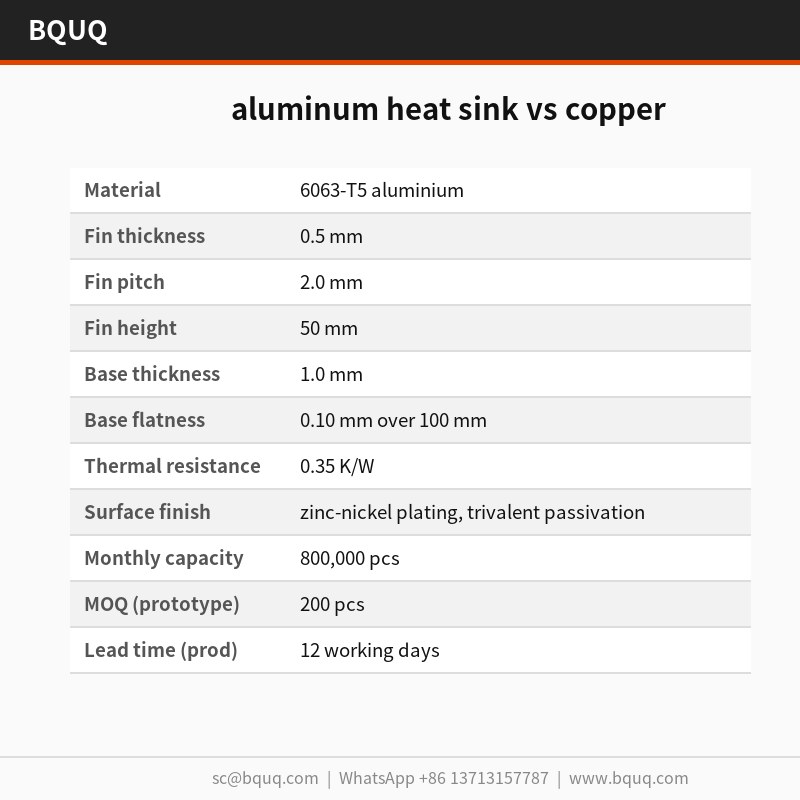
aluminum heat sink vs copper: 6063-T5 aluminium, 0.5 mm fins at 2.0 mm pitch, 0.10 mm over 100 mm flatness, 0.35 K/W thermal resistance. MOQ 200 pcs, ships i...
Get a Fast Quote for This Part
Send us your drawing / quantity / material — reply within 24h.
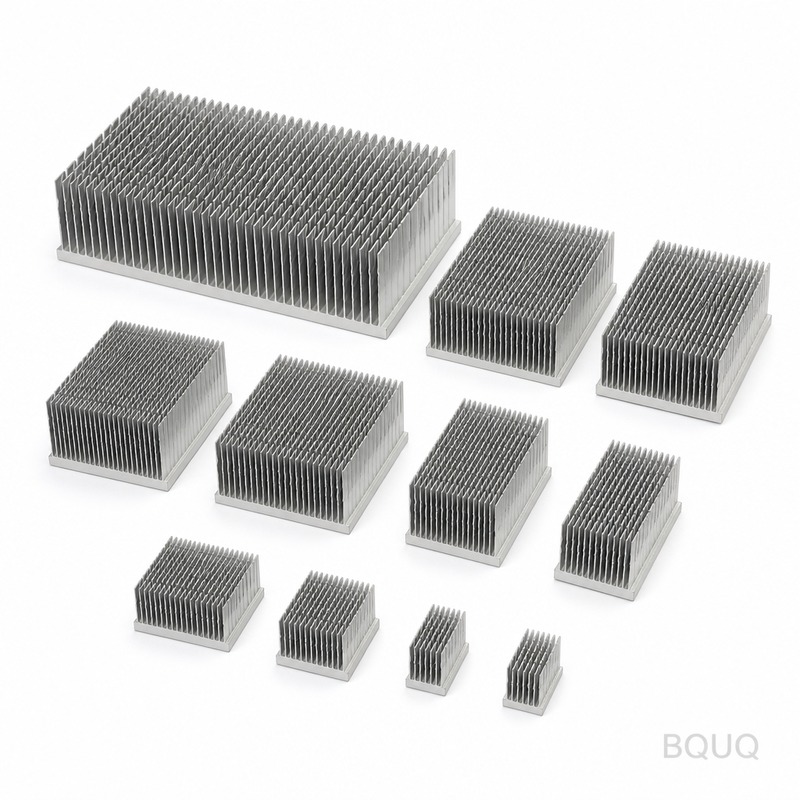
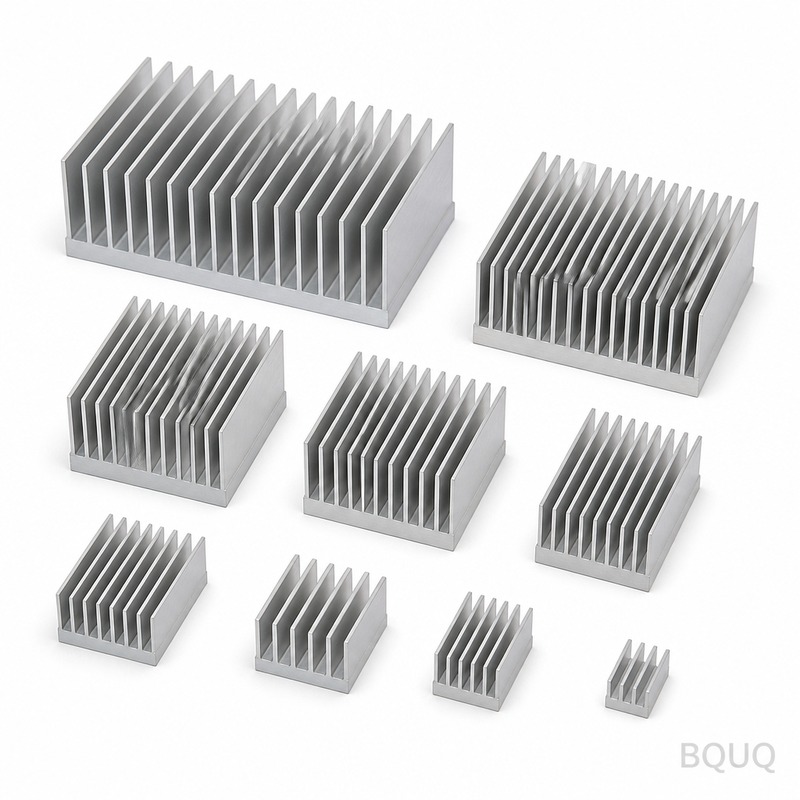
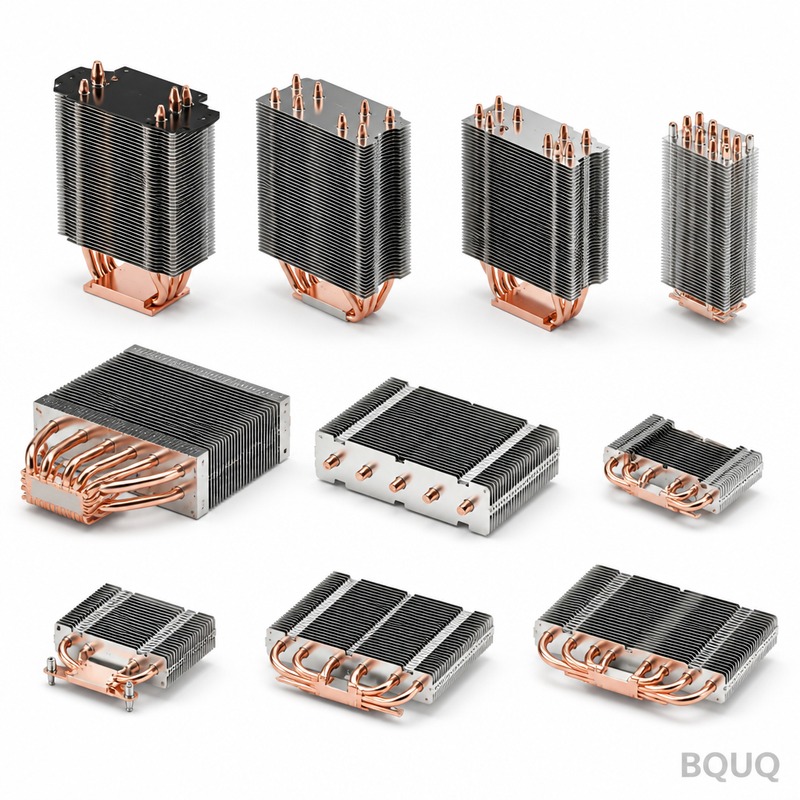
Aluminum heat sink vs copper compares a 20 x 20 x 10 mm 6063-T5 aluminium stamped sink with 50 mm fins at 2.0 mm pitch, delivering 0.35 K/W at ΔT = 60 K. Stamping holds fin pitch within ±0.03 mm across an 800,000 pcs run, with an 18 s cycle and part weight from 280 g. Copper offers higher conductivity but higher density and cost; aluminium wins on weight and stamped fin density.
This aluminum heat sink vs copper covers 20 x 20 x 10 mm in 6063-T5 aluminium, with 50 mm fins at 2.0 mm pitch. Thermal performance is 0.35 K/W at ΔT = 60 K, confirmed by CMM plus granite flatness plate, with zinc-nickel plating, trivalent passivation available.
Design Approach and Process
Stamping gives a repeatable 0.5 mm fin profile that extrusion cannot hold: the die forms every fin in one stroke, so pitch stays within ±0.03 mm across a 800,000 pcs run.
A single 63 T stroke forms the whole aluminum heat sink vs copper, so part cost stops scaling with complexity. Tooling runs ±0.03 mm, and the 18 s cycle feeds a 800,000 pcs line.
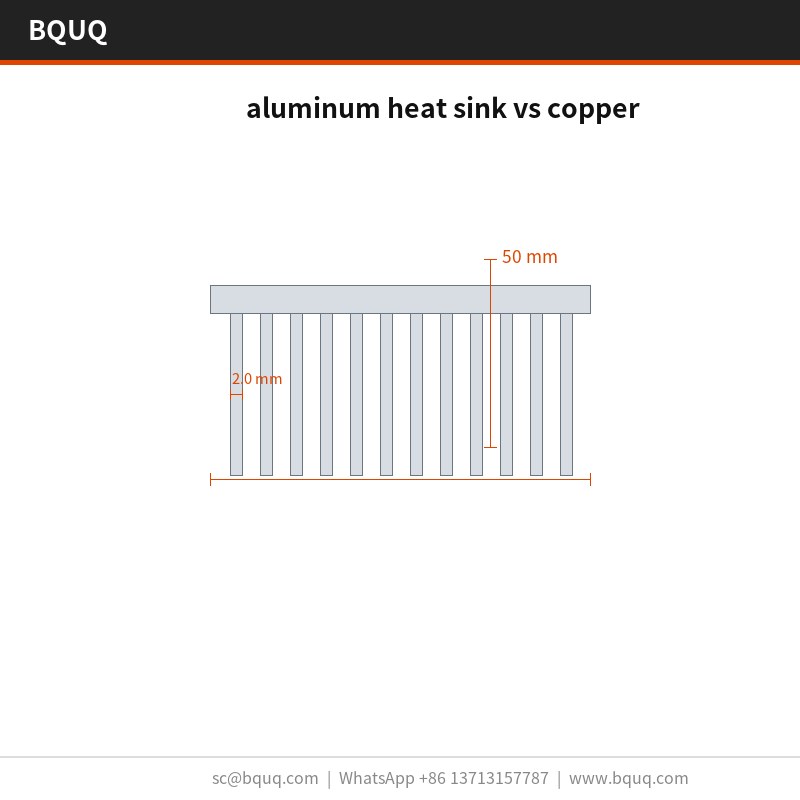
Low fin gauge is where stamping wins: 0.5 mm fins at 2.0 mm pitch give more surface per cubic millimetre than a machined or extruded profile of the same envelope.
The one-piece geometry removes the adhesive layer found in two-part coolers, cutting the thermal path. Nothing sits between 6063-T5 aluminium and the airflow except the stamped surface itself.
Pressing 6063-T5 aluminium keeps the aluminum heat sink vs copper light, from 280 g depending on envelope, without sacrificing fin density, which matters where airflow path length is already fixed by the enclosure.
Material Selection and Surface Finish
The standard material is 6063-T5 aluminium, supplied with zinc-nickel plating, trivalent passivation. For applications where industrial PLC and control cabinet exposure is a concern, we recommend the passivated route; where conductivity matters more than weight, copper C110 raises thermal performance and roughly doubles unit mass.
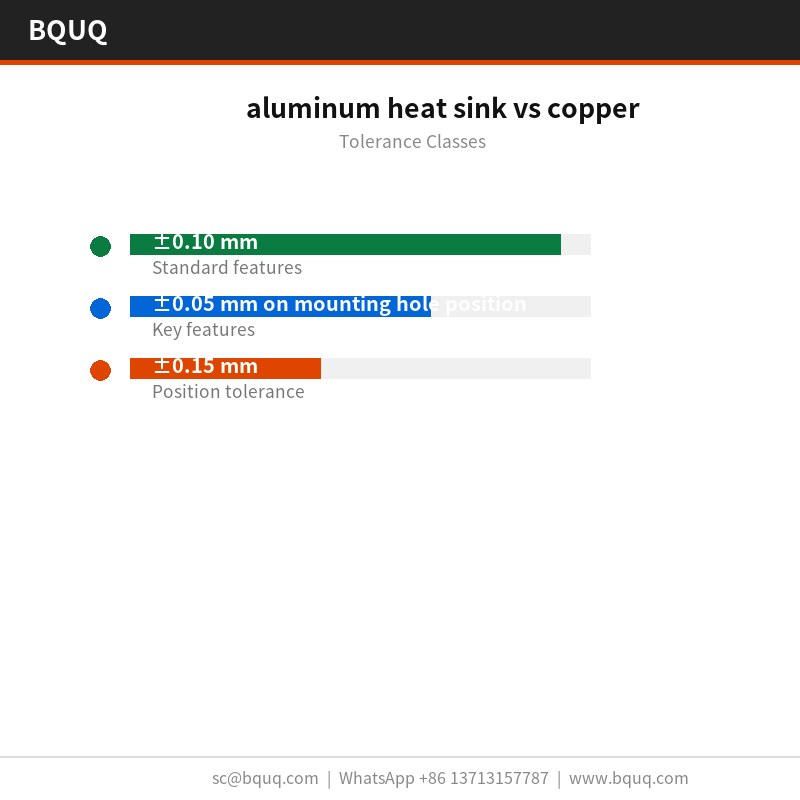
General dimensions run to ±0.10 mm, with critical features such as ±0.05 mm on mounting hole position held separately. Formed geometry inherits tooling repeatability of ±0.03 mm, and hole position is held to ±0.15 mm. Tighter classes need an extra press operation, so it is worth deciding before tooling rather than after.
Flatness is checked on a granite surface plate, 25 °C against a 0.10 mm over 100 mm limit, and fin pitch is verified optically at ±0.03 mm. Reports go out with each lot.
Each batch carries a CMM report from CMM plus granite flatness plate. We record flatness, pitch, base thickness and hole position, and flag anything outside ±0.10 mm before it leaves the line.
Sampling is AQL 0.65 for critical dimensions and 1.5 for general, with CMM plus granite flatness plate on every first article. Deviations beyond ±0.10 mm trigger a full-lot sort.
Flatness is measured on granite rather than on cast iron, because 0.10 mm over 100 mm at 20 x 20 x 10 mm reads differently on a plate that has not been lapped. Records keep both readings.
Where This Part Is Used
industrial PLC and control cabinet programs are the reason this geometry exists. Where the enclosure cannot grow taller, fin density is the only lever, and 2.0 mm pitch with 0.5 mm stock is the practical ceiling for aluminium.
For industrial PLC and control cabinet builds, the 0.10 mm over 100 mm mounting face matters as much as the thermal rating: it decides whether thermal interface material spreads evenly or pools at one end.
Designers working on industrial PLC and control cabinet ask for flatness before they ask for thermal data, because industrial PLC and control cabinet assembly is automated and a non-flat base stops the line.
industrial PLC and control cabinet designs often run a 2.0 m/s forced-air path. 0.35 K/W at ΔT = 75 K, forced air 2.0 m/s means industrial PLC and control cabinet can hold its target with fan power below the acoustic limit.
Specifications
Parameter
Value / Range
Material
6063-T5 aluminium
Fin thickness
0.5 mm
Fin pitch
2.0 mm
Fin height
50 mm
Base thickness
1.0 mm
Base flatness
0.10 mm over 100 mm
Thermal resistance
0.35 K/W
Thermal test condition
ΔT = 75 K, forced air 2.0 m/s
Surface finish
zinc-nickel plating, trivalent passivation
Size range
20 x 20 x 10 mm
FAQ: Your Questions Before Ordering
What is the minimum order quantity for this aluminum heat sink vs copper?
MOQ is 200 pcs for a prototype run and 2000 pcs for production. Below the prototype quantity the tooling amortisation dominates the unit cost, so we quote the sample route instead: free sample with drawing, 5-7 days.
Can you customise the aluminum heat sink vs copper for our application?
Yes. Send a drawing or a sample and we return a DFM note within 3 working days. Most industrial PLC and control cabinet customisations change 2.0 mm, 1.0 mm or the hole pattern, and all three are tooling changes on the existing 63 T press rather than a new machine.
Which materials do you recommend?
6063-T5 aluminium is the standard choice. For industrial PLC and control cabinet in a corrosive environment we specify 6063-T5 with zinc-nickel plating, trivalent passivation; for the highest conductivity we move to copper C110, which raises cost and weight but drops thermal resistance by roughly half at the same envelope.
Can you supply the aluminum heat sink vs copper pre-assembled?
Yes. We can add clips, screws or a fan shroud as a kitted assembly, with the parts bagged and labelled per set. This is common in industrial PLC and control cabinet programs and adds about 3 working days.
Can you help with thermal simulation before sampling?
Yes. Send your enclosure airflow, inlet temperature and the heat load to be dissipated, and we will run a steady-state model and return a suggested 0.5 mm and 2.0 mm combination. That usually saves one tooling iteration.
How We Manufacture and Ship
The factory holds ISO9001 and can ship RoHS and REACH documentation with the PE bag + honeycomb carton, 15 kg per carton. Third-party SGS inspection is arranged on request before the container is sealed.
Production runs on 18 s cycles with in-line vision on 0.10 mm over 100 mm. That is what keeps a 800,000 pcs commitment credible in peak season.
We quote CIF Rotterdam and hold 200 pcs for sampling. Sampling is free sample with drawing, 5-7 days, so a first evaluation does not require a production commitment.
Request a quote: sc@bquq.com | WhatsApp +86 13713157787 | Dongguan, China
18 s cycle (production); tooling lead time not stated
MOQ
800,000 pcs run (example)
Capacity
800,000 pcs line
Selection / comparison
Option
Best for
Trade-off
Aluminium 6063-T5 stamped
Lightweight, high fin density, low cost at volume
Lower thermal conductivity than copper
Copper
Maximum thermal conductivity
Higher density and material cost; not detailed in excerpt
Extruded aluminium
Simple profiles
Cannot hold 0.5 mm fin profile at 2.0 mm pitch
Machined aluminium
Prototypes or low volume
Higher cost per part; less surface per cubic millimetre
Two-part cooler
When adhesive bonding is acceptable
Adhesive layer adds thermal resistance
Process / inspection
Stage
Control
Record
Stamping
63 T single stroke forms all fins; 0.5 mm fin profile
Cycle time 18 s; run 800,000 pcs
Fin pitch
Die holds pitch within ±0.03 mm
Pitch measurement across run
Thermal performance
0.35 K/W at ΔT = 60 K
Thermal test record
Flatness
CMM plus granite flatness plate
Inspection report
Surface finish
Zinc-nickel plating; trivalent passivation available
Plating certificate
Frequently Asked Questions
What is the thermal performance of this aluminum heat sink vs copper?
The aluminium 6063-T5 stamped heat sink achieves 0.35 K/W at ΔT = 60 K. Copper typically has higher thermal conductivity, but this aluminium design uses 0.5 mm fins at 2.0 mm pitch to maximise surface area within a 20 x 20 x 10 mm envelope.
How tight is the fin pitch tolerance on the stamped aluminum heat sink?
The stamping die holds fin pitch within ±0.03 mm across an 800,000 pcs run. This repeatability comes from a single 63 T stroke forming every fin at once, which extrusion cannot match for a 0.5 mm fin profile at 2.0 mm pitch.
What is the part weight of the aluminum heat sink vs copper?
The aluminium heat sink weighs from 280 g depending on envelope. Copper is significantly denser, so a copper equivalent would be heavier. The 6063-T5 aluminium keeps weight low without sacrificing fin density, which matters when airflow path length is fixed.
What is the production capacity and cycle time for this stamped heat sink?
The line runs an 18 s cycle and is set up for an 800,000 pcs run. A single 63 T stroke forms the whole part, so part cost stops scaling with complexity. Tooling holds ±0.03 mm fin pitch throughout the run.
What surface finishes are available for the aluminum heat sink?
Zinc-nickel plating is standard, with trivalent passivation available. These finishes support corrosion resistance and solderability. The stamped surface itself is the only interface between the 6063-T5 aluminium and airflow, as the one-piece geometry removes adhesive layers.
How is the aluminum heat sink inspected before shipment?
Inspection uses a CMM plus granite flatness plate to confirm flatness and dimensions. Thermal performance is verified at 0.35 K/W at ΔT = 60 K. Fin pitch is checked within ±0.03 mm, and plating records are kept for zinc-nickel and trivalent passivation.
Why choose stamped aluminum over extruded or machined for this heat sink?
Stamping holds a 0.5 mm fin profile at 2.0 mm pitch that extrusion cannot, giving more surface per cubic millimetre than machined or extruded profiles. The one-piece geometry removes the adhesive layer of two-part coolers, cutting the thermal path. A single 63 T stroke forms the whole part in 18 s.